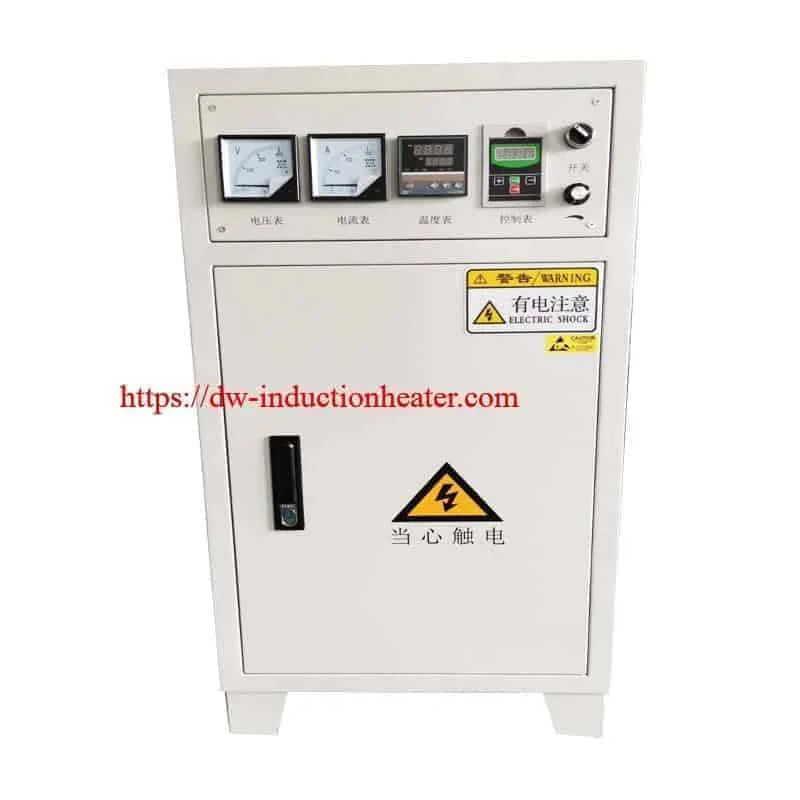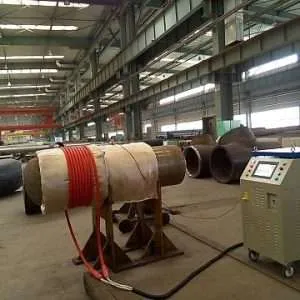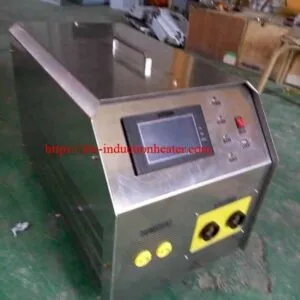


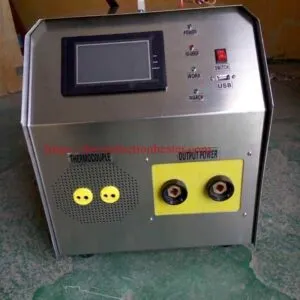
Portable Air Cooling Induction System
Portable Air Cooled Induction Heating System for Welding and Pipe Preheating
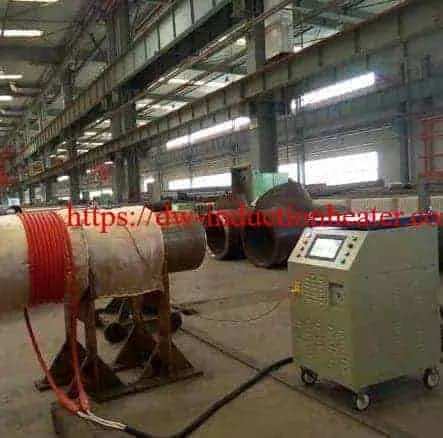
The HLQ Portable Air Cooled Induction Heating System is a compact industrial heating solution designed for localized metal heating, weld preheating, pipe joint heating and selected field maintenance applications.
Available in MYD-10KW and MYD-20KW configurations, the system combines a portable induction power generator, air-cooling technology, flexible induction heating cables and built-in temperature monitoring.
The MYD-10KW provides a published nominal output range of 1–10 kW, while the MYD-20KW offers 1–20 kW. Both models operate within a published frequency range of 5–30 kHz.
Unlike industrial induction heating installations that require a separate external water-chilling system, the portable MYD equipment uses air cooling for the power unit. The exact cooling configuration and allowable operating duty must be confirmed for the selected generator and induction cable.
Typical applications include carbon steel pipe preheating, weld joint heating, localized fabrication heating and suitable industrial repair operations.

Quick Answer
What is a portable air-cooled induction heating system?
A portable air-cooled induction heating system is an electrically powered metal heating machine that uses high-frequency electromagnetic induction to generate heat inside conductive materials while using air cooling to remove heat from designated generator components.
The HLQ MYD-10KW and MYD-20KW models have nominal maximum output ratings of 10 kW and 20 kW, respectively, with a published output frequency range of 5–30 kHz.
The published equipment weights are 26 kg for MYD-10KW and 32 kg for MYD-20KW. Both models use a listed three-phase 380 V, 50/60 Hz input supply and support K-type thermocouple temperature monitoring.
Main applications: Industrial weld preheating, steel pipe joint heating, localized metal heating, welding maintenance and selected postheating operations.
Important distinction: Air cooling refers to the equipment cooling method. The actual continuous output capacity, ventilation requirements and heating cable operating limits depend on the equipment configuration.
| Quick Specification | MYD-10KW | MYD-20KW |
|---|---|---|
| Nominal Maximum Output | 10 kW | 20 kW |
| Output Frequency | 5–30 kHz | 5–30 kHz |
| Input Voltage | 3 × 380 V | 3 × 380 V |
| Generator Cooling | Air-cooled configuration | Air-cooled configuration |
| Published Machine Weight | 26 kg | 32 kg |
| Temperature Monitoring | K-type thermocouple | K-type thermocouple |
Table of Contents
- What Is a Portable Air-Cooled Induction Heating System?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages and Limitations
- Why Choose HLQ?
- 10 Core FAQs
What Is a Portable Air-Cooled Induction Heating System?
A portable air-cooled induction heating system is a compact industrial induction heater that converts electrical power into high-frequency alternating current and uses electromagnetic induction to generate heat within conductive metal workpieces.
The generator contains power conversion components, control electronics and a cooling arrangement designed to remove heat produced during electrical operation.
In an air-cooled configuration, airflow removes heat from designated internal components without requiring the same external water-cooling infrastructure used by many larger industrial induction heating installations.
The induction power output is connected to a compatible heating cable or coil. When alternating current flows through the coil, a changing magnetic field is produced around the workpiece.
This magnetic field induces electrical currents inside the conductive metal, generating heat through electrical resistance.
The workpiece temperature is monitored using suitable temperature sensors, allowing the operator to control or supervise the heating process.
Main Components of an Air-Cooled Induction Heating System
| Component | Main Function | Engineering Consideration |
|---|---|---|
| Induction Power Generator | Converts industrial electrical input into high-frequency output. | Power rating, frequency and operating duty. |
| Power Electronic Module | Controls high-frequency power conversion. | Electrical loading and heat dissipation. |
| Air-Cooling System | Removes heat from designated generator components. | Airflow, ambient temperature and ventilation clearance. |
| Control Panel | Provides the operator interface. | Available settings and control functions. |
| Flexible Induction Cable | Produces the alternating magnetic field. | Cable length, operating frequency and load matching. |
| K-Type Thermocouple | Measures workpiece temperature. | Direct metal contact and proper positioning. |
| Thermal Insulation Blanket | Reduces heat loss from the metal. | Thickness, temperature rating and coverage. |
| Non-Metallic Fixing Straps | Secure insulation and heating cables. | Mechanical strength and high-temperature insulation. |
Air Cooling Versus Water Cooling
Air cooling and water cooling are both used in industrial induction heating equipment, but they serve different operating requirements.
| Comparison | Air-Cooled Induction System | Water-Cooled Induction System |
|---|---|---|
| Heat Removal | Airflow through designated components. | Liquid circulation through cooling circuits. |
| External Cooling Equipment | May not require a separate chiller in a verified fully air-cooled configuration. | Generally requires suitable cooling-water infrastructure. |
| Installation | Potentially simpler for portable applications. | Requires coolant connections and monitoring. |
| Maintenance | Ventilation, fans and dust management. | Coolant flow, water quality, hoses and heat exchangers. |
| Thermal Capacity | Depends on airflow and equipment design. | Depends on flow rate, temperature and cooling capacity. |
| Operating Duty | Must comply with the manufacturer’s rating. | Must comply with the manufacturer’s rating. |
| Typical Selection | Portable and application-specific heating equipment. | High-power or high-thermal-load applications where required. |
Engineering note: An air-cooled generator does not automatically mean that every heating cable, connection or accessory is air-cooled. The complete system must be assessed as a matched assembly.

Key Applications
1. Welding Preheating
Many steel welding procedures require the base metal to reach a specified minimum temperature before welding begins.
For suitable steels, preheating can reduce weld cooling rates and help manage conditions associated with hydrogen-assisted cracking.
Portable induction heating equipment may be used for localized weld preparation when the required heating zone and temperature are compatible with the generator.
For additional welding-specific applications, see HLQ portable induction welding preheaters.
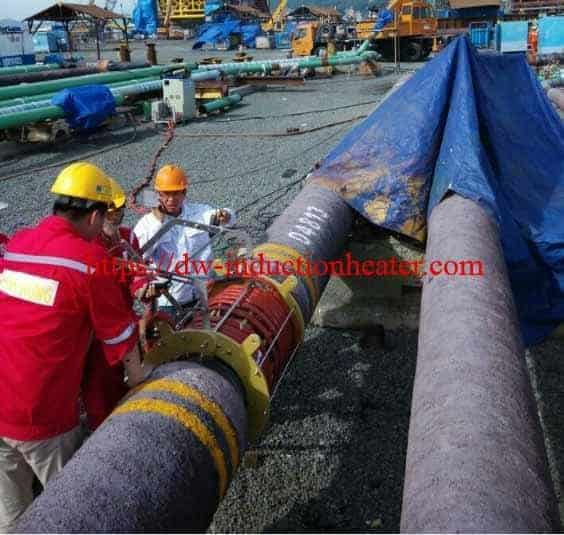
2. Steel Pipe Joint Heating
Steel pipe joints often require controlled heating before welding or repair.
A flexible induction heating cable can be arranged around an insulated pipe section to generate heat in the conductive steel underneath.
The actual heating performance depends on pipe diameter, wall thickness, material composition and heating-zone width.
3. Industrial Pipe Fabrication
Portable air-cooled induction heaters may be used in suitable workshop operations involving fabricated metal pipes, steel fittings and welded assemblies.
Applications should be selected according to available electrical power, component accessibility and operating duty.
4. On-Site Welding Maintenance
Portable induction equipment can be useful at suitable field locations where a compact generator is preferable to a larger stationary heating system.
Before heating an existing installation, assess internal fluids, pressure, combustible materials, coatings, access restrictions and electrical safety.
5. Steel Component Preheating
Selected steel fittings, flanges, plates and other conductive components may require localized preheating during fabrication or maintenance.
Heating cable configuration and electromagnetic coupling must be evaluated for each workpiece shape.
6. Selected Postheating Applications
Some industrial procedures specify heating or temperature holding after welding.
These operations differ from formal post-weld heat treatment, which may require controlled heating and cooling rates, multiple thermocouples and traceable temperature records.
Application Suitability Table
| Application | Heating Objective | Important Selection Factor |
|---|---|---|
| Steel Pipe Welding | Establish the specified preheat temperature. | WPS, wall thickness and heating-zone width. |
| Industrial Weld Repair | Provide localized heating for an approved repair. | Material, temperature and site safety. |
| Structural Steel Fabrication | Prepare selected metal regions before welding. | Steel grade and component geometry. |
| Steel Pipe Joint Heating | Heat the required pipe circumference. | Pipe diameter and heating cable arrangement. |
| Localized Postheating | Maintain a prescribed temperature after welding. | Required holding duration and operating duty. |
| Field Maintenance | Provide portable metal-heating capability. | Electrical supply and environmental conditions. |
Suitable Materials
Electromagnetic induction heating requires an electrically conductive workpiece.
The heating response depends on electrical resistivity, magnetic permeability, thermal conductivity, specific heat capacity and component geometry.
Carbon steels are common workpieces for induction welding preheating because they can provide favorable magnetic coupling under suitable conditions.
Material Compatibility
| Material | General Suitability | Engineering Consideration |
|---|---|---|
| Low-Carbon Steel | Generally Suitable | Common welding preheat material. |
| Structural Carbon Steel | Generally Suitable | Follow the applicable welding procedure. |
| Carbon Steel Pipes | Generally Suitable | Wall thickness and heating band determine thermal load. |
| Low-Alloy Steel | Application-Dependent | Grade-specific temperature requirements. |
| Cr-Mo Alloy Steel | Conditional | May require specialized heating procedures. |
| High-Strength Steel | Conditional | Excessive heating may affect material properties. |
| Ferritic Stainless Steel | Requires Evaluation | Magnetic and thermal properties vary by grade. |
| Austenitic Stainless Steel | Requires Evaluation | Different electromagnetic coupling from carbon steel. |
| Cast Iron | Conditional | Thermal stress and cracking sensitivity. |
| Aluminum | Specialized Application | Requires suitable generator and coil matching. |
| Copper | Specialized Application | High thermal conductivity affects heating response. |
| Nonconductive Materials Alone | Not Directly Suitable | Conventional induction heating requires a conductive target. |
Material Properties Affecting Heating Performance
| Property | Effect on Heating |
|---|---|
| Electrical Resistivity | Influences resistive heating within the metal. |
| Magnetic Permeability | Affects magnetic coupling and current penetration. |
| Thermal Conductivity | Determines how heat spreads through the workpiece. |
| Specific Heat Capacity | Determines required thermal energy. |
| Workpiece Thickness | Affects thermal mass and temperature distribution. |
| Material Heat Treatment History | May limit permissible heating temperatures. |
Working Principle
How Does the Portable Air-Cooled Induction Heater Work?
The induction generator receives three-phase AC electrical power and converts it into high-frequency electrical energy.
This energy is transferred through a compatible induction heating cable or coil.
The alternating current in the coil produces a changing magnetic field around the conductive workpiece.
Electrical currents are induced within the metal. These currents generate heat through electrical resistance.
The generated heat spreads through the workpiece by thermal conduction.
Temperature sensors monitor selected locations, allowing the heating operation to be supervised or controlled according to the available equipment functions.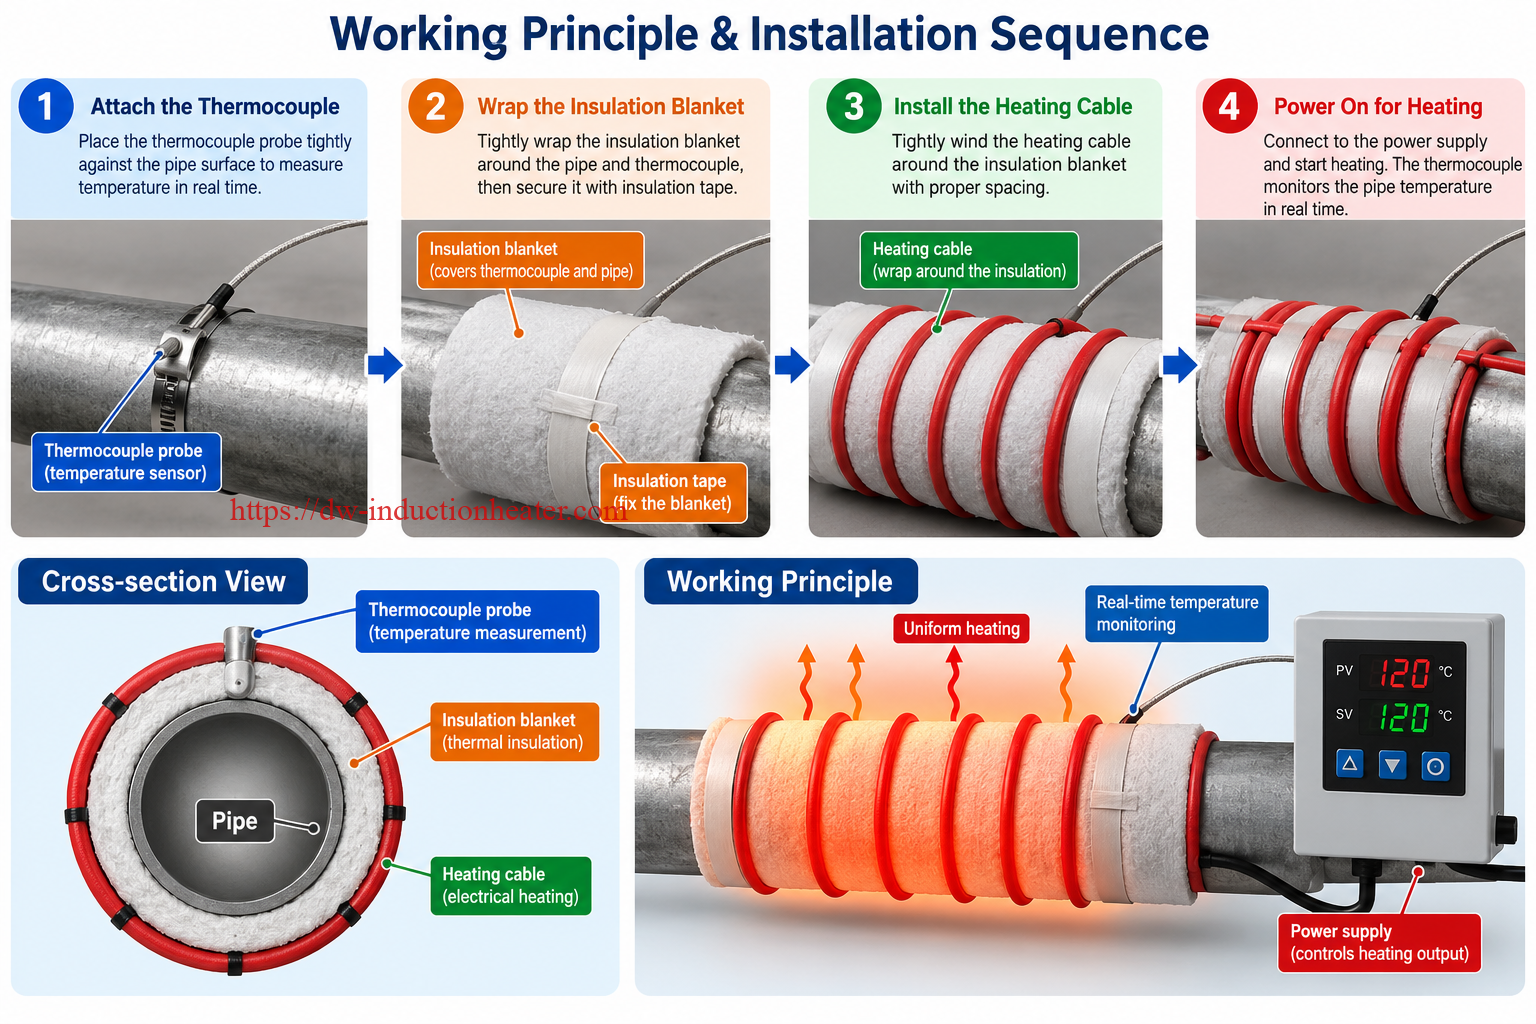
Energy Conversion Process
| Stage | Process | Result |
|---|---|---|
| 1 | Three-Phase AC Input | Electrical power enters the generator. |
| 2 | High-Frequency Conversion | Induction power is generated. |
| 3 | Coil Energization | An alternating magnetic field is produced. |
| 4 | Eddy Current Generation | Electrical currents develop within the conductive metal. |
| 5 | Resistive Heating | Electrical energy is converted into thermal energy. |
| 6 | Thermal Conduction | Heat spreads through the workpiece. |
| 7 | Temperature Measurement | Thermocouples measure selected workpiece temperatures. |
| 8 | Air Cooling | Airflow removes heat from designated generator components. |
How Does Air Cooling Protect the Generator?
During operation, internal power electronic components generate heat because electrical conversion is not perfectly efficient.
An appropriately designed air-cooling system moves air through designated cooling passages and heat-dissipation components.
Cooling performance depends on ambient temperature, airflow, component heat losses, ventilation clearance and operating duty.
If airflow becomes restricted by dust, blocked ventilation openings or unsuitable installation conditions, generator temperatures may rise.
For this reason, air-cooled equipment must be installed with the ventilation clearances specified by the manufacturer.
Air-Cooled Generator Operating Factors
| Factor | Possible Effect | Recommended Action |
|---|---|---|
| Ambient Temperature | Affects heat rejection from the generator. | Verify the approved operating range. |
| Airflow | Controls convective cooling. | Keep ventilation passages unobstructed. |
| Dust and Contamination | May obstruct cooling passages. | Inspect and maintain the cooling system. |
| Power Output | Influences internal component losses. | Operate within verified output ratings. |
| Continuous Operating Duty | Determines sustained cooling requirements. | Confirm the allowable full-load duty cycle. |
| Cabinet Installation | Can restrict incoming or outgoing cooling air. | Maintain appropriate clearance around the generator. |
Correct Pipe Heating Installation
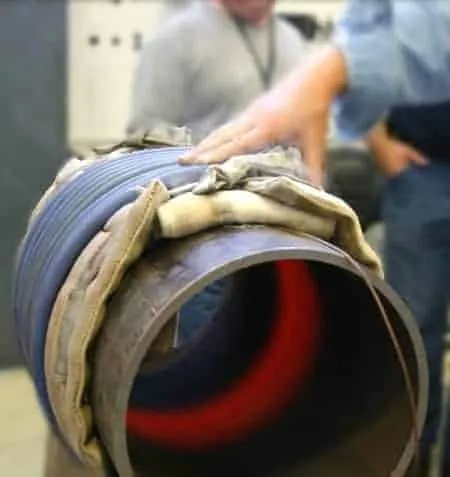
For pipe heating with flexible induction cables, the correct order of temperature sensors, insulation and heating cable installation is essential.
Correct installation sequence:
- Prepare and clean the steel pipe surface.
- Install K-type thermocouples directly against the metal surface at the specified measurement points.
- Wrap the steel pipe and temperature sensors tightly with suitable thermal insulation blankets.
- Secure the insulation blankets using approved non-metallic, high-temperature insulating straps.
- Wind the flexible induction heating cable around the outside of the insulation blankets.
- Secure the heating cable using suitable non-metallic insulating straps or approved fixtures.
- Connect the coil and temperature sensors to the designated equipment terminals.
- Check all electrical connections, temperature readings and cooling conditions before heating.
Correct Installation Layer Structure
| Layer | Component | Function |
|---|---|---|
| 1 – Workpiece | Steel Pipe | Electrically conductive metal heated by induction. |
| 2 – Direct Metal Contact | Temperature Sensors | Measure the pipe surface temperature. |
| 3 – Middle Layer | Thermal Insulation Blanket | Covers sensors and metal while reducing heat loss. |
| 4 – Outer Layer | Flexible Induction Heating Cable | Produces the alternating magnetic field. |
| 5 – Fixing Method | Non-Metallic Insulating Straps | Secure the blanket and cable as specified. |
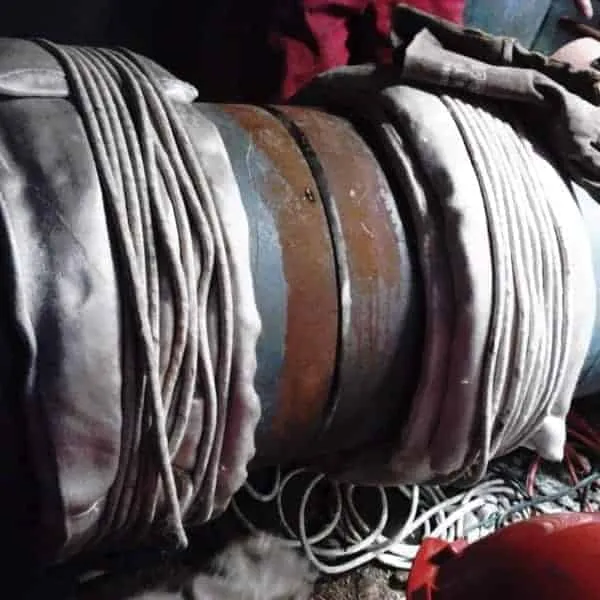
Safety requirement: Do not use unapproved metallic straps, steel wires or conductive bands to secure thermal insulation inside the active induction heating area.
Suitable non-metallic materials may include properly rated fiberglass or ceramic insulating straps.
The thermocouple junctions must remain in reliable contact with the metal beneath the insulation.
For further information about coil selection and installation, see HLQ flexible induction heating cables.
Technical Specifications
The following technical parameters reproduce the original published specifications of the MYD-10KW and MYD-20KW portable air-cooled induction heating systems.
Some historical values require verification because the source does not fully define their testing conditions or operating limitations.
MYD-10KW and MYD-20KW Comparison
| Technical Parameter | MYD-10KW | MYD-20KW |
|---|---|---|
| Nominal Output Power | 1–10 kW | 1–20 kW |
| Input Voltage | 3 × 380 V | 3 × 380 V |
| Input Frequency | 50/60 Hz | 50/60 Hz |
| Published Input Connection | 4 Wires | 4 Wires |
| Published Input Current | 1–15 A | 1–30 A |
| Published Output Current | 0–200 A | 0–300 A |
| Output Frequency | 5–30 kHz | 5–30 kHz |
| Generator Cooling | Air-Cooled | Air-Cooled |
| Temperature Sensor | K-Type | K-Type |
| Temperature System | Built-In | Built-In |
| Published Maximum Heating Temperature | 500°C | 800°C |
| Cabinet Dimensions | 650 × 310 × 410 mm | 700 × 330 × 410 mm |
| Machine Weight | 26 kg | 32 kg |
| Published Heating Cable Length | 10–20 m | 10–20 m |
| Published Heating Cable Diameter | 15 mm | 15 mm |
| Published Ambient Temperature | -30°C to +45°C | -30°C to +45°C |
| Published Pipe Outside Diameter Range | 50–500 mm | 50–500 mm |
Important Technical Clarifications
- The original MYD-10KW specification includes an additional 15 kW / 150% overload statement without a defined overload duration.
- The published three-phase input currents require reconciliation with the stated maximum output power ratings.
- The listed maximum temperatures do not establish the permissible temperature of every workpiece material.
- The published pipe diameter range does not guarantee a particular heating rate or duty capability.
- The ambient temperature range should be confirmed against the current equipment revision.
- The published induction cable length and diameter require confirmation of the supplied configuration.
- Temperature recording functions, sensor channel counts and continuous full-power operation should be verified for the ordered equipment.
Electrical Input Assessment
For a balanced three-phase electrical supply, the apparent input power is:
S = 1.732 × U × I / 1000
Where:
- S = apparent power, kVA.
- U = line-to-line voltage, V.
- I = line current, A.
| Model | Published Maximum Input Current | Calculated Apparent Power at 380 V | Published Maximum Output |
|---|---|---|---|
| MYD-10KW | 15 A | 9.87 kVA | 10 kW |
| MYD-20KW | 30 A | 19.75 kVA | 20 kW |
The calculated apparent input powers are slightly below the respective nominal output ratings.
Since practical electrical power conversion involves losses, the stated input-current and maximum-output values should not be treated as simultaneous verified continuous-duty ratings without further factory confirmation.
Air-Cooled System Accessories
| Accessory | Purpose | Selection Consideration |
|---|---|---|
| Induction Power Generator | High-frequency electrical power supply. | MYD-10KW or MYD-20KW. |
| Induction Heating Cable | Generates the magnetic field. | Electrical compatibility, length and insulation. |
| Thermocouple | Workpiece temperature measurement. | Type, length, calibration and quantity. |
| Thermal Insulation Blanket | Reduces external heat loss. | Temperature rating and thickness. |
| Non-Metallic Straps | Secure insulation and cables. | Electrical insulation and thermal resistance. |
| Connection Accessories | Connect heating and measurement circuits. | Rated compatibility with the generator. |
| Temperature Recorder | Documents heating cycles when equipped. | Number of channels and recording functions. |
| Air-Cooling Components | Support generator heat dissipation. | Airflow and maintenance requirements. |
Accessory quantities and included items should be confirmed for the selected system configuration.
For higher-power equipment and larger industrial configurations, compare HLQ industrial air-cooled induction heating systems.
Recommended Model Selection
Selection between MYD-10KW and MYD-20KW depends on required useful thermal power, workpiece mass, temperature rise, heating time and operating duty.
The nominal generator output alone does not establish a guaranteed heating rate.
MYD-10KW Versus MYD-20KW
| Selection Factor | MYD-10KW | MYD-20KW |
|---|---|---|
| Nominal Maximum Output | 10 kW | 20 kW |
| Weight | 26 kg | 32 kg |
| Equipment Dimensions | More compact | Moderately larger |
| Published Maximum Heating Temperature | 500°C | 800°C |
| Preliminary Application | Relatively small localized heating loads | More demanding localized heating loads |
| Continuous Operating Duty | Requires verification | Requires verification |
| Actual Pipe Heating Capacity | Application-dependent | Application-dependent |
Preliminary Model Recommendations
| Application | Preliminary Selection | Required Verification |
|---|---|---|
| Small Steel Pipe Welding Preheat | MYD-10KW | Wall thickness, temperature and heating time. |
| Localized Steel Fitting Heating | MYD-10KW / MYD-20KW | Metal mass and cable arrangement. |
| Moderate Pipe Joint Heating | MYD-20KW | Heating-zone width and useful thermal power. |
| Industrial Weld Repair | Application-Dependent | Repair procedure and worksite conditions. |
| Localized Postheating | Application-Dependent | Temperature, duration and generator duty. |
| Large Thick-Wall Pipe Heating | Higher-Power System Evaluation | Full thermal load and operating requirements. |
| Formal PWHT | Special Engineering Review | Qualified thermal cycle and temperature records. |
For larger pipe diameters, wider heating bands and higher thermal loads, see HLQ induction pipeline preheating machines.
Selection Data Checklist
| Required Information | Why It Matters |
|---|---|
| Metal Grade | Determines thermal and electromagnetic properties. |
| Outside Diameter | Influences coil length and heating geometry. |
| Wall Thickness | Determines heated metal mass. |
| Heating Band Width | Determines the selected heated region. |
| Initial Temperature | Determines the required temperature rise. |
| Target Temperature | Determines the sensible heat requirement. |
| Required Heating Time | Determines useful heating power demand. |
| Operating Duration | Determines continuous-duty requirements. |
| Ambient Conditions | Affect generator cooling and external heat loss. |
| Electrical Supply | Determines power installation compatibility. |
Process Workflow
The following workflow describes a typical insulated steel-pipe heating arrangement using a portable air-cooled induction generator.
Step 1: Confirm the Heating Requirements
Identify the material grade, outside diameter, wall thickness, heating-zone width and required target temperature.
Review any applicable welding procedure or thermal treatment requirements.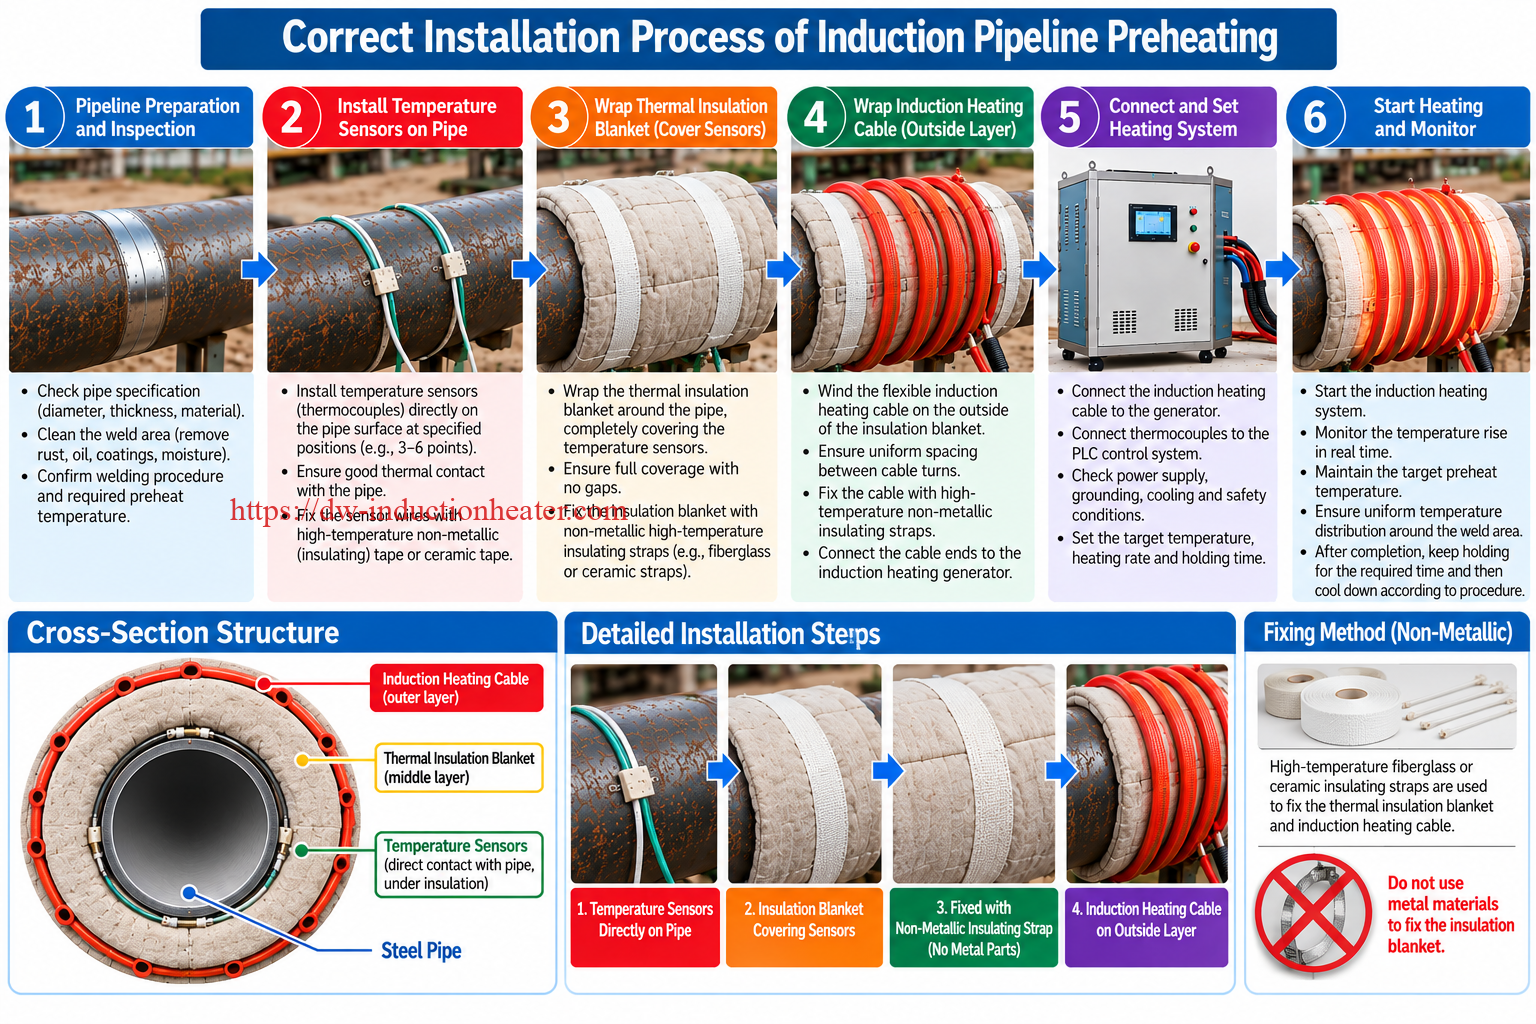
Step 2: Prepare the Steel Pipe
Inspect the workpiece and clean the areas where temperature sensors will be attached.
Confirm that the work area is suitable for safe heating.
Step 3: Install Temperature Sensors Directly on the Pipe
Attach K-type thermocouples directly against the steel surface at the specified measurement locations.
Use an approved attachment method to ensure reliable thermal contact.
Step 4: Wrap Thermal Insulation Blankets
Cover the pipe and temperature sensors tightly with suitable thermal insulation blankets.
Ensure the required heating area is covered without unwanted gaps.
Step 5: Secure the Blankets with Non-Metallic Straps
Use high-temperature, electrically insulating fixing straps suitable for the operating conditions.
Do not use unapproved metallic bands, steel wire or other conductive fixing materials in the active heating zone.
Step 6: Install the Induction Heating Cable
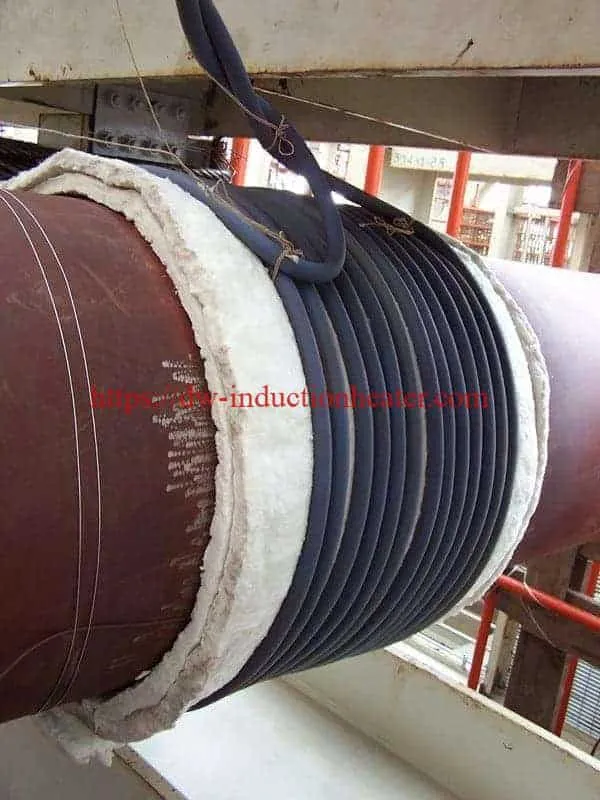
Wind the flexible induction heating cable around the outside of the insulation blanket.
Maintain the approved cable spacing and number of turns.
Step 7: Connect the Generator and Sensors
Connect the heating cable to the generator output and connect the thermocouple leads to their designated measurement terminals.
Step 8: Inspect the Air-Cooling System
Check the generator ventilation openings and confirm that the cooling arrangement is suitable for the planned operating conditions.
Verify the electrical supply and other relevant safety requirements before energizing the system.
Step 9: Start Heating and Monitor Temperature
Apply the approved heating settings and monitor the actual workpiece temperature.
Adjust the heating process according to the specified temperature requirements and available control functions.
Step 10: Complete the Process
Maintain the required temperature for the specified duration, then follow the approved cooling and inspection procedure.
Installation Inspection Table
| Inspection Point | Correct Condition |
|---|---|
| Temperature Sensors | Directly contacting the steel pipe. |
| Thermal Insulation | Fully covering the required region and sensors. |
| Insulation Fixing | Suitable non-metallic insulating straps. |
| Induction Cable | Installed outside the insulation. |
| Cable Fixing | Approved insulated securing arrangement. |
| Electrical Connections | Correct and secure. |
| Cooling Airflow | Ventilation passages unobstructed. |
| Control System | Correct temperature readings and operating settings. |
Common Problems and Solutions
The performance of an air-cooled induction heating system depends on electrical loading, ventilation, coil matching, material properties and correct installation.
Troubleshooting Table
| Problem | Possible Cause | Recommended Solution |
|---|---|---|
| Generator Overheating | Restricted ventilation or excessive operating duty. | Stop operation and check airflow and permitted duty. |
| Frequent Thermal Protection | High ambient temperature or excessive internal loading. | Check ventilation, load and rated conditions. |
| Slow Workpiece Heating | Insufficient useful power or large thermal mass. | Recalculate heating requirements and verify matching. |
| Uneven Pipe Temperature | Nonuniform cable placement or heat losses. | Inspect cable spacing and insulation coverage. |
| Incorrect Temperature Reading | Thermocouple not contacting metal correctly. | Reinstall the sensor directly against the workpiece. |
| Temperature Overshoot | Excessive heating rate or delayed feedback. | Review available control settings and sensor response. |
| Heating Cable Overheating | Incorrect configuration or operating load. | Stop heating and inspect the approved coil arrangement. |
| Abnormal Heating of Fasteners | Metallic fixing materials near the active induction coil. | Remove unapproved metal components and use suitable insulating fixtures. |
| Unstable Heating Performance | Electrical matching or connection problems. | Inspect the induction output system using approved procedures. |
| Insufficient Holding Temperature | Heat losses exceed available useful heating power. | Review thermal insulation and generator capacity. |
Air-Cooling Maintenance Checklist
| Inspection Item | Recommended Check | Purpose |
|---|---|---|
| Ventilation Openings | Inspect for obstruction. | Maintain cooling airflow. |
| Cooling Fan | Verify operation according to equipment instructions. | Prevent inadequate cooling. |
| Dust Accumulation | Inspect and clean using approved maintenance methods. | Reduce airflow restrictions. |
| Induction Cable | Inspect insulation and connections. | Maintain safe heating performance. |
| Thermocouples | Check condition, placement and calibration. | Maintain reliable temperature measurement. |
| Thermal Insulation | Inspect for damage and contamination. | Maintain suitable thermal protection. |
| Non-Metallic Straps | Inspect for damage or degradation. | Maintain secure insulated installation. |
Air-Cooled Heating Versus Postheating
The cooling method of the generator and the thermal process performed on the workpiece are different concepts.
An air-cooled induction heater may be considered for suitable preheating or postheating applications, but the required temperature cycle determines whether the equipment can perform the process.
For post-weld applications, review HLQ portable induction postheating systems.
Engineering Selection Guide
Engineering selection should begin with the required thermal energy rather than the nominal power rating alone.
1. Calculate the Heated Pipe Mass
For a cylindrical steel pipe with a defined axial heating band:
m = π × (D − t) × t × L × ρ
Where:
- m = heated metal mass, kg.
- D = pipe outside diameter, m.
- t = wall thickness, m.
- L = axial heating band length, m.
- ρ = metal density, kg/m³.
2. Calculate the Required Sensible Heat
Q = m × Cp × ΔT
Where:
- Q = required sensible heat, kJ.
- m = metal mass, kg.
- Cp = average specific heat capacity, kJ/(kg·K).
- ΔT = required temperature rise, K.
3. Engineering Calculation Example
Consider a hypothetical carbon steel pipe preheating application with the following dimensions and thermal conditions.
| Input Parameter | Value |
|---|---|
| Pipe Outside Diameter | 168.3 mm |
| Wall Thickness | 7.11 mm |
| Axial Heating Band Width | 250 mm |
| Initial Temperature | 25°C |
| Target Temperature | 150°C |
| Temperature Rise | 125 K |
| Assumed Steel Density | 7,850 kg/m³ |
| Assumed Average Specific Heat | 0.49 kJ/(kg·K) |
4. Calculate the Metal Mass
m = π × (0.1683 − 0.00711) × 0.00711 × 0.250 × 7850
Calculated heated mass ≈ 7.07 kg
5. Calculate the Thermal Energy
Q = 7.07 × 0.49 × 125
Q ≈ 433 kJ
In kilowatt-hours:
Q ≈ 0.120 kWh
This represents the approximate sensible heat needed for the selected pipe band under the stated assumptions.
It does not represent the actual electrical energy consumed by the induction generator.
6. Calculate the Idealized Heating Time
For an assumed average useful thermal power:
Heating Time (seconds) = Thermal Energy (kJ) / Useful Thermal Power (kW)
| Hypothetical Useful Thermal Power | Idealized Heating Time |
|---|---|
| 1.5 kW | 289 seconds |
| 2.0 kW | 217 seconds |
| 3.0 kW | 144 seconds |
| 4.0 kW | 108 seconds |
| 5.0 kW | 87 seconds |
| 6.0 kW | 72 seconds |
Engineering clarification: These assumed useful thermal power values are illustrative and are not measured MYD-10KW or MYD-20KW output values.
Actual heating time depends on magnetic coupling, workpiece properties, thermal conduction into adjacent metal, external heat losses, cable configuration and generator operating limits.
7. Factors Affecting Generator Sizing
| Engineering Factor | Effect on Required Heating Capacity |
|---|---|
| Pipe Outside Diameter | Affects heating circumference and coil length. |
| Wall Thickness | Determines approximate metal mass. |
| Heating Band Width | Determines the selected heated volume. |
| Target Temperature | Determines required temperature rise. |
| Heating Time | Determines required average useful power. |
| Thermal Insulation | Influences external heat loss. |
| Ambient Temperature | Affects both generator cooling and workpiece heat losses. |
| Coil Configuration | Affects electromagnetic coupling and electrical matching. |
| Continuous-Duty Requirement | Determines sustained output and cooling requirements. |
8. Portable Air Cooling and Operating Duty
For continuous industrial operation, the required equipment rating must consider both the workpiece heating demand and the generator’s capacity to reject internal heat.
A nominal 20 kW output rating does not automatically establish continuous 20 kW operation at every ambient temperature.
Actual operation must remain within the manufacturer’s verified temperature, ventilation and duty-cycle limits.
9. Preheating Versus PWHT
| Process | Main Purpose | Required Control |
|---|---|---|
| Weld Preheating | Establish the specified temperature before welding. | Qualified minimum preheat temperature. |
| Interpass Temperature Control | Manage the weld area temperature between passes. | Permitted minimum and maximum temperatures. |
| Localized Postheating | Apply a prescribed temperature after welding. | Holding temperature and duration. |
| Post-Weld Heat Treatment | Apply a qualified post-weld thermal cycle. | Heating rate, soaking temperature, holding period, cooling rate and required records. |
For applications requiring formal thermal-cycle control and recording, review dedicated induction PWHT equipment.
Advantages and Limitations
Advantages of Portable Air-Cooled Induction Heating
1. Compact Generator Construction
Published machine weights of 26 kg and 32 kg make the MYD portable configurations manageable for relocation between suitable industrial workstations.
2. Air-Cooled Generator Design
Air cooling can reduce reliance on external water-cooling infrastructure when a verified fully air-cooled system configuration is appropriate.
3. Localized Electromagnetic Heating
Heat is generated within conductive metal components rather than transferred solely from an external flame.
4. Flexible Induction Cable Arrangement
Flexible heating cables can be configured around suitable pipes and other accessible metal workpieces.
5. Temperature Monitoring
The published equipment includes K-type thermocouple temperature-monitoring capability.
6. Suitable for Selected Field Applications
Portable equipment can be useful for localized industrial heating where suitable electrical power and operating conditions are available.
7. No Combustion Flame Required
Induction heating does not require an open gas flame as the primary heat source.
Electrical hazards, hot metal surfaces and combustible surrounding materials still require appropriate controls.
Technical Limitations
| Limitation | Engineering Explanation | Recommended Response |
|---|---|---|
| Air-Cooling Capacity | Heat rejection depends on airflow and ambient temperature. | Verify cooling and operating-duty limits. |
| Nominal Power | Generator rating does not equal useful heat absorbed by the workpiece. | Calculate thermal demand and verify performance. |
| Material Compatibility | Different metals have different electromagnetic properties. | Confirm suitability for the actual material. |
| High Ambient Temperature | Reduced temperature difference can affect cooling. | Confirm operating conditions and ventilation. |
| Dusty Environments | Dust can obstruct cooling passages. | Inspect and maintain the air-cooling system. |
| Temperature Accuracy | Incorrect sensor installation can affect readings. | Use direct metal contact and proper calibration. |
| Continuous Operation | Full-load duty capability is not fully defined by the historical source. | Confirm current factory test specifications. |
| Large Thermal Loads | 10–20 kW may be insufficient for demanding workpieces. | Consider higher-power systems. |
Induction Heating Versus Flame and Resistance Heating
| Comparison | Induction Heating | Flame Heating | Resistance Heating |
|---|---|---|---|
| Heat Generation | Within conductive metal. | Combustion outside the workpiece. | Electrical resistance elements. |
| Open Flame | No. | Yes. | No. |
| Heating Distribution | Depends on coil arrangement. | Depends on burner placement. | Depends on heating element arrangement. |
| Temperature Monitoring | Can use direct-contact thermocouples. | Requires suitable measurement. | Can use thermocouples. |
| Primary Technical Limitation | Electrical matching and electromagnetic coupling. | Combustion and heat-transfer control. | Element placement and heat transfer. |
| Energy Efficiency | Application-dependent. | Application-dependent. | Application-dependent. |
Claims about heating speed, energy savings or temperature uniformity should be supported by comparable tests performed on equivalent workpieces under equivalent conditions.

Why Choose HLQ?
HLQ Induction Equipment Co., Ltd. supplies induction heating equipment for welding preparation, industrial metal heating, heat treatment and related manufacturing applications.
Portable Induction Heating Configurations
The MYD-10KW and MYD-20KW provide compact nominal 10 kW and 20 kW configurations for suitable localized heating requirements.
Air-Cooled Generator Technology
Air-cooled generator construction can simplify cooling infrastructure where the selected power rating, duty cycle and ambient conditions permit this configuration.
Flexible Heating Cable Applications
Compatible flexible induction heating cables allow heating arrangements to be adapted to suitable steel pipes and metal-component geometries.
Temperature Monitoring
The published portable systems include K-type thermocouple temperature-monitoring functionality.
Application-Specific Engineering Selection
Equipment suitability should be evaluated using material properties, heated metal mass, operating temperature, heating time, electrical input and cooling requirements.
Industrial Heating Application Coverage
HLQ induction heating products cover localized weld preheating, pipe heating, selected postheating operations and other industrial thermal applications.
Final specifications and process capability should be confirmed against the current equipment configuration and representative application testing.
10 Core FAQs
1. What is a portable air-cooled induction heating system?
It is a compact induction heater that uses high-frequency electromagnetic induction to generate heat inside conductive metal while employing air cooling for designated generator components. It is suitable for selected weld preheating, pipe heating and industrial maintenance applications.
2. What is the difference between MYD-10KW and MYD-20KW?
MYD-10KW has a published nominal output range of 1–10 kW and weighs 26 kg. MYD-20KW has a published output range of 1–20 kW and weighs 32 kg. Actual application suitability depends on heating load and verified continuous-duty performance.
3. Does an air-cooled induction heater require a water chiller?
A verified fully air-cooled configuration may operate without an external industrial water chiller. However, the cooling requirements of the complete generator, heating cable and accessories must be checked for the ordered system.
4. What is the operating frequency of the MYD portable series?
The original published output frequency range is 5–30 kHz. Actual operation depends on the generator configuration, induction cable and connected load.
5. Can the equipment heat carbon steel pipes?
Yes, when the generator and heating cable are suitable for the pipe geometry and required thermal cycle. Wall thickness, heating-zone width and target temperature must be evaluated before equipment selection.
6. Where should temperature sensors be installed?
K-type thermocouples should contact the metal pipe directly at the specified measurement positions. Thermal insulation blankets must cover the pipe and sensors, while the induction heating cable is installed outside the insulation.
7. Can metal straps be used to secure thermal insulation blankets?
Unapproved metallic fixing bands and steel wire should not be used in the active induction heating region. Suitable non-metallic, high-temperature insulating straps should be selected according to the installation requirements.
8. What pipe diameters can the portable MYD models heat?
The original product page publishes a pipe outside-diameter range of 50–500 mm. This is not a guaranteed processing capacity. Actual suitability depends on wall thickness, target temperature, heating time, insulation and available useful heating power.
9. Can the MYD-20KW operate continuously at 20 kW?
The historical source does not provide sufficient information to verify continuous full-power operation. The permissible output, duty cycle and cooling conditions must be confirmed against current factory test data.
10. How do I select a portable air-cooled induction heater?
Identify the material grade, dimensions, initial temperature, target temperature, heating time, operating duration, ambient conditions and available electrical supply. Estimate the thermal load and verify the generator, heating cable and cooling performance before selecting the final model.
HLQ-Portable-Induction-Preheat-Welding-System-Brochure
Related products
-

80KW Electromagnetic Induction Heater
-
Induction PWHT System for Oil & Gas Pipeline Welding Projects
-
Induction Post Weld Heating Treatment Machine
-
Plastic Injection Molding Machine Electromagnetic Induction Heater 30KW
-
Induction thermal for the expansion and removal of large bearings, shafts and couplings for turbines and generators