
Case Study: Removing 3mm Epoxy Coating from Steel Using a 30kW RPR Induction Heater
Case Study Quick Answer: In this representative engineering case, a 3 mm thick industrial epoxy coating bonded to a 10 mm carbon-steel plate was removed using a 30 kW RPR induction heater. The optimized process used approximately 75–80% generator output, controlled scanning at about 0.6–0.7 m/min, and a target steel/coating interface temperature window of approximately 200–230°C. Under the modeled working conditions, the practical net removal rate was approximately 3.5–4.0 m²/h, with most of the epoxy separating in large sheets rather than being pulverized.
Removing a 3 mm industrial epoxy coating from carbon steel can be surprisingly difficult. The coating is thick enough to make grinding slow, yet strongly bonded enough that conventional scraping alone is ineffective.
This case study examines a different strategy: using a 30kW RPR induction heater to generate controlled heat inside the steel substrate and weaken the epoxy-to-steel bond from underneath.
The purpose of the test was not simply to determine whether induction could remove the coating. The more important engineering question was:
What combination of power, coil geometry, scanning speed and interface temperature gives reliable disbonding without unnecessarily overheating the steel or degrading the epoxy?
The mechanism is based on the fundamental principles of electromagnetic induction heating: alternating current in the induction coil produces a magnetic field, which induces electrical currents in the conductive steel substrate and generates localized heat.

1. The Engineering Challenge
The test scenario represented a common maintenance problem found in storage tanks, offshore structures, process equipment and heavy industrial steelwork.
The steel had been protected by a multi-component epoxy system with an overall dry-film thickness of approximately 3 mm.
After long-term service, the coating needed to be removed before inspection and recoating.
The project objectives were:
- Remove the bulk epoxy coating without aggressive mechanical attack on the steel.
- Minimize abrasive-media consumption.
- Reduce secondary waste.
- Determine whether a 30 kW system offered sufficient thermal capacity.
- Establish a stable operating window for handheld scanning.
- Avoid unnecessary thermal exposure of the substrate.
- Produce coating fragments large enough for convenient collection.
2. Workpiece and Coating Conditions
| Parameter | Representative Case Value | Engineering Importance |
|---|---|---|
| Substrate | Carbon steel | High electromagnetic coupling makes ferromagnetic steel well suited to induction heating. |
| Steel Thickness | 10 mm | Determines thermal mass and heating response. |
| Coating | Industrial epoxy system | Thermoset coating requiring interface disbonding rather than melting. |
| Total Coating Thickness | Approx. 3.0 mm | Significantly thicker than conventional decorative paint. |
| Surface Geometry | Flat plate | Allows use of a broad flat induction head. |
| Initial Steel Temperature | Approx. 25°C | Used as the baseline for process development. |
| Test Area | Representative 1 m² sections | Allows repeatable comparison of parameter sets. |
| Removal Objective | Bulk coating disbonding | Final surface profiling is treated as a separate preparation stage. |
3. Why a 30kW RPR Induction Heater Was Selected
A larger 60 kW system could theoretically supply more heat, but maximum available power was not the primary objective of this case.
The engineering team wanted to determine whether a more compact 30kW RPR induction coating removal heater could produce a stable thermal disbonding condition for a moderate-thickness steel plate carrying a 3 mm epoxy coating.
This is important because oversized equipment can introduce disadvantages:
- Higher capital cost
- Heavier equipment
- Greater electrical infrastructure requirements
- Higher risk of applying excessive heat if scanning control is poor
- No proportional productivity gain when manual scraping becomes the process bottleneck
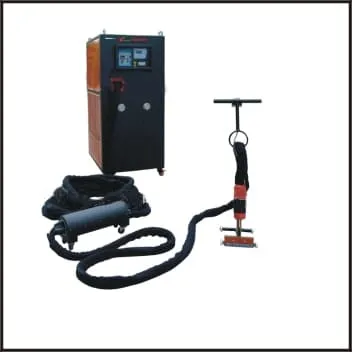
DWS-30P Reference Equipment Configuration
| Parameter | DWS-30P Reference Specification |
|---|---|
| Maximum Input Power | 30 kW |
| Output Frequency | 20–50 kHz |
| Input Supply | 380 V, 3 Phase, 50/60 Hz |
| Output Current Range | Approx. 6–54 A |
| Long-Distance Cable | 20 m / 40 m configuration available |
| Cooling Requirement | Industrial water cooling |
| Recommended Application | Paint, epoxy, rubber and other bonded coating removal from conductive steel |

4. Why 3mm Epoxy Is an Interesting Induction Application
A 3 mm epoxy coating sits in an interesting process window.
It is thick enough that completely grinding through the coating can require substantial labor and abrasive consumption, but it is not so thick that the coating itself provides extreme thermal insulation.
Induction avoids trying to heat the entire epoxy layer uniformly.
Instead, the steel underneath the coating is heated. Thermal energy reaches the steel/epoxy interface, where differential thermal expansion and changes in adhesive strength can reduce bonding.
The objective is therefore:
Heat the interface enough to achieve disbonding, but not more than necessary.
5. Process Development: Finding the Correct Temperature Window
The most important finding was that maximum temperature was not the same thing as maximum process quality.
Four process windows were evaluated conceptually during parameter development.
| Trial | Generator Setting | Scanning Speed | Estimated Interface Temperature | Coating Behavior | Assessment |
|---|---|---|---|---|---|
| A | 55–60% | 0.85–0.95 m/min | 150–175°C | Localized lifting, significant areas remained bonded | Insufficient heat input |
| B | 65–70% | 0.70–0.80 m/min | 180–205°C | Good edge lifting, partial sheet removal | Usable but inconsistent |
| C | 75–80% | 0.60–0.70 m/min | 200–230°C | Large sheets released with moderate scraping force | Preferred process window |
| D | 90–100% | 0.40–0.50 m/min | 250°C+ | Very rapid release but increased smoke, local epoxy degradation and unnecessary steel heating | Excessive thermal input |
Important: These temperature ranges are representative process-development values rather than universal epoxy-removal temperatures. Actual disbonding temperature varies with resin chemistry, primer system, adhesion strength, substrate thickness and coating age.
Why Trial C Was Selected
Trial C created the best balance between three competing requirements:
- Sufficient interface temperature to break adhesion.
- Enough scanning speed to achieve commercially useful productivity.
- Limited unnecessary thermal exposure of the steel and coating.
This illustrates a key principle of induction stripping and coating removal: the process should be optimized around the disbonding threshold, not around the highest temperature the machine can produce.
6. Heating Head and Coil Design
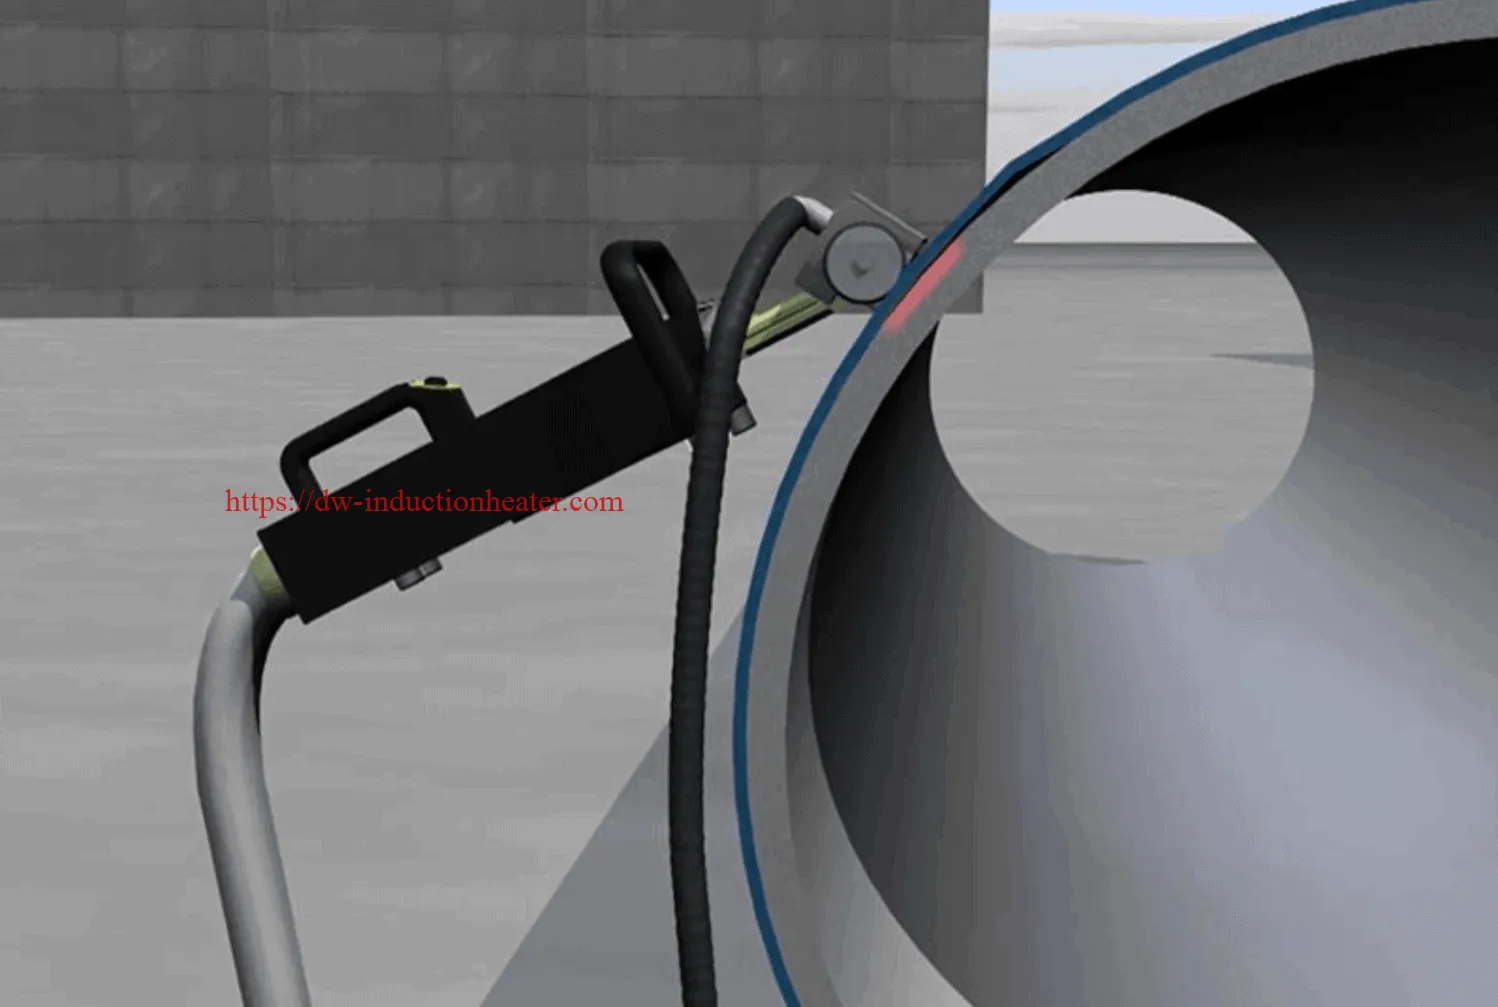
For the flat steel test panel, a broad handheld heating head was preferable to a narrow concentrated coil.
A highly concentrated magnetic field can produce a narrow hot zone. That can be useful for brazing or localized heat treatment, but coating removal requires a relatively uniform thermal footprint.
The representative case therefore used:
- Flat induction-head geometry
- Single-turn or low-turn copper inductor
- Approximate effective heating width: 140–160 mm
- Controlled stand-off distance
- Approximately 10–15% pass overlap
Different workpieces require different induction heating coil designs. A flat storage-tank wall and a small-diameter pipeline should not use identical heating-head geometry.

7. Optimized Scanning Strategy
A common mistake in coating-removal applications is moving the induction head randomly over the workpiece.
The test instead used a repeatable parallel-pass strategy.
Recommended Sequence
- Start at one edge of the coated panel.
- Establish a stable travel speed before increasing power.
- Scan in parallel straight-line passes.
- Maintain approximately 10–15% overlap between adjacent passes.
- Follow the heating head with a mechanical scraper.
- Peel the coating while the interface remains in the weakened state.
- Avoid reheating already-clean steel unless necessary.
Why Scraper Timing Matters
The coating does not remain equally easy to remove indefinitely.
After the heating head passes, the steel begins losing heat through:
- Conduction into surrounding steel
- Convection to ambient air
- Radiation
- Heat transfer into the remaining coating
The most efficient workflow therefore positions the scraping operation shortly behind the induction head.
8. Representative Removal Results
After process optimization, the coating behavior changed considerably compared with mechanical removal alone.
| Performance Indicator | Representative Optimized Result |
|---|---|
| Epoxy Thickness | 3.0 mm |
| Steel Thickness | 10 mm |
| Generator | 30 kW RPR induction heater |
| Working Power Setting | Approx. 75–80% |
| Typical Travel Speed | Approx. 0.60–0.70 m/min |
| Effective Working Width | Approx. 140–160 mm |
| Pass Overlap | Approx. 10–15% |
| Representative Interface Window | Approx. 200–230°C |
| Coating Release | Predominantly large flakes / sheets |
| Practical Net Removal Rate | Approx. 3.5–4.0 m²/h |
| Secondary Abrasive Waste | None during induction bulk-removal stage |
| Final Surface Profiling | Separate preparation step if required by coating specification |
9. Electrical Energy Consumption per Square Meter
For industrial buyers, removal speed alone is not enough. Electrical energy intensity is also useful when comparing operating costs.
A simple engineering relationship is:
Specific Electrical Energy = Average Electrical Load ÷ Net Removal Rate
Assume the optimized case operates at an average effective electrical load of approximately 22.5 kW and achieves 3.8 m²/h net productivity.
22.5 kW ÷ 3.8 m²/h ≈ 5.9 kWh/m²
If auxiliary cooling and pumping add approximately 1.5 kW:
24 kW ÷ 3.8 m²/h ≈ 6.3 kWh/m² total system electricity
Illustrative Electricity-Cost Sensitivity
| Electricity Price | Energy Consumption | Estimated Electricity Cost per m² |
|---|---|---|
| US$0.08/kWh | 6.3 kWh/m² | US$0.50/m² |
| US$0.12/kWh | 6.3 kWh/m² | US$0.76/m² |
| US$0.20/kWh | 6.3 kWh/m² | US$1.26/m² |
| US$0.30/kWh | 6.3 kWh/m² | US$1.89/m² |
These figures represent electricity only. A complete economic comparison must also consider labor, abrasive media, water, containment, waste collection, surface preparation and equipment depreciation.
10. Why the Coating Came Off in Sheets
The result can be explained by the difference between coating destruction and interfacial disbonding.
Grinding destroys coating material mechanically.
Abrasive blasting progressively erodes it.
Induction attempts to preserve much of the coating layer while breaking its adhesion to the underlying steel.
Once adhesion becomes lower than the mechanical strength of the epoxy layer itself, the coating can detach as comparatively large pieces.
This distinction is important for waste management.
Instead of creating a mixture of:
- Epoxy particles
- Dust
- Spent abrasive
- Rust
- Contaminants
the bulk induction-removal stage may produce comparatively large solid coating fragments that are easier to collect.
11. 30kW vs 60kW: Was the 30kW Machine Large Enough?
For this particular 3 mm epoxy / 10 mm steel scenario, the representative analysis indicates that a 30 kW system can provide a practical process window.
However, that does not mean 30 kW is ideal for every epoxy-removal project.
| Parameter | 30kW System | 60kW System |
|---|---|---|
| 3 mm Epoxy on Moderate Steel Thickness | Very suitable candidate | More capacity than required in some cases |
| Handheld Operation | Good balance | Possible but requires careful power control |
| Large Heating Head | Limited by available power density | Better suited |
| Very Thick Steel | Slower thermal response | More available thermal capacity |
| High-Throughput Production | Moderate | Higher potential productivity |
| Electrical Infrastructure | Lower requirement | Higher requirement |
| Equipment Size / Mobility | Generally easier to deploy | Larger system |
| Process Control Sensitivity | Relatively forgiving | High power requires controlled scanning |
When Would We Recommend 60kW Instead?
A 60 kW machine becomes increasingly attractive when one or more of the following conditions apply:
- Very thick steel substrate
- Large induction-head working area
- Higher required m²/h productivity
- Very thick rubber or PFP coatings
- Automated rather than handheld movement
- Large storage tanks or long pipelines
- Continuous industrial stripping operation
12. Comparison with Alternative 3mm Epoxy Removal Methods
| Factor | 30kW Induction | Abrasive Blasting | UHP Water Jetting | Laser Cleaning |
|---|---|---|---|---|
| Removal Principle | Interface thermal disbonding | Mechanical erosion | High-pressure mechanical removal | Optical ablation |
| Suitability for 3mm Epoxy | High where adhesion can be thermally weakened | High | High | Application-dependent; thick coatings require substantial ablation volume |
| Abrasive Consumption | None during bulk removal | High | None | None |
| Water Consumption | Cooling circuit only | Low / none depending on method | High | Low |
| Secondary Waste | Mainly removed coating | Coating + abrasive mixture | Coating + wastewater | Fine ablated material / fumes requiring extraction |
| Dust Potential | Relatively low during sheet removal | High without containment | Low airborne dust but wastewater generated | Requires extraction of process emissions |
| Surface Profile Creation | Minimal | Excellent | Limited / application dependent | Limited |
| Bulk Thick-Coating Removal | Strong advantage | Effective | Effective | Generally better suited to thinner or precision applications |
| Final Recoating Preparation | May need secondary preparation | Often integrated | May require additional preparation | Depends on coating specification |
13. Induction Should Not Be Marketed as a Complete Replacement for Surface Preparation
This case revealed an important distinction.
Coating removal and surface preparation are not always the same operation.
The induction system can efficiently remove the bulk epoxy coating, but a new coating specification may require:
- Defined surface cleanliness
- Specified anchor profile
- Removal of residual primer
- Salt contamination testing
- Removal of flash rust or corrosion products
A technically sound workflow may therefore be:
| Stage | Process | Objective |
|---|---|---|
| 1 | Induction heating | Break epoxy-to-steel adhesion |
| 2 | Mechanical peeling/scraping | Remove bulk 3 mm coating |
| 3 | Inspection | Assess steel and residual contamination |
| 4 | Light blasting / power-tool cleaning if required | Produce specified cleanliness and profile |
| 5 | Surface verification | Confirm suitability for recoating |
| 6 | New coating application | Restore corrosion protection |
14. Thermal Control: Why More Heat Is Not Always Better
The highest-power test condition produced fast coating release, but it was not selected.
This is because excessive thermal input can create several disadvantages:
- Increased coating decomposition
- More smoke or process fumes
- Higher steel temperature
- Unnecessary electrical consumption
- Greater heat-affected area
- Reduced operator control
The preferred strategy is therefore to identify a process window just above the threshold where reliable disbonding occurs.
This concept can be summarized as:
Insufficient Heat: coating remains bonded.
Optimized Heat: bond weakens and coating peels in sheets.
Excessive Heat: removal may be fast, but coating degradation and unnecessary substrate heating increase.
15. Temperature Measurement Challenges
Measuring temperature during coating removal deserves special attention.
An infrared thermometer pointed at the outer epoxy surface does not necessarily measure the steel/coating interface temperature accurately.
Potential measurement errors arise from:
- Different surface emissivity
- Coating color
- Reflections
- Changing coating condition during peeling
- Temperature gradient through the 3 mm epoxy layer
Recommended Development Method
For a controlled qualification test:
- Use an infrared camera to map the overall temperature pattern.
- Validate readings with a contact thermocouple on an accessible steel location.
- Record generator power percentage.
- Record scanning speed.
- Record working-head stand-off distance.
- Document coating release behavior.
This creates a reproducible process recipe rather than relying only on operator experience.
16. Why Cable Length Matters in Real Projects
A laboratory test panel can be placed next to the power supply. A storage tank or offshore platform cannot.
Real industrial applications may require the operator to work:
- Inside tanks
- On scaffolding
- Around large-diameter vessels
- Along pipelines
- On ship decks
- At elevated steel structures
For this reason, a long-distance output cable is an important part of an RPR-style induction coating-removal system.
The main generator and cooling package can remain at a practical service location while the handheld induction head is taken to the coating-removal area.
17. Quality-Control Criteria for the Finished Surface
Success should not be defined simply as “the paint came off.”
A professional coating-removal process should evaluate:
| Inspection Item | Acceptance Question |
|---|---|
| Bulk Coating Removal | Has the 3 mm epoxy layer been substantially removed? |
| Residual Primer | Is residual material acceptable for the next preparation stage? |
| Steel Condition | Is there any unacceptable distortion or thermal effect? |
| Corrosion Exposure | Has hidden corrosion become visible for inspection? |
| Surface Profile | Does recoating require additional abrasive profiling? |
| Contamination | Are salts, oil or other contaminants present? |
| Waste Condition | Can removed coating be collected efficiently? |
18. Productivity Analysis: Where the Real Bottleneck Moves
Once induction heating becomes sufficiently fast, generator power may no longer be the only productivity limitation.
The process bottleneck can shift to:
- Manual scraping
- Coating collection
- Operator walking speed
- Work-platform repositioning
- Inspection
- Final surface preparation
This explains why doubling generator power from 30 kW to 60 kW does not necessarily double completed square meters per hour.
For large projects, the entire workflow should be analyzed rather than the heater alone.
19. Suggested Two-Person Operating Method
For a flat 3 mm epoxy-coated steel surface, an efficient crew can consist of:
| Operator | Responsibility |
|---|---|
| Operator 1 | Controls induction heating head, travel speed and overlap. |
| Operator 2 | Follows immediately with scraper, removes released epoxy and monitors coating behavior. |
This separation of tasks allows the induction operator to maintain a consistent heating pattern instead of repeatedly stopping to remove coating.
20. Safety Considerations for Epoxy Removal
Although induction coating removal can reduce abrasive dust, it remains an industrial thermal process.
The following controls should be evaluated:
- Electrical safety
- Electromagnetic-field procedures
- Hot-surface protection
- Ventilation
- Local fume extraction where required
- Coating composition review
- Respiratory protection where required
- Protective gloves and clothing
- Cooling-water monitoring
- Fire prevention
Before heating an existing coating, the project owner should identify its chemical composition whenever possible.
Older industrial coatings may contain hazardous pigments or additives, so “lower dust” must never be interpreted as “no exposure risk.”

21. Key Engineering Lessons from the 3mm Epoxy Case
The most important lessons from this engineering case are not simply that a 30 kW machine can remove epoxy.
The deeper findings are:
- Interface temperature matters more than maximum generator power.
- Travel speed and power must be optimized together.
- Uniform coil geometry is critical for predictable sheet release.
- Excessive temperature can reduce process quality even when removal becomes faster.
- Scraping should closely follow the induction head.
- Coating removal and final surface preparation should be treated as separate engineering stages.
- A 30 kW unit can be more appropriate than a larger system when manual handling and coating collection are the productivity bottlenecks.
22. Frequently Asked Questions
Can a 30kW induction heater remove a 3mm epoxy coating?
Yes, a 30 kW induction heater can be a suitable candidate for a 3 mm epoxy coating on ferromagnetic steel. Actual performance depends on steel thickness, epoxy chemistry, adhesion strength, heating-head size and required productivity.
What temperature is required to remove epoxy by induction?
There is no universal temperature. In this representative engineering case, reliable disbonding occurred in an approximate 200–230°C interface-temperature window. The actual optimum temperature must be established by testing the specific coating system.
Does induction melt the epoxy coating?
Not necessarily. The objective is to weaken the adhesion at the coating-to-steel interface. The coating may remain sufficiently intact to be removed in sheets or large fragments.
Does the entire 10mm steel plate need to reach 200°C?
No. Induction produces localized surface heating. The objective is to develop sufficient thermal energy near the coating interface rather than uniformly heating the complete steel component.
How fast can 3mm epoxy be removed?
The representative optimized case produced an estimated net productivity of approximately 3.5–4.0 m²/h using handheld operation. Actual site productivity can be higher or lower depending on geometry, operator skill, coating adhesion and work access.
How much electricity does induction epoxy removal consume?
Under the representative conditions in this case, total electrical energy intensity was estimated at approximately 6.3 kWh/m². This value must not be treated as a universal specification.
Is 60kW better than 30kW?
Not automatically. A 60 kW unit provides more heating capacity and can support larger heads or higher throughput, but a 30 kW system can be a better balance for moderate steel thickness and handheld coating-removal work.
Can induction remove epoxy without sandblasting?
Induction can remove the bulk epoxy without abrasive blasting. However, light blasting or another preparation process may still be required to achieve the surface cleanliness and anchor profile specified for a new coating.
Can the same machine remove rubber and PFP coatings?
Potentially yes. Induction disbonding can be applied to several bonded coating systems, but each coating requires its own qualified power, travel-speed and temperature window.
Should a sample be tested before buying the machine?
Yes. A representative coated steel sample is the best way to determine suitable generator power, heating-head design, temperature range, scanning speed and expected productivity.
23. Information Required for an Application Test
For a reliable equipment recommendation, provide:
- Steel grade
- Steel thickness
- Coating type
- Coating thickness
- Number of coating layers
- Workpiece dimensions
- Flat or curved geometry
- Required removal area
- Target productivity
- Available electrical supply
- Required cable length
- Photographs of the coated workpiece
- A physical coated sample whenever possible
Conclusion: Is a 30kW RPR Induction Heater Suitable for 3mm Epoxy?
This engineering case demonstrates why equipment selection for coating removal should be based on the complete thermal process rather than kW rating alone.
For a representative 3 mm epoxy coating bonded to a 10 mm carbon-steel substrate, a 30 kW RPR induction heater provides sufficient capacity to establish a practical disbonding window while retaining good control during handheld operation.
The optimized strategy is not to maximize temperature.
Instead, the objective is to coordinate:
generator power + induction coil geometry + coupling distance + scanning speed + interface temperature + scraper timing.
When those parameters are correctly balanced, the epoxy can separate in relatively large sheets, significantly reducing the amount of material that must be mechanically ground or abrasively blasted away.
For thicker steel, larger working heads, heavier rubber or PFP systems, or substantially higher productivity requirements, a higher-power system may be preferable.
HLQ offers several RPR induction coating removal heater systems for different coating-removal requirements.
Need to Test Your Coating?
Send HLQ your steel grade, steel thickness, coating material, coating thickness, workpiece dimensions, required removal speed and application photos.
A sample coating test is recommended before final machine selection.