
Induction Coating Removal: How It Works, Applications, Benefits and Equipment Selection
Induction coating removal is an advanced thermal disbonding process used to remove paint, epoxy, rubber linings, pipeline coatings, passive fire protection and other strongly bonded industrial coatings from steel surfaces.
Unlike abrasive blasting, grinding or water jetting, induction does not rely primarily on mechanical force to destroy the coating. Instead, electromagnetic energy heats the steel substrate underneath the coating. This controlled heating weakens the bond at the steel/coating interface, allowing the coating to be peeled, scraped or lifted away.
The technology is based on the same electromagnetic principles used in industrial induction heating technology, but the process is optimized specifically for coating disbonding and surface maintenance.
Typical applications include:
- Storage tank coating removal
- Oil and gas pipeline coating removal
- Rubber lining removal
- Marine and ship coating removal
- Offshore platform maintenance
- Epoxy coating stripping
- Passive fire protection removal
- Bridge and structural steel maintenance
- Petrochemical equipment refurbishment
- Mining equipment coating removal
What Is Induction Coating Removal?
Induction coating removal is a controlled heating process in which electromagnetic energy is used to generate heat directly in an electrically conductive metal substrate.
When the metal surface heats, thermal energy reaches the interface between the steel and the coating. At an appropriate temperature, the adhesion strength between them decreases significantly.
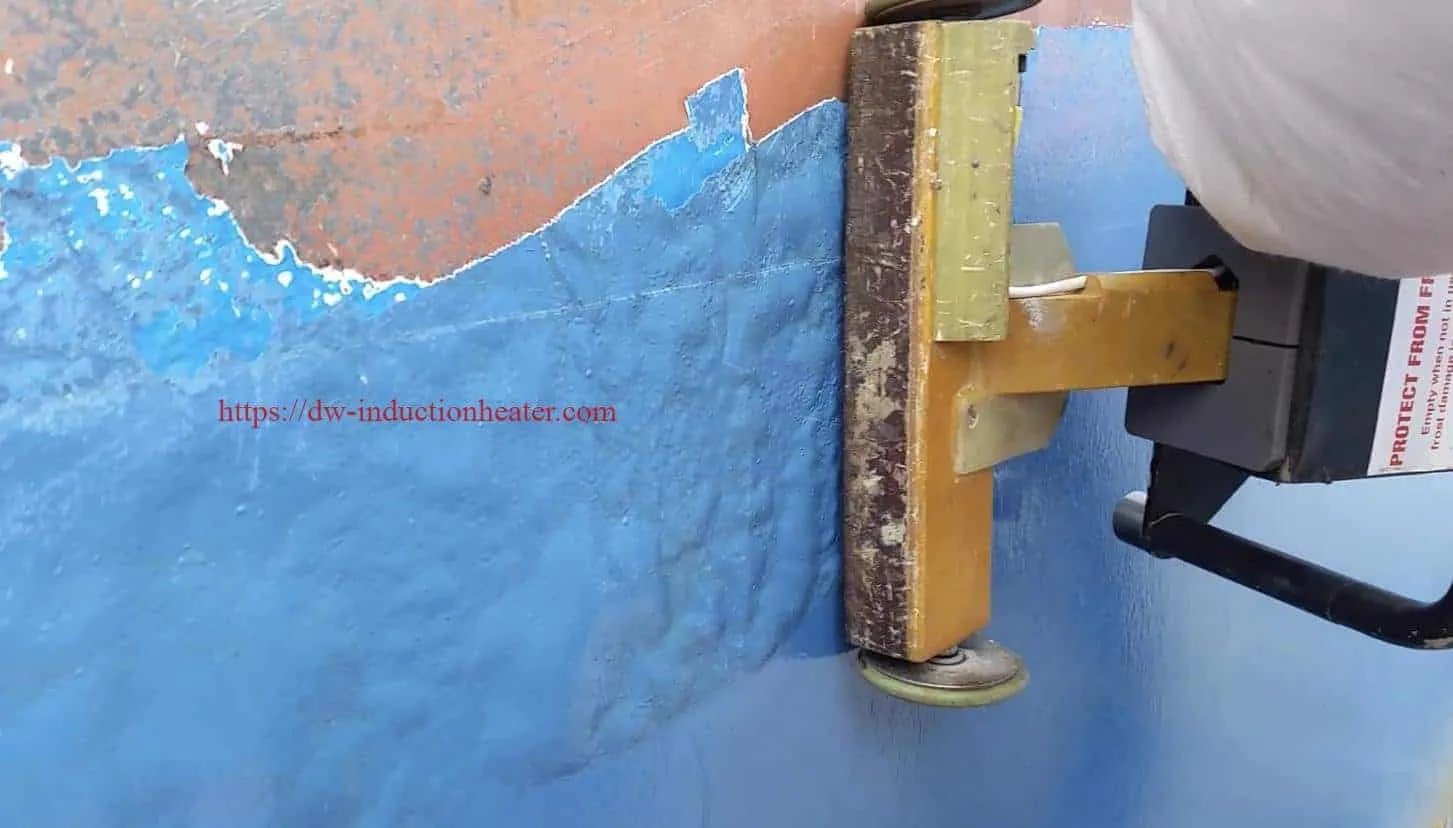
The operator can then remove the loosened coating with a scraper or other mechanical removal tool.
In suitable applications, thick coating systems can separate in sheets, strips or relatively large sections instead of being pulverized into fine particles.
This characteristic makes an industrial induction coating removal machine especially attractive for applications involving thick or strongly bonded coatings on carbon steel.
How Does Induction Coating Removal Work?
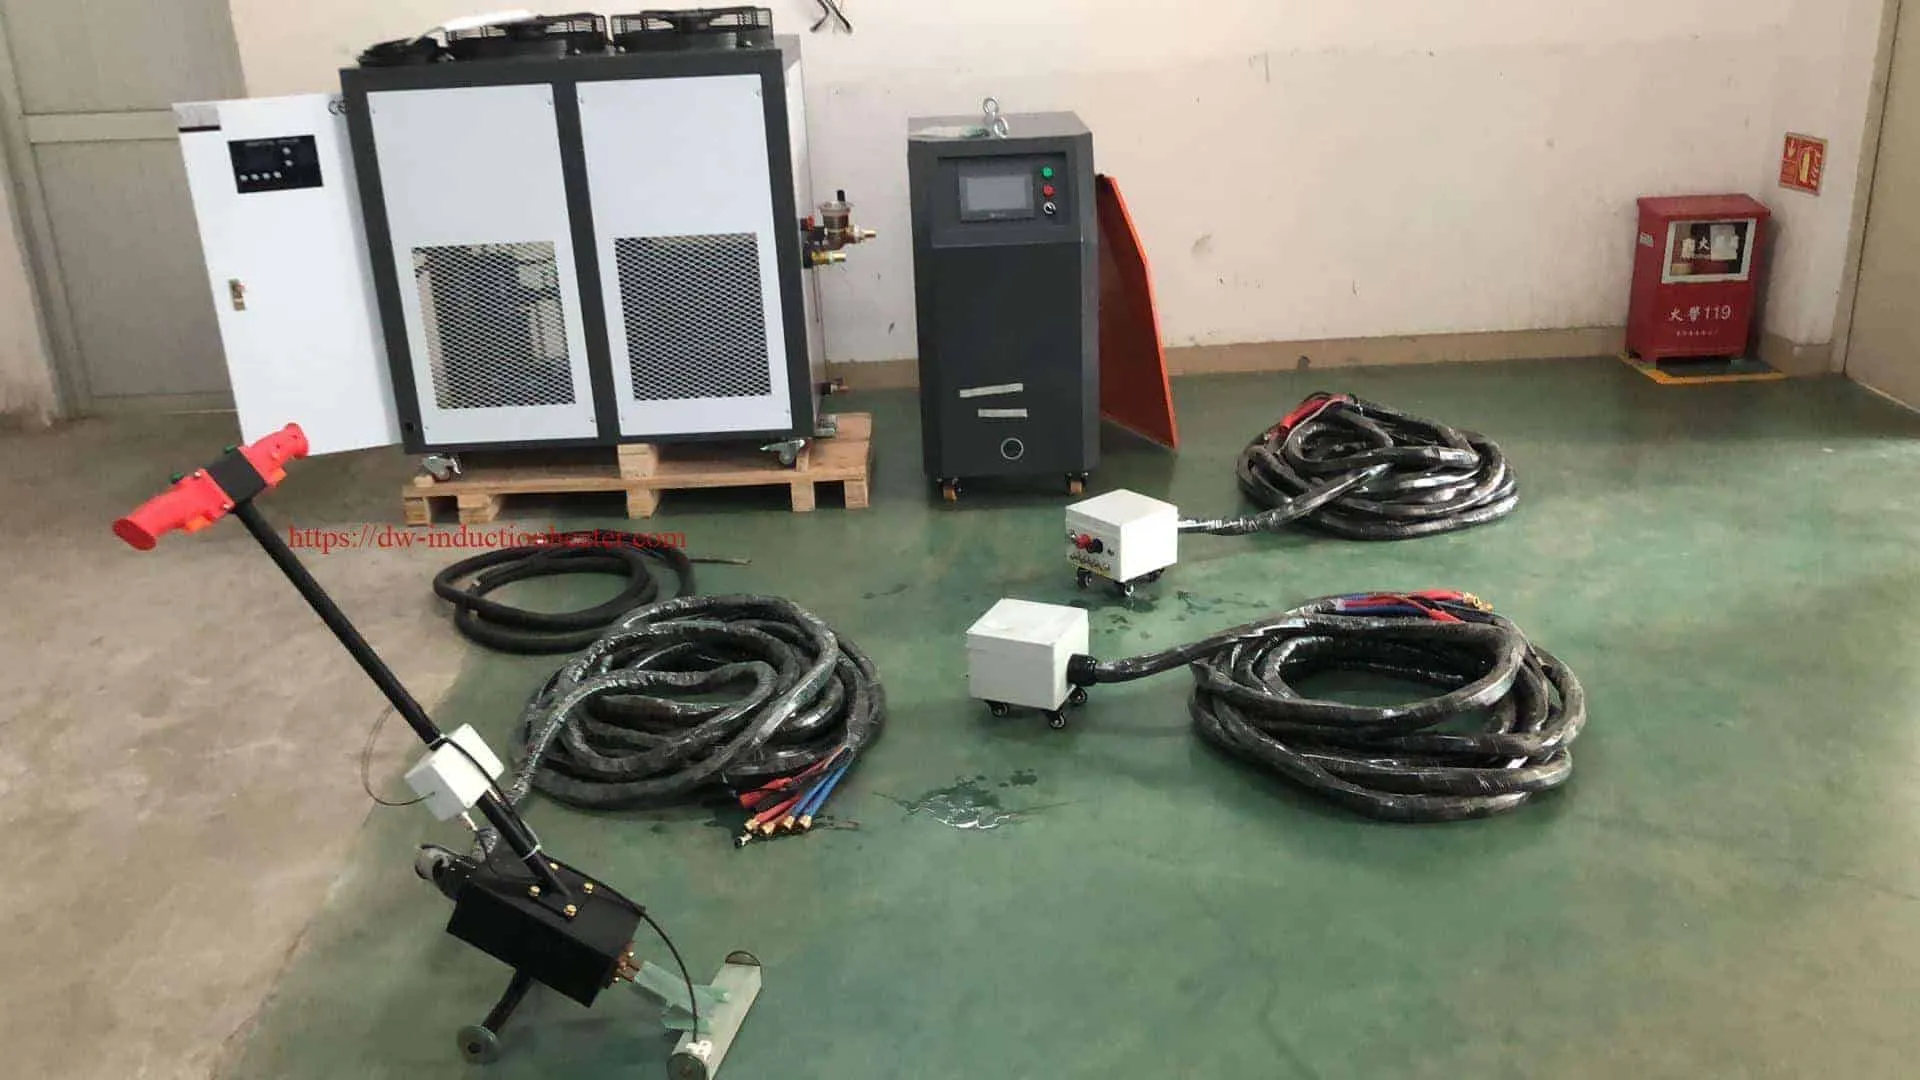
An induction coating removal system normally consists of several main components:
- Induction heating power generator
- Power conversion and control system
- Long-distance flexible cable
- Handheld induction heating head
- Flat or application-specific induction coil
- Industrial water cooling system
- Temperature monitoring and process controls
Step 1: Alternating Current Is Supplied to the Induction Coil
The induction generator converts industrial electrical power into controlled alternating electrical current at a suitable operating frequency.
The alternating current flows through an induction coil installed inside the heating head.
Step 2: An Electromagnetic Field Is Generated
The alternating current creates a rapidly changing electromagnetic field around the induction coil.
When the heating head is placed close to a conductive metal surface such as carbon steel, the electromagnetic field couples with the substrate.
Step 3: Eddy Currents Generate Heat in the Steel
Electrical currents are induced inside the steel substrate. The electrical resistance of the steel converts these currents into heat.
This means the steel itself becomes the heat source.
The process is therefore fundamentally different from applying a flame, hot air or radiant heat to the outside of the coating.
Step 4: The Coating Bond Is Weakened
Heat generated inside the steel travels toward the coating interface.
When the interface reaches an appropriate disbonding condition, the adhesive strength between the coating and metal decreases.
Step 5: The Coating Is Mechanically Removed
The operator follows the induction heating head with a scraper or removal tool.
Depending on the coating system, the material may separate in strips, sheets or large pieces.
Why Is Induction Effective for Removing Industrial Coatings?
Traditional coating removal technologies normally attack the coating from its outer surface.
Examples include:
- Abrasive blasting
- Grinding
- Needle scaling
- Water jetting
- Mechanical scraping
- Chemical stripping
For extremely thick coatings, these processes may require considerable time because the entire coating thickness must be mechanically removed.
Induction approaches the problem differently.
Instead of removing every coating layer from the outside inward, induction targets the bonding interface between the coating and the steel.
This makes the technology particularly interesting for thick and difficult coating systems.
What Coatings Can Be Removed by Induction Heating?
Induction coating removal can be evaluated for many industrial coating systems installed over conductive metal substrates.
Typical examples include:
- Epoxy coatings
- Coal tar epoxy
- Rubber linings
- Vulcanized rubber
- Polyethylene coatings
- 3LPE pipeline coatings
- 3LPP pipeline coatings
- Bituminous coatings
- Anti-skid coatings
- Fiberglass-based coatings
- Passive fire protection
- Intumescent coatings
- Thick multilayer paint systems
HLQ provides a range of induction stripping and coating removal systems for different industrial applications and coating conditions.
Epoxy Coating Removal from Steel
Epoxy coatings are extensively used to protect industrial steel against corrosion, chemicals, seawater and atmospheric exposure.
They are commonly found on:
- Storage tanks
- Marine equipment
- Structural steel
- Petrochemical equipment
- Pipelines
- Process vessels
Heavy-duty epoxy systems can be extremely difficult to remove using grinding alone.
Induction heating can reduce adhesion at the epoxy-to-steel interface so that the coating can be mechanically separated after heating.
Rubber Lining Removal Using Induction Heating
Rubber lining is commonly bonded to steel equipment that requires corrosion, abrasion or chemical resistance.
Examples include:
- Mining tanks
- Chemical vessels
- Rubber-lined pipelines
- Process tanks
- Drums
- Wear-resistant equipment
Traditional rubber removal may involve cutting, grinding and extensive manual labor.
Induction heating can apply energy through the steel substrate and weaken the bonding interface underneath the rubber.
The loosened rubber may then be peeled or mechanically lifted from the steel.
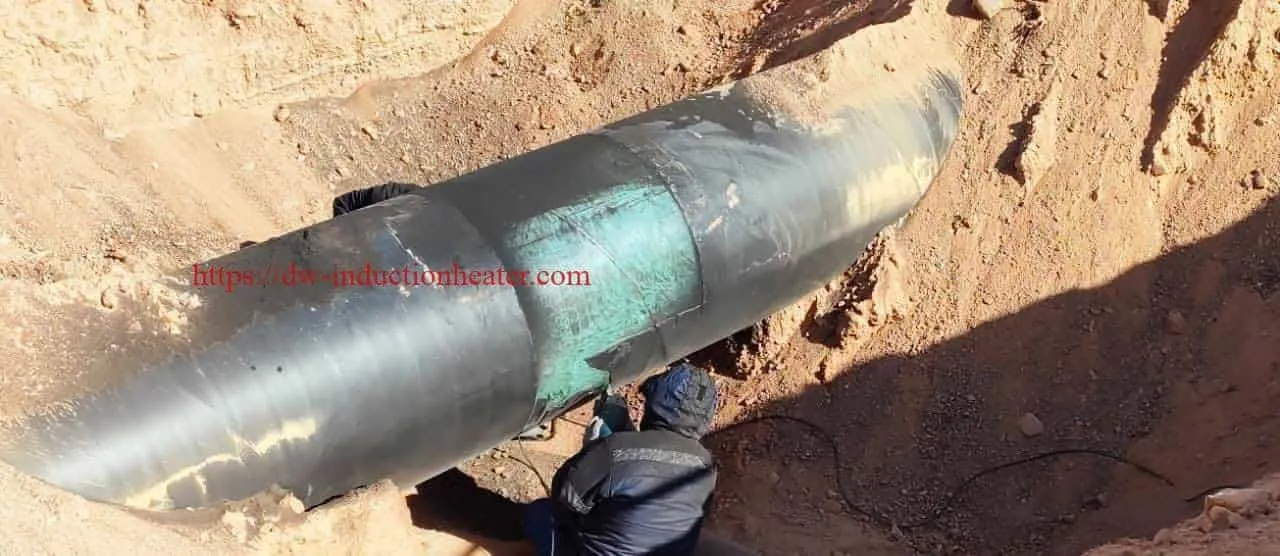
Pipeline Coating Removal with Induction Heating
Pipeline rehabilitation is one of the most important applications for induction coating removal.
Oil, gas and industrial pipelines frequently use durable external coating systems designed to remain bonded to steel for many years.
Common pipeline coatings include:
- 3LPE
- 3LPP
- Coal tar
- Coal tar epoxy
- Ebonite
- Rubber
- Polyethylene
- Heavy epoxy systems
When pipelines require repair, welding, inspection, recoating or corrosion assessment, these coatings may need to be removed locally.
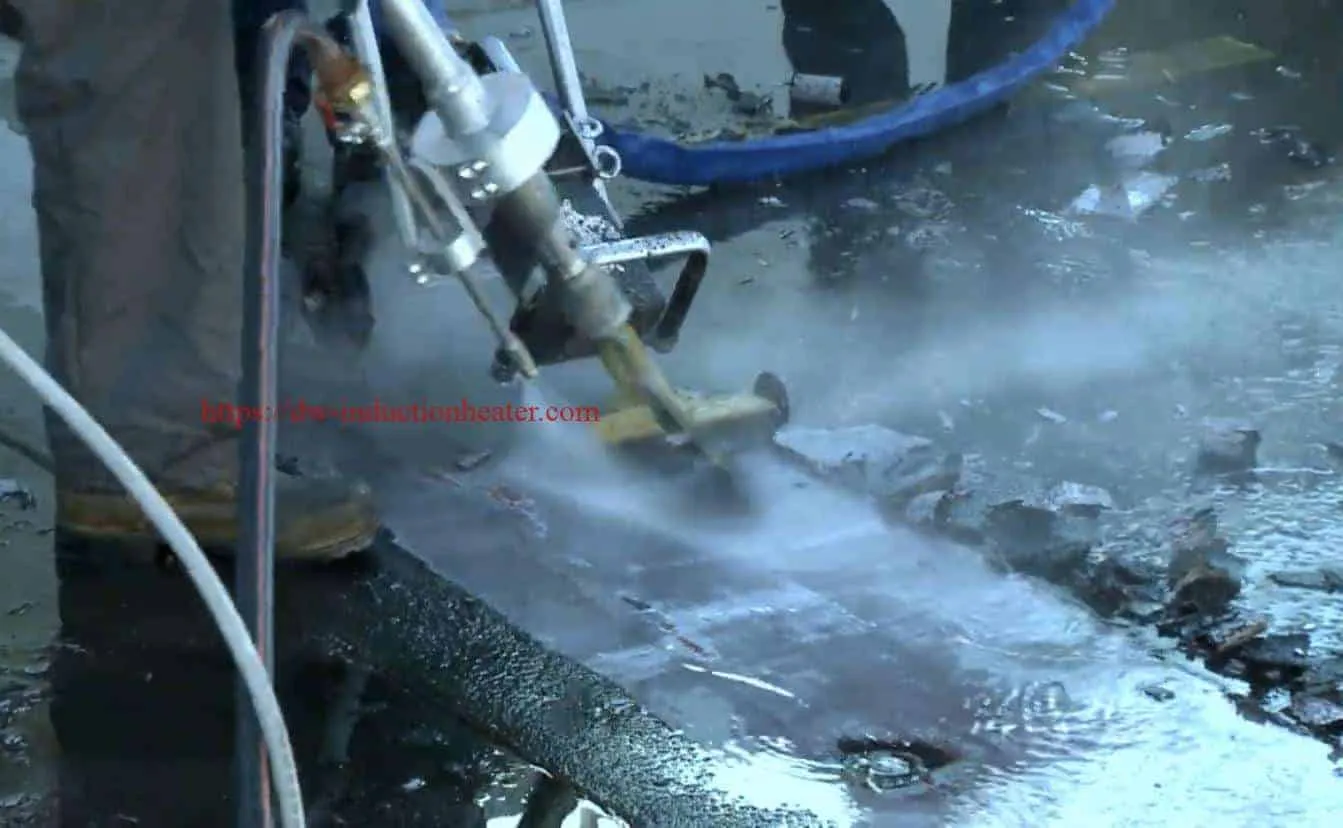
An induction pipeline coating removal system can heat the steel below the coating and weaken the interface without requiring large quantities of blasting grit or water during the bulk-removal stage.
Typical Pipeline Applications
- Pipeline rehabilitation
- Coating replacement
- Inspection area preparation
- Corrosion assessment
- Weld-area preparation
- Repair sleeve installation
- Field joint work
- Removal of aging pipeline coatings
3LPE and 3LPP Pipeline Coating Removal
Three-layer polyethylene (3LPE) and three-layer polypropylene (3LPP) systems are widely used for external pipeline corrosion protection.
These systems typically contain multiple strongly bonded layers.
Mechanical removal can therefore be labor intensive.
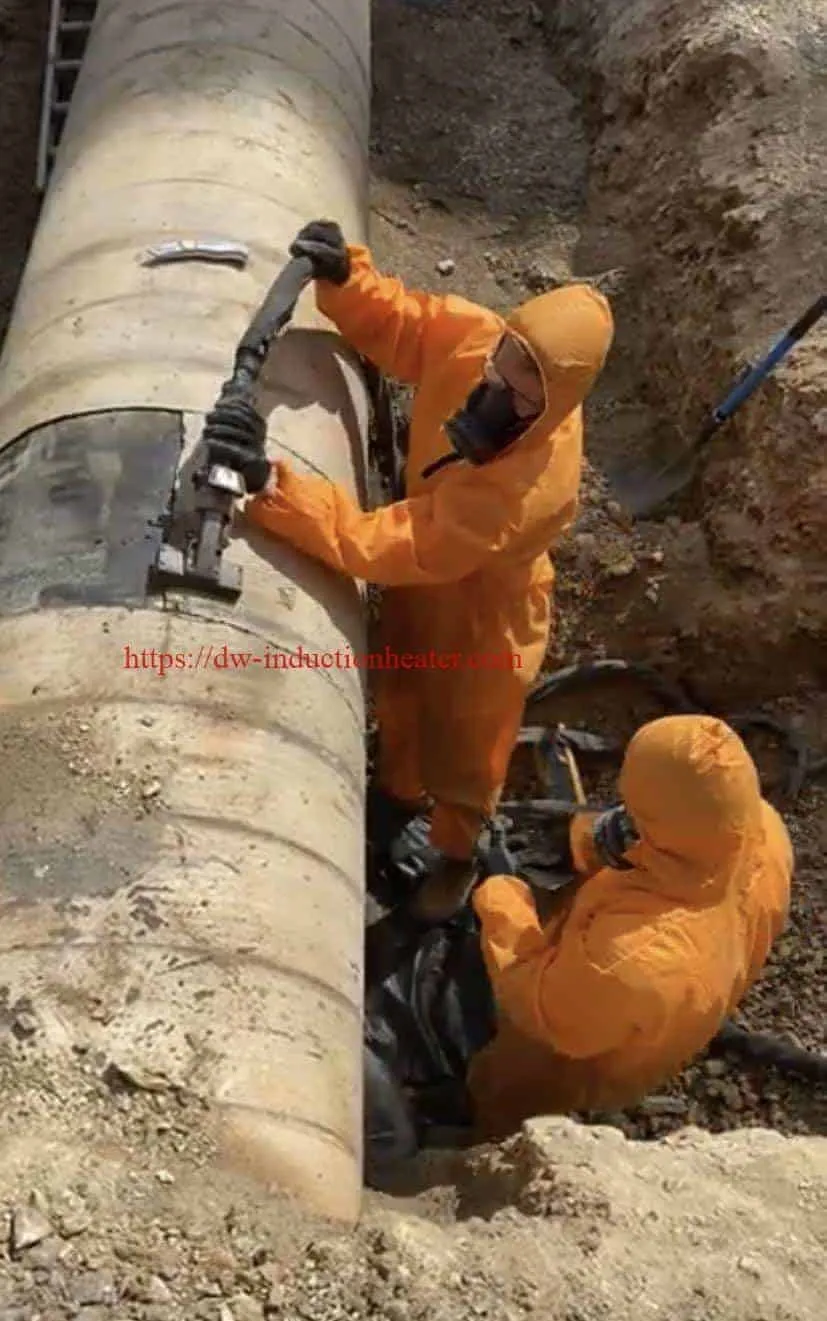
By heating the pipeline substrate underneath the coating, induction can reduce interfacial adhesion and assist removal of selected sections.
This can be especially useful for maintenance locations where only a controlled area of the pipeline requires coating removal.
PFP and Intumescent Coating Removal
Passive fire protection, often abbreviated as PFP, can be among the most difficult industrial coatings to remove.
PFP systems can be very thick and are widely used in:
- Offshore oil and gas structures
- Refineries
- Petrochemical plants
- Structural steel
- Process modules
- Marine installations
Instead of mechanically grinding through the entire fire-protection layer, induction heating can target the steel/coating interface.
This creates an opportunity for large sections of coating to be separated after suitable thermal disbonding.
Marine and Ship Coating Removal
Marine structures require durable coatings because they operate in highly corrosive environments.
Potential applications include:
- Ship decks
- Hull structures
- Bulkheads
- Helidecks
- Anti-skid coatings
- Marine epoxy coatings
- Offshore modules
- Port infrastructure
For thick coating systems, induction can be used as the bulk coating-removal step before final surface preparation.
Storage Tank Coating and Lining Removal
Large industrial storage tanks often contain multiple layers of corrosion-protection coating or internal lining.
Applications may include:
- Crude oil storage tanks
- Fuel tanks
- Chemical tanks
- Water tanks
- Process vessels
- Petrochemical storage tanks
Induction coating removal can be especially useful on large flat or gently curved steel surfaces where a handheld heating head can be moved continuously across the work area.
Induction Coating Removal vs Sandblasting
Abrasive blasting is one of the most established surface-preparation technologies and remains important in industrial maintenance.
However, induction coating removal and sandblasting work in fundamentally different ways.
| Parameter | Induction Coating Removal | Abrasive Sandblasting |
|---|---|---|
| Primary Mechanism | Thermal disbonding at coating/substrate interface | Mechanical abrasion from the outside surface |
| Blasting Media | Not required for bulk disbonding | Normally required |
| Secondary Abrasive Waste | Low | Can be substantial |
| Dust Generation | Generally lower | Can be significant |
| Very Thick Coatings | Particularly attractive | Possible but can consume significant media |
| Surface Profile Generation | Limited | Excellent |
| Steel Abrasion | Minimal when properly controlled | Intentional abrasive action |
| Removed Material | May remain in strips or sheets | Normally fragmented and mixed with abrasive |
| Noise Level | Relatively low | Typically high |
| Final Surface Preparation | Additional cleaning may be required | Can remove coating and create profile simultaneously |
Does Induction Completely Replace Sandblasting?
Not necessarily.
This is an important engineering consideration.
When the specification for a new coating requires a particular surface profile or cleanliness standard, abrasive blasting or another final surface-preparation process may still be required.
A practical workflow can therefore be:
- Use induction to remove the bulk of the thick coating.
- Collect and dispose of the removed coating.
- Perform lighter abrasive or mechanical surface preparation.
- Inspect the steel substrate.
- Apply the new coating system.
This approach can reduce the quantity of material that must be removed using abrasive blasting.
Induction Coating Removal vs Laser Cleaning
Laser cleaning and induction disbonding are sometimes considered for the same surface-maintenance project, but their strengths differ.
Laser Cleaning Is Particularly Suitable For:
- Rust
- Oxides
- Thin paint
- Localized contamination
- Precision cleaning
- Fine surface preparation
Induction Coating Removal Is Particularly Suitable For:
- Thick coatings
- Rubber linings
- Heavy epoxy systems
- Pipeline coatings
- Passive fire protection
- Large coated steel structures
For some projects, a hybrid process may be practical: induction removes the bulk coating while another technology completes the final surface cleaning.
What Determines Induction Coating Removal Speed?
There is no single universal removal rate for all coatings.
Actual productivity depends on several engineering factors.
1. Coating Material
Rubber, epoxy, polyethylene and fireproof coatings have different thermal and bonding characteristics.
2. Coating Thickness
A thin paint system and a 10–20 mm thick lining require completely different process settings.
3. Steel Thickness
Steel acts as a thermal mass.
Thicker steel generally requires more energy to increase the interface temperature at the same rate.
4. Induction Power
The available output power determines the maximum rate at which electromagnetic energy can be delivered to the workpiece.
Industrial induction heating power supplies should therefore be selected according to the steel thickness, heating-head area, coating type and target productivity rather than power rating alone.
5. Coil and Heating Head Design
The geometry of the induction coil determines how electromagnetic energy is distributed across the steel.
A flat steel plate may use a broad flat coil, while a curved pipeline may require a head that follows the pipe radius.
6. Coupling Distance
The distance between the induction head and steel affects electromagnetic coupling and heating efficiency.
7. Travel Speed
The operator must balance travel speed with power input and required disbonding temperature.
Importance of Induction Coil Design
The induction coil is one of the most important parts of a coating-removal system.
For coating stripping, the coil normally needs to distribute heat over a relatively broad surface instead of producing an extremely concentrated hot spot.
The shape should therefore be designed according to:
- Workpiece geometry
- Required working width
- Power level
- Operating frequency
- Steel thickness
- Coating characteristics
- Desired travel speed
Different induction heating coil designs can be developed for flat plate, curved pipe and other industrial steel structures.
How to Choose an Induction Coating Removal Machine
Machine selection should not be based only on the rated output power.
Before selecting equipment, the following information should be evaluated.
| Parameter | Why It Matters |
|---|---|
| Steel Material | Determines electromagnetic and thermal behavior. |
| Steel Thickness | Affects thermal mass and required heating power. |
| Coating Type | Different coatings have different disbonding behavior. |
| Coating Thickness | Influences heating conditions and removal method. |
| Workpiece Geometry | Determines the required induction-head design. |
| Required Working Width | Affects heating-head size and power density. |
| Required Removal Speed | Influences required generator capacity. |
| Cable Length | Important for tanks, pipelines and remote working areas. |
| Duty Cycle | Important for continuous industrial operation. |
| Cooling Conditions | Affects generator and heating-head reliability. |
Typical HLQ Induction Coating Removal System Configuration
An industrial HLQ coating-removal package may include:
- 25–60 kW induction generator
- Long-distance output cable
- Handheld induction heating head
- Application-specific flat induction coil
- Industrial water cooling system
- Temperature monitoring
- Operator control system
- Mobile equipment configuration
- Scraping and removal tools
Typical HLQ models include:
- DWS-25P
- DWS-30P
- DWS-60P
The appropriate model should be selected according to the actual industrial application rather than simply choosing the highest available power.
Example: Storage Tank Epoxy Removal
Consider a typical project with the following conditions:
| Application | Storage Tank Maintenance |
| Substrate | Carbon Steel |
| Coating | Heavy-Duty Epoxy |
| Surface | Tank Wall |
| Operation | Handheld Continuous Scanning |
| Possible Power Range | 30–60 kW, subject to testing |
A preliminary system may include a medium-frequency induction generator, long-distance cable, flat heating head and industrial cooling system.
However, a sample test should be carried out before confirming:
- Final power requirement
- Working frequency
- Heating-head size
- Travel speed
- Target interface temperature
- Estimated removal productivity
Benefits of Induction Coating Removal
1. No Abrasive Media Required for Bulk Disbonding
The thermal disbonding stage does not require blasting grit.
This can significantly reduce secondary abrasive waste.
2. Suitable for Thick Industrial Coatings
Induction is especially interesting for thick coatings that are expensive or slow to remove layer by layer.
3. Lower Dust Generation
If the coating separates in solid strips or sheets, airborne particulate generation can be lower than highly aggressive abrasive removal.
4. Localized Energy Application
Only the steel underneath the working area needs to be heated.
5. Reduced Mechanical Attack on Steel
The coating bond is weakened thermally rather than by continuously abrading the metal substrate.
6. Lower Secondary Waste Volume
Removed coating does not have to be mixed with large quantities of spent blasting media.
7. Relatively Low Noise
The induction process itself does not rely on a high-velocity abrasive stream striking the steel surface.
Industries Using Induction Coating Removal
Oil and Gas
- Pipelines
- Storage tanks
- Refineries
- Offshore structures
- Process equipment
Marine and Shipbuilding
- Ship decks
- Hull structures
- Bulkheads
- Helidecks
- Marine infrastructure
Petrochemical
- Storage vessels
- Process tanks
- PFP-coated steel
- Structural steel
Mining
- Rubber-lined tanks
- Rubber-lined pipes
- Wear-resistant equipment
- Processing equipment
Infrastructure
- Steel bridges
- Structural steel
- Large coated steel components
Safety Considerations
Induction coating removal is an industrial heating process and should only be operated by trained personnel.
A proper project risk assessment should consider:
- Electrical safety
- Hot steel surfaces
- Hot removed coatings
- Electromagnetic fields
- Cooling-water conditions
- Coating fumes
- Ventilation
- Fire risk
- Personal protective equipment
- Potentially hazardous coating materials
Older industrial coatings may contain hazardous substances.
Therefore, low dust generation should never be interpreted as eliminating the need for appropriate worker protection, containment or environmental controls.
Frequently Asked Questions
What is induction coating removal?
Induction coating removal is a thermal disbonding process that generates heat in a conductive metal substrate to weaken the bond between the coating and the metal.
Can induction heating remove paint from steel?
Yes. When suitable operating parameters are used, induction heating can weaken the paint-to-steel interface so that the paint can be mechanically removed.
Can induction remove thick epoxy coatings?
Yes. Thick industrial epoxy systems are one of the important potential applications for induction coating removal.
Can induction heating remove rubber lining?
Yes. Induction can be particularly useful where rubber is bonded to a conductive steel substrate because the steel can be heated underneath the lining.
Can induction remove 3LPE pipeline coating?
Yes. Pipeline coating removal is a major industrial application and can include 3LPE, 3LPP, coal tar, rubber and other bonded coating systems.
Does induction coating removal damage steel?
The process is designed to create controlled localized heating sufficient to weaken the coating bond without damaging the steel. However, acceptable temperature limits should always be confirmed for the specific material and application.
Does induction coating removal eliminate sandblasting?
Not necessarily. Induction can remove the bulk coating, while abrasive blasting may still be required to produce the specified surface profile or cleanliness before recoating.
What power is required for an induction coating removal machine?
The required power depends on steel thickness, coating material, coating thickness, heating-head area and required productivity. Industrial equipment is commonly available in power ranges from tens of kilowatts upward.
Is a 60 kW machine always better than a 30 kW machine?
No. Higher power provides greater heating capacity, but correct power density, heating-head geometry, frequency and travel speed are equally important.
What information is required before selecting a machine?
For an accurate recommendation, provide:
- Steel material
- Steel thickness
- Coating material
- Coating thickness
- Workpiece dimensions
- Photos or drawings
- Required removal area
- Required productivity
- Available electrical supply
- Required cable length
Application Testing Is Recommended
Because coating formulations and adhesion characteristics vary considerably, laboratory or workshop testing using the customer’s actual coated sample is highly recommended.
A coating test can help determine:
- Whether induction disbonding is suitable
- Required interface temperature
- Recommended power level
- Heating-head dimensions
- Travel speed
- Expected removal behavior
- Approximate productivity
This is much more reliable than selecting equipment only from coating thickness or machine power.
Conclusion
Induction coating removal provides an alternative way to remove difficult industrial coatings from steel by attacking the coating-to-metal bond rather than mechanically destroying the entire coating from the outside.
The technology is particularly suitable for evaluating applications involving:
- Heavy epoxy coatings
- Rubber linings
- 3LPE and 3LPP pipeline coatings
- Coal tar coatings
- PFP and intumescent coatings
- Marine coatings
- Storage tank linings
- Large industrial steel structures
Successful coating removal depends on correctly matching the induction generator, operating frequency, heating-head design, cable configuration, coupling distance and travel speed to the steel substrate and coating system.
HLQ Induction Equipment can provide industrial induction coating-removal systems and application-specific heating solutions for tanks, pipelines, marine structures, offshore equipment, mining machinery and other coated steel structures.
For equipment selection, please provide your coating type, coating thickness, steel material, steel thickness, workpiece dimensions, required removal speed and photos of the application.