

Induction Pipe Bending Machine for Steel Pipe, Tube and Pipeline Fabrication
Induction Pipe Bending Machine
Table of Contents
- Quick Answer
- What Is This Product?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Coil and Fixture Design
- Control System and Automation
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages
- Limitations
- Why Choose HLQ Induction Equipment?
- FAQ
An induction pipe bending machine is a hot forming system used to bend carbon steel, stainless steel, alloy steel, boiler tubes, structural tubes and large-diameter pipeline pipes by localized induction heating. It is widely used in oil and gas pipelines, petrochemical plants, power stations, shipbuilding, offshore platforms, steel structures and pressure piping fabrication. By heating only a narrow bending zone, the equipment reduces forming force, improves bend quality, minimizes welding joints and helps buyers produce customized long-radius pipe bends that standard elbows or cold bending methods cannot easily achieve.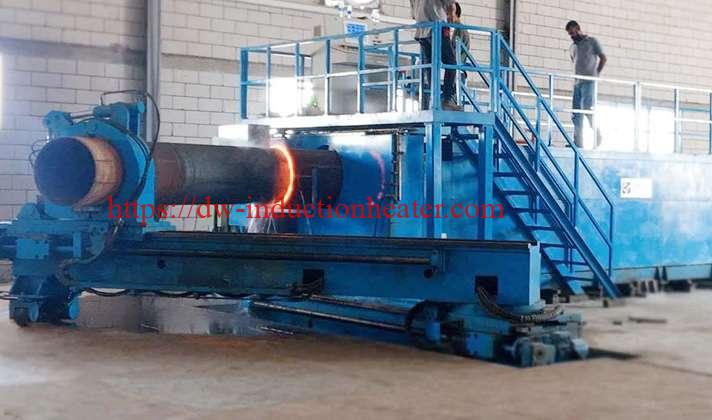
Quick Answer
An induction pipe bending machine is best suited for producing accurate, smooth and repeatable hot bends on medium to large metal pipes, especially when the application requires long-radius bends, thick-wall pipe bending, customized angles, fewer welded elbows and better flow performance in industrial piping systems.
What Is This Product?
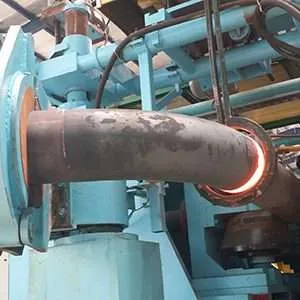
An induction pipe bending machine is an industrial machine that combines electromagnetic induction heating with controlled hydraulic or CNC bending motion. It heats a narrow ring-shaped area of the pipe and bends that heated section around a selected radius. The process is different from cold bending because the pipe is locally heated to a forming temperature before deformation. This reduces the bending resistance of the metal and allows large pipes or thick-wall pipes to be bent with better dimensional control.
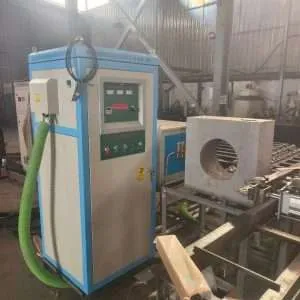
A complete machine normally includes an induction heating power supply, matching transformer, water-cooled copper induction coil, machine bed, hydraulic pushing unit, bending arm, pipe clamp, guide rollers, cooling system, infrared temperature measuring device and PLC or CNC control cabinet. The machine can be configured for different pipe diameters, wall thicknesses, materials, bend radii and production requirements.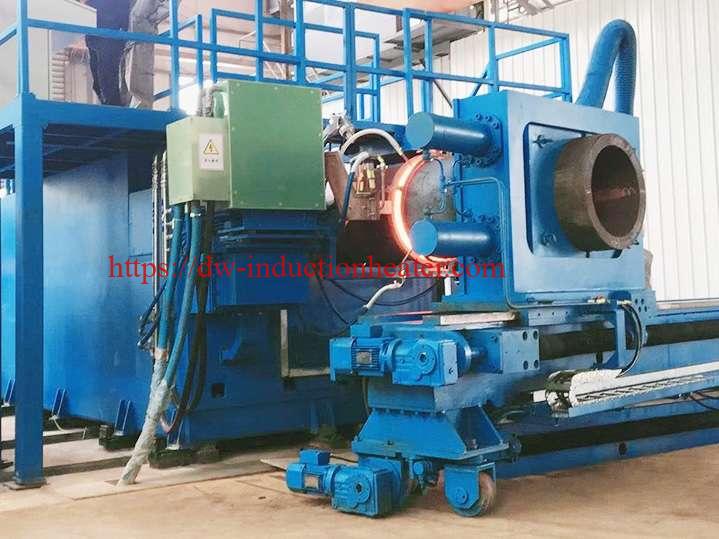
For pipe fabrication companies, the main value of this equipment is flexibility. Instead of relying only on standard elbows, a manufacturer can produce custom bends according to project drawings. This is especially useful for pipeline construction, power plant piping, shipbuilding, chemical plant installation and steel structure projects where pipe routing is often complex.
| Product Function | Engineering Value | Typical Buyer Problem Solved |
|---|---|---|
| Localized pipe heating | Reduces forming force | Large pipe cannot be bent cold |
| Controlled hot bending | Improves bend smoothness | Cold bend cracking or excessive springback |
| Custom bend radius | Supports project-specific pipe routing | Standard elbows are not suitable |
| Long-radius bend production | Reduces flow resistance | Too many short elbows increase pressure loss |
| PLC/CNC control | Improves repeatability | Manual bending quality is unstable |
Key Applications
Induction pipe bending machines are used wherever pipe systems need smooth directional changes, large bend radii or special bend angles. In many industrial projects, the pipe bend is not simply a connection part. It affects fluid flow, installation layout, welding quantity, stress distribution and long-term safety. A properly designed induction bend can replace several welded elbows and simplify the whole piping system.
| Industry | Application | Why Induction Bending Is Used |
|---|---|---|
| Oil and gas | Long-distance pipeline bends, station piping, offshore lines | Large diameter, long radius and fewer welds |
| Petrochemical | Process piping, refinery pipework, chemical transfer lines | Complex routing and high quality requirements |
| Power generation | Steam pipes, boiler tubes, superheater tubes | High-temperature and high-pressure service |
| Shipbuilding | Marine pipe systems, ballast lines, hydraulic lines | Compact pipe routing in limited space |
| Offshore engineering | Platform piping, FPSO modules, subsea support lines | Custom bends and strong structural reliability |
| Steel structure | Curved structural tubes, bridge tubes, architectural frames | Large radius curved steel components |
| Boiler and heat exchanger | Tube coils, economizer tubes, furnace wall tubes | Repeatable tube bending and thermal equipment production |
| Construction machinery | Hydraulic pipes, heavy machine tubes | Durable formed pipes for high-load systems |
Application Coverage Chart
Oil & Gas Pipelines        ████████████████████
Petrochemical Plants       ████████████████
Power Plants               ███████████████
Shipbuilding               ████████████
Steel Structures           ███████████
Boilers & Heat Exchangers  ██████████
Construction Machinery     ████████
Suitable Materials
The induction pipe bending process is suitable for many conductive metals. However, each material has its own heating behavior, deformation range and cooling requirement. Carbon steel and low-alloy steel are the most common materials because they respond well to induction heating and are widely used in pipelines and industrial piping. Stainless steel and alloy steel can also be bent successfully, but they require more precise temperature control to protect surface quality and mechanical properties.
| Material | Suitability | Engineering Notes |
|---|---|---|
| Carbon steel pipe | Excellent | Common for pipelines, steel structures and general industrial piping |
| Low-alloy steel pipe | Excellent | Suitable for pressure piping and power plant applications |
| Stainless steel pipe | Good | Requires accurate temperature control to reduce oxidation and distortion |
| Heat-resistant alloy steel | Good | Used for boilers, steam pipelines and high-temperature equipment |
| Duplex stainless steel | Conditional | Requires strict thermal procedure to protect microstructure |
| Low-temperature steel | Good | Impact properties may need verification after bending |
| Aluminum alloy pipe | Conditional | Lower forming temperature and special tooling required |
| Copper alloy pipe | Conditional | High thermal conductivity requires suitable power and coil design |
| Square and rectangular tube | Conditional | Requires special coil and fixture to control deformation |
Working Principle
The working principle of an induction pipe bending machine is based on electromagnetic induction. When alternating current flows through a copper induction coil, an alternating magnetic field is generated around the coil. When a conductive pipe is placed inside this magnetic field, eddy currents are induced in the pipe wall. These eddy currents generate heat inside the metal because of electrical resistance.
For magnetic steels, magnetic hysteresis also contributes to heating below the Curie temperature. This makes induction heating especially efficient for carbon steel and low-alloy steel pipes. The machine heats only a narrow band around the pipe, not the entire pipe length. Once this heated zone reaches the target bending temperature, the hydraulic pushing system moves the pipe forward while the radius arm guides the pipe into the required curve.
The heated zone continuously moves along the pipe as the pipe advances. After the hot zone passes, the bent section can be cooled by water spray, air cooling or natural cooling. This combination of localized heating, controlled pushing and controlled cooling creates a smooth induction bend.
Induction Pipe Bending Principle Diagram
Straight Pipe Feed Direction
            →
 ┌────────────────────────────────────┐
 │       Guide Rollers / Machine Bed   │
 └────────────────────────────────────┘
               │
               ▼
       ┌───────────────────┐
       │ Induction Coil     │
       │ Local Heating Zone │
       └───────────────────┘
               │
               ▼
       Heated Plastic Zone
               │
               ▼
       Bending Arm / Radius Arm
               │
               ▼
       Finished Long-Radius Bend
Energy Conversion Flow
Electrical Power
      ↓
Induction Power Supply
      ↓
Alternating Current in Coil
      ↓
Alternating Magnetic Field
      ↓
Eddy Currents in Pipe Wall
      ↓
Localized Heat Generation
      ↓
Plastic Deformation and Bending
Technical Specifications
The technical specification of an induction pipe bending machine should be selected according to pipe diameter, wall thickness, material, bend radius, bend angle and production capacity. A machine with the correct pipe diameter range may still fail if the power supply, frequency, coil design or hydraulic pushing force is not suitable. Therefore, engineering selection should be based on the full forming requirement, not only on maximum pipe size.
| Parameter | Specification | Notes |
|---|---|---|
| Product name | Induction Pipe Bending Machine | Hot induction bending equipment for pipes and tubes |
| Heating method | Electromagnetic induction heating | Localized heating of bending zone |
| Applicable pipe OD | 21 mm to 1620 mm or customized | Depends on machine model and pipe material |
| Wall thickness | 2 mm to 120 mm or customized | Thicker pipes require higher power and stronger pushing force |
| Bend radius | 1.5D to 20D | D means pipe outside diameter |
| Bend angle | 0° to 180° | Custom angles available according to project needs |
| Heating power | 60 kW to 2500 kW+ | Selected according to pipe size and production speed |
| Frequency range | 0.5 kHz to 30 kHz typical | Lower frequency is preferred for larger or thicker pipes |
| Power supply type | IGBT or thyristor-based induction power supply | Selected according to power and frequency requirement |
| Pushing method | Hydraulic or servo hydraulic | Controls pipe feeding speed and stability |
| Control system | PLC or CNC | CNC is recommended for repeatable batch production |
| Temperature measurement | Infrared thermometer | Closed-loop control improves heating consistency |
| Cooling method | Water spray, air cooling or natural cooling | Selected according to material and procedure |
| Coil type | Water-cooled copper induction coil | Customized for pipe diameter and heating width |
| Machine layout | Horizontal machine bed | Common for industrial pipe bending |
| Applicable shapes | Round pipe, square tube, rectangular tube, profiles | Special fixtures and coils are required for non-round parts |
Recommended Model Selection
The following model selection table provides a practical reference for engineering evaluation. The final machine configuration should be confirmed after checking the actual pipe grade, outside diameter, wall thickness, bend radius, bend angle and production rhythm.
| Application | Material | Recommended Power | Frequency |
|---|---|---|---|
| Small boiler tube bending | Carbon steel / alloy steel | 60–160 kW | 10–30 kHz |
| Heat exchanger tube bending | Carbon steel / stainless steel | 80–200 kW | 8–25 kHz |
| Medium process pipe bending | Carbon steel / stainless steel | 160–300 kW | 3–15 kHz |
| Shipbuilding pipe bending | Carbon steel / stainless steel | 200–500 kW | 2–10 kHz |
| Petrochemical pipe bending | Carbon steel / alloy steel / stainless steel | 300–800 kW | 1–8 kHz |
| Power plant steam pipe bending | Alloy steel / heat-resistant steel | 500–1200 kW | 0.8–5 kHz |
| Oil and gas pipeline bending | Pipeline steel | 800–1800 kW | 0.5–3 kHz |
| Large-diameter heavy pipe bending | Carbon steel / alloy steel | 1200–2500 kW+ | 0.5–2 kHz |
Power Selection Reference by Pipe Size
| Pipe OD Range | Wall Thickness Range | Typical Power Range | Machine Type |
|---|---|---|---|
| 21–89 mm | 2–12 mm | 60–160 kW | Small tube induction bending machine |
| 89–219 mm | 4–25 mm | 160–300 kW | Medium pipe induction bending machine |
| 219–426 mm | 6–40 mm | 300–600 kW | Heavy-duty pipe bending system |
| 426–720 mm | 8–60 mm | 600–1000 kW | Large pipe induction bending machine |
| 720–1020 mm | 10–80 mm | 1000–1600 kW | Large-diameter pipeline bending system |
| 1020–1620 mm+ | 12–120 mm | 1600–2500 kW+ | Customized heavy-duty induction bending line |
Process Workflow
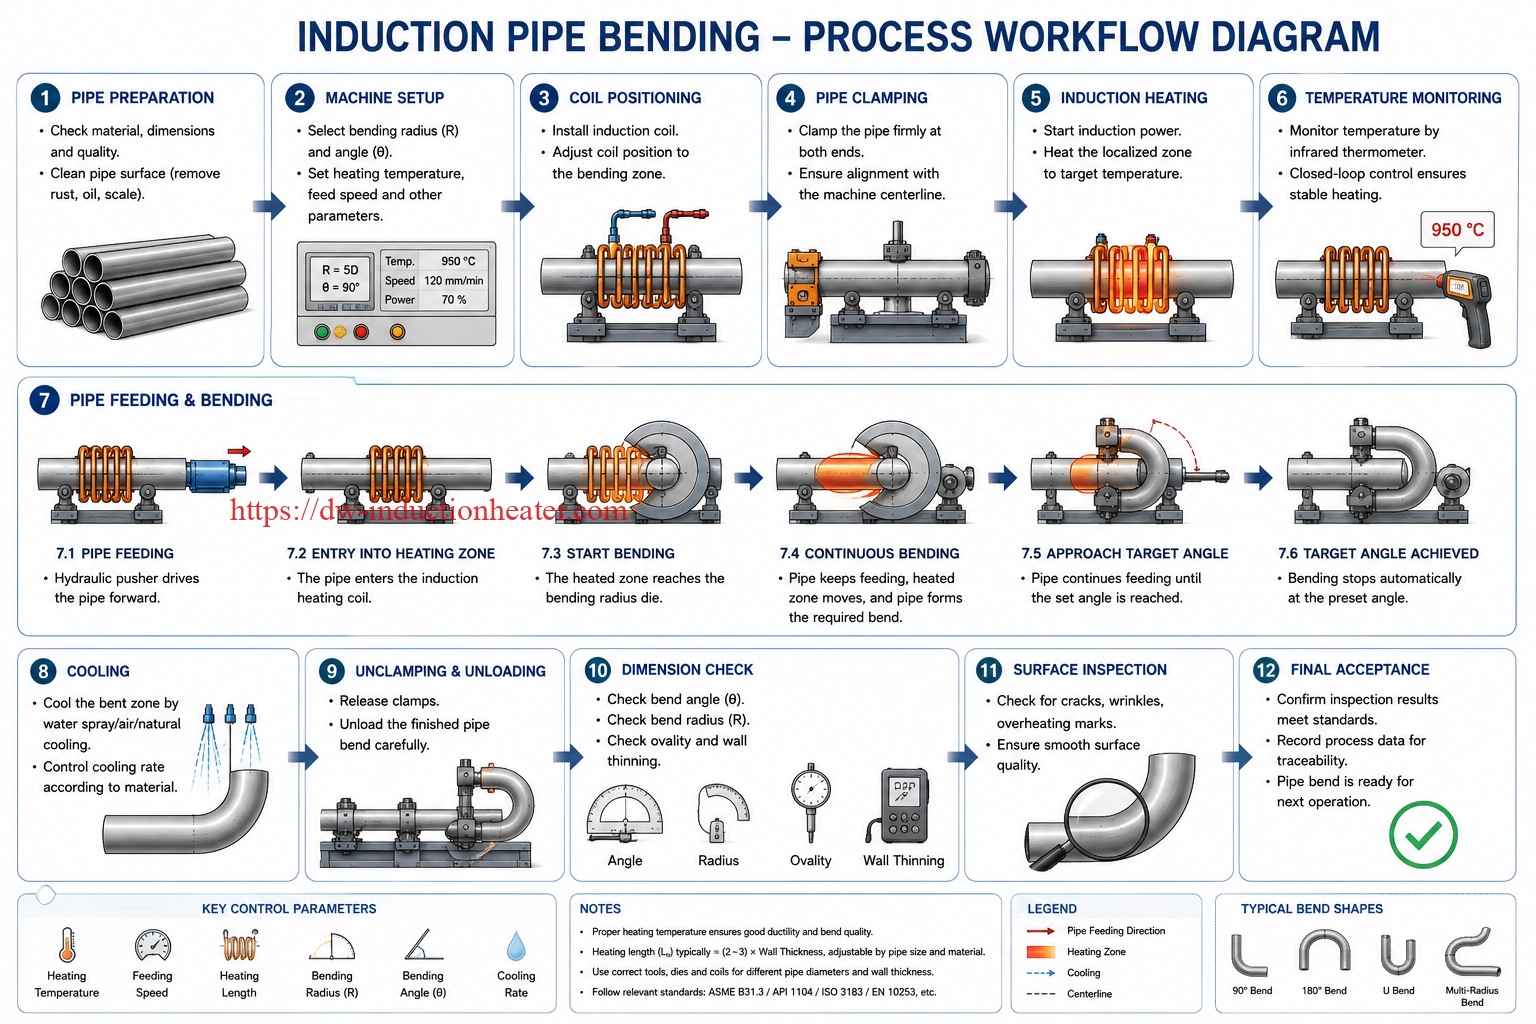
The induction pipe bending process must be stable and repeatable. A good workflow helps reduce defects such as wall thinning, ovality, wrinkles, cracking and inconsistent bend angle. Before production, the operator should confirm the pipe material certificate, pipe size, target bend radius, required angle, heating temperature, cooling method and inspection standard.
Process Flow Chart
Pipe Material Confirmation
        ↓
Pipe Surface Cleaning
        ↓
Machine Parameter Setting
        ↓
Induction Coil Installation
        ↓
Pipe Loading and Clamping
        ↓
Heating Zone Alignment
        ↓
Induction Heating Start
        ↓
Temperature Closed-Loop Control
        ↓
Hydraulic Pushing
        ↓
Radius Arm Bending
        ↓
Controlled Cooling
        ↓
Angle Stop and Unloading
        ↓
Dimensional Inspection
        ↓
Final Quality Record
| Step | Operation | Engineering Checkpoint |
|---|---|---|
| 1 | Confirm pipe data | Material grade, OD, wall thickness and heat number |
| 2 | Clean pipe surface | Remove oil, rust and heavy scale near heating zone |
| 3 | Install induction coil | Check coil diameter, clearance and water flow |
| 4 | Set bend parameters | Radius, angle, speed, temperature and cooling mode |
| 5 | Clamp pipe | Ensure alignment with machine bed and radius arm |
| 6 | Start heating | Reach target temperature evenly around pipe circumference |
| 7 | Start pushing | Maintain stable speed without vibration |
| 8 | Perform bending | Monitor angle, radius and pipe movement |
| 9 | Cool pipe | Select water, air or natural cooling according to material |
| 10 | Inspect bend | Check angle, radius, ovality, wall thickness and surface |
Coil and Fixture Design
The induction coil and fixture are critical to bending quality. The coil controls the heating zone, while the fixture controls pipe movement and deformation. A poorly designed coil may cause uneven temperature, local overheating, slow heating or low energy efficiency. A poor fixture may cause pipe slipping, ovality, wrinkling or inaccurate bend angle.
Induction Coil Design Factors
| Design Factor | Engineering Influence | Recommendation |
|---|---|---|
| Coil inner diameter | Affects coupling efficiency and pipe clearance | Keep suitable clearance for safe movement and efficient heating |
| Coil width | Determines heating band width | Match pipe diameter, wall thickness and bend radius |
| Number of turns | Affects heating intensity and impedance | Design according to power supply and frequency |
| Copper tube size | Affects current capacity and cooling capacity | Use sufficient section for high-current operation |
| Water flow | Prevents coil overheating | Use flow switch and temperature monitoring |
| Magnetic concentrator | Improves heating focus in some cases | Use when heating efficiency or direction control is required |
| Coil insulation | Prevents electrical short circuit | Use heat-resistant and water-resistant insulation |
Fixture and Radius Arm Design
| Fixture Part | Function | Design Requirement |
|---|---|---|
| Pipe clamp | Fixes the pipe during bending | Strong clamping force without surface damage |
| Guide rollers | Support pipe movement | Accurate alignment and low friction |
| Radius arm | Controls bend radius | Rigid structure and accurate positioning |
| Mandrel or internal support | Supports thin-wall pipes if required | Used for difficult bending conditions |
| Cooling spray ring | Cools the pipe after heating | Uniform spray angle and adjustable flow |
| Machine bed | Supports pipe and mechanical load | Heavy-duty welded structure with good straightness |
Control System and Automation
Modern induction pipe bending machines use PLC or CNC control to improve repeatability and reduce operator dependence. The control system should coordinate heating power, pipe pushing speed, bend angle, cooling flow and safety protection. For high-specification pipe bends, process data recording is very important because buyers may need production records for quality traceability.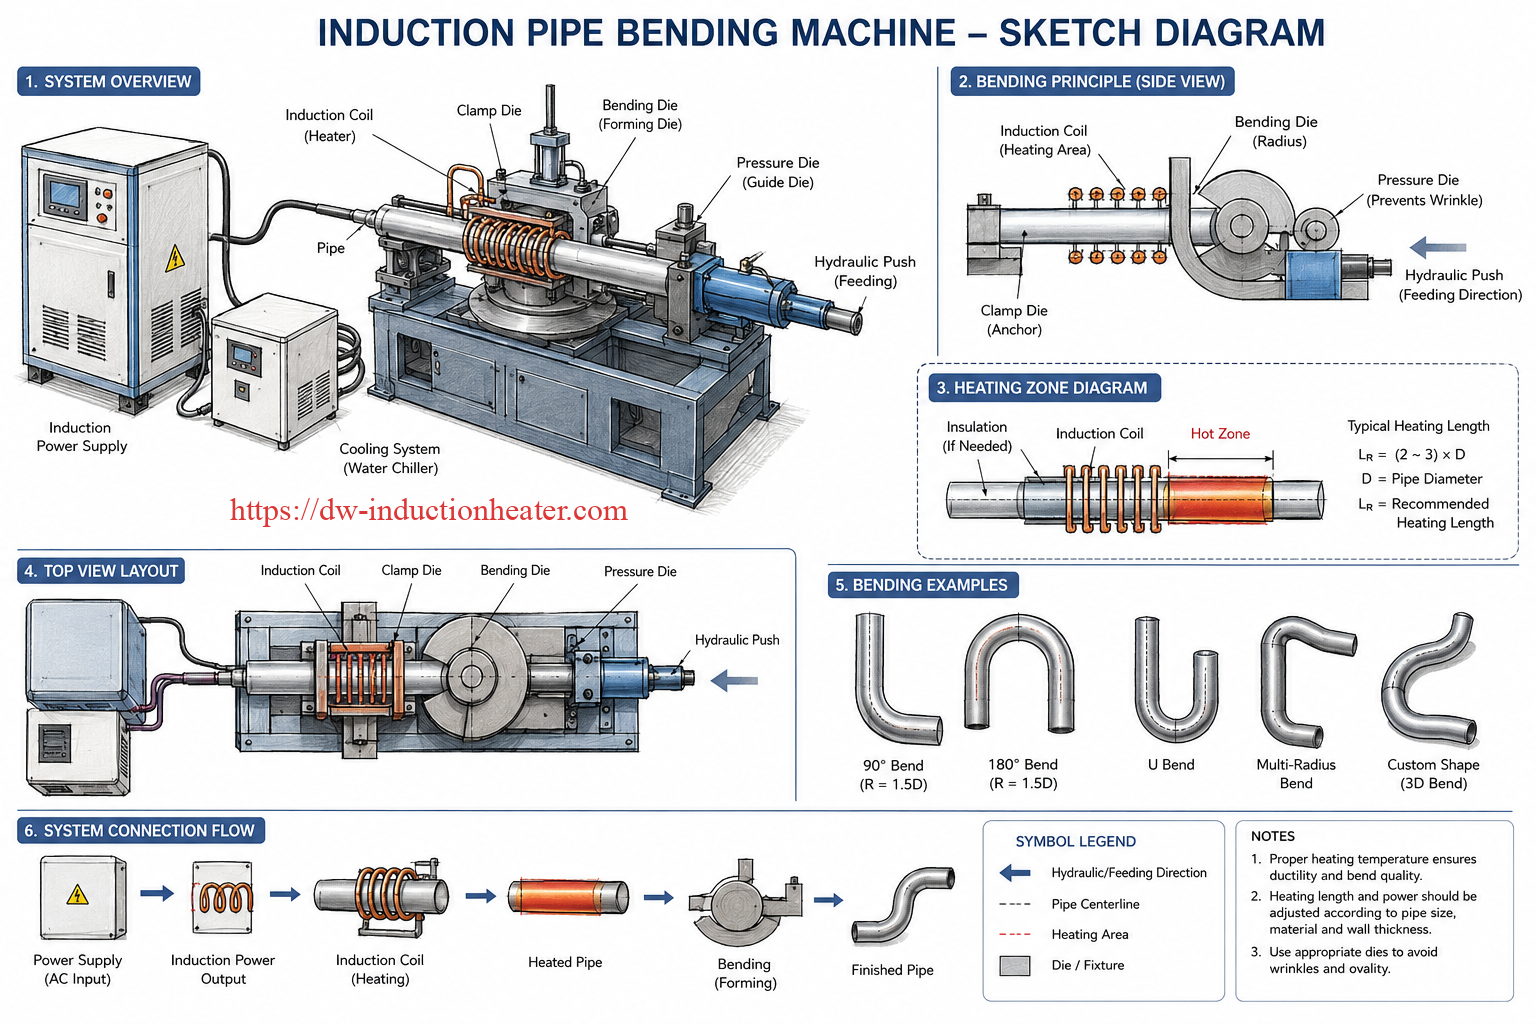
| Control Function | Purpose | Benefit |
|---|---|---|
| Closed-loop temperature control | Adjusts power according to measured temperature | Improves heating stability |
| Hydraulic speed control | Controls pipe pushing speed | Improves bend consistency |
| Bend angle control | Stops machine at target angle | Improves dimensional accuracy |
| Recipe storage | Saves parameters for different pipes | Reduces setup time |
| Water flow monitoring | Protects coil and power supply | Prevents overheating damage |
| Alarm system | Detects abnormal conditions | Improves safety |
| Data recording | Records temperature, speed and time | Supports quality traceability |
| Touchscreen HMI | Operator interface | Simplifies operation and troubleshooting |
Automation Level Comparison
| Automation Level | Features | Suitable Buyer |
|---|---|---|
| Manual assisted | Manual setup, basic control, lower cost | Small workshops and occasional bending |
| PLC control | Automatic heating and speed control | General industrial pipe fabrication |
| CNC control | Recipe storage, angle control and data management | Batch production and high-quality pipe bends |
| Customized production line | Integrated loading, bending, cooling and inspection | Large pipeline bend manufacturers |
Common Problems and Solutions
The most common defects in induction pipe bending are usually related to temperature, speed, coil design, fixture support and cooling method. A stable bending procedure should be developed before mass production.
| Problem | Possible Cause | Engineering Solution |
|---|---|---|
| Excessive wall thinning | Bend radius too small, temperature too high, speed improper | Increase radius, optimize temperature and reduce deformation rate |
| Pipe ovality too high | Poor support, unstable heating, excessive bending force | Adjust guide rollers, improve coil heating uniformity and use better fixture |
| Wrinkles on inner arc | Compression stress too high or radius too tight | Increase bend radius, optimize speed or add internal support |
| Surface cracking | Low material ductility, wrong temperature or rapid cooling | Verify material, adjust heating temperature and cooling method |
| Uneven heating | Incorrect coil clearance or poor coil design | Redesign coil, adjust coupling distance and check power matching |
| Coil overheating | Insufficient water flow or blocked cooling channel | Increase water flow, clean filter and install flow protection |
| Inaccurate bend angle | Control error, pipe slipping or hydraulic instability | Calibrate angle sensor, improve clamping and check hydraulic system |
| Surface scale | High temperature exposure for too long | Optimize heating time and consider protective measures |
| Hardness variation | Improper cooling rate or uncontrolled thermal cycle | Use controlled cooling and perform heat treatment if required |
| Low production speed | Insufficient power or poor coil efficiency | Increase power, improve coil design or optimize frequency |
Engineering Selection Guide
As an engineer, the first step in selecting an induction pipe bending machine is not asking for the maximum pipe diameter. The correct approach is to define the bending task completely. Pipe material, wall thickness, bend radius, heating temperature, production rate and inspection standard all influence machine configuration.
Step 1: Define Pipe Material
Carbon steel is easier to heat and bend by induction than many non-ferrous metals. Stainless steel, duplex steel and alloy steel require more careful thermal control. If the pipe is used in pressure service, material properties after bending must be considered.
Step 2: Confirm Pipe Size
Pipe outside diameter and wall thickness determine the heating power, coil diameter, pushing force and machine bed strength. A thick-wall pipe may require a lower frequency for deeper heating.
Step 3: Confirm Bend Radius
A small radius increases deformation, wall thinning and ovality. A long radius is easier to control and provides better fluid flow. Many pipeline applications prefer long-radius bends to reduce pressure loss.
Step 4: Confirm Production Capacity
If the buyer only produces occasional custom bends, a semi-automatic system may be enough. If the buyer produces large quantities of pipeline bends, CNC control, recipe storage and data recording are strongly recommended.
Step 5: Confirm Quality Standard
Industrial pipe bends may require wall thickness inspection, ovality measurement, hardness testing, NDT, mechanical testing or post-bend heat treatment. The machine should be able to support the required process control.
| Selection Question | Why It Matters | Information Needed from Buyer |
|---|---|---|
| What is the pipe material? | Determines heating and cooling procedure | Material grade and standard |
| What is the pipe OD range? | Determines machine size and coil design | Minimum and maximum outside diameter |
| What is the wall thickness? | Determines power and heating depth | Minimum and maximum wall thickness |
| What is the bend radius? | Determines radius arm and deformation level | 1.5D, 3D, 5D, 10D or custom |
| What is the bend angle? | Determines machine stroke and angle control | Common angle or maximum angle |
| What is the production volume? | Determines automation level | Pieces per day or per month |
| What is the workshop power supply? | Determines electrical configuration | Voltage, phase and frequency |
| What quality tests are required? | Determines process control and records | NDT, hardness, wall thickness, ovality |
Advantages
Compared with traditional bending and elbow welding methods, induction pipe bending provides both production and engineering advantages. It is especially valuable when the project requires custom geometry, large pipe size or reduced welding points.
| Advantage | Explanation | Buyer Benefit |
|---|---|---|
| Localized heating | Only the bending zone is heated | Improves energy efficiency and reduces thermal distortion |
| Lower forming force | Hot metal is easier to deform | Suitable for large and thick-wall pipes |
| Custom bend radius | Radius can be selected according to project needs | More flexible pipe routing |
| Fewer welds | One induction bend can replace several elbows | Reduces welding and inspection cost |
| Smooth flow | Long-radius bend reduces turbulence | Lower pressure loss in pipeline systems |
| Good repeatability | PLC/CNC control stabilizes parameters | Better quality consistency |
| Wide material range | Can process carbon steel, stainless steel and alloy steel | Suitable for many industries |
| Cleaner process | No open flame is required for heating | Improves workshop environment |
Advantages Chart
Custom Radius Flexibility    ████████████████████
Large Pipe Capability        ██████████████████
Reduced Welding Points       █████████████████
Repeatable Quality           ████████████████
Energy Efficiency            ███████████████
Clean Heating Process        █████████████
Limitations
Although induction pipe bending is powerful, it is not the best solution for every pipe forming task. Buyers should understand the limitations before purchasing equipment.
| Limitation | Reason | Practical Recommendation |
|---|---|---|
| Higher initial investment | Machine includes power supply, coil, hydraulic system and controls | Best for regular production or high-value pipe bends |
| Requires process knowledge | Temperature, speed and cooling affect bend quality | Use supplier support and procedure testing |
| Different pipe sizes need different coils | Coil coupling must match pipe diameter | Prepare coil sets for common pipe sizes |
| Not ideal for every non-ferrous metal | High thermal conductivity may reduce heating efficiency | Perform process testing for aluminum or copper alloys |
| Quality inspection still required | Hot bending changes geometry and thermal history | Inspect wall thinning, ovality and surface defects |
| Large machines need factory space | Pipe loading and radius arm movement require room | Plan workshop layout before purchase |
Why Choose HLQ Induction Equipment?
HLQ Induction Equipment Co., Ltd. focuses on industrial induction heating solutions for metal heating applications such as brazing, hardening, forging, melting, annealing, preheating, shrink fitting and customized thermal processing. For induction pipe bending applications, the heating system is one of the most important parts of the entire machine. Stable power output, suitable frequency, reliable coil cooling and accurate temperature control directly affect bending quality.
HLQ can support pipe bending equipment projects with induction heating power supply selection, medium-frequency heating system design, water-cooled coil engineering, transformer matching, cooling system configuration and application testing support. For customers who need to bend carbon steel pipe, stainless steel pipe, alloy pipe, boiler tube or large pipeline pipe, HLQ can help evaluate the proper heating power, frequency range and coil structure according to pipe size and process requirements.
| HLQ Support Area | Customer Value |
|---|---|
| Induction power supply selection | Helps match power and frequency to pipe size and wall thickness |
| Customized coil design | Improves heating uniformity and efficiency |
| Cooling system recommendation | Protects coil, power supply and bending process stability |
| Engineering consultation | Supports material, temperature and process evaluation |
| Application-oriented configuration | Provides solutions for different industries and pipe specifications |
| Export communication support | Helps international buyers clarify technical requirements |
For buyers, a reliable induction pipe bending solution should not be judged only by machine appearance. It should be evaluated as a complete engineering system: heating power, frequency, coil design, hydraulic force, control system, cooling, safety and process support must work together.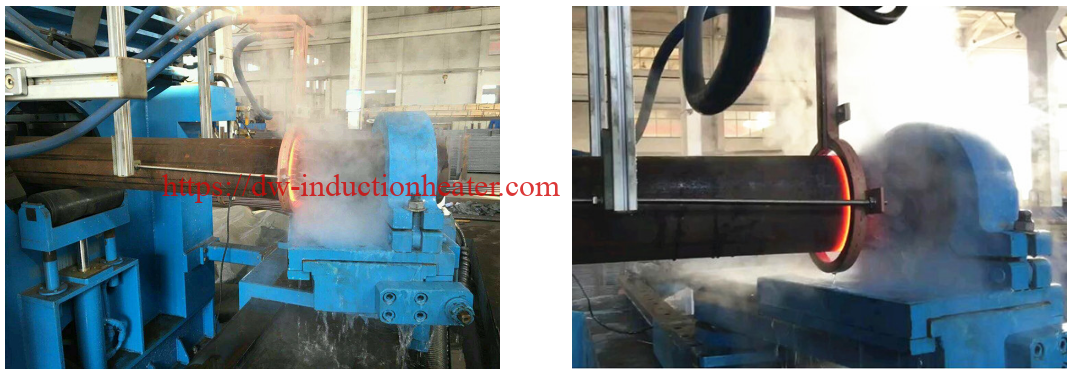
FAQ
1. What is an induction pipe bending machine?
An induction pipe bending machine is equipment that heats a local zone of a pipe by electromagnetic induction and bends the heated section with controlled hydraulic or CNC force.
2. What materials can be bent by induction pipe bending?
Common materials include carbon steel, low-alloy steel, stainless steel, heat-resistant alloy steel, boiler tube steel, pipeline steel and some non-ferrous metals with special process design.
3. Is induction bending better than cold bending?
For large-diameter, thick-wall or high-strength pipes, induction bending is usually better because localized heating reduces forming force and improves bend quality. Cold bending is still useful for smaller and thinner pipes.
4. What is the typical bend radius?
Common bend radii include 1.5D, 3D, 5D and 10D. D means pipe outside diameter. Long-radius bends are often used for pipelines to reduce pressure loss.
5. Does induction bending reduce wall thickness?
Some wall thinning normally occurs on the outer arc of the bend. A correct process can control wall thinning within acceptable engineering limits.
6. Can stainless steel pipe be bent by induction?
Yes. Stainless steel pipe can be bent by induction, but temperature control, oxidation control and cooling method must be carefully selected.
7. What power is needed for an induction pipe bending machine?
Power depends on pipe diameter, wall thickness, material, heating temperature and production speed. Small tube bending may use 60–160 kW, while large pipeline bending may require 1000 kW or more.
8. What frequency is suitable for pipe bending?
Large and thick-wall pipes usually need lower or medium frequency for deeper heating. Smaller tubes can use higher frequency. The final frequency should be selected according to heating depth and pipe size.
9. What is the role of the induction coil?
The induction coil generates the alternating magnetic field that heats the pipe. It is normally made from water-cooled copper tube and customized for the pipe diameter.
10. Can one machine bend different pipe sizes?
Yes, but different pipe sizes usually require different coils, clamps and process settings to maintain heating efficiency and bending accuracy.
11. What cooling method is used after induction bending?
Cooling may be water spray, air cooling or natural cooling. The correct method depends on pipe material, wall thickness and mechanical property requirements.
12. What should be inspected after pipe bending?
Typical inspection items include bend angle, bend radius, ovality, wall thinning, surface cracks, hardness and material properties if required by the project.
13. Can induction bends replace standard elbows?
Yes. In many pipeline and industrial piping projects, induction bends can replace multiple standard elbows, reduce welds and improve flow path design.
14. Is CNC control necessary?
CNC control is recommended for batch production, high accuracy, recipe storage and quality traceability. For occasional bending, PLC control may be sufficient.
15. What information is needed for a quotation?
The buyer should provide pipe material, pipe outside diameter, wall thickness, bend radius, bend angle, production quantity, workshop voltage, cooling water condition and required quality standard.
16. Why is induction pipe bending suitable for oil and gas pipelines?
Oil and gas pipelines often require large-diameter, long-radius and custom-angle bends. Induction bending can produce these bends with fewer welds and smoother flow.
17. What is the difference between pipe bending and tube bending?
Pipe bending usually refers to industrial piping measured by nominal pipe size, while tube bending often refers to tubes measured by outside diameter. Induction heating can be used for both if the machine and coil are designed correctly.
18. How can buyers reduce bending defects?
Buyers should use correct heating temperature, suitable coil design, stable pushing speed, proper cooling method and reliable fixture support. Trial bending and inspection are recommended before batch production.
19. Can induction bending be used for square or rectangular tubes?
Yes, but square and rectangular tubes require special coil design and fixtures to control corner heating, wall collapse and shape deformation.
20. How should I choose a supplier?
Choose a supplier that understands both induction heating and pipe bending engineering. The supplier should provide power selection, coil design, cooling configuration, process support and after-sales service.
Related products
-

Induction Pipe and Tube Heating Applications-Electromagnetic Induction Heating Systems for Pipeline Processing & Manufacturing
-
Medium frequency supplies for induction heating
-
induction billet heaters for hot forming of Steel, Copper, and Aluminum
-
Steel, Titanium,Brass Induction Billet Forging Heater For Extrusion Aluminium, Copper Billet Bar Dies Rod
-
Medium Frequency Induction Power Generator