


High Frequency Induction Heating Equipment
DW-HF-25kW High Frequency Induction Heating Equipment for Brazing and Hardening
Quick Answer
What is the DW-HF-25kW High Frequency Induction Heating Equipment?
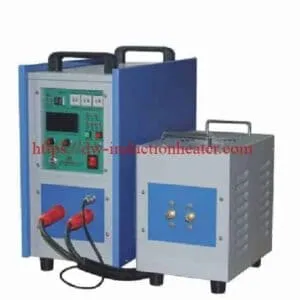
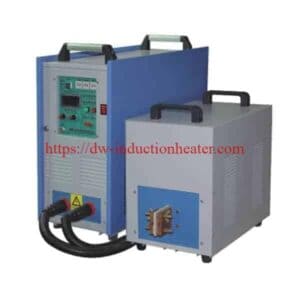
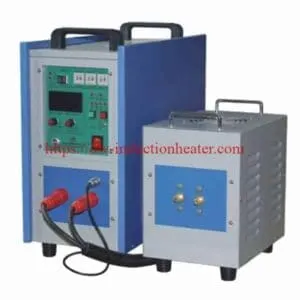
The HLQ DW-HF-25KW-B(A) is a three-phase high-frequency induction heating system designed for industrial brazing, surface hardening, annealing, shrink fitting, soldering, and localized metal heating. The original product page specifies a maximum oscillating-power rating of 25kVA, an operating frequency of 30–80kHz, and a three-phase 380V, 50/60Hz electrical supply. The equipment features a separate main power unit and extension unit, allowing flexible installation in industrial heating stations.
Best-Fit Applications: Copper tube brazing, HVAC fittings, carbide tool brazing, small shaft hardening, selected gear surface hardening, stainless steel heating, bearing assembly, annealing, and localized preheating.
Engineering Selection: The appropriate induction heating equipment must be selected according to workpiece material, effective heated mass, target temperature, required cycle time, operating frequency, induction coil design, and cooling requirements. The published 25kVA rating should not be interpreted as a guaranteed 25kW of useful heat delivered to the workpiece.
Table of Contents
- What is the DW-HF-25kW High Frequency Induction Heating Equipment?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages and Limitations
- Why Choose HLQ?
- 10 Core FAQs
What is the DW-HF-25kW High Frequency Induction Heating Equipment?
The DW-HF-25kW High Frequency Induction Heating Equipment is an industrial electromagnetic heating system developed for rapid, localized heating of electrically conductive metal components.
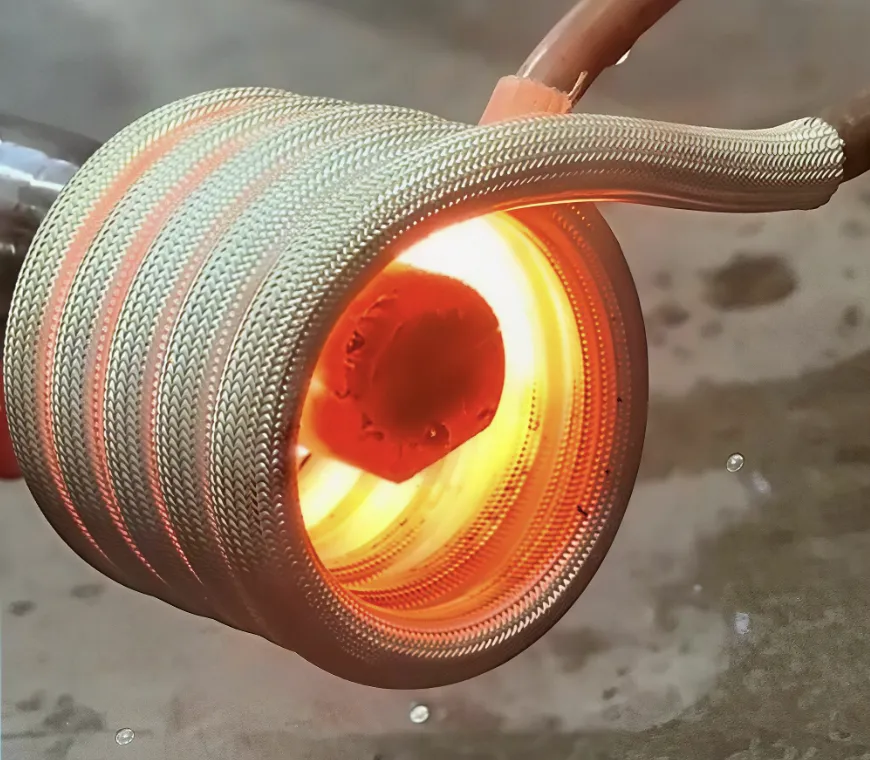
It converts incoming three-phase electrical power into high-frequency alternating current. When this current flows through an induction coil, it produces a changing magnetic field that induces electrical currents inside a nearby conductive workpiece.
The resistance of the metal converts the induced currents into heat. Depending on the application, this heat can be used for brazing, hardening, annealing, thermal expansion, or other industrial processes.
Unlike conventional resistance furnaces, induction heating does not necessarily require the entire component to be heated. An appropriately designed coil can concentrate useful heating in the selected region.
The DW-HF-25 series is particularly relevant to manufacturing workshops and production cells that require controlled heating of small and medium-sized metal components.
Main Components of the DW-HF-25 Induction Heating System
| Component | Function | Engineering Requirement |
|---|---|---|
| Main Power Unit | Converts electrical input into controlled high-frequency power | Correct supply voltage, rated load, and protection |
| Extension Unit | Provides a separate heating-head or transformer arrangement | Compatible electrical connection and cooling |
| Inverter Circuit | Generates alternating current at the operating frequency | Appropriate semiconductor and control configuration |
| Resonant Matching Circuit | Matches the induction load to the power stage | Compatible coil inductance and operating frequency |
| Induction Coil | Generates the alternating magnetic field | Application-specific geometry and cooling |
| Heating Control | Adjusts operating parameters | Control functions must match the process |
| Cooling Circuit | Removes waste heat from designated equipment components | Specified water flow, pressure, temperature, and quality |
| Protection System | Monitors selected electrical and cooling faults | Verified alarms and safe shutdown functions |

Advantages of the Split-Type Construction
The separated equipment arrangement allows the main power unit to be positioned away from the immediate heating area while the smaller extension unit is installed closer to the workpiece.
This arrangement can be beneficial in production environments where heating equipment must be integrated into a workbench, fixture, or manufacturing station.
| Feature | Potential Benefit | Engineering Consideration |
|---|---|---|
| Separate Main Unit | Flexible equipment positioning | Electrical access and ventilation |
| Compact Extension Unit | Can be installed closer to the heating station | Mechanical support and operating clearance |
| Interconnecting Cable | Allows separation between units | Electrical matching and approved cable length |
| Interchangeable Coils | Supports different heating applications | Each coil must be electrically compatible |
| Production Integration | Facilitates installation in selected manufacturing cells | Requires suitable fixture and control design |
Key Applications
The DW-HF-25 high-frequency induction heater can be considered for several industrial metal-heating processes.
Each application requires a suitable induction coil, heating temperature, operating frequency, and production procedure.
1. Induction Brazing of Copper Tubes
Induction heating is widely used to raise copper tube joints and compatible fittings to the temperature required for brazing.
The induction coil should heat the joint sufficiently for the selected filler metal to melt, wet the joining surfaces, and flow through the joint clearance.
Typical applications include HVAC refrigeration pipes, air-conditioning copper tubing, heat exchanger connections, and industrial pipe fittings.
Joint preparation, filler selection, and the heating profile are essential for reliable brazing quality.
2. Carbide Tool Brazing
Induction brazing can be used to attach suitable carbide cutting tips to steel holders.
Localized heating allows the brazing region to reach the required temperature while limiting unnecessary heating of surrounding material.
The final process must control joint clearance, filler metal, thermal expansion, and cooling conditions.
3. Steel Shaft Surface Hardening
For suitable carbon and alloy steels, induction heating can rapidly raise selected surface regions to the required austenitizing temperature.
The heated region is then quenched according to an approved heat-treatment procedure.
Final surface hardness and hardened case depth depend on the steel grade, operating frequency, heating time, temperature distribution, and quenching conditions.
4. Gear and Sprocket Hardening
Small gears and sprockets may be heated with appropriately designed induction coils.
Depending on the required hardening pattern, the system may use a circular coil, scanning arrangement, or special-profile inductor.
The heating process should be validated for the specified tooth geometry and hardened depth.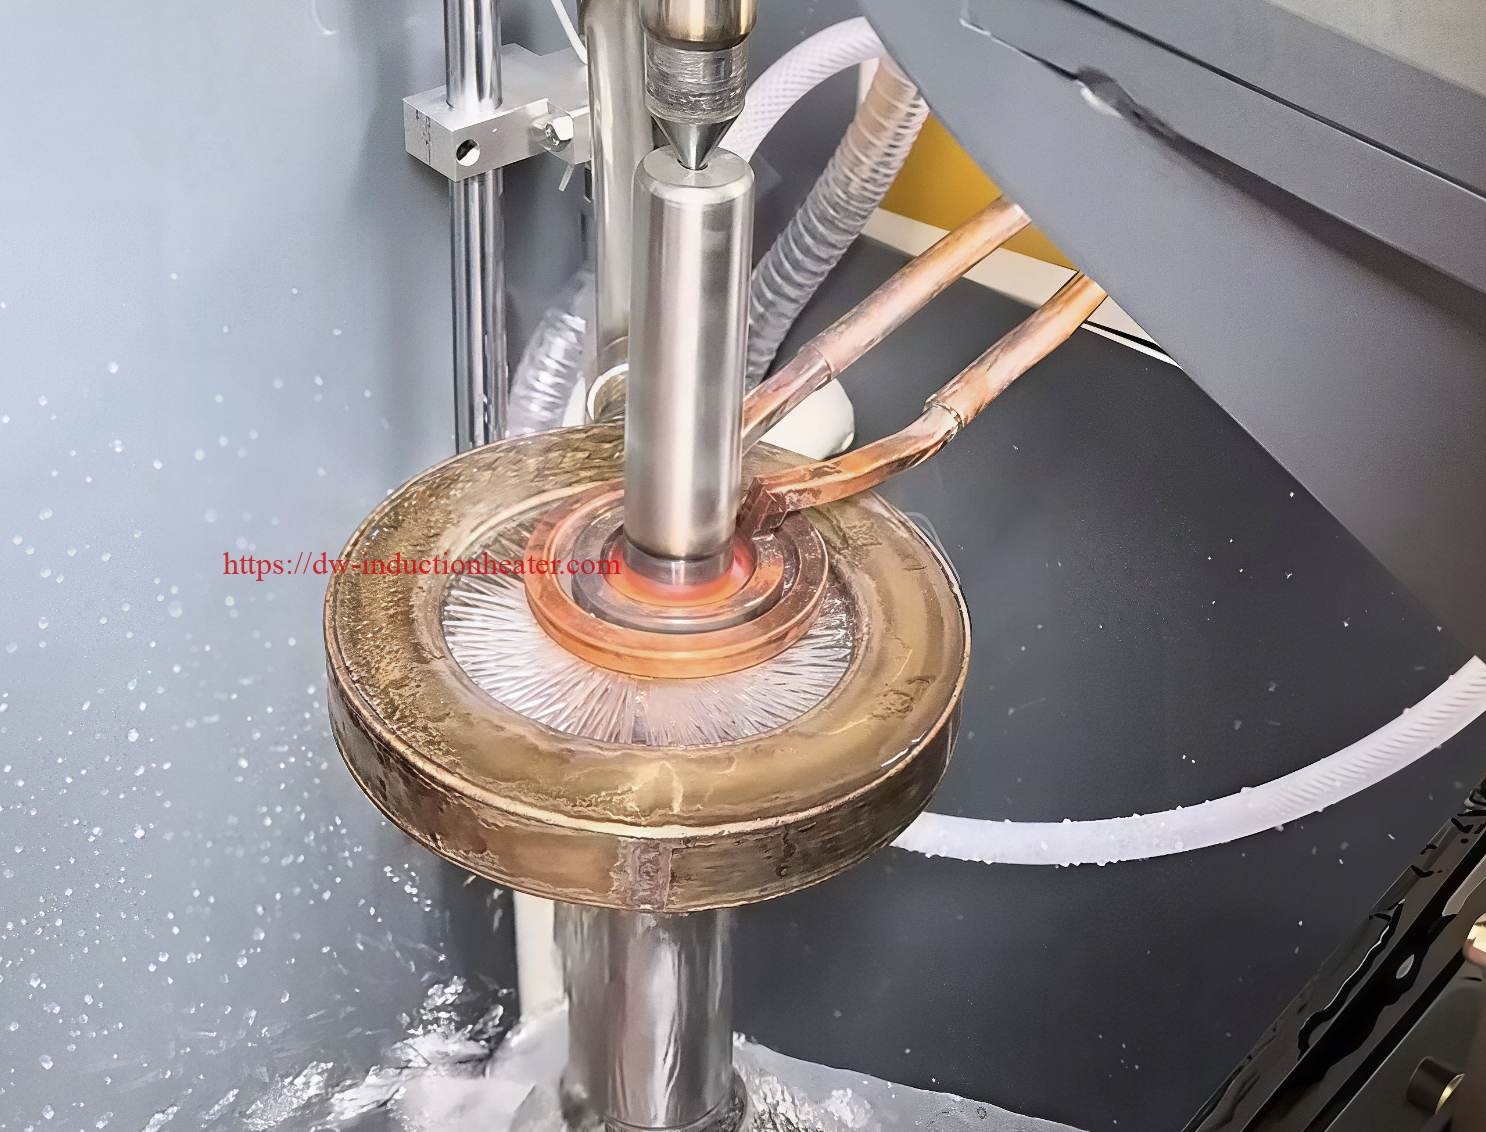
5. Induction Annealing
The machine may be used for selected annealing and localized heat-treatment applications involving steel, copper, brass, and stainless steel components.
The required heating temperature, holding time, and cooling conditions depend on the material and metallurgical objective.
6. Induction Shrink Fitting
Induction heating can produce controlled thermal expansion of steel rings, gears, sleeves, and similar components before assembly.
The temperature must be selected according to the required expansion, material properties, and permissible component temperature.
7. Localized Industrial Preheating
The system may be used for local heating before joining, forming, mechanical assembly, or selected coating operations.
The suitability of the DW-HF-25 depends on the heated area, required temperature, and production cycle.
| Application | Material | Typical Coil | Process Objective |
|---|---|---|---|
| Copper Tube Brazing | Copper and brass | Helical or U-shaped | Heat the joint for filler metal flow |
| HVAC Fitting Brazing | Copper and compatible alloys | Split or custom-profile | Produce repeatable brazed joints |
| Carbide Tool Brazing | Steel and tungsten carbide | Pancake or profile | Controlled heating of the brazing interface |
| Small Shaft Hardening | Carbon and alloy steel | Encircling or scanning | Localized surface austenitizing |
| Gear Hardening | Suitable gear steel | Profile or scanning | Heat specified tooth regions |
| Annealing | Copper, brass, selected steels | Helical or tunnel | Provide the required thermal cycle |
| Shrink Fitting | Steel rings and sleeves | Encircling | Produce controlled thermal expansion |
| Localized Preheating | Conductive metal components | Application-specific | Heat a selected processing region |
For application-specific joints and tooling, explore HLQ’s custom induction brazing coils and their engineering design considerations.
Suitable Materials
High-frequency induction heating can be applied to a wide range of electrically conductive materials.
However, each material responds differently because electrical resistivity, magnetic permeability, thermal conductivity, and heat capacity vary with material composition and temperature.
| Material | Typical Application | Heating Characteristics | Engineering Requirement |
|---|---|---|---|
| Carbon Steel | Surface hardening, shrink fitting, preheating | Magnetic behavior changes with temperature | Consider the Curie transition and required heating depth |
| Alloy Steel | Tool heating and localized hardening | Material properties depend on alloy composition | Use grade-specific heat-treatment requirements |
| Stainless Steel | Brazing, annealing, preheating | Electromagnetic properties vary with grade | Verify actual stainless steel composition |
| Copper | Tube brazing and electrical connectors | High electrical and thermal conductivity | Optimize coil coupling and heating time |
| Brass | Valves, fittings, connectors | Conductive copper-zinc alloy | Control temperature and zinc-related process risks |
| Aluminum | Selected localized heating operations | Nonferromagnetic and highly conductive | Verify sufficient coupling and prevent overheating |
| Carbide-Steel Assemblies | Cutting-tool brazing | Dissimilar electromagnetic and thermal properties | Control joint temperature and thermal stress |
Material Properties Affecting Induction Heating
| Property | Influence on Heating | Selection Consideration |
|---|---|---|
| Electrical Resistivity | Affects induced electrical losses | Use values appropriate to the operating temperature |
| Magnetic Permeability | Affects induced current distribution | Consider changes in ferromagnetic materials |
| Thermal Conductivity | Influences temperature distribution | Evaluate local and bulk heating requirements |
| Specific Heat Capacity | Determines thermal energy demand | Use suitable material data |
| Workpiece Geometry | Changes coupling and effective heated mass | Match the induction coil to the workpiece |
| Initial Temperature | Changes total temperature rise | Account for actual starting conditions |
| Heating Duration | Influences heat conduction and final temperature profile | Verify the required process cycle |
Working Principle
The DW-HF-25 operates according to electromagnetic induction.
The induction power supply converts incoming three-phase electrical power into alternating current at the selected high-frequency operating point.
The alternating current flows through an induction coil, producing a changing magnetic field around the conductive workpiece.
Electrical currents are induced in the workpiece. Their resistance generates heat within the metal.
The resulting temperature distribution depends on the induction frequency, coil geometry, coupling distance, material properties, and heating time.
High Frequency Induction Heating Process
| Step | Component | Function |
|---|---|---|
| 1 | Three-Phase Electrical Supply | Provides electrical input energy |
| 2 | Power Conversion Circuit | Converts electrical input into controlled high-frequency output |
| 3 | Resonant Matching Circuit | Matches the induction load to the power stage |
| 4 | Induction Heating Coil | Generates the changing magnetic field |
| 5 | Conductive Workpiece | Absorbs electromagnetic energy and generates heat |
| 6 | Heating Controller | Adjusts the selected operating parameters |
| 7 | Cooling System | Removes waste heat from designated system components |
Induction Frequency and Heating Depth
Operating frequency influences the distribution of induced electrical current inside the metal.
Under simplified conditions, increasing the frequency reduces the reference electrical skin depth.
However, the final temperature penetration depth also depends on heating duration, thermal conductivity, material geometry, and temperature-dependent electromagnetic properties.
The electrical skin depth can be estimated from:
δ = √[ρ / (π × f × μ)]
Where:
- δ = Reference electrical skin depth, m.
- ρ = Electrical resistivity, Ω·m.
- f = Operating frequency, Hz.
- μ = Absolute magnetic permeability, H/m.
Important: Electrical skin depth is not identical to the final temperature penetration depth or hardened case depth.
The original DW-HF-25 page lists an operating frequency of 30–80kHz. Other HLQ product literature lists a wider legacy range for certain DW-HF-25 variants. Final frequency must be confirmed for the specific machine and induction load.
Induction Coil Design
The coil is one of the most important components of an induction heating system.
Its geometry, number of turns, active length, electrical connections, and coupling distance influence electromagnetic heating performance.
For brazing, the coil should provide suitable heating around the joint.
For hardening, the coil should produce the required surface temperature distribution before quenching.
For shrink fitting, heating should provide sufficient and reasonably uniform thermal expansion.
| Application | Recommended Coil Concept | Primary Design Requirement |
|---|---|---|
| Copper Tube Brazing | Helical or U-shaped | Heat distribution around the joint |
| Carbide Tool Brazing | Pancake or custom-profile | Controlled brazing-interface temperature |
| Small Shaft Hardening | Encircling or scanning | Required surface-heating pattern |
| Gear Hardening | Profile or scanning coil | Tooth geometry and hardening-zone control |
| Annealing | Helical or tunnel | Correct thermal-cycle coverage |
| Shrink Fitting | Encircling or specialized coil | Controlled component expansion |
For detailed inductor development, refer to HLQ’s custom induction heating coil design engineering guide.

Technical Specifications
The following technical specifications are based on the original HLQ DW-HF-25 product page.
Some parameters differ from information published on other HLQ pages. Such discrepancies should be resolved in the final equipment datasheet.
DW-HF-25KW-B(A) Technical Specifications
| Parameter | Specification | Notes |
|---|---|---|
| Model | DW-HF-25KW-B(A) | Manufacturer-published designation |
| Equipment Category | High Frequency Induction Heating Equipment | Localized industrial metal heating |
| Input Voltage | 3-Phase 380V | Confirm permitted voltage tolerance |
| Input Frequency | 50/60Hz | Industrial electrical supply |
| Maximum Oscillating Power | 25kVA | Manufacturer-published value |
| Oscillation Frequency | 30–80kHz | Target-page operating-frequency range |
| Published Duty Cycle | 100% at 30°C | Another HLQ page states 80% at 30°C |
| Main Unit Dimensions | 550 × 240 × 485mm | Manufacturer-published dimensions |
| Extension Unit Dimensions | 340 × 205 × 340mm | Manufacturer-published dimensions |
| Published Weight | 55kg | Confirm net or total assembly weight |
| Interconnecting Cable | 2m | Longer cables require electrical matching review |
| Cooling Method | Water Cooling | Flow and pressure not fully published |
| Control Functions | Constant-current or constant-power operation described | Confirm actual supplied controller |
| Timer Functions | Available on timer configuration | Confirm standard or optional status |
| Electrical Protection | Overcurrent, voltage, phase, cooling and load-related alarms described | Verify actual interlock implementation |
| Induction Coil | Application-specific | Matched to generator and workpiece |
| Cooling Water Flow | Not specified on the target page | Request formal equipment requirement |
| Cooling Water Pressure | Not specified on the target page | Request permitted operating range |
Specification Verification Requirements
| Parameter | Published Information | Required Verification |
|---|---|---|
| Power Rating | 25kVA maximum oscillating power | Confirm input active power and output-rating definition |
| Operating Frequency | 30–80kHz; older source states 20–80kHz | Confirm actual inverter configuration |
| Duty Cycle | 100% at 30°C; another page states 80% at 30°C | Confirm continuous operating conditions |
| A/B Model Difference | Both designations shown | Clarify structural and control differences |
| Power Semiconductor | IGBT technology described; older literature mentions earlier semiconductor configurations | Confirm the supplied power-stage version |
| Cooling Requirements | Detailed figures not published | Confirm water flow, pressure, temperature and quality |
| Production Capacity | No universal kg/h or pieces/hour rating | Verify through application testing |
Recommended Model Selection
The appropriate induction heating equipment should be selected according to the material, effective heated mass, heating-zone dimensions, target temperature, and required cycle time.
The DW-HF-25 can be considered for small and medium localized heating applications. Larger or heavier components may require a higher-power system or a different operating frequency.
| Application | Material | Recommended Power Class | Frequency | Engineering Note |
|---|---|---|---|---|
| Small Copper Tube Brazing | Copper | DW-HF-15 / DW-HF-25 | Application-specific | Compare joint mass and required heating time |
| Medium Copper Joint Brazing | Copper and brass | DW-HF-25 candidate | Within verified loaded range | Check filler metal and joint geometry |
| Carbide Tool Brazing | Steel and carbide | DW-HF-25 candidate | Joint-specific | Control thermal stress and filler flow |
| Small Shaft Hardening | Carbon or alloy steel | DW-HF-25 candidate | Selected according to hardening requirements | Verify case depth and quenching |
| Medium Shaft Heating | Steel | DW-HF-35 or higher-power alternative | Load-dependent | Calculate heated mass and required cycle |
| Localized Annealing | Copper, brass, stainless steel | DW-HF-25 candidate | Material-dependent | Validate the required thermal cycle |
| Thermal Shrink Fitting | Steel rings and sleeves | DW-HF-25 candidate | Application-specific | Calculate thermal expansion requirement |
Selection Note: These are preliminary engineering recommendations. The manufacturer does not publish a universal workpiece-size or heating-time guarantee for the DW-HF-25.
For comparison with other power levels, refer to HLQ’s high frequency induction heating power supply product series.
Process Workflow
The industrial induction heating process requires correct workpiece preparation, induction coil selection, electrical matching, heating control, and final quality verification.
General Induction Heating Process
| Step | Operation | Engineering Objective |
|---|---|---|
| 1 | Material Inspection | Confirm workpiece material and dimensions |
| 2 | Process Preparation | Prepare surfaces and fixtures according to the application |
| 3 | Coil Selection | Choose a compatible induction coil |
| 4 | Cooling Inspection | Verify coolant flow and temperature |
| 5 | Electrical Inspection | Confirm supply and protection conditions |
| 6 | Workpiece Positioning | Maintain the required coil-to-workpiece relationship |
| 7 | Induction Heating | Apply the selected heating cycle |
| 8 | Temperature Verification | Check the required process temperature |
| 9 | Process Completion | Complete brazing, quenching, annealing or assembly |
| 10 | Quality Inspection | Verify the required product characteristics |
Induction Brazing Process
For brazing, the process involves cleaning the base materials, assembling the joint, positioning a suitable filler metal, applying induction heat, allowing filler-metal flow, and inspecting the completed joint.
The heating process must bring the joint surfaces to the required brazing temperature without intentionally melting the base materials.
Induction Hardening Process
For induction hardening, suitable steel components are heated to the required austenitizing condition and then quenched according to the metallurgical process.
Final hardness and case depth must be verified by appropriate inspection or testing.
For specialized surface-heating components, review HLQ’s induction hardening coil for steel surface hardening solutions.
Cooling System Requirements
The DW-HF-25 is a water-cooled induction heating system.
The complete cooling circuit should provide sufficient heat removal from the induction coil and designated electrical components.
| Parameter | Requirement | Verification |
|---|---|---|
| Cooling Method | Water cooling | Confirm approved system configuration |
| Cooling Water Flow | Manufacturer-specified minimum | Measure actual flow |
| Water Pressure | Manufacturer-specified range | Verify inlet and differential pressure |
| Water Temperature | Within approved operating limits | Measure inlet and return temperatures |
| Water Quality | Compatible with the cooling circuit | Control scale, corrosion and contamination |
| Cooling Connections | Correctly installed and leak-free | Inspect hoses and connections |
| Water-Flow Protection | Required safe operating interlock | Verify protection response |
| Heat Rejection | Matched to total equipment losses | Size the cooling equipment appropriately |
Common Problems and Solutions
High-frequency induction heating performance may be affected by electrical matching, coil design, workpiece positioning, cooling conditions and operating parameters.
| Problem | Possible Cause | Recommended Solution |
|---|---|---|
| Slow Heating | Poor coupling, unsuitable coil or insufficient useful power | Verify coil design and loaded power |
| Uneven Heating | Incorrect coil geometry or positioning | Improve alignment and heating-zone design |
| Excessive Local Heating | Field concentration or excessive heating duration | Review coil geometry and heating parameters |
| Insufficient Joint Temperature | Inadequate power transfer or heating time | Verify loaded power and joint temperature |
| Poor Brazing Filler Flow | Incorrect filler, contamination or inadequate heating | Check filler compatibility and joint preparation |
| Hardening Variation | Temperature variation or inconsistent quenching | Validate the complete hardening process |
| Cooling Alarm | Low water flow, blockage or excessive temperature | Stop heating and inspect the cooling circuit |
| Overcurrent Alarm | Electrical mismatch or component fault | Isolate the equipment and conduct qualified inspection |
| Coil Overheating | Insufficient cooling or excessive electrical losses | Verify water flow and current conditions |
| Unstable Frequency | Changing load or resonant matching problem | Verify coil and matching-network compatibility |
| Frequent Shutdown | Electrical, cooling or protection fault | Record fault information and investigate safely |
Engineering Selection Guide
Correct equipment selection begins with the workpiece and its heating requirements.
The power supply, induction coil and production process must be engineered together.
Step 1: Identify the Workpiece Material
Specify the material grade, electrical and thermal properties, and any relevant metallurgical requirements.
Step 2: Determine Workpiece Dimensions
Provide the complete dimensions, weight and required heating zone.
The effective heated mass may differ from the total component mass when only a localized region is heated.
Step 3: Define the Required Temperature
Specify the initial temperature and target process temperature.
For brazing, the required temperature depends on the selected filler metal. For hardening, the required temperature depends on the steel grade and treatment process.
Step 4: Calculate Theoretical Heating Energy
For a simplified sensible-heating calculation:
Q = m × Cp × ΔT
Where:
- Q = Thermal energy, kJ.
- m = Effective heated mass, kg.
- Cp = Approximate mean specific heat capacity, kJ/kg·K.
- ΔT = Temperature increase, K.
Step 5: Engineering Calculation Example
Consider an illustrative copper joint assembly with an effective heated mass of 0.25kg.
Assume the joint is heated from 25°C to 725°C, using an approximate mean specific heat capacity of 0.42kJ/kg·K.
The theoretical thermal energy is:
Q = 0.25 × 0.42 × 700 = 73.5kJ
This is equivalent to approximately 0.0204kWh of useful thermal energy.
| Parameter | Value | Data Status |
|---|---|---|
| Material | Copper | Illustrative example |
| Effective Heated Mass | 0.25kg | Assumed |
| Initial Temperature | 25°C | Assumed |
| Target Temperature | 725°C | Assumed |
| Temperature Increase | 700K | Calculated |
| Mean Specific Heat | 0.42kJ/kg·K | Approximate assumption |
| Theoretical Thermal Energy | 73.5kJ | Calculated |
| Equivalent Thermal Energy | 0.0204kWh | Calculated |
Step 6: Heating Time and Power Relationship
For the same theoretical thermal energy, the required average useful thermal power increases as the heating time decreases.
| Heating Time | Useful Thermal Power | Estimated Electrical Input at Assumed 50% Efficiency |
|---|---|---|
| 8 seconds | 9.19kW | 18.38kW |
| 10 seconds | 7.35kW | 14.70kW |
| 15 seconds | 4.90kW | 9.80kW |
| 20 seconds | 3.68kW | 7.35kW |
| 30 seconds | 2.45kW | 4.90kW |
| 45 seconds | 1.63kW | 3.27kW |
Engineering Qualification: These values are theoretical estimates, not measured DW-HF-25 performance. They do not establish that the machine can deliver a particular heating cycle. The assumed 50% electrical-to-workpiece efficiency is for comparison only.
The published 25kVA maximum oscillating-power rating must not be directly compared with the calculated useful thermal power without establishing the actual power-rating definition.
Step 7: Evaluate Coil Geometry
Select a coil that matches the workpiece dimensions, heating-zone shape, electrical matching requirements and available mechanical clearance.
Step 8: Confirm Electrical Requirements
Verify the three-phase power supply, full-load input current, power factor, voltage tolerance and electrical protection.
Step 9: Confirm Cooling Requirements
Obtain the manufacturer’s required water flow, inlet pressure, temperature limits, water quality and cooling protection requirements.
Step 10: Validate the Application
For industrial production, perform a representative application test using the actual material and workpiece geometry.
Record heating time, temperature, loaded frequency, input power, cooling conditions and applicable quality results.
Published HLQ Brazing Application Reference
HLQ has published a separate induction brazing application involving copper tubing and a DW-UHF-10kW induction system.
The reported test used heavy-wall 5/16-inch copper tubing and an available split laboratory coil. The brazing alloy flowed after approximately 5.0–5.2 seconds of heating, with a reported temperature reference of approximately 815°C.
| Parameter | Published Information | Important Qualification |
|---|---|---|
| Application | Copper tube brazing | Related induction heating application |
| Equipment | DW-UHF-10kW | Not a DW-HF-25 test |
| Tube Material | Copper | Heavy-wall 5/16-inch test tubing |
| Coil Type | Split laboratory coil | Production design may differ |
| Reported Temperature | Approximately 815°C | Reported test reference |
| Reported Heating Time | Approximately 5.0–5.2 seconds | Specific laboratory test only |
| Brazing Material | 505 alloy brazing paste | As reported in the application |
| DW-HF-25 Performance | Not measured in this test | Separate validation required |
This example illustrates the importance of coil design, joint preparation and heating-cycle control.
It does not establish that a DW-HF-25 will reproduce the same heating time.
For the original test details, review the induction brazing copper tubing case study.
Recommended Factory Acceptance Test
| Test Item | Verification Method | Acceptance Basis |
|---|---|---|
| Input Voltage | Measure actual three-phase voltage | Approved electrical limits |
| Input Current | Measure during representative heating | Approved full-load rating |
| Output Rating | Verify according to manufacturer test method | Agreed rated performance |
| Operating Frequency | Record actual loaded frequency | Approved operating range |
| Heating Time | Record representative cycles | Agreed process duration |
| Workpiece Temperature | Use a suitable calibrated measurement method | Required temperature range |
| Coil Compatibility | Verify stable operation and mechanical clearance | Approved coil and workpiece combination |
| Cooling Flow | Measure actual coolant flow | Manufacturer-specified minimum |
| Cooling Temperature | Measure inlet and return temperatures | Approved operating limits |
| Protection Functions | Test specified alarms and interlocks | Safe fault response |
| Process Quality | Perform application-specific inspection | Agreed brazing, hardness or dimensional requirements |
Advantages and Limitations
Advantages of DW-HF-25 High Frequency Induction Heating Equipment
| Advantage | Engineering Benefit |
|---|---|
| Localized Heating | Allows selected workpiece regions to be heated |
| High-Frequency Operation | Suitable for selected surface and localized heating processes |
| Split-Type Construction | Provides flexibility in equipment installation |
| Adjustable Heating Control | Supports controlled heating cycles |
| Interchangeable Coils | Allows different compatible workpiece configurations |
| No Direct Burner Flame | Eliminates the need for direct combustion at the heating station |
| Production Integration | Can be incorporated into suitable manufacturing cells |
| Repeatable Operating Cycles | Supports consistency when process conditions are controlled |
| Application Flexibility | Can be considered for brazing, hardening, annealing and shrink fitting |
Limitations and Engineering Considerations
| Limitation | Engineering Consideration |
|---|---|
| Power Capacity | Large or heavy workpieces may require higher-power equipment |
| Workpiece-Specific Coil | Different parts may require dedicated induction coils |
| Electrical Supply | Requires a suitable three-phase industrial supply |
| Cooling Requirements | Water-cooled components require reliable circulation |
| Frequency Range | Exact operating frequency depends on electrical load |
| Continuous Operation | Duty-cycle claims require verification under defined conditions |
| Heating Uniformity | Large components may require additional heating time |
| Temperature Control | Precision applications may require calibrated external sensors |
| Melting Capacity | No universal metal-melting capacity is established |
| Process Validation | Critical applications require representative testing |
Why Choose HLQ?
HLQ Induction Equipment Co., Ltd. provides industrial induction heating equipment for brazing, hardening, annealing, forging, melting and other metalworking applications.
The DW-HF-25 series offers a split-type high-frequency heating arrangement for suitable industrial workstations.
Application-Based Equipment Selection
Equipment selection can be based on material properties, workpiece dimensions, heating temperature, required production rate and available electrical supply.
High-Frequency Induction Power Supply
The DW-HF series includes different power classes for localized industrial heating applications.
The appropriate generator should be selected according to the actual load and process conditions.
Custom Induction Coil Design
Different workpieces may require different induction coil geometries.
Coil design should account for the operating frequency, electrical matching, coupling distance, cooling and mechanical clearance.
Industrial Heating Applications
The equipment can be evaluated for copper tube brazing, carbide tool joining, suitable steel hardening, annealing, and thermal assembly.
Engineering Testing
For production applications, representative heating tests help verify the required cycle time, temperature distribution and process quality.
10 Core FAQs
1. What is the DW-HF-25 high frequency induction heater?
The DW-HF-25 is an industrial high-frequency induction heating system designed for localized heating of electrically conductive metal components. Typical applications include brazing, surface hardening, annealing, shrink fitting and preheating.
2. What is the rated power of the DW-HF-25?
The original product page lists a maximum oscillating-power rating of 25kVA. The actual input active power, output power and useful heating power should be confirmed for the supplied configuration.
3. What electrical supply does the DW-HF-25 require?
The target product page specifies three-phase 380V, 50/60Hz electrical input. Exact voltage tolerance, full-load input current and protection requirements must be verified before installation.
4. What is the operating frequency?
The target page lists 30–80kHz. Other legacy HLQ information includes a 20–80kHz range for certain DW-HF-25 configurations. The actual frequency range should be confirmed from the specific equipment datasheet.
5. Can the DW-HF-25 braze copper tubes?
Yes, it can be considered for suitable copper tube and fitting brazing applications. Actual performance depends on tube dimensions, joint mass, filler metal, coil design and required heating time.
6. Can the DW-HF-25 harden steel shafts?
It can be considered for localized hardening of suitable steel components. The achievable hardness and case depth depend on steel composition, operating frequency, heating time, temperature distribution and quenching.
7. Does the DW-HF-25 require cooling water?
Yes. The equipment uses water cooling for designated electrical and induction coil components. Water flow, pressure, temperature and quality requirements must be confirmed for the actual configuration.
8. Can the DW-HF-25 operate continuously?
The target product page claims 100% duty at 30°C, while another HLQ product page lists 80% duty at 30°C. The continuous-duty capability must therefore be verified under defined electrical, cooling and ambient conditions.
9. Can different induction coils be used with the machine?
Yes, compatible induction coils may be used for different workpieces and applications. Each coil must satisfy the electrical matching, mechanical clearance and cooling requirements of the heating system.
10. How is the correct induction heating machine selected?
The correct machine is selected according to the material, workpiece dimensions, effective heated mass, target temperature, required heating time, operating frequency, available electrical supply and cooling conditions. Engineering calculations and representative application tests provide the basis for final selection.
HLQ-DW-HF-25-high-frequency-induction-heating-equipment-brochure