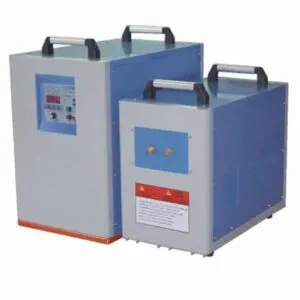
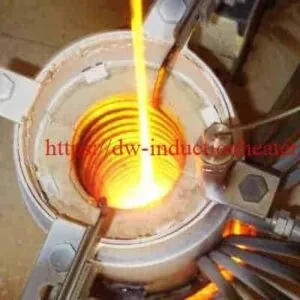
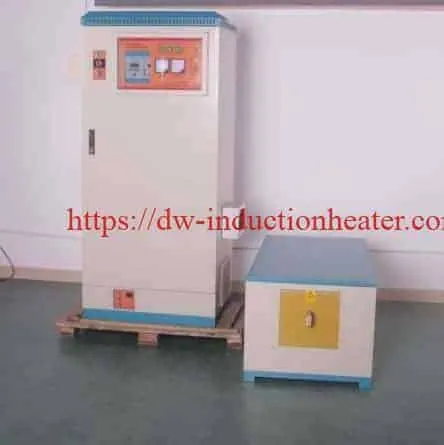
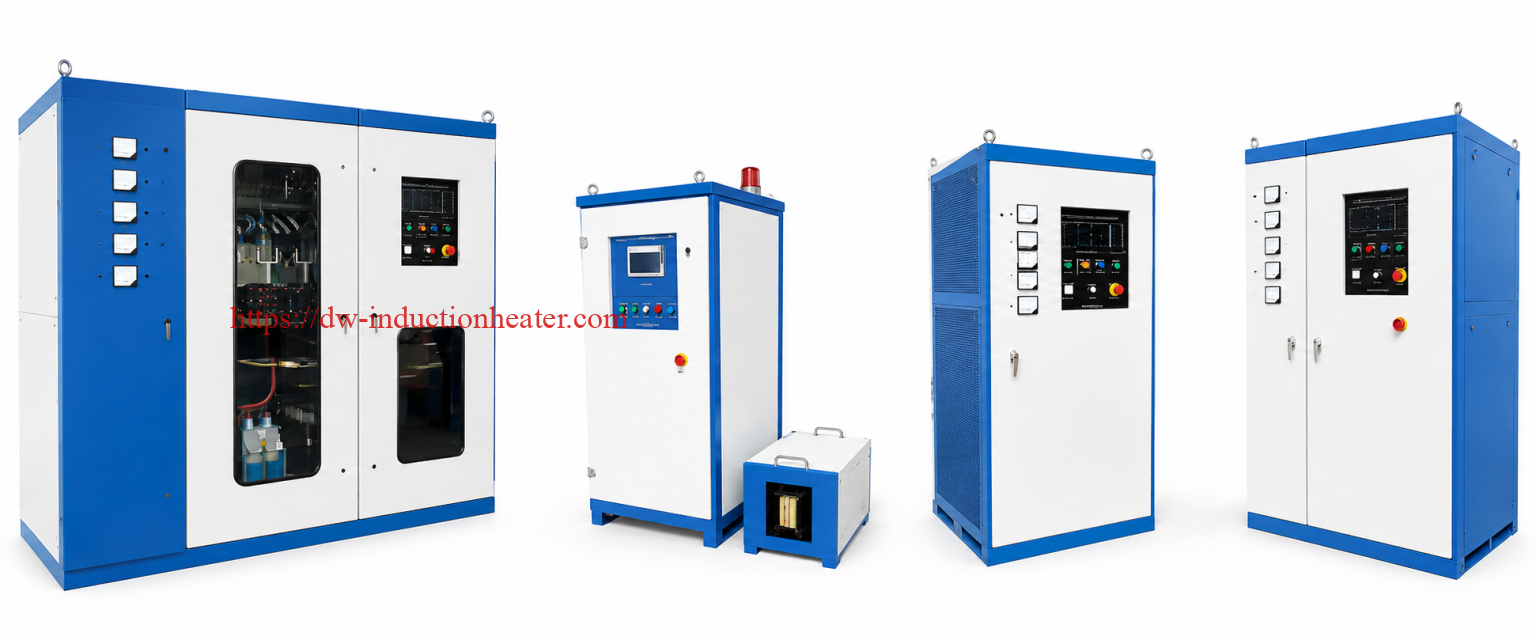
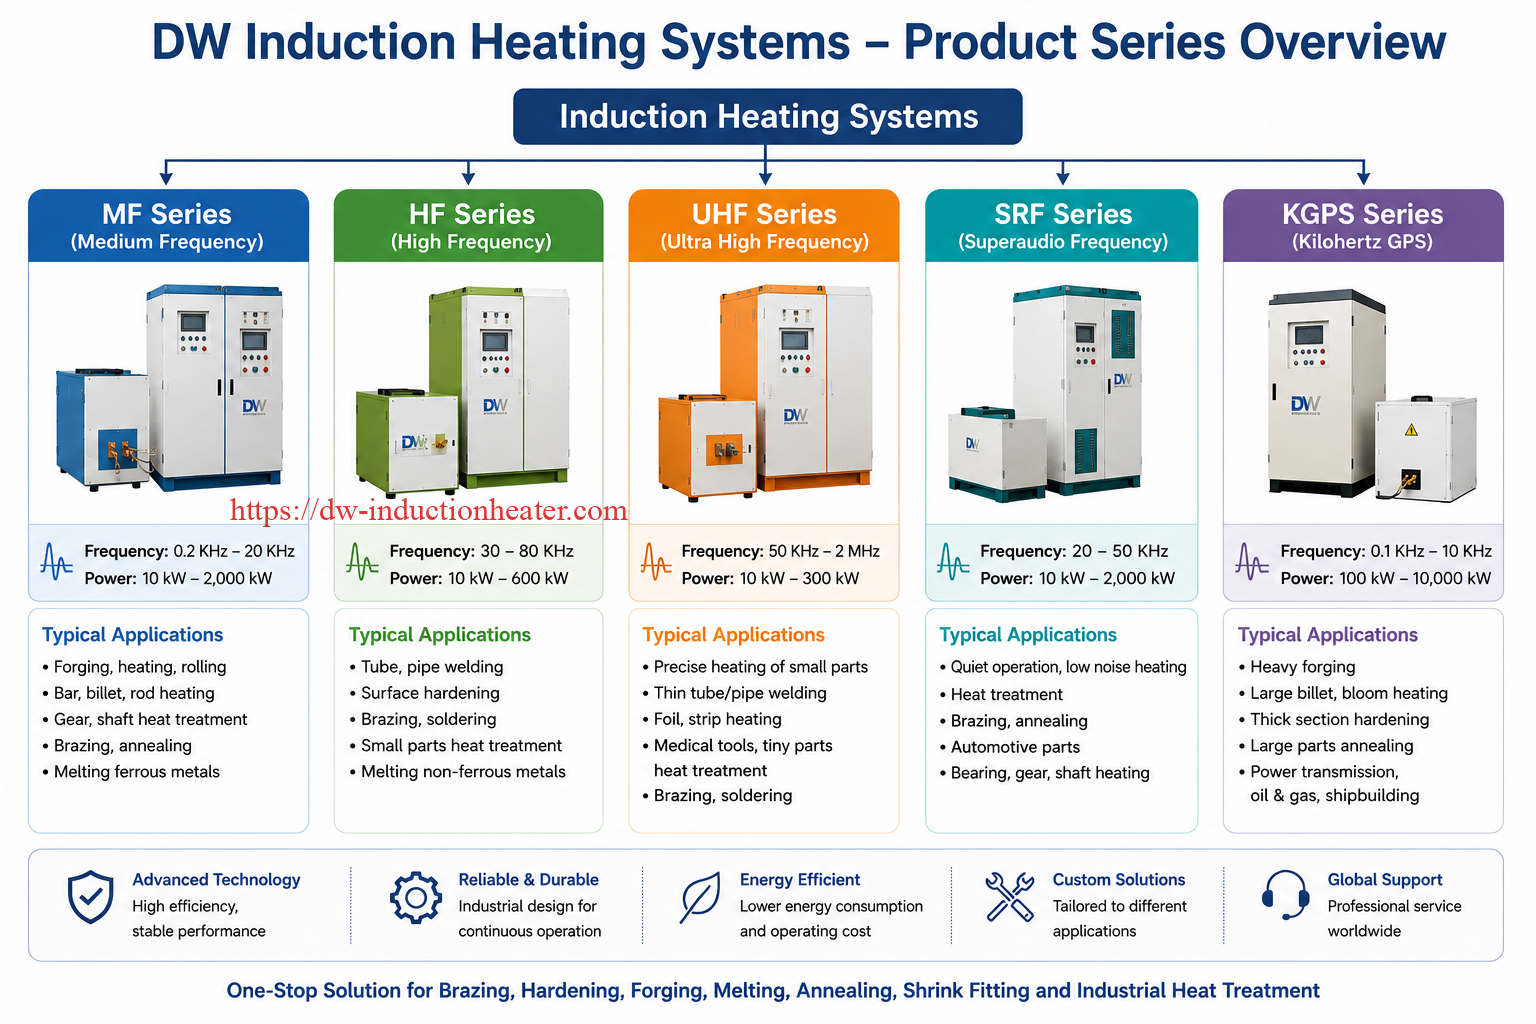
HLQ induction heating power supplies cover a complete range of industrial induction generators, including MF medium frequency series, HF high frequency series, UHF ultra high frequency series, SRF superaudio frequency series and KGPS induction generator series. These power supplies are designed for brazing, hardening, forging, melting, annealing, shrink fitting, bonding, soldering, welding preheating and industrial heat treatment. With available frequency ranges from low kHz to MHz level and power ratings from compact precision units to heavy-duty furnace generators, HLQ provides suitable induction power solutions for small parts, medium components, large billets, melting furnaces and automated production lines.
Quick Answer
An induction heating power supply is the core generator of an induction heating system. It converts industrial AC electricity into controlled medium-frequency power supplies, high-frequency, ultra-high-frequency, superaudio-frequency or KGPS furnace power output. This output energizes an induction coil, creates an alternating magnetic field and generates heat directly inside conductive metal workpieces. HLQ supplies MF, HF, UHF, SRF and KGPS induction heating power supplies for different heating depths, workpiece sizes, production speeds and industrial applications.
Product Series Overview
Series
Full Name
Typical Frequency Range
Typical Power Range
Best-Fit Applications
Main Advantage
MF Series
Medium Frequency Induction Power Supply
0.2kHz–20kHz
15kW–2000kW
Billet heating, forging, melting, deep hardening, bar heating, rod heating.
Deep heat penetration and strong through-heating capability.
Fast localized heating with good process flexibility.
UHF Series
Ultra High Frequency Induction Power Supply
50kHz–2.0MHz
4.5kW–600kW
Precision brazing, micro soldering, fine parts heating, electronic components.
Very shallow, accurate and fast localized heating.
SRF Series
Superaudio Frequency Induction Heating System
20kHz–50kHz
30kW–2000kW
Billet heating, auto parts heat treatment, medium-depth hardening, forging preheating.
Balanced heating depth between MF and HF, suitable for many heat treatment processes.
KGPS Series
KGPS Induction Generator Power Supply
Medium frequency furnace range, customizable by furnace design
Usually medium to high power, customizable
Induction melting furnace, forging furnace, industrial heating furnace, metal smelting.
Traditional robust furnace power supply for melting and heavy heating applications.
What Is an Induction Heating Power Supply?
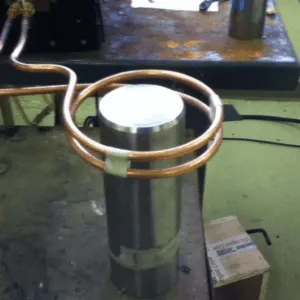
An induction heating power supply, also called an induction generator, induction inverter, induction power source or induction heating generator, is the electrical core of an induction heating machine. It converts input power into a controlled alternating current with a selected frequency. The current flows through a copper induction coil and produces a magnetic field. When a metal workpiece is placed inside or near the coil, eddy currents are induced inside the metal and generate heat directly within the workpiece.
The correct power supply series determines heating speed, heating depth, temperature uniformity, power efficiency, coil matching and production stability. For example, a small copper tube brazing job may require a HF or UHF generator, while a steel billet forging line may require an MF or SRF generator. A large induction melting furnace may require a KGPS or high-power MF furnace generator.
Why HLQ Offers Five Induction Power Supply Series
Buyer Requirement
Suitable Series
Reason
Deep heating for large steel bars or billets
MF / SRF / KGPS
Lower and medium frequency ranges provide better penetration for large cross-sections.
Surface hardening of shafts, gears and mechanical parts
HF / SRF / MF
Frequency can be selected according to required hardening depth.
Copper tube, brass fitting or carbide tool brazing
HF / UHF
High frequency gives fast localized heating around the joint area.
Precision heating of small metal parts
UHF
Ultra high frequency offers shallow heating and accurate thermal control.
Induction melting furnace
KGPS / MF
Melting applications need strong furnace power, stable output and continuous duty.
Automated billet heating or auto parts heat treatment
SRF / MF / HF
SRF provides a practical middle-frequency range for many industrial heat treatment systems.
Working Principle
Step
Process
Engineering Explanation
1
Industrial power input
The system receives factory electricity such as single-phase 220V or three-phase 380V, depending on model and power rating.
2
Power conversion
The power supply converts incoming AC power into controlled medium-frequency, high-frequency or furnace-frequency output.
3
Resonant output
The inverter, capacitors and transformer form a resonant circuit to deliver high-current energy to the induction coil.
4
Coil excitation
The induction coil receives alternating current and generates a rapidly changing magnetic field.
5
Eddy current generation
Conductive metal workpieces generate eddy currents inside the heating zone.
6
Heat generation
Electrical resistance and, in magnetic materials, hysteresis effect generate heat directly inside the metal.
7
Process control
Power, frequency, time, coil shape, cooling and optional temperature feedback determine the final heating result.
MF Medium Frequency Induction Power Supply
MF medium frequency induction power supplies are designed for deeper heat penetration and larger thermal loads. They are suitable for billet forging, bar heating, rod heating, induction melting, large shaft heating and deep heat treatment. The MF series is commonly selected when the workpiece is large, the required heating depth is high, or the process requires strong through-heating.
Model
Input Power
Max Input Current
Frequency Range
Input Voltage
Duty Cycle
Recommended Applications
DW-MF-15
15kW
23A
1kHz–20kHz
3-phase 380V ±10%
100%
Small forging, preheating, small furnace heating.
DW-MF-25
25kW
36A
1kHz–20kHz
3-phase 380V ±10%
100%
Small bar heating, small melting furnace, preheating.
DW-MF-35
35kW
51A
1kHz–20kHz
3-phase 380V ±10%
100%
Rod heating, forging preparation, medium workpiece heating.
DW-MF-45
45kW
68A
1kHz–20kHz
3-phase 380V ±10%
100%
Billet preheating, forging, medium melting.
DW-MF-70
70kW
105A
1kHz–20kHz
3-phase 380V ±10%
100%
Steel bar forging, copper billet heating, aluminum billet heating.
DW-MF-90
90kW
135A
1kHz–20kHz
3-phase 380V ±10%
100%
Medium forging line, larger rod heating, induction melting.
DW-MF-110
110kW
170A
1kHz–20kHz
3-phase 380V ±10%
100%
Deep hardening, heavy forging, medium melting furnace.
DW-MF-160
160kW
240A
1kHz–20kHz
3-phase 380V ±10%
100%
Large billet heating, high-output heating, large shaft heating.
DW-MF-300
300kW
400A
1kHz–20kHz
3-phase 380V ±10%
100%
Heavy-duty forging, large melting, continuous industrial production.
HF High Frequency Induction Heating Power Supply
HF high frequency induction heating power supplies are mainly used for fast localized heating. They are suitable for brazing, soldering, surface hardening, annealing, shrink fitting, carbide tool brazing, copper pipe brazing and stainless steel fitting heating. HF systems are flexible and widely used in manual workstations, semi-automatic heating stations and automated production lines.
Model
Rated Power
Frequency Range
Typical Heating Depth
Recommended Applications
Best-Fit Workpieces
DW-HF-15
15kVA
30kHz–100kHz
Shallow to medium surface heating
Small brazing, soldering, small part heating.
Copper joints, small tools, small rings.
DW-HF-25
25kVA
30kHz–80kHz
Localized heating
Copper tube brazing, tool brazing, small shaft hardening.
HVAC fittings, carbide tools, small shafts.
DW-HF-35
35kVA
30kHz–80kHz
Localized to medium heating
Medium brazing, annealing, surface hardening.
Gears, fittings, mechanical parts.
DW-HF-45
45kVA
30kHz–80kHz
Medium surface heating
Shrink fitting, pipe joint brazing, gear heating.
Rings, bearings, pipe joints, gears.
DW-HF-60
60kVA
30kHz–80kHz
Medium heating depth
Automotive parts hardening, medium brazing, bearing heating.
Shafts, gears, bushings, bearings.
DW-HF-80 to DW-HF-160
80kVA–160kVA
30kHz–80kHz
Medium to deeper localized heating
Large brazing, surface hardening, heat treatment lines.
Large gears, shafts, tooling, production-line components.
UHF Ultra High Frequency Induction Power Supply
UHF ultra high frequency induction power supplies are used for very small components, shallow heating, precision brazing, micro soldering, connectors, terminals, fine wires and localized heating processes where thermal influence must be minimized. UHF systems are suitable for high-precision applications that require fast response and concentrated heat input.
Model
Rated Power
Frequency Range
Input Voltage
Recommended Applications
Engineering Notes
DW-UHF-4.5
4.5kW
1.1MHz–2.0MHz
Single-phase 220V ±10%
Micro soldering, fine connector heating, small component heating.
Very shallow heating zone and fast response.
DW-UHF-6.0
6.0kW
1.1MHz–2.0MHz
Single-phase 220V ±10%
Precision soldering, small metal parts, electronic terminals.
Suitable for very small workpieces.
DW-UHF-10
10kW
100kHz–500kHz
3-phase 380V ±10%
Precision brazing, small shaft heating, fine surface heating.
Good for small but slightly larger parts than MHz units.
DW-UHF-20
20kW
50kHz–250kHz
3-phase 380V ±10%
Small tool brazing, thin-wall components, localized heating.
Balances precision heating and higher output power.
DW-UHF-30 to DW-UHF-60
30kW–60kW
50kHz–200kHz / 50kHz–150kHz
3-phase 380V ±10%
Automated precision brazing, small part hardening, localized heat treatment.
Suitable for higher-output precision heating stations.
SRF Superaudio Frequency Induction Heating System
The SRF power supplies series fills the application range between typical medium frequency and high frequency induction heating. It is especially useful for billet heating, auto parts heat treatment, medium-depth hardening, forging preheating and industrial heating applications where both heating speed and reasonable penetration depth are required. The DW-SRF series uses IGBT series resonant design and can support remote control interfaces such as 0–10V, 4–20mA, RS485 and RS232 according to application requirements.
SRF Series Feature
Specification / Description
Application Value
Power Range
30kW–2000kW
Suitable for medium and heavy industrial heating applications.
Frequency Range
20kHz–50kHz
Provides a balanced heating depth between MF and HF.
Control System
Digital design control system
Displays working voltage, current, frequency and fault indication.
Inverter Technology
IGBT series resonant design
Improves reliability and heating efficiency.
Remote Control
0–10V / 4–20mA power control, RS485 and RS232 options
Easy to connect with external automation systems.
Duty Cycle
100%
Suitable for continuous industrial production.
Typical Applications
Billet heating, auto parts heat treatment, medium-depth hardening
Useful for production lines requiring repeatable heating quality.
SRF Model Selection Table
Model
Max Output Power
Frequency
Max Input Current
Input Voltage
Duty Cycle
Water Flow
DW-SRF-30A
30kW
20kHz–50kHz
48A
3-phase 380V, 50Hz/60Hz
100%
15L/min at 0.2MPa
DW-SRF-30ABS
30kW
20kHz–50kHz
48A
3-phase 380V, 50Hz/60Hz
100%
15L/min at 0.2MPa
DW-SRF-40ABS
40kW
20kHz–50kHz
62A
3-phase 380V, 50Hz/60Hz
100%
32L/min at 0.2MPa
DW-SRF-50ABS
50kW
20kHz–50kHz
75A
3-phase 380V, 50Hz/60Hz
100%
32L/min at 0.2MPa
DW-SRF-40AB
40kW
20kHz–50kHz
62A
3-phase 380V, 50Hz/60Hz
100%
32L/min at 0.2MPa
DW-SRF-50AB
50kW
20kHz–50kHz
75A
3-phase 380V, 50Hz/60Hz
100%
32L/min at 0.2MPa
DW-SRF-60AB
60kW
20kHz–50kHz
90A
3-phase 380V, 50Hz/60Hz
100%
40L/min at 0.2MPa
High-power SRF models
80kW–300kW
20kHz–50kHz
According to model
3-phase 380V, customizable
100%
According to model and transformer configuration
KGPS Induction Generator Power Supply
KGPS induction generator power supplies are widely used for induction melting furnaces, forging furnaces and other heavy-duty thermal equipment. Compared with compact IGBT high-frequency machines, KGPS systems are usually selected for furnace-type applications requiring stable medium-frequency output, large current, strong furnace load capacity and continuous metal heating or melting.
KGPS series is especially suitable for foundries, metal recycling plants, forging workshops, steel processing plants and non-ferrous metal melting applications. It can be configured with induction melting furnaces, industrial forging furnaces, furnace transformers, capacitor banks, water cooling systems and furnace bodies according to metal type, furnace capacity and production output.
KGPS Feature
Description
Typical Buyer Benefit
Main Application
Induction melting furnace, forging furnace and heavy industrial heating furnace.
Suitable for high thermal load and continuous furnace operation.
Power Range
Customizable according to furnace capacity and production output.
Can be matched with different melting capacities and furnace sizes.
Frequency Type
Medium frequency furnace power output.
Good for metal melting, smelting, holding and large workpiece heating.
5 seconds, 30 seconds, 3 minutes, 1 hour per batch.
Heating depth
Determines frequency selection.
Surface heating, 2mm hardening depth, full through-heating.
Production capacity
Determines power supply size and automation level.
Pieces/hour, kg/hour, tons/day.
Factory input voltage
Ensures correct electrical configuration.
220V single phase, 380V three phase, 415V, 440V, 480V.
Cooling water condition
Determines cooling system design.
Water flow, pressure, inlet temperature and water quality.
Frequently Asked Questions
Q: What series of induction heating power supplies does HLQ provide? A: HLQ provides MF medium frequency, HF high frequency, UHF ultra high frequency, SRF superaudio frequency and KGPS induction generator power supplies.
Q: What is the difference between MF and HF induction power supplies? A: Medium Frequency (MF) units operate at 1–20KHz and are designed for deep, through-heating of large workpieces like billets and bars. High Frequency (HF) units operate at 20–100KHz and are optimized for surface heating, brazing, and shallow case hardening.
Q: Can your induction power supplies replace existing SCR machines? A: Yes. Our IGBT-based units are direct drop-in replacements for SCR-controlled induction generators, offering the same or higher power output in 1/10 the physical footprint with significantly lower energy consumption.
Q: Do you offer custom frequency or power configurations? A: Yes. HLQ offers OEM and custom-specification units. Contact our engineering team with your workpiece dimensions, material, and target temperature for a tailored recommendation.
Q: What input voltage is required? A: Most units in the MF and HF series require 3-phase 380V ±10%. The DW-HF-15KW and UHF-4.5/6.0KW models operate on single-phase 220V.
Q: What warranty and after-sales support do you provide? A: All HLQ induction power supplies come with a 12-month warranty. We provide remote technical support, spare IGBT modules, and on-site service for large installations.
Q: Which series is best for steel billet forging? A: MF or SRF series is generally suitable for steel billet forging because they provide stronger penetration and enough thermal energy for larger cross-sections.
To provide the best experiences, we use technologies like cookies to store and/or access device information. Consenting to these technologies will allow us to process data such as browsing behavior or unique IDs on this site. Not consenting or withdrawing consent, may adversely affect certain features and functions.
Functional
Always active
The technical storage or access is strictly necessary for the legitimate purpose of enabling the use of a specific service explicitly requested by the subscriber or user, or for the sole purpose of carrying out the transmission of a communication over an electronic communications network.
Preferences
The technical storage or access is necessary for the legitimate purpose of storing preferences that are not requested by the subscriber or user.
Statistics
The technical storage or access that is used exclusively for statistical purposes.The technical storage or access that is used exclusively for anonymous statistical purposes. Without a subpoena, voluntary compliance on the part of your Internet Service Provider, or additional records from a third party, information stored or retrieved for this purpose alone cannot usually be used to identify you.
Marketing
The technical storage or access is required to create user profiles to send advertising, or to track the user on a website or across several websites for similar marketing purposes.







 How to Choose the Right Induction Heating Power Supply