

Induction Strip Heating Solutions
Induction Strip Heating Solutions: Complete Engineering Guide
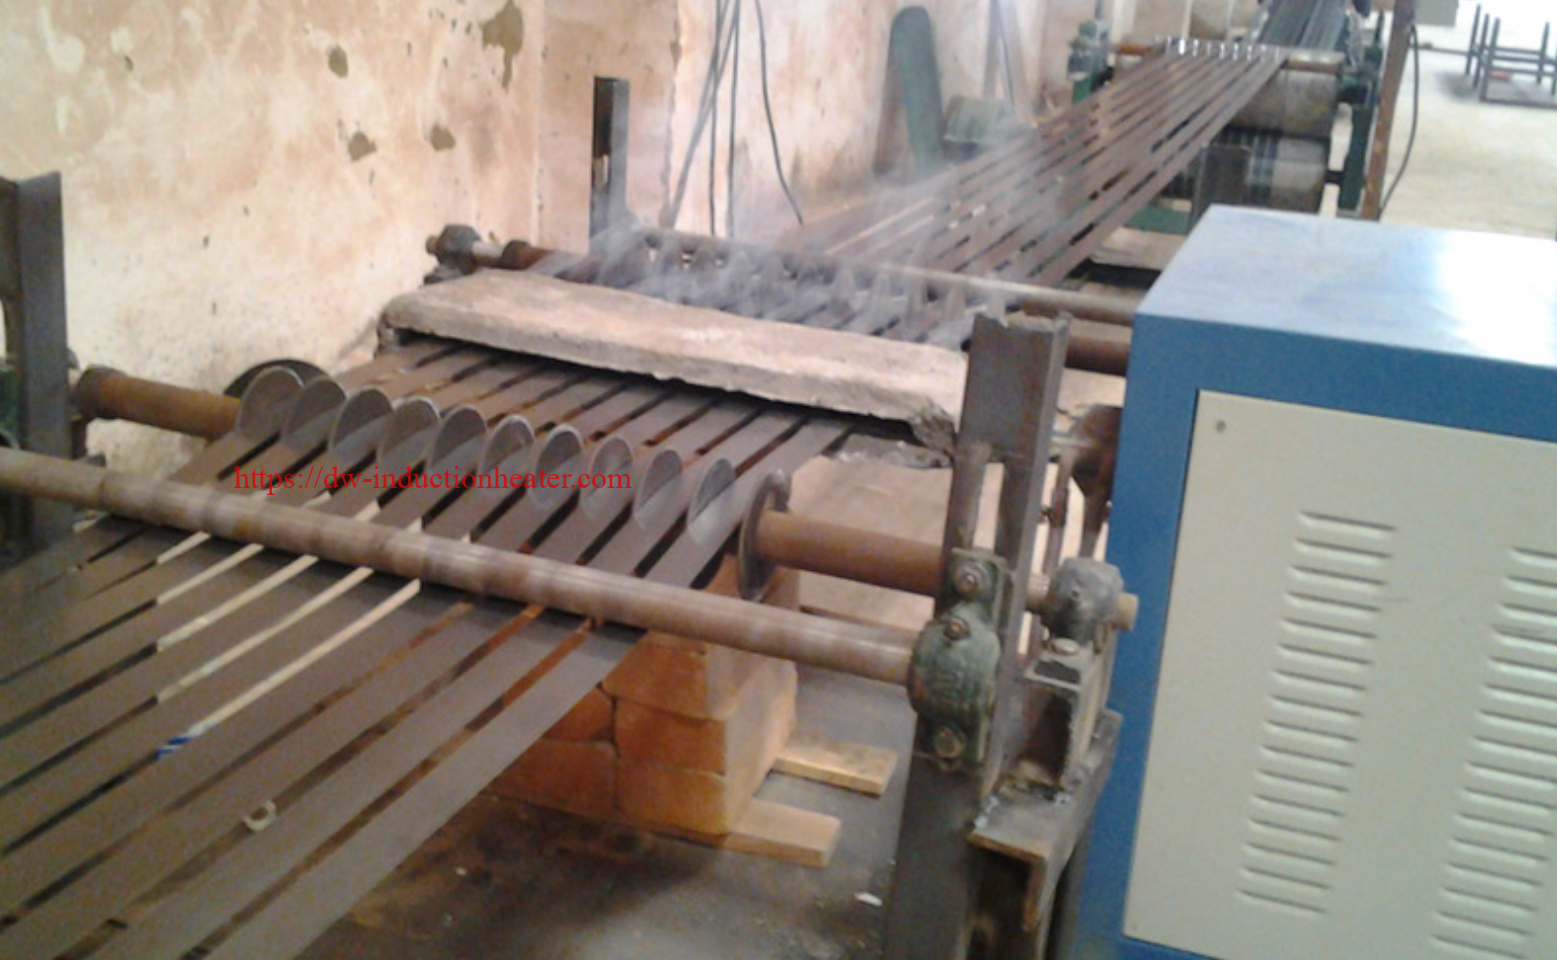
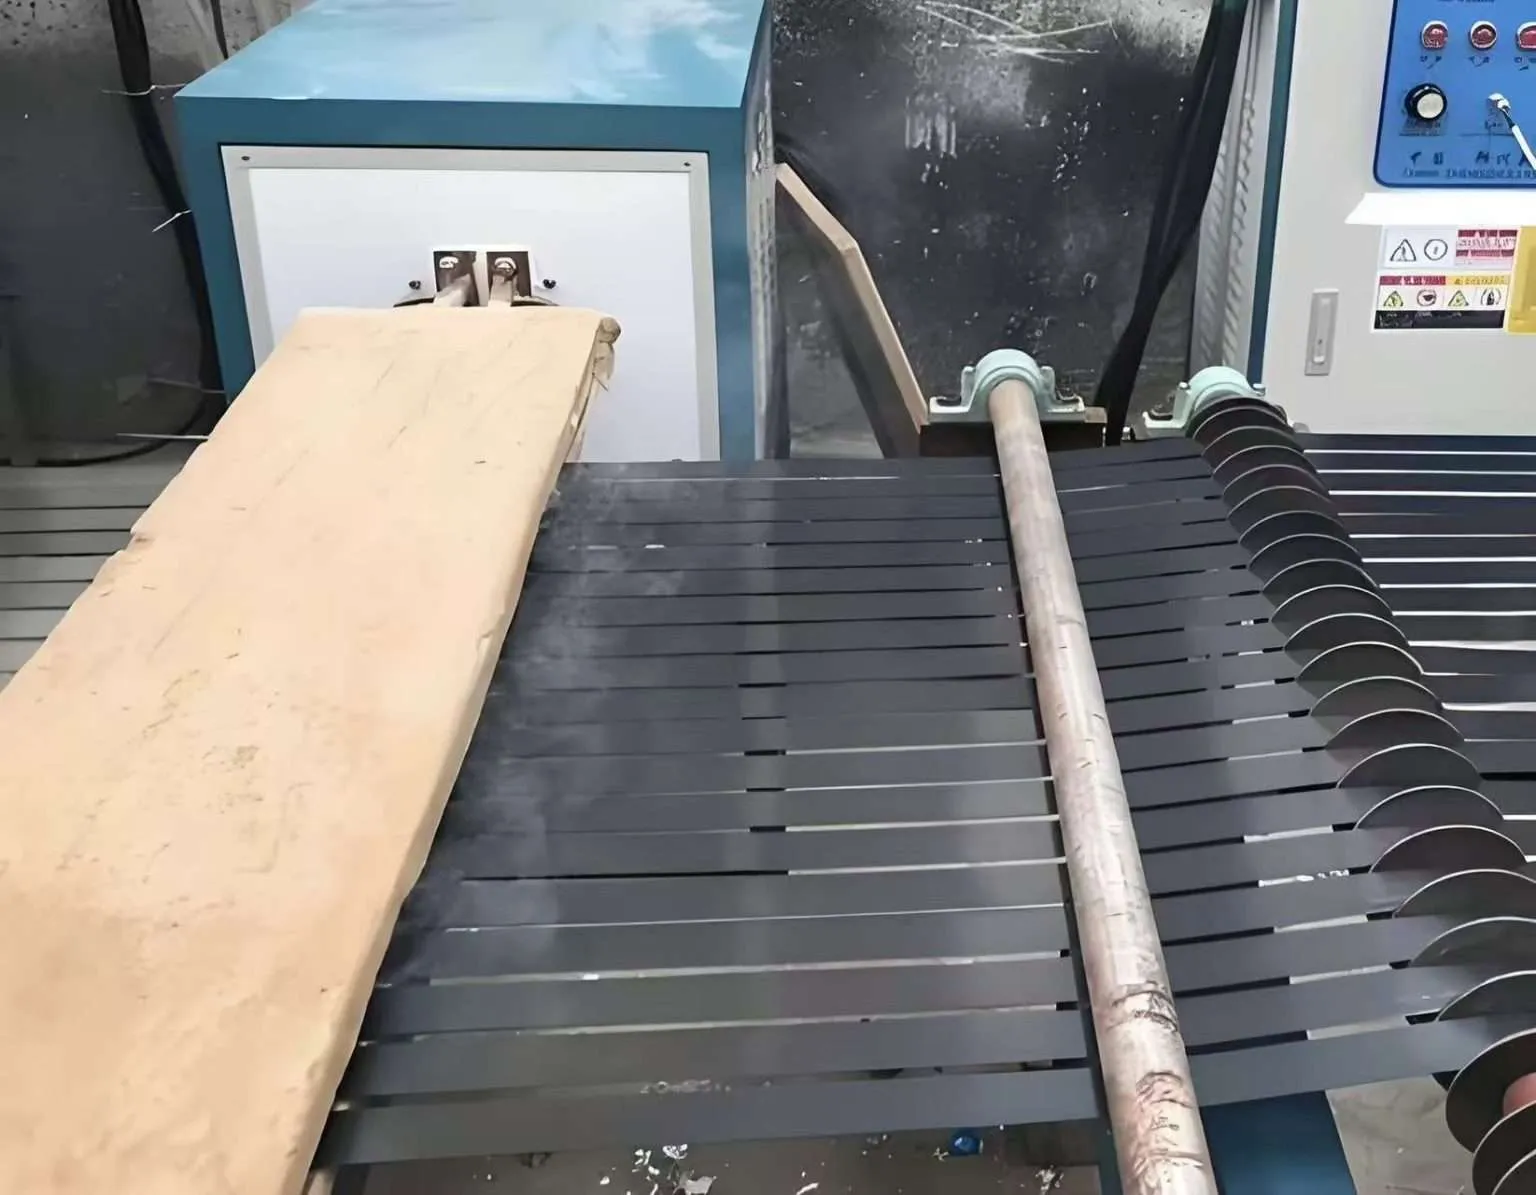
Induction strip heating is a continuous, inline heat treatment process that uses electromagnetic induction to rapidly and precisely heat electrically conductive metal strips — including steel, copper, aluminum, stainless steel, and specialty alloys — as they travel at production speed through a compact induction coil. The technology eliminates conventional long-tunnel furnaces, enabling strip producers and processors to anneal, temper, harden, preheat, cure coatings, and stress-relieve strip material with 90–95% electrical efficiency, minimal oxidation, and full digital process control. HLQ Induction Equipment designs and manufactures custom induction strip heating systems from 15 kW to 2,000 kW for strip widths from 5 mm to 2,000 mm and thicknesses from 0.05 mm to 25 mm, servicing customers in steel mills, copper fabricators, automotive stamping lines, and electronics manufacturing worldwide.
Quick Answer
Induction strip heating passes a metal strip at continuous production speed through one or more induction coils energized by a solid-state IGBT power supply. The alternating electromagnetic field induces eddy currents directly inside the strip, heating it to the required process temperature — from 150°C for coating curing to over 1,100°C for stainless steel solution annealing — in a fraction of the time and space required by conventional gas or resistance furnaces. It is used wherever a metal strip must be heat-treated inline during rolling, drawing, slitting, stamping, or coating operations. The correct induction strip heating system is defined by strip material, dimensions, line speed, target temperature, and required throughput — parameters that determine power rating, frequency, coil geometry, and cooling arrangement.
Table of Contents
- What Is Induction Strip Heating?
- Working Principle
- Key Applications
- Suitable Materials and Industries
- Key Technical Parameters
- Equipment Types
- Engineering Selection Guide
- Process Workflow
- Common Problems and Solutions
- Real Engineering Case Studies
- Standards and Safety Considerations
- Why Choose HLQ Induction Equipment?
- FAQ
What Is Induction Strip Heating?
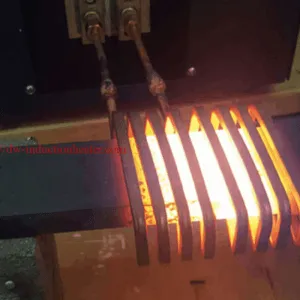
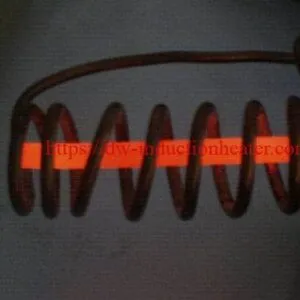
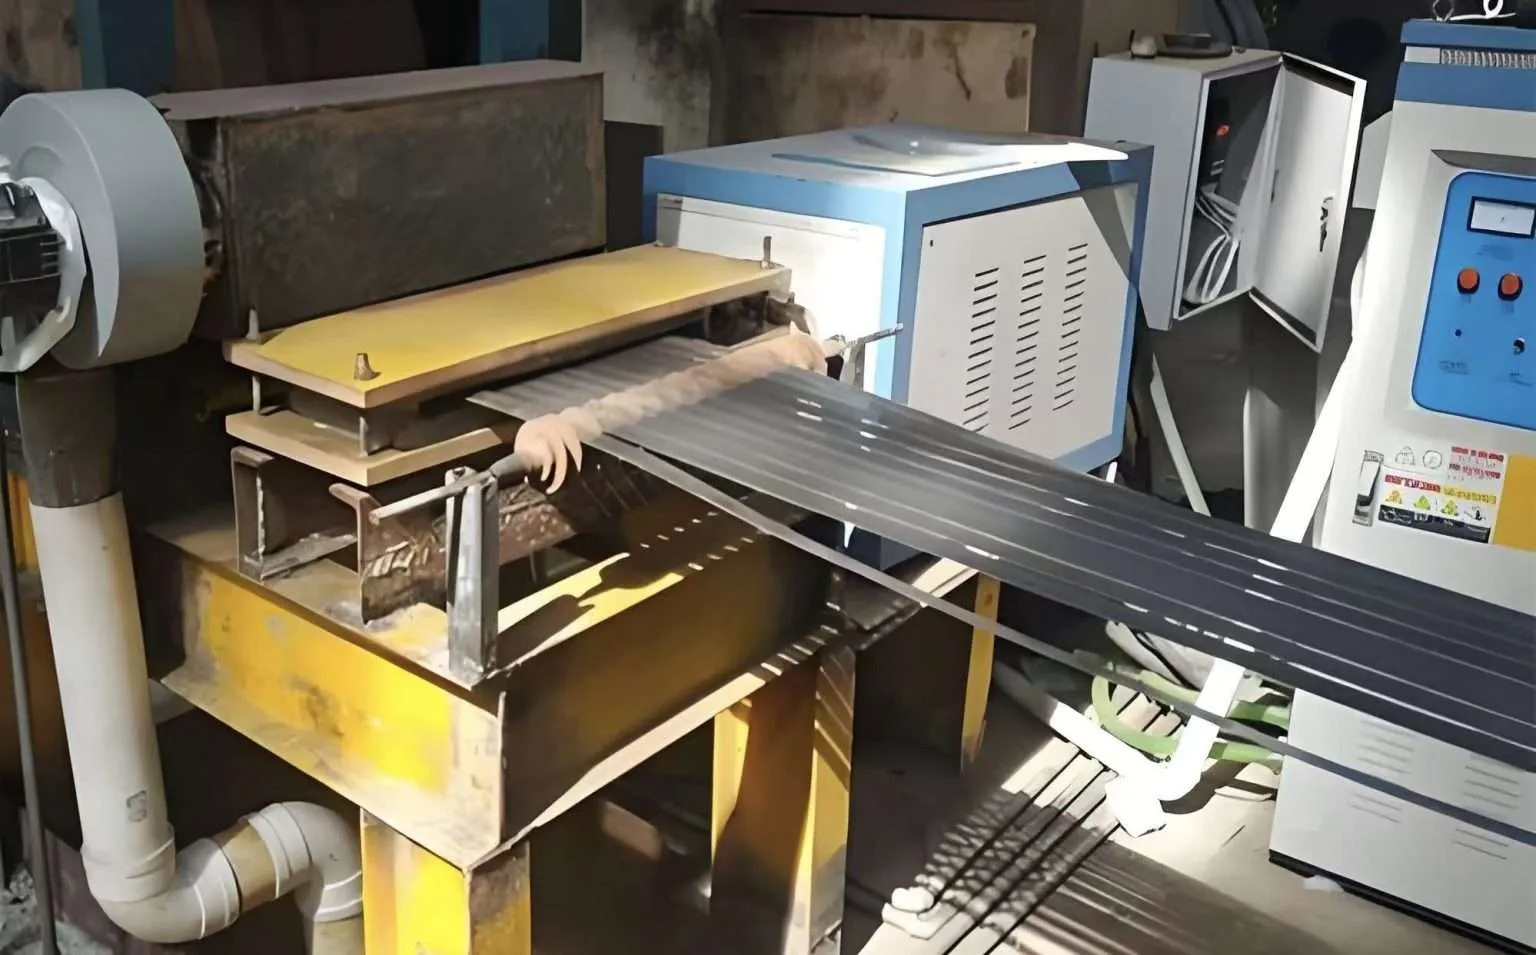
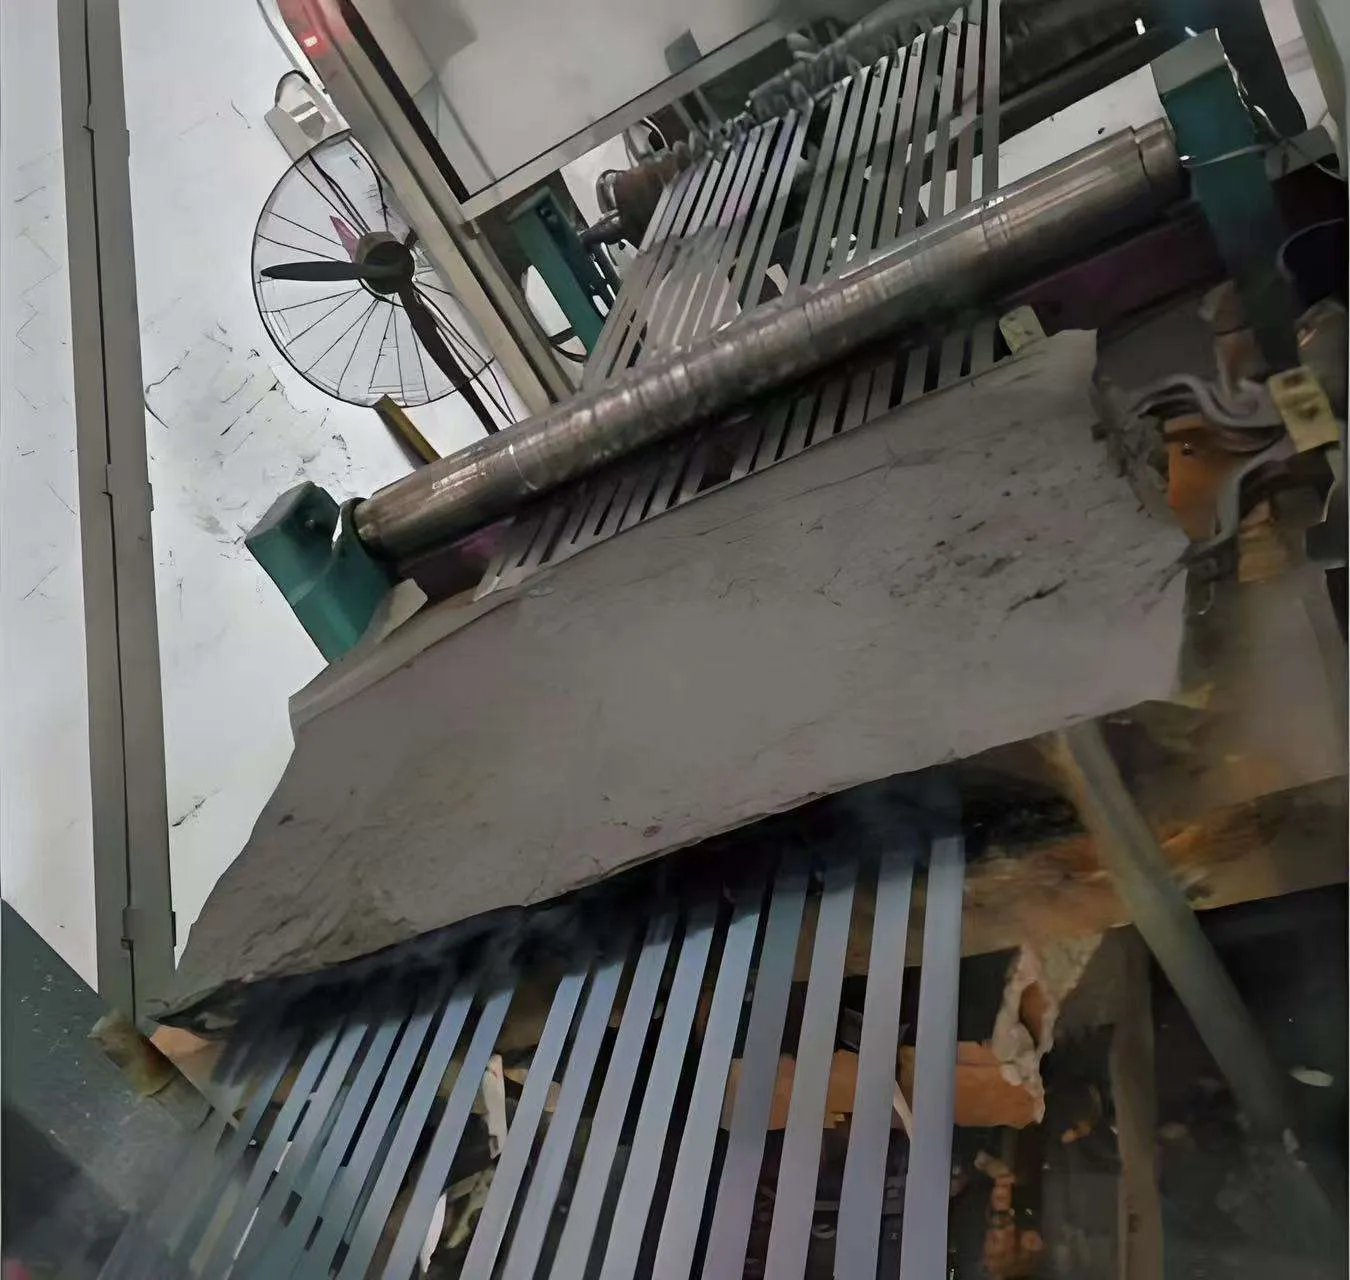
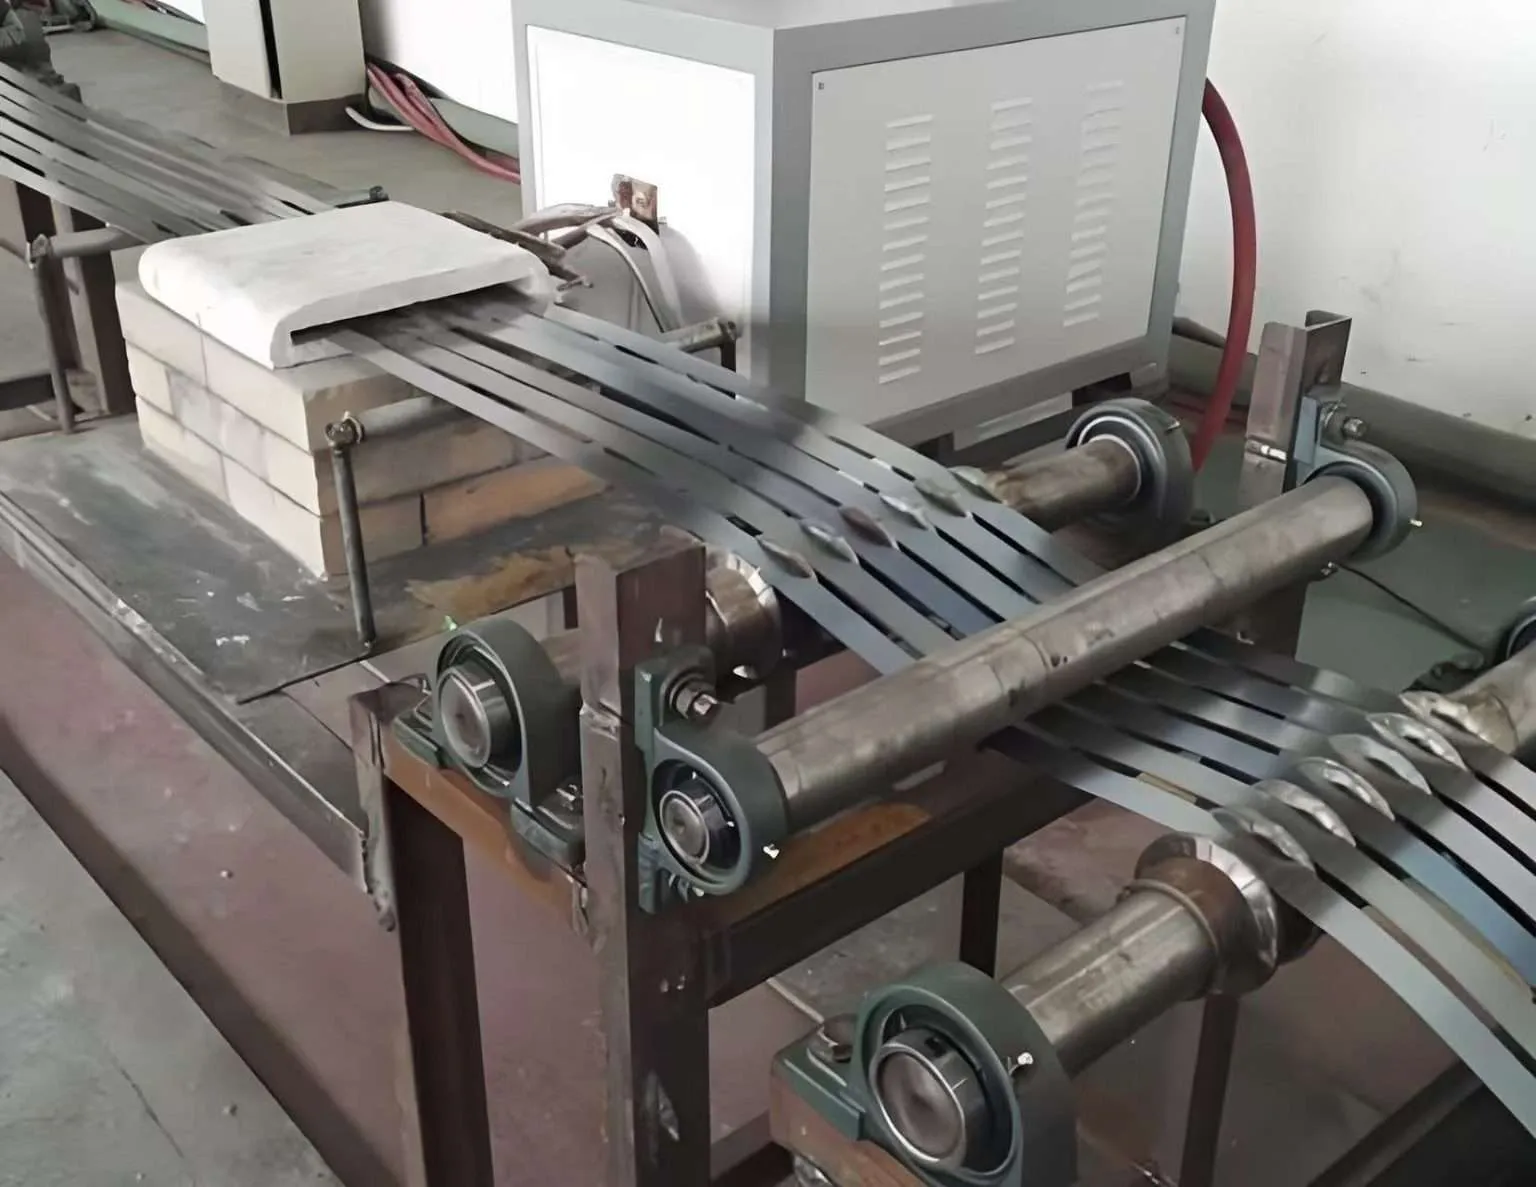
Induction strip heating is a category of continuous electromagnetic heat treatment specifically engineered for flat metal strip — a product form defined by its large width-to-thickness ratio, continuous length, and high production speed. The strip passes horizontally or vertically through a transverse flux or longitudinal flux induction coil, where it absorbs electromagnetic energy and reaches its target process temperature within a heated zone that is typically 200 mm to 2,000 mm in length, depending on strip dimensions and line speed.
Unlike induction heating of discrete parts (gears, billets, or fittings), strip heating is inherently a continuous process. The power supply operates without interruption, and the process parameters — power, frequency, and coil geometry — are fixed for a given strip grade and line speed combination. When line speed or material grade changes, the control system adjusts power output automatically to maintain the target exit temperature.
The two fundamental coil configurations used in strip heating differ in how the magnetic field is oriented relative to the strip:
- Longitudinal Flux Induction (LFI): The strip passes through a solenoid-type coil with the magnetic field running parallel to the strip travel direction. The induced currents flow circumferentially around the strip cross-section. LFI is the most common configuration for narrow strips (width <200 mm) and for thick strips where through-heating is required.
- Transverse Flux Induction (TFI): Opposing coil segments are positioned above and below the strip surface, with the magnetic field passing perpendicularly through the strip thickness. The induced currents flow longitudinally along the strip surface, making TFI extremely efficient for wide, thin strips where the skin depth is large relative to strip thickness. TFI is the preferred technology for wide strip (200–2,000 mm) and very thin gauges.
A third configuration, Edge Induction Heating, targets only the strip edges using specially shaped coils positioned at the strip margins. This is used in rolling mill entry edge preheating, seam weld annealing, and edge-only differential treatment applications.
Working Principle
The physical basis of induction strip heating is Faraday’s law of electromagnetic induction. When an alternating current at frequency f flows through the induction coil, it creates a time-varying magnetic field H that penetrates the strip material. According to Lenz’s law, this field induces eddy currents within the strip that oppose the change in flux. These eddy currents, encountering the electrical resistance of the strip material, convert electromagnetic energy into thermal energy (Joule heating) directly within the strip. No external heat transfer medium — no flame, no hot gas, no radiation from a furnace wall — is involved. This is why induction heating is fast, efficient, and highly controllable.
Skin Effect and Penetration Depth
Eddy currents are not uniformly distributed through the strip thickness. Due to the skin effect, current density is highest at the strip surface and decreases exponentially toward the center. The depth at which current density falls to 1/e (approximately 37%) of its surface value is defined as the reference depth or skin depth (δ), given by:
δ (mm) = 503 × √(ρ / (μr × f))
Where ρ is electrical resistivity in Ω·m, μr is relative magnetic permeability (dimensionless), and f is frequency in Hz. For practical strip heating engineering, the rule is: strip thickness should be at least 2× skin depth for efficient coupling. If strip thickness < skin depth, the electromagnetic field passes through the strip with insufficient energy absorption, reducing efficiency sharply.
For ferromagnetic steels below the Curie temperature (~770°C), μr is 50–200, so skin depth is small and efficiency is high even at moderate frequencies. Above the Curie point, steel becomes non-magnetic (μr = 1), skin depth jumps significantly, and higher power density is needed to maintain heating rate. Non-ferrous metals (copper, aluminum) have μr = 1 at all temperatures, requiring higher frequencies to achieve adequate skin depth relative to strip thickness.
Skin Depth Reference Table
| Material | Condition | Resistivity ρ (Ω·m) | μr | δ at 10 kHz (mm) | δ at 50 kHz (mm) | δ at 200 kHz (mm) |
|---|---|---|---|---|---|---|
| Carbon Steel | Cold, below Curie | 1.6 × 10⁻⁷ | 100 | 1.27 | 0.57 | 0.28 |
| Carbon Steel | Hot, above Curie (800°C+) | 1.2 × 10⁻⁶ | 1 | 34.7 | 15.5 | 7.8 |
| Stainless Steel 304 | All temperatures | 7.2 × 10⁻⁷ | 1 | 26.9 | 12.0 | 6.0 |
| Copper (ETP) | At 20°C | 1.72 × 10⁻⁸ | 1 | 4.16 | 1.86 | 0.93 |
| Copper (ETP) | At 500°C | 5.5 × 10⁻⁸ | 1 | 7.43 | 3.32 | 1.66 |
| Aluminum 1100 | At 20°C | 2.82 × 10⁻⁸ | 1 | 5.32 | 2.38 | 1.19 |
| Titanium Gr.2 | At 20°C | 5.6 × 10⁻⁷ | 1 | 23.7 | 10.6 | 5.3 |

Power and Energy Balance
The theoretical minimum power required to heat a strip at a given production rate is determined by the thermal energy equation:
Pthermal = ṁ × Cp × ΔT = (w × t × v × ρm) × Cp × ΔT
Where: w = strip width (m), t = strip thickness (m), v = line speed (m/s), ρm = material density (kg/m³), Cp = specific heat capacity (J/kg·°C), ΔT = temperature rise (°C). Divide by electrical-to-thermal efficiency η (typically 0.82–0.90 for well-coupled induction strip heating systems) to obtain installed electrical power. Always add a 20–30% design margin for line speed variation, gauge tolerance, and coil coupling losses.
Key Applications
Induction strip heating addresses a broad range of heat treatment and process heating requirements across metal forming and processing industries. The following sections describe the most commercially significant applications, along with the specific process objectives and typical temperature ranges involved.
1. Continuous Strip Annealing
Full or partial recrystallization annealing after cold rolling restores ductility and reduces yield strength to specified levels. Induction annealing compresses the furnace section of a continuous annealing line from 30–80 meters of gas-fired or resistively heated tunnel to 1–4 meters of induction heating zone. This is the highest-volume application for induction strip heating in the steel and copper industries. Target temperatures: 500–720°C for carbon steel strip; 450–650°C for copper strip; 300–430°C for aluminum strip.
2. Strip Tempering After Hardening
High-carbon and spring steel strip that has been quench-hardened to martensite must be tempered to relieve brittleness and set final mechanical properties. Induction tempering heats the strip to 150–500°C immediately after quenching on the same production line. Precise temperature control at ±5–10°C is critical in tempering because the hardness-toughness balance is sensitive to temperature in this range.
3. Entry Zone Preheating for Rolling Mills
Cold strip entering a rolling mill experiences edge cracking and shape defects if the material’s yield strength and ductility are not brought into the required window before deformation. Induction preheating at 100–400°C immediately ahead of the roll bite eliminates this problem, reduces rolling force by 15–30%, and allows thinner gauge targets in a single pass.
4. Coating Curing and Bonding
Organic coatings, adhesives, and functional layers applied to strip surfaces require controlled thermal curing. Induction strip heating with susceptor foil or direct heating of the metal substrate raises the strip surface to curing temperature (120–280°C) faster and more uniformly than air convection ovens, producing better adhesion and reduced line length.
5. Galvanizing Line Strip Preheating
In continuous hot-dip galvanizing lines, the steel strip must be preheated to 450–500°C before entering the zinc bath to ensure metallurgically sound zinc-iron bonding. Induction preheating provides rapid, uniform temperature across the strip width and replaces or supplements gas-fired radiant tube furnaces in the entry section, shortening line length and improving temperature uniformity across the strip width.
6. Differential Heating and Edge Heating
Some forming operations require the strip edges to be at a different temperature from the center — either hotter (for edge rolling or differential drawing) or treated separately (for seam weld annealing after tube forming). Edge induction heaters using profiled coils positioned at the strip margins achieve selective heating within ±15 mm of the edge without significantly affecting the strip center temperature.
7. Stainless Steel and Special Alloy Strip Annealing
Austenitic stainless steel strip requires solution annealing at 1,050–1,100°C after cold rolling to dissolve carbide precipitates and restore corrosion resistance. At these temperatures, conventional furnaces require long soak zones and controlled atmosphere management. Induction solution annealing with nitrogen atmosphere and rapid water quench produces equivalent metallurgical results in a fraction of the line length, with measurable improvements in surface quality.
Application Summary Table
| Application | Typical Materials | Target Temperature | Key Process Objective | Line Speed Range |
|---|---|---|---|---|
| Full recrystallization annealing | Cold-rolled carbon steel, copper, aluminum | 450–720°C | Restore ductility, reduce yield strength | 5–120 m/min |
| Strip tempering | High-carbon steel, spring steel | 150–500°C | Relieve martensite brittleness | 10–200 m/min |
| Rolling mill preheating | Carbon steel, stainless steel, titanium | 100–450°C | Reduce rolling force, prevent edge cracking | 20–300 m/min |
| Coating and adhesive curing | Steel, aluminum (coated strip) | 120–280°C | Cure organic coating uniformly | 10–150 m/min |
| Galvanizing preheating | Low carbon steel | 430–500°C | Prepare surface for zinc adhesion | 30–150 m/min |
| Edge-only heating | Steel, stainless, copper strip | 200–800°C (edge zone) | Differential forming, seam weld anneal | 5–100 m/min |
| Stainless solution annealing | 304, 316, 321, 430 stainless | 950–1,100°C | Dissolve carbides, restore corrosion resistance | 5–60 m/min |
| Titanium and nickel alloy annealing | Ti Gr.1/2, Inconel 625, Hastelloy C276 | 700–1,050°C | Stress relief, recrystallization | 2–30 m/min |
Suitable Materials and Industries
Any electrically conductive flat metal strip can be induction heated. The engineering considerations — frequency, power density, and coil configuration — vary by material, but the fundamental process is applicable across the full range of metals processed in strip and coil form.
| Material Group | Typical Strip Dimensions | Recommended Frequency | Primary Industries | Special Considerations |
|---|---|---|---|---|
| Low / Medium Carbon Steel | 0.2–6 mm thick, 10–1,500 mm wide | 1–30 kHz | Automotive stamping, construction, packaging, appliance | Ferromagnetic below Curie point — high efficiency. Requires N₂ above 650°C for bright finish. |
| High Carbon and Spring Steel | 0.1–4 mm thick, 5–500 mm wide | 10–80 kHz | Springs, blades, saws, fasteners | Temper immediately after quench to prevent cracking. Precise temperature control critical. |
| Stainless Steel (austenitic) | 0.05–4 mm thick, 5–1,200 mm wide | 10–200 kHz | Food equipment, medical devices, chemical processing, architecture | Non-magnetic — higher frequency needed. Forming gas or N₂ atmosphere essential at annealing temperature. |
| Copper and Copper Alloys | 0.05–6 mm thick, 5–600 mm wide | 50–300 kHz | Electronics, connectors, heat exchangers, coin blanks | High thermal conductivity requires rapid heating. Water quench standard for bright anneal. |
| Aluminum Alloys | 0.3–8 mm thick, 100–2,000 mm wide | 10–100 kHz (TFI preferred for wide) | Automotive body panels, packaging, aerospace | Wide strips require TFI configuration. Temperature limit critical — narrow window between anneal and melt. |
| Titanium Alloys | 0.1–3 mm thick, 5–400 mm wide | 10–100 kHz | Aerospace, medical implants, chemical processing | Reactive at temperature — argon atmosphere required. High value — precision process control essential. |
| Nickel and Nickel Alloys | 0.05–3 mm thick, 5–300 mm wide | 10–150 kHz | Aerospace, power generation, chemical industry | High resistivity — good induction coupling efficiency. Atmosphere control critical above 800°C. |
| Electrical Steel (Si-Fe) | 0.1–0.65 mm thick, 100–1,200 mm wide | 1–10 kHz | Electric motors, transformers | Hysteresis loss significant — accounts for additional heating contribution. Insulation coating annealing application. |
Key Technical Parameters
The following table provides engineering reference ranges for the key parameters that define an induction strip heating system. These values cover the majority of industrial applications; extreme combinations (very wide thin strip, very high speed, or exotic alloys) may require values outside these ranges and should be reviewed with HLQ engineering.
| Parameter | Typical Range | Engineering Notes |
|---|---|---|
| Strip Width | 5 mm – 2,000 mm | Narrow strip (<200 mm): LFI solenoid coil. Wide strip (>200 mm): TFI transverse flux coil for uniform cross-width heating. Edge-only: profile coil. |
| Strip Thickness | 0.05 mm – 25 mm | Strip thickness must be ≥ 1× skin depth for adequate coupling efficiency. Very thin foil (<0.1 mm) may require UHF (500 kHz+) or susceptor-assisted heating. |
| Line Speed | 0.5 m/min – 1,200 m/min | Line speed × strip cross-section × density = mass flow rate, which directly determines minimum required power. Closed-loop speed-to-power control mandatory for variable speed lines. |
| Target Temperature | 100°C – 1,150°C | Temperature at coil exit measured by non-contact IR pyrometer. For temperatures above 800°C, thermal camera cross-width profiling recommended. |
| Temperature Uniformity | ±3°C – ±20°C across width | TFI coils achieve better cross-width uniformity (<±5°C) than LFI solenoids for wide strip. Active power profiling across coil segments improves uniformity for complex alloys. |
| Installed Power | 15 kW – 2,000 kW | Calculate thermal power from mass flow × Cp × ΔT, then divide by efficiency (0.82–0.90). Add 25% design margin. Round up to standard rating. |
| Operating Frequency | 1 kHz – 500 kHz | 1–10 kHz: wide steel strip, heavy gauge. 10–80 kHz: general strip annealing (steel, copper medium gauge). 80–300 kHz: copper and aluminum fine gauge, stainless thin strip. 300 kHz+: very thin foil. |
| Heating Zone Length | 100 mm – 3,000 mm | Heating zone length = coil length. Determined by dwell time requirement: dwell time (s) = coil length (m) ÷ line speed (m/s). Minimum dwell for uniform through-heating: 0.1–5 seconds. |
| Coil-to-Strip Clearance | 5 mm – 50 mm | Smaller clearance improves coupling efficiency but increases risk of strip-coil contact on strip flutter or tension transients. Use ceramic or PTFE guide rollers to maintain gap stability. |
| Atmosphere | Open air / N₂ / N₂+H₂ / Ar | Open air: copper below 600°C (with water quench), steel below 650°C for matte finish. N₂: carbon steel bright anneal above 650°C. N₂+H₂ (5% H₂): stainless, bright steel. Ar: titanium, reactive alloys above 600°C. |
| Cooling Rate (post-heat) | 5°C/s – 2,000°C/s | Copper: rapid water quench preferred (fine grain). Carbon steel: controlled cooling rate determines microstructure (ferrite-pearlite vs martensite). Stainless: rapid water quench after solution anneal to suppress sensitization. |
| Temperature Control Accuracy | ±2°C – ±15°C | IGBT power supply response time: <10 ms. IR pyrometer + PID closed loop achieves ±5°C in steady-state production. Tighter control (<±3°C) requires two-zone control with upstream and exit pyrometers. |
| Electrical Efficiency | 82% – 95% | Highest efficiency for carbon steel below Curie point with LFI coil (high μr). Lowest for non-ferrous wide strip with significant coupling gap. TFI with active flux concentrators approaches 88% for aluminum wide strip. |
Equipment Types
HLQ Induction Equipment manufactures four primary induction strip heating system configurations, each optimized for a specific range of strip dimensions, line speeds, and process requirements. All systems are built around IGBT solid-state power supplies with digital closed-loop control and can be integrated into new or existing production lines.
Type 1: Longitudinal Flux Induction (LFI) Strip Heater
The LFI strip heater uses a solenoid-type coil through which the strip passes horizontally or vertically. The magnetic field runs parallel to the strip travel direction, and eddy currents flow circumferentially around the strip cross-section. LFI systems are the simplest in mechanical design, offer excellent coupling efficiency for round and near-square cross-sections, and are ideal for narrow strip (width up to 200 mm) at any thickness. They are also used for edge bar and flat bar heating in the same power supply range. LFI systems from HLQ cover strip widths from 5 to 200 mm at line speeds from 0.5 to 600 m/min and power ratings from 15 kW to 500 kW.
Type 2: Transverse Flux Induction (TFI) Strip Heater
TFI strip heaters position opposing coil segments above and below the strip surface, with field-shaping flux concentrators directing the magnetic field perpendicularly through the strip thickness. The induced eddy currents flow in the plane of the strip surface, making TFI inherently suitable for wide, thin strip where LFI coils would be impractically large. TFI achieves excellent cross-width temperature uniformity (±5°C) when coil segments are independently powered and controlled. HLQ TFI systems cover strip widths from 200 mm to 2,000 mm and are available from 100 kW to 2,000 kW for aluminum, wide stainless, and wide carbon steel applications.
Type 3: Edge Strip Induction Heater
Edge induction heaters mount at each side of the strip line and heat only a 10–50 mm margin at each strip edge using C-shaped or horseshoe coils that cradle the strip edge. The active zone per edge is typically 100–400 mm long. Two independently powered units (one per edge) allow differential edge temperature control. Edge heaters are used ahead of rolling mill entry, in tube forming seam weld annealing, and for differential strip edge treatment in specialty forming operations. Power per edge unit: 5–100 kW.
Type 4: Multi-Zone Modular Strip Heating System
For applications requiring long controlled heating zones, multiple ramp stages, or complex temperature profiles (e.g., heat-soak-quench sequences), HLQ supplies modular multi-zone strip heating systems comprising 2–12 individual induction heating modules in series, each independently controlled. This configuration allows the strip to be brought to temperature in a controlled ramp profile rather than a single step, reducing thermal stress in sensitive alloys and allowing process recipes with different ramp rates to be programmed for different material grades. Multi-zone systems are used in high-grade stainless steel annealing, titanium strip processing, and spring steel continuous hardening and tempering lines.
Equipment Comparison Table
| System Type | Strip Width Range | Best For | Temperature Uniformity | Power Range | Relative Complexity |
|---|---|---|---|---|---|
| LFI Solenoid | 5–200 mm | Narrow strip, bar, rod, wire | ±5–10°C | 15–500 kW | Low |
| TFI Transverse Flux | 200–2,000 mm | Wide and thin strip (steel, Al, SS) | ±3–8°C | 100–2,000 kW | High |
| Edge Heater | Any (edge zone only) | Selective edge treatment, seam weld annealing | ±5–15°C (edge zone) | 5–100 kW per edge | Low–Medium |
| Multi-Zone Modular | 5–1,200 mm | Controlled ramp profiles, complex alloys | ±3–8°C (zoned control) | 50–1,500 kW total | High |
Engineering Selection Guide
Use the following decision table to identify the correct system configuration for your application. Begin by identifying your strip material and width, then cross-reference with your line speed and temperature requirement. For borderline cases or combinations not covered here, request a free application engineering review from HLQ.
| Application Condition | Recommended System | Frequency | Reason |
|---|---|---|---|
| Narrow copper strip ≤100 mm wide, 0.3–3 mm thick, annealing at 550°C, 20 m/min | LFI Solenoid, 50–100 kW, 50–150 kHz | 100 kHz | Narrow strip — LFI solenoid provides full circumferential coupling. High frequency for copper skin depth matching. |
| Wide carbon steel strip 1,200 mm wide, 0.5 mm thick, galvanizing preheat at 480°C, 80 m/min | TFI Transverse Flux, 400–600 kW, 3–10 kHz | 5 kHz | Wide strip requires TFI for cross-width uniformity. Carbon steel ferromagnetic — low frequency sufficient for thin strip below Curie. |
| Stainless steel 304 strip 300 mm wide, 0.8 mm thick, solution anneal at 1,050°C, 15 m/min, N₂+H₂ atmosphere | TFI or LFI with N₂+H₂ atmosphere enclosure, 150–250 kW, 30–100 kHz | 50 kHz | Non-magnetic — higher frequency required. Atmosphere enclosure mandatory. TFI preferred for width uniformity. |
| Aluminum alloy 6061 strip 600 mm wide, 1.5 mm thick, anneal at 380°C, 30 m/min | TFI Transverse Flux, 200–350 kW, 10–30 kHz | 15 kHz | Wide aluminum — TFI essential. Lower frequency for thicker aluminum (skin depth matching). Tight temperature control required — narrow process window. |
| High-carbon spring steel strip 50 mm wide, 1.0 mm thick, continuous hardening and tempering | Multi-Zone LFI: Zone 1 (hardening, 900°C, 80 kW, 50 kHz) + water quench + Zone 2 (tempering, 350°C, 30 kW, 50 kHz) | 50 kHz | Two-stage inline process on narrow strip — LFI solenoid optimal. Multi-zone allows independent hardening and tempering temperature control. |
| Steel strip edge preheating before roll forming mill, 400 mm wide strip, edge zone only ±20 mm, 200°C, 60 m/min | Edge Induction Heaters × 2 (one per edge), 15 kW each, 50 kHz | 50 kHz | Only edge zones require heating — edge heaters minimize energy waste and prevent center strip overheating. |
| Titanium Grade 2 strip 100 mm wide, 0.5 mm thick, stress relief at 700°C, argon atmosphere, 5 m/min | Multi-Zone LFI, 40–80 kW, 30–80 kHz, argon enclosure, controlled air cooling | 50 kHz | Reactive material — argon atmosphere mandatory. Multi-zone ramp control prevents thermal shock. Slow line speed — compact heating zone, low power. |
| Cold-rolled carbon steel strip 800 mm wide, 2.0 mm thick, full anneal at 700°C, 40 m/min | TFI, 600–800 kW, 3–8 kHz, N₂ atmosphere | 5 kHz | Heavy gauge wide steel — large thermal mass requires high power TFI. Low frequency penetrates 2 mm thickness effectively below Curie point. |
Process Workflow
The following step-by-step workflow describes the complete operating sequence for a continuous induction strip heating station integrated into a production line. The sequence is applicable to LFI and TFI configurations; multi-zone systems follow the same steps repeated per zone.
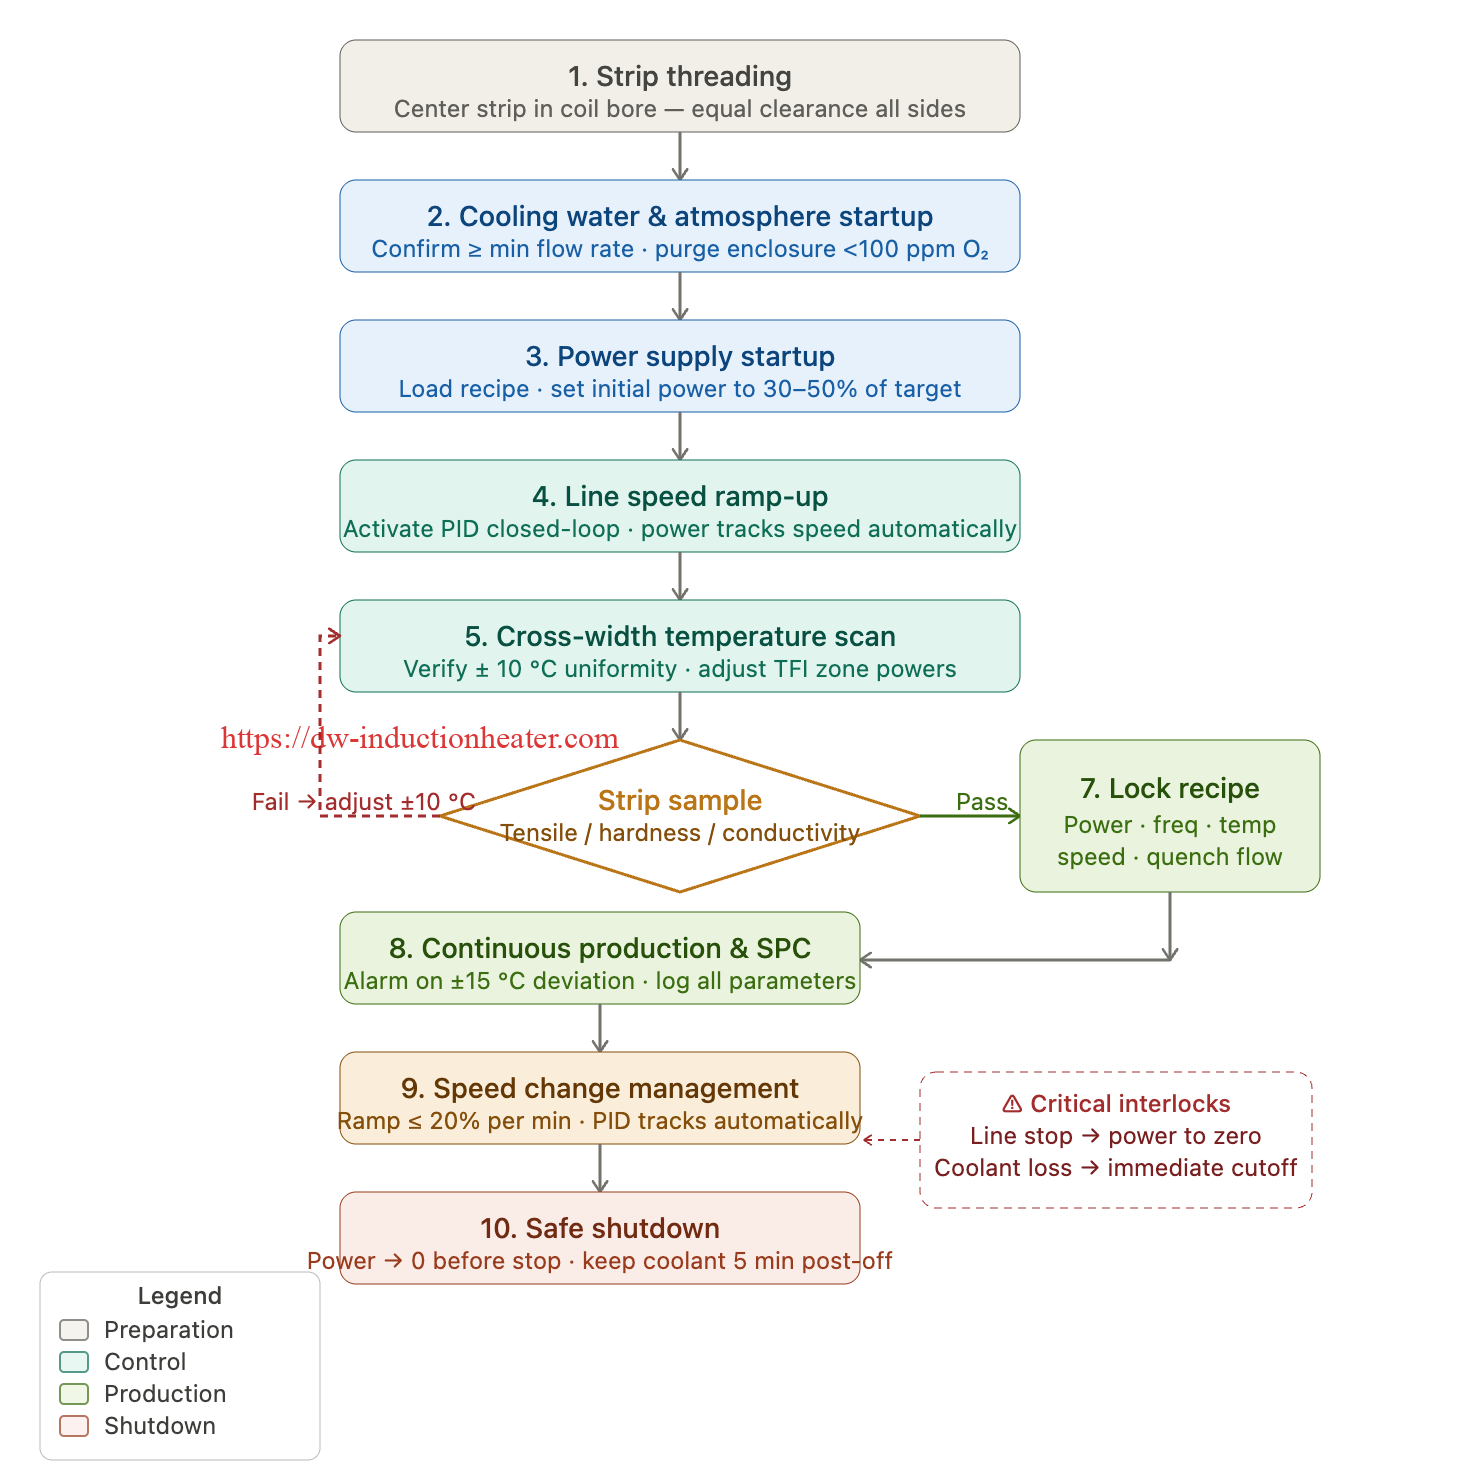
- Strip threading and coil alignment check. Thread the strip from the pay-off reel or upstream process through the induction coil and into the downstream cooling or quench section. Verify that the strip runs centered through the coil bore or TFI gap with equal clearance on all sides. For LFI solenoid coils, check centering using a feeler gauge or laser alignment tool. For TFI coils, verify that both upper and lower coil segments are equally spaced from the strip surface. Misalignment causes non-uniform cross-width heating and is the most common source of quality variation.
- Cooling water and atmosphere system startup. Start coil cooling water flow and confirm ≥ minimum flow rate at the coil return line. For atmosphere-controlled applications, purge the enclosure with the specified gas (nitrogen, argon, or forming gas) for a minimum of 3 volumes of the enclosure space before starting the power supply. Confirm O₂ level in enclosure is below 100 ppm using inline oxygen analyzer before heating above 600°C for oxidation-sensitive materials.
- Power supply startup and initial parameter loading. Power up the IGBT induction power supply and load the process recipe for the current strip grade and dimensions. The recipe contains: frequency set-point, initial power set-point (30–50% of target), temperature set-point, PID control parameters, and alarm limits. Do not apply full power immediately — the gradual startup protects the coil from thermal shock and allows the strip to reach temperature smoothly.
- Line speed ramp-up with closed-loop temperature control activation. Start the line at 30–50% of target line speed. Activate closed-loop temperature control using the exit IR pyrometer as the feedback sensor. As line speed increases, power output automatically increases to maintain the temperature set-point. Allow the system to stabilize for 60–120 seconds at each speed increment before continuing.
- Cross-width temperature verification. Once the line is running at target speed and temperature, perform a cross-width temperature scan using a scanning pyrometer or thermal camera. Record temperatures at the strip center, quarter-width positions, and each edge. Acceptable uniformity tolerance is typically ±10°C for general annealing and ±5°C for critical applications. Adjust individual TFI segment powers or reposition coil if uniformity is outside tolerance.
- Strip sampling and quality verification. After 3–5 minutes of stable production, sample 500–1,000 mm of strip from the take-up reel. Perform tensile testing (yield strength, UTS, elongation), hardness measurement, and metallographic examination as required by the material specification. Adjust temperature set-point in ±10°C steps if properties are outside specification.
- Process recipe locking and production start. Once all quality checks are confirmed, lock the process parameters into the recipe management system. Document the verified parameters as the baseline for this material-speed combination. Production can now proceed with automatic temperature regulation and alarm monitoring.
- Continuous monitoring and SPC logging. The control system continuously logs strip exit temperature, power output, frequency, and line speed at configurable intervals (typically 1–10 seconds). Statistical process control (SPC) charts for temperature are monitored in real time. Alarms are configured for temperature deviations >±15°C from set-point, power output exceeding 95% of rated capacity, or cooling water flow below minimum.
- Speed change management. When line speed changes are required, the closed-loop temperature controller adjusts power automatically. For speed changes greater than ±30% of operating speed, program the speed change as a ramp over 30–60 seconds to allow the temperature controller to track without overshoot. Very large speed steps may temporarily exceed controller range — monitor exit temperature manually during such transitions.
- Safe shutdown procedure. Reduce power set-point to zero before stopping the line. Never stop strip motion while induction power is at full output — the stationary strip segment in the coil will overheat and may oxidize, anneal unevenly, or in extreme cases melt. After power-down, keep cooling water flowing for a minimum of 5 minutes to remove residual heat. For atmosphere-controlled systems, maintain gas flow until the coil enclosure temperature drops below 200°C.

Common Problems and Solutions
| Problem | Root Cause | Solution | Prevention |
|---|---|---|---|
| Non-uniform cross-width temperature (hot or cold edges) | TFI coil misalignment; flux concentrator degradation at coil edges; strip running off-center in coil bore | Realign coil segments to equal gap across strip width. Replace worn flux concentrators. Adjust strip guide rollers to restore centerline tracking. | Scheduled coil gap verification every 500 hours. Flux concentrator condition inspection monthly. Install strip edge position sensors with automatic guide correction. |
| Strip temperature oscillating (hunting) in closed-loop control | PID gains too high (proportional or integral); pyrometer response time too slow for line speed; power supply response latency | Reduce proportional gain by 30–50%. Increase derivative gain. Switch to faster pyrometer (response time <5 ms). Enable feed-forward control from line speed signal. | Commission PID tuning at actual production speed. Use pyrometers with <1 ms response time for high-speed lines (>100 m/min). Include line speed as feed-forward input to power controller. |
| Surface oxidation on copper strip at annealing temperature | Insufficient quench water flow rate; coil exit to quench gap too long; residual oxygen in N₂ atmosphere enclosure | Increase quench flow rate. Reduce coil exit-to-quench distance to <50 mm. Verify atmosphere O₂ level <50 ppm. Lower temperature set-point by 20°C. | Install O₂ analyzer on atmosphere enclosure with interlock. Inspect quench nozzle condition weekly. Design quench box to start within 30 mm of coil exit. |
| Strip breaking inside the coil | Tension upset from upstream coil change or strip weld passing through at reduced tension; thermal stress from temperature spike during slow pass; strip defect (hole, edge crack) acting as stress concentration | Install tension monitoring with power interlock — automatically reduce power to 20% if tension drops below threshold. Slow line speed during strip weld pass-through. | Add strip break sensor (optical) with immediate power cutoff. Configure coil power to reduce proportionally with line speed below 50% of set speed. Inspect incoming strip for edge cracks before processing. |
| Induction coil arcing to strip surface | Strip flutter reducing coil-strip clearance below electrical safety gap; coil bore contaminated with conductive debris; strip camber exceeding coil clearance | Increase coil bore clearance by 5–10 mm. Clean coil bore interior. Add ceramic anti-flutter guides at coil entry and exit. Check strip flatness and camber before entry. | Inspect coil bore for arc marks and metallic contamination weekly. Apply ceramic coating to coil bore inner surface. Install electromagnetic strip stabilizer upstream of coil for high-speed lines. |
| Insufficient heating at high line speed | Power supply at rated maximum — insufficient installed power for throughput; frequency mismatch reducing coupling efficiency; coil coupling gap too large | Verify power calculation vs. installed rating. Add second induction heating module in series. Reduce coil-strip clearance. Check resonant frequency matching. | Size power supply with 25–30% margin above calculated requirement. Verify coil impedance matching at design line speed during commissioning. Document maximum certified line speed for each product. |
| Aluminum strip over-softened (tensile strength below minimum) | Annealing temperature too high; line speed too low; incorrect temperature set-point for alloy variant | Reduce temperature set-point in 5°C steps. Increase line speed. Verify alloy certificate and compare recrystallization temperature against assumed value. | Maintain separate process recipes for each aluminum alloy grade. Program alloy-specific temperature limits in the control system to prevent operator set-point errors. |
| Stainless steel sensitization after annealing | Cooling rate too slow in 550–850°C sensitization range after solution anneal; water quench flow insufficient | Increase quench water flow rate. Inspect quench nozzle for blockage. Reduce temperature set-point to minimize time above 900°C if solution was achieved at lower temperature. | Design quench system to achieve cooling rate >50°C/second through 900–550°C range for standard 304/316 grades. Perform Huey test (boiling nitric acid corrosion) on production samples periodically. |
Real Engineering Case Studies
Case Study 1: Copper Strip Continuous Annealing Line, Electronics Connector Manufacturer, Germany
Requirement: A European electronics connector manufacturer needed to replace a 25-meter resistance furnace annealing line for ETP copper strip (width 80 mm, thickness 0.4 mm) running at 15 m/min with a system that could fit within a 3-meter floor space constraint imposed by a factory expansion. Target exit condition: HV 60–75 (fully soft annealed), elongation ≥ 35%, conductivity ≥ 100% IACS.
HLQ Solution: LFI solenoid induction heating system, 60 kW, 150 kHz, 350 mm heating zone length, integrated water quench box, open-air operation with nitrogen collar at coil exit. Closed-loop IR pyrometer temperature control with set-point 560°C.
Results: Installed footprint 2.4 meters total (heater + quench + dryer). Exit temperature stability ±6°C over full production shift. HV 62–70 measured across 50 production coils — consistently within specification. Conductivity 101.2% IACS average. Energy consumption 38% lower than replaced resistance furnace on equivalent tonnage. Line startup from cold in under 2 minutes versus 45-minute furnace warm-up.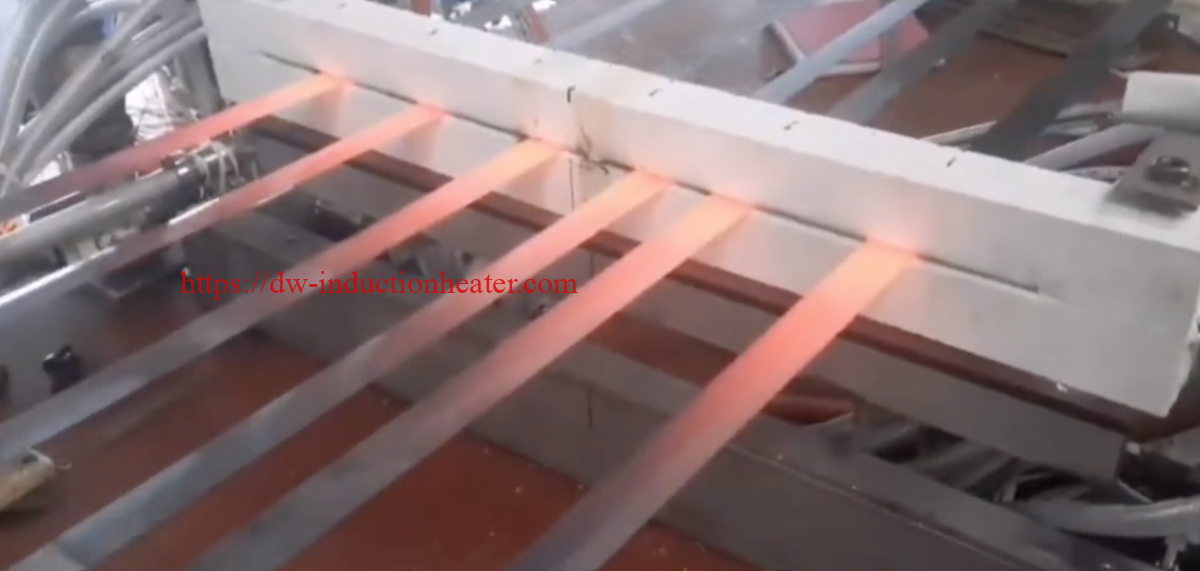
Case Study 2: Wide Carbon Steel Strip Galvanizing Preheat, Steel Service Center, South Korea
Requirement: Integration of an induction preheating system immediately upstream of the zinc bath in an existing continuous hot-dip galvanizing line. Strip specifications: low carbon steel, width 900–1,250 mm (variable), thickness 0.6–2.5 mm, line speed 40–120 m/min (variable). Required preheat temperature at zinc bath entry: 460°C ±15°C across full width regardless of speed or gauge change.
HLQ Solution: TFI transverse flux induction heating system, 1,200 kW total (two 600 kW modules in series), 5 kHz operating frequency, active edge compensation coils, independent cross-width power profiling across 5 lateral zones, closed-loop speed feed-forward control, dual-point IR pyrometer at zone 1 exit and zone 2 exit.
Results: Cross-width temperature uniformity ±8°C achieved at all tested gauge and speed combinations. Speed change from 60 to 100 m/min managed within 12 seconds with temperature deviation <±15°C during transition. Zinc adhesion defect rate reduced from 0.8% to 0.12% of coil surface area. System paid back capital cost in 14 months from reduced zinc consumption and eliminated pre-bath rejects.
Case Study 3: Spring Steel Strip Continuous Hardening and Tempering Line, Automotive Spring Manufacturer, China
Requirement: Replace a 60-meter gas-fired salt bath patenting and tempering line for 65Mn spring steel strip (width 20–80 mm, thickness 0.8–3.0 mm, line speed 5–25 m/min). Target final properties: HRC 44–50, tensile strength 1,380–1,520 MPa, elongation ≥8%.
HLQ Solution: Four-zone LFI multi-zone induction system: Zone 1 (austenitizing, 900°C, 120 kW, 30 kHz, N₂ atmosphere) + polymer quench section + Zone 2 (pyrometer-verified martensite check) + Zone 3 (first temper, 380°C, 60 kW, 50 kHz) + Zone 4 (second temper, 420°C, 60 kW, 50 kHz) + final air cooling section. Full PLC control with recipe management for 24 product combinations.
Results: Eliminated lead and salt bath — zero hazardous waste discharge. HRC 45–49 across 95% of production coils, compared to HRC 42–52 range from old line. Tensile strength 1,410–1,490 MPa (tighter than specification). Floor space reduced from 60 meters to 18 meters. Energy cost reduced by 47% on equivalent output. Line qualification approved by Tier 1 automotive customer on first audit.
Case Study 4: Stainless Steel 304 Thin Strip Solution Annealing, Medical Device Component Supplier, USA
Requirement: Continuous solution annealing of cold-rolled 304 stainless steel strip (width 60 mm, thickness 0.15–0.6 mm) for medical instrument blanks. Required exit hardness: HV ≤ 200 (fully soft), grain size ASTM 8–10, no sensitization detectable by oxalic acid etch test. Bright surface finish required — no scale, no discoloration.
HLQ Solution: Multi-zone LFI system, two 40 kW zones in series, 100 kHz, total heated length 600 mm, set-point 1,080°C, sealed N₂+5%H₂ forming gas enclosure, immediate water quench with deionized water at <20°C, post-quench drying. Oxygen-controlled atmosphere system with <20 ppm O₂ interlock.
Results: HV 155–185 across all thickness variants. ASTM grain size 8–9 confirmed by metallographic review of 100 production coils. Zero sensitization in oxalic acid etch tests across 6-month production period. Surface brightness equivalent to No. 2B finish without additional rolling. Lot-to-lot consistency improved significantly versus previous bell furnace annealing process, reducing customer incoming inspection failure rate from 3.2% to 0.1%.
Standards and Safety Considerations
Induction strip heating systems must comply with applicable electrical, mechanical, and process safety standards in the jurisdiction of installation. The following standards and safety requirements are most commonly applicable to industrial induction strip heating installations.
Applicable Standards
| Standard / Directive | Scope | Applicability |
|---|---|---|
| IEC 60519-1 | Safety in electroheat installations — general requirements | All induction heating systems globally |
| IEC 60519-10 | Safety in electroheat installations — particular requirements for induction heating equipment | Industrial induction heating systems including strip heaters |
| EU Low Voltage Directive (2014/35/EU) | Electrical safety of equipment operating at 50–1,000V AC / 75–1,500V DC | European installations — CE marking required |
| EU EMC Directive (2014/30/EU) | Electromagnetic compatibility — limits for conducted and radiated emissions | European installations — CE marking required |
| NFPA 86 | Standard for ovens and furnaces (atmosphere-controlled systems) | North American installations with controlled atmosphere enclosures (N₂, H₂, forming gas) |
| OSHA 29 CFR 1910.303 | Electrical safety — general industry wiring requirements | North American installations |
| ICNIRP Guidelines | Electromagnetic field exposure limits for workers | All installations — operator EMF exposure assessment required above 50 kHz at high power |
| ISO 9001 / IATF 16949 | Quality management system requirements | Automotive supplier installations; HLQ manufacturing process |
Key Safety Requirements for Induction Strip Heating Systems
Cooling water interlock: The induction power supply must be interlocked with the cooling water flow switch so that the system cannot operate without confirmed minimum flow. Loss of cooling water destroys the induction coil within seconds at rated power. A flow switch on the coil return line with hardwired power cutoff — not software interlock alone — is mandatory.
Strip break / line stop interlock: A line stop sensor (tension monitor or speed encoder) must be hardwired to immediately reduce induction power to zero when the line stops or strip tension drops below a minimum threshold. A stationary strip segment in a powered coil at full output will overheat in under 1 second for thin strip at high power density.
Atmosphere enclosure safety: For systems operating with nitrogen, hydrogen, or forming gas atmospheres, the enclosure must be purged to below 1% oxygen before heating commences and maintained in purge condition during operation. Hydrogen-containing atmospheres require explosion-proof electrical installations within the hazardous zone, automatic gas detection, and thermal cut-off at purge failure. Comply with NFPA 86 or equivalent national standard.
Electromagnetic field (EMF) safety: At operating frequencies above 10 kHz and power levels above 50 kW, the magnetic field in the vicinity of the induction coil may exceed occupational exposure limits defined by ICNIRP guidelines. Operators should not stand within 0.5–1.5 m of the coil during operation. Workers with cardiac pacemakers or metal implants must not operate near high-power induction systems. EMF boundary marking, safety signage, and restricted access zones are required.
Electrical isolation and lockout/tagout (LOTO): The induction power supply cabinet must be equipped with a lockable main isolator switch. Maintenance procedures require full LOTO compliance before accessing the coil, capacitor bank, or IGBT module compartments. Note that resonant capacitors in induction power supplies retain dangerous charge after mains isolation — a minimum 5-minute discharge wait (or verified discharge) is mandatory before opening the capacitor compartment.
Why Choose HLQ Induction Equipment?
HLQ Induction Equipment is a specialist manufacturer of industrial induction heating systems with a dedicated engineering team focused exclusively on electromagnetic heat treatment technology. For induction strip heating applications specifically, HLQ offers capabilities that general-purpose induction heating suppliers cannot match.
In-House Application Engineering
HLQ’s application engineering team performs complete process design for every strip heating inquiry: power calculation from actual strip dimensions and line speed data, frequency selection based on material properties and skin depth analysis, coil geometry design, and thermal simulation of cross-width temperature uniformity. This is not a sales process — it is engineering verification that the proposed system will meet specification before any order is placed.
Custom Coil Design and Fabrication
Induction coils for strip heating — particularly TFI flux concentrator assemblies and profiled edge heater coils — are precision engineered components. HLQ fabricates all coils in-house from oxygen-free copper, with computer-modeled flux concentrator geometry to achieve specified cross-width uniformity. Coils are hydraulically tested before installation and are available as spare parts with 48-hour global shipping.
Full System Integration
HLQ supplies complete induction strip heating stations including power supply, coil assembly, atmosphere enclosure, cooling water manifold, quench system, IR pyrometer, and PLC control panel — as a single integrated module with one point of electrical and water connection to the production line. This approach eliminates multi-supplier integration complexity and provides a single source for performance warranty and after-sales support.
Proven Performance in Demanding Applications
HLQ strip heating systems have been installed in steel mills, copper rolling mills, aluminum processing lines, medical device manufacturing, and aerospace component processing in over 40 countries. Customer case studies demonstrate consistent achievement of ±5°C temperature uniformity, 90%+ energy efficiency, and >8,000 hours annual operating availability in continuous production environments.
After-Sales Support and Spare Parts
Every HLQ strip heating system is supplied with full electrical schematics, PLC source code, and a spare parts list. Critical spare parts — IGBT modules, capacitor banks, flux concentrator materials, coil assemblies — are stocked and available for 48-hour global express delivery. Remote diagnostic capability via VPN allows HLQ engineers to access the control system and diagnose faults without on-site travel for most electrical and control issues.
| HLQ Strip Heating Capability | Specification |
|---|---|
| Strip width range | 5 mm – 2,000 mm |
| Strip thickness range | 0.05 mm – 25 mm |
| Power range | 15 kW – 2,000 kW per station |
| Frequency range | 1 kHz – 500 kHz |
| Line speed capability | 0.5 m/min – 1,200 m/min |
| Temperature range | 100°C – 1,150°C |
| Temperature uniformity | ±3°C – ±10°C cross-width |
| Countries served | 40+ |
| Warranty | 24 months on power electronics |
| Certifications | CE, ISO 9001 |
FAQ
What is the difference between longitudinal flux and transverse flux induction strip heating?
In longitudinal flux induction (LFI), the strip passes through a solenoid coil and the magnetic field is parallel to the strip travel direction. Induced currents flow around the strip perimeter. LFI is optimal for narrow strip (under 200 mm) and rod or bar. In transverse flux induction (TFI), coil segments above and below the strip create a field that passes perpendicular through the strip thickness. Induced currents flow along the strip surface in the travel direction. TFI achieves superior cross-width uniformity for wide strip and is significantly more efficient for very wide, thin material where an LFI solenoid coil would need to be impractically large to enclose the full strip width.
Can induction strip heating replace a conventional continuous annealing furnace?
Yes, in most cases. Induction strip heating can replace or supplement the heating sections o f a conventional continuous annealing line. The primary trade-off is heated zone length: a gas or resistance furnace typically includes a long soak section after heating to allow temperature equalization through the strip thickness, while induction heating at the correct frequency can
achieve full through-temperature in the heating coil itself (for strip thickness ≤ 2× skin depth) without a separate soak. For very thick strip (>8 mm) requiring long soak times, a hybrid system — induction fast heating followed by a short holding furnace — is the recommended approach. For thin strip (under 4 mm), induction replacement of the full furnace heating section is straightforward.
How is cross-width temperature uniformity achieved in wide strip heating?
For TFI systems, cross-width uniformity is achieved through flux concentrator geometry design (shaping the magnetic field distribution across the strip width), active lateral zone control (splitting the TFI coil into 3–8 independently powered segments across the strip width), and edge compensation coils that counteract the naturally lower power density at strip edges. For LFI systems with narrow strip, uniformity is primarily a function of coil bore centering and frequency selection ensuring adequate skin depth relative to strip width. Thermal simulation using FEM (finite element method) is performed at the design stage to predict cross-width temperature distribution and optimize coil geometry before manufacture.
What atmosphere is required for induction strip annealing of stainless steel?
Austenitic stainless steel annealed above 900°C in air will develop a chromium oxide scale that requires pickling (nitric-hydrofluoric acid treatment) to remove before further processing. For a bright, scale-free finish, an atmosphere of nitrogen with 3–10% hydrogen (forming gas, also called dissociated ammonia) is used. The hydrogen reduces any residual oxide on the strip surface and prevents re-oxidation. Oxygen level inside the atmosphere enclosure must be maintained below 50 ppm, verified by continuous oxygen analyzer. For applications where a small amount of surface oxide is acceptable, pure nitrogen (O₂ < 200 ppm) is sufficient and avoids the explosion risk associated with hydrogen-containing atmospheres.
How is power calculated for an induction strip heating system?
The required thermal power is: Pthermal = w × t × v × ρm × Cp × ΔT, where w is strip width (m), t is thickness (m), v is line speed (m/s), ρm is density (kg/m³), Cp is specific heat (J/kg·°C), and ΔT is temperature rise (°C). Divide by system efficiency (0.82–0.90) to get electrical power. Add 25% design margin. For example: annealing 600 mm wide × 1.0 mm thick copper strip at 20 m/min (0.333 m/s) from 20°C to 550°C: P = 0.6 × 0.001 × 0.333 × 8,900 × 385 × 530 / 0.85 ≈ 477 kW → select 500 kW system with 25% margin built in.
How do I choose power for strip induction heating?
Power selection depends on strip width, thickness, material density, specific heat, line speed and target temperature rise. Engineers calculate mass flow rate and heat duty, then add efficiency correction and safety margin for real production losses.
How is strip temperature controlled?
Strip temperature is usually controlled with infrared pyrometers, thermal cameras, line-speed encoder feedback and PLC power regulation. For wide strip, multiple temperature measurement points or segmented power control may be required.
Can induction strip heating replace a gas furnace?
In some applications, yes. Induction heating can replace or reduce the load of gas or resistance furnaces when fast response, compact layout, localized heating and electric process control are required. In other cases, induction works best as a booster before or after an existing furnace.
What causes strip edge overheating?
Edge overheating can be caused by transverse flux edge effects, incorrect coil width, poor strip centering, excessive power density or lack of magnetic shielding. The solution is coil redesign, edge compensation, segmented control or better strip positioning.