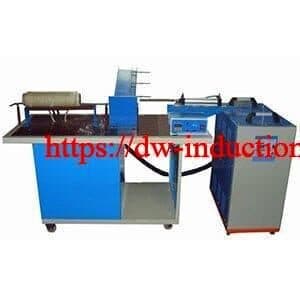
RF Forging Bars Induction Machinery
70kW Induction Forging Machine – Medium Frequency Steel Bar and Rod Heating Equipment
What Is an RF Induction Forging Bar Heating Machine?
An induction forging machine is industrial electromagnetic heating equipment designed to rapidly heat metal bars, steel rods, and billets to the required temperature before hot forging, upsetting, extrusion, and other metal forming processes.
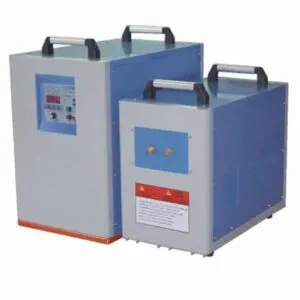
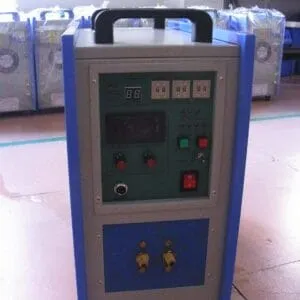
The HLQ DW-MF-70KW RF Forging Bars Induction Machinery is a 70kW medium-frequency induction heating system operating at 1–20kHz. It uses solid-state IGBT inverter technology to generate controlled electromagnetic heating for steel bars, metal rods, billets, and other conductive metal components.
Unlike conventional gas-fired furnaces, induction forging equipment generates heat directly within the metal workpiece through induced electrical currents. This enables rapid heating, localized temperature control, and repeatable processing when the induction coil and operating conditions are properly designed.
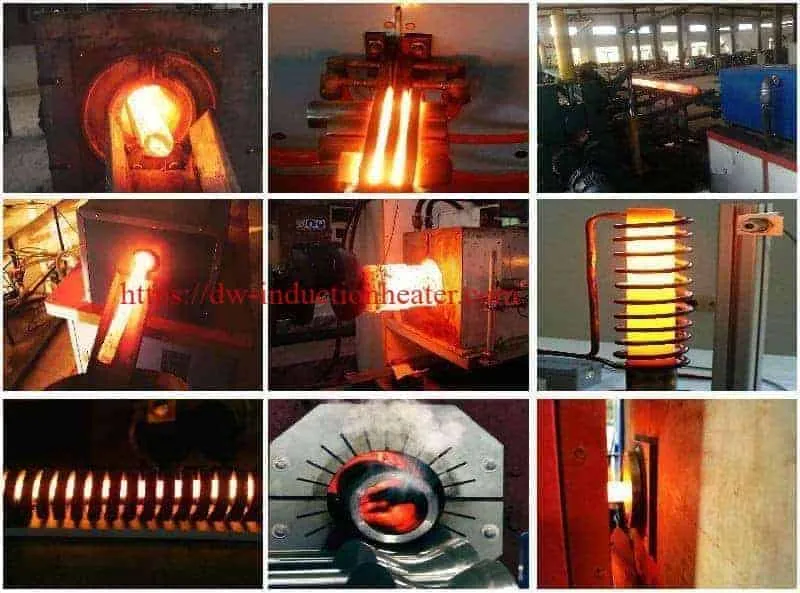
The DW-MF-70KW is suitable for selected industrial heating applications, including:
- Steel bar induction heating for forging
- Steel rod end heating and upsetting
- Carbon steel and alloy steel forging
- Small and medium metal billet heating
- Copper and brass bar heating
- Aluminum rod and billet heating
- Metal tube-end heating before extrusion
- Induction shrink fitting and thermal assembly
- Selected shaft and gear heat-treatment applications
- Industrial mold and die preheating
Manufactured by HLQ Induction Equipment Co., Ltd., the DW-MF-70KW combines medium-frequency electromagnetic heating, an IGBT parallel inverter circuit, water cooling, and multiple electrical protection functions.
For additional power ratings and industrial configurations, explore HLQ’s
industrial induction heating power supplies.
Important: Although the product is described as RF forging bars induction machinery, the published frequency range of 1–20kHz places this model within HLQ’s medium-frequency induction heating series.
Key Features of the 70kW Medium Frequency Induction Forging Machine
- 70kW Maximum Oscillation Power:
Provides substantial induction heating capability for selected steel bar forging and industrial metal heating applications. - 1–20kHz Operating Frequency:
Medium-frequency operation supports applications requiring relatively deep electromagnetic penetration. - IGBT Inverter Technology:
Solid-state power electronics provide controlled electrical energy for induction heating. - Three-Phase 380V Electrical Input:
Designed for industrial power supply installations. - Water-Cooled Heating Circuit:
Supports thermal management of the power supply and compatible induction heating components. - 100% Published Duty Cycle:
Designed for continuous operation at 40°C under specified conditions. - Customized Induction Coils:
Coils can be designed for different bar diameters, heating lengths, and metal materials. - Integrated Protection Functions:
Overvoltage, overcurrent, overheating, phase-loss, and cooling-water shortage protection. - Flexible Industrial Applications:
Steel bar forging, billet heating, rod upsetting, hot forming, and thermal assembly.

DW-MF-70KW Induction Forging Machine Technical Specifications
The DW-MF-70KW medium frequency induction forging machine uses an IGBT parallel inverter circuit to generate electromagnetic heating power for industrial metal processing.
The following technical specifications are based on the published product information.
| Technical Parameter | Specification |
|---|---|
| Product Name | RF Forging Bars Induction Machinery |
| Product Category | Medium Frequency Induction Forging Equipment |
| Manufacturer | HLQ Induction Equipment Co., Ltd. |
| Brand | HLQ |
| Model Number | DW-MF-70KW |
| Published Maximum Oscillation Power | 70kW |
| Operating Frequency | 1–20kHz |
| Input Voltage | Three-Phase AC 380V ±10% |
| Input Frequency | 50/60Hz |
| Published Maximum Input Current | 105A |
| Power Electronics | IGBT |
| Inverter Configuration | Solid-State Parallel Inverter |
| Heating Technology | Medium Frequency Electromagnetic Induction |
| Cooling Method | Water Cooling |
| Published Cooling Water Pressure | >0.2MPa |
| Published Cooling Water Flow | 6L/min |
| Published Duty Cycle | 100% at 40°C |
| Generator Dimensions | 560 × 270 × 470mm |
| Capacitor Unit Dimensions | 550 × 300 × 420mm |
| Generator Net Weight | Approximately 45kg |
| Capacitor Unit Net Weight | Approximately 55kg |
| Connecting Cable Length | 2–6m |
| Electrical Protection | Overvoltage and Overcurrent Protection |
| Additional Protection | Overtemperature, Phase-Loss and Water-Shortage Protection |
| Induction Coil | Customized According to Workpiece Requirements |
| Suitable Materials | Carbon Steel, Alloy Steel, Copper, Brass, Aluminum and Other Conductive Metals |
| Primary Application | Steel Bar and Rod Heating for Forging |
| Additional Applications | Billet Heating, Shrink Fitting, Hot Forming and Heat Treatment |
| Production Integration | Manual or Customized Automated Heating Station |
| Manufacturing Country | China |
Engineering Note: The published 70kW rating is described as maximum oscillation power. The actual continuous output capability should be confirmed against the supplied equipment configuration.
The published cooling-water flow of 6L/min should also be verified for the complete system, including the generator, capacitor unit, induction coil, and connecting components.
Actual workpiece capacity and heating performance depend on material properties, workpiece dimensions, induction coil design, operating frequency, and required heating time.
Recommended Induction Forging Applications and Heating Parameters
The DW-MF-70KW can be configured for different industrial heating applications. The appropriate induction coil, operating frequency, and heating cycle must be selected according to each workpiece.
| Application | Material | Indicative Temperature | Heating Purpose |
|---|---|---|---|
| Steel Bar Hot Forging | Carbon Steel | 950–1200°C | Heating Before Forging |
| Alloy Steel Rod Forging | Alloy Steel | 900–1150°C | Hot Forming and Upsetting |
| Steel Billet Heating | Carbon Steel | 950–1200°C | Through-Heating Before Forging |
| Copper Bar Heating | Copper | 600–900°C | Hot Forming |
| Brass Rod Forging | Brass | 600–800°C | Hot Forging |
| Aluminum Billet Heating | Aluminum Alloy | 350–550°C | Hot Forming and Extrusion Preparation |
| Steel Tube-End Heating | Steel | Application-Dependent | Tube Forming and Expansion |
| Metal Shrink Fitting | Steel Components | Application-Dependent | Thermal Assembly |
| Mold Preheating | Tool Steel | Application-Dependent | Controlled Preheating |
Important: These temperature ranges are general engineering references, not guaranteed processing conditions. The required temperature depends on the alloy grade, forming process, metallurgical requirements, and equipment configuration.
Advantages of RF Forging Bars Induction Machinery
1. Rapid and Efficient Metal Heating
The DW-MF-70KW generates heat directly within conductive metal workpieces through electromagnetic induction.
Compared with conventional furnace heating, induction heating can reduce unnecessary thermal exposure of surrounding equipment and provide faster heating cycles for suitable workpieces.
This makes induction heating an attractive solution for repetitive steel bar forging and industrial hot forming.
2. Greater Electromagnetic Penetration
The operating frequency range of 1–20kHz makes the DW-MF-70KW suitable for evaluating applications requiring deeper electromagnetic penetration than many high-frequency surface-heating processes.
Medium-frequency induction heating is widely used for steel rods, bars, and billets requiring controlled heating before mechanical forming.
The actual temperature distribution depends on operating frequency, workpiece diameter, heating time, and thermal conduction.
3. Solid-State IGBT Inverter Technology
The machine adopts an IGBT parallel inverter circuit for industrial medium-frequency induction heating.
IGBT technology provides electronically controlled power conversion and supports industrial heating applications requiring repeatable operating conditions.
The final electrical efficiency depends on inverter design, load matching, induction coil geometry, and operating conditions.
4. Localized Heating and Reduced Material Oxidation
Induction heating allows energy to be concentrated in selected regions of a workpiece.
When the heating cycle is properly controlled, shorter high-temperature exposure may help reduce oxidation and surface scaling compared with some conventional heating arrangements.
However, oxidation also depends on temperature, exposure time, material composition, and furnace atmosphere.
5. Customized Induction Coil Design
Different workpiece diameters, lengths, and materials require different induction coil configurations.
HLQ can provide customized induction coils for metal bars, steel rods, billet ends, shafts, tubes, and other industrial components.
A properly designed induction coil helps improve magnetic coupling, heating distribution, and production repeatability.
6. Flexible Forging and Hot Forming Applications
The DW-MF-70KW can be configured for selected bar heating, rod-end forging, upsetting, and other hot forming applications.
For a related technical application, see HLQ’s
induction forging steel rod end heating
solution.
7. Industrial Continuous-Duty Design
The published equipment specification indicates a 100% duty-cycle rating at 40°C.
Continuous production requires a stable electrical supply, adequate cooling-water capacity, properly matched induction coils, and suitable operating conditions.
8. Integrated Electrical Protection
The induction heating system includes electrical and thermal protection functions for overvoltage, overcurrent, overheating, phase loss, and cooling-water shortages.
These functions help protect the equipment when combined with correct installation, machine guarding, and preventive maintenance.
Industrial Applications of the 70kW Induction Forging Machine
The DW-MF-70KW medium frequency induction forging equipment is suitable for selected metalworking processes requiring controlled heating of steel bars, rods, billets, and other electrically conductive components.
1. Steel Bar Induction Heating for Hot Forging
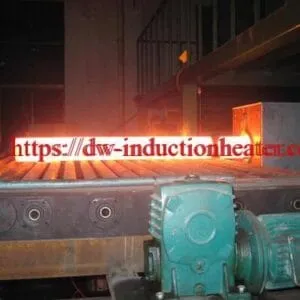
Induction heating is widely used to raise steel bars to suitable temperatures before hot forging.
During the heating process, an alternating magnetic field generates heat inside the metal workpiece.
The required forging temperature depends on the steel composition, bar dimensions, and manufacturing process.
The DW-MF-70KW can be considered for selected steel bar heating applications where the required power and frequency are compatible with the equipment.
2. Steel Rod End Heating and Upsetting
Rod-end induction heating is commonly used in the production of forged fasteners, mechanical connecting rods, shaft ends, and other formed steel components.
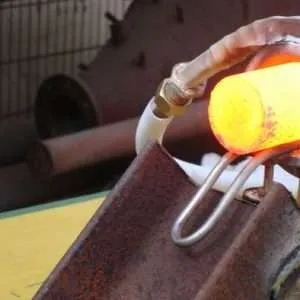
Instead of heating the complete rod, a customized induction coil concentrates heating in the required end section.
This approach can reduce unnecessary heating of the remaining workpiece and improve process flexibility.
The heating time depends on rod diameter, heated length, material properties, and required forging temperature.
3. Steel Billet Induction Heating for Forging
Medium-frequency induction heating is widely used to heat steel billets before forging, extrusion, and other hot forming operations.
Compared with higher-frequency induction heating, medium-frequency systems can provide greater electromagnetic penetration under comparable material conditions.
However, achieving a sufficiently uniform billet temperature requires appropriate coil design, heating time, and thermal equalization.
For larger billets or higher production rates, a more powerful induction heating system may be necessary.
Explore HLQ’s
induction billet heating systems for forging and extrusion
for additional equipment configurations.
4. Copper and Brass Bar Heating
The DW-MF-70KW can potentially be configured for selected copper and brass bar heating applications.
Copper and brass have different electrical conductivity and thermal properties compared with carbon steel.
Therefore, the induction frequency, heating power, and coil design must be selected according to the material and workpiece geometry.
Typical applications include localized hot forming, bar-end heating, and preparation for selected forging processes.
5. Aluminum Rod and Billet Heating
Induction heating can be used for aluminum alloy rods and billets before extrusion and hot forming.
Because aluminum is nonferromagnetic and highly conductive, its induction heating behavior differs substantially from that of ferromagnetic steel.
The appropriate frequency, heating cycle, and temperature control must be established according to the aluminum alloy and workpiece dimensions.
Excessive temperature must be avoided because different aluminum alloys have different solidus temperatures and hot-working limits.
6. Metal Tube-End Heating
The DW-MF-70KW can be considered for localized heating of suitable steel tube ends before expanding, reducing, extrusion, or other forming operations.
Customized induction coils can be designed according to tube diameter, wall thickness, and required heating length.
Temperature uniformity through the tube wall is important for preventing unwanted deformation during forming.
7. Induction Shrink Fitting and Thermal Assembly
Induction heating can be used to temporarily expand metal components during interference-fit assembly.
Typical applications include heating steel hubs, mechanical housings, shaft-mounted components, and selected industrial fittings.
The required heating temperature depends on the material’s thermal expansion coefficient, component geometry, interference allowance, and permissible thermal stress.
8. Shaft and Gear Heat Treatment
The DW-MF-70KW may be suitable for selected shaft and gear heat-treatment applications when combined with appropriate induction coils and process equipment.
For induction hardening, suitable steel must be heated to the required austenitizing temperature and subsequently quenched.
The achievable hardened depth depends on operating frequency, steel grade, heating time, and quenching conditions.
9. Mold and Die Preheating
Medium-frequency induction heating can also be applied to preheating suitable metal molds, dies, and tooling components.
The induction coil and heating cycle must be designed according to the mass, material, geometry, and target temperature of the tooling.
Controlled preheating can help reduce thermal gradients before subsequent manufacturing operations.
How Does a Medium Frequency Induction Forging Machine Work?
A medium frequency induction forging machine converts industrial electrical power into controlled alternating current, which generates an electromagnetic field through an induction coil.
The heating process generally includes the following stages.
Step 1: Industrial AC Power Input
The DW-MF-70KW receives three-phase AC electrical power.
The incoming electricity is converted through the power supply’s rectification and power conversion circuitry.
Step 2: IGBT Inverter Power Conversion
The solid-state IGBT inverter generates medium-frequency electrical power for the induction heating circuit.
The operating frequency must be compatible with the inverter, resonant circuit, induction coil, and connected workpiece.
Step 3: Alternating Magnetic Field Generation
Medium-frequency alternating current passes through the water-cooled copper induction coil.
The coil generates a changing magnetic field around the conductive workpiece.
Step 4: Eddy Current Heating
The changing magnetic field induces circulating electrical currents within the metal.
These induced currents generate heat through electrical resistance.
For ferromagnetic steels, magnetic losses may also contribute to heating below the Curie temperature.
Step 5: Heating to Forging Temperature
The metal workpiece is heated until it reaches the required processing temperature.
For through-heating applications, the cycle must allow sufficient time for heat to conduct toward the workpiece center.
Temperature uniformity should be evaluated using appropriate process monitoring and testing.
Step 6: Transfer to the Forging Operation
Once the required forging temperature is achieved, the heated workpiece can be transferred to a forging press, upsetting machine, or other forming equipment.
Workpiece transfer may be manual or automated, depending on the production requirements.
How to Select the Right Induction Forging Machine for Steel Bars
Selecting suitable induction forging equipment requires evaluating workpiece material, diameter, length, heating temperature, production capacity, and heating time.
The required average heating power can be estimated using the following relationship:
P = m × Δh / (t × η)
Where:
- P: Required average electrical heating power, kW
- m: Mass of metal being heated, kg
- Δh: Specific enthalpy increase, kJ/kg
- t: Heating time, seconds
- η: Overall heating efficiency, expressed as a decimal
This formula provides an initial engineering estimate. The enthalpy change should reflect the actual material properties and operating temperature range.
For continuous production, heating capacity can also be evaluated using the material throughput in kilograms per hour and the required energy per kilogram.
Important Parameters for Equipment Selection
| Selection Parameter | Required Information |
|---|---|
| Workpiece Material | Carbon Steel, Alloy Steel, Copper, Brass or Aluminum |
| Bar Diameter | Actual Diameter in mm |
| Workpiece Length | Actual Length in mm |
| Workpiece Weight | Weight per Piece in kg |
| Heating Length | Full-Length or Localized Heating |
| Initial Temperature | Actual Starting Temperature |
| Target Temperature | Required Forging Temperature |
| Heating Time | Seconds per Workpiece |
| Production Capacity | Pieces per Hour or kg/h |
| Electrical Supply | Voltage, Frequency and Phase |
| Automation Requirement | Manual, Semi-Automatic or Automatic |
The DW-MF-70KW should be evaluated according to the required heating capacity rather than its power rating alone.
For larger steel bars, high-volume billet production, or fully automated forging lines, higher-power industrial induction furnaces may be more appropriate.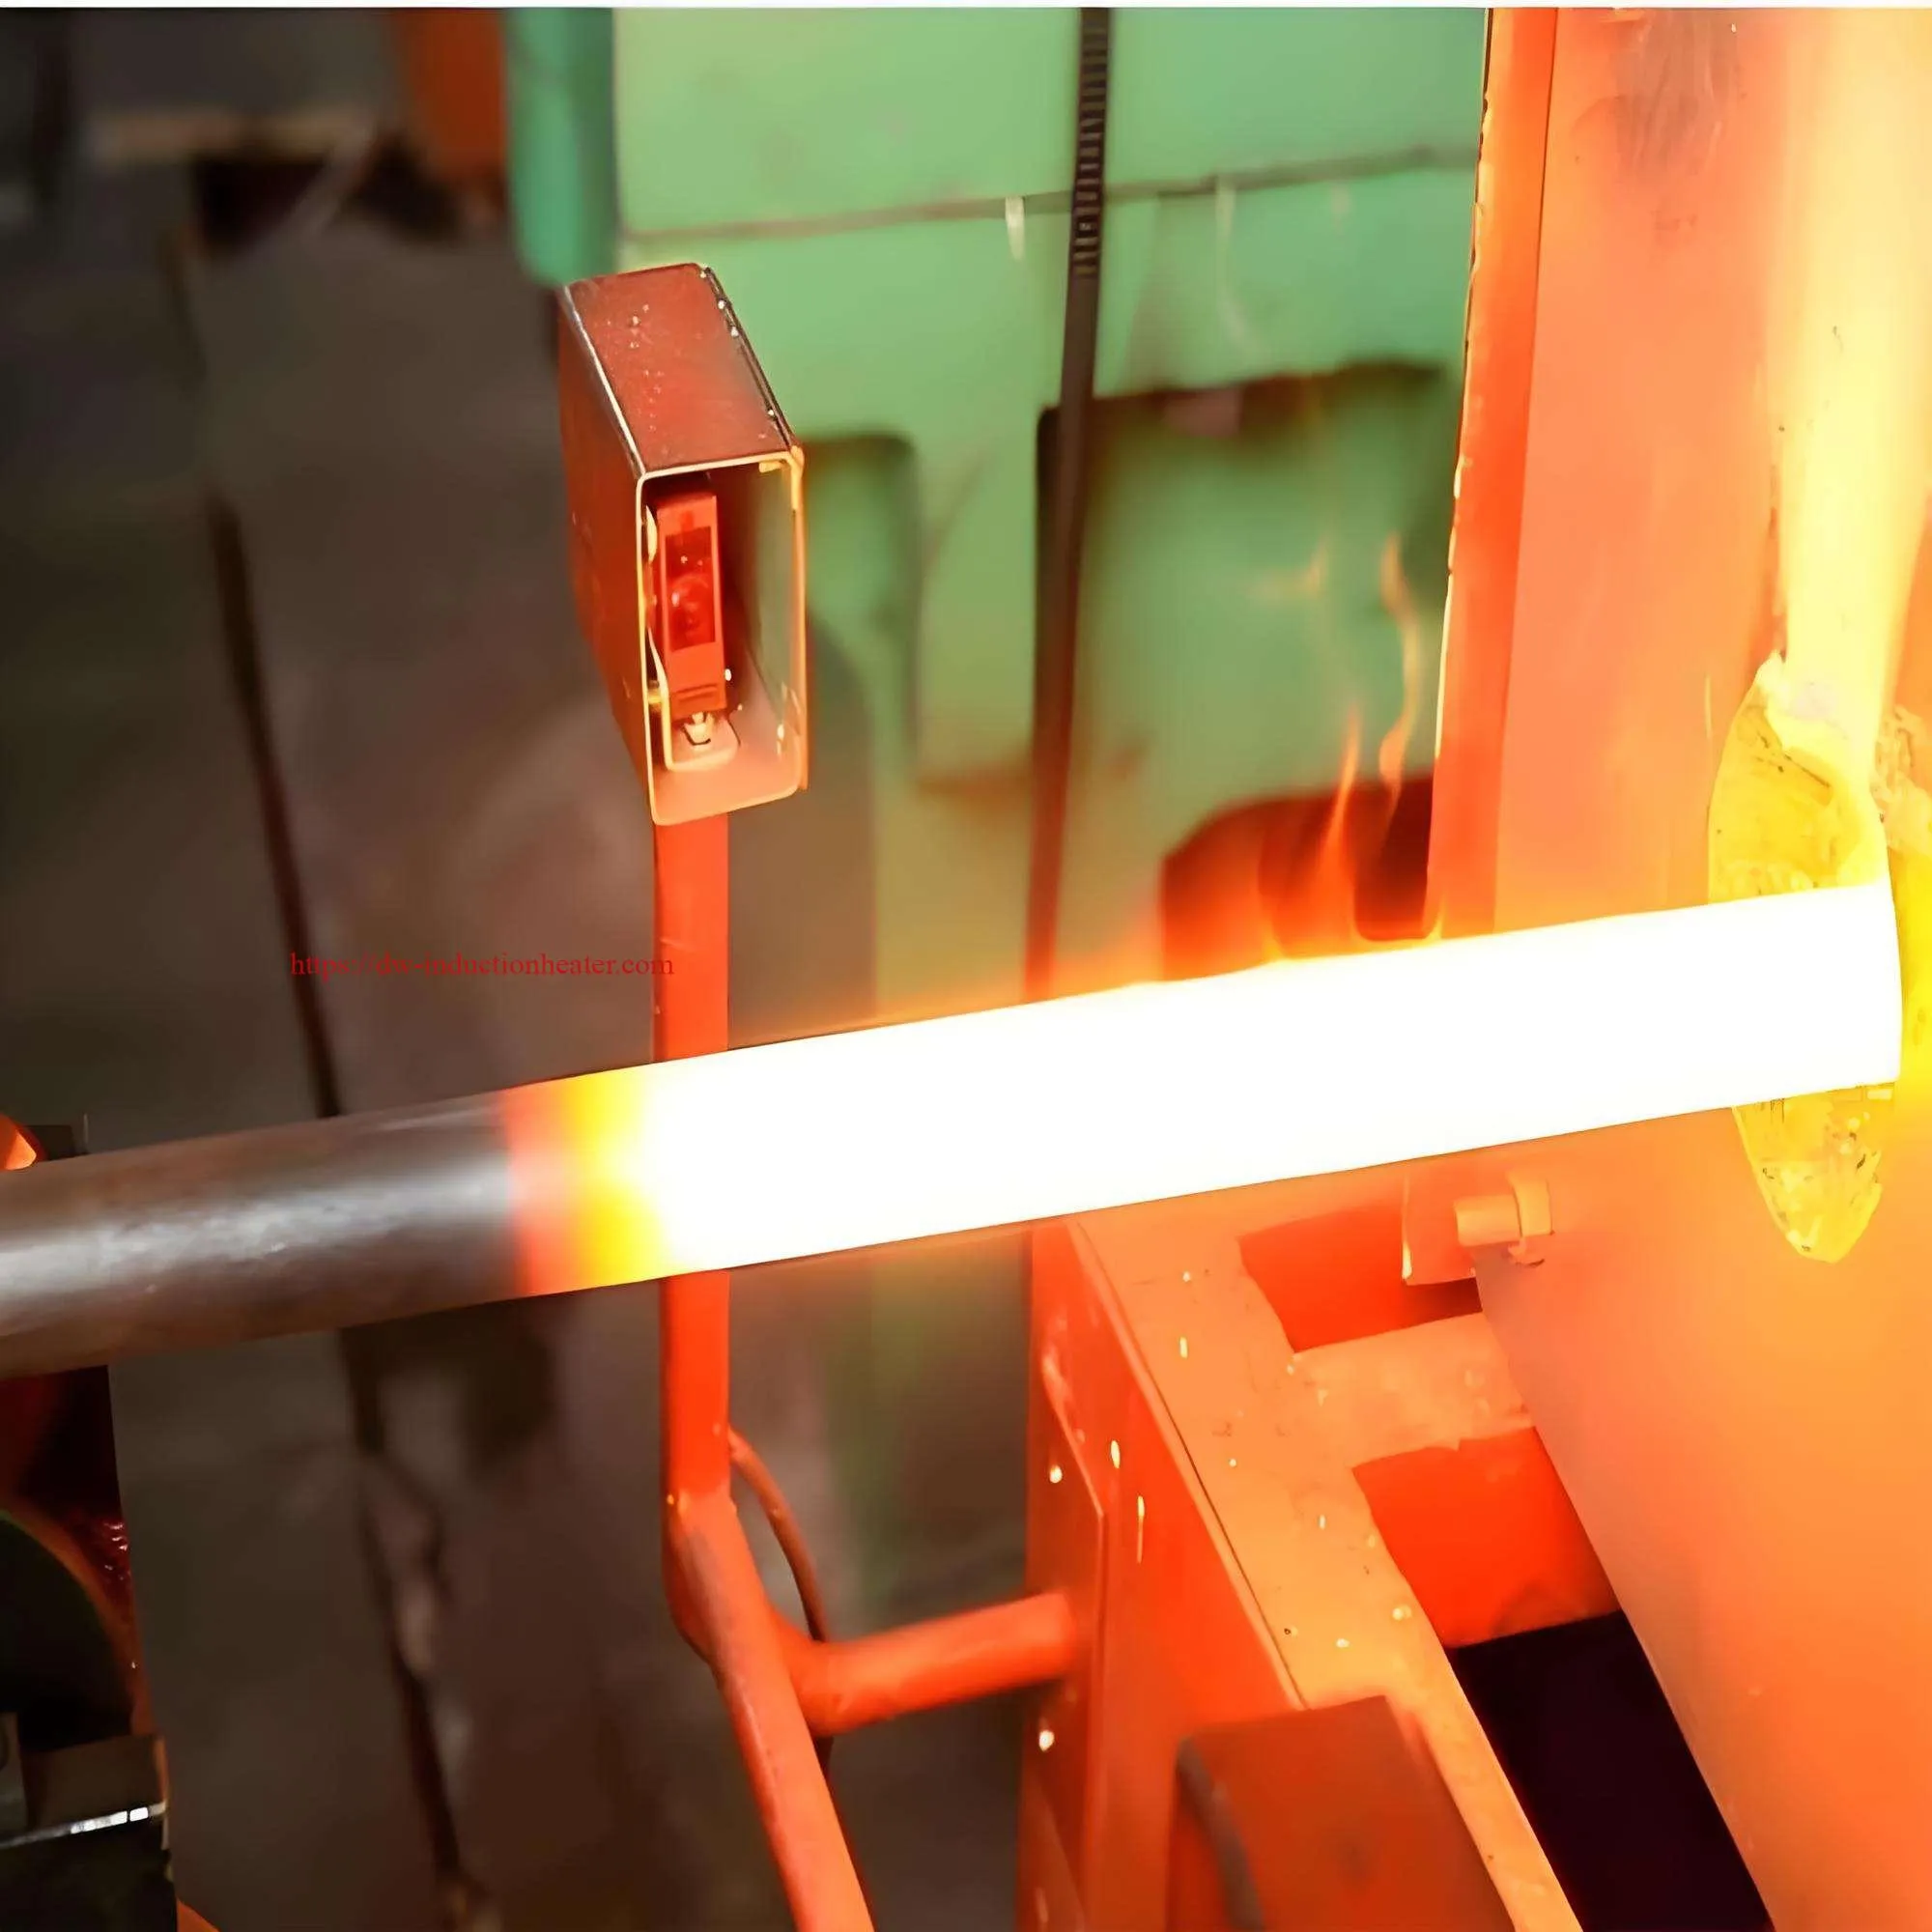
Explore HLQ’s
induction forging bar and billet furnaces
for larger-scale industrial forging applications.
FAQs About RF Forging Bars Induction Machinery
FAQ 1: What is an induction forging machine?
An induction forging machine is industrial electromagnetic heating equipment designed to heat metal rods, bars, and billets before forging or hot forming.
The induction power supply sends alternating electrical current through an induction coil, generating a changing magnetic field.
This field induces electrical currents within conductive metal workpieces, producing heat through electrical resistance.
The HLQ DW-MF-70KW is a medium-frequency induction heating machine with a published maximum oscillation power of 70kW and an operating frequency range of 1–20kHz.
Typical applications include steel bar heating, rod-end forging, billet heating, and localized metal hot forming.
FAQ 2: Is RF forging bar machinery different from medium frequency induction forging equipment?
The term RF induction heating is sometimes used broadly to describe electromagnetic induction heating equipment.
However, industrial induction heating machines are commonly classified according to their operating frequency and intended applications.
The HLQ DW-MF-70KW operates at 1–20kHz and belongs to the medium-frequency induction heating category.
This frequency range is typically associated with applications requiring greater electromagnetic penetration than many high-frequency surface-heating processes.
Therefore, the DW-MF-70KW is more accurately described as a medium-frequency induction forging machine rather than a conventional high-frequency induction heater.
FAQ 3: Can a 70kW induction forging machine heat steel bars to 1100°C?
Yes. A properly configured 70kW induction forging machine can heat suitably sized steel bars to approximately 1100°C for selected hot forging applications.
However, the achievable workpiece diameter, heating time, and production rate depend on the steel grade, bar dimensions, induction coil design, and overall heating efficiency.
Larger bars require greater thermal energy and may need additional heating time or higher installed power.
For accurate equipment selection, manufacturers should provide the bar diameter, length, material grade, target temperature, and required production capacity.
FAQ 4: What frequency is best for induction heating steel bars before forging?
The appropriate induction heating frequency depends on steel bar diameter, material properties, heating depth, and required temperature uniformity.
Lower frequencies generally provide greater electromagnetic penetration, making them useful for heating larger metal cross-sections.
Higher frequencies concentrate electromagnetic heating closer to the workpiece surface.
The DW-MF-70KW has a published operating frequency range of 1–20kHz.
The final operating frequency must be compatible with the induction coil and resonant heating circuit.
FAQ 5: What is the production capacity of a 70kW induction forging machine?
The production capacity of a 70kW induction forging machine depends on the workpiece material, dimensions, initial temperature, target temperature, heating time, and overall heating efficiency.
For steel forging applications, the required energy per kilogram depends on the steel grade and temperature range.
The number of bars heated per hour also depends on the workpiece mass and handling cycle.
The published 70kW maximum oscillation power does not independently establish a guaranteed hourly production capacity.
A reliable production estimate requires engineering calculations and, where appropriate, practical heating tests.
FAQ 6: Can induction forging equipment heat copper, brass, and aluminum bars?
Yes. Electromagnetic induction heating can be used with electrically conductive materials, including copper, brass, aluminum, carbon steel, and alloy steel.
However, each material has different electrical and thermal properties.
Copper and aluminum are highly conductive, nonferromagnetic metals, so their induction heating characteristics differ significantly from those of ferromagnetic steel.
The induction frequency, coil geometry, and heating cycle must be selected according to the material and workpiece dimensions.
The suitability of the DW-MF-70KW for a specific nonferrous application should be confirmed through engineering evaluation.
FAQ 7: Can a 70kW induction forging machine operate continuously for 24 hours?
The HLQ DW-MF-70KW has a published 100% duty-cycle rating at 40°C under specified conditions.
This indicates that the equipment is designed for continuous industrial operation when the electrical supply, cooling system, induction coil, and operating parameters meet the manufacturer’s requirements.
The published cooling-water specification is pressure above 0.2MPa and flow of 6L/min.
However, the complete installation may require additional cooling capacity.
The actual cooling requirements should be confirmed before commissioning, particularly for extended high-load operation.
FAQ 8: How do I choose the right induction forging machine for steel rods and billets?
Selecting the correct induction forging machine requires evaluating the workpiece material, diameter, length, weight, target temperature, heating time, and production capacity.
The required heating power depends on the thermal energy needed to raise the metal temperature within the available processing time.
Operating frequency must also be selected according to electromagnetic penetration and required temperature uniformity.
The HLQ DW-MF-70KW is a potential solution for selected steel bar forging, rod-end heating, and medium-frequency induction heating applications.
For larger billets or high-throughput forging lines, higher-power induction heating equipment may be required.
HLQ Induction Equipment Co., Ltd. can assist with power selection, frequency matching, customized coil design, and industrial heating system configuration.
Why Choose HLQ Induction Forging Equipment?
HLQ Induction Equipment Co., Ltd. manufactures industrial induction heating equipment and customized electromagnetic heating solutions for metalworking and manufacturing applications.
Our product range includes medium-frequency induction forging machines, induction heating power supplies, steel billet heating systems, induction melting furnaces, induction hardening machines, and industrial heat-treatment equipment.
The DW-MF-70KW RF Forging Bars Induction Machinery is designed for manufacturers requiring a medium-frequency heating solution for selected steel rod forging, bar heating, billet heating, and industrial hot forming.
HLQ can assist customers with equipment selection based on workpiece specifications, production requirements, induction coil geometry, and available electrical infrastructure.
Information Required for a Technical Quotation
- Workpiece material and metal grade
- Steel bar or rod diameter
- Workpiece length and weight
- Required heating length
- Initial and target temperatures
- Required heating time
- Hourly production capacity
- Available electrical supply
- Cooling-water requirements
- Manual or automated operation
- Workpiece drawings or photographs
Providing complete technical requirements helps ensure that the selected induction forging equipment matches the intended production process.