Induction Brazing Copper Tube
Induction Brazing Copper Tube Without Flux: 1450 °F in 45 Seconds in Argon/Hydrogen
Quick Answer
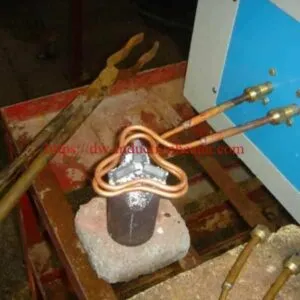
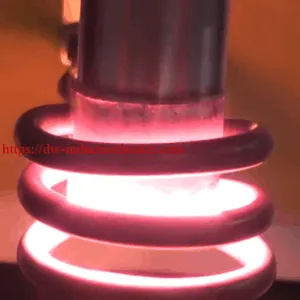
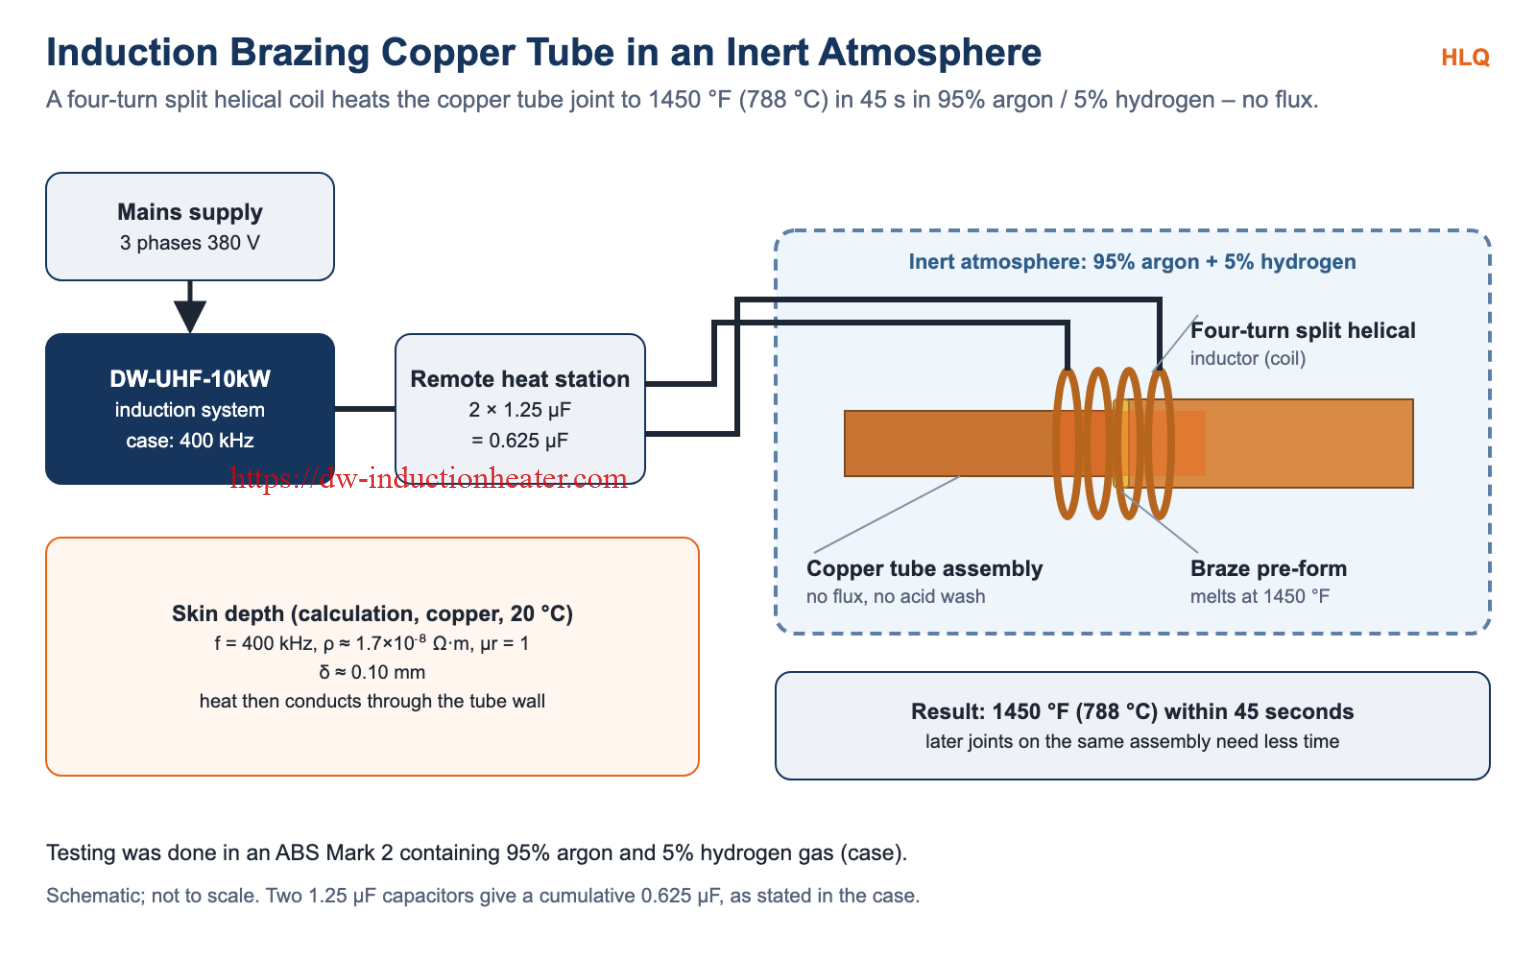
Induction brazing of copper tube heats the tube joint with an induction coil until the braze filler melts and flows into the joint. In this HLQ case, a copper tube assembly with braze pre-forms was heated in an inert atmosphere of 95% argon and 5% hydrogen, so it could be brazed without flux or acid wash clean-up. A DW-UHF-10kW induction power supply at 400 kHz, with a remote heat station of two 1.25 µF capacitors (0.625 µF cumulative) and a four-turn split helical coil, reached 1450 °F (788 °C) in 45 seconds. Because heat conducts through the tube assembly, subsequent joints on the same assembly need less time.
Table of Contents
- What is Induction Brazing of Copper Tube?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages and Limitations
- Why Choose HLQ?
- 10 Core FAQs
What is Induction Brazing of Copper Tube?
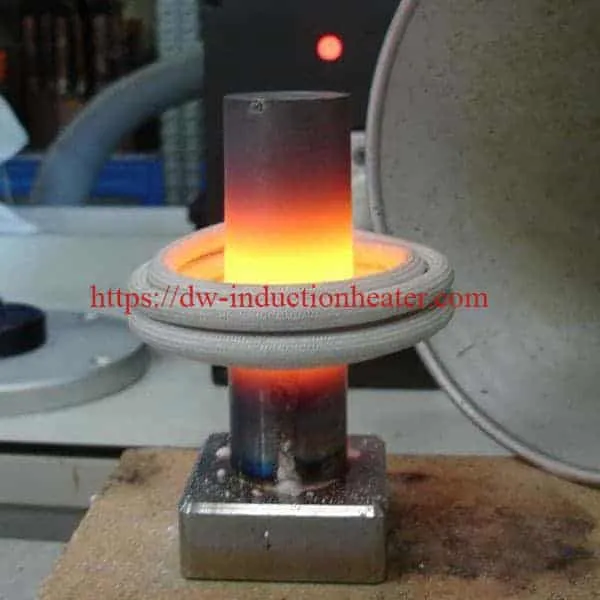
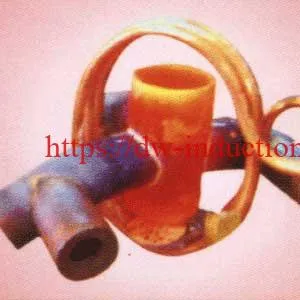
Induction brazing of copper tube uses a coil placed around the tube joint to heat the copper until the braze pre-form melts and is drawn into the joint; the copper itself is not melted. In this HLQ case, brazing was done in a protective gas instead of with flux, so the assembly needed no flux and no acid wash clean-up afterwards. For the general method, see the induction brazing process. Brazing copper tube assemblies is an excellent application for induction heating.
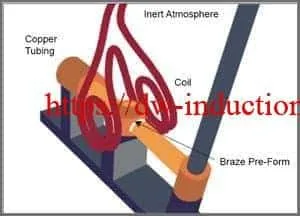
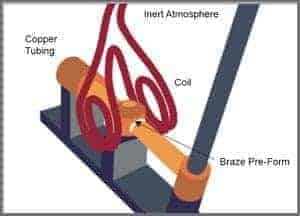
 The case drawing shows the copper tubing, the induction coil around the joint, the braze pre-form and the inert atmosphere supply.
Key Applications
- Copper tube assemblies without flux: inert-atmosphere brazing (this case).
- Copper suction tubes: see brazing copper tubing with induction.
- Refrigeration tubing: see induction brazing copper tube for refrigeration.
- Heat exchangers: see induction brazing copper tube of heat exchanger.
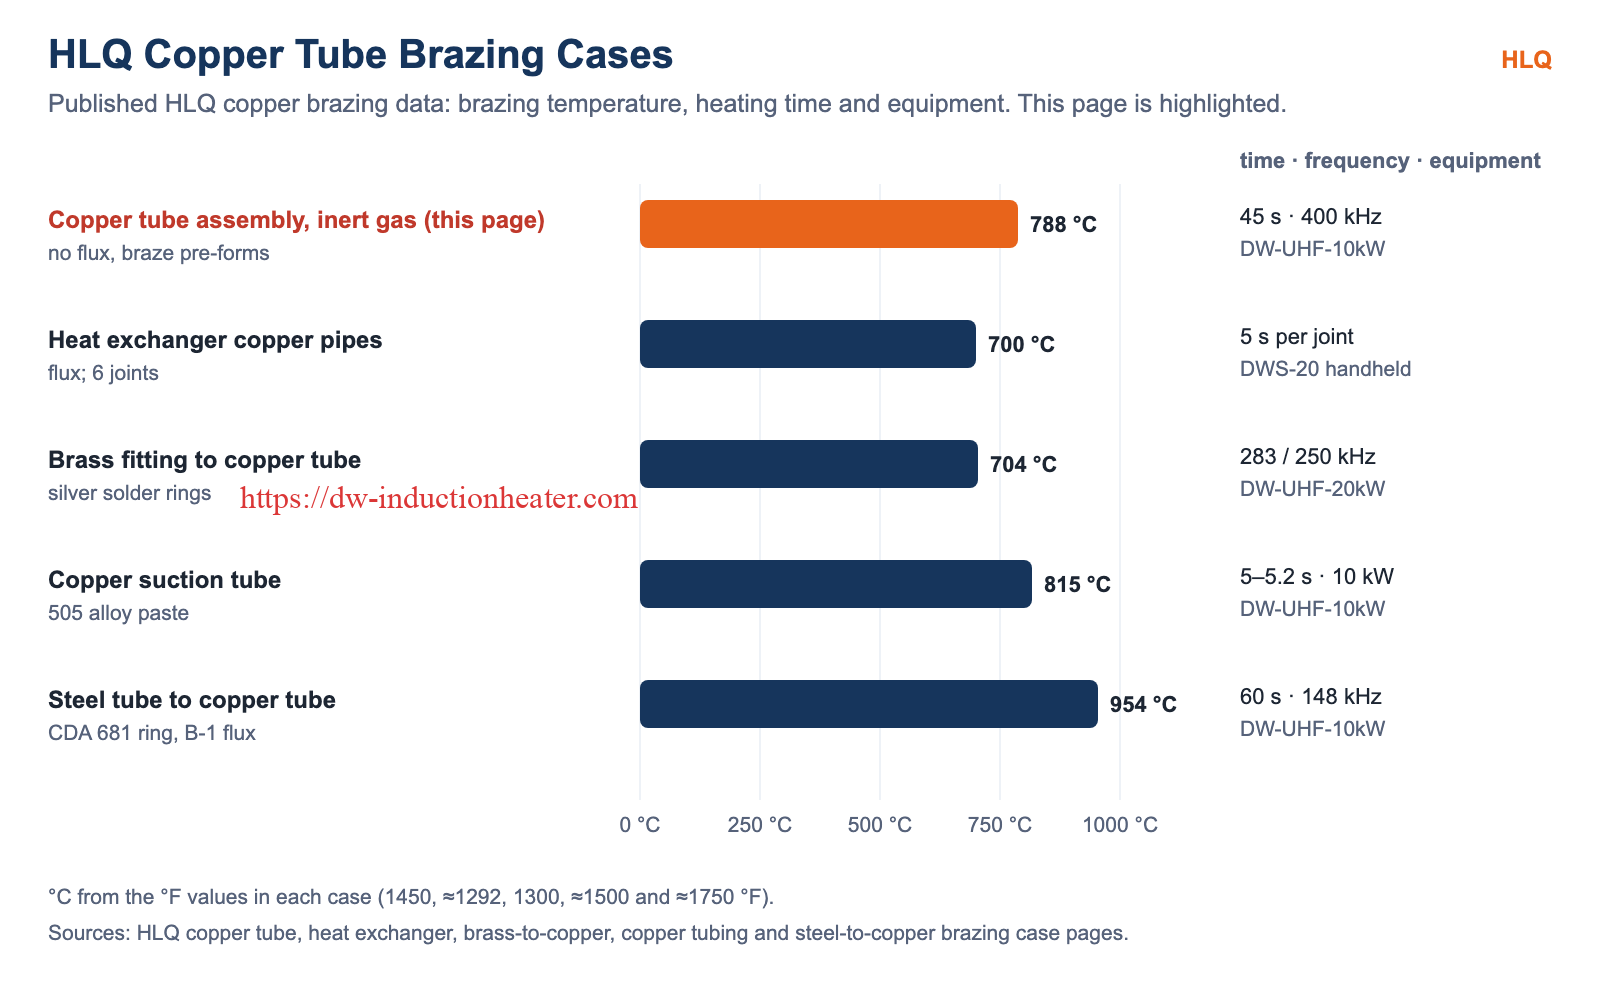
| HLQ copper brazing case | Filler / flux | Temperature | Time | Equipment |
|---|---|---|---|---|
| Copper tube assembly, inert gas (this page) | Braze pre-forms, no flux | 1450 °F (788 °C) | 45 s | DW-UHF-10kW, 400 kHz |
| Copper suction tube | 505 alloy paste | ≈ 1500 °F (815 °C) | 5–5.2 s, 10 kW | DW-UHF-10kW |
| Heat exchanger copper pipes | Brazing flux | ≈ 1292 °F (700 °C) | 5 s per joint | DWS-20 handheld |
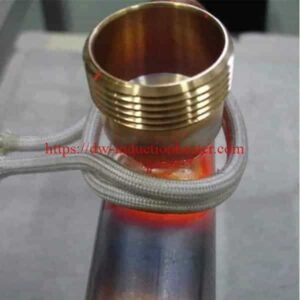
| Brass fitting to copper tube | Silver solder rings | 1300 °F (704 °C) | – | DW-UHF-20kW, 283 / 250 kHz |
| Steel tube to copper tube | CDA 681 ring, B-1 flux | ≈ 1750 °F (954 °C) | 60 s | DW-UHF-10kW, 148 kHz |
Suitable Materials
| Item | This case | Related HLQ data |
|---|---|---|
| Base metal | Copper tube assembly | Copper to brass (brazing copper tube to brass fitting); copper to steel (brazing steel tube to copper tube) |
| Filler | Braze pre-forms | 505 alloy paste; silver solder rings; CDA 681 ring |
| Flux / atmosphere | No flux; 95% argon + 5% hydrogen | Flux used in open-air cases (for example B-1 flux) |
Working Principle
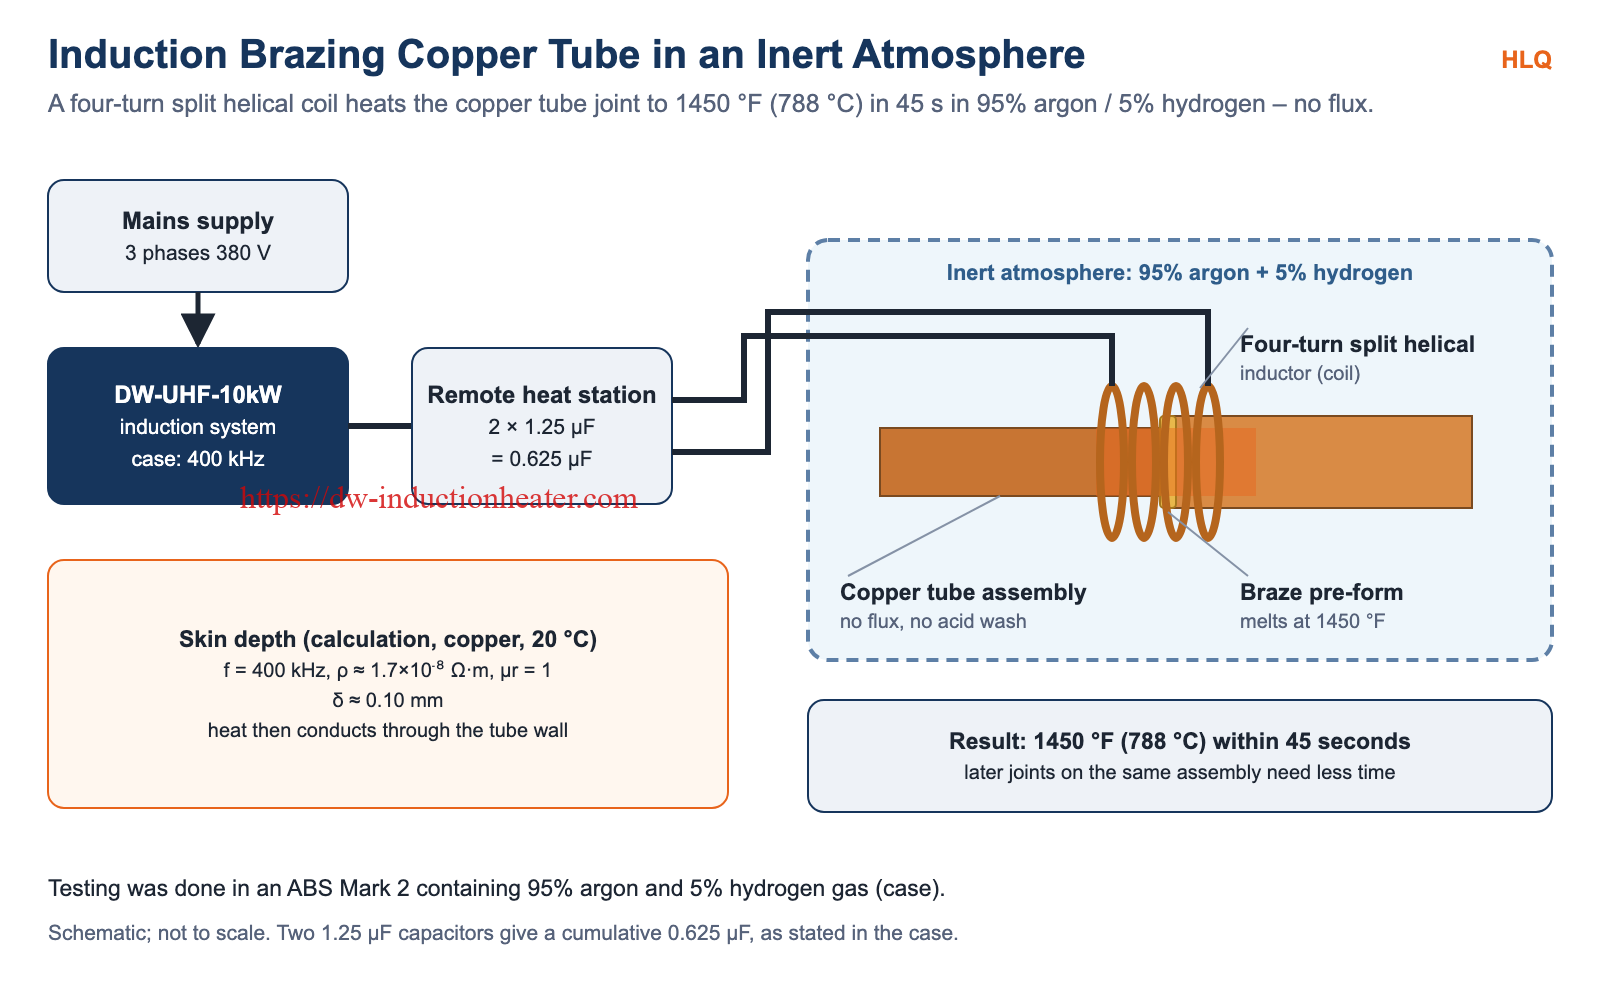
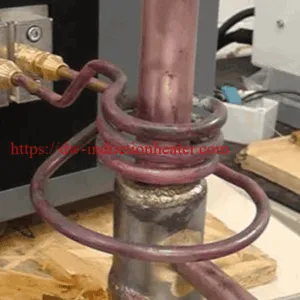
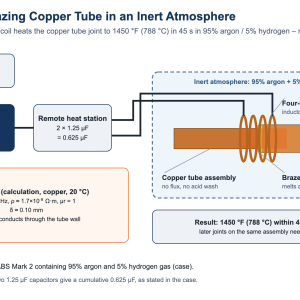
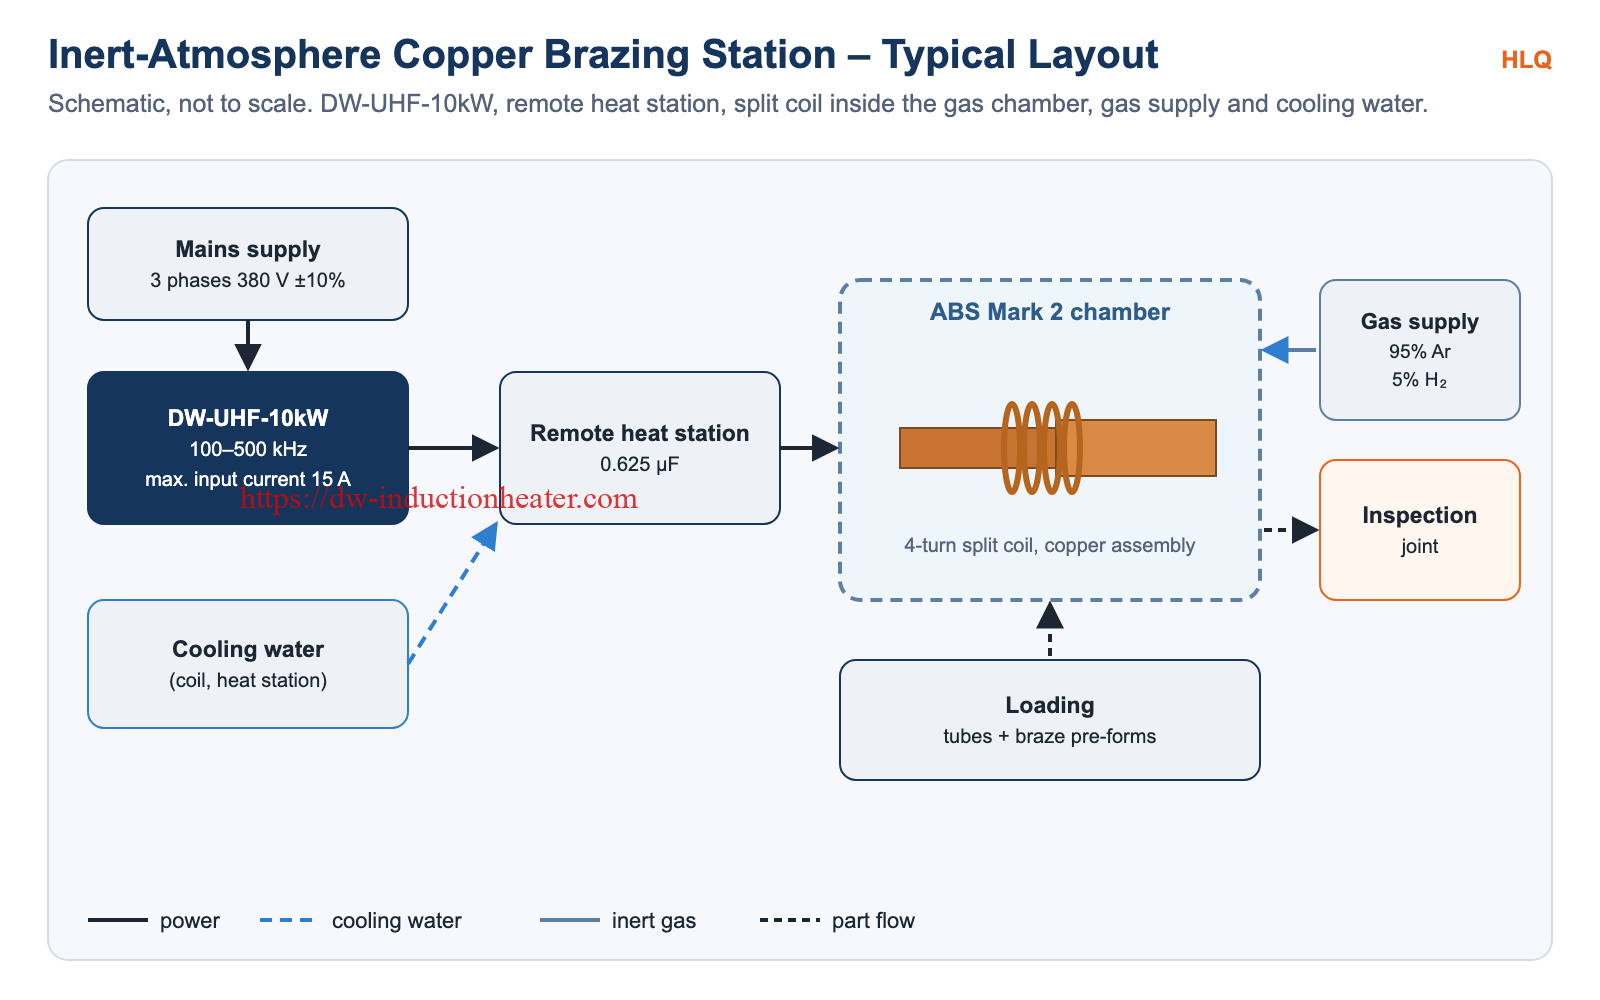
The DW-UHF-10kW drives 400 kHz current through the remote heat station (two 1.25 µF capacitors, 0.625 µF cumulative) and a specially designed four-turn split helical inductor. The split coil fits around the tube assembly. Eddy currents heat the copper tube at the joint, and heat conducts to the braze pre-forms, which melt at 1450 °F. The argon/hydrogen atmosphere protects the joint, so no flux is needed.
Skin depth calculation (δ = 503·√(ρ/f), copper at 20 °C, ρ ≈ 1.7×10⁻⁸ Ω·m, µr = 1): δ ≈ 0.10 mm at 400 kHz. Heat is generated at the tube surface and conducts through the wall, which is also why subsequent joints on the same assembly need less time.
Technical Specifications
| Parameter | Case data |
|---|---|
| Research objective | Heat a copper tube assembly in an inert atmosphere to 1450 °F within 45 seconds for brazing without flux or acid wash clean-up |
| Parts and materials | Copper tube assembly; braze pre-forms; temperature sensing paint |
| Temperature required | 1450 °F (788 °C) |
| Induction heating equipment | DW-UHF-10kW induction heating power supply |
| Heat station | Remote, with two 1.25 µF capacitors (cumulative 0.625 µF) |
| Coil | Specially designed four-turn split helical inductor |
| Operating frequency | 400 kHz |
| Atmosphere | ABS Mark 2 containing 95% argon and 5% hydrogen gas |
| Heating time | 1450 °F reached in 45 seconds |
| Result | Successful brazing at 1450 °F within 45 seconds; subsequent joints on the same assembly require less time |
Recommended Model Selection
DW-UHF series from the HLQ induction heating device model table (all 100% duty cycle):
| Model | Power | Max. input current | Frequency | Supply |
|---|---|---|---|---|
| DW-UHF-6.0kW | 6.0 kW | 28 A | 300–1100 kHz | 1-phase 220 V |
| DW-UHF-10kW (this case) | 10 kW | 15 A | 100–500 kHz | 3-phase 380 V |
| DW-UHF-20kW | 20 kW | 30 A | 50–250 kHz | 3-phase 380 V |
| DW-UHF-30kW | 30 kW | 45 A | 50–200 kHz | 3-phase 380 V |
| DW-UHF-40kW | 40 kW | 60 A | 50–200 kHz | 3-phase 380 V |
| DW-UHF-60kW | 60 kW | 90 A | 50–150 kHz | 3-phase 380 V |
Process Workflow
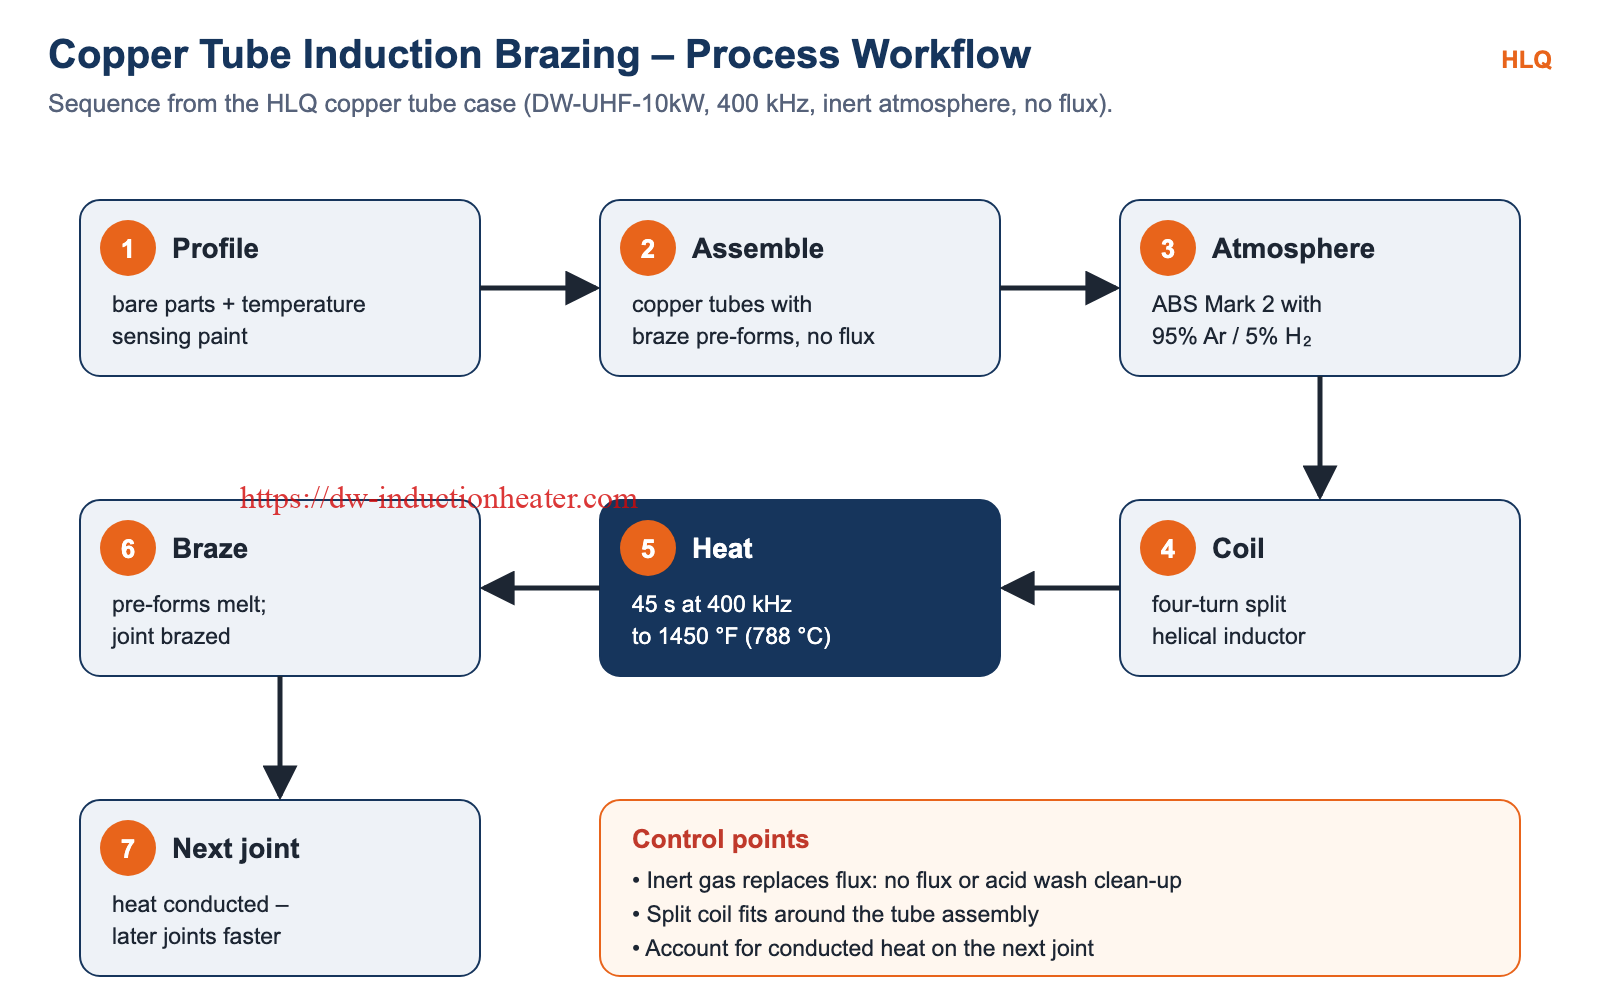
- Profile – heat bare parts with temperature sensing paints to establish time-to-temperature and heating profiles.
- Assemble – fit the copper tubes with braze pre-forms; no flux.
- Atmosphere – place the assembly in the ABS Mark 2 with 95% argon and 5% hydrogen.
- Coil – position the four-turn split helical inductor around the joint.
- Heat – apply 400 kHz power; 1450 °F is reached in 45 seconds.
- Braze – the pre-forms melt and the joint is brazed.
- Next joint – heat conducted through the assembly shortens the time for subsequent joints.
Common Problems and Solutions
| Problem | Possible cause | Solution (HLQ case data) |
|---|---|---|
| Flux residue and acid wash clean-up | Flux used in open air | Braze in an inert atmosphere (95% argon / 5% hydrogen) without flux, as in this case |
| Later joints overheat | Heat conducted from earlier joints | Shorten heating time for subsequent joints on the same assembly |
| Unknown time-to-temperature | New assembly or coil | Profile bare parts with temperature sensing paints first |
| Coil cannot be placed around the assembly | Closed coil on a complex tube assembly | Use a split helical inductor, as in this case |
| Coil overheats | Insufficient cooling water | Check water flow, pressure and water quality |
Engineering Selection Guide
- Fluxless copper assemblies: DW-UHF-10kW at 400 kHz in an argon/hydrogen atmosphere; 45 seconds to 1450 °F.
- Fast copper joints with filler paste in air: DW-UHF-10kW, 5–5.2 seconds in the copper suction tube case.
- Joints brazed in place: DWS handheld systems; 5 seconds per joint in the heat exchanger case.
- Coil: a split coil allows placement around tube assemblies.
- Data to send: tube assembly drawing, filler form, flux or protective atmosphere, cycle time, parts per hour, supply voltage and cooling water.
Advantages and Limitations
| Advantages | Limitations |
|---|---|
| No flux and no acid wash clean-up | Requires an inert-gas chamber (95% argon / 5% hydrogen) |
| 1450 °F reached in 45 seconds | Heating time depends on heat already conducted into the assembly |
| Split coil fits tube assemblies | The coil must be designed for the assembly |
| Subsequent joints need less time | Water cooling is required |
Why Choose HLQ?
- Documented fluxless copper tube brazing in an argon/hydrogen atmosphere.
- Copper brazing cases for suction tubes, heat exchangers, brass fittings and steel-to-copper joints.
- DW-UHF power supplies with remote heat stations and split coils.
- Heating profiles established with temperature sensing paints before production.
10 Core FAQs
1. What was brazed in this case?
A copper tube assembly, using braze pre-forms.
2. Why was an inert atmosphere used?
To braze without flux or acid wash clean-up.
3. What gas mixture was used?
95% argon and 5% hydrogen, in an ABS Mark 2.
4. What temperature was required?
1450 °F (788 °C).
5. How long did heating take?
1450 °F was reached in 45 seconds.
6. Which induction machine was used?
A DW-UHF-10kW induction heating power supply.
7. What frequency and capacitance were used?
400 kHz, with a remote heat station of two 1.25 µF capacitors (0.625 µF cumulative).
8. Which coil was used?
A specially designed four-turn split helical inductor.
9. Why do later joints take less time?
Heat conducts through the tube assembly, so subsequent joints on the same assembly are already partly heated.
10. What information is needed for a quotation?
The tube assembly drawing, filler form, flux or protective atmosphere, cycle time, output, and available power supply and cooling water.