
What Is an Induction Brazing Machine?
An induction brazing machine is industrial heating equipment used to join two or more metal parts by heating them with electromagnetic induction and melting a brazing filler metal between the joint surfaces.
Unlike welding, induction brazing usually does not melt the base metals. Only the filler metal melts, flows into the joint gap, and forms a strong metallurgical bond after cooling.
It is widely used for:
|
Application |
Typical Parts |
|---|---|
|
HVAC & refrigeration |
Copper tube joints, brass fittings, distributors |
|
Automotive |
Aluminum heat exchangers, fuel pipes, sensors |
|
Electrical industry |
Copper busbars, connectors, terminals |
|
Tool manufacturing |
Carbide tips, saw blades, cutting tools |
|
Machinery |
Steel shafts, bushings, rings, gears |
|
Plumbing |
Copper/brass pipe fittings |
How Does Induction Brazing Work?
Induction brazing works by using a high-frequency alternating current to create a magnetic field around the workpiece. This magnetic field induces electrical currents inside the metal part, causing it to heat rapidly.
Basic Working Process
Power Supply
     ↓
High-Frequency Current
     ↓
Induction Coil
     ↓
Alternating Magnetic Field
     ↓
Eddy Currents in Metal Parts
     ↓
Rapid Local Heating
     ↓
Filler Metal Melts and Flows
     ↓
Joint Cools and Solidifies
Main Components of an Induction Brazing Machine
|
Component |
Function |
|---|---|
|
Induction power supply |
Converts input power into medium/high-frequency current |
|
Induction coil |
Generates the magnetic field around the brazing area |
|
Water cooling system |
Cools the coil and power supply |
|
Transformer |
Matches voltage/current to the coil and workpiece |
|
Brazing filler metal |
Melts and fills the joint gap |
|
Flux or protective atmosphere |
Prevents oxidation during heating |
|
Fixture or clamp |
Keeps parts aligned during brazing |
Step-by-Step Induction Brazing Process
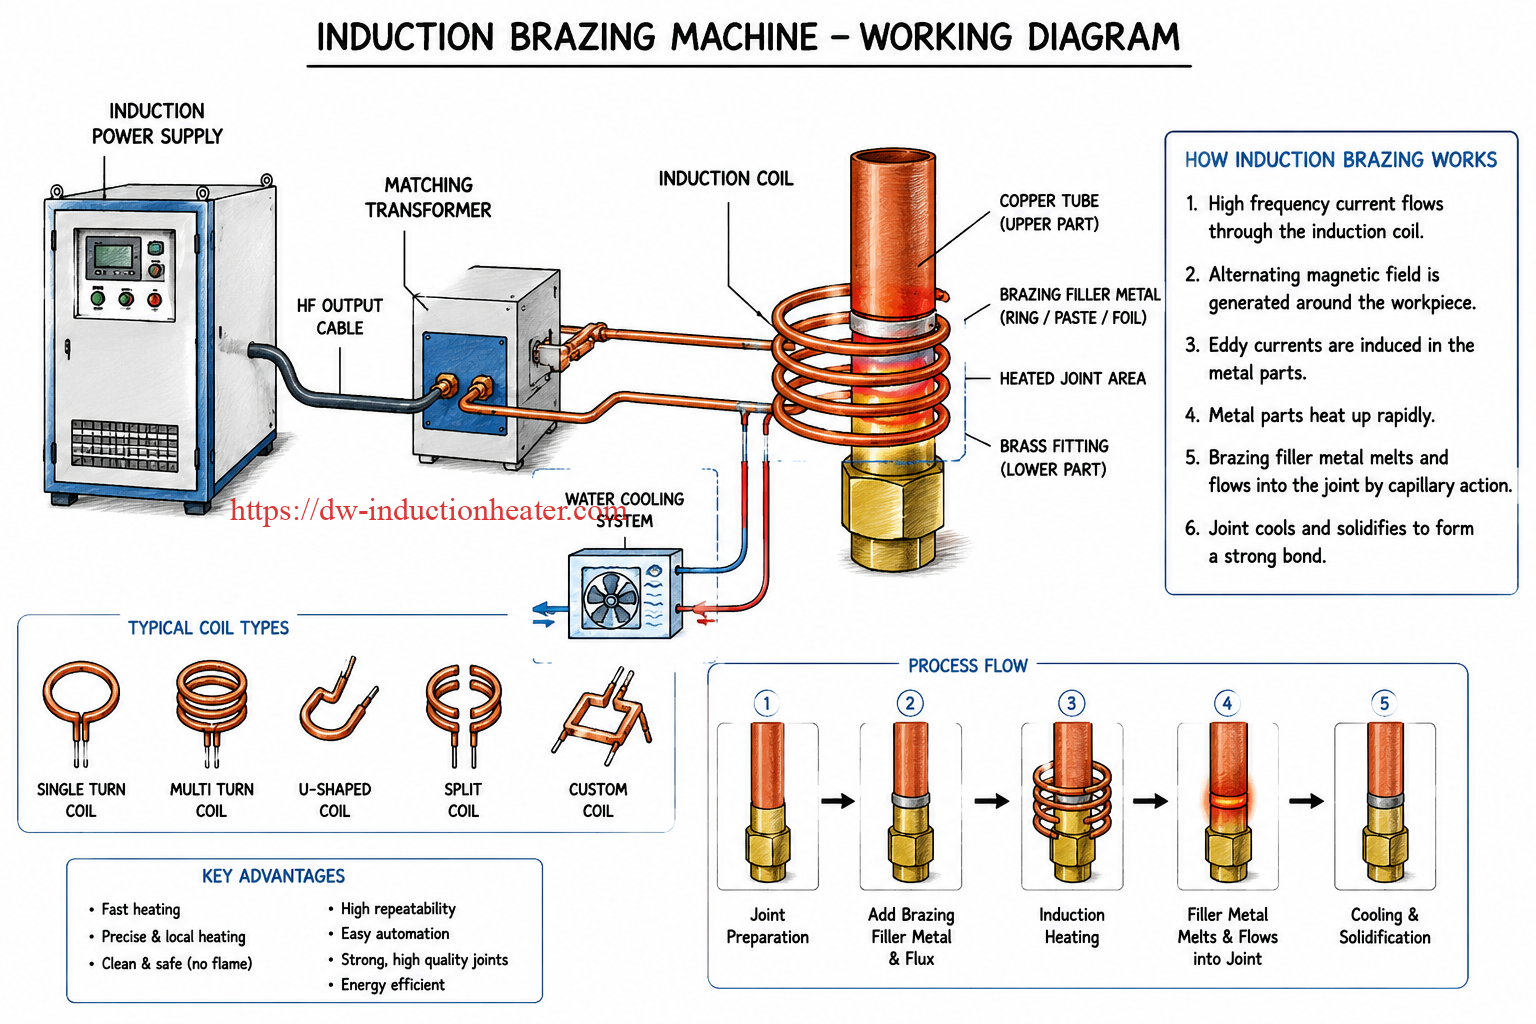
1. Joint Preparation
The parts must be clean and properly fitted. Oil, oxide, rust, and dirt should be removed before brazing.
A proper joint gap is very important. If the gap is too large, the filler may not form a strong joint. If the gap is too small, the filler may not flow properly.
Typical brazing clearance:
|
Material Combination |
Recommended Gap |
|---|---|
|
Copper to copper |
0.02–0.10 mm |
|
Copper to brass |
0.03–0.12 mm |
|
Steel to steel |
0.04–0.15 mm |
|
Carbide to steel |
0.03–0.10 mm |
|
Aluminum to aluminum |
0.05–0.20 mm |
2. Add Brazing Filler Metal
The filler metal can be supplied as:
|
Filler Type |
Example |
|---|---|
|
Brazing ring |
Copper tube joints |
|
Brazing wire |
Manual or automatic feeding |
|
Brazing paste |
Small parts, electrical contacts |
|
Brazing foil |
Flat joints, carbide tools |
|
Brazing rod |
Manual brazing operation |
Common filler metals include:
|
Base Material |
Common Filler Metal |
|---|---|
|
Copper/copper |
Phosphorus copper alloy |
|
Copper/brass |
Silver brazing alloy |
|
Steel/steel |
Silver alloy, copper alloy |
|
Carbide/steel |
Silver-copper-zinc alloy |
|
Aluminum/aluminum |
Aluminum-silicon alloy |
3. Place the Induction Coil Around the Joint
The induction coil is designed according to the part shape. The coil should heat the joint area evenly.
Common coil types:
|
Coil Type |
Suitable Application |
|---|---|
|
Single-turn coil |
Ring joints, small fittings |
|
Multi-turn coil |
Tube joints, shafts, bushings |
|
U-shaped coil |
Side heating, flat parts |
|
Split coil |
Large or hard-to-load parts |
|
Custom-shaped coil |
Special geometry parts |
4. Start Induction Heating
When the machine starts, high-frequency current flows through the induction coil. The magnetic field heats the metal parts directly.
The filler metal reaches its melting temperature and flows into the joint by capillary action.
For example:
|
Material |
Typical Brazing Temperature |
|---|---|
|
Copper brazing |
650–850°C |
|
Brass brazing |
650–800°C |
|
Steel brazing |
750–950°C |
|
Carbide brazing |
700–850°C |
|
Aluminum brazing |
580–620°C |
5. Cooling and Solidification
After the filler metal fully flows into the joint, heating stops. The joint cools naturally or by controlled cooling. Once solidified, the filler metal creates a strong bond between the parts.
Why Induction Brazing Is Efficient
Induction brazing is fast because the heat is generated inside the metal itself, not transferred from an external flame or furnace.
Comparison with Flame Brazing
|
Item |
Induction Brazing |
Flame Brazing |
|---|---|---|
|
Heating method |
Electromagnetic heating |
Gas flame |
|
Heating speed |
Very fast |
Medium |
|
Temperature control |
Accurate |
Depends on operator skill |
|
Repeatability |
High |
Lower |
|
Automation |
Easy |
Difficult |
|
Local heating |
Excellent |
Less precise |
|
Oxidation |
Lower with proper flux/gas |
Higher |
|
Operator skill requirement |
Lower after setup |
Higher |
|
Production consistency |
Very good |
Variable |
Advantages of Induction Brazing Machine
- Fast heating speed
The joint area can often be heated in a few seconds. - Precise local heating
Only the brazing area is heated, reducing distortion. - Clean and safe operation
No open flame is required. - High repeatability
Heating time, power, and temperature can be controlled accurately. - Easy automation
Suitable for robotic brazing, conveyor production, and automatic feeding systems. - Energy saving
Heat is concentrated directly on the workpiece. - Better joint quality
Uniform heating helps the filler metal flow evenly.
Typical Induction Brazing Machine Selection
|
Workpiece Type |
Recommended Power |
Frequency Range |
|---|---|---|
|
Small copper tube joints |
5–15 kW |
100–500 kHz |
|
HVAC copper/brass fittings |
10–30 kW |
50–300 kHz |
|
Carbide tool brazing |
15–40 kW |
30–200 kHz |
|
Steel/copper parts |
25–60 kW |
20–100 kHz |
|
Large steel assemblies |
60–160 kW |
10–50 kHz |
|
Aluminum brazing |
10–80 kW |
20–100 kHz |
Simple Example: Copper Tube Induction Brazing
For a copper tube and brass fitting:
- Clean the tube and fitting.
- Insert the copper tube into the brass fitting.
- Place a silver brazing ring around the joint.
- Apply flux if required.
- Position the induction coil around the joint.
- Heat for several seconds.
- The brazing ring melts and flows into the joint.
- Stop heating and allow the joint to cool.
Result: a clean, strong, leak-tight brazed joint.
In Simple Words
An induction brazing machine uses an induction coil to heat metal parts quickly and locally. When the joint area reaches the brazing temperature, the filler metal melts, flows into the joint gap, and bonds the parts together.
It is a fast, clean, energy-saving, and highly repeatable brazing method, especially suitable for copper tubes, brass fittings, carbide tools, steel parts, aluminum components, and automated production lines.