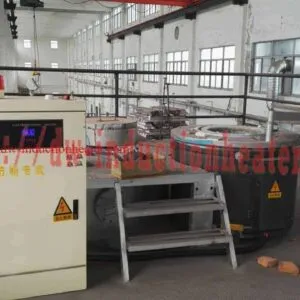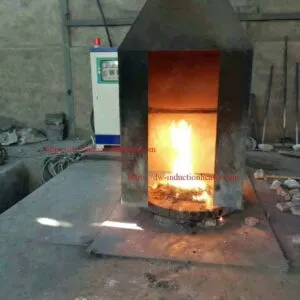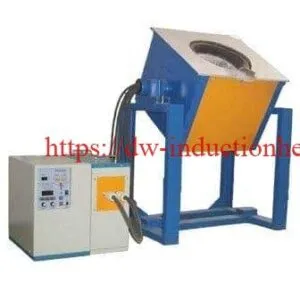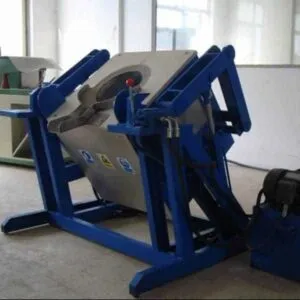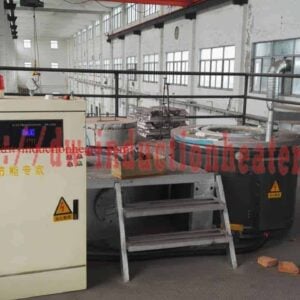
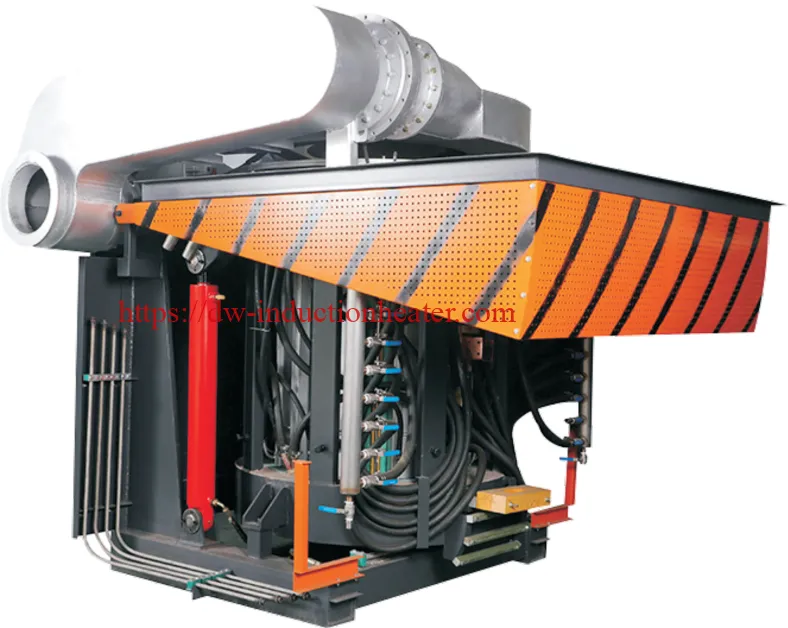
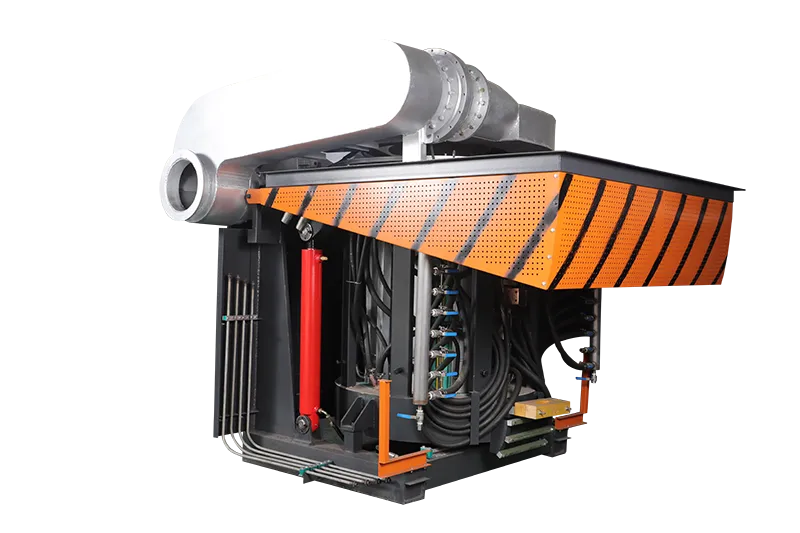
Induction Furnace for Melting Iron and Steel
Induction Furnace for Melting Iron and Steel | Engineering Selection Guide
Table of Contents
- Quick Answer
- What Is This Product?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Coil and Fixture Design
- Control System and Automation
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages
- Limitations
- Why Choose HLQ Induction Equipment?
- FAQ
An induction furnace for melting iron and steel is an electric metal melting system used to melt cast iron, carbon steel, stainless steel, alloy steel, pig iron, return scrap and steel scrap in foundries, casting plants and metal recycling workshops. It uses electromagnetic induction to generate heat directly inside the metal charge, providing fast melting, cleaner operation, stable temperature control and lower oxidation loss compared with many fuel-fired furnaces. For buyers, it solves problems such as slow melting, unstable molten metal temperature, high fuel pollution, difficult pouring control and inconsistent casting quality.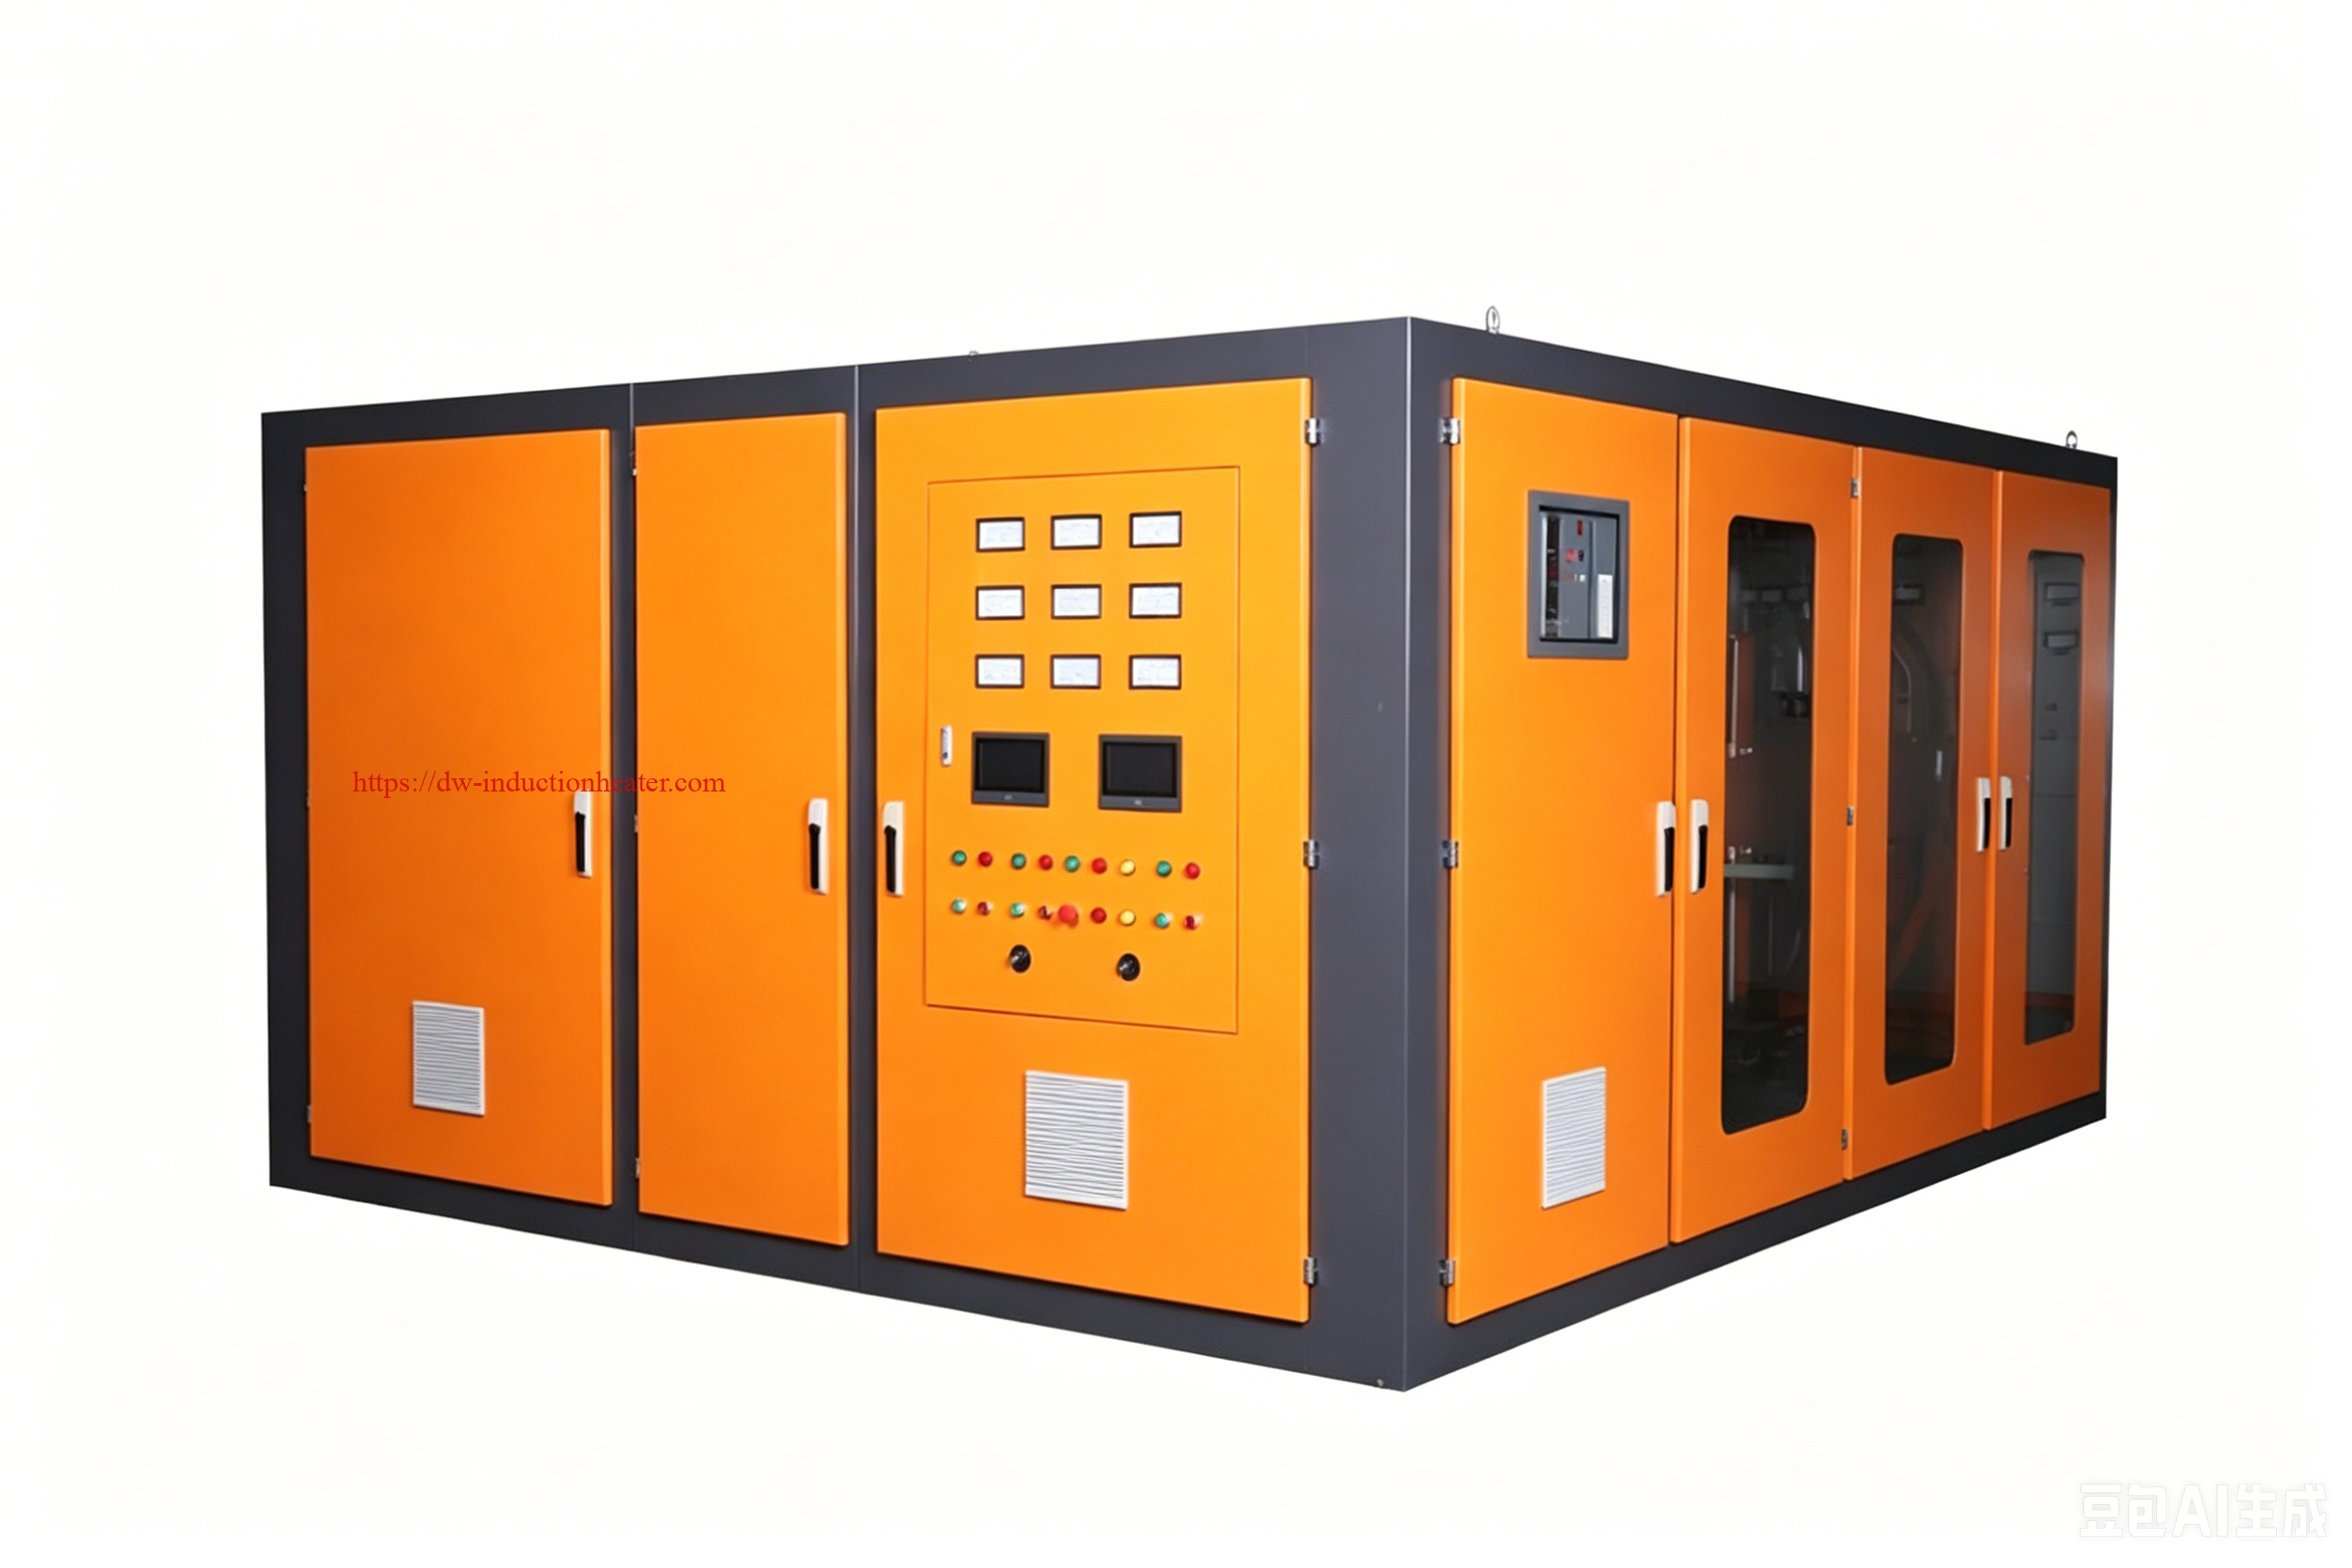
Quick Answer
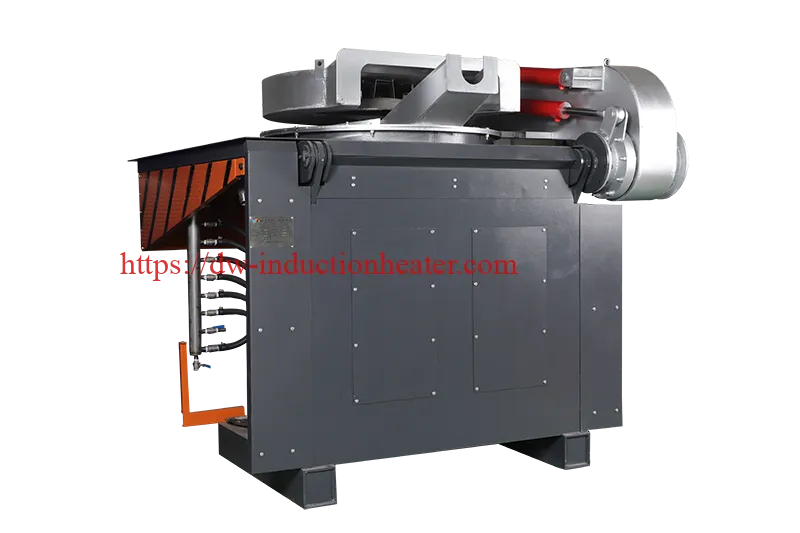
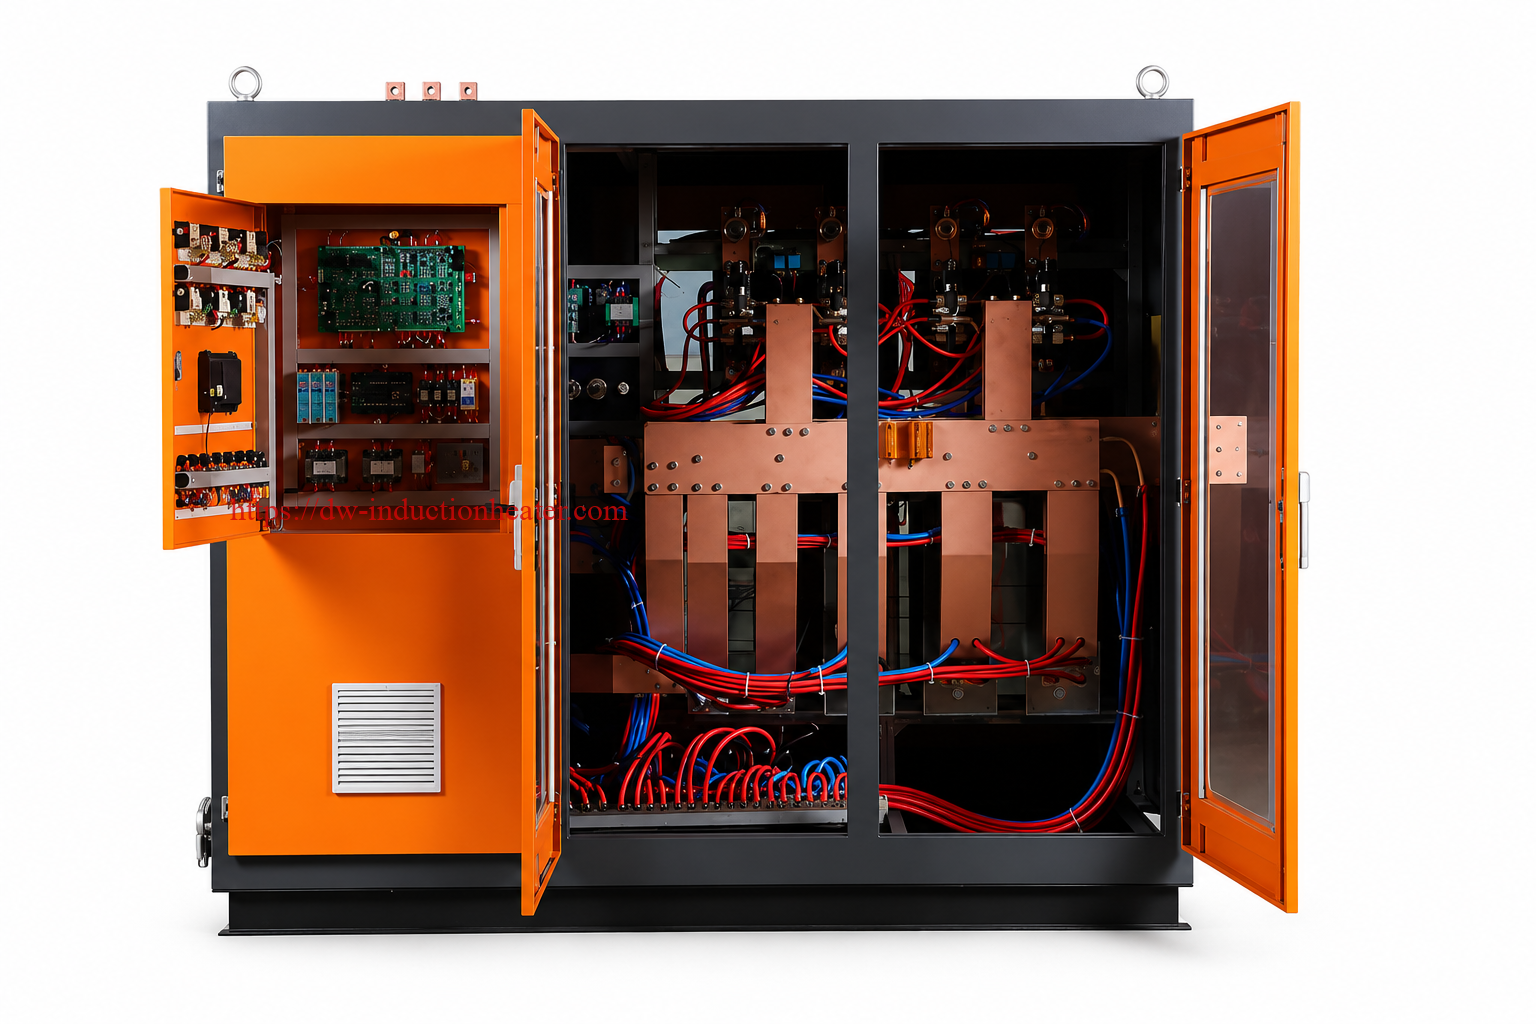
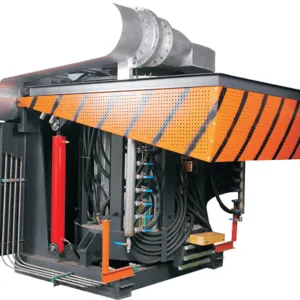
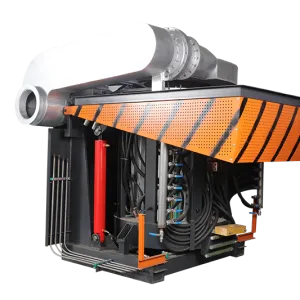
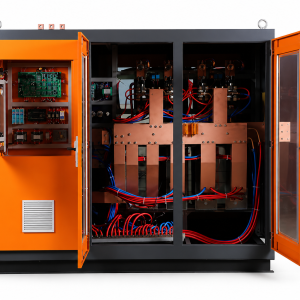
An induction furnace for melting iron and steel is a medium-frequency electric furnace that heats metal by electromagnetic induction. It is best suited for foundries, steel casting plants, iron casting workshops and scrap metal recycling operations that need fast, clean and controllable melting of cast iron, carbon steel, alloy steel and stainless steel. A complete system normally includes an induction power supply, capacitor cabinet, furnace body, water-cooled copper induction coil, refractory lining, hydraulic tilting system, water-cooled cables, cooling system and electrical control cabinet.
What Is This Product?
An induction furnace for melting iron and steel is a coreless induction melting furnace designed for high-temperature ferrous metal melting. Unlike a cupola furnace, gas furnace or oil-fired furnace, an induction furnace does not rely on combustion as the main heat source. Instead, it uses an alternating electromagnetic field to induce electric currents inside the metal charge. These currents produce heat inside the iron or steel itself, allowing the charge to melt quickly and uniformly.
In practical industrial use, this type of furnace is commonly called a medium frequency induction furnace, IF induction furnace, KGPS induction furnace, steel melting induction furnace, cast iron induction furnace or electric steel melting furnace. The exact configuration depends on melting capacity, metal type, power supply, production schedule, pouring method and workshop layout.
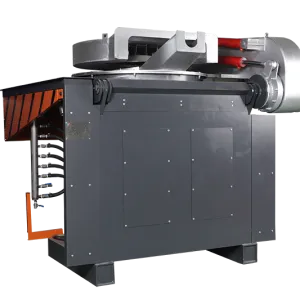
For iron and steel melting, furnace structure is especially important because the melting temperature is high and the furnace lining must withstand severe thermal, mechanical and chemical stress. A steel shell furnace is often selected for medium and large-capacity production because it provides stronger mechanical support, better safety and better suitability for heavy-duty foundry operation. Aluminum shell furnaces are often used for smaller or lighter production requirements.
| Item | Description | Engineering Meaning |
|---|---|---|
| Product Name | Induction Furnace for Melting Iron and Steel | Electric furnace for melting ferrous metals by electromagnetic induction. |
| Furnace Type | Medium frequency / IF / KGPS induction melting furnace | Suitable for foundry melting and steel/iron casting preparation. |
| Main Metals | Cast iron, carbon steel, stainless steel, alloy steel, scrap iron, scrap steel | Covers most ferrous melting applications. |
| Heating Method | Electromagnetic induction and eddy current heating | Heat is generated directly inside the metal charge. |
| Main Users | Foundries, casting plants, recycling workshops, steel processing factories | Designed for industrial molten metal production. |
| Common Furnace Structure | Steel shell or aluminum shell, with hydraulic tilting | Selected according to capacity and production intensity. |
 Key Applications

Iron and steel melting is one of the most demanding applications for an induction furnace. The furnace must reach high temperature, maintain stable power output, protect the induction coil, resist refractory wear and deliver controlled pouring for casting. A properly selected induction furnace can support many ferrous metal production processes.
| Application | Typical Material | Recommended Furnace Configuration | Buyer Benefit |
|---|---|---|---|
| Cast Iron Melting | Gray iron, ductile iron, pig iron, return scrap | Medium frequency induction furnace with suitable iron lining | Stable molten iron supply for casting production. |
| Carbon Steel Melting | Steel scrap, carbon steel, low-alloy steel | Steel shell induction furnace with hydraulic tilting | Fast melting and good temperature control for steel casting. |
| Alloy Steel Melting | Cr-Mo steel, Mn steel, tool steel, wear-resistant alloy | Temperature-controlled induction furnace | Improves alloy composition uniformity and repeatability. |
| Stainless Steel Melting | 304, 316, stainless scrap, stainless alloy | Medium frequency induction furnace with controlled slag practice | Supports stainless casting and alloy recycling. |
| Scrap Iron and Steel Recycling | Clean steel scrap, iron scrap, rejected castings | Hydraulic tilting induction melting furnace | Converts scrap into reusable molten metal. |
| Foundry Casting | Molten iron or steel for molds | Steel shell furnace with ladle pouring layout | Improves casting quality and production flexibility. |
| Small Batch Alloy Development | Experimental steel or iron alloy | Small or medium induction crucible furnace | Flexible melting for trials and specialty production. |
Suitable Materials
An induction furnace can melt electrically conductive metals. For iron and steel melting, the furnace must be designed for high temperature, high power density and correct refractory lining. Carbon steel and cast iron are very common induction melting materials. Stainless steel and alloy steels can also be melted, but require more careful temperature and composition control.
| Material | Melting Suitability | Typical Melting Temperature Range | Engineering Notes |
|---|---|---|---|
| Gray Cast Iron | Excellent | Approximately 1150–1400°C depending on composition | Very common foundry application; charge mix and carbon equivalent should be controlled. |
| Ductile Iron | Excellent | Approximately 1300–1500°C | Requires good base iron quality before nodularizing treatment. |
| Carbon Steel | Excellent | Approximately 1450–1600°C | Requires high-temperature lining and sufficient power capacity. |
| Low-Alloy Steel | Excellent | Approximately 1450–1650°C | Alloy loss and final chemistry should be monitored. |
| Stainless Steel | Good | Approximately 1400–1550°C | Oxidation and chromium loss should be controlled with correct slag practice. |
| High-Manganese Steel | Good | Approximately 1400–1500°C | Suitable for wear-resistant casting, but lining compatibility matters. |
| Tool Steel | Good | Approximately 1450–1600°C | Requires accurate temperature control and alloy management. |
| Scrap Iron and Steel | Good if clean and dry | Depends on composition | Moisture, sealed cavities, oil and contamination must be removed before charging. |
Working Principle
The working principle of an induction furnace for melting iron and steel is electromagnetic induction. The induction power supply converts factory AC electricity into medium-frequency current. This current flows through a water-cooled copper induction coil surrounding the crucible or refractory lining. The coil generates an alternating magnetic field, which penetrates the iron or steel charge inside the furnace.
Because iron and steel are conductive, the changing magnetic field induces circulating currents inside the metal charge. These circulating currents are called eddy currents. When eddy currents flow through the electrical resistance of the metal, heat is generated. As heating continues, the charge softens, collapses, melts and forms a molten bath.
After melting begins, electromagnetic force creates a natural stirring action in the molten bath. This stirring helps distribute heat and alloying elements more evenly. For foundry production, this is important because uniform temperature and uniform chemistry help improve casting consistency.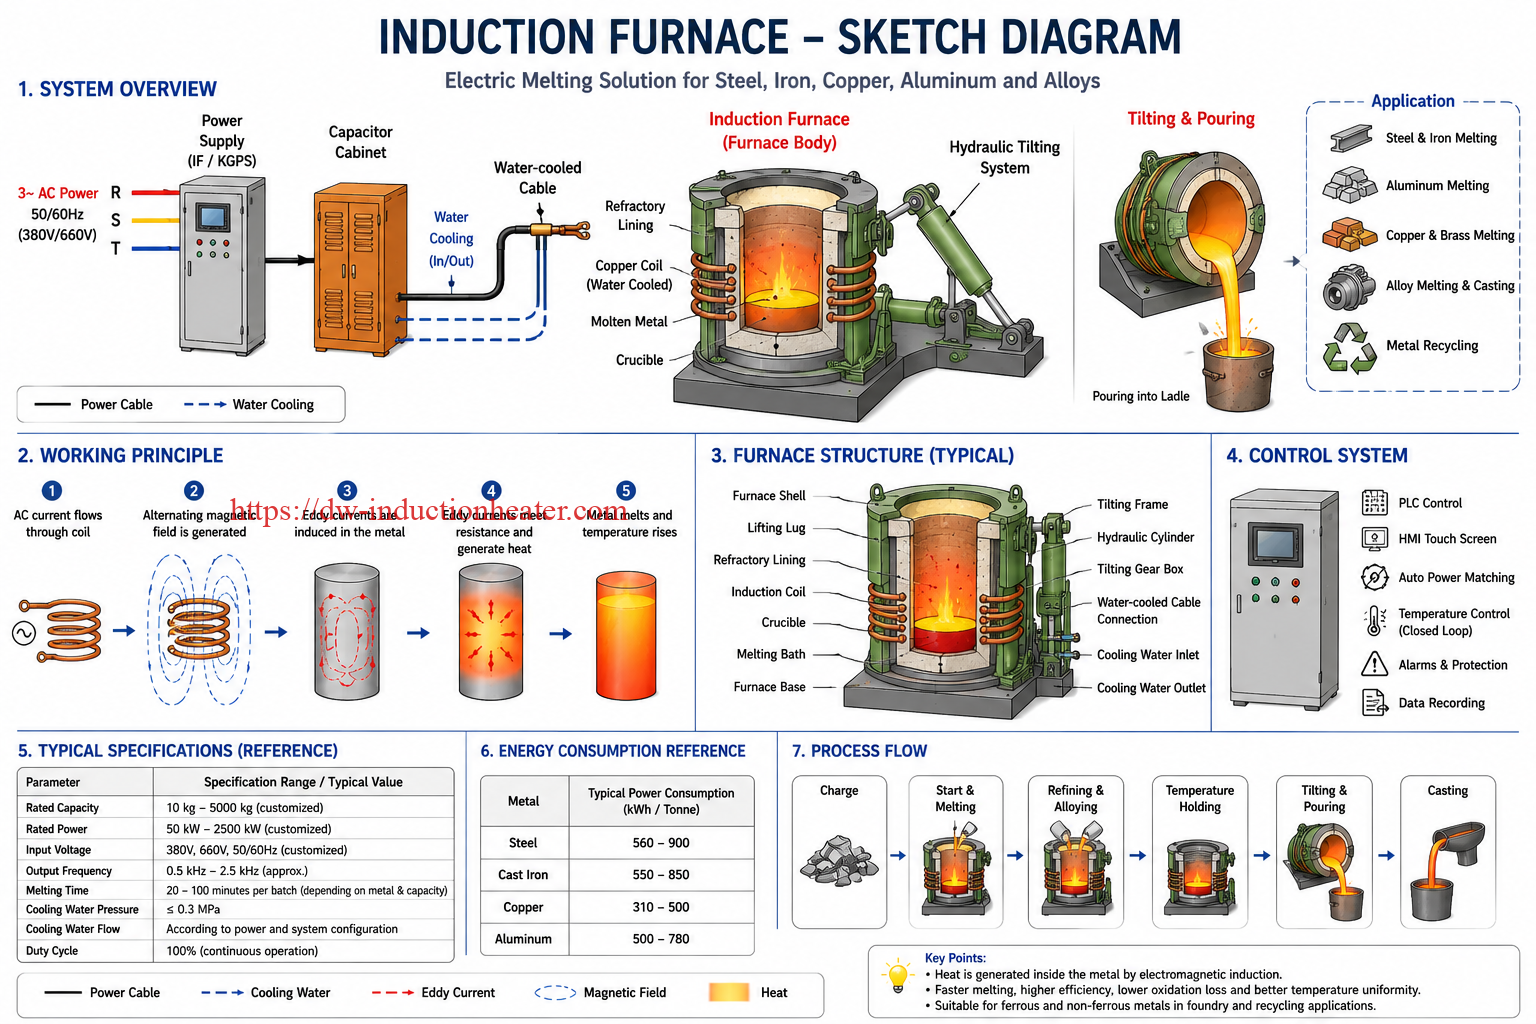
| Step | Process | What Happens in the Furnace |
|---|---|---|
| 1 | Power Input | Three-phase factory power enters the induction furnace power supply. |
| 2 | Frequency Conversion | The power supply converts input power into medium-frequency furnace current. |
| 3 | Coil Excitation | Current flows through the water-cooled copper induction coil. |
| 4 | Magnetic Field Formation | The coil generates an alternating magnetic field around the crucible. |
| 5 | Eddy Current Heating | Eddy currents are induced inside the iron or steel charge. |
| 6 | Joule Heat Generation | Electrical resistance converts induced current into heat. |
| 7 | Melting | The solid charge melts into a molten iron or steel bath. |
| 8 | Electromagnetic Stirring | The molten metal circulates, helping temperature and composition uniformity. |
| 9 | Tilting and Pouring | The hydraulic system tilts the furnace to pour molten metal into ladles or molds. |
Simple Working Principle Chart
| Input | Power Conversion | Induction Field | Metal Reaction | Final Output |
|---|---|---|---|---|
| 3-phase AC power | MF / KGPS power supply | Water-cooled copper coil creates magnetic field | Eddy currents heat iron or steel charge | Molten iron or steel ready for casting |
Technical Specifications
| Parameter | Specification | Notes |
|---|---|---|
| Product Type | Medium frequency induction furnace for iron and steel melting | Suitable for foundry and steel casting applications. |
| Furnace Capacity | 10kg to 5000kg per batch, customizable | Select according to batch weight and daily production. |
| Power Range | 50kW to 2500kW or higher customized systems | Higher power shortens melting time but requires stronger electrical infrastructure. |
| Output Frequency | Usually around 0.5kHz to 2.5kHz for many medium-frequency melting furnaces | Lower frequency is generally used for larger furnace capacities. |
| Input Voltage | 380V, 660V, 750V, 1000V or customized | Depends on power level and local factory electrical supply. |
| Furnace Body | Steel shell or aluminum shell | Steel shell is recommended for larger iron and steel melting systems. |
| Tilting Method | Hydraulic tilting, mechanical tilting or fixed furnace design | Hydraulic tilting improves pouring control and operator safety. |
| Cooling Method | Water cooling for coil, power supply, capacitor cabinet and cables | Cooling water flow and pressure must be monitored continuously. |
| Refractory Lining | Acidic, neutral or basic lining depending on metal and process | Lining selection affects safety, life and metal quality. |
| Control System | Digital control, PLC, HMI, temperature feedback and protection alarms optional | Useful for stable production and easier operation. |
| Safety Protection | Over-current, over-voltage, water pressure, phase loss, leak furnace alarm optional | Large iron and steel furnaces should use full protection configuration. |
| Typical Application | Iron melting, steel melting, foundry casting, scrap recycling and alloy production | Designed for high-temperature ferrous metal production. |
Recommended Model Selection
| Application | Material | Recommended Power | Frequency |
|---|---|---|---|
| Small cast iron melting | Gray iron, pig iron, return scrap | 100kW–250kW | Medium frequency, typically 0.5–2.5kHz depending on furnace size |
| Small steel casting workshop | Carbon steel, low-alloy steel | 160kW–350kW | Medium frequency / KGPS |
| 500kg cast iron melting | Cast iron, pig iron, foundry returns | 250kW–500kW | Medium frequency |
| 1-ton iron or steel melting | Cast iron, carbon steel, alloy steel | 500kW–800kW | Medium frequency / KGPS |
| 2-ton foundry melting | Iron, carbon steel, alloy steel | 1000kW–1500kW | Medium frequency |
| 3-ton heavy-duty steel melting | Steel scrap, alloy steel, stainless steel | 1500kW–2000kW | Medium frequency, lower range for larger bath |
| 5-ton industrial foundry melting | Cast iron, steel, heavy scrap | 2000kW–2500kW+ | Medium frequency / high-power furnace system |
| Stainless steel melting | Stainless scrap and stainless alloy | Depends on batch size, typically 500kW–2500kW | Medium frequency with accurate temperature control |
Capacity Selection Reference
| Furnace Capacity | Typical Use | Recommended Furnace Body | Engineering Comment |
|---|---|---|---|
| 10–100kg | Laboratory, trial melting, small castings | Small crucible furnace | Good for samples and specialty alloys. |
| 150–350kg | Small foundry, repair casting, small batch production | Aluminum shell or compact steel shell | Lower investment and flexible operation. |
| 500–1000kg | Medium foundry production | Hydraulic tilting steel shell furnace | Common choice for continuous casting workshops. |
| 1500–3000kg | Large foundry and steel casting | Steel shell furnace | Requires strong transformer, cooling and safety system. |
| 3000–5000kg | Heavy industrial melting | Heavy-duty steel shell furnace | Designed for high output and long production shifts. |
Process Workflow
A safe and efficient iron or steel melting process requires more than turning on the power. Operators must prepare the charge correctly, inspect the lining, confirm cooling water, follow a proper melting curve and control pouring temperature. The following workflow can be used as a practical engineering reference.
| Step | Operation | Key Control Point |
|---|---|---|
| 1 | System Inspection | Check power cabinet, cooling water, hydraulic system, grounding and alarms. |
| 2 | Lining Inspection | Confirm refractory lining thickness, cracks, erosion and sintering condition. |
| 3 | Charge Preparation | Use dry, clean and properly sized iron or steel charge. Avoid sealed or wet scrap. |
| 4 | Initial Charging | Place suitable bottom charge carefully to protect the furnace lining. |
| 5 | Power Start | Start at appropriate power level and increase as charge condition becomes stable. |
| 6 | Main Melting | Monitor voltage, current, water pressure, furnace noise and melting progress. |
| 7 | Additional Charging | Add remaining scrap gradually after molten pool formation; avoid bridging. |
| 8 | Alloying and Chemistry Adjustment | Add carbon, silicon, manganese, chromium or other alloying materials as required. |
| 9 | Slag Removal | Remove slag to improve molten metal cleanliness. |
| 10 | Temperature Measurement | Confirm pouring temperature using suitable measurement equipment. |
| 11 | Tilting and Pouring | Use hydraulic tilting to pour molten metal into ladle or mold safely. |
| 12 | Post-Melting Check | Inspect lining, record energy consumption, melting time and production data. |
 Iron and Steel Melting Flow Chart

| Charge Preparation | Melting | Refining / Adjustment | Pouring | Production Record |
|---|---|---|---|---|
| Dry scrap, pig iron, returns, alloy materials | Power heating, molten pool formation, electromagnetic stirring | Slag removal, carbon/alloy adjustment, temperature control | Hydraulic tilting, ladle transfer, mold filling | Energy, time, lining condition, casting quality |
Coil and Fixture Design
In an induction furnace, the “coil and fixture” design is different from a small induction brazing or hardening machine. The induction coil is built around the crucible and furnace lining. It must deliver high current, create a stable magnetic field, support efficient melting and remain safely cooled during continuous operation.
For iron and steel melting, coil insulation, water cooling, mechanical support and refractory protection are critical. A coil failure in a melting furnace can cause serious downtime and safety risk, so the furnace body must be designed as a complete thermal, electrical and mechanical system.
| Design Item | Function | Engineering Recommendation |
|---|---|---|
| Water-Cooled Copper Coil | Generates the magnetic field for melting. | Use high-conductivity copper tube with reliable water passage. |
| Coil Insulation | Prevents electrical short circuit and protects coil. | Use high-temperature and high-voltage insulation materials. |
| Refractory Lining | Contains molten metal and protects the coil. | Select acidic, neutral or basic lining according to metal and slag chemistry. |
| Furnace Shell | Supports coil, lining and tilting structure. | Steel shell is recommended for large iron and steel furnaces. |
| Hydraulic Tilting Frame | Tilts furnace for pouring molten metal. | Use strong shaft, cylinder, limit switch and safety lock design. |
| Magnetic Yoke | Improves magnetic field distribution and reduces stray field. | Recommended for many steel shell furnace designs. |
| Water-Cooled Cable | Transfers high current from power cabinet to furnace body. | Size cable according to current and distance; inspect connection regularly. |
Control System and Automation
Modern induction furnaces for melting iron and steel can be equipped with digital control, automatic load tracking, PLC, HMI, temperature feedback and alarm protection. These systems help operators maintain stable melting performance and reduce manual adjustment.
| Control Function | Purpose | Benefit for Iron and Steel Melting |
|---|---|---|
| Automatic Load Matching | Adjusts output according to charge and melting condition. | Improves power utilization during different melting stages. |
| Constant Power Control | Maintains stable output power. | Shortens melting time and improves production repeatability. |
| PLC Control | Coordinates power, alarms, cooling and auxiliary systems. | Supports intelligent foundry operation. |
| HMI Interface | Displays parameters and operation status. | Makes operation easier and reduces training difficulty. |
| Temperature Feedback | Measures molten metal or process temperature. | Helps control pouring temperature and reduce overheating. |
| Water Pressure Monitoring | Protects coil, cables and power components. | Prevents overheating caused by cooling failure. |
| Leak Furnace Alarm | Detects lining failure risk. | Strongly recommended for large iron and steel furnaces. |
| Energy Data Recording | Records melting time and kWh consumption. | Helps optimize operating cost and melting pattern. |
Common Problems and Solutions
Most induction furnace problems are related to incorrect power selection, poor charge preparation, weak cooling, unsuitable lining, unstable electrical supply or poor operating practice. The table below summarizes common issues in iron and steel melting.
| Problem | Possible Cause | Engineering Solution |
|---|---|---|
| Melting time is too long | Power is too low, charge is too large, voltage is unstable or lining insulation is poor. | Select higher power, improve charge size, inspect lining and confirm transformer capacity. |
| Power consumption is too high | Long holding time, wet charge, excessive superheating or poor lining condition. | Reduce holding time, dry charge, optimize temperature target and maintain lining. |
| Furnace alarms frequently | Cooling water problem, over-current, over-voltage, load mismatch or capacitor fault. | Check water pressure, water flow, capacitor cabinet, input voltage and furnace load. |
| Molten bath temperature is uneven | Poor charge distribution, insufficient melting time or weak stirring. | Improve charging sequence and allow complete melting before temperature measurement. |
| Furnace lining wears quickly | Wrong refractory material, poor sintering, thermal shock or mechanical damage during charging. | Use correct lining material, follow sintering procedure and avoid heavy impact loading. |
| Molten metal splashes during charging | Wet scrap, sealed cavities, oil contamination or improper charging. | Use dry clean scrap, remove sealed containers and charge carefully. |
| Oxidation or alloy loss is high | Overheating, long holding time, poor slag practice or incorrect alloy addition sequence. | Control temperature, shorten holding time and optimize alloy/slag practice. |
| Pouring is unstable | Hydraulic system issue, poor ladle position or worn tilting structure. | Inspect hydraulic cylinder, hinge, limit switch and pouring layout. |
Engineering Selection Guide
Selecting an induction furnace for melting iron and steel should not be based only on furnace capacity. Two furnaces with the same capacity may have very different melting speeds, energy consumption and safety performance depending on power rating, furnace shell design, lining material, transformer capacity and cooling system.
| Selection Factor | What to Confirm | Engineering Recommendation |
|---|---|---|
| Metal Type | Cast iron, carbon steel, stainless steel or alloy steel. | Select lining chemistry and power density according to metal type. |
| Batch Capacity | Required kilograms or tons per melt. | Select furnace capacity with practical loading and pouring margin. |
| Target Melting Time | Required minutes per batch. | Higher power shortens melting time but requires stronger electrical infrastructure. |
| Daily Production | Tons per shift or tons per day. | Determine whether one furnace is enough or multiple furnaces are needed. |
| Input Power Supply | Factory voltage, transformer capacity and cable size. | Confirm electrical room capacity before ordering high-power furnace. |
| Furnace Body | Steel shell or aluminum shell. | Use steel shell for larger iron/steel melting or heavy-duty foundry operation. |
| Tilting System | Manual, mechanical or hydraulic tilting. | Hydraulic tilting is recommended for medium and large furnaces. |
| Cooling System | Water flow, pressure, temperature and water quality. | Use closed-loop cooling tower or industrial chiller according to local conditions. |
| Safety Protection | Leak furnace alarm, water pressure protection, emergency stop and over-current protection. | Do not reduce safety configuration for steel and iron melting projects. |
| Workshop Layout | Charging area, crane, ladle path, mold area and cooling equipment position. | Plan furnace layout before finalizing equipment dimensions. |
Practical Selection Logic
| Buyer Requirement | Recommended Choice | Reason |
|---|---|---|
| Small batch cast iron melting | 100–350kg induction furnace | Flexible operation and lower investment. |
| Medium foundry production | 500kg–1 ton hydraulic tilting furnace | Balanced capacity, power and pouring convenience. |
| Large steel casting | 2–5 ton steel shell induction furnace | Strong structure and suitable for high-temperature heavy-duty melting. |
| Scrap recycling with frequent batch changes | Medium frequency tilting furnace | Fast melting and flexible charge handling. |
| High-alloy steel production | Temperature-controlled furnace with good slag practice | Better control of alloy composition and molten metal quality. |
Advantages
| Advantage | Engineering Meaning | Buyer Value |
|---|---|---|
| Fast Melting | Heat is generated directly inside the iron or steel charge. | Shorter melting cycle and higher production output. |
| Clean Electric Heating | No combustion flame inside the furnace. | Cleaner workshop environment than many fuel-fired systems. |
| Good Temperature Control | Electrical power can be adjusted quickly. | More stable pouring temperature and casting quality. |
| Electromagnetic Stirring | Molten metal circulates naturally under magnetic force. | Improves bath temperature uniformity and alloy mixing. |
| Lower Oxidation Loss | Reduced flame contact and controlled melting atmosphere. | Improves metal yield and reduces material waste. |
| Flexible Raw Material Use | Can melt pig iron, return scrap, steel scrap and alloy additions. | Useful for foundries and recycling plants. |
| Automation Compatibility | Can be integrated with PLC, HMI and temperature feedback. | Supports intelligent production and operation traceability. |
| Controlled Pouring | Hydraulic tilting enables stable molten metal discharge. | Improves safety and casting workflow. |
 Limitations
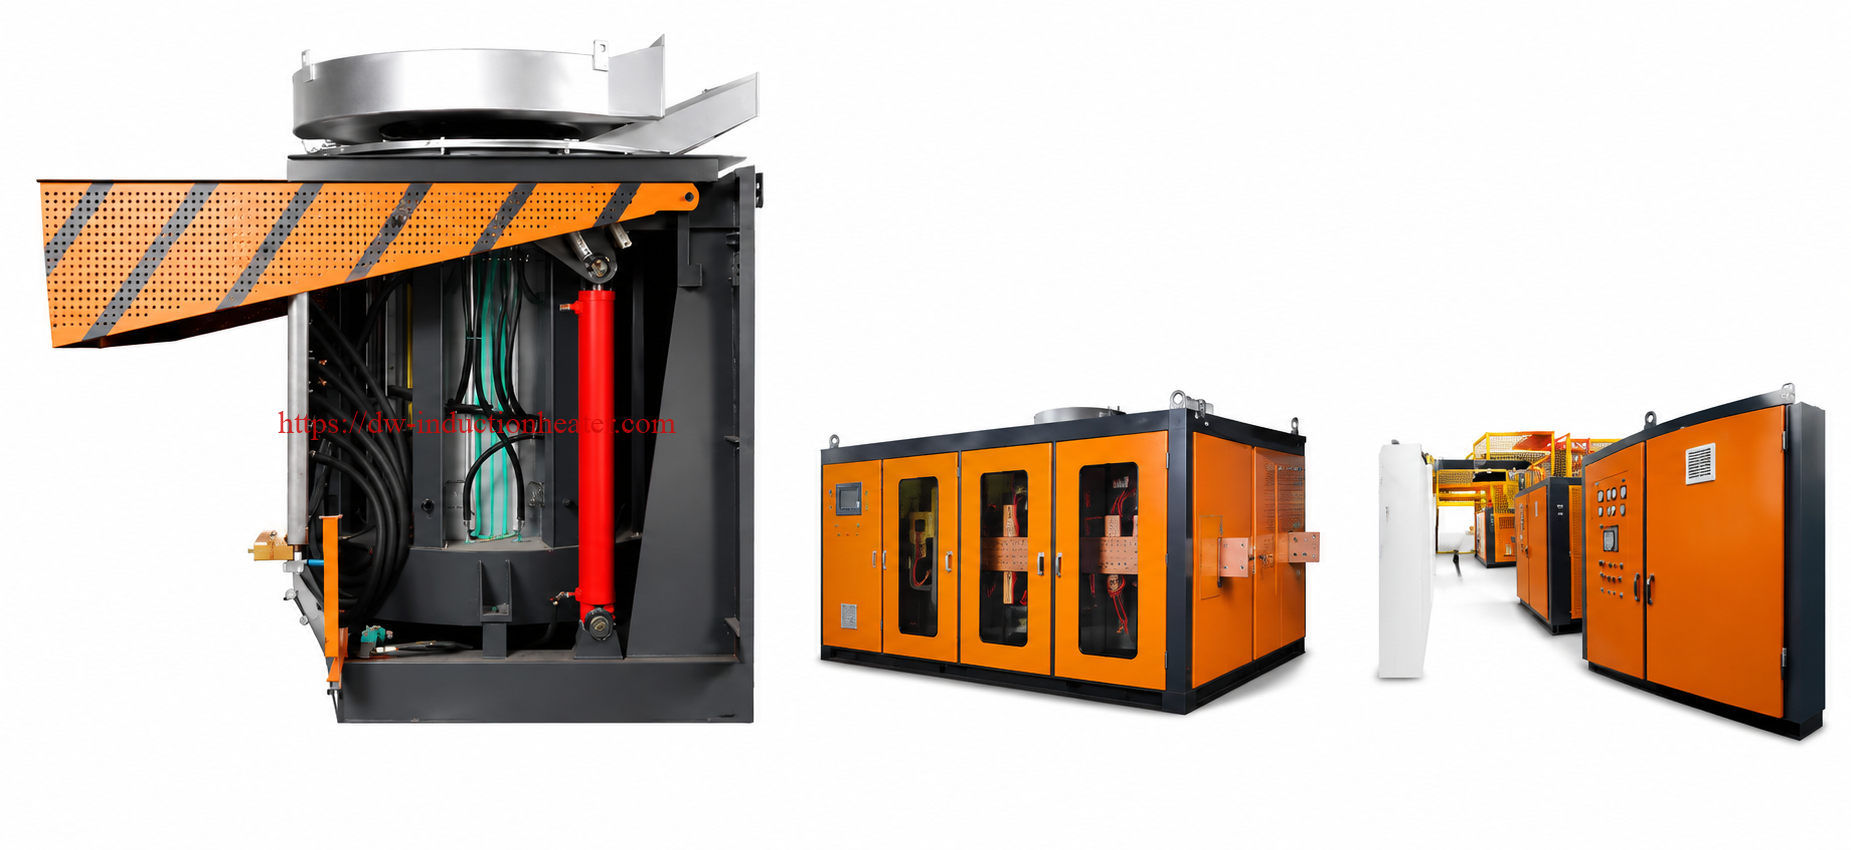
Although induction furnaces are efficient and clean, they are not free from engineering limitations. Before purchasing a furnace for melting iron and steel, buyers should evaluate electrical capacity, cooling water, lining maintenance, operator training and safety protection.
| Limitation | Reason | Recommended Solution |
|---|---|---|
| High electrical demand | Melting iron and steel requires large electrical power. | Confirm transformer capacity, input voltage and cable size before installation. |
| Cooling water is essential | Coil, cables, power supply and capacitor cabinet produce heat during operation. | Use reliable water cooling with flow and pressure protection. |
| Refractory lining is consumable | Lining is exposed to high temperature, slag attack and mechanical damage. | Select correct lining and follow sintering, inspection and repair procedure. |
| Wet scrap is dangerous | Moisture can expand rapidly and cause molten metal splashing. | Use dry clean charge materials and avoid sealed scrap pieces. |
| Wrong furnace size increases cost | Oversized or undersized furnaces reduce efficiency and productivity. | Select capacity according to real batch weight and daily production plan. |
| Alloy control needs process discipline | Overheating or long holding can cause alloy loss. | Use correct temperature control, sampling and alloy addition sequence. |
Why Choose HLQ Induction Equipment?
HLQ Induction Equipment provides induction heating and induction melting solutions for industrial metal processing. For iron and steel melting projects, the value is not only the furnace body or power cabinet. A reliable system requires correct matching of furnace capacity, power supply, capacitor cabinet, cooling system, refractory lining, hydraulic tilting mechanism, safety protection and workshop layout.
For buyers, a properly engineered induction furnace can reduce melting time, improve molten metal consistency, support scrap recycling and improve foundry production efficiency. HLQ can support furnace selection according to metal type, batch capacity, target melting time, local voltage, transformer capacity, cooling water condition and casting process.
| HLQ Capability | What It Means | Customer Benefit |
|---|---|---|
| Iron and Steel Melting Application Support | Furnace configuration can be selected for cast iron, steel, stainless steel and alloy steel. | Improves project matching and reduces wrong selection risk. |
| Medium Frequency / KGPS Furnace Systems | Power supply and furnace body can be matched according to capacity. | Supports stable melting performance and practical foundry use. |
| Steel Shell and Aluminum Shell Options | Different furnace structures are available for different production levels. | Buyers can balance cost, strength and safety. |
| Hydraulic Tilting Design | Furnace can be tilted for controlled pouring. | Improves operator safety and pouring stability. |
| Cooling and Safety Configuration | Cooling system, alarms and protection can be integrated. | Reduces downtime and improves operating safety. |
| Engineering Selection Guidance | Support for capacity, power, voltage, cooling and layout selection. | Helps buyers build a practical melting system rather than only purchasing a furnace. |
FAQ
1. What is an induction furnace for melting iron and steel?
It is an electric melting furnace that uses electromagnetic induction to heat and melt cast iron, carbon steel, alloy steel, stainless steel and scrap steel. It is commonly used in foundries, casting plants and metal recycling workshops.
2. How does an induction furnace melt iron and steel?
The power supply sends medium-frequency current through a water-cooled copper coil. The coil creates an alternating magnetic field, which induces eddy currents inside the iron or steel charge. These currents generate heat and melt the metal.
3. What type of induction furnace is best for steel melting?
For steel melting, a medium-frequency steel shell induction furnace is usually recommended for medium and large production. KGPS induction furnaces are also widely used for ferrous metal melting and foundry applications.
4. Can an induction furnace melt cast iron?
Yes. Cast iron is one of the most common materials melted in induction furnaces. Gray iron, ductile iron, pig iron and foundry returns can all be melted with proper lining, charge preparation and temperature control.
5. Can an induction furnace melt stainless steel?
Yes. Stainless steel can be melted in an induction furnace. However, temperature control, slag practice and alloy loss control are important, especially for chromium-containing alloys.
6. What capacity induction furnace should I choose?
Choose capacity according to batch weight, daily production and melting time. Small foundries may use 100–350kg furnaces, while medium and large foundries may use 500kg, 1 ton, 2 ton, 3 ton or 5 ton induction furnaces.
7. How much power is needed for melting iron and steel?
Power depends on furnace capacity, metal type and required melting time. Small furnaces may use 100–250kW, while 1-ton furnaces may use around 500–800kW and larger 3–5 ton systems may require 1500–2500kW or more.
8. What is the difference between steel shell and aluminum shell induction furnace?
A steel shell furnace has a stronger mechanical structure and is better for larger or heavy-duty iron and steel melting. An aluminum shell furnace is usually lighter and more economical for smaller or medium-capacity applications.
9. Does an induction furnace require water cooling?
Yes. The induction coil, induction heating power supply, capacitor cabinet and water-cooled cables all require stable cooling water. Water flow and pressure protection are important for safe operation.
10. What refractory lining is used for iron and steel melting?
The lining can be acidic, neutral or basic depending on the metal, slag chemistry and furnace operation. Correct lining selection and sintering are essential for safety and service life.