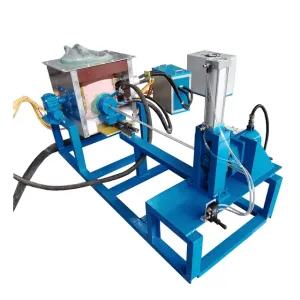
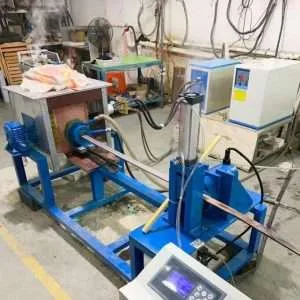
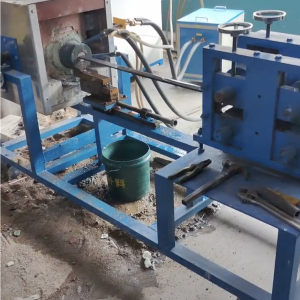
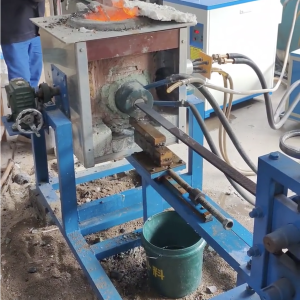
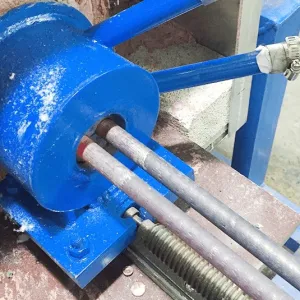
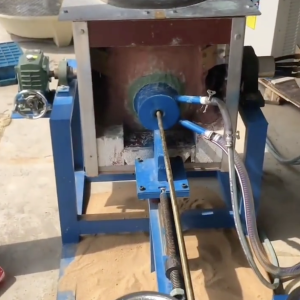
Small Induction Melting and Continuous Copper Rod Bar Plate Strip Wire Casting Furnace
Small Induction Melting and Continuous Copper Rod | Bar | Plate | Strip | Wire Casting Furnace
Table of Contents
- Quick Answer
- What Is This Product?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Coil and Fixture Design
- Control System and Automation
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages
- Limitations
- Why Choose HLQ Induction Equipment?
- FAQ
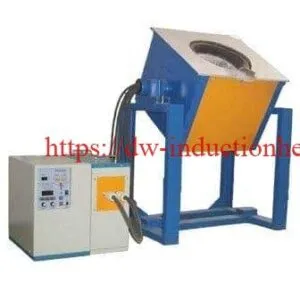
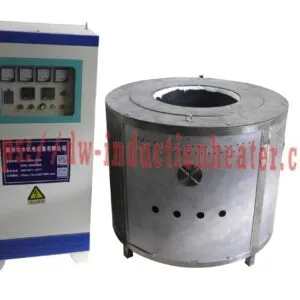
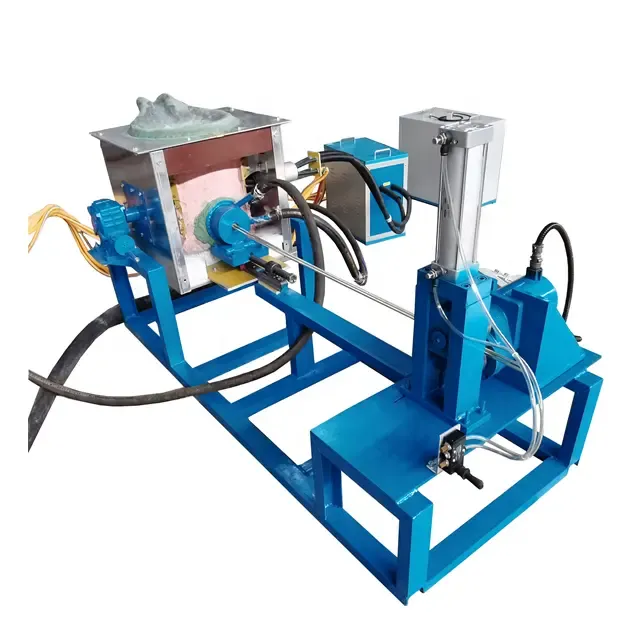
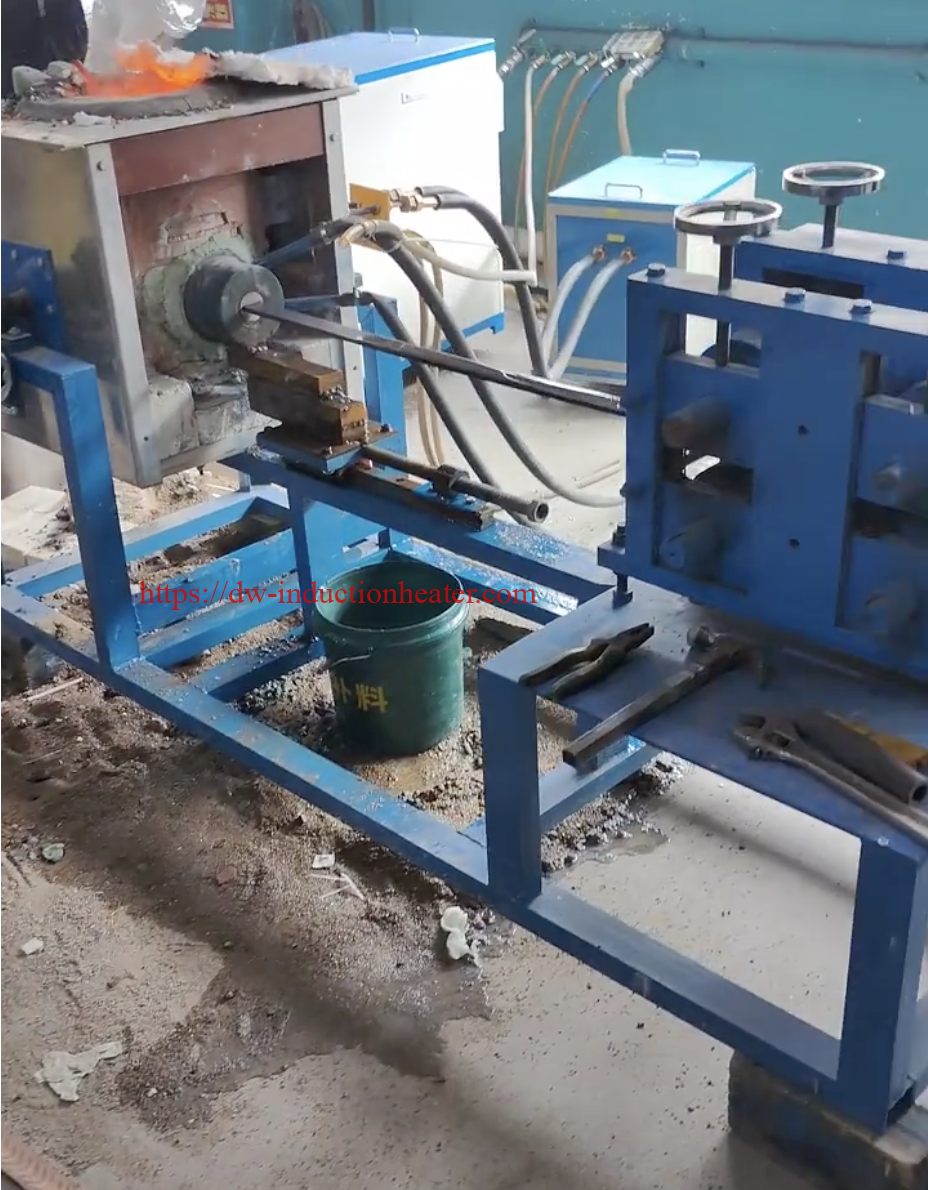
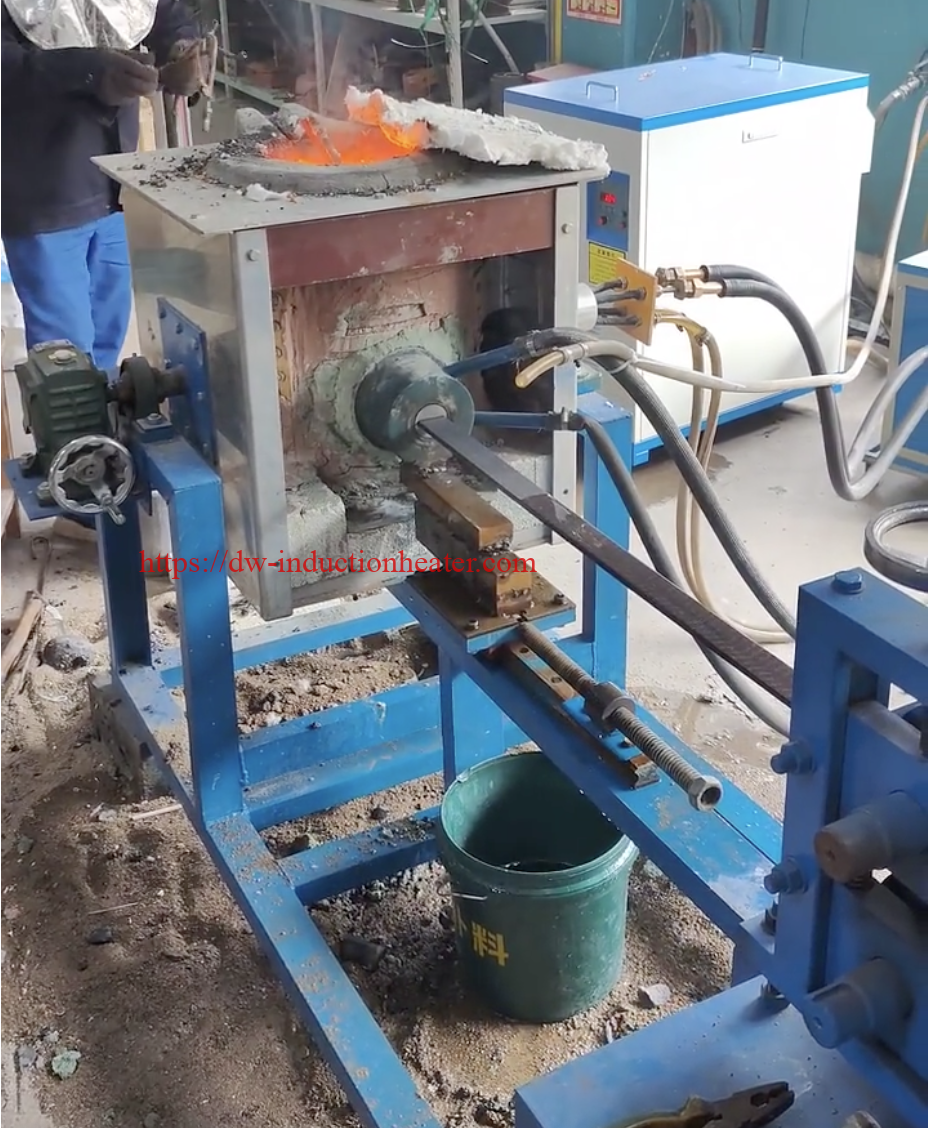
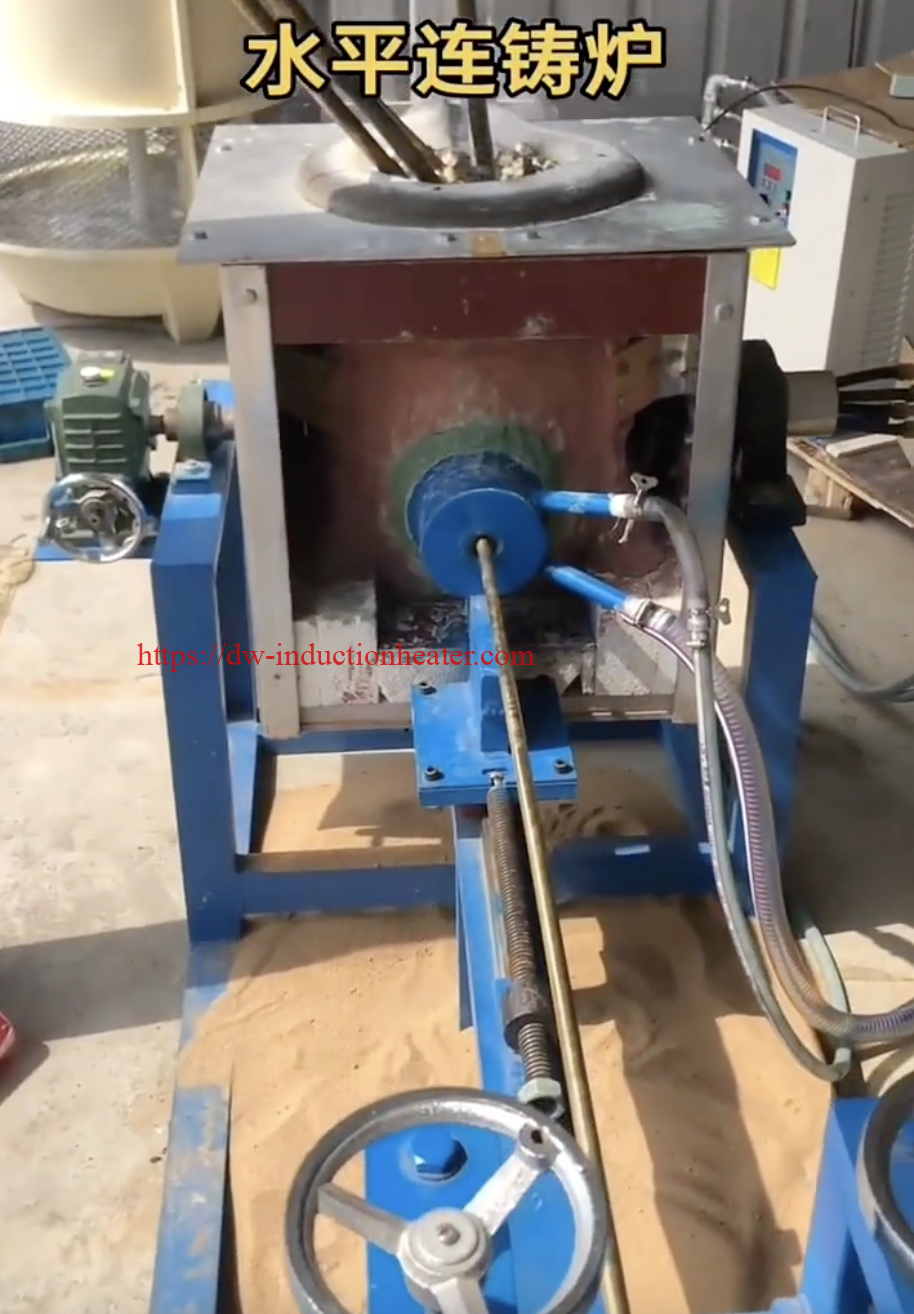
A small induction melting and continuous copper rod/bar/plate/strip/wire casting furnace is a compact metal production system used to melt copper, brass, bronze and copper alloys, then cast them into continuous semi-finished products. It is used in copper recycling plants, cable material workshops, electrical component factories, foundries, alloy laboratories and small-to-medium metal processing lines. The system helps buyers solve problems such as high melting cost, unstable casting quality, limited workshop space, inconsistent product dimensions, oxidation loss, low material recovery and difficulty producing multiple copper product shapes with one flexible melting platform.
Quick Answer
A small induction melting and continuous copper rod/bar/plate/strip/wire casting furnace is an integrated copper melting and casting solution that uses electromagnetic induction to melt copper or copper alloys and then forms the molten metal into rods, bars, plates, strips or wire feedstock through continuous casting dies, molds, crystallizers, pulling rollers and cooling systems. It is best suited for small and medium copper processing plants that need flexible production, clean electric heating, stable temperature control, high material utilization and customized copper semi-finished products for wire drawing, rolling, machining, stamping, electrical conductivity applications and alloy manufacturing.
What Is This Product?
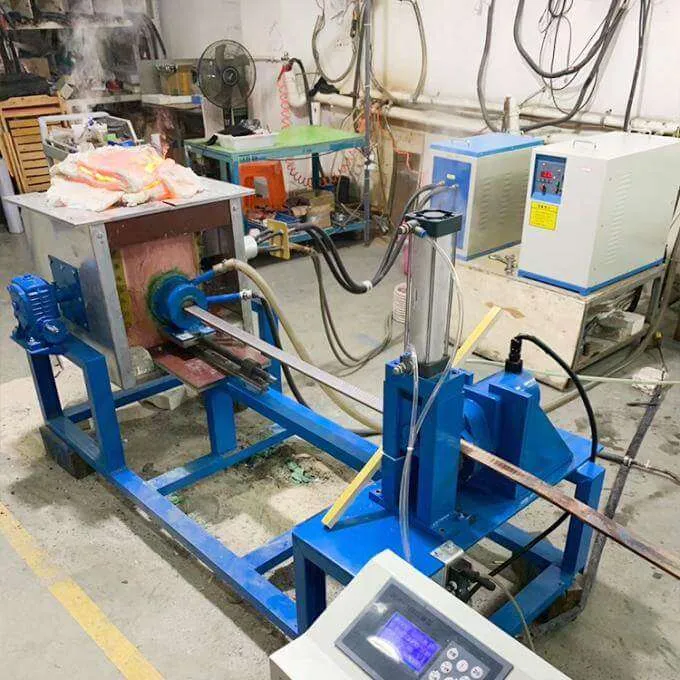
The small induction melting and continuous copper rod/bar/plate/strip/wire casting furnace is a customized production line that combines a compact induction melting furnace with a continuous casting module. It is designed for customers who do not need a huge copper smelting plant but still require industrial-level melting speed, reliable temperature control and stable casting quality. The system can process copper cathode, clean copper scrap, copper wire scrap, copper granules, brass scrap, bronze ingots and other copper alloy materials, then convert them into valuable semi-finished products.
Unlike a simple crucible melting furnace, this system includes both thermal processing and shape-forming functions. The induction furnace melts the charge material and homogenizes the molten bath. The holding or transfer section stabilizes the temperature before casting. The casting section forms the copper into the required shape. The traction system controls pulling speed. The cooling system controls solidification. The cutting, coiling or collecting equipment prepares the product for downstream processing.
From an engineering perspective, the system is built around four core requirements: stable melt temperature, controlled metal flow, balanced solidification and synchronized traction. Copper has high thermal conductivity and high electrical conductivity, which makes it excellent for electrical products but challenging during melting and casting. If temperature, cooling or pulling speed is not controlled correctly, the final product may have surface cracks, internal shrinkage, oxide inclusions, poor conductivity, uneven thickness, edge defects or unstable dimensions.
For this reason, a good small copper continuous casting furnace is not selected only by power rating. It must be designed according to the final product shape. Rod casting, bar casting, plate casting, strip casting and wire feedstock casting all require different mold structures, cooling methods and pulling controls. HLQ induction equipment can be configured as a compact melting system, a melting and holding system, or a customized melting-casting line depending on the buyer’s production target.
Key Applications
The furnace is suitable for small and medium copper processing operations where flexible product sizes and controlled production cost are more important than ultra-large mass production. It can be used for recycling, electrical material production, alloy testing, casting stock preparation and semi-finished copper product manufacturing.
| Application | Final Product | Typical User | Engineering Purpose |
|---|---|---|---|
| Copper rod production | Round copper rods, wire rods | Cable material workshop, wire drawing plant | Prepare feedstock for drawing and electrical use |
| Copper bar production | Round bar, square bar, rectangular bar | Machining factory, electrical component plant | Produce conductive or machinable copper stock |
| Copper plate casting | Thin or medium copper plate blanks | Rolling mill, stamping plant | Prepare plate stock for rolling, cutting or stamping |
| Copper strip casting | Continuous strip, flat copper strip | Electrical strip producer, transformer material plant | Produce flat stock for rolling or electrical components |
| Copper wire feedstock casting | Small rod or wire preform | Wire drawing factory | Produce material for subsequent drawing |
| Copper scrap recycling | Rod, bar, plate or strip stock | Metal recycler, foundry | Convert clean scrap into higher-value products |
| Brass rod/bar casting | Machining brass rods and bars | Valve, fitting and hardware manufacturer | Prepare brass stock with controlled composition |
| Bronze bar casting | Bearing bronze, bushing bar, wear-resistant bar | Mechanical parts manufacturer | Produce alloy bar for machining |
| Oxygen-free copper production | High-conductivity copper rod or strip | Electrical and electronics material supplier | Reduce oxidation and improve conductivity |
| R&D alloy testing | Small rods, plates, strips or sample bars | Laboratory, university, alloy developer | Test new copper alloy compositions |
Product Shape and Downstream Process Chart
| Casting Product | Typical Downstream Process | Typical End Use | Key Quality Requirement |
|---|---|---|---|
| Rod | Drawing, straightening, cutting | Wire, cable, connectors | Roundness, surface quality, conductivity |
| Bar | Machining, turning, milling | Terminals, bushings, fittings, fasteners | Density, straightness, chemical uniformity |
| Plate | Rolling, cutting, stamping | Busbar blanks, heat sinks, electrical plates | Thickness consistency, flatness, internal soundness |
| Strip | Cold rolling, slitting, annealing | Transformer strips, connectors, terminals | Edge quality, thickness control, surface finish |
| Wire feedstock | Multi-pass drawing | Fine copper wire, winding wire | Low inclusions, good ductility, stable diameter |
 Suitable Materials

The system is mainly designed for copper and copper-based alloys. Material selection affects furnace lining, crucible type, casting temperature, atmosphere protection, pulling speed and cooling intensity. Pure copper requires high temperature and oxidation control. Brass requires zinc loss control. Bronze requires alloy uniformity and segregation control. Copper-nickel and high-strength copper alloys may need higher melting power and stronger refractory compatibility.
| Material | Typical Product | Melting/Casting Concern | Recommended Control Method |
|---|---|---|---|
| Pure copper | Rod, bar, plate, strip, wire feedstock | Oxidation and conductivity loss | Use clean charge, covered bath and controlled superheat |
| Oxygen-free copper | Conductive rod, strip, wire feedstock | Oxygen pickup during melting and casting | Use protected melt surface and low-turbulence casting |
| Electrolytic copper cathode | High-purity rod or strip | Maintain purity | Avoid contaminated scrap and dirty tools |
| Copper wire scrap | Recycled rod or bar | Insulation, oil and mixed metal contamination | Pre-clean, sort and dry before melting |
| Brass | Rod, bar, strip | Zinc burning loss and fume generation | Control temperature and use fume extraction |
| Tin bronze | Bar, plate, strip | Segregation and slag formation | Use electromagnetic stirring and correct pouring temperature |
| Aluminum bronze | High-strength bar and plate | Aluminum oxidation and refractory reaction | Use suitable crucible and controlled atmosphere |
| Copper-nickel alloy | Corrosion-resistant bars and strips | Higher melting demand and alloy uniformity | Select suitable power density and holding time |
| Phosphor bronze | Strip, plate, spring material | Composition control and strip surface quality | Use accurate alloy addition and stable casting speed |
| Special copper alloys | Custom rod, bar, plate or strip | Different alloy elements have different oxidation behavior | Confirm process through sample testing |
Material Suitability Matrix
| Material | Rod | Bar | Plate | Strip | Wire Feedstock |
|---|---|---|---|---|---|
| Pure copper | Excellent | Excellent | Good | Good | Excellent |
| Oxygen-free copper | Excellent | Good | Good | Excellent | Excellent |
| Brass | Excellent | Excellent | Good | Good | Limited |
| Tin bronze | Good | Excellent | Good | Good | Limited |
| Aluminum bronze | Good | Excellent | Good | Limited | Limited |
| Phosphor bronze | Good | Good | Good | Excellent | Good |
| Copper-nickel alloy | Good | Good | Good | Good | Limited |
Working Principle
The working principle is based on electromagnetic induction. The induction power supply converts industrial three-phase power into medium-frequency alternating current. This current flows through a water-cooled copper coil surrounding the crucible or furnace chamber. The alternating magnetic field penetrates the conductive copper charge and induces eddy currents inside the material. These eddy currents generate heat through electrical resistance, causing the copper or copper alloy to melt rapidly.
Once the metal becomes liquid, electromagnetic stirring helps equalize temperature and composition. This is useful for alloy melting because alloying elements must be distributed evenly before casting. However, too much stirring, too high temperature or too long holding time can increase oxidation and alloy loss. Therefore, the system should use correct frequency, power density, crucible geometry and temperature control.
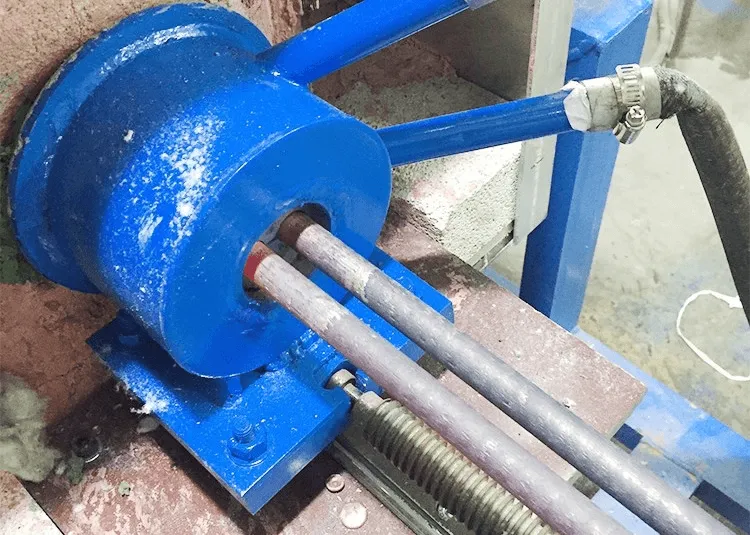
After melting, the molten copper is guided into a continuous casting section. Depending on the product, the line may use vertical upcasting, horizontal casting, downward casting, twin-roll casting or mold-based strip/plate casting. The molten metal enters a graphite die, water-cooled crystallizer or shaped mold. Heat is extracted through controlled cooling. The solidified shell forms first, then the internal core solidifies as the product is pulled forward. The pulling speed must match the solidification rate; otherwise, defects may occur.
Figure 1: Induction Melting and Continuous Casting Principle
| Stage | Process Action | Engineering Function | Key Control Parameter |
|---|---|---|---|
| 1 | Power conversion | Convert grid power to medium-frequency current | Voltage, current, frequency, power factor |
| 2 | Magnetic field generation | Induction coil creates alternating magnetic field | Coil turns, coil current, cooling water |
| 3 | Eddy current heating | Copper charge heats internally | Power density and coupling efficiency |
| 4 | Melting and stirring | Metal becomes liquid and homogenized | Bath temperature and stirring intensity |
| 5 | Holding and refining | Slag removal, alloy adjustment and temperature stabilization | Holding temperature and atmosphere |
| 6 | Mold feeding | Molten metal enters casting die or crystallizer | Metal level and flow stability |
| 7 | Controlled solidification | Rod, bar, plate, strip or wire feedstock forms | Cooling water flow and die temperature |
| 8 | Traction and collection | Product is pulled, cooled, cut or coiled | Pulling speed and tension |
Figure 2: Simplified Layout Diagram
Copper Cathode / Clean Scrap / Alloy Charge
        ↓
Weighing + Sorting + Drying
        ↓
Induction Melting Furnace
        ↓
Holding / Temperature Stabilization
        ↓
Casting Mold / Die / Crystallizer
        ↓
Traction Rollers / Servo Pulling System
        ↓
Cooling Tank / Spray Cooling / Roll Cooling
        ↓
Rod / Bar / Plate / Strip / Wire Feedstock
        ↓
Cutting / Coiling / Straightening / Inspection
Technical Specifications
| Parameter | Specification | Notes |
|---|---|---|
| Product name | Small induction melting and continuous copper rod/bar/plate/strip/wire casting furnace | Customized for copper semi-finished product production |
| Applicable materials | Copper, oxygen-free copper, brass, bronze, copper-nickel alloy and other copper alloys | Material composition affects crucible, atmosphere and casting parameters |
| Typical melting capacity | 10 kg to 1000 kg per batch | Higher capacity can be customized |
| Typical output range | 20 kg/h to 1500 kg/h | Depends on power, product shape and casting speed |
| Recommended power range | 15 kW to 500 kW for small and medium systems | Larger production lines may use higher power |
| Power supply type | IGBT medium-frequency induction power supply | Stable output and fast power response |
| Frequency range | 0.5 kHz to 20 kHz typical | Selected according to load size and furnace geometry |
| Input voltage | Three-phase industrial voltage | Customized according to local power supply |
| Melting temperature | Designed according to copper or copper alloy process | Pure copper melts at about 1085°C, but casting requires controlled superheat |
| Temperature control | Thermocouple, immersion probe, infrared pyrometer or combined measurement | Closed-loop control available |
| Crucible material | Graphite, silicon carbide graphite, ceramic or refractory-lined crucible | Selected according to alloy and temperature |
| Furnace structure | Stationary, tilting, melting-holding integrated or separated melting and holding type | Selected according to output and operation mode |
| Casting methods | Upcasting, horizontal casting, downward casting, plate/strip casting or custom die casting | Chosen by product shape |
| Rod diameter | Approx. 6 mm to 80 mm | Customized mold required |
| Bar size | Round, square or rectangular bar | Depends on die and pulling system |
| Plate width | Small and medium custom widths | Requires flat mold or roll-assisted casting design |
| Strip thickness | Customized thin or medium strip blank | Usually followed by rolling or annealing |
| Wire feedstock | Small rod or pre-wire casting | Used before wire drawing |
| Pulling system | Servo pulling, inverter motor traction or roller traction | Stable speed improves product quality |
| Cooling method | Water-cooled crystallizer, cooling jacket, cooling tank, spray cooling or roll cooling | Must match product shape and speed |
| Control system | Manual, semi-automatic, PLC + HMI automatic control | Recipe function available |
| Protection functions | Overcurrent, overvoltage, water pressure, water temperature, phase loss and emergency stop | Protects furnace and operator |
| Cooling water system | Closed-loop chiller or cooling tower recommended | Protects power supply, coil and crystallizer |
| Atmosphere protection | Covering agent, charcoal cover, nitrogen or inert gas optional | Useful for oxygen-free copper and high-quality copper alloys |
| Collection method | Cutting table, coiler, receiving table or straightening unit | Depends on product shape |
| Installation style | Compact skid, modular line or custom workshop layout | Designed according to available space |
| Operator requirement | 1 to 3 operators typical | Depends on automation level |
Recommended Model Selection
The correct model should be selected according to target product, material type, hourly output, product size and production continuity. A furnace that is suitable for a 10 mm copper rod may not be suitable for a 200 mm wide copper strip. Rod and wire feedstock need stable roundness and low inclusions. Plate and strip need flatness, thickness control and edge quality. Bar products need density, straightness and machinability.
| Application | Material | Recommended Power | Frequency |
|---|---|---|---|
| Laboratory copper rod or strip sample casting | Pure copper, brass, bronze | 15–35 kW | 10–30 kHz |
| Small copper wire feedstock casting | Pure copper, oxygen-free copper | 35–80 kW | 4–20 kHz |
| Small copper rod casting | Copper cathode, clean copper scrap | 60–120 kW | 2–10 kHz |
| Small brass rod/bar casting | Brass ingot, brass scrap | 80–160 kW | 1–8 kHz |
| Bronze bar or plate blank casting | Tin bronze, aluminum bronze | 100–250 kW | 1–6 kHz |
| Copper strip blank casting | Pure copper, phosphor bronze, brass | 120–300 kW | 0.8–6 kHz |
| Medium copper bar or plate production | Pure copper, brass, bronze | 160–350 kW | 0.8–4 kHz |
| Higher-output copper semi-finished product line | Copper and copper alloys | 300–500 kW | 0.5–3 kHz |
Product-Based Selection Chart
| Target Product | Recommended Casting Method | Important Equipment | Critical Control Point |
|---|---|---|---|
| Copper rod | Upcasting or horizontal casting | Graphite die, crystallizer, servo pulling machine | Roundness and surface finish |
| Copper bar | Horizontal casting or downward casting | Shaped mold, cooling jacket, traction rollers | Density and straightness |
| Copper plate | Flat mold casting or plate blank casting | Flat die, support rollers, cooling bed | Thickness and flatness |
| Copper strip | Strip mold casting or roll-assisted casting | Thin rectangular die, roll cooling, tension control | Edge quality and thickness control |
| Wire feedstock | Small rod upcasting | Small-diameter die, precise traction, coiler | Low inclusions and stable diameter |
Power and Output Reference Table
| Power Level | Typical Production Role | Suitable Buyer | Typical Product |
|---|---|---|---|
| 15–35 kW | Trial melting and sample casting | Laboratory, university, R&D center | Small rods, strips, plates and alloy samples |
| 35–80 kW | Small batch production | Small recycler or foundry | Wire feedstock and small rods |
| 80–160 kW | Workshop production | Electrical parts factory or brass processor | Rods, bars and small strips |
| 160–350 kW | Medium industrial production | Copper product manufacturer | Bars, plates and strip blanks |
| 350–500 kW | High compact output | Professional copper semi-product plant | Multiple product shapes and larger cross-sections |
Process Workflow
A reliable copper casting workflow begins before the furnace is started. Raw material must be sorted, weighed, cleaned and dried. Oil, moisture, insulation, paint, steel pieces, aluminum contamination and unknown alloys should be removed. Good raw material control reduces slag, gas defects, oxide inclusions and conductivity problems.
Figure 3: Complete Process Workflow
| Step | Operation | Purpose | Engineering Checkpoint |
|---|---|---|---|
| 1 | Raw material sorting | Separate copper, brass, bronze and impurities | Material grade and contamination check |
| 2 | Weighing and batching | Control composition and production cost | Batch record and alloy recipe |
| 3 | Cleaning and drying | Remove oil, moisture and coating | Dry charge and clean surface |
| 4 | Charging | Load material into crucible | Avoid crucible impact and overloading |
| 5 | Induction melting | Melt charge rapidly and cleanly | Power curve, water cooling and melting time |
| 6 | Slag removal | Remove oxide and floating impurities | Clean bath surface |
| 7 | Alloy adjustment | Correct chemical composition | Sampling and composition control |
| 8 | Temperature holding | Stabilize casting temperature | Superheat and holding time |
| 9 | Mold preheating | Prevent thermal shock and sticking | Die temperature and alignment |
| 10 | Continuous casting start | Form initial product section | Starting speed and metal flow |
| 11 | Stable traction | Pull product continuously | Speed, tension and vibration |
| 12 | Primary cooling | Control solidification in die | Cooling water flow and temperature |
| 13 | Secondary cooling | Reduce product temperature | Cooling tank or spray control |
| 14 | Product collection | Cut, coil, straighten or receive product | Product length, coil quality or flatness |
| 15 | Quality inspection | Confirm product acceptance | Surface, dimension, conductivity and internal defects |
Figure 4: Product-Specific Workflow
| Product | Melting | Casting | Cooling | Collection |
|---|---|---|---|---|
| Rod | Induction melting and holding | Round graphite die or crystallizer | Water jacket and secondary cooling | Coiling or cutting |
| Bar | Induction melting and alloy adjustment | Round, square or rectangular mold | Controlled cooling channel | Straightening and cutting |
| Plate | Melting and temperature stabilization | Flat mold or plate blank mold | Roller table or cooling bed | Cutting or transfer to rolling |
| Strip | Clean melt and controlled superheat | Thin rectangular die or roll-assisted casting | Roll cooling or spray cooling | Coiling or slitting preparation |
| Wire feedstock | High-purity copper melting | Small rod upcasting | Stable water cooling | Coiling before drawing |
Coil and Fixture Design
The induction coil is the main energy transfer component. It is usually made of water-cooled copper tube and designed according to crucible diameter, melt capacity, frequency, power and furnace structure. Good coil design improves magnetic coupling, reduces energy loss and protects the furnace from overheating. Poor coil design can cause slow melting, uneven bath temperature, power supply overload or coil insulation failure.
| Design Area | Recommended Engineering Practice | Purpose |
|---|---|---|
| Coil material | Water-cooled copper tube | High conductivity and reliable heat removal |
| Coil turns | Calculated according to frequency and crucible size | Provide correct magnetic field distribution |
| Coil insulation | High-temperature electrical insulation | Prevent arcing and electrical breakdown |
| Magnetic yoke | Optional laminated magnetic yoke | Improve magnetic efficiency and reduce stray field |
| Crucible support | Refractory base and mechanical support frame | Maintain stable crucible position |
| Tilting mechanism | Manual, electric or hydraulic tilting | Improve pouring control and safety |
| Holding section | Insulated bath or holding furnace | Stabilize temperature before casting |
| Die fixture | Rigid and adjustable mold support | Maintain alignment and dimension stability |
| Traction fixture | Servo or inverter-driven pulling rollers | Control speed, tension and product quality |
| Cooling fixture | Water jacket, spray manifold or roll cooling | Control solidification profile |
Fixture Requirements by Product Shape
| Product Shape | Mold/Die Design | Traction Design | Cooling Design |
|---|---|---|---|
| Rod | Round graphite die or crystallizer | Continuous pulling with low vibration | Uniform circumferential cooling |
| Bar | Round, square or rectangular die | Stronger roller traction | Balanced cooling to avoid bending |
| Plate | Flat mold with stable support | Roller table or step pulling | Wide-area cooling with flatness control |
| Strip | Thin rectangular die or roll gap | Tension-controlled pulling | Controlled roll or spray cooling |
| Wire feedstock | Small round die | Fine servo traction | Stable cooling to prevent microcracks |
For plate and strip casting, fixture rigidity and alignment are especially important. Even small die misalignment can cause uneven thickness, edge cracks or surface waves. For rod and wire feedstock, traction stability is more critical because vibration creates diameter fluctuation and surface marks. For bar casting, the mold must remove enough heat to prevent shrinkage while avoiding excessive thermal stress.
Control System and Automation
The control system coordinates melting power, temperature, cooling water, casting speed, product tension and safety protection. For small manual systems, the operator may control power and pulling speed directly. For industrial systems, PLC and HMI control is recommended because it improves repeatability and helps operators store process recipes.
| Control Function | Component | Purpose | Recommended Option |
|---|---|---|---|
| Power regulation | IGBT induction power supply | Control melting and holding energy | Constant power or programmed power curve |
| Temperature monitoring | Thermocouple, infrared pyrometer or immersion probe | Maintain casting temperature | Digital display with alarm |
| Cooling water protection | Flow switch, pressure sensor, temperature sensor | Protect coil, power supply and crystallizer | Automatic interlock shutdown |
| Traction control | Servo motor or inverter motor | Control casting speed and product dimension | Recipe-based speed control |
| Melt level control | Manual observation or level sensor | Keep metal head pressure stable | Recommended for continuous production |
| Cooling control | Flow valve, temperature control, pump control | Control solidification speed | Independent zones for die and secondary cooling |
| Product length control | Encoder and cutting control | Cut bars or plates to required length | Automatic length measurement |
| Coiling control | Torque-controlled coiler | Collect rod, strip or wire feedstock | Tension feedback for smooth coiling |
| Alarm recording | PLC and HMI | Trace abnormal conditions | Water, power, temperature and motor alarm history |
| Safety interlock | Emergency stop, cabinet door switch, water interlock | Protect operator and equipment | Required for industrial production |
Automation Level Comparison
| Automation Level | Main Features | Suitable User | Advantage |
|---|---|---|---|
| Manual | Manual power setting, manual casting observation | Laboratory or occasional casting | Low investment and simple operation |
| Semi-automatic | Digital temperature display, inverter traction, water alarms | Small workshop production | Better control with moderate cost |
| PLC automatic | HMI recipes, speed control, alarm record, automatic protection | Industrial copper product manufacturer | Stable repeatability and lower operator error |
| Customized intelligent line | Data logging, multi-zone cooling, length control, remote support | Professional copper processing plant | Higher quality traceability and productivity |
Common Problems and Solutions
| Problem | Possible Cause | Solution | Prevention Method |
|---|---|---|---|
| Rod surface cracks | Excessive cooling, high pulling speed or low casting temperature | Reduce pulling speed and adjust cooling water | Use stable casting temperature and controlled cooling curve |
| Bar internal shrinkage | Insufficient feeding or poor solidification control | Adjust melt level, mold length and cooling intensity | Use correct die design and stable traction |
| Plate warping | Uneven cooling or poor support | Balance cooling and improve support rollers | Use flat mold alignment and cooling bed |
| Strip edge cracks | Die misalignment, excessive tension or uneven cooling | Adjust die position and reduce tension | Use precise strip fixture and edge cooling control |
| Wire feedstock breaks during drawing | Inclusions, microcracks or unstable diameter | Improve melt cleanliness and casting stability | Use clean copper and fine traction control |
| Oxide inclusions | Dirty scrap, overheating or poor slag removal | Clean charge and remove slag before casting | Use covering agent and avoid excessive superheat |
| Low conductivity | Impurities, oxygen pickup or mixed scrap | Improve raw material purity and melt protection | Use copper cathode or qualified clean copper scrap |
| Unstable dimensions | Traction speed fluctuation or mold wear | Use servo traction and inspect die condition | Set speed recipe and maintenance schedule |
| Die sticking | Cold mold, wrong clearance or poor graphite quality | Preheat mold and use correct graphite die | Control mold temperature before startup |
| High energy consumption | Poor insulation, long holding time or wrong furnace size | Improve insulation and optimize production schedule | Match furnace capacity with actual output |
| Zinc loss in brass | Overheating or long holding time | Lower superheat and shorten holding time | Use accurate temperature control and fume extraction |
| Power supply alarm | Cooling water fault, overcurrent or coil insulation issue | Check water circuit, load matching and insulation | Use interlock protection and regular inspection |
Engineering Selection Guide
A successful small induction melting and continuous copper casting project should begin with the final product specification, not with the furnace price. Buyers should define product shape, material grade, output, quality requirements, workshop power supply, cooling water condition, available space and operator skill level.
1. Define the Product Shape
Rod, bar, plate, strip and wire feedstock require different casting systems. A round rod needs a round die and precise pulling speed. A bar needs stronger traction and better straightness control. A plate requires flat support and uniform cooling. A strip requires edge control and tension control. Wire feedstock requires excellent melt cleanliness and stable diameter.
| Product Shape | Key Design Question | Recommended Engineering Focus |
|---|---|---|
| Rod | What diameter and final use? | Roundness, surface quality and pulling stability |
| Bar | Round, square or rectangular? | Straightness, density and mold strength |
| Plate | What width and thickness? | Flatness, cooling uniformity and support structure |
| Strip | What thickness tolerance and edge quality? | Die precision, tension control and cooling profile |
| Wire feedstock | Will it be drawn into fine wire? | Low inclusions, good ductility and diameter stability |
2. Select Capacity by Hourly Output
Crucible capacity alone does not determine productivity. For continuous casting, hourly output is more important. The furnace must melt enough copper to supply the casting line without long interruptions. For stable industrial production, a separate holding section or continuous charging strategy may be necessary.
3. Choose the Correct Casting Method
| Casting Method | Best Fit | Advantages | Limitations |
|---|---|---|---|
| Upcasting | Oxygen-free copper rod and wire feedstock | Low turbulence, clean rod, compact layout | Requires stable melt level and precise traction |
| Horizontal casting | Rod, bar, strip and some plate blanks | Flexible mold shapes and easy operation | Needs accurate die alignment and cooling control |
| Downward casting | Bar and billet production | Gravity-assisted flow and simple structure | Requires careful flow and solidification control |
| Flat mold casting | Plate blanks | Suitable for wide flat products | Flatness and cooling uniformity are challenging |
| Roll-assisted strip casting | Strip blanks | Good for thin continuous products | Higher precision requirement and more complex control |
4. Match Power and Frequency
Small furnaces usually use higher frequency because smaller metal loads benefit from stronger electromagnetic coupling at shallower penetration depth. Larger crucibles and heavier copper batches often use lower frequency for deeper penetration and stronger bath stirring. HLQ can recommend frequency according to furnace size, material, melt weight and product output.
5. Design the Cooling System Correctly
Cooling is as important as melting. The induction coil, power supply, crystallizer and secondary cooling system all require stable water flow. If cooling water temperature fluctuates too much, product dimensions and surface quality may change. For industrial use, a closed-loop cooling system is recommended to protect electrical components and maintain process consistency.
6. Plan for Quality Inspection
| Product | Recommended Inspection | Reason |
|---|---|---|
| Rod | Diameter, roundness, surface, conductivity | Important for drawing and electrical use |
| Bar | Straightness, density, surface, composition | Important for machining and mechanical performance |
| Plate | Thickness, flatness, surface cracks, internal defects | Important for rolling and stamping |
| Strip | Thickness tolerance, edge cracks, surface finish | Important for rolling, slitting and electrical stamping |
| Wire feedstock | Inclusions, ductility, diameter stability, conductivity | Important for multi-pass wire drawing |
Advantages
| Advantage | Engineering Meaning | Buyer Benefit |
|---|---|---|
| Fast melting | Heat is generated directly inside copper charge | Shorter production cycle and higher output |
| Clean electric heating | No direct flame in the melt zone | Cleaner workshop and reduced contamination |
| Accurate temperature control | Power can be adjusted quickly | Stable casting quality and lower scrap rate |
| Flexible product shapes | Different molds can produce rods, bars, plates, strips or wire feedstock | One melting platform supports multiple products |
| Compact layout | High power density and modular equipment design | Suitable for small and medium workshops |
| Good alloy uniformity | Electromagnetic stirring improves bath mixing | More consistent copper alloy products |
| Lower oxidation potential | No combustion flame directly contacting melt | Better material recovery when process is protected |
| Automation compatible | Can integrate PLC, HMI, servo traction and alarms | Better repeatability and easier operation |
| Suitable for recycling | Can process clean copper scrap and alloy scrap | Turns scrap into valuable semi-finished products |
| Energy-efficient operation | Direct heating reduces unnecessary heat loss | Lower operating cost compared with poorly insulated fuel heating |
Comparison: Induction Melting vs Fuel-Fired Melting
| Item | Induction Melting and Casting | Fuel-Fired Melting | Engineering Comment |
|---|---|---|---|
| Heat source | Electromagnetic heating | Gas, oil or other fuel flame | Induction gives fast response and clean heating |
| Temperature control | Precise and adjustable | Slower and less direct | Important for continuous casting |
| Workshop environment | Cleaner and less combustion heat | More exhaust and radiant heat | Induction is better for compact workshops |
| Oxidation risk | Lower with covered bath | Higher with open flame exposure | Important for copper conductivity |
| Start-stop flexibility | Good | Slower | Useful for small batch production |
| Automation | Easy to integrate | More difficult | Induction fits PLC control better |
| Maintenance focus | Power supply, coil, crucible and cooling system | Burner, refractory and exhaust system | Both require scheduled maintenance |
Limitations
| Limitation | Why It Matters | How to Manage It |
|---|---|---|
| Higher initial investment | Power supply, coil, cooling and casting controls cost more than simple manual melting | Evaluate total cost including energy, quality, labor and recovery |
| Cooling water dependency | Power supply, coil and crystallizer must be cooled | Use stable closed-loop water cooling |
| Raw material sensitivity | Dirty scrap causes inclusions and poor conductivity | Sort, clean and test raw material |
| Operator training required | Temperature, pulling speed and cooling must be coordinated | Use standard procedures and recipe control |
| Crucible wear | Copper alloys and thermal cycling consume crucibles | Select suitable crucible and inspect regularly |
| Product-specific tooling | Rod, bar, plate and strip require different molds | Plan tooling according to product range |
| Brass fume risk | Zinc may evaporate at high temperature | Use fume extraction and avoid overheating |
| Not ideal for very large mass production alone | Large copper rod plants may need high-capacity integrated lines | Use this system for flexible small and medium production |
Why Choose HLQ Induction Equipment?
HLQ Induction Equipment focuses on industrial induction heating solutions for melting, forging, brazing, hardening, preheating, post weld heat treatment and customized thermal processing. For small induction melting and continuous copper rod/bar/plate/strip/wire casting furnace projects, HLQ can provide engineering support from process analysis to equipment configuration.
A copper casting project requires more than a furnace body. It requires correct power, frequency, coil design, crucible selection, holding method, mold structure, pulling equipment, cooling system and automation logic. HLQ can help buyers evaluate material type, production target, product shape, workshop voltage, cooling water condition and automation requirement before recommending a practical equipment solution.
| HLQ Support Area | Customer Benefit | Project Value |
|---|---|---|
| Power supply selection | Correct power and frequency for copper melting | Improves melting speed and energy efficiency |
| Customized furnace design | Furnace capacity matches actual production | Avoids underpowered or oversized equipment |
| Induction coil design | Better coupling, cooling and reliability | Improves long-term stability |
| Casting system integration | Rod, bar, plate, strip or wire casting can be customized | Supports multiple copper products |
| Automation configuration | PLC, HMI, alarms and recipe control available | Reduces operator error |
| Cooling system planning | Coil, power supply and crystallizer cooling are matched | Improves safety and product quality |
| Application engineering | Process suggestions for copper, brass and bronze | Shortens commissioning time |
| Compact layout design | Equipment can fit limited workshop space | Useful for small and medium factories |
| After-sales support | Installation, operation and maintenance guidance | Improves production reliability |
FAQ
1. What is a small induction melting and continuous copper casting furnace?
It is an integrated system that melts copper or copper alloy by induction heating and casts the molten metal continuously into rods, bars, plates, strips or wire feedstock through controlled molds and pulling equipment.
2. What products can it produce?
It can produce copper rods, copper bars, copper plate blanks, copper strip blanks and small wire feedstock. The exact product range depends on mold design, cooling system and traction equipment.
3. What materials can be melted?
The furnace can melt pure copper, oxygen-free copper, electrolytic copper, clean copper scrap, brass, bronze, phosphor bronze, aluminum bronze and other copper-based alloys.
4. Can it process copper scrap?
Yes. It can process clean copper scrap, but the scrap must be sorted, cleaned and dried. Oil, insulation, steel, aluminum and unknown mixed metals should be removed before melting.
5. What power range is recommended?
Small systems may use 15–80 kW, while workshop production often uses 80–350 kW. Higher-output copper casting lines may require 300–500 kW or customized power.
6. Which frequency is suitable for copper melting?
Typical small and medium copper induction melting systems use approximately 0.5–20 kHz, depending on crucible size, power rating, charge weight and required stirring.
7. Can one furnace produce rod, bar, plate and strip?
One induction melting platform can support different casting modules, but each product shape usually requires its own die, fixture, traction and cooling design.
8. Is upcasting better than horizontal casting?
Upcasting is often preferred for clean copper rods and wire feedstock. Horizontal casting is more flexible for rods, bars, strips and some plate blanks. The best method depends on the final product.
9. How can oxidation be reduced?
Use clean raw material, avoid excessive superheat, reduce holding time, cover the molten bath, remove slag carefully and use protective atmosphere when high conductivity is required.
10. Why does copper strip have edge cracks?
Edge cracks may be caused by uneven cooling, excessive tension, die misalignment or incorrect casting temperature. The solution is to optimize die alignment, cooling balance and traction speed.
11. Why does copper rod diameter fluctuate?
Diameter fluctuation may result from unstable pulling speed, mold wear, vibration, temperature fluctuation or inconsistent cooling. Servo traction and stable process recipes help solve this issue.
12. What cooling system is required?
A closed-loop cooling system is recommended for the induction power supply, coil and crystallizer. Stable cooling water improves safety, equipment life and casting quality.
13. Can it produce oxygen-free copper?
Yes, it can be configured for oxygen-free copper production, but it requires high-purity charge, protected melt surface, low-turbulence casting and strict process control.
14. Is the system suitable for brass casting?
Yes. It can cast brass rods, bars and strips, but zinc loss and fumes must be controlled by proper temperature management and ventilation.
15. What is the difference between rod and wire feedstock?
Rod may be used directly or machined, while wire feedstock is usually drawn into smaller wire. Wire feedstock requires lower inclusions, better ductility and more stable diameter.
16. What inspections are needed for finished products?
Common inspections include surface quality, dimension, straightness, flatness, conductivity, chemical composition and internal defect testing depending on the final application.
17. How long does installation take?
Installation time depends on induction furnace size, automation level, cooling system, casting line complexity and workshop preparation. Small systems are faster to install than fully automated production lines.
18. Can the casting line be automated?
Yes. The system can use PLC, HMI, recipe control, servo traction, cooling alarms, length control and data recording for more stable production.