



Induction Coating Removal from Steel Surface
Induction Coating Removal-Induction Rust Paint Coating Removal From Steel Surface
What Is Induction Coating Removal from Steel?
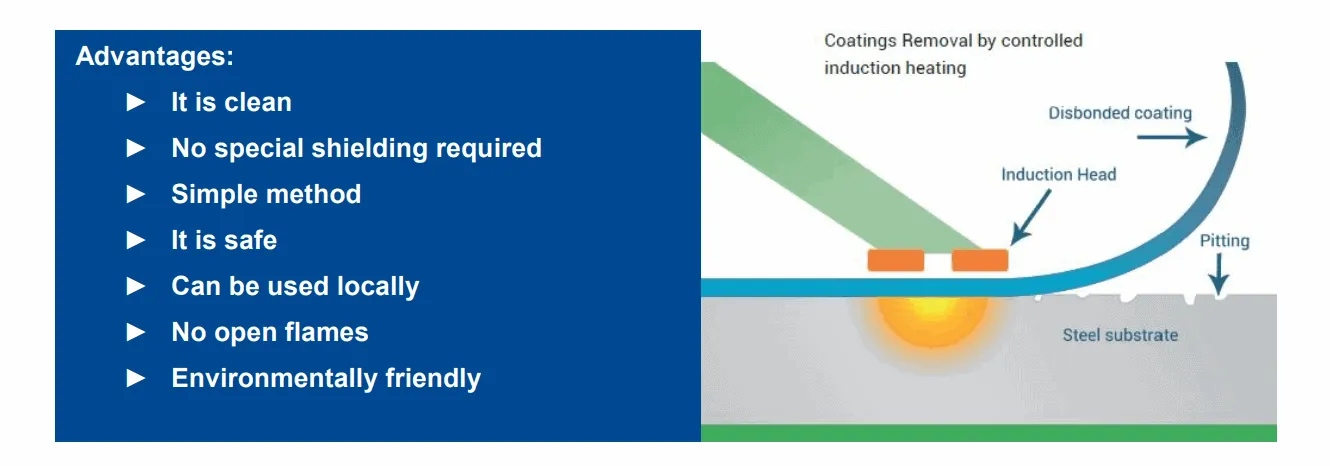
Induction coating removal is a surface-maintenance process in which electromagnetic energy is used to heat an electrically conductive steel substrate beneath paint or another bonded coating.
An induction power supply sends alternating current through an induction coil located inside or near the handheld heating head. The resulting alternating magnetic field induces electrical currents in the steel. Resistance within the steel converts this electrical energy into heat.
Instead of attempting to heat the entire coating from its outer surface, the process generates heat underneath it. When the temperature at the steel/coating interface reaches an appropriate level, adhesion decreases and the coating can be removed mechanically.
This process is also commonly referred to as Induction stripping, induction disbonding, electromagnetic coating removal or heat induction paint removal.
How induction coating removal | Induction Stripping Works?
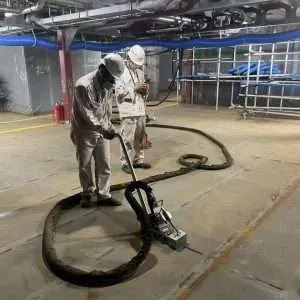
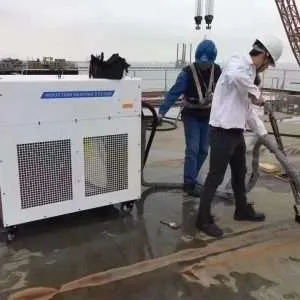
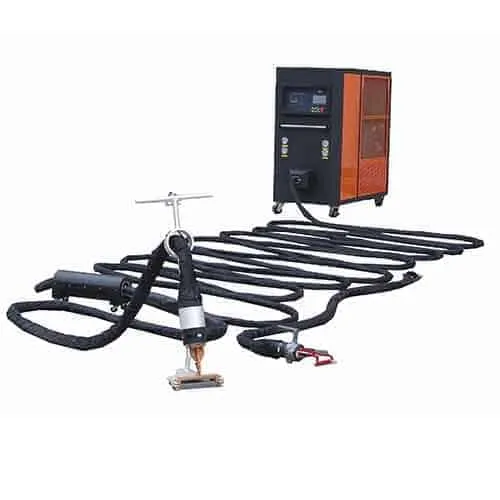
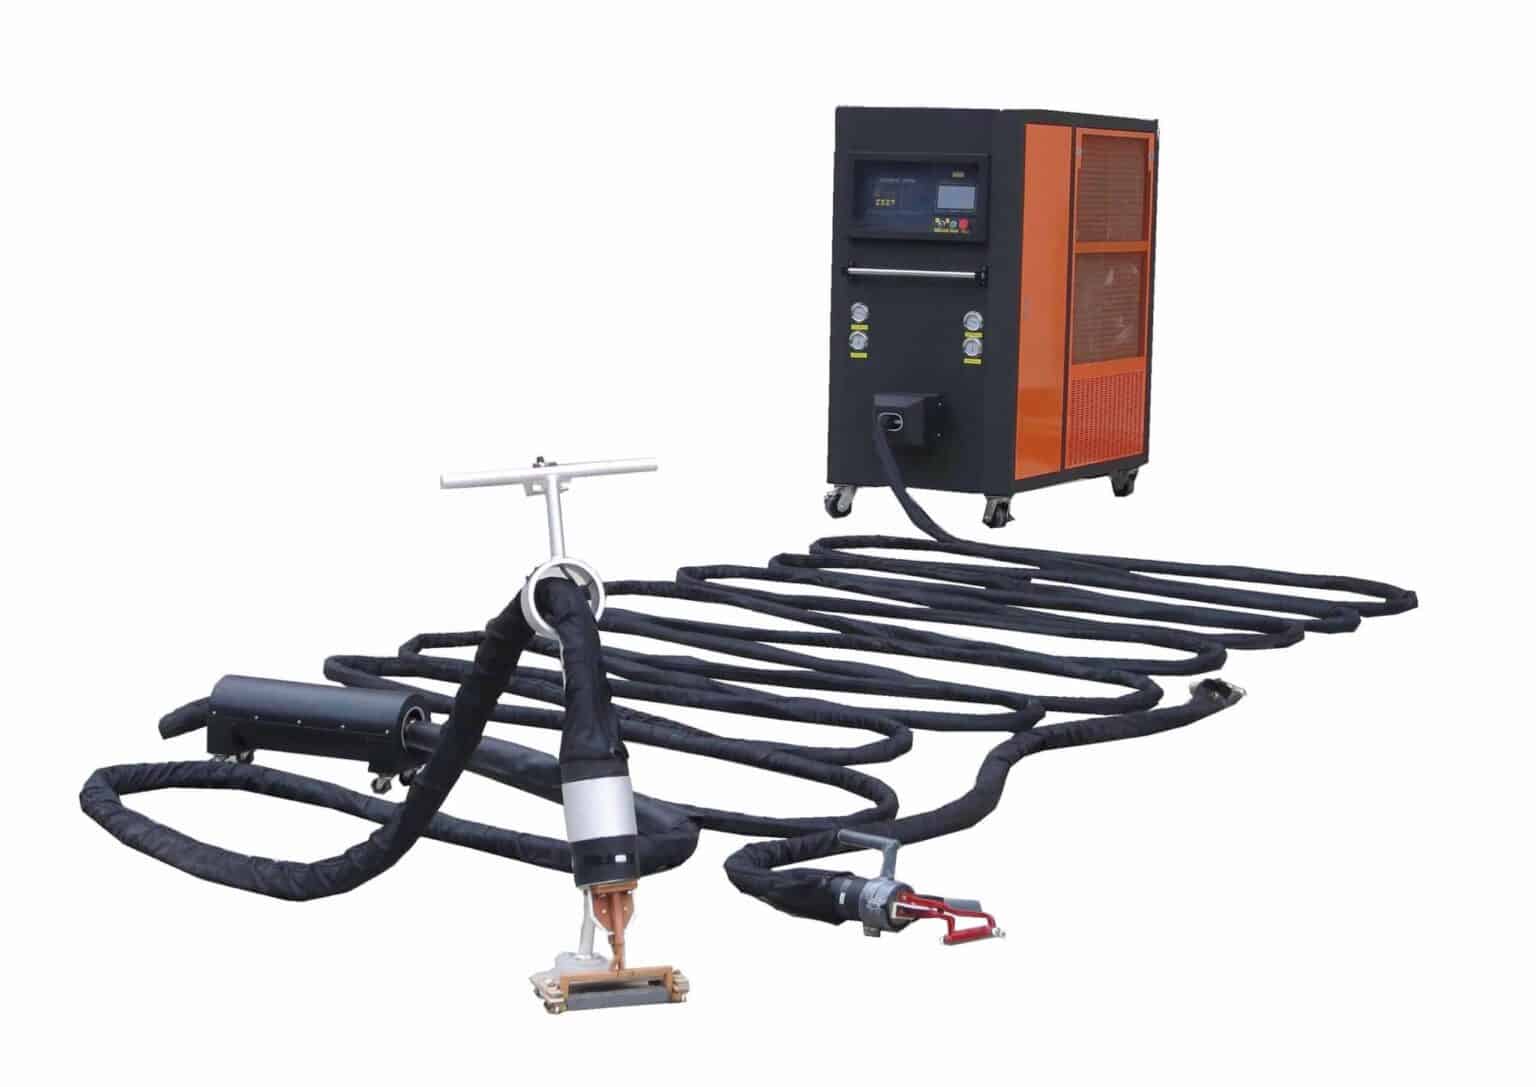
induction coating removal | Induction stripping is a hot surface preparation process.An induction heating generator sends alternating current through an induction coil, which generates an electromagnetic field. This field induces currents that are converted into heat in contact with conducting materials such as steel. The heat is generated beneath the coating, causing the coating to peel rapidly. This method is suitable for treating flat or curved surfaces on the jobsite and does not require any confinement.
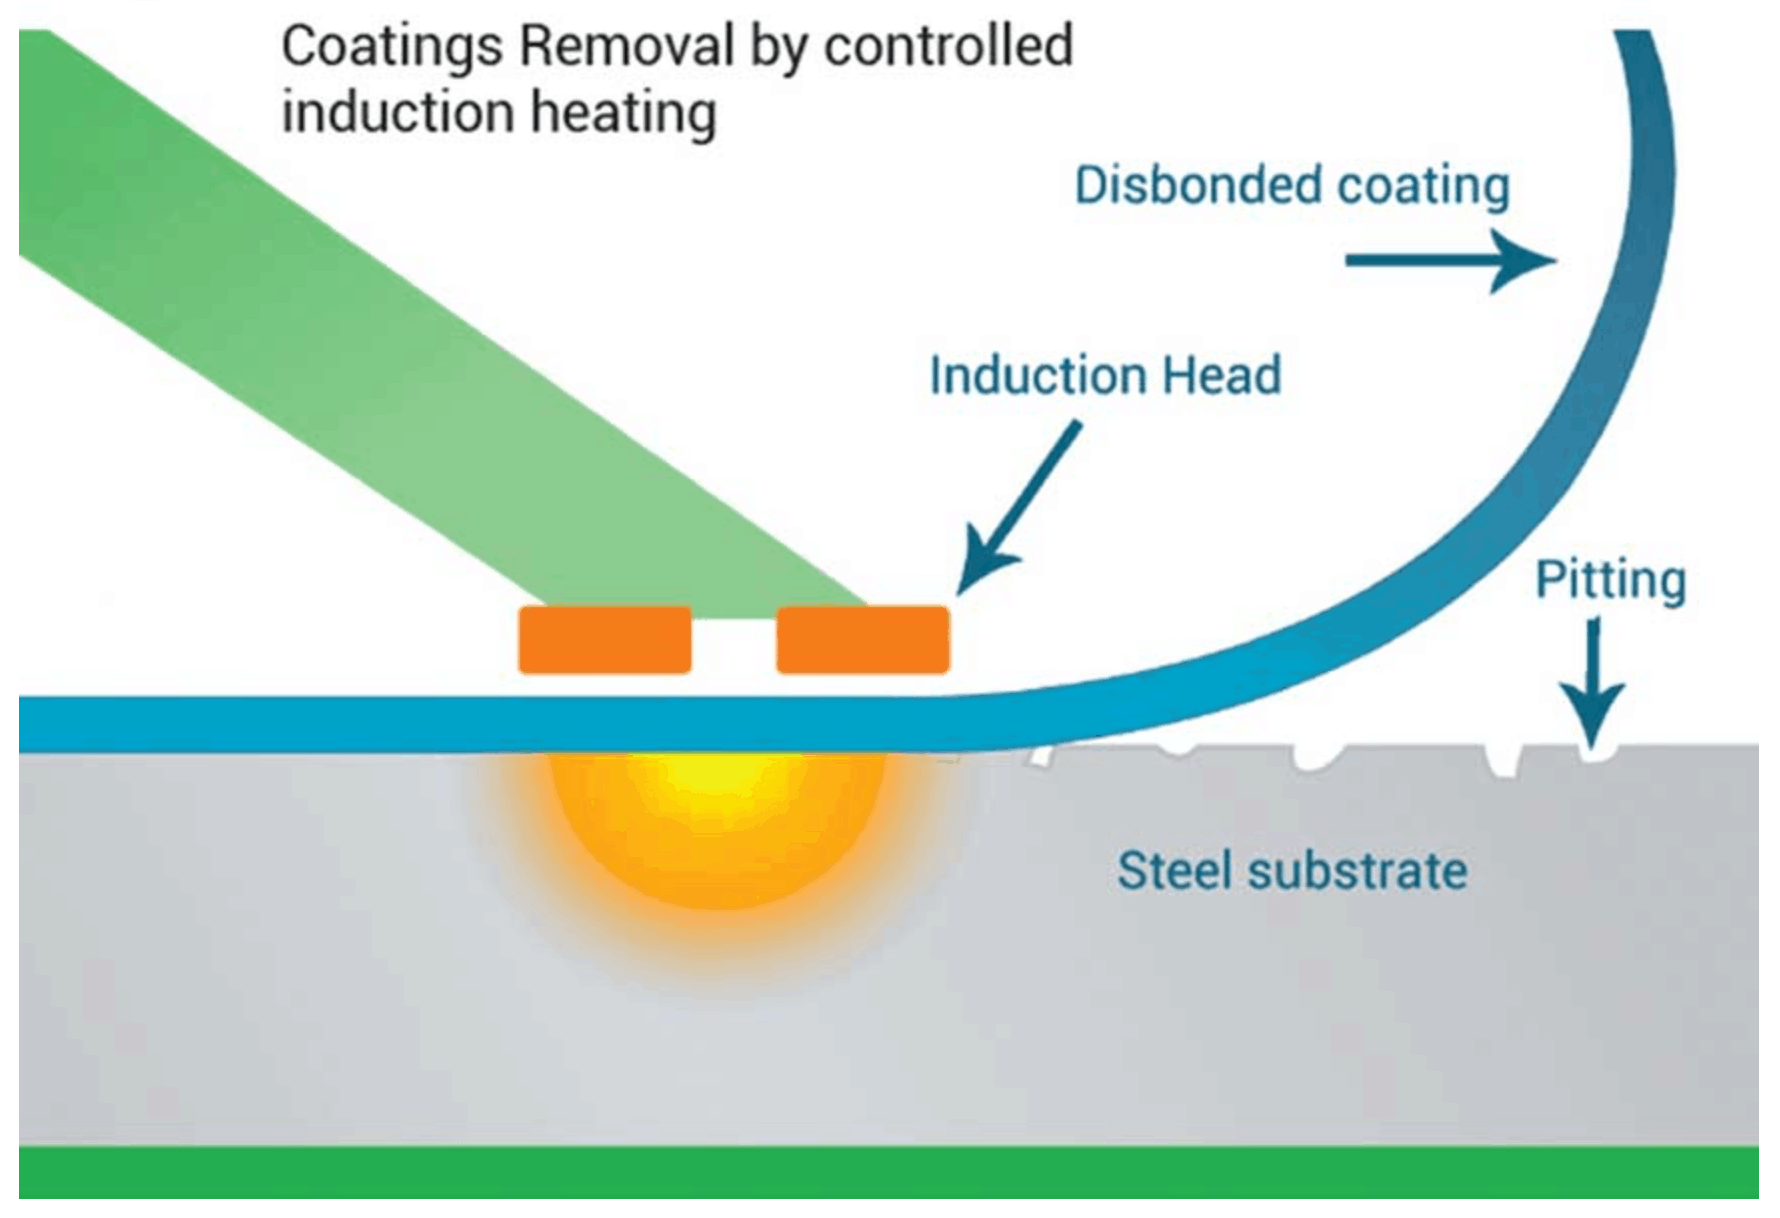
The induction coating removal|induction stripping system will strip paint, other coatings, heavy rust, bacterial corrosion and oil and grease electrically conductive surfaces (ferromagnetic steel) breaking the interfacial bonding between the material and the substrate etch residues, induction heating localized and controlled which consumes minimal energy.
HLQ simplifies your coatings removal needs with yet another revolutionary technology: Induction Stripping! HLQ’s induction stripping equipment removes your toughest coatings from steel structures with no noise or secondary waste—getting right down to the steel.
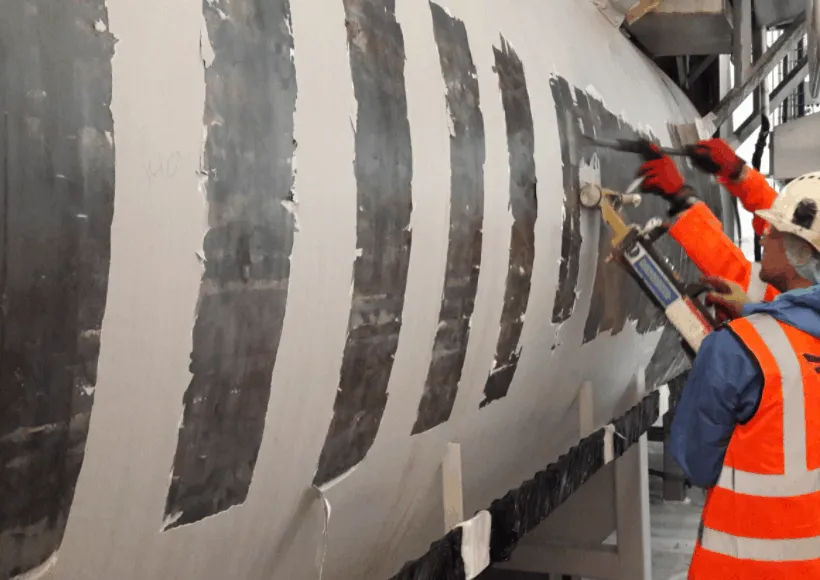
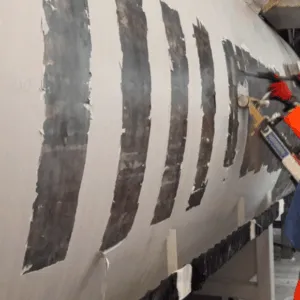
If you have ever wished for a magic wand to solve your coatings removal headaches, HLQ has the next best thing. HLQ technician can wave our induction wand over your coating catastrophe and dis-bond some of the hardest to remove coatings at rates that are up to 10 times faster than competing technologies like sandblasting.It’s not magic, but our induction stripping technology is a close second! When HLQ technicians move our induction head over a steel surface, it creates sufficient heat (typically 300 to 400 degrees) to quickly unbond most coatings from tanks, tankers, pipelines, ships and offshore platforms, allowing coatings (up to 1-inch thick) to be removed in sheets.
RPR Heat Induction Coating Removal
RPR Heat Induction coating removal works by the principle of induction. Heat is generated in the steel substrate and the bond at the steel and coating interface is broken. The coating is then removed entirely without disintegrating and completely free from contaminating agents, i.e.. blast media. This makes disposal and recycling of waste easier and more cost effective.
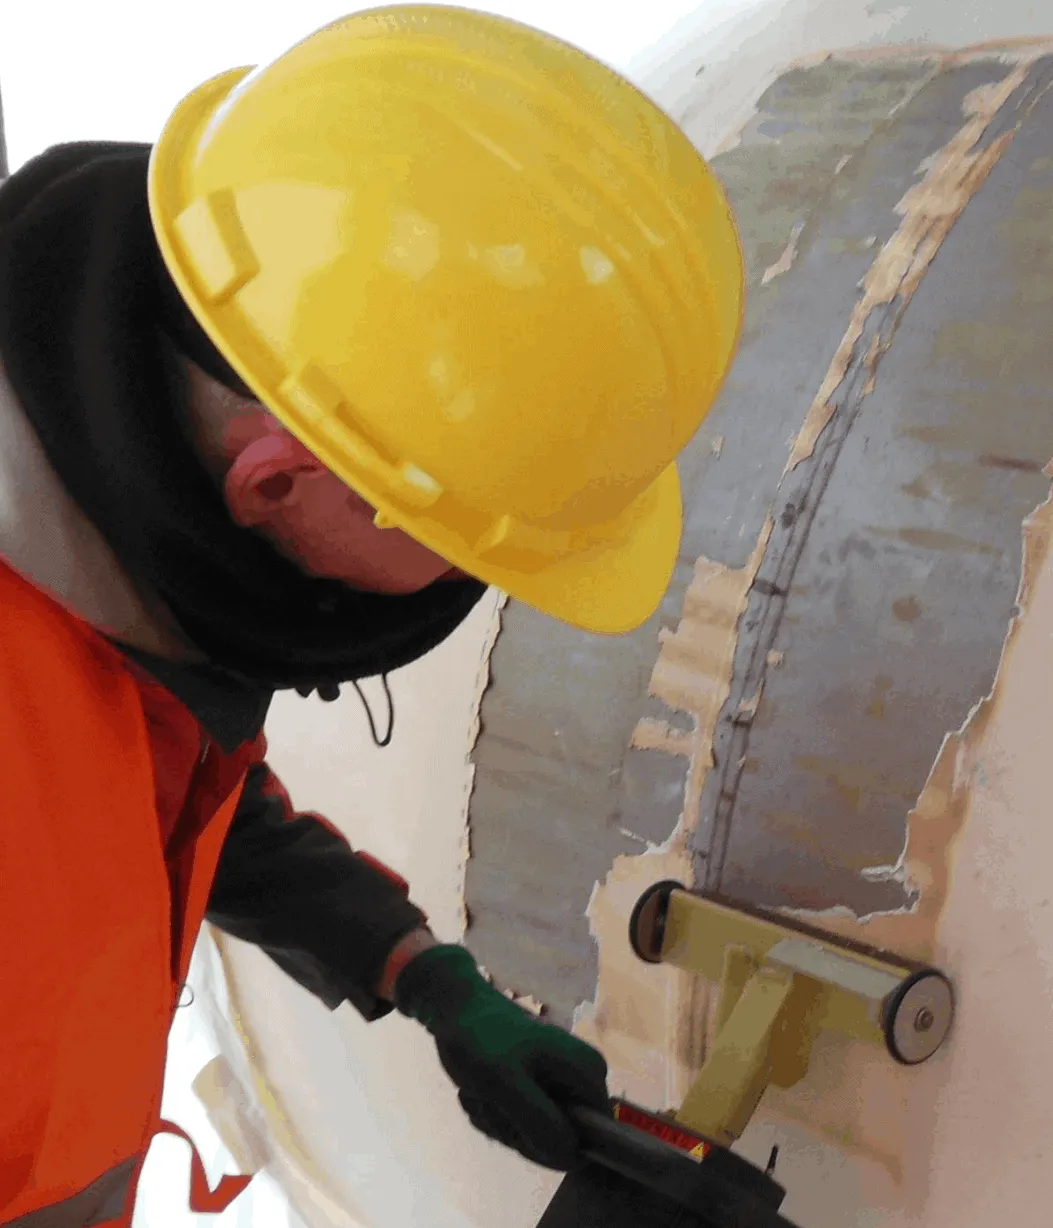
With minimum power consumption even the thickest and hardest coatings can be completely removed. RPR Heat Induction is faster than conventional methods. A silent method of coating removal means that our engineers can operate day or night with no noise pollution.
Because of the many advantages of our induction heating process, we’ve been able to provide a wide range of Alliance customers with the service they need. We’ve worked with customers in industries such as:
- Oil & gas
- Financial
- Food & beverage processing
- Retail and food services
- Marine
- Hotels & hospitality
- Commercial pools and aquariums
HLQ’s jaw-dropping induction dis-bonding process removes most coating types, including:
- Coal Tar Epoxy
- Polyethylene
- Fiberglass
- Anti-skid
- Rubber
- Chartek fireproofing or other intumescent coatings
Faster, Quieter, Cleaner, Safer Surface Preparation
A faster, safer and cleaner method for removing industrial coatings from steel surfaces.
Some might say induction stripping is the “quick and dirty” way to get the job done, but truthfully it’s quick, and not messy at all. Because induction stripping creates no secondary waste, cleanup is simplified. Dealing with sheets or strips of coating is infinitely easier than dealing with blast media and dust.
In many cases, containment can be simplified or eliminated altogether. Imagine eliminating a costly scaffolding and containment project and replacing it with a snorkel lift and a drop cloth!
Other trades can work in close proximity to HLQ’s induction stripping activities because it is a very quiet process that will not create obnoxious noises that disrupt the productivity of other contractors you may have working on your project.
Our induction stripping equipment has no moving parts, making our process much safer than hydro-blasting or sandblasting for your employees, other contractors, customers and passersby.

RPR induction removes paint, coatings, thick rust, bacterial corrosion and oil & grease residues from electrically conductive surfaces (steel, etc.) by breaking the interfacial bonding between the material to be removed and the substrate using controlled, localized induction heating with a mini- mum consumption of energy.
The induction heating principle
The RPR induction generator sends alternating current through an induction heating coil, which gener- ates an electro-magnetic field. This magnetic field induces eddy currents in a conductive mate- rial like steel. Due to the resistance of the steel, these currents are converted to heat = induction heating. The heat is generated below the coat- ing, resulting in quick and clean disbonding.
RPR Heat Induction works by the principle of induction. Heat is generated in the steel substrate and the bond at the steel and coating interface is broken. The coating is then removed entirely without disintegrating and completely free from contaminating agents, i.e.. blast media. This makes disposal and recycling of waste easier and more cost effective.
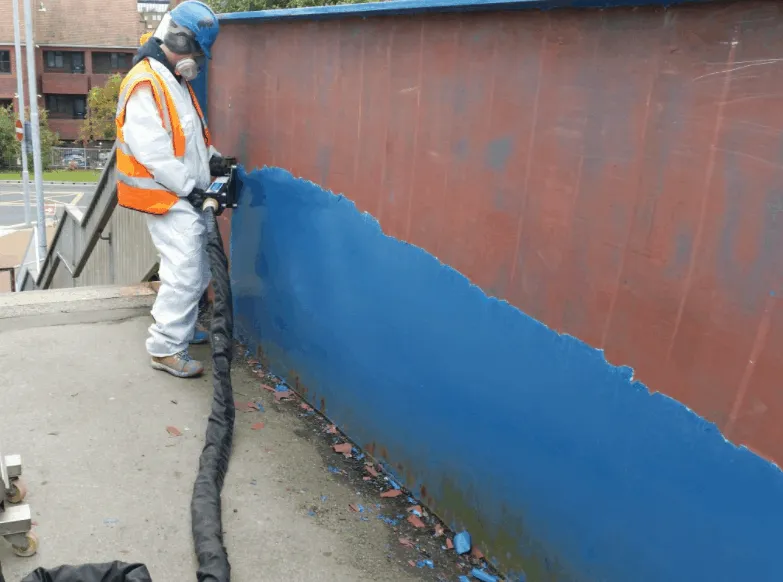 With minimum power consumption even the thickest and hardest coatings can be completely removed. RPR Heat Induction heating is faster than conventional methods. A silent method of coating removal means that our engineers can operate day or night with no noise pollution.
The RPR system is ideal for the removing paint, rust, and other coatings (vulcanized rubber, fire protectant, epoxies, etc. with control possibili- ties for the following functions:
• Energy consumption
• Disbonding temperature range
• Heat penetration
• Removal speed
With above setting possibilities, RPR delivers unequalled performance and is the system of choice for cost-effective, safe and environmentally friendly surface coating removal from steel substrates.
RPR is ideal for: marine, tanks, offshore and land-based pipelines
Induction Coating Machine & Induction Coating Removal Machine & RPR Induction System


Induction Coating Removal from Steel Surface – RPR Paint & Coating Stripping
Quick Answer: Induction coating removal from steel is a controlled thermal disbonding process that uses electromagnetic induction to generate heat directly inside the conductive steel substrate beneath a coating. The localized heat reduces adhesion at the steel-to-coating interface, allowing industrial paint, epoxy, rubber lining, polyethylene and other bonded coatings to be peeled, lifted or scraped from the surface. It is particularly useful for pipelines, storage tanks, ships, offshore structures and other large steel assets.
Unlike conventional methods that attack a coating primarily from the outside, an induction coating removal system transfers electromagnetic energy into the steel beneath the coating. This makes the interface between the steel and coating the primary heating zone.
HLQ induction stripping technology is designed for industrial surface-maintenance applications where operators need controlled, localized heating on flat or curved steel surfaces. For pipeline applications, see our dedicated induction coating removal solution.
Why Induction Heating Is Effective for Coating Removal from Steel
Steel is particularly suitable for induction-based coating removal because it responds efficiently to alternating electromagnetic fields.
The important engineering advantage is that energy does not need to pass through the full coating thickness before the substrate starts heating. Energy is generated directly in the conductive steel.
Heat then travels toward the steel/coating interface, where disbonding needs to occur.
This makes the process fundamentally different from external flame heating, hot-air heating or infrared heating, in which thermal energy must first pass through the outside of the coating.
RPR Heat Induction coating removal is therefore particularly useful for industrial coating systems that are strongly bonded to carbon-steel substrates.
What Coatings Can Be Removed from Steel by Induction Heating?
The suitability of induction disbonding depends on coating chemistry, coating thickness, steel thickness, geometry and required productivity. Typical industrial applications include:
- Industrial paint
- Epoxy coatings
- Coal-tar epoxy
- Fusion-bonded epoxy coatings
- Polyethylene coatings
- Pipeline protective coatings
- Rubber linings
- Anti-skid coatings
- Fiberglass-reinforced coating systems
- Intumescent coatings
- Passive fire protection coatings
- Corrosion-protection coatings
- Marine protective coatings
- Heavy-duty industrial coatings
Because different coating formulations soften, expand and disbond at different temperatures, a representative sample test is recommended when the coating composition or bonding behavior is unknown.
Induction Paint Removal from Steel
Induction paint removal is one of the primary applications of electromagnetic coating disbonding.
When the induction heating head moves across painted carbon steel, heat is generated directly underneath the paint layer. Instead of grinding through every layer of paint, the process aims to weaken adhesion at the metal interface.
The loosened coating can then be mechanically removed.
This approach is particularly attractive for:
- Large steel plates
- Pipelines
- Storage tanks
- Ship structures
- Offshore platforms
- Bridge steelwork
- Industrial vessels
- Heavy machinery
- Localized repair areas
Epoxy Coating Removal from Steel by Induction Heating
Industrial epoxy coatings are widely used because of their strong adhesion and corrosion resistance. These same characteristics can make maintenance removal difficult.
With induction epoxy coating removal, the objective is not to melt or burn the complete epoxy layer. Instead, the steel beneath the epoxy is heated until the bonding condition at the interface changes sufficiently for mechanical separation.
The ideal process window depends on:
- Epoxy formulation
- Coating thickness
- Steel grade
- Steel thickness
- Coil geometry
- Heating-head stand-off distance
- Generator power
- Travel speed
- Required production rate
Correct coordination of these parameters is more important than simply applying maximum heating power.
Pipeline Coating Removal with Induction Heating
Oil, gas and industrial pipelines frequently require localized coating removal before inspection, repair, welding, recoating or rehabilitation.
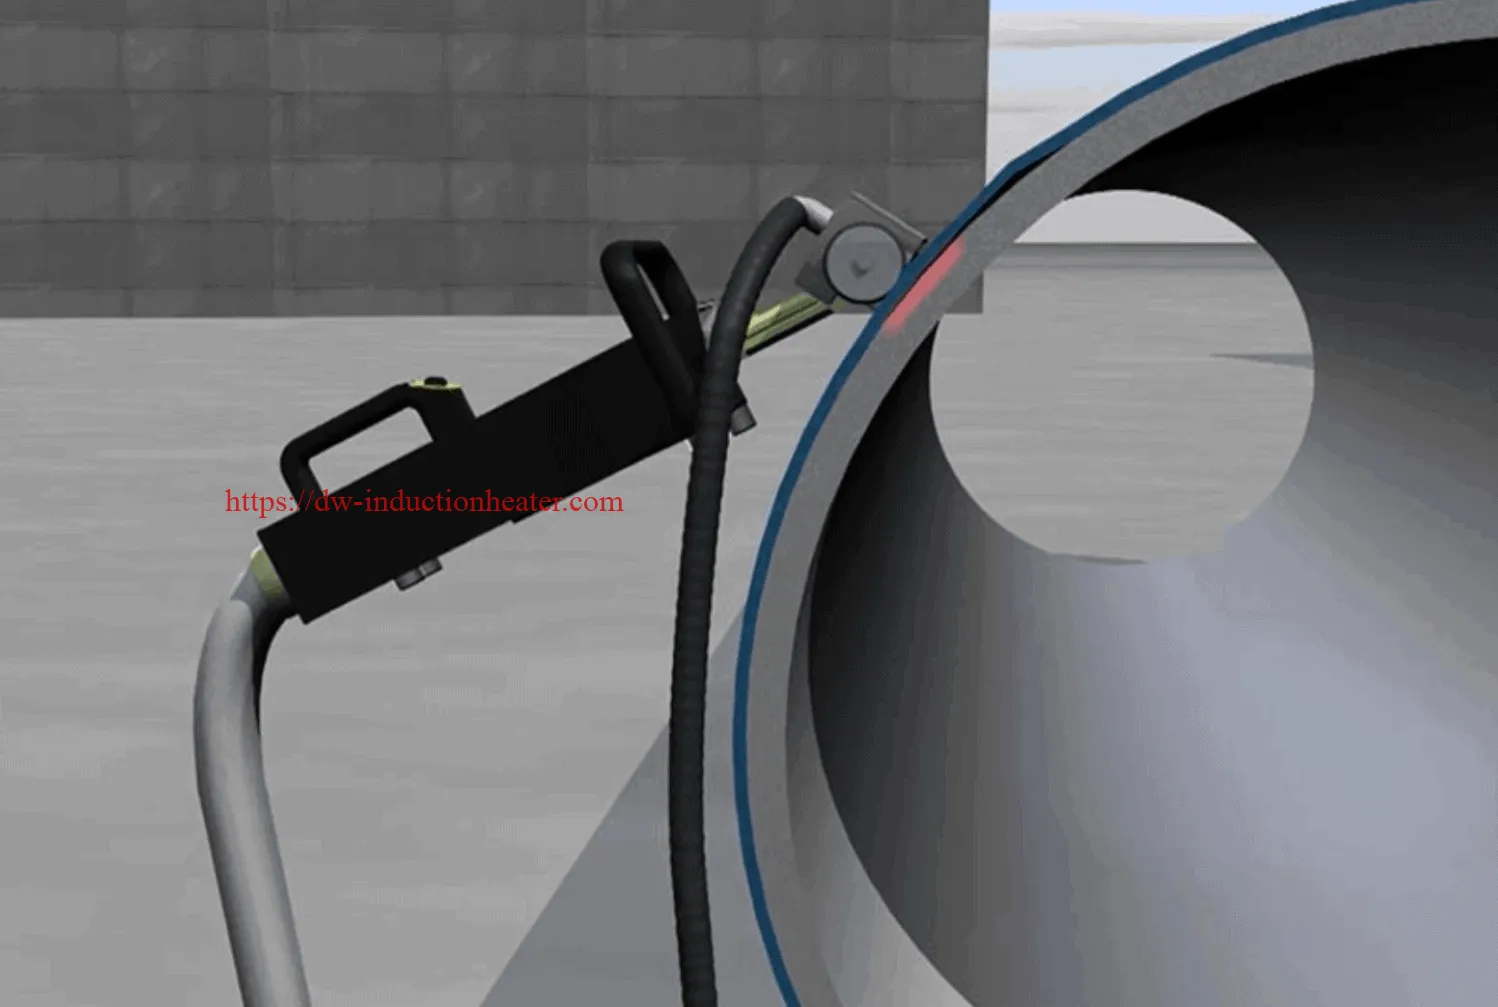
Pipeline surfaces introduce an additional design consideration: curvature.
The induction heating coil and heating-head geometry should be designed to maintain appropriate electromagnetic coupling across the required working width of the curved pipe surface.
Typical pipeline applications include:
- Pipeline coating cutback
- Weld-zone preparation
- Repair-zone coating removal
- External corrosion inspection
- Pipeline rehabilitation
- Epoxy coating removal
- Polyethylene coating removal
- Rubber coating removal
- Localized recoating preparation
3LPE Pipeline Coating Removal
Three-layer polyethylene, commonly known as 3LPE, typically combines multiple functional layers and can be more difficult to remove than a conventional single-layer paint system.
Induction heating can be used to introduce heat through the underlying steel rather than relying solely on heating the polyethylene from its external surface.
For a 3LPE pipeline application, the process should be evaluated according to:
| Engineering Parameter | Why It Matters |
|---|---|
| Pipe outside diameter | Determines heating-head curvature and effective coverage. |
| Pipe wall thickness | Affects thermal mass and heating response. |
| Total coating thickness | Influences heat transfer and removal behavior. |
| Coating construction | Different adhesive and polymer layers respond differently to heating. |
| Required stripping width | Determines coil and heating-head dimensions. |
| Removal speed | Affects required generator power and scanning strategy. |
| Pipeline condition | Corrosion, scale and previous repairs can affect heat transfer and removal. |
Rubber Lining Removal from Steel
Bonded rubber linings are frequently found inside or outside steel tanks, vessels, pipes and mining equipment.
Mechanical rubber removal can be labor intensive because both the rubber and adhesive system may resist cutting or grinding.
When technically suitable, induction heating generates heat in the steel beneath the rubber lining. This can weaken the adhesive interface and make the rubber easier to separate from the substrate.
Rubber thickness, adhesive chemistry and substrate geometry vary significantly, so a sample test is recommended before establishing final production parameters.
Applications of Induction Coating Removal Systems
Oil & Gas Pipelines
Induction disbonding can be used during pipeline inspection, field-joint repair, coating rehabilitation and localized maintenance.
Storage Tanks
Large carbon-steel storage tanks can contain multiple layers of protective paint, epoxy or lining materials. A mobile induction heating head allows localized treatment of selected areas.
Marine and Shipbuilding
Steel decks, structural sections and selected coated marine components may be treated using controlled induction heating where substrate geometry and coating construction are suitable.
Offshore Structures
Induction coating removal can support maintenance of coated steel components on offshore platforms and associated oil-and-gas infrastructure.
Structural Steel
Beams, columns, plates and fabricated steel components can be treated without relying entirely on aggressive mechanical coating-removal processes.
Mining Equipment
Selected rubber-lined and heavily coated steel components used in mining and mineral-processing equipment can also be evaluated for induction-assisted disbonding.
Induction Coating Removal vs. Abrasive Blasting
| Comparison | Induction Coating Removal | Abrasive Blasting |
|---|---|---|
| Primary mechanism | Thermal disbonding at the steel/coating interface | Mechanical impact and abrasion |
| Energy application | Heat generated directly in conductive steel | Abrasive particles impact the outer coating surface |
| Abrasive media | Not required for the induction-disbonding stage | Normally required |
| Coating waste | Coating may separate in flakes, strips or larger sections | Waste normally includes removed coating and spent abrasive |
| Dust during bulk removal | Generally lower during the induction-disbonding stage | Dust control and containment are often required |
| Localized removal | Well suited to controlled local treatment | Possible with appropriate blasting control |
| Surface profile creation | Not the primary function | Can create a specified abrasive-blast profile |
| Suitable substrates | Conductive metals, particularly steel for this application | Broad range of suitable substrates |
Engineering note: Coating removal and final surface preparation are not always the same operation. Induction heating may efficiently remove the bulk coating, while the new coating specification may still require light abrasive blasting, power-tool cleaning or another preparation process to achieve the required surface cleanliness and anchor profile.
Induction Coating Removal vs. Grinding and Mechanical Stripping
Grinding attacks the coating mechanically from the outside. For thick industrial coatings, this can require considerable tool contact and can generate substantial coating fragments and dust.
Induction disbonding takes a different approach: it targets the bonding interface underneath the coating.
This makes induction particularly interesting for applications in which the coating can be separated in relatively large sections after adhesion has been weakened.
The two methods can also be combined. Induction can remove the majority of the coating, while mechanical tools are subsequently used for localized residues or final preparation.
Induction Coating Removal vs. Water Jetting
High-pressure and ultra-high-pressure water jetting use water energy to break and remove coatings from the substrate.
Induction coating removal does not rely on high-pressure water for the disbonding stage. This can be advantageous where managing large quantities of process water is undesirable.
However, the correct process should always be selected according to coating type, substrate condition, required final cleanliness, site restrictions and project specifications.
Key Advantages of Induction Coating Removal from Steel
- Direct substrate heating: Electromagnetic energy generates heat in the conductive steel beneath the coating.
- Localized energy delivery: Heating can be concentrated in the area being treated.
- Non-contact electromagnetic heating: An open flame is not required to generate heat in the steel.
- No abrasive media during disbonding: Bulk coating removal can be performed without introducing blasting media into the process.
- Reduced secondary abrasive waste: Removed material is not automatically mixed with large volumes of spent blast media.
- Flat or curved components: Heating heads can be designed for steel plates, tanks and pipelines.
- Adjustable process parameters: Generator output, travel speed, coil geometry and working distance can be optimized for the application.
- Suitable for industrial maintenance: The process can be applied to localized coating-repair areas as well as larger surfaces.
The Induction Heating Principle Behind Coating Disbonding
The underlying physics are based on Induction heating.
Alternating electrical current passes through an induction coil and creates an alternating magnetic field. When conductive steel enters the magnetic field, electrical currents are induced within the material.
The electrical resistance of the steel converts part of this current into thermal energy.
For conventional induction hardening or forging, the objective may be to raise the workpiece itself to a specific processing temperature.
For coating removal, the objective is different: sufficient localized heat is generated near the steel surface to modify the bonding condition at the steel/coating interface.
Therefore, successful coating removal depends on controlling the thermal interface rather than simply maximizing steel temperature.
Critical Process Parameters for Induction Coating Removal
| Parameter | Effect on the Process | Engineering Consideration |
|---|---|---|
| Generator power | Controls available heating capacity | Should match steel thickness, working width and required production rate |
| Frequency | Influences electromagnetic penetration and coupling | Selected as part of the complete generator/coil design |
| Coil geometry | Determines heating pattern | Must match flat, cylindrical or irregular workpiece geometry |
| Coil-to-steel distance | Affects coupling efficiency | Should remain reasonably consistent during scanning |
| Travel speed | Controls energy delivered per unit area | Too fast may cause incomplete disbonding; unnecessary dwell increases heat input |
| Steel thickness | Changes thermal mass | Thicker steel generally requires a different power/time strategy |
| Coating thickness | Affects heat transfer and peeling behavior | Thick multi-layer coatings should be tested before production |
| Interface temperature | Strongly affects adhesion | The optimum window depends on the coating and adhesive system |
Why Coil and Heating-Head Design Matters
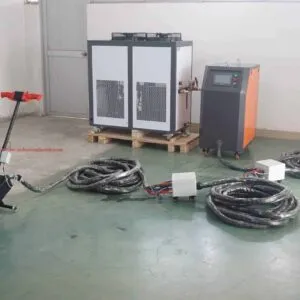
The power supply is only one part of an induction coating-removal system.
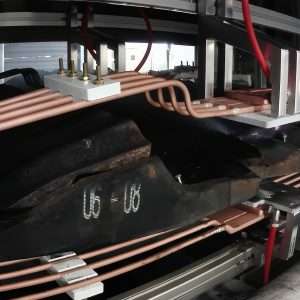
The heating head determines how effectively electromagnetic energy is coupled into the steel. A heating head designed for a flat plate may not provide the same field distribution when used on a small-diameter pipeline.
Important coil-design factors include:
- Effective heating width
- Pipe curvature
- Coil stand-off
- Power density
- Cooling-water flow
- Workpiece accessibility
- Operator movement
- Required stripping pattern
For this reason, customized heating heads may be required when moving from flat steel structures to pipelines, tanks or irregular components.
Typical Induction Coating Removal Process
- Identify the substrate material.
- Determine steel thickness.
- Identify the coating material and coating system.
- Measure the coating thickness.
- Select the appropriate generator and heating-head configuration.
- Establish an initial power level and scanning speed.
- Perform a sample test area.
- Confirm that the coating is disbonding without unnecessary overheating.
- Move the heating head over the working area at a controlled speed.
- Lift or scrape the loosened coating.
- Inspect the exposed steel.
- Perform additional surface preparation if required by the recoating specification.
How to Select an Induction Coating Removal Machine
Before selecting an induction coating removal machine, provide the following information:
- Steel material: carbon steel, alloy steel or other substrate
- Steel thickness: mm
- Coating type: epoxy, paint, rubber, polyethylene, PFP, etc.
- Coating thickness: mm
- Workpiece geometry: plate, pipe, tank, vessel or irregular structure
- Pipe outside diameter: when applicable
- Required stripping width: mm
- Required productivity: m²/h or linear m/h
- Available electrical supply: voltage, frequency and phase
- Required cable length: distance between power source and working area
- Operating environment: workshop, pipeline field, shipyard, tank farm, offshore, etc.
These parameters allow the induction power supply, heating-head dimensions, coil geometry and operating strategy to be selected more accurately.
Where Induction Coating Removal Is Most Useful
The technology is particularly attractive when the project involves one or more of the following conditions:
- Thick industrial coatings bonded strongly to steel
- Large steel assets requiring maintenance
- Localized coating removal around repair zones
- Pipeline coating cutbacks
- Projects seeking to reduce abrasive-media consumption
- Areas where controlling dust is important
- Applications requiring controlled local heating
- Coatings that can be separated in sheets or large fragments after disbonding
Important Limitation: Coating Removal Is Not Always Final Surface Preparation
One of the most important engineering distinctions is the difference between removing a coating and preparing steel for a new coating.
An induction coating-removal system is primarily designed to disbond and remove the existing coating.
A new protective coating specification may additionally require:
- A specified steel cleanliness grade
- A specified anchor profile
- Removal of corrosion products
- Removal of remaining primer
- Salt-contamination testing
- Dust testing
- Oil and grease removal
Therefore, induction coating removal can form the first major stage of a complete surface-preparation process rather than automatically replacing every subsequent preparation operation.
Recommended Workflow for Steel Recoating Projects
| Stage | Operation | Objective |
|---|---|---|
| 1 | Induction heating | Reduce coating-to-steel adhesion |
| 2 | Scraping / peeling | Remove the bulk coating |
| 3 | Steel inspection | Check corrosion, pitting and remaining coating |
| 4 | Secondary preparation if required | Achieve specified cleanliness and surface profile |
| 5 | Surface verification | Confirm readiness for recoating |
| 6 | New coating application | Restore corrosion protection |
Frequently Asked Questions About Induction Coating Removal from Steel
What is induction coating removal?
Induction coating removal is a thermal disbonding process that uses electromagnetic induction to generate heat in a conductive steel substrate. The heat weakens the coating-to-steel bond so that the coating can be mechanically removed.
Can induction heating remove paint from steel?
Yes. Paint and protective coating removal from carbon steel is one of the principal applications of induction disbonding technology. Actual operating conditions depend on the coating composition, thickness and steel geometry.
Can induction heating remove epoxy coating?
Many industrial epoxy coatings on steel can be evaluated for induction removal. The steel is heated beneath the epoxy, helping reduce adhesion at the interface.
Can induction heating remove rubber lining?
It can be suitable for some bonded rubber linings on conductive steel substrates. Rubber thickness, adhesive chemistry and steel thickness should be evaluated before selecting operating parameters.
Can an induction coating removal system be used on pipelines?
Yes. Pipeline coating removal is an important application. The heating-head curvature and working width should be matched to the pipe outside diameter.
Can induction heating remove 3LPE pipeline coating?
Induction heating can be applied to selected 3LPE removal applications by generating heat in the underlying steel. Because 3LPE is a multi-layer system, a representative test is recommended before defining the final process.
Does induction coating removal require abrasive media?
No abrasive media is required for the electromagnetic heating and thermal-disbonding stage itself. However, additional abrasive or mechanical surface preparation may still be required when the subsequent coating specification demands a defined cleanliness grade or anchor profile.
Does induction coating removal work on curved steel surfaces?
Yes. The heating head and induction coil can be designed for curved structures such as pipelines and tanks. Correct coil geometry is important for maintaining consistent coupling.
Does induction coating removal damage the steel?
The process is designed to provide controlled localized heating. Appropriate generator output, coil design, scanning speed and temperature control should be established for the steel grade, thickness and application.
What determines coating removal speed?
Removal speed is influenced by generator power, heating width, steel thickness, coating type, coating thickness, adhesion strength, coil coupling, scanning speed and mechanical removal efficiency.
What information should I provide for equipment selection?
Provide the steel material and thickness, coating material and thickness, workpiece dimensions, pipe diameter if applicable, required stripping width, required production rate, available electrical supply, cable length and photos of the actual application.
RPR Induction Coating Removal System for Industrial Steel Maintenance
HLQ induction coating removal systems are designed for industrial applications involving paint, epoxy, rubber, pipeline coatings and other bonded protective materials on steel substrates.
For a new project, the most reliable equipment-selection method is to evaluate the entire application rather than selecting generator power based only on coating thickness.
The combination of generator power + induction coil design + heating-head geometry + steel thickness + coating system + scanning speed determines the final coating-disbonding performance.