


Induction Brazing Brass Tube to Brass Disk
High Frequency Induction Brazing Brass Tube to Brass Disk Applications
Quick Answer: How Does Induction Brazing Join a Brass Tube to a Brass Disk?

Induction brazing brass tube to brass disk uses a high-frequency electromagnetic field to rapidly and uniformly heat the joint area until the brazing alloy melts and flows around the interface by capillary action.

Objective
Customer needs to silver solder a brass stem to a brass monument marker.
– Uses Silver Solder for Brazing Alloy, with Stay Silv flux
– Current process uses a torch, which takes 2-3 minutes per piece.
Equipment
DW-HF-15kw induction brazing heater
Materials
• Sample materials are both brass. Center tube – .500” (12.7mm) OD (0.0605” (1.537mm) wall thickness) x 2.9/3” (73.66mm) high
• Marker plate – 3.6” (91.44mm) OD x 0.125” (3.175mm) thick (nominal) slightly concave.
• Alloy – Sil Fos rod- 0.125” (3.175mm) x 0.050” (1.27mm)
• Flux
Key Parameters
Temperature: 1475-1500°F (801-815°C)
Power: 5 kW
Time: 45 seconds

Proces of induction brazing:
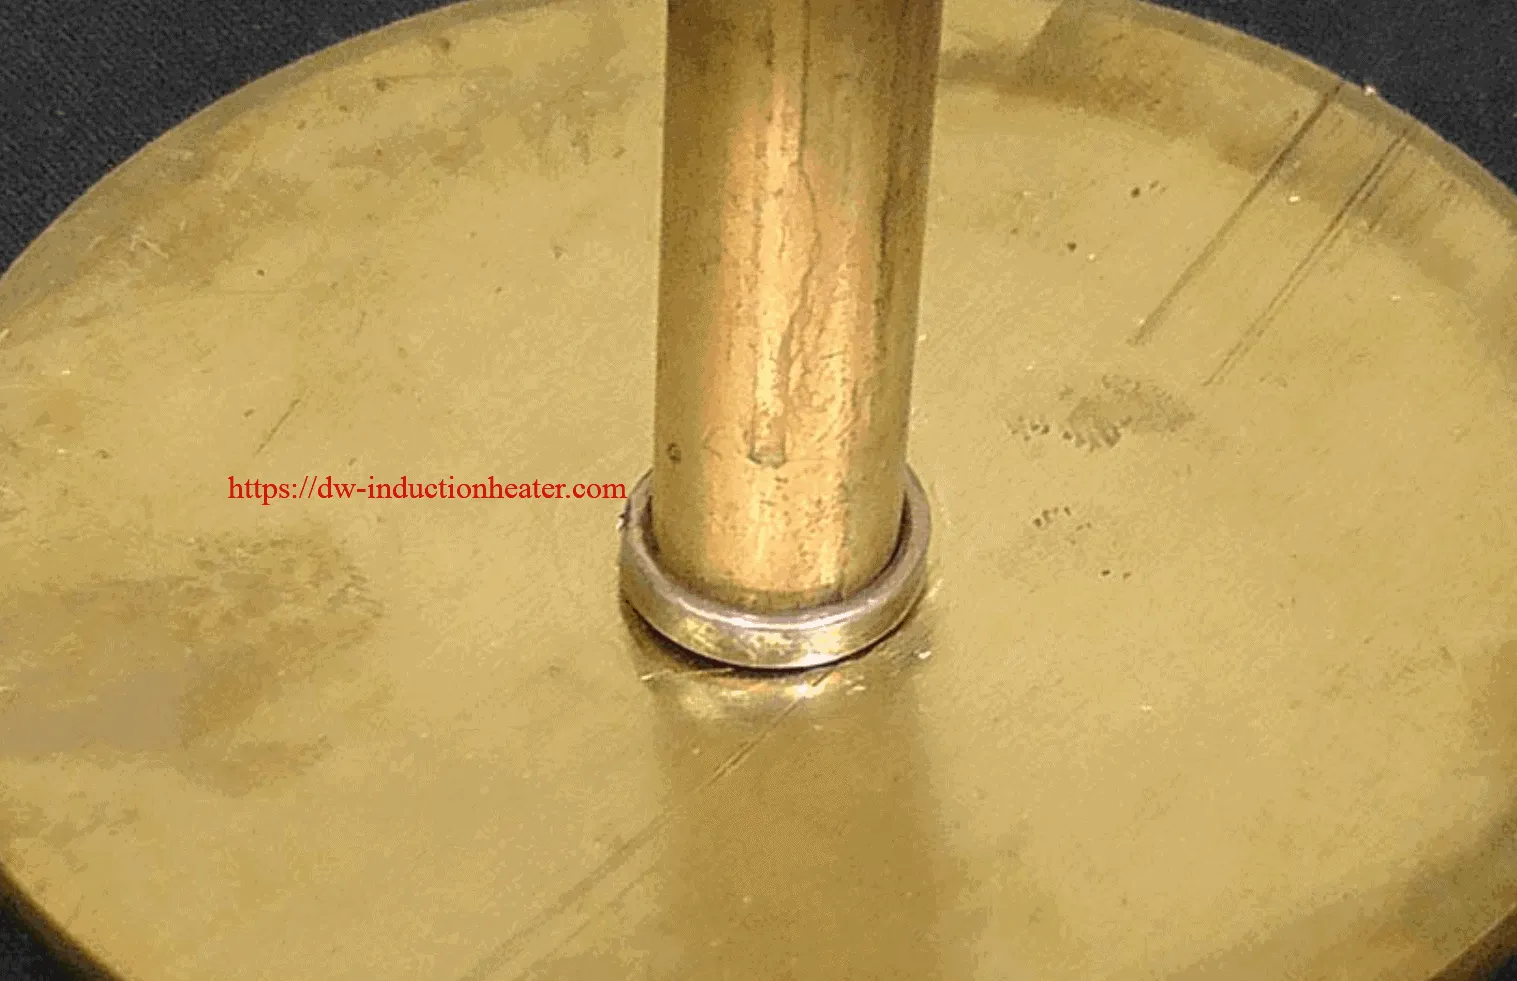
- To demonstrate elimination of “hand feeding” the alloy (common practice when torch brazing), we formed the customer’s alloy into a ring to tightly fit over the center post tube. This method affords several benefits in production operations: (a) Alloy in pre-formed rings provides a uniform amount for each cycle, resulting in uniform joints and wetting (b) operator control is replaces with uniform alloy rings – operators need no particular skills as with torch brazing. Pre-form alloy rings can be provided by the alloy supplier to tightly fit the tube OD.
- We fluxed the tube and mating area on the marker plate with the provided Stay Silv whit flux and moved the pre-formed alloy ring to the bottom of the tube to make contact both with the tube and the marker based at their interface position.
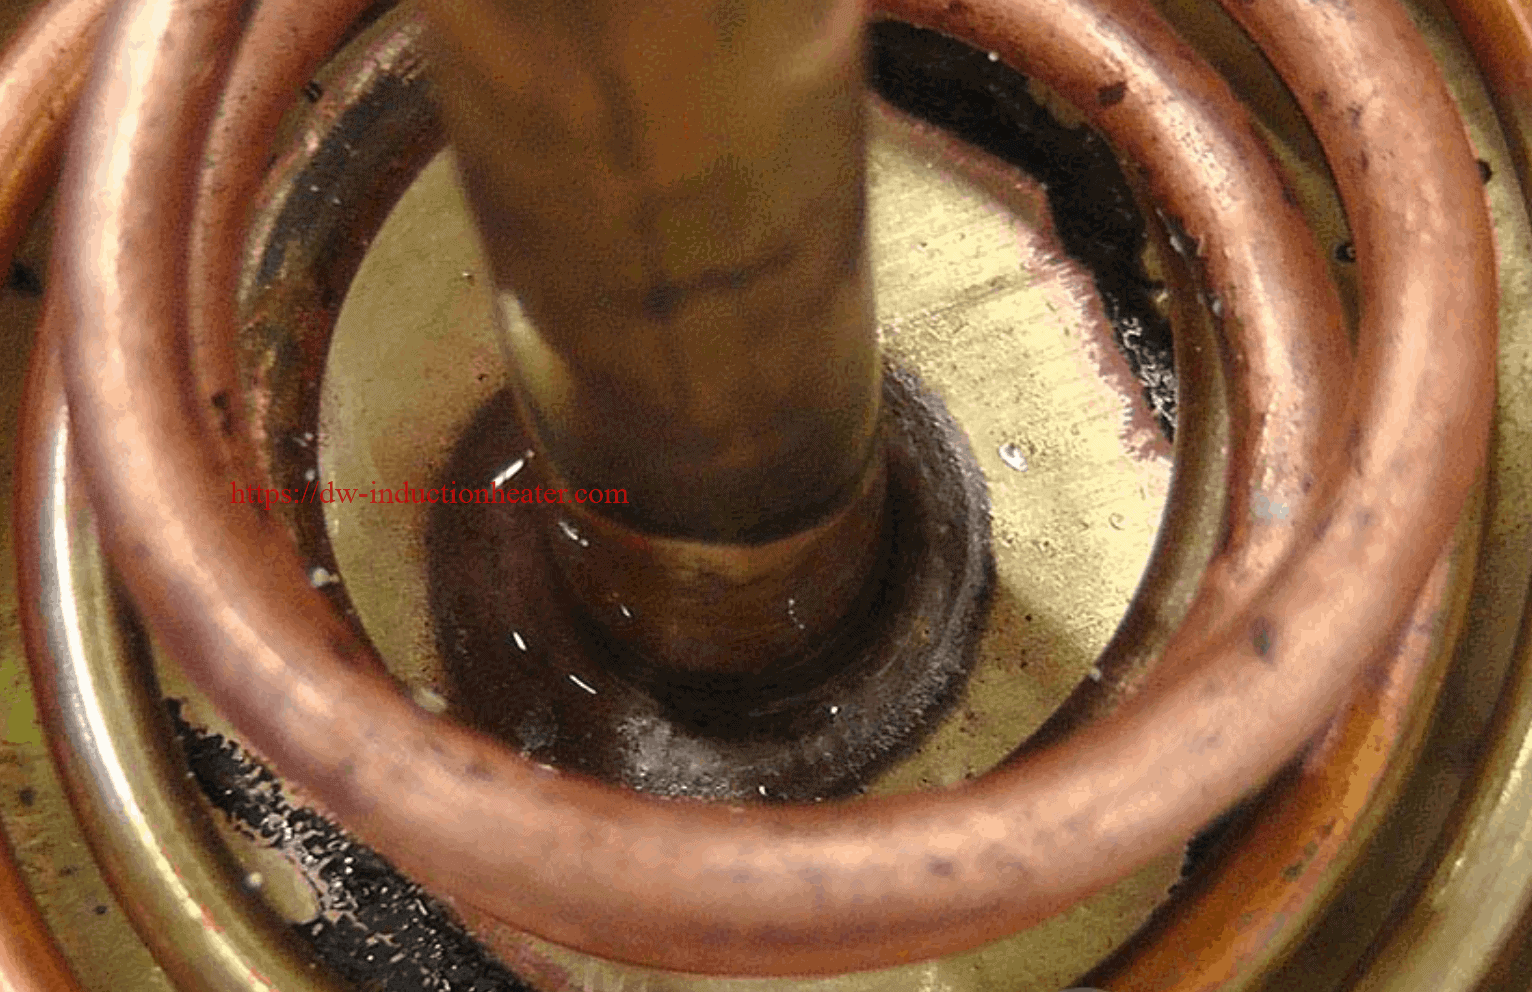
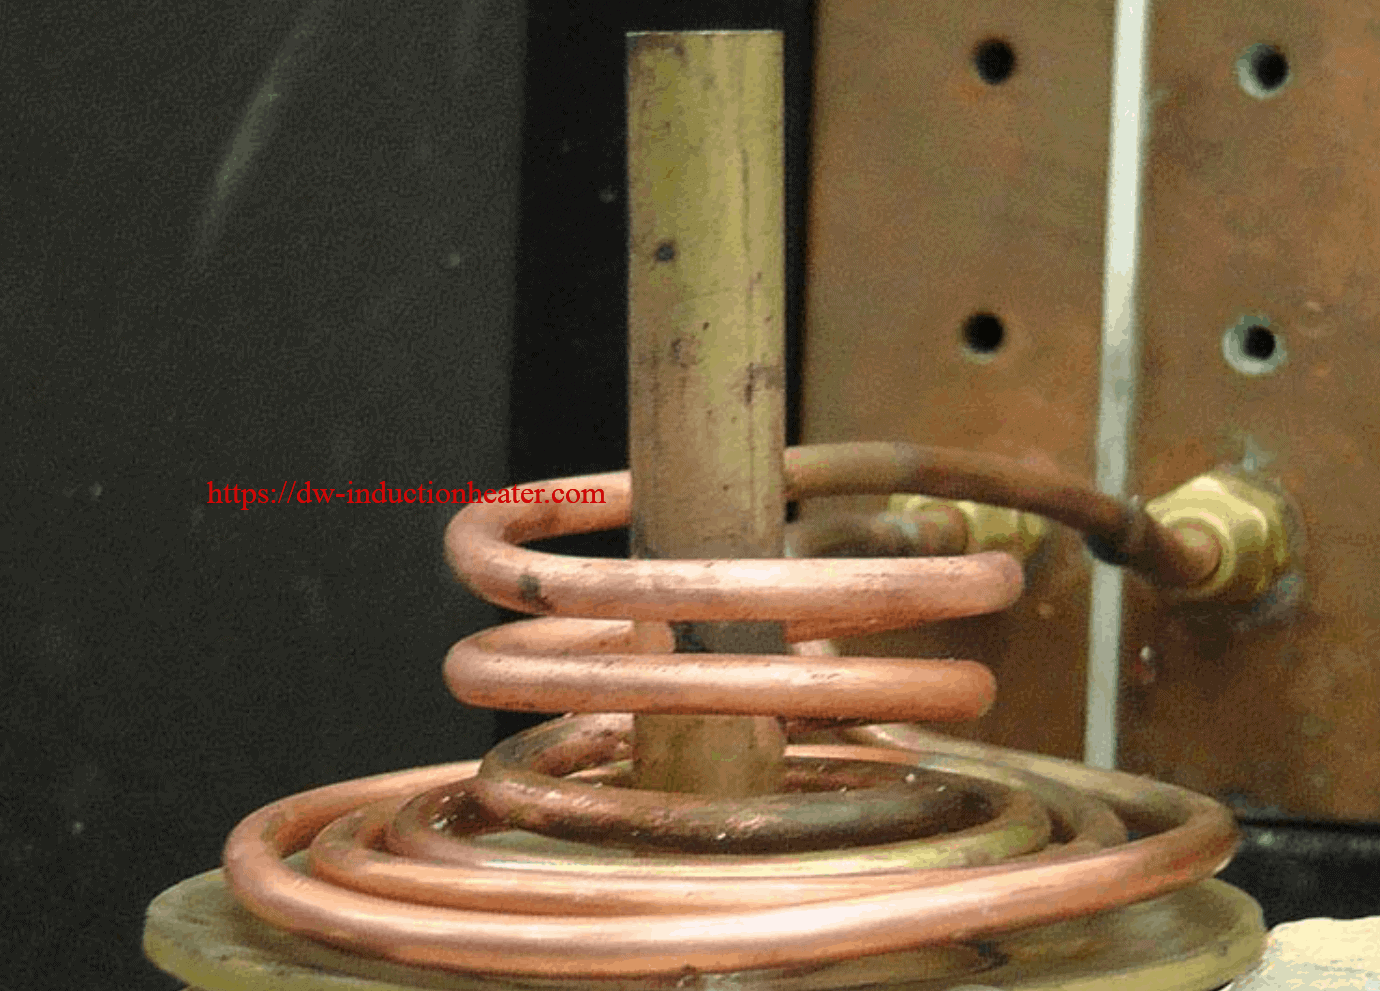
- A dual section/diameter coil was designed to uniformly heat the tube and plate to approximately 1500 0F at the interface of the parts – once temperature was to flow the alloy was reached, the pre-formed rings flowed around the tube and marker plated forming a complete braze filet. The apply was permitted to solidify, then the assembly was lowered out of the coil and subjected to a water bath to remove the residual flux residue.

Benefits of induction brazing:
- Precise control of the time and temperature
- Power on demand with rapid heat cycles
- Repeatable process, not operator dependent
- Safe heating with no open flames
- Energy efficient heating


FAQs About Induction Brazing Brass Tube to Brass Disk
1. Can brass be brazed using induction heating?
Yes. Brass is well suited to induction brazing when the correct induction frequency, coil geometry, brazing alloy and flux are selected.
The electromagnetic field heats the brass components rapidly around the joint, allowing the brazing alloy to melt and flow between the mating surfaces.
2. What temperature is required to induction braze brass?
The required brazing temperature depends mainly on the selected filler metal.
For this brass tube-to-disk application, the joint was heated to approximately 1475–1500°F (801–815°C).
The production temperature should always be matched to the brazing alloy, flux and brass grade being used.
3. How long does induction brazing brass take?
Heating time depends on component size, joint mass, induction power, frequency and coil design.
In this application, approximately 45 seconds was required to heat the brass tube and disk to brazing temperature and obtain complete filler-metal flow around the joint.
Higher power or optimized coil geometry may reduce the cycle time for suitable production applications.
4. What size induction brazing machine is suitable for brass components?
The required power depends on:
- Brass component dimensions
- Total heated mass
- Required cycle time
- Brazing temperature
- Joint geometry
- Production rate
- Coil-to-workpiece coupling
For this application, an HLQ DW-HF-15kW induction brazing heater was used, with approximately 5 kW of applied power during the brazing test.
5. Why use a preformed brazing alloy ring?
A preformed brazing ring provides a controlled quantity of filler metal around every joint.
This offers several advantages for production brazing, including more consistent filler-metal volume, more uniform fillet formation, reduced operator dependence and easier automation.
Once the joint reaches the correct temperature, the ring melts and flows around the brass tube-to-disk interface by capillary action.
6. What type of induction coil is used for brazing a brass tube to a brass disk?
A custom dual-section or dual-diameter induction coil can be used to balance heating between the relatively thin brass tube and the larger brass disk.
The exact coil shape depends on tube diameter, disk diameter, joint location, heating time and access around the workpiece.
Proper coil design is one of the most important factors for achieving uniform brazing temperature.
7. Is induction brazing better than torch brazing for brass parts?
For repetitive industrial production, induction brazing offers important advantages over manual torch brazing.
It provides controlled heating time, localized energy, programmable power, consistent joint quality and no direct flame. It also reduces dependence on individual operator brazing technique.
Torch brazing may still be practical for repair work or very low-volume production, while induction brazing is particularly attractive for repeatable manufacturing.
8. Can brass induction brazing be automated?
Yes. Brass tube-to-disk induction brazing can be integrated into semi-automatic or fully automatic manufacturing systems.
An automated system may include:
- PLC-controlled heating cycles
- Automatic workpiece loading
- Pneumatic or servo fixtures
- Automatic brazing-ring placement
- Temperature monitoring
- Robotic handling
- Automatic cooling
- Multi-station indexing tables
This makes induction brazing suitable for high-volume production of brass fittings, valves, hardware and other assemblies.