


induction preheating aluminum wheels for spray painting
induction preheating aluminum wheels for spray painting
Quick answer: Induction preheating heats a 22-inch aluminum wheel to 275 ºF (135 ºC) in about 30 seconds before spray painting or powder coating. The setup is a DW-MF-70kW medium frequency induction heater running at 8 kHz with a custom multi-turn helical/pancake coil. After the power is switched off, the wheel stays at or above 150 ºF (65 ºC) for 108 seconds. That gives the paint line almost two minutes to move the wheel to the spray booth and coat it at the right temperature.
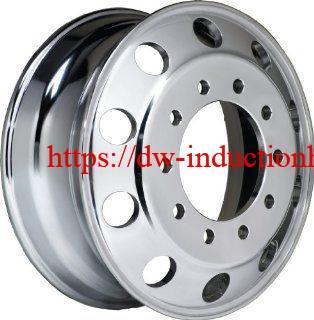
Application Summary
| Parameter | Value |
|---|---|
| Workpiece | 22″ cast aluminum automotive wheel (customer-supplied parts) |
| Process | Induction preheating before spray painting / coating |
| Target temperature | 275 ºF (135 ºC) |
| Heating time | 30 seconds |
| Temperature hold after heating | ≥ 150 ºF (65 ºC) for 108 seconds |
| Frequency | 8 kHz (medium frequency) |
| Induction heater | DW-MF-70kW, 70 kW output |
| Capacitors | Remote workhead, 3 × 27 μF = 81 μF |
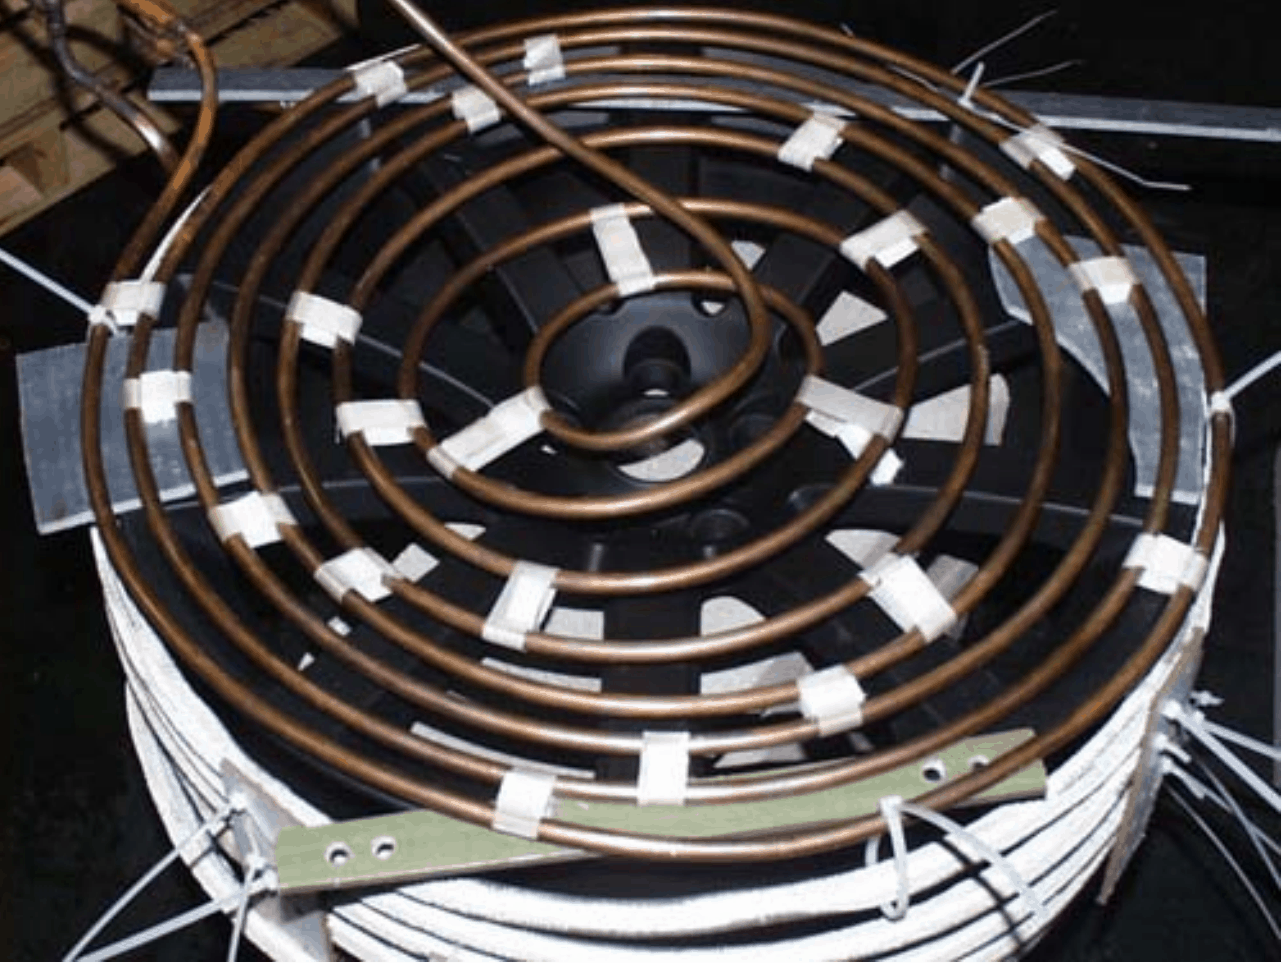
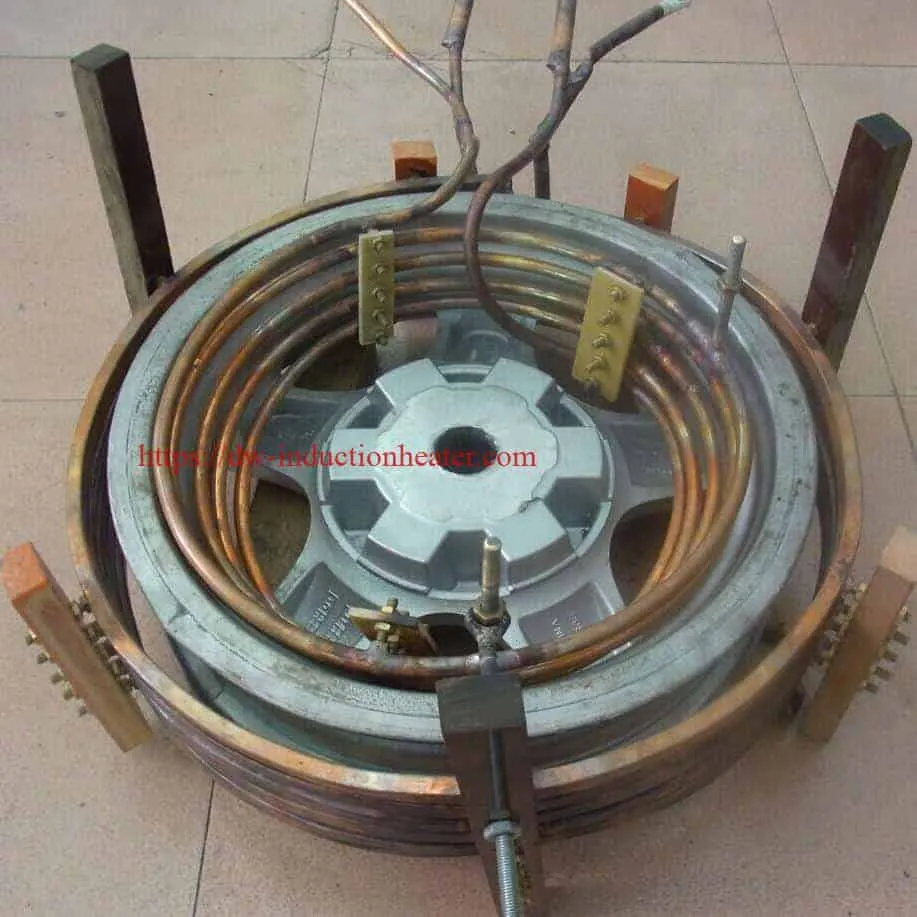
| Induction coil | Custom multi-turn combination helical/pancake coil |
Objective: Why Aluminum Wheels Are Preheated Before Spray Painting
Objective: The paint system needs the aluminum wheel preheated before spraying. It also needs the wheel to stay above a set minimum temperature until the coating is applied. A warm wheel drives off surface moisture, helps the coating flow and wet the surface evenly, and shortens the curing time. If the wheel cools below the target temperature on the way to the spray booth, the coating can adhere poorly, show orange peel, or cure unevenly.
Induction Heating Equipment
Equipment:
- DW-MF-70kW induction heating system, equipped with a remote workhead containing three 27 μF capacitors for a total of 81 μF.
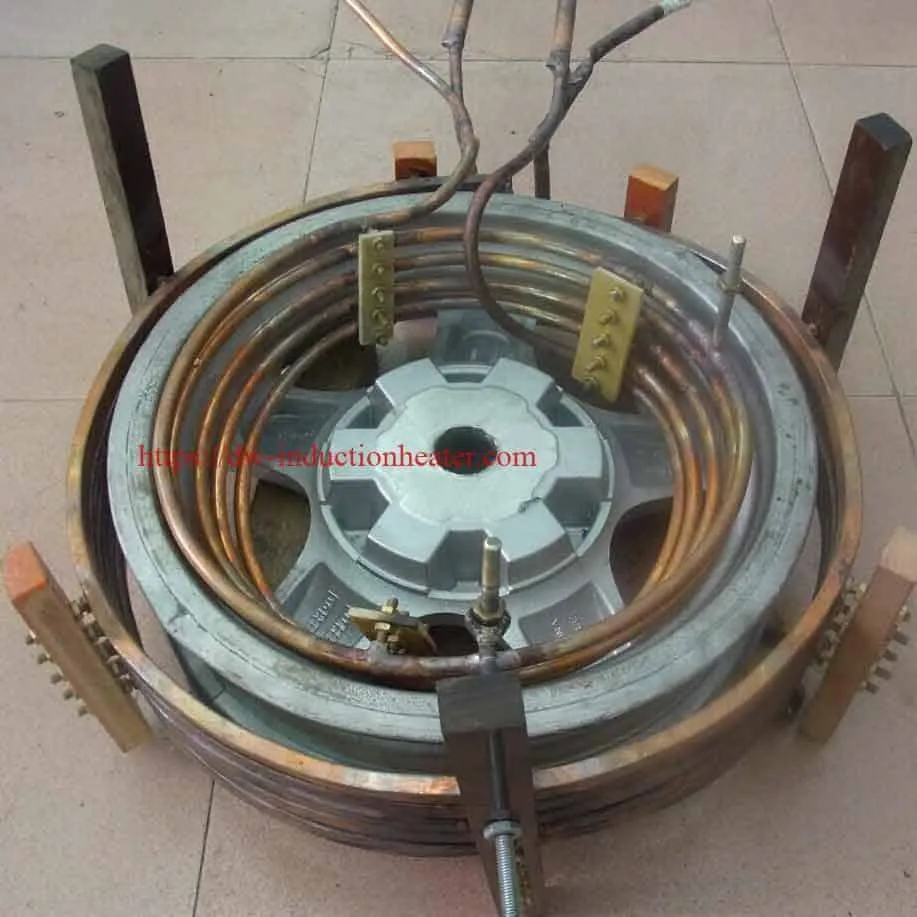
- An induction heating coil designed and developed specifically for this application: a multi-turn combination helical/pancake coil that covers both the wheel rim and the wheel face (spokes).
The 8 kHz frequency was chosen for aluminum. Aluminum is non-magnetic and has low electrical resistivity, so a medium frequency drives eddy currents deep enough into the rim and spokes to heat the whole wheel evenly, not only its outer surface.
Induction Heating Process: Step by Step
- Load: The 22” aluminum wheel is placed inside the combination helical/pancake induction coil.
- Heat: The DW-MF-70kW power supply runs at 8 kHz for 30 seconds and brings the wheel to 275 ºF (135 ºC).
- Hold: When heating stops, the wheel remains at or above 150 ºF for 108 seconds, which meets the target heat requirement.
- Coat: The warm wheel moves to the spray booth and is painted or powder coated within that 108-second window.
Test Results
| Stage | Time | Wheel temperature |
|---|---|---|
| Start of induction heating | 0 s | Ambient |
| End of induction heating | 30 s | 275 ºF (135 ºC) |
| Hold window after power off | up to 108 s | ≥ 150 ºF (65 ºC) |
Result: the heating cycle met the customer’s requirements for both preheat temperature and heat retention.
Results/Benefits
Results/Benefits Induction heating provides:
- Uniform heat distribution over the wheel: The custom coil heats the rim and spokes evenly, so the coating goes onto a surface with a consistent temperature.
- Precise control of heating and pattern: Power, time and temperature are set digitally, so every wheel follows the same cycle.
- Efficiency and reduced energy costs: The wheel itself generates the heat, so there is no need to keep a large preheat oven hot. The heater draws power only while a wheel is in the coil.
- Short cycle time: 30 seconds per wheel, which suits inline painting and powder coating lines.
- Small footprint and clean process: No flame and no combustion gases, and the heater takes much less floor space than a convection oven.
Induction Preheating vs. Convection Oven Preheating
| Item | Induction preheating | Convection / gas oven |
|---|---|---|
| Heating time per wheel | About 30 seconds | Usually several minutes or longer |
| Energy use | Only while a wheel is in the coil | Oven chamber and air must stay hot continuously |
| Temperature control | Precise and repeatable, set by power and time | Depends on airflow and oven load |
| Startup | Instant on/off | Long warm-up time |
| Floor space | Compact coil station | Large oven or tunnel |
Typical Applications
- Preheating aluminum alloy wheels before spray painting, powder coating or clear coating
- Preheating wheels before paint refinishing and wheel repair
- Preheating other aluminum parts before coating, bonding or curing
FAQ
What temperature should aluminum wheels be preheated to before painting?
In this application the wheel is preheated to 275 ºF (135 ºC) and must stay at or above 150 ºF (65 ºC) until it is sprayed. The right target depends on the coating supplier’s specification.
How long does it take to induction preheat a 22-inch aluminum wheel?
About 30 seconds with a DW-MF-70kW induction heater at 8 kHz and a custom helical/pancake coil.
Can induction heating be used on aluminum, which is non-magnetic?
Yes. Induction heating works on any electrically conductive metal. Aluminum heats through eddy currents only, with no magnetic hysteresis losses, so a suitable frequency (here 8 kHz) and a well-matched coil are the keys to efficient heating.
How long does the wheel stay hot after induction heating?
After heating stops, the 22″ wheel stays at or above 150 ºF for 108 seconds, which is enough time to move it to the spray booth.
Which induction heater is recommended for aluminum wheel preheating?
This project used the DW-MF-70kW medium frequency induction heating system with a remote workhead (81 μF capacitance). Wheel size, cycle time and line speed determine the final power rating and coil design. Send us your wheel size and line requirements for a matched solution.