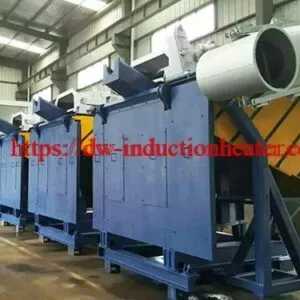
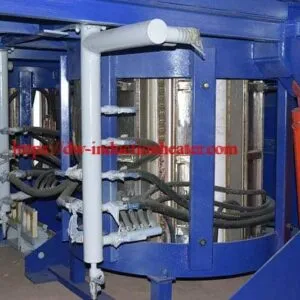
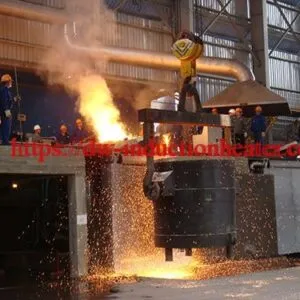
Medium Frequency Steel Melting Furnace
Medium Frequency Steel Melting Furnace — GW Series, 0.35–30 Tonnes at 0.25–1 kHz
An medium frequency steel melting furnace melts steel, iron, stainless steel, copper and aluminium with induction heating and no burner. A medium-frequency power supply drives alternating current through a water-cooled copper coil around a conductive crucible, the coil’s alternating magnetic field induces eddy currents in the charge, and the resistance of the metal turns that current into heat. There is no flame and no combustion gas in contact with the melt, and the same rotating field stirs the bath so temperature and composition are uniform before the pour.
Quick Answer
The medium frequency steel melting furnace is the electric, medium-frequency route into a ferrous melt. A dry, sorted charge of pig iron, steel scrap or foundry returns is melted at constant power output with electromagnetic stirring, the bath is refined and skimmed, the pouring temperature is confirmed, and the steel-shell furnace is tilted hydraulically into a ladle or mould. Frequency is the variable that scales with the job: the published GW series drops from 1 kHz at GW‑0.35T to 0.25 kHz at GW‑20T and GW‑30T as capacity rises, because lower frequency is used for the larger furnaces.
Medium frequency steel melting furnace — the key figures at a glance
| Parameter | Published value |
|---|---|
| Model series | GW, 12 models from GW-0.35T to GW-30T |
| Capacity basis | Equivalent electric arc furnace capacity, 0.35 t to 30 t |
| Rated power | 250 kW – 15,000 kW |
| Intermediate frequency | 0.25 kHz – 1 kHz (1 kHz at GW-0.35T down to 0.25 kHz at GW-20T and GW-30T) |
| Small-capacity family | DW-MF IF series, 15 kW – 160 kW, oscillate frequency 1 kHz – 20 kHz |
| Melting time per batch | 20–45 min (GW-0.35T) to 50–90 min (GW-20T, GW-30T) |
| Energy index, cast iron | 560 kWh/T down to 470 kWh/T |
| Energy index, red copper | 420 kWh/T down to 330 kWh/T |
| Energy index, brass | 390 kWh/T down to 300 kWh/T |
| Energy index, aluminium | 540 kWh/T down to 450 kWh/T |
| In-furnace temperature | Steel 1650 °C · Cast iron 1450 °C · Red copper 1150 °C · Brass 1000 °C · Aluminium 700 °C · Zinc 400 °C |
| Power output behaviour | Constant power output — no operator adjustment through the melt |
| Power factor | Always reaches the highest state (≥ 0.96) |
| Melting time claim | Single furnace melting time can be as fast as under 40 minutes |
| Coil loss | About 25 % of total power |
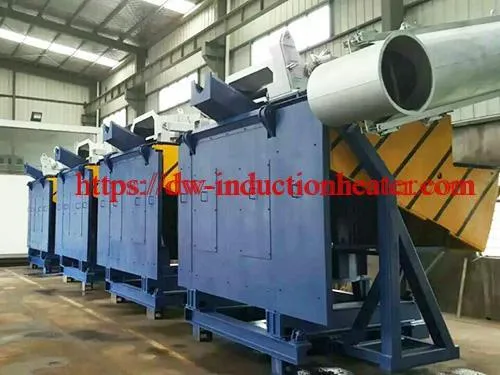
| Furnace body | Steel shell or aluminium shell |
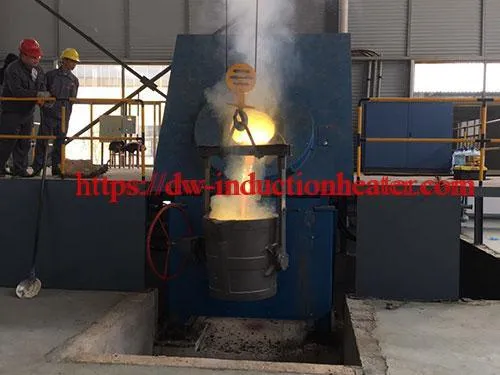
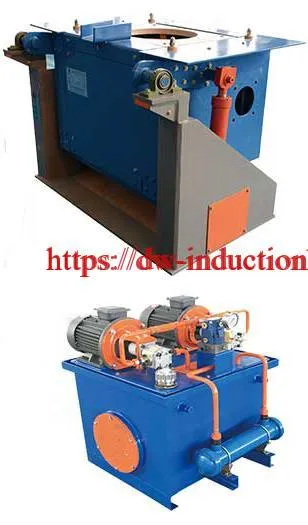
| Tilting | Hydraulic station (or reducer) tilting system |
| Rectifier | Full-wave rectifier power supply series |
| Protection | Over-current, over-voltage, current-limiting, voltage-limiting, water-break and default protection |
| Environmental equipment | Whirlwind and side-suction heat-preservation furnace cover, ring dust hood |
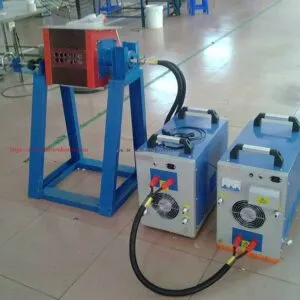
| Equipment configuration | Medium frequency power supply, capacitor cabinet, furnace body, hydraulic tilting system, water cooling cables |
For the rest of the HLQ range see induction heating equipment and the induction melting furnace category.
Table of Contents
- Quick Answer
- Table of Contents
- What is the Medium Frequency Steel Melting Furnace?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages and Limitations
- Why Choose HLQ?
- 6 Core FAQs
What is the Medium Frequency Steel Melting Furnace?
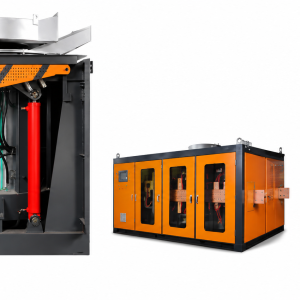
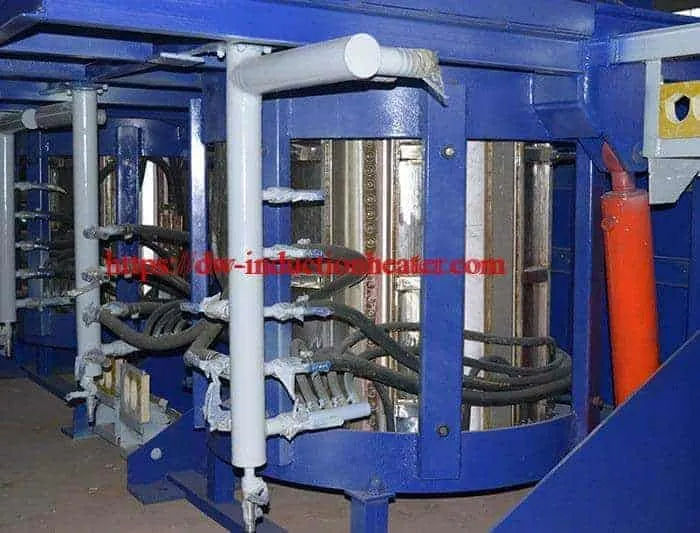
A medium frequency steel melting furnace is a steel-shell, medium-frequency induction melting furnace for ferrous metals. The published description is a medium frequency steel melting furnace with full digital control, constant power output, steel shell construction and hydraulic tilting — and the published supply is electricity, so there is no gas or oil burner anywhere in the specification and no combustion gas in contact with the melt.
Frequency is the design variable that scales with the job. On the published GW series the intermediate frequency falls as capacity rises: 1 kHz at GW‑0.35T, 0.8 kHz at GW‑0.5T and GW‑0.75T, 0.7 kHz at GW‑1T and GW‑1.5T, 0.5 kHz at GW‑2T and GW‑3T, 0.3 kHz at GW‑5T, GW‑10T and GW‑15T, and 0.25 kHz at GW‑20T and GW‑30T. That is the published general rule — lower frequency is used for the larger furnace capacities — and it is why a 30-tonne heat and a 0.35-tonne heat are not the same machine with a bigger lid.
Two further published behaviours matter to the buyer. The medium-frequency power supply delivers constant power output: whatever the furnace condition is doing, the supply keeps delivering maximum power, so from the start of the melt to the end of the batch no operator adjustment is needed. And the induction coil is the biggest single loss in the furnace — the published figure is 25 % of total power — which is why the coil construction is specified in detail: TU1 oxygen-free copper in aluminium, high silver brazing at the joint, and insulation materials between the turns.
Capacity is quoted on the metal’s density. The published basis is the density of steel, 7.8; aluminium is 2.7, so aluminium of equal weight needs the same matched power but a furnace body about three times the size.


Key Applications
Published applications for the HLQ iron and steel melting range:
| Application | Typical material | Recommended furnace configuration | Buyer benefit |
|---|---|---|---|
| Cast iron melting | Gray iron, ductile iron, pig iron, return scrap | Medium frequency induction furnace with a suitable iron lining | Stable molten iron supply for casting production |
| Carbon steel melting | Steel scrap, carbon steel, low-alloy steel | Steel shell induction furnace with hydraulic tilting | Fast melting and good temperature control for steel casting |
| Alloy steel melting | Cr-Mo steel, Mn steel, tool steel, wear-resistant alloy | Temperature-controlled induction furnace | Improves alloy composition uniformity and repeatability |
| Stainless steel melting | 304, 316, stainless scrap, stainless alloy | Medium frequency induction furnace with controlled slag practice | Supports stainless casting and alloy recycling |
| Scrap iron and steel recycling | Clean steel scrap, iron scrap, rejected castings | Hydraulic tilting induction melting furnace | Converts scrap into reusable molten metal |
| Foundry casting | Molten iron or steel for moulds | Steel shell furnace with ladle pouring layout | Improves casting quality and production flexibility |
| Small batch alloy development | Experimental steel or iron alloy | Small or medium induction crucible furnace | Flexible melting for trials and specialty production |
The published usage statement covers melting steel, iron, copper, aluminium and alloy, and lists the properties that make it suitable for all kinds of metal melting: high melting efficiency, good electricity saving effect, good metal component uniformity, less burning loss, speedy temperature rise and easy control of temperature.
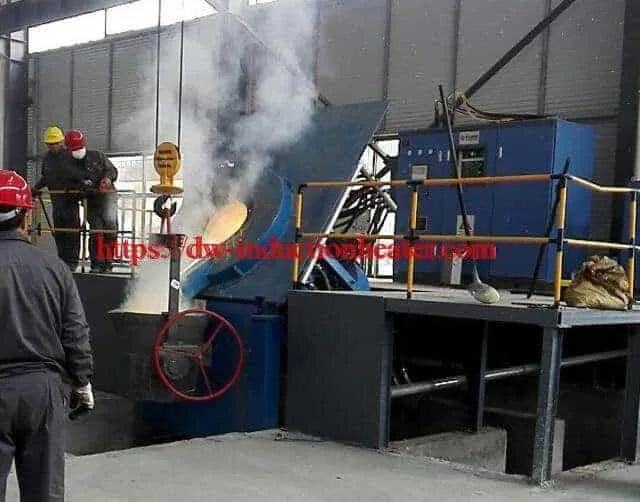

Suitable Materials
Any conductive metal can be melted, but the lining has to match the metal and the slag it will see. The table below lists the ferrous metals published for the HLQ iron and steel melting range, with the operating temperatures and the engineering notes that go with each.
| Material | Melting suitability | Typical melting temperature range | Engineering notes |
|---|---|---|---|
| Gray cast iron | Excellent | About 1150–1400 °C depending on composition | Very common foundry application; charge mix and carbon equivalent should be controlled |
| Ductile iron | Excellent | About 1300–1500 °C | Requires good base iron quality before nodularizing treatment |
| Carbon steel | Excellent | About 1450–1600 °C | Requires high-temperature lining and sufficient power capacity |
| Low-alloy steel | Excellent | About 1450–1650 °C | Alloy loss and final chemistry should be monitored |
| Stainless steel | Good | About 1400–1550 °C | Oxidation and chromium loss should be controlled with correct slag practice |
| High-manganese steel | Good | About 1400–1500 °C | Suitable for wear-resistant casting, but lining compatibility matters |
| Tool steel | Good | About 1450–1600 °C | Requires accurate temperature control and alloy management |
| Scrap iron and steel | Good if clean and dry | Depends on composition | Moisture, sealed cavities, oil and contamination must be removed before charging |
The published in-furnace temperatures for the GW series are steel 1650 °C, cast iron 1450 °C, red copper 1150 °C, brass 1000 °C, aluminium 700 °C and zinc 400 °C. The refractory lining is selected as acidic, neutral or basic according to the metal and the slag chemistry — that choice affects safety, lining life and metal quality.
Working Principle
The heating principle is the same for every furnace in this family. Through the internal rectifier and filter circuit the AC supply is converted into DC power; the control circuit converts that DC power into medium-frequency magnetic energy; the high-speed changing current in the coil produces a high-speed changing magnetic field; the field induces eddy currents inside the crucible; the resistance of the metal converts that current into heat; and the heat passes into the charge until it melts. The rotating field then circulates the bath, and the furnace is tilted hydraulically to pour.
What is published as distinctive about the medium frequency steel melting furnace’s electrical behaviour is the chain behind that sequence. The rectifier is a full-wave series that stays in a state of full open — equivalent to a diode rectifier — so no higher harmonics are produced, there is basically no pollution to the power network, and the substation’s reactive power compensation capacitor is unaffected. The supply holds constant power output whatever the furnace is doing, the power factor always reaches the highest state (≥ 0.96), and a single-furnace melt can be as fast as under 40 minutes.
At medium frequency the coil, the capacitor bank and the supply are one system rather than three separate purchases: the capacitor cabinet provides the reactive compensation and resonance matching that make the frequency stable, the water-cooled cable carries the high current from the power cabinet to the furnace body, and the isolation (exchange) switch lets one furnace be de-energised for overhaul without stopping the others. The background is set out on HLQ’s induction heating principle page.

Technical Specifications
All values below are reproduced from HLQ’s published SMJD induction melting furnace parameter sheet and the Aluminum, Copper, Iron induction melting furnace manual.
1. GW series — power input and rated output
| Type | Rated power (kW) | Incoming voltage (V) | Incoming line current (A) | Rectifying pulse number | Rectifier transformer capacity (kVA) |
|---|---|---|---|---|---|
| GW-0.35T | 250 | 380 | 400 | 6 | Three-phase 315 |
| GW-0.5T | 350 | 380 | 560 | 6 | Three-phase 400 |
| GW-0.75T | 500 | 380 | 800 | 6 | Three-phase 630 |
| GW-1T | 800 | 380 / 750 | 1,280 / 656 | 6 / 6 | Three-phase 1,000 / Three-phase 1,000 |
| GW-1.5T | 1,000 | 380 / 750 | 800 / 820 | 12 / 6 | Double three-phase 1,250 / Three-phase 1,250 |
| GW-2T | 1,400 | 750 / 750 | 1,148 / 574 | 6 / 12 | Three-phase 1,800 / Double three-phase 1,800 |
| GW-3T | 2,000 | 750 | 820 | 12 | Double three-phase 2,500 |
| GW-5T | 3,000 | 950 | 1,140 | 12 | Double three-phase 4,000 |
| GW-10T | 6,000 | 950 | 2,280 | 12 | Double three-phase 8,000 |
| GW-15T | 8,000 | 950 | 1,520 | 24 | Four three-phase 10,000 |
| GW-20T | 10,000 | 950 | 1,900 | 24 | Four three-phase 12,500 |
| GW-30T | 15,000 | 950 | 2,850 | 24 | Four three-phase 20,000 |
2. GW series — rectified output, frequency and melting time
| Type | DC voltage (V) | Direct current (A) | Medium frequency voltage (V) | Intermediate frequency (kHz) | Melting time (min) |
|---|---|---|---|---|---|
| GW-0.35T | 500 | 500 | 750 | 1 | 20–45 |
| GW-0.5T | 500 | 700 | 750 | 0.8 | 30–50 |
| GW-0.75T | 500 | 1,000 | 750 | 0.8 | 40–50 |
| GW-1T | 500 / 990 | 1,600 / 808 | 750 / 1,480 | 0.7 | 40–50 |
| GW-1.5T | 500 / 990 | 1,000 / 1,010 | 750 / 1,480 | 0.7 | 40–60 |
| GW-2T | 990 / 990 | 1,414 / 707 | 1,480 / 1,480 | 0.5 | 45–60 |
| GW-3T | 990 | 1,010 | 1,480 | 0.5 | 50–70 |
| GW-5T | 1,260 | 1,190 | 1,900 | 0.3 | 50–80 |
| GW-10T | 1,260 | 2,380 | 1,900 | 0.3 | 50–90 |
| GW-15T | 1,260 | 1,590 | 1,900 | 0.3 | 50–90 |
| GW-20T | 1,260 | 1,980 | 1,900 | 0.25 | 50–90 |
| GW-30T | 1,260 | 2,980 | 1,900 | 0.25 | 50–90 |
Note on the two published tables: the source header row is offset by one column relative to the data row — the first header cell, “EAF type Electric furnace capacity”, labels the model column. The alignment shown above is the verified one: DC volts × direct current equals the rated power for every model (500 V × 500 A = 250 kW at GW‑0.35T, 990 V × 1,414 A = 1,400 kW at GW‑2T), and rated power per tonne of EAF-equivalent capacity falls smoothly from about 714 kW/t at GW‑0.35T to 500 kW/t at GW‑30T. On GW‑1T, GW‑1.5T and GW‑2T the published row carries two configurations in each cell — a full-power tap and a reduced-power tap — reproduced here as published.
3. Published energy consumption index and in-furnace temperature
| Type | Cast iron (kWh/T) | Red copper (kWh/T) | Brass (kWh/T) | Aluminium (kWh/T) |
|---|---|---|---|---|
| GW-0.35T | 560 | 420 | 390 | 540 |
| GW-0.5T | 550 | 410 | 380 | 530 |
| GW-0.75T | 550 | 410 | 380 | 530 |
| GW-1T | 540 | 400 | 370 | 520 |
| GW-1.5T | 530 | 390 | 360 | 510 |
| GW-2T | 520 | 380 | 350 | 500 |
| GW-3T | 510 | 370 | 340 | 490 |
| GW-5T | 500 | 360 | 330 | 480 |
| GW-10T | 490 | 350 | 320 | 470 |
| GW-15T | 480 | 340 | 310 | 460 |
| GW-20T | 470 | 330 | 300 | 450 |
| GW-30T | 470 | 330 | 300 | 450 |
Published in-furnace temperature: steel 1650 °C · cast iron 1450 °C · red copper 1150 °C · brass 1000 °C · aluminium 700 °C · zinc 400 °C.
4. DW-MF IF series — the small-capacity member of the same range
| Model | Input power max | Max melting ability — steel and stainless steel | Max melting ability — gold, silver | Max melting ability — aluminium |
|---|---|---|---|---|
| DW-MF-15 | 15 kW | — | — | 3 kg |
| DW-MF-25 | 25 kW | 4 kg or 8 kg | 10 kg or 20 kg | 6 kg |
| DW-MF-35 | 35 kW | 10 kg or 14 kg | 20 kg or 30 kg | 12 kg |
| DW-MF-45 | 45 kW | 18 kg or 22 kg | 40 kg or 50 kg | 21 kg |
| DW-MF-70 | 70 kW | 28 kg | 60 kg or 80 kg | 30 kg |
| DW-MF-90 | 90 kW | 50 kg | 80 kg or 100 kg | 40 kg |
| DW-MF-110 | 110 kW | 75 kg | 100 kg or 150 kg | 50 kg |
| DW-MF-160 | 160 kW | 100 kg | 150 kg or 250 kg | 75 kg |
Published DW-MF series electrical data: generator input voltage 70–550 V, input desired 3 × 380 V, 380 V ± 20 %, 50 or 60 Hz; oscillate frequency 1 kHz – 20 kHz according to the application, normally about 4 kHz, 8 kHz, 11 kHz, 15 kHz or 20 kHz; duty cycle 100 %, 24 hours work; weight 50–145 kg; published melting time 30–50 minutes per batch, with the first melt on a cold furnace taking about 20–30 minutes longer. The main parts of the system are the medium-frequency induction heating generator, the melting furnace and the compensation capacitor.
5. Published specification notes
| Note | Published text |
|---|---|
| Capacity basis | The capacity of the electric steel melting furnace is based on the density of steel (7.8). The density of aluminium is 2.7, so aluminium of equal weight needs the same matching power, and the capacity needs about three times the furnace body. |
| Melting time | The melting time and tons of power consumption have an important relationship with the equipment matching power, the raw material shape, the raw material density and worker proficiency. |
| Energy index | The “ton power consumption (kWh/T)” figures above are a new series of power consumption, which will consume 15 % or more of the power supply than a common parallel IF power supply. |
| Equipment configuration | Medium frequency power supply, capacitor cabinet, furnace body (steel shell or aluminium shell), hydraulic station (or reducer) tilting system, water cooling cable, etc. |
| Standard data | The above is the standard product data. Different power can be designed according to the user’s demand, giving a non-standard product with a different melting speed. |

Recommended Model Selection
Start from the metal and the charge, then work to the model. The published selection data below maps an application to a power range and a frequency, and a furnace capacity to a furnace body.
| Application | Material | Recommended power | Frequency |
|---|---|---|---|
| Small cast iron melting | Gray iron, pig iron, return scrap | 100–250 kW | Medium frequency, typically 0.5–2.5 kHz depending on furnace size |
| Small steel casting workshop | Carbon steel, low-alloy steel | 160–350 kW | Medium frequency / KGPS |
| 500 kg cast iron melting | Cast iron, pig iron, foundry returns | 250–500 kW | Medium frequency |
| 1-ton iron or steel melting | Cast iron, carbon steel, alloy steel | 500–800 kW | Medium frequency / KGPS |
| 2-ton foundry melting | Iron, carbon steel, alloy steel | 1,000–1,500 kW | Medium frequency |
| 3-ton heavy-duty steel melting | Steel scrap, alloy steel, stainless steel | 1,500–2,000 kW | Medium frequency, lower range for larger bath |
| 5-ton industrial foundry melting | Cast iron, steel, heavy scrap | 2,000–2,500 kW+ | Medium frequency / high-power furnace system |
| Stainless steel melting | Stainless scrap and stainless alloy | Depends on batch size, typically 500–2,500 kW | Medium frequency with accurate temperature control |
| Furnace capacity | Typical use | Recommended furnace body | Engineering comment |
|---|---|---|---|
| 10–100 kg | Laboratory, trial melting, small castings | Small crucible furnace | Good for samples and specialty alloys |
| 150–350 kg | Small foundry, repair casting, small batch production | Aluminium shell or compact steel shell | Lower investment and flexible operation |
| 500–1,000 kg | Medium foundry production | Hydraulic tilting steel shell furnace | Common choice for continuous casting workshops |
| 1,500–3,000 kg | Large foundry and steel casting | Steel shell furnace | Requires strong transformer, cooling and safety system |
| 3,000–5,000 kg | Heavy industrial melting | Heavy-duty steel shell furnace | Designed for high output and long production shifts |
On the GW series, the model number is the EAF-equivalent capacity, the frequency falls with size and the rated power follows: 250 kW at 1 kHz for GW‑0.35T, 800 kW at 0.7 kHz for GW‑1T, 2,000 kW at 0.5 kHz for GW‑3T, 6,000 kW at 0.3 kHz for GW‑10T and 15,000 kW at 0.25 kHz for GW‑30T. Below GW‑0.35T the published route is the DW‑MF IF series, which starts at 15 kW with a 3 kg aluminium melt and reaches 100 kg of steel or stainless steel at DW‑MF‑160.
For the same duty on the other published names, see the induction furnace for melting iron and steel guide, the iron steel scrap melting furnace, the induction furnace for steel melting, the induction melting stainless steel range, the induction metals melting furnace IF series and the iron steel melting induction furnace.
Process Workflow
The published batch cycle for this equipment, with the control point that belongs to each stage.
| Step | Operation | Key control point |
|---|---|---|
| 1 | Check furnace system | Power cabinet, cooling water, hydraulic system, grounding and alarms |
| 2 | Check the lining | Refractory lining thickness, cracks, erosion and sintering condition |
| 3 | Prepare the charge | Dry, clean, properly sized iron or steel charge — no sealed or wet scrap |
| 4 | Charge the furnace | Place suitable bottom charge carefully to protect the furnace lining |
| 5 | Start power | Start at the appropriate power level and increase as the charge condition stabilises |
| 6 | Melt | Monitor voltage, current, water pressure, furnace noise and melting progress |
| 7 | Add charge | Add remaining scrap gradually after the molten pool forms; avoid bridging |
| 8 | Alloy and adjust chemistry | Add carbon, silicon, manganese, chromium or other alloying materials as required |
| 9 | Remove slag | Remove slag to improve the cleanliness of the molten metal |
| 10 | Measure temperature | Confirm the pouring temperature with suitable measurement equipment |
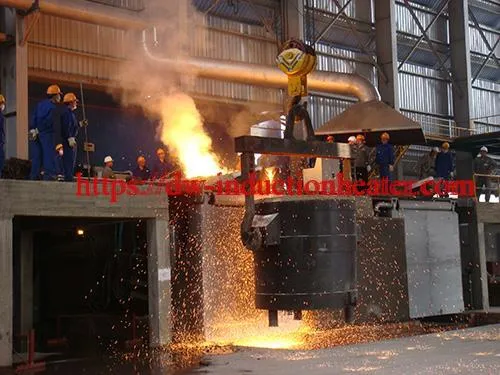
| 11 | Tilt and pour | Use hydraulic tilting to pour the molten metal safely into a ladle or mould |
| 12 | Post-melting check | Inspect the lining; record energy consumption, melting time and production data |
Two published points belong at this point in the cycle. The in-furnace temperature for steel is published as 1650 °C, so the temperature measurement at step 10 is the gate between an in-furnace temperature and a pouring temperature. And the published environment equipment — the whirlwind and side-suction heat-preservation furnace cover and the ring dust hood — is part of the furnace, not an accessory: the waste gas generated in smelting has to be captured for the exhaust-emission effect to meet the requirements of the environmental impact assessment design.


Common Problems and Solutions
| Problem | Possible cause | Published solution |
|---|---|---|
| Melting time too long | Power too low, charge too large, voltage unstable or lining insulation poor | Select higher power, improve charge size, inspect the lining and confirm transformer capacity |
| Power consumption too high | Long holding time, wet charge, excessive superheating or poor lining condition | Reduce holding time, dry the charge, optimise the temperature target and maintain the lining |
| Furnace alarms frequently | Cooling water problem, over-current, over-voltage, load mismatch or capacitor fault | Check water pressure, water flow, the capacitor cabinet, input voltage and furnace load |
| Bath temperature uneven | Poor charge distribution, insufficient melting time or weak stirring | Improve the charging sequence and allow complete melting before measuring temperature |
| Lining wears quickly | Wrong refractory material, poor sintering, thermal shock or mechanical damage during charging | Use the correct lining material, follow the sintering procedure and avoid heavy impact loading |
| Molten metal splashes when charging | Wet scrap, sealed cavities, oil contamination or improper charging | Use dry clean scrap, remove sealed containers and charge carefully |
| Oxidation or alloy loss high | Overheating, long holding time, poor slag practice or wrong alloy addition sequence | Control temperature, shorten holding time and optimise alloy and slag practice |
| Pouring unstable | Hydraulic system issue, poor ladle position or worn tilting structure | Inspect the hydraulic cylinder, hinge, limit switch and pouring layout |
| Harmonics or compensation complaints from the substation | Rectifier supply not operating in the published full-open condition | Use the full-wave rectifier power supply series, which stays fully open, so no higher harmonics are produced and the substation reactive compensation capacitor is unaffected |
| Frequent start-up trips | Supply not suited to repeated starting | Use the published zero-voltage sweep-frequency style start, which is adapted to the requirement of frequently starting |
Engineering Selection Guide
Ten factors decide the specification. Work through them in order, because each one constrains the next.
| Selection factor | What to confirm | Published recommendation |
|---|---|---|
| Metal type | Cast iron, carbon steel, stainless steel or alloy steel | Select lining chemistry and power density according to metal type |
| Batch capacity | Required kilograms or tons per melt | Select furnace capacity with a practical loading and pouring margin |
| Target melting time | Required minutes per batch | Higher power shortens melting time but requires stronger electrical infrastructure |
| Daily production | Tons per shift or tons per day | Determine whether one furnace is enough or multiple furnaces are needed |
| Input power supply | Factory voltage, transformer capacity and cable size | Confirm the electrical room capacity before ordering a high-power furnace |
| Furnace body | Steel shell or aluminium shell | Use steel shell for larger iron/steel melting or heavy-duty foundry operation |
| Tilting system | Manual, mechanical or hydraulic tilting | Hydraulic tilting is recommended for medium and large furnaces |
| Cooling system | Water flow, pressure, temperature and water quality | Use a closed-loop cooling tower or industrial chiller according to local conditions |
| Safety protection | Leak furnace alarm, water pressure protection, emergency stop and over-current protection | Do not reduce the safety configuration for steel and iron melting projects |
| Workshop layout | Charging area, crane, ladle path, mould area and cooling equipment position | Plan the furnace layout before finalizing the equipment dimensions |
Three published design items belong on the drawing rather than in the quotation. The coil is a water-cooled copper tube with a reliable water passage, insulated between turns with high-temperature and high-voltage materials. The furnace shell for large iron and steel furnaces should be steel, and a magnetic yoke is recommended for many steel-shell designs to improve magnetic field distribution and reduce stray field. The hydraulic tilting frame needs a strong shaft, cylinder, limit switch and safety lock design.
Advantages and Limitations
Advantages
- Fast melting. Heat is generated directly inside the iron or steel charge, so the melting cycle is short and the production output high — a single furnace melt can be as fast as under 40 minutes.
- Clean electric heating. No combustion flame inside the furnace, so the workshop is cleaner than many fuel-fired systems, with no dust and little noise.
- Good temperature control. Electrical power is adjusted quickly, giving a more stable pouring temperature and better casting quality.
- Electromagnetic stirring. The molten metal circulates naturally under magnetic force, improving bath temperature uniformity and alloy mixing.
- Lower oxidation loss. Reduced flame contact and a controlled melting atmosphere improve metal yield and reduce material waste.
- Flexible raw material. Pig iron, return scrap, steel scrap and alloy additions can all be melted — the published furnace is used for steel, iron, stainless steel, copper, aluminium and alloys.
- Automation compatibility. PLC, HMI, temperature feedback and energy data recording can be integrated, supporting intelligent production and operation traceability.
- Controlled pouring. Hydraulic tilting gives a stable molten metal discharge and improves operator safety and the casting workflow.
- No pollution to the power network. The full-wave rectifier series stays fully open, so no higher harmonics are produced and the substation’s compensation capacitor is unaffected.
- Constant power output. No operator adjustment is needed from the start of the melt to the end of the batch, which is what makes repeat heats repeatable.
- Suited to frequent starting. The published zero-voltage sweep-frequency style start is adapted to the requirement of frequently starting.
Limitations and things to plan for
- High electrical demand. Melting iron and steel requires large electrical power. Confirm transformer capacity, input voltage and cable size before installation.
- Cooling water is essential. The coil, cables, power supply and capacitor cabinet produce heat during operation. Insufficient cooling causes alarms, insulation damage, coil failure or safety hazards.
- The refractory lining is a consumable. It is exposed to high temperature, slag attack and mechanical damage, and must be selected, sintered, inspected and repaired on a schedule.
- Wet scrap is dangerous. Moisture can expand rapidly and cause molten metal to splash.
- Wrong furnace size increases cost. Oversized or undersized furnaces reduce efficiency and productivity.
- Alloy control needs process discipline. Overheating or long holding causes alloy loss; correct temperature control, sampling and alloy addition sequence are required.
- The coil is a quarter of the power. The published coil loss is 25 % of total power, and the published ton-consumption series consumes 15 % or more of the power supply than a common parallel IF power supply.
- Melting time is not a fixed number. It depends on the equipment’s matched power, the raw material shape, the raw material density and worker proficiency.
- The published data is standard product data. Different power can be designed to the user’s demand, but a non-standard product comes with a different melting speed.
Why Choose HLQ?
- Iron and steel application support. Furnace configuration can be selected for cast iron, steel, stainless steel and alloy steel, which improves project matching and reduces the risk of wrong selection.
- Medium frequency / KGPS furnace systems. Power supply and furnace body can be matched according to capacity, supporting stable melting performance and practical foundry use.
- One published principle across two capacity bands. The GW production series runs from 0.35 t to 30 t at 0.25–1 kHz, and the DW-MF IF series covers small melts at 1–20 kHz — so a plant can be scaled without changing technology.
- Steel shell and aluminium shell options. Different furnace structures for different production levels, so buyers can balance cost, strength and safety.
- Hydraulic tilting design. The furnace can be tilted for controlled pouring, improving operator safety and pouring stability.
- Cooling and safety configuration. Cooling system, alarms and protection can be integrated, reducing downtime and improving operating safety.
- Engineering selection guidance. Support for capacity, power, voltage, cooling and layout selection — helping buyers build a practical melting system rather than only purchasing a furnace.
- A documented component strategy. Imported high-pressure carbon-free hose with 304 stainless steel clamp, optical-fibre inverter trigger pulse signal plate, square-type water cooling radiator, a customised capacitor with a magnesium-aluminium alloy outer shell, large thick conductive copper bar with a sandblasted and anti-oxidised contact surface, an isolation (exchange) switch, and a plate heat exchange system that keeps external hard water out of the power supply.
- Direct manufacturer with 25 years of R&D in induction heating, every machine test-run before shipment.
6 Core FAQs
1. What does “medium frequency” actually mean for a steel melting furnace?
It is the operating frequency of the power supply, and it is the variable that scales with the job. On the published GW series the intermediate frequency falls as capacity rises — 1 kHz at GW‑0.35T, 0.8 kHz at GW‑0.5T and GW‑0.75T, 0.7 kHz at GW‑1T and GW‑1.5T, 0.5 kHz at GW‑2T and GW‑3T, 0.3 kHz at GW‑5T to GW‑15T, and 0.25 kHz at GW‑20T and GW‑30T — because lower frequency is used for the larger furnace capacities. The small-capacity IF series runs higher, at 1–20 kHz, normally about 4, 8, 11, 15 or 20 kHz according to the application.
2. Which capacity and frequency do I need for a cast iron foundry?
The published selection table puts small cast iron melting at 100–250 kW, a 500 kg cast iron heat at 250–500 kW, and a 1-ton iron or steel heat at 500–800 kW, at medium frequency of typically 0.5–2.5 kHz depending on furnace size. The GW ladder follows the same progression as an EAF equivalent: GW‑0.35T at 250 kW and 1 kHz, GW‑1T at 800 kW and 0.7 kHz, GW‑3T at 2,000 kW and 0.5 kHz, GW‑30T at 15,000 kW and 0.25 kHz. Below 100 kg of iron, the published IF series starts at DW‑MF‑25 with 4 kg or 8 kg of steel or stainless steel.
3. How much energy does it take to melt cast iron?
The published index runs from 560 kWh per tonne at GW‑0.35T down to 470 kWh per tonne at GW‑20T and GW‑30T, with HLQ’s published claim of about 530 kWh/T for cast iron and about 20 % energy saving against a common parallel-inverter power supply. The index improves with scale on every metal — red copper from 420 to 330 kWh/T, brass from 390 to 300 kWh/T and aluminium from 540 to 450 kWh/T. Note that this ton-consumption series consumes 15 % or more of the power supply than a common parallel IF power supply.
4. What temperature does the furnace reach for steel, and how is the pour controlled?
The published in-furnace temperature for steel is 1650 °C, with cast iron 1450 °C, red copper 1150 °C, brass 1000 °C, aluminium 700 °C and zinc 400 °C. The published melting temperature ranges for ferrous alloys are gray cast iron 1150–1400 °C, ductile iron 1300–1500 °C, carbon steel 1450–1600 °C, low-alloy steel 1450–1650 °C, stainless steel 1400–1550 °C, high-manganese steel 1400–1500 °C and tool steel 1450–1600 °C. The pouring temperature is confirmed separately with suitable measurement equipment before the hydraulic tilt.
5. Does the furnace upset the power network, and can one unit be serviced without stopping the others?
No on both counts. The rectifier is a full-wave power supply series that stays in a state of full open — equivalent to a diode rectifier — so no higher harmonics are produced, there is basically no pollution to the power network, and the substation’s reactive power compensation capacitor is unaffected. And the isolation (exchange) switch means that when one furnace is replaced or overhauled, its power can be cut off without affecting the normal operation of another furnace.
6. What happens if the charge is wet, or if the furnace is started and stopped repeatedly?
Wet, oily or sealed scrap must not go in: moisture can expand rapidly and cause molten metal to splash, and sealed cavities are a published cause of a violent eruption on charging. On the start side, the published zero-voltage sweep-frequency style start is specifically adapted to the requirement of frequently starting, and the protection set — over-current, over-voltage, current-limiting, voltage-limiting, water-break and default protection — is there so that the equipment runs reliably under the premise of the melting speed being guaranteed.