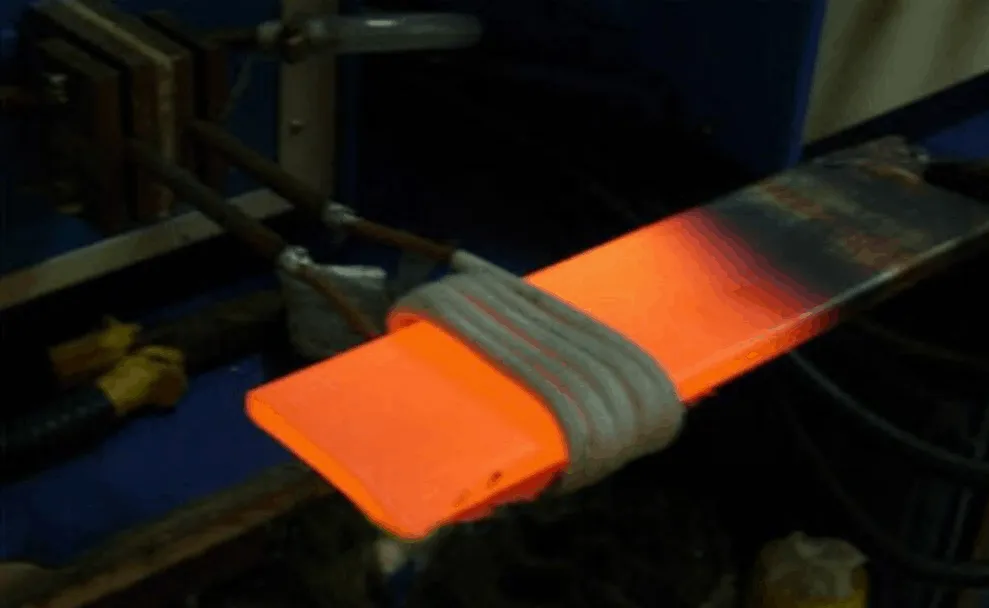


Induction Heating Steel Plate for Forging
Induction Heating Steel Plate for Forging and Hot Forming
Quick Answer: How Does Induction Heating Heat Steel Plates for Forging?
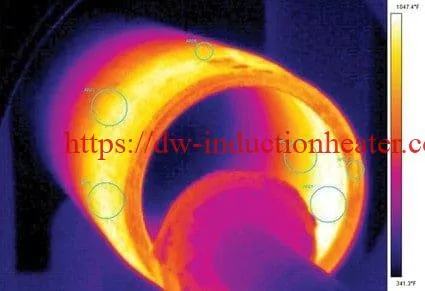
Induction heating is a fast and controllable method for heating steel plates before forging and hot forming. A medium-frequency induction system generates heat directly inside the conductive steel workpiece, enabling rapid and repeatable heating without heating an entire furnace chamber. For a 100 × 190 × 19 mm steel plate, a 125 kW, 7 kHz induction heating system can heat the plate to approximately 1200°C for forging. In a multi-position coil configuration, the process can deliver one heated plate approximately every 37 seconds after startup, making induction heating suitable for automated high-volume forging lines.
Metal induction heating steel plate for forging and hot forming are excellent induction heating applications. Industrial Induction forging and hot forming processes involve bending or shaping a metal billet or bloom after it has been heated to a temperature at which its resistance to deformation is weak. Blocks of non-ferrous materials can also be used. 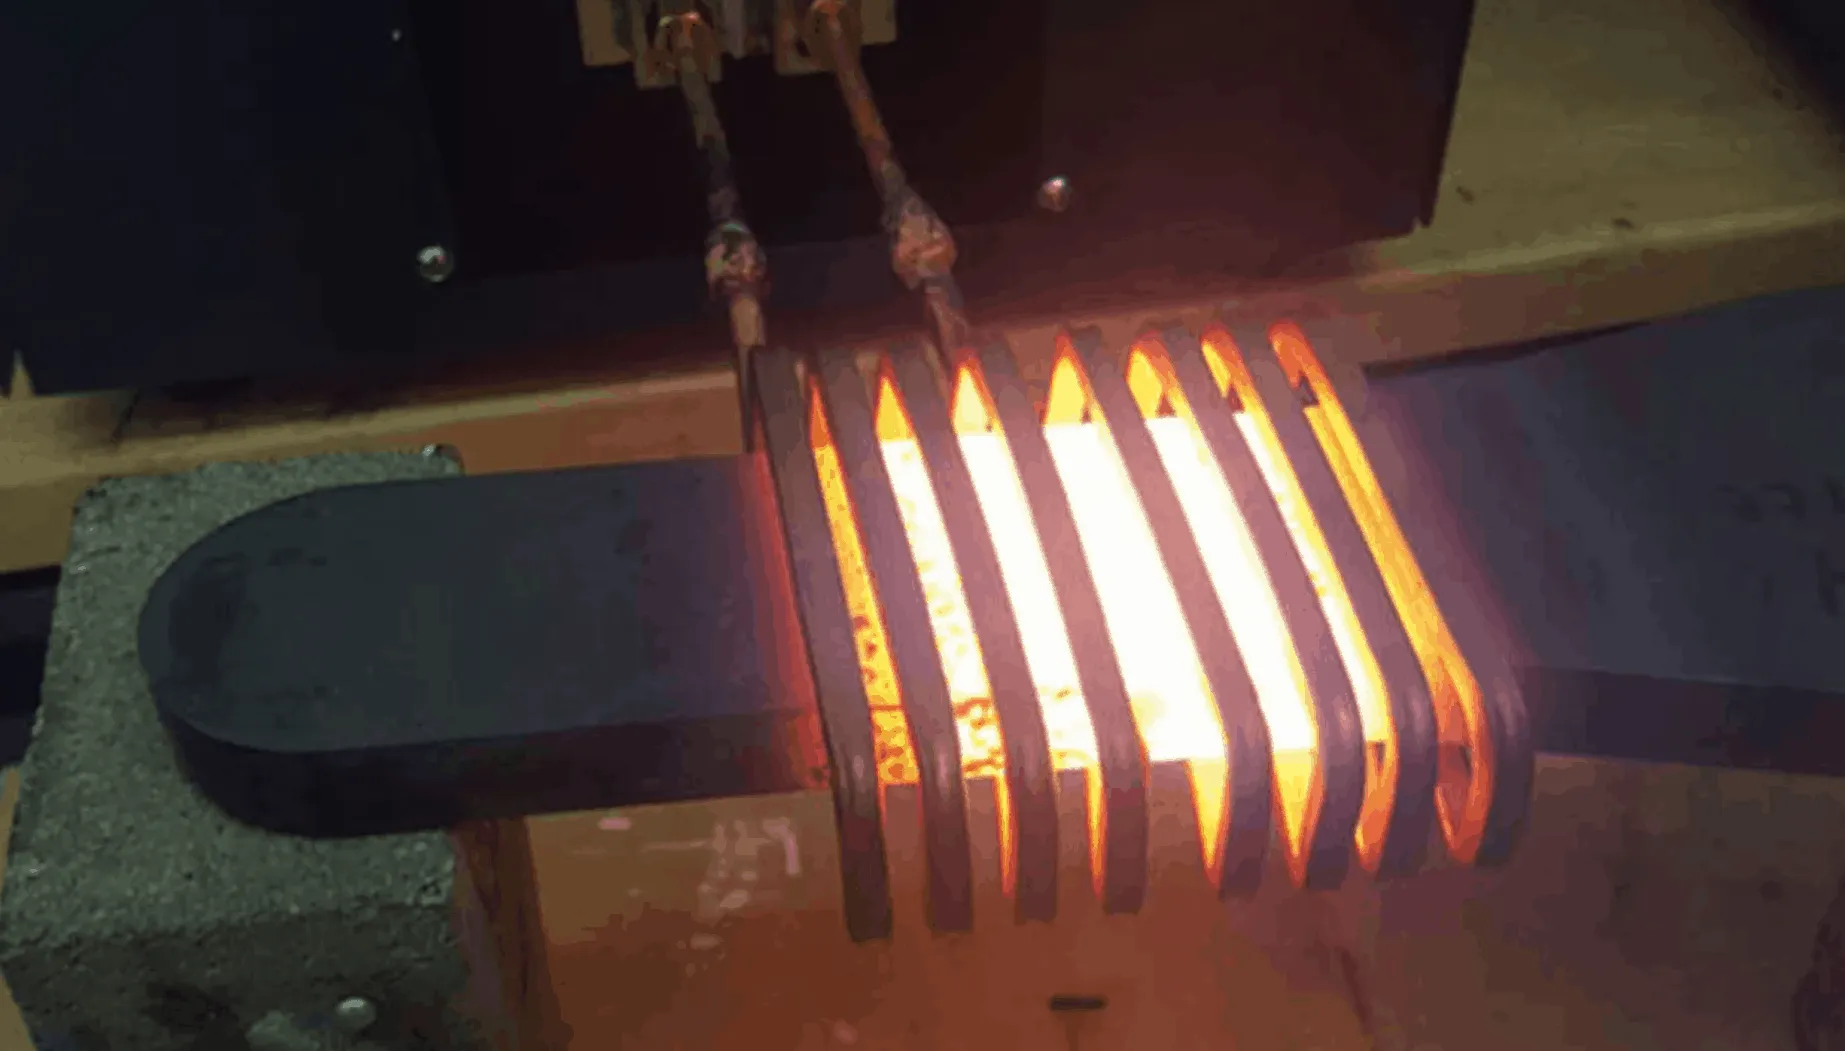
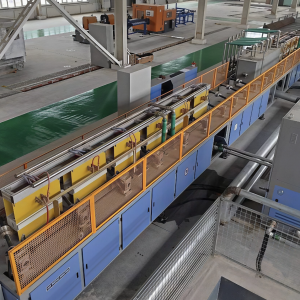
Induction heating machines or conventional furnaces are used for the initial heating process. Billets can be transported through the inductor via a pneumatic or hydraulic pusher; pinch roller drive; tractor drive; or walking beam. Non-contact pyrometers are used to measure the billet temperature.
Other machines such as mechanical impact presses, bending machines, and hydraulic extrusion presses are used to bend or shape the metal.
Objective: Preheat a steel plate (3.9” x 7.5” x 0.75” / 100mm x 190mm x 19mm) prior to forging to create a hoe head with the goal of increasing production compared to preheating with a gas furnace.
Material: Steel Plate
Temperature: 2192 ºF (1200 ºC)
Frequency: 7 kHz
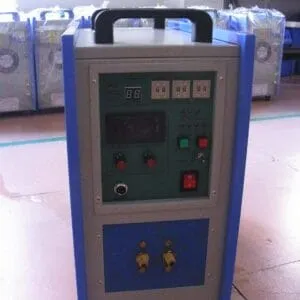
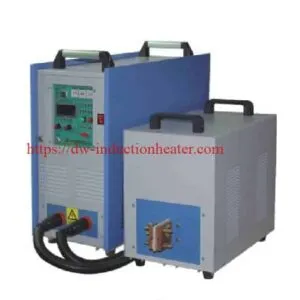
Induction Heating Equipment: DW-MF-125/100, 125 kW induction heating system equipped with a remote heat station containing three 26.8 μF capacitors.
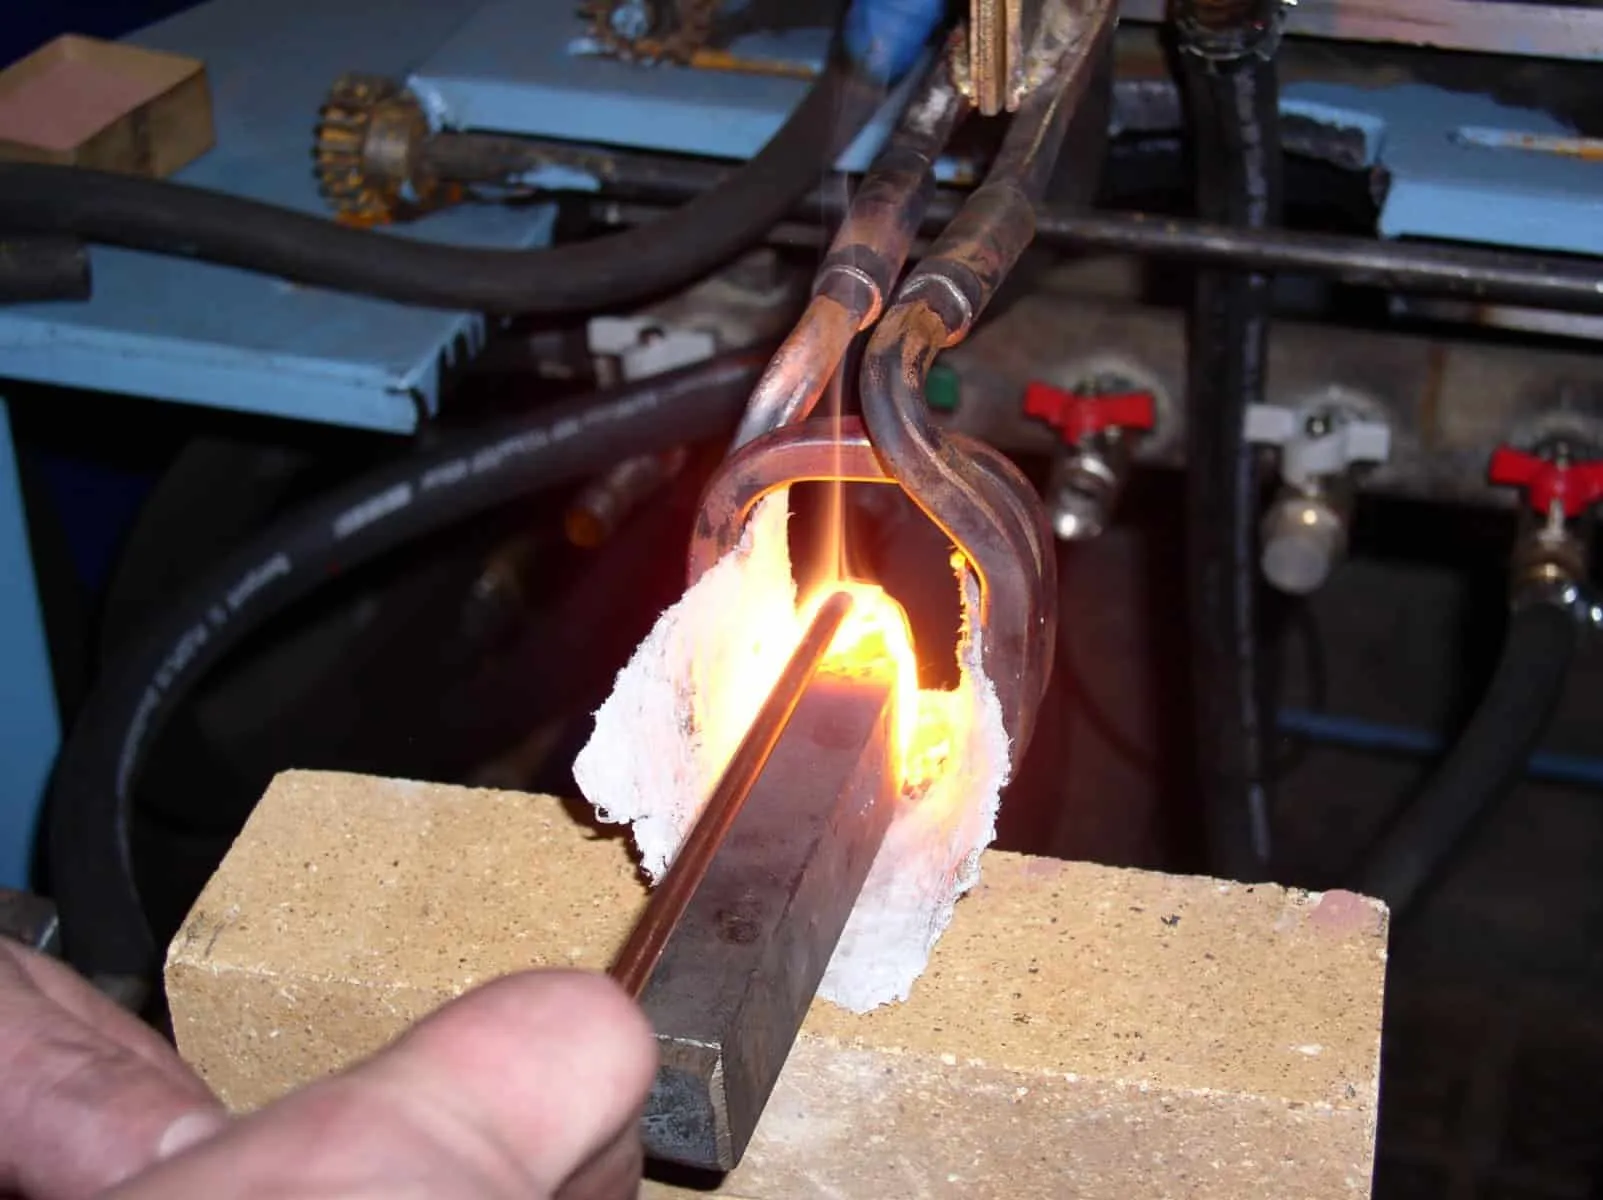
– A three position, multi-turn helical coil designed and developed to generate the required heat for this application.
Process The steel plate was inserted into the three position multi-turn helical coil and the power supply was turned on. At 37 seconds, a second stainless steel plate was inserted, and at 75 seconds a third stainless steel plate was inserted. At 115 seconds, the desired temperature was achieved for the first part, and the process continued.
After startup, parts can be heated every 37 seconds from the sequence they were entered. While total cycle time is 115
seconds, a part can be removed every 37 seconds, which allowed for induction to achieve the desired production rate
and realize considerable gains when compared to using a gas furnace.
Results/Benefits
Higher production rate: The process achieved a production rate of 100 parts per hour, while a gas furnace produced 83 parts per hour
– Repeatability: This process is repeatable and can be integrated into a production process
– Precision and efficiency: Heating is precise and efficient, with heat only applied to the steel plates
The approximate hot forming temperatures of the most commonly used industrial materials are:
• Steel 1200º C • Brass 750º C • Aluminium 550º C
Total Induction Hot Forming Applications
Induction heating machines are commonly used to heat steel billets, bars, brass blocks, and titanium blocks to the proper temperature for forging and hot forming.
Partial Forming Applications
Induction heating is also used to heat parts such as pipe ends, axle ends, automotive parts, and bar ends for partial forming and forging processes.
The Induction Heating Advantage
When compared to conventional furnaces, induction heating machines for forging offer significant process and quality advantages:
Much shorter heating times, minimizing scaling and oxidation
Easy and accurate temperature temperature control. Parts at temperatures outside specifications can be detected and removed
No time lost waiting for the furnace to ramp up to the required temperature
Automated induction heating machines require minimal manual labor
Heat can be directed to one specific point, which is highly important for parts with only one forming area.
Greater thermal efficiency – heat is generated in the part itself and does not need to be heated in a large chamber.
Better working conditions. The only heat present in the air is that of the parts themselves. The working conditions are much more pleasant than with a fuel furnace.
How to Select an Induction Heater for Steel Plate Forging
For a new steel plate forging project, power should not be selected from plate dimensions alone.
HLQ should obtain at least:
| Selection Parameter | Information Required |
|---|---|
| Material | Carbon steel, alloy steel, stainless steel, etc. |
| Plate Width | mm |
| Plate Length | mm |
| Plate Thickness | mm |
| Initial Temperature | °C |
| Forging Temperature | °C |
| Heating Time | seconds |
| Required Output | pcs/hour or kg/hour |
| Heated Area | Full plate or partial area |
| Feeding Method | Manual / pneumatic / hydraulic / robot |
| Electrical Supply | Voltage / frequency / 3-phase |
| Continuous Operation | Hours/day |
FAQs
1. What induction heating power is required for steel plate forging?
The required induction power depends on the steel plate mass, thickness, target forging temperature, required heating time and production rate. For the application described on this page, a 100 × 190 × 19 mm steel plate was heated to approximately 1200°C using a 125 kW induction heating system operating at 7 kHz. Larger plates or shorter cycle times generally require more installed power.
2. What temperature should a steel plate reach before forging?
The appropriate forging temperature depends on the steel grade and forming process. In this specific steel-plate application, the target temperature was approximately 1200°C (2192°F). The required temperature for an actual production line should be confirmed according to the material grade and forging specifications.
3. What frequency is suitable for induction heating thick steel plates?
Medium frequencies are commonly suitable for relatively thick steel sections because heating penetration becomes important as workpiece thickness increases. The application shown here operates at approximately 7 kHz for a 19 mm thick steel plate. Frequency selection should nevertheless be optimized according to plate thickness, coil geometry, heating uniformity and required cycle time.
4. Can induction heating replace a gas furnace for steel forging?
Yes, induction heating can replace gas-furnace preheating in many repetitive forging applications. In the documented application on this page, induction heating increased production from approximately 83 parts/hour to 100 parts/hour. The suitability of replacement depends on part geometry, throughput, heating temperature, automation and electrical infrastructure.
5. Can induction heating be integrated with an automatic forging line?
Yes. Induction heating systems can be integrated with pneumatic or hydraulic pushers, roller feeds, walking-beam systems, robotic handling, non-contact pyrometers and forging presses. A PLC can coordinate feeding, heating time, temperature verification and transfer of each hot workpiece to the forming station.
6. Can only part of a steel plate be heated for forging?
Yes. One advantage of induction heating is the ability to concentrate energy in a selected area. Coil geometry can be designed for full-plate heating or localized heating where only one end, edge or forming zone needs to reach forging temperature. This can reduce unnecessary heating and simplify downstream forming operations.