Applications of Induction PWHT Machines in the Oil and Gas Pipelines Field
Pipeline Induction PWHT Machines for Oil & Gas Weld Heat Treatment
Quick Answer
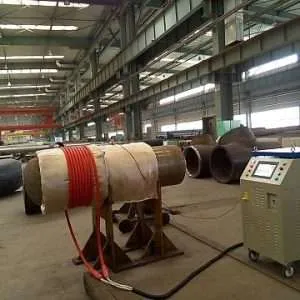
An induction PWHT machine is an industrial heating system used to perform controlled post weld heat treatment on steel pipelines, pressure piping, and welded metal components. It uses electromagnetic induction to generate heat directly within the pipe wall, while thermocouples and programmable temperature controls monitor the required heating, soaking, and cooling cycle.
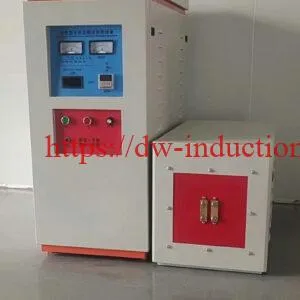
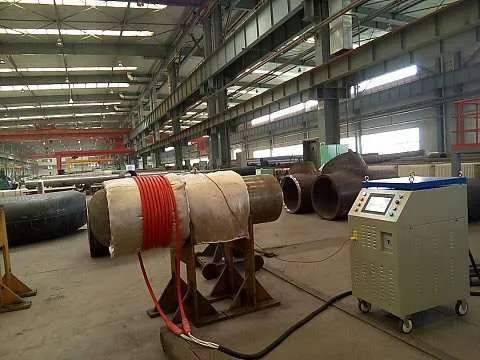
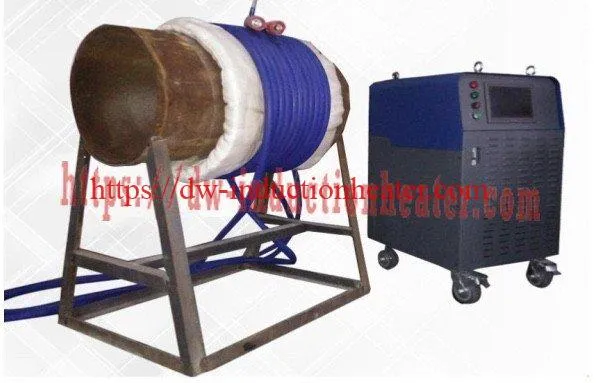
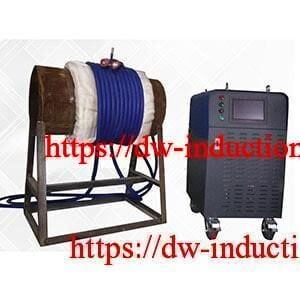
HLQ induction PWHT systems can be configured with flexible induction heating cables, thermal insulation blankets, temperature monitoring, and recording equipment. They are suitable for selected oil and gas pipeline construction, refinery maintenance, pressure piping fabrication, and weld stress-relieving applications.
The published HLQ MYD equipment range includes 40 kW, 50 kW, 60 kW, 80 kW, 100 kW, and 120 kW models. Higher-power configurations require application-specific engineering confirmation.
| Parameter | Engineering Overview |
|---|---|
| Equipment | Induction Post Weld Heat Treatment Machine |
| Brand | HLQ Induction |
| Main Application | Oil and gas pipeline weld heat treatment |
| Published MYD Models | 40–120 kW |
| Additional Reference Power Classes | 160–300 kW, subject to configuration confirmation |
| Published MYD Frequency Range | 2–30 kHz |
| Heating Method | Electromagnetic induction |
| Heating Accessories | Flexible induction cable and insulation blanket |
| Temperature Measurement | Thermocouples with suitable controller and recorder |
| Typical Industries | Oil and gas, petrochemical, refinery, power generation, and pressure piping |
Engineering Note: The required PWHT temperature, heating rate, holding period, cooling rate, and heated-band dimensions must be determined by the approved heat-treatment procedure and applicable project requirements. Equipment capability does not automatically establish code compliance.
Table of Contents
What is a Pipeline Induction PWHT Machine?
A pipeline induction post weld heat treatment machine is a specialized industrial heating system designed to produce a controlled thermal cycle around a welded joint.
During welding, localized heating and cooling can generate residual stresses and modify the microstructure of the weld metal and heat-affected zone. Depending on the material, wall thickness, welding procedure, service conditions, and applicable construction code, post weld heat treatment may be required to achieve specified metallurgical or mechanical properties.
Induction PWHT uses alternating electromagnetic fields to generate heat within the electrically conductive material. The system can be installed directly around a pipeline weld, allowing localized heating without moving the entire pipeline section into a furnace.
HLQ supplies induction heating technology for welding, pipeline fabrication, and industrial thermal processing. Related induction PWHT equipment can be configured around the requirements of individual fabrication and maintenance projects.
Main Components of an Induction PWHT System
| Component | Function | Engineering Considerations |
|---|---|---|
| Induction Power Supply | Generates alternating electrical current for induction heating. | Power rating, frequency, duty cycle, input voltage, and cooling requirements. |
| Flexible Induction Heating Cable | Creates an alternating magnetic field around the pipe. | Current capacity, cable length, turn arrangement, insulation, and cooling. |
| Insulation Blanket | Reduces heat loss and helps maintain the required heating distribution. | Temperature rating, thickness, installation, and compatibility. |
| Thermocouples | Measure temperature at selected locations around the weld. | Sensor type, attachment method, calibration, and positioning. |
| Temperature Controller | Adjusts heating power according to the programmed thermal cycle. | Control algorithm, measurement inputs, alarms, and recipe management. |
| Temperature Recorder | Records the actual time-temperature history. | Logging interval, traceability, channel count, and reporting. |
| Connection Cables | Connect the power supply, induction coil, and instrumentation. | Electrical rating, cable routing, mechanical protection, and safety. |
Induction PWHT vs. Welding Preheating
Welding preheating and post weld heat treatment are related but distinct processes.
| Comparison | Welding Preheating | Post Weld Heat Treatment |
|---|---|---|
| Process Stage | Before or during welding | After completion of welding |
| Primary Purpose | Control welding cooling conditions and reduce specific cracking risks | Achieve a prescribed post-weld metallurgical and stress-relief treatment |
| Temperature | Specified by the WPS | Specified by the approved PWHT procedure |
| Holding Requirement | Maintain required preheat or interpass conditions | Controlled soak at the prescribed temperature |
| Temperature Recording | According to welding and project requirements | Often requires a documented complete thermal cycle |
| Engineering Basis | WPS, material, thickness, hydrogen control, and applicable code | Material, code, wall thickness, service, and approved procedure |
Key Applications of Induction PWHT Machines
Induction PWHT systems are used where large welded components cannot conveniently be placed in conventional heat-treatment furnaces or where localized treatment is technically appropriate.
1. Oil and Gas Transmission Pipelines
Pipeline induction PWHT equipment can be used for selected weld joints during construction, modification, and maintenance of oil and gas transmission systems.
Applications include circumferential girth welds, tie-in welds, replacement sections, and specific repair welds where an approved procedure requires post weld heat treatment.
For large-diameter pipeline projects, carefully designed pipeline induction PWHT systems can support localized heating of weld regions under controlled and documented conditions.
2. Refinery and Petrochemical Piping
Refineries and petrochemical plants use a wide range of pressure piping materials, including carbon steel, low-alloy steel, and chromium-molybdenum alloy steel.
The applicable post weld heat treatment requirements depend on material classification, design conditions, wall thickness, service, and construction specifications.
3. Pipeline Repair and Section Replacement
Pipeline repair projects may require localized heating where a section has been replaced or a repair weld has been completed.
The suitability of induction PWHT must be assessed before installation, particularly when nearby components, coatings, insulation systems, or process equipment have temperature limitations.
4. Offshore Fabrication and Platform Piping
Induction heating may be considered for suitable offshore spool fabrication and platform piping work where installation space, power availability, environmental protection, and project safety requirements have been evaluated.
Special attention must be given to potentially hazardous atmospheres, electrical protection, equipment enclosures, and approved site operating procedures.
5. Pressure Piping and Heavy Fabrication
In addition to pipeline girth welds, induction PWHT can be applied to selected welded fittings, pipe spools, heavy-wall components, and other structures where local heat treatment is permitted by the applicable design and fabrication requirements.
Application Comparison
| Application | Workpiece | Typical Objective | Important Design Factor |
|---|---|---|---|
| Pipeline Tie-In Welding | Carbon steel pipe | Perform specified post-weld thermal treatment | Circumferential temperature distribution |
| Refinery Piping | Carbon or alloy steel | Meet material-specific PWHT requirements | Temperature accuracy and documentation |
| Pipeline Weld Repair | Approved repaired weld | Complete prescribed treatment after repair | Existing component limitations |
| Cr-Mo Process Piping | P11, P22, or similar alloys | Material-specific post-weld heat treatment | Qualified holding temperature and cooling profile |
| Large Pipe Spools | Heavy-wall fabricated piping | Controlled localized treatment | Heating bandwidth and installed power |
| Offshore Fabrication | Welded pipe assemblies | On-site or workshop PWHT | Safety, access, and electrical protection |

Suitable Materials for Induction Pipeline PWHT
Induction heating can generate heat in many electrically conductive metals. However, the ability to heat a material does not necessarily mean that the material requires post weld heat treatment.
Material selection must distinguish electromagnetic heating compatibility from metallurgical and code requirements.
| Material | Representative Grade | Induction Heating Compatibility | PWHT Considerations |
|---|---|---|---|
| Carbon Steel | ASTM A106 Gr. B | Suitable | PWHT depends on code, thickness, welding, and service conditions. |
| Carbon Steel Pipe | ASTM A53 | Suitable | Evaluate the approved welding and heat-treatment requirements. |
| Pipeline Steel | API 5L X52 | Suitable | PWHT is not automatically mandatory for every joint. |
| Pipeline Steel | API 5L X60 / X65 | Suitable | Review strength, toughness, welding procedure, and project restrictions. |
| High-Strength Pipeline Steel | API 5L X70 | Suitable for induction heating | Any PWHT must be justified and qualified for the material and joint. |
| Low-Alloy Steel | ASTM A335 P11 | Suitable | Follow applicable Cr-Mo heat-treatment requirements. |
| Low-Alloy Steel | ASTM A335 P22 | Suitable | Control soaking temperature, duration, and cooling carefully. |
| Creep-Resistant Alloy | ASTM A335 P91 | Suitable for induction heating | Requires particularly strict alloy-specific procedures and controls. |
| Austenitic Stainless Steel | 304 / 316 | Can be induction heated | Routine carbon-steel stress-relief assumptions must not be applied. |
Material Engineering Notes
Carbon Steel: Heat-treatment requirements depend on more than carbon content or wall thickness alone. The construction code, material specification, welding procedure, service conditions, and exemptions must be reviewed.
Low-Alloy Steel: Chromium-molybdenum steels may require controlled PWHT to achieve the prescribed properties after welding. A qualified procedure is essential.
High-Strength Pipeline Steel: Heat treatment must not be applied without evaluating its effect on strength, toughness, and other required material properties.
Stainless Steel: Different stainless steel families require different thermal treatments. Heating capability does not imply that conventional PWHT is appropriate.
Working Principle of an Induction PWHT Machine
An induction PWHT machine operates by electromagnetic induction.
The power supply delivers alternating current to an induction coil or flexible heating cable installed around the workpiece.
The alternating current creates a changing magnetic field. When this field interacts with the electrically conductive pipe wall, it induces eddy currents within the metal.
The electrical resistance of the pipe material converts these induced currents into thermal energy.
For ferromagnetic steels, magnetic effects can also influence heating below the Curie temperature. At elevated temperatures, the magnetic properties and electromagnetic penetration behavior change, affecting coupling and heating distribution.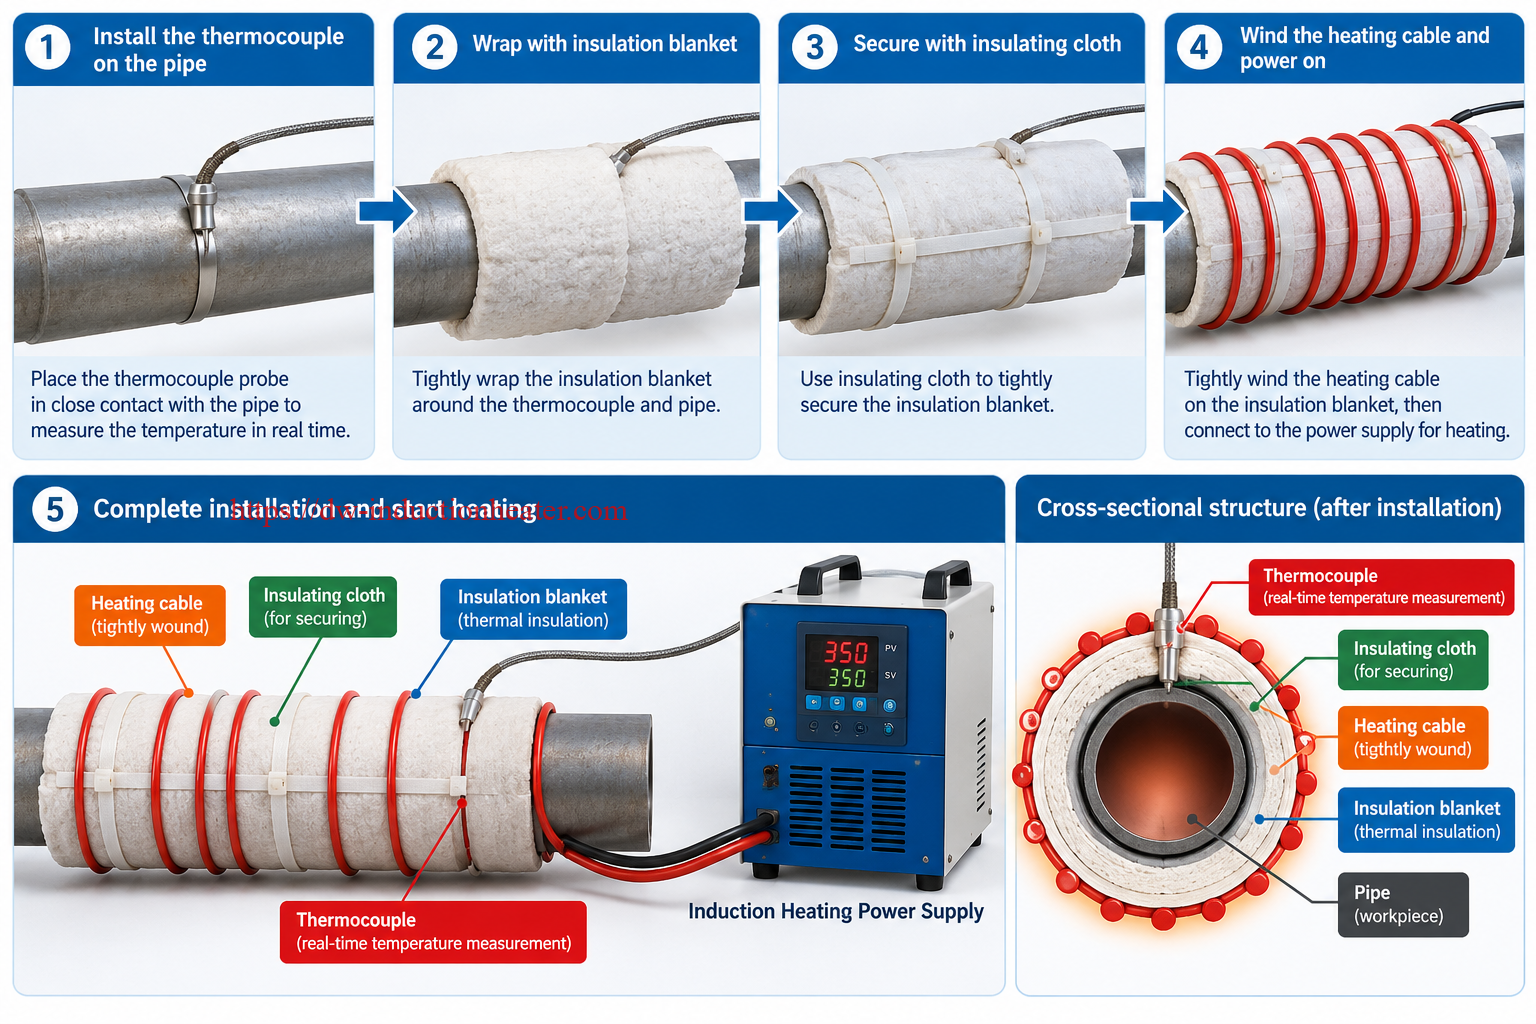
Induction Heating Process
| Step | Process | Technical Explanation |
|---|---|---|
| 1 | Electrical Power Input | The power supply receives electrical energy from the incoming AC power system. |
| 2 | Frequency Conversion | The inverter generates alternating current at a suitable operating frequency. |
| 3 | Magnetic Field Generation | Current flowing through the induction cable creates an alternating magnetic field. |
| 4 | Induced Current | Eddy currents are generated within the electrically conductive pipe wall. |
| 5 | Heat Generation | Electrical losses produce heat within the workpiece. |
| 6 | Temperature Measurement | Thermocouples measure the temperature at designated control and monitoring points. |
| 7 | Power Regulation | The controller adjusts heating output according to the prescribed thermal cycle. |
| 8 | Temperature Recording | The recorder documents the thermal history for inspection and traceability. |
Flexible Induction Heating Cable Arrangement
For many pipeline applications, flexible induction cables can be installed around the pipe circumference. The coil arrangement must accommodate the required heated band and minimize excessive local temperature differences.
The number of cable turns cannot be determined from pipe diameter alone. It also depends on operating frequency, matching characteristics, wall thickness, cable current rating, heating bandwidth, and available power.
Suitable thermal insulation helps reduce heat losses and maintain a more stable heating profile.

Temperature Control During PWHT
A typical controlled PWHT operation includes a heating stage, a temperature-holding stage, and a controlled cooling stage.
During heating, the controller regulates the induction output while monitoring temperature feedback.
During soaking, the required temperature distribution must remain within the limits defined by the approved procedure.
During cooling, the system may progressively reduce power output, while the actual workpiece cooling behavior depends on stored thermal energy, heat loss, insulation, and the environment.
Temperature monitoring and recording should continue for the duration required by the approved procedure.
Why Thermal Insulation Matters
Thermal insulation is an important part of the total PWHT system. It reduces heat loss, helps protect the heating arrangement, and can improve the stability of the temperature profile.

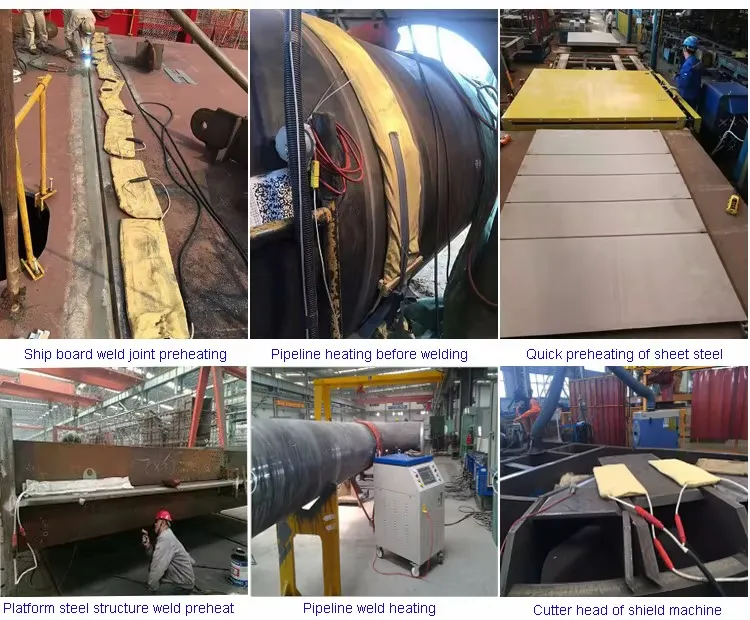
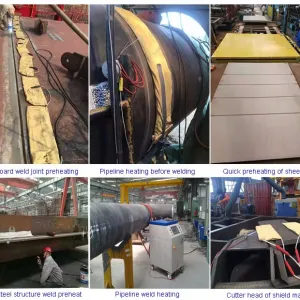
Related pipe weld preheating equipment may use similar induction heating principles, although welding preheat and PWHT have different thermal cycle requirements.
Technical Specifications of HLQ Induction PWHT Machines
HLQ publishes the MYD induction heating series for welding preheating, post weld heat treatment, and related industrial heating applications.
The following table summarizes the published MYD model ratings. Final specifications must be confirmed against the selected model’s current technical datasheet.
HLQ MYD Series Technical Parameters
| Model | Rated Power | Published Input Current | Published Frequency |
|---|---|---|---|
| MYD-40KW | 40 kW | 60 A | 2–30 kHz |
| MYD-50KW | 50 kW | 75 A | 2–30 kHz |
| MYD-60KW | 60 kW | 90 A | 2–30 kHz |
| MYD-80KW | 80 kW | 120 A | 2–30 kHz |
| MYD-100KW | 100 kW | 150 A | 2–30 kHz |
| MYD-120KW | 120 kW | 180 A | 2–30 kHz |
Important: The published input-current figures are reference values from an existing MYD product listing. Actual supply current and protective-device sizing depend on the final electrical configuration, rated input conditions, power factor, efficiency, and applicable electrical standards.
Published MYD System Features
| Feature | Published Information | Selection Note |
|---|---|---|
| Input Supply | 3-phase 380 V standard on the referenced MYD listing | Alternative voltages require confirmation. |
| Line Frequency | 50/60 Hz | Confirm the destination electrical supply. |
| Output Frequency | 2–30 kHz | Actual operating point depends on the configuration. |
| Temperature Capability | Up to 900°C stated on the MYD listing | Actual workpiece capability requires verification. |
| Temperature Measurement | K-type thermocouple equipment listed | Confirm sensor rating, quantity, and calibration. |
| Temperature Recording | Multi-channel recording equipment listed | Confirm recorder configuration and data output. |
| Heating Cable | Flexible induction cable options | Confirm length, current capacity, and cooling method. |
| Insulation | High-temperature blankets listed as accessories | Select according to the thermal cycle. |
| Cooling | Configuration-dependent | Verify power-module and coil cooling separately. |
| Control | DSP and temperature-control features listed | Confirm recipe, alarm, and logging functions. |
Additional Power Ratings Referenced on This Product Page
The original product page also lists the following higher-power classes for induction PWHT applications:
| Reference Power Rating | Engineering Classification | Verification Status |
|---|---|---|
| 60 kW | Lower-power industrial PWHT class | MYD-60KW model also listed on the HLQ website |
| 80 kW | Medium-power industrial PWHT class | MYD-80KW model also listed on the HLQ website |
| 120 kW | Higher-power MYD configuration | MYD-120KW model listed on the HLQ website |
| 160 kW | Higher-power reference class | Final model and configuration require confirmation |
| 200 kW | Higher-power reference class | Final model and configuration require confirmation |
| 240 kW | Higher-power reference class | Final model and configuration require confirmation |
| 300 kW | High-power reference class | Final model and configuration require confirmation |
These reference power classes should not be interpreted as independently verified standard equipment models. Frequency range, dimensions, weight, operating temperature, cooling system, and control topology must be checked for the actual proposed configuration.
More information about published MYD induction heating systems is available in HLQ’s PWHT product information.
Recommended Model Selection for Pipeline Induction PWHT
Selecting an induction PWHT machine requires more than matching the equipment power rating to the pipeline diameter.
The correct configuration depends on the mass of steel being heated, the target thermal cycle, the geometry of the welded joint, the insulation system, the available electrical supply, and the required treatment productivity.
Preliminary Model Selection Guide
| System Rating | Potential Application | Selection Considerations |
|---|---|---|
| 40 kW | Selected smaller pipe joints or localized welding applications | Confirm heated mass, cycle time, and coupling. |
| 50 kW | Selected low-to-medium thermal-load applications | Check required heating width and insulation performance. |
| 60 kW | General industrial pipe heating and selected PWHT duties | Verify heating uniformity and available electrical power. |
| 80 kW | Higher thermal-load pipe weld applications | Evaluate pipe wall thickness and required heat-up rate. |
| 100 kW | Larger or heavier weld heating arrangements | Confirm coil cooling, duty cycle, and system matching. |
| 120 kW | Higher-power PWHT applications | Check zoning requirements and actual thermal demand. |
| 160–300 kW Reference Classes | Large-scale or high thermal-load industrial applications | Require individually engineered configuration and verified specifications. |
Selection Principle: These application descriptions are preliminary screening guidance, not guaranteed pipe-diameter or wall-thickness capacities.
Factors Affecting Required Heating Power
| Factor | Effect on Heating Requirements |
|---|---|
| Pipe Outside Diameter | Affects the heated surface area and steel mass. |
| Pipe Wall Thickness | Affects total heated mass and through-wall temperature response. |
| Heated Band Width | A wider heated zone requires more energy. |
| Target Temperature | A higher target temperature increases thermal energy demand. |
| Heating Time | A shorter permitted heat-up time increases required average heating power. |
| Thermal Insulation | Heat losses affect energy consumption and temperature distribution. |
| Coil Configuration | Influences electromagnetic coupling and local power distribution. |
| Ambient Conditions | Wind, temperature, and installation conditions affect losses. |
| Additional Heated Steel | Steel outside the nominal band also absorbs heat. |
Pipeline Induction PWHT Process Workflow
A properly controlled induction PWHT procedure follows a defined sequence from weld inspection and equipment installation to heat-treatment recording and final acceptance.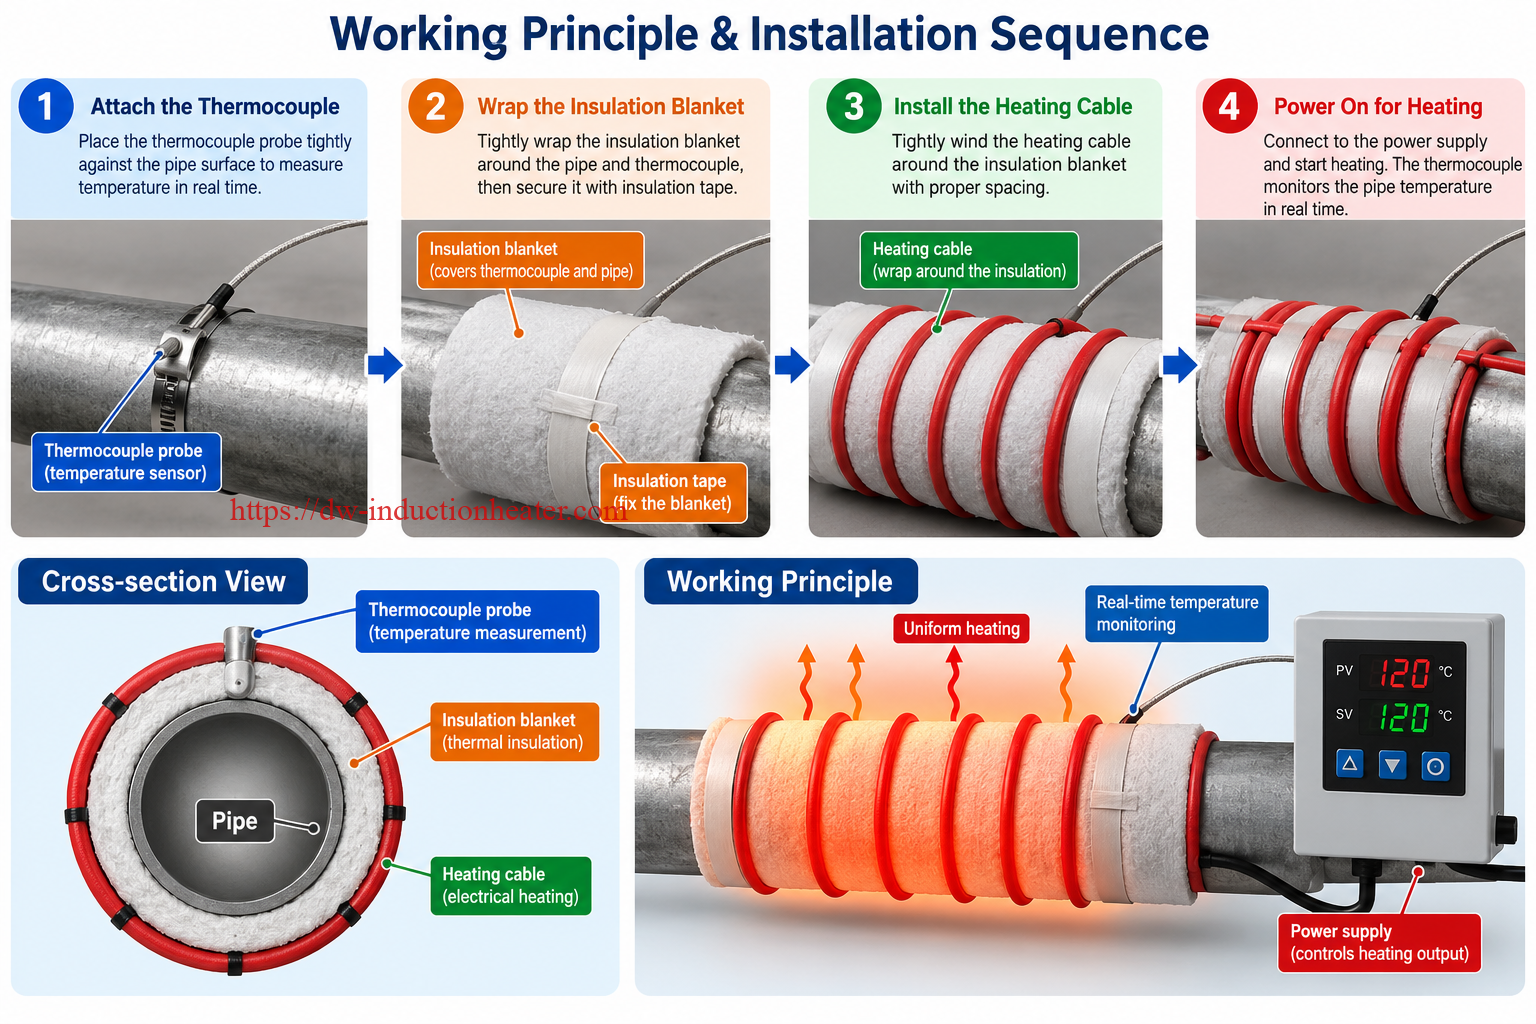
Step-by-Step PWHT Procedure
| Step | Operation | Quality Control Requirement |
|---|---|---|
| 1 | Review the Approved Procedure | Confirm material, weld details, code, temperature, heating band, and thermal cycle. |
| 2 | Inspect the Weld Area | Verify weld condition and required inspection status. |
| 3 | Install Thermocouples | Position and secure the required control and monitoring sensors. |
| 4 | Install Insulation | Apply the specified thermal insulation arrangement. |
| 5 | Install Induction Cable | Arrange cable turns according to the approved heating configuration. |
| 6 | Check Electrical and Cooling Systems | Verify connections, grounding, insulation condition, and cooling operation. |
| 7 | Program Temperature Cycle | Enter the approved heating, soaking, and cooling settings. |
| 8 | Perform Controlled Heating | Monitor temperature differences, alarms, and heating response. |
| 9 | Complete Soaking Stage | Verify that applicable measurement points meet the specified conditions. |
| 10 | Perform Controlled Cooling | Follow the required cooling profile and continue recording. |
| 11 | Review Temperature Records | Check deviations, completeness, and traceability. |
| 12 | Complete Final Inspection | Perform required examination and documentation according to the project procedure. |
Temperature Monitoring and Documentation
Accurate PWHT temperature monitoring requires appropriately selected and positioned sensors.
The number of thermocouples and their positions depend on the applicable procedure, pipe geometry, heating arrangement, and inspection requirements.
Temperature recording should preserve the relevant time-temperature history, including heating, soaking, controlled cooling, alarms, and deviations.
For pipeline construction projects requiring welding preheating before the PWHT stage, related pipeline preheating machines can be considered as part of the wider induction heating process.
Common Problems and Solutions in Induction PWHT
Successful post weld heat treatment depends on correct equipment operation, installation quality, measurement accuracy, and compliance with the approved procedure.
| Problem | Possible Cause | Recommended Engineering Action |
|---|---|---|
| Slow Heating Rate | Insufficient delivered power, poor coupling, excessive heat loss, or unexpectedly high heated mass. | Check actual output, cable arrangement, insulation, heated mass, and supply conditions. |
| Uneven Circumferential Temperature | Unequal coil spacing, inconsistent insulation, local geometry, or poor sensor positioning. | Review coil installation and perform temperature mapping before production. |
| Excessive Temperature Overshoot | Controller tuning, measurement delay, or excessive applied power. | Review control settings, power limits, and sensor installation. |
| Inadequate Through-Wall Temperature | Insufficient soak time or unsuitable heating configuration. | Verify through-wall thermal requirements and validate the process. |
| Thermocouple Reading Error | Poor attachment, damaged wiring, incorrect polarity, or calibration problems. | Inspect sensors, connections, recorder channels, and calibration records. |
| Induction Cable Overheating | Excessive current, unsuitable cable, poor cooling, or inadequate installation. | Stop operation and inspect cable ratings, cooling, and electrical matching. |
| Power Supply Alarm | Cooling fault, overcurrent, temperature protection, or other electrical fault. | Follow manufacturer troubleshooting procedures before restarting. |
| Cooling Rate Outside Procedure Limits | Insulation loss, ambient conditions, or unsuitable heating-power reduction. | Review thermal insulation and adjust the validated cooling strategy. |
| Incomplete Temperature Records | Recorder setup, sensor failure, power interruption, or logging error. | Investigate and document the deviation according to the quality procedure. |
| Temperature Differences Near Fittings | Changes in wall thickness, local mass, geometry, or thermal conductivity. | Consider a modified heating arrangement and additional measurement points. |
Engineering Selection Guide for Pipeline Induction PWHT Machines
1. Calculate the Mass of the Heated Pipe Section
For a straight steel pipe section, the approximate heated metal mass can be estimated using:
m = π × (D × t − t²) × L × ρ
Where:
- m = Heated steel mass, kg
- D = Pipe outside diameter, m
- t = Pipe wall thickness, m
- L = Assumed heated axial length, m
- ρ = Steel density, kg/m³
This formula estimates the mass of a cylindrical pipe-wall section. In a real PWHT operation, heat also spreads beyond the nominal heated band, so the effective heated mass may be greater.
2. Calculate the Required Thermal Energy
The simplified sensible-heat equation is:
Q = m × Cp × ΔT
Where:
- Q = Required thermal energy, kJ
- m = Heated steel mass, kg
- Cp = Assumed average specific heat capacity, kJ/(kg·K)
- ΔT = Temperature rise, K
For higher-accuracy engineering calculations, temperature-dependent material properties and additional heated components should be considered.
3. Calculate Preliminary Heating Power
An initial power estimate can be calculated as:
P = Q / (3600 × h × η)
Where:
- P = Estimated heating power, kW
- Q = Calculated energy, kJ
- h = Available heating time, hours
- η = Assumed overall net heat-delivery factor
The factor η is an engineering assumption for preliminary sizing and must not be interpreted as a guaranteed manufacturer efficiency.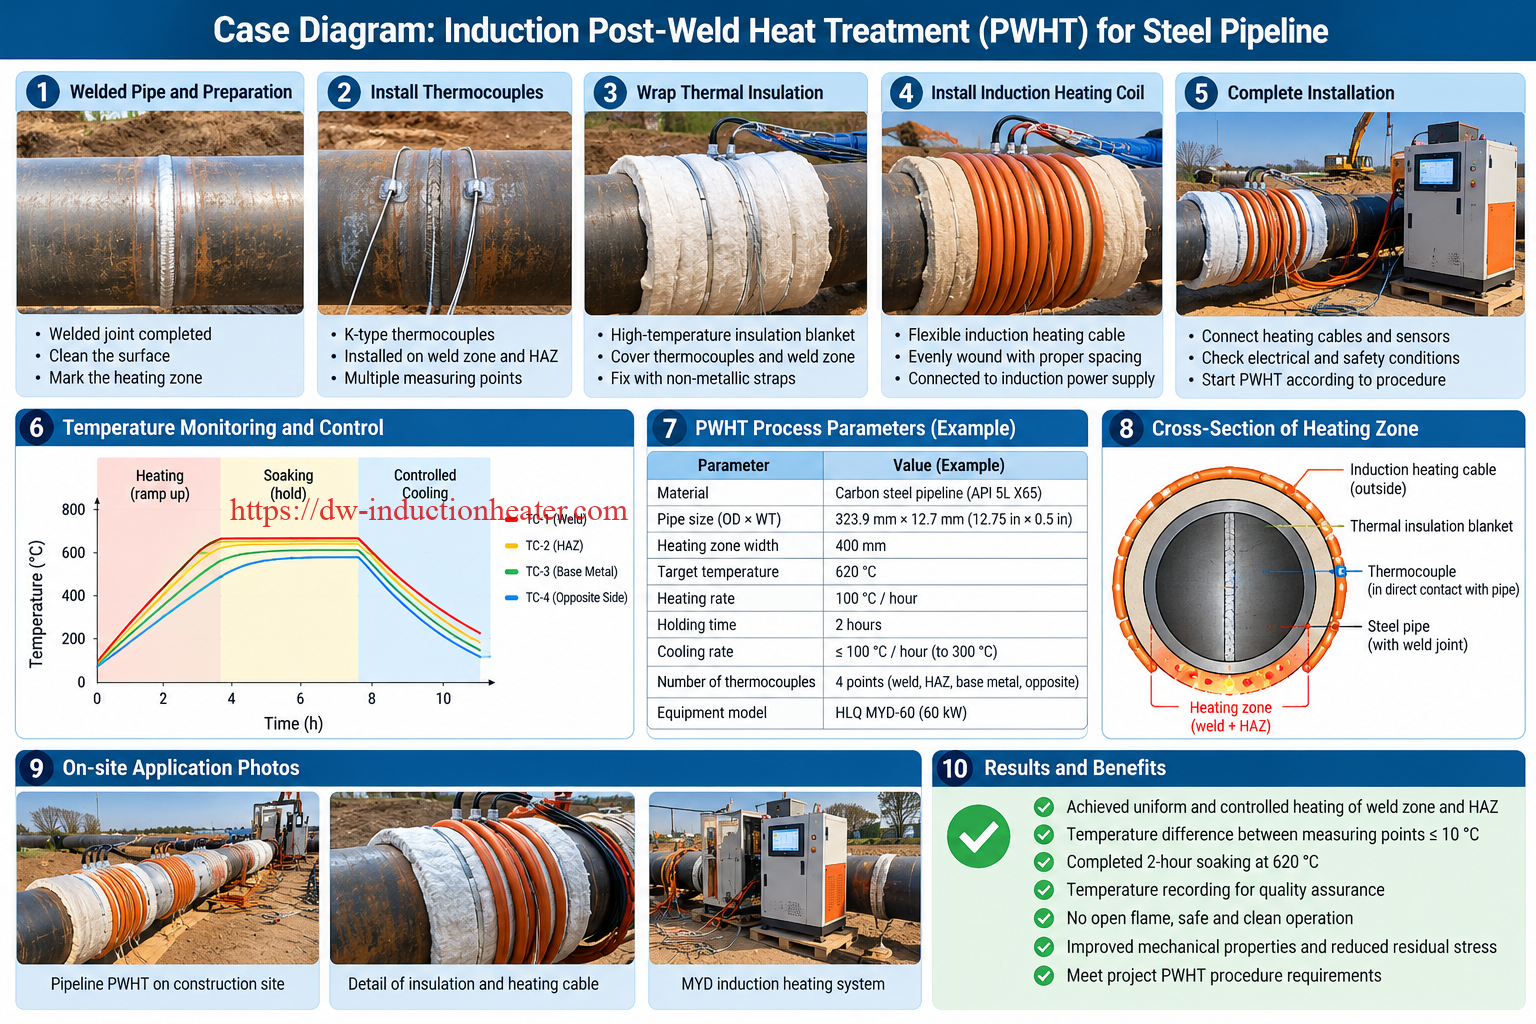
4. Worked Example: 20-Inch Carbon Steel Pipeline
Consider a preliminary engineering calculation for heating a steel pipe weld area.
| Parameter | Assumed Value |
|---|---|
| Pipe Outside Diameter | 508 mm |
| Wall Thickness | 12.7 mm |
| Nominal Heated Band Width | 300 mm |
| Material | Carbon Steel |
| Initial Temperature | 25°C |
| Illustrative Target Temperature | 650°C |
| Assumed Steel Density | 7,850 kg/m³ |
| Assumed Mean Specific Heat Capacity | 0.60 kJ/(kg·K) |
| Required Heat-Up Time | 35 minutes |
| Assumed Overall Net Heat-Delivery Factor | 60% |
5. Calculation Results
| Calculation | Result |
|---|---|
| Nominal Heated Steel Mass | Approximately 46.5 kg |
| Temperature Rise | 625 K |
| Calculated Sensible Heat | Approximately 17,452 kJ |
| Calculated Sensible Heat in kWh | Approximately 4.85 kWh |
| Ideal Average Heating Power | Approximately 8.3 kW |
| Power at Assumed 60% Net Heat Delivery | Approximately 13.9 kW |
Engineering Interpretation: The result represents a simplified average power estimate for the nominal pipe section only.
It does not account fully for axial heat conduction, additional heated pipe mass, local temperature variations, real insulation losses, coil matching, or all required operating margins.
A commercial power supply should therefore be selected using a more complete thermal assessment, appropriate engineering allowances, and practical heating trials.
For this illustrative geometry, a 40–60 kW MYD-class system may be a reasonable starting point for engineering evaluation, but suitability cannot be confirmed without checking the actual installation and thermal procedure.
6. Power Sensitivity to Heat-Delivery Assumptions
| Assumed Net Heat-Delivery Factor | Estimated Average Power |
|---|---|
| 40% | 20.8 kW |
| 50% | 16.6 kW |
| 60% | 13.9 kW |
| 70% | 11.9 kW |
These values illustrate the sensitivity of the simplified model to the assumed effective heat delivery. They are not published efficiency figures for any HLQ model.
7. Applicable Standards and Engineering Documentation
The correct heat-treatment procedure must follow the standards, material specifications, and project documents applicable to the specific welded joint.
| Standard or Document | Relevance | Important Qualification |
|---|---|---|
| ASME B31.3 | Process piping fabrication and heat treatment | Apply the relevant edition and material-specific requirements. |
| ASME B31.4 | Liquid pipeline transportation systems | Verify the applicable construction and welding provisions. |
| ASME B31.8 | Gas transmission and distribution piping | Review project-specific welding and heat-treatment requirements. |
| ASME Section VIII | Pressure vessel construction | Applicable where the project involves covered pressure vessels. |
| ASME Section IX | Welding and brazing qualifications | Use with the applicable construction code and qualified procedures. |
| Approved WPS / PWHT Procedure | Defines the required thermal treatment | The actual procedure governs operating parameters. |
| Project Inspection and Test Plan | Defines verification and documentation | Confirm witness points, records, and acceptance criteria. |
8. Essential Information for Equipment Selection
| Required Information | Engineering Purpose |
|---|---|
| Pipe Material Grade | Confirm electromagnetic and metallurgical requirements. |
| Pipe Outside Diameter | Determine cable installation geometry. |
| Pipe Wall Thickness | Estimate heated mass and through-wall thermal response. |
| Weld Joint Drawing | Determine the weld location and heating arrangement. |
| Target PWHT Temperature | Establish thermal energy requirements. |
| Required Heating Rate | Estimate installed power and control requirements. |
| Holding Time | Define continuous operation and insulation requirements. |
| Cooling Rate | Determine the required cooling strategy. |
| Heated and Soak Band Widths | Determine coil coverage and thermal distribution. |
| Number of Simultaneous Joints | Determine total power and independent heating requirements. |
| Electrical Supply | Confirm voltage, phases, frequency, and available capacity. |
| Working Environment | Review ambient conditions, ventilation, safety, and accessibility. |
| Documentation Requirements | Specify temperature logging, reports, and traceability. |
Advantages and Limitations of Induction PWHT
Main Advantages
| Advantage | Practical Benefit |
|---|---|
| Localized Heating | Heat can be applied to the required weld region without heating the entire structure in a furnace. |
| Programmable Temperature Control | The system can follow a defined thermal cycle when properly configured and validated. |
| Flexible Heating Cable | Suitable cable configurations can accommodate different pipe geometries. |
| No Combustion Flame at the Coil | Eliminates the need for a direct heating flame at the treated joint. |
| Potentially Reduced Setup Requirements | May avoid transporting large welded components to a fixed furnace. |
| Temperature Traceability | Compatible recording systems can document the treatment history. |
| Automation Capability | Programmable controllers can support repeatable operation. |
| Application Flexibility | Can be engineered for selected field and workshop heating tasks. |
Engineering Limitations
| Limitation | Engineering Consideration |
|---|---|
| Electromagnetic Coupling | Coil design and material properties affect achievable heating performance. |
| Temperature Uniformity | Requires careful cable arrangement, insulation, and monitoring. |
| Electrical Infrastructure | Power supplies require suitable incoming electrical capacity. |
| Complex Geometries | Branches, fittings, and irregular welds may require customized arrangements. |
| High-Temperature Accessories | Cables, insulation, and sensors must match the operating conditions. |
| Hazardous Locations | Electrical equipment must satisfy applicable site safety requirements. |
| Procedure Qualification | Heating capability alone does not demonstrate acceptable PWHT results. |
| Application-Specific Economics | Energy savings and cycle-time improvements require comparison under equivalent conditions. |
Induction PWHT vs. Resistance Heating vs. Furnace PWHT
| Comparison | Induction PWHT | Resistance Heating | Furnace PWHT |
|---|---|---|---|
| Heating Principle | Electromagnetic induction | Electrical resistance heating | Heating the component in a furnace environment |
| Localized Treatment | Yes | Yes | Dependent on furnace arrangement |
| Field Installation | Possible | Possible | Generally less convenient for fixed pipelines |
| Heating Flexibility | Depends on coil design | Depends on heating element layout | Depends on furnace dimensions |
| Temperature Recording | Available with suitable instrumentation | Available with suitable instrumentation | Available with suitable instrumentation |
| Heating Uniformity | Depends on design and validation | Depends on design and validation | Depends on furnace loading and validation |
| Relative Energy Consumption | Application-dependent | Application-dependent | Application-dependent |
| Preferred Selection Basis | Geometry, access, thermal cycle, and productivity | Geometry, access, thermal cycle, and productivity | Component dimensions and full-furnace treatment requirements |
Why Choose HLQ Induction PWHT Equipment?
HLQ Induction Equipment Co., Ltd. provides industrial induction heating equipment for applications including welding preheating, post weld heat treatment, induction hardening, induction brazing, and customized industrial heating.
For oil and gas pipeline projects, the principal engineering objective is to match the induction heating system to the actual pipe geometry, material, thermal cycle, and site operating requirements.
Engineering-Oriented Equipment Configuration
A complete pipeline induction PWHT solution may include the induction power supply, flexible heating cable, high-temperature insulation, temperature sensors, control equipment, and recording accessories.
The equipment arrangement should be selected according to the workpiece geometry and required heat-treatment procedure rather than nominal equipment power alone.
Flexible Industrial Heating Applications
HLQ induction heating technology can also be applied to related industrial tasks, including pipe heating, welding preheating, heat treatment of suitable fabricated components, and selected induction heating for pressure vessels.
Recommended Technical Evaluation
| Evaluation Item | Recommended Verification |
|---|---|
| Power Supply | Confirm the actual model rating and available site electrical capacity. |
| Operating Frequency | Verify the achievable operating range with the proposed coil arrangement. |
| Heating Cable | Confirm length, thermal rating, current capacity, and cooling requirements. |
| Temperature Monitoring | Confirm thermocouple inputs, calibration, and installation arrangement. |
| Temperature Control | Check programmable heating, soaking, and cooling capabilities. |
| Data Recording | Confirm required temperature records and export formats. |
| System Protection | Confirm applicable electrical, thermal, and cooling protection functions. |
| Application Testing | Validate actual performance using representative pipe geometry and procedures. |
A correctly engineered induction PWHT system combines suitable electrical power, effective electromagnetic coupling, reliable temperature measurement, thermal insulation, and an approved heat-treatment procedure.
10 Core FAQs About Induction PWHT Machines
1. What is an induction PWHT machine used for?
An induction PWHT machine is used to apply controlled heating to welded metal components after welding. In pipeline applications, it can perform a prescribed post weld heat treatment cycle at selected weld joints where such treatment is required by the applicable procedure.
2. How does induction post weld heat treatment work?
An induction power supply sends alternating current through a heating coil or flexible cable. The resulting electromagnetic field induces currents within the conductive pipe wall, generating heat. Thermocouples and a temperature controller help regulate and record the required thermal cycle.
3. What temperature is required for pipeline PWHT?
There is no universal PWHT temperature for all pipelines. The required temperature depends on the steel grade, construction code, welding procedure, wall thickness, and service conditions. A temperature in the approximate 600–700°C range may be relevant to certain steels and procedures, but it must not be applied automatically to every pipeline material.
4. How much power does a pipeline induction PWHT machine need?
Required power depends on pipe diameter, wall thickness, heated length, target temperature, heating rate, insulation, and heat losses. HLQ publishes MYD models rated from 40 kW to 120 kW, while larger reference power classes appear in related product information. Final selection requires engineering calculations and application verification.
5. Can induction PWHT be used for API 5L X65 and X70 pipelines?
These pipeline steels can be heated by induction. However, post weld heat treatment is not automatically necessary or appropriate for every X65 or X70 weld. The procedure must be evaluated against the material properties, welding qualification, applicable code, and project requirements.
6. Can a portable induction PWHT machine treat large-diameter pipes?
A portable induction heating system may be used on large-diameter piping when its heating cable, power rating, electrical supply, insulation, and temperature control arrangement are suitable. Pipe diameter alone is not sufficient to determine equipment capacity.
7. What is the difference between induction preheating and induction PWHT?
Preheating is normally performed before or during welding to establish specified welding temperature conditions. PWHT is performed after welding and follows a prescribed heating, soaking, and cooling cycle. Although both processes can use electromagnetic induction, their metallurgical objectives and control requirements differ.
8. Can induction PWHT reduce residual welding stresses?
A properly specified and performed stress-relief heat-treatment cycle can reduce residual stresses in suitable materials. The outcome depends on temperature, holding time, material behavior, geometry, and procedure qualification. Induction is the heating method used to deliver the prescribed cycle.
9. Is induction PWHT more energy-efficient than resistance heating?
Induction heating can provide efficient localized energy transfer, but actual energy consumption depends on the complete installation. A valid comparison must consider the same workpiece, thermal cycle, insulation, heating time, and measured electrical input. No universal energy-saving percentage applies to every PWHT application.
10. What information is required to select an induction PWHT system?
The essential information includes pipe material, outside diameter, wall thickness, weld geometry, target PWHT temperature, permitted heating and cooling rates, holding time, heated-band dimensions, number of joints, site electrical supply, ambient conditions, and required temperature recording.