

Induction Brazing HVAC Pipes
Induction Brazing HVAC Pipes
Quick Answer: What Is Induction Brazing for HVAC Pipes?
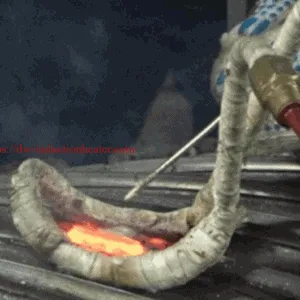
Induction brazing for HVAC pipes is a flameless metal-joining process that uses electromagnetic induction to rapidly heat copper tubes, brass fittings, compressor connections, evaporator lines and condenser assemblies to brazing temperature. The brazing filler metal melts and flows into the joint by capillary action while the copper or other base materials remain solid. Compared with manual torch brazing, induction heating provides repeatable heating time, localized heat input and easier integration into automated HVAC and refrigeration production lines.
Induction Brazing HVAC Pipes and Copper Tubing
HVAC and refrigeration systems contain many brazed tube connections that must provide reliable mechanical strength and sealing performance under changing operating temperatures and pressures.
Typical HVAC brazing applications include:
- copper tube-to-copper tube joints
- copper tube-to-brass fittings
- condenser tube connections
- evaporator tube connections
- compressor inlet and outlet tubing
- distributor and valve connections
- heat exchanger assemblies
- refrigeration copper piping
Refrigeration piping is always brazed as brazing makes a very solid leak-free joint that withstands high and low temperatures and pressures. When soldering refrigeration pipe it is best to use solder which has a composition of silver in it as the silver bounds with the copper and makes for an excellent leak free strong joint (capillary attraction).
HLQ Induction are experts at devising customized induction heating solutions for brazing of compressor parts, heating elements and heat distributors.
Air conditioners have several parts that are brazed. The most common materials are copper and aluminium:
Aluminium parts, for example evaporator and condenser connections (tube-to-tube, tube-to-block, tube-to-tank)
Tube-to-fittings on the condenser unit
Tube-to-fittings on the evaporator unit
Tube-to-fittings on the compressor
Tube-to-valves in distribution systems
Induction Brazing is similar to soldering except the temperature is above 800 degreesF.
For copper, the brazing compound most commonly used is commonly called sil-phos as seen on the left.
There are several types of this compound.
15% Phosphorus/Copper/Silver Alloy is one type that uses 15% silver and is the standard for service techs doing repairs of refrigeration equipment.5% Phosphorus/Copper/Silver Alloy is another compound that is cheaper and some say works well for repairs. It does not work as well as 15%.
There is also a Phosphorus/Copper Alloy with no silver that I find to be largely useless for repairs.
Copper Brazing for the HVAC Industry
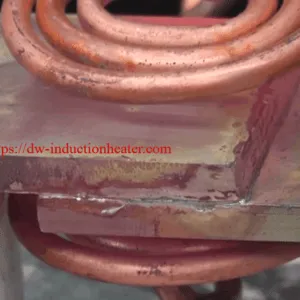
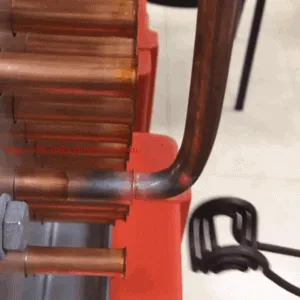
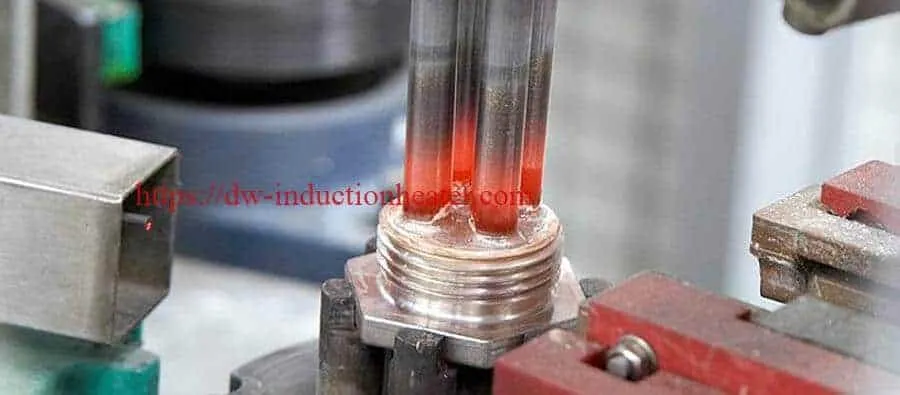
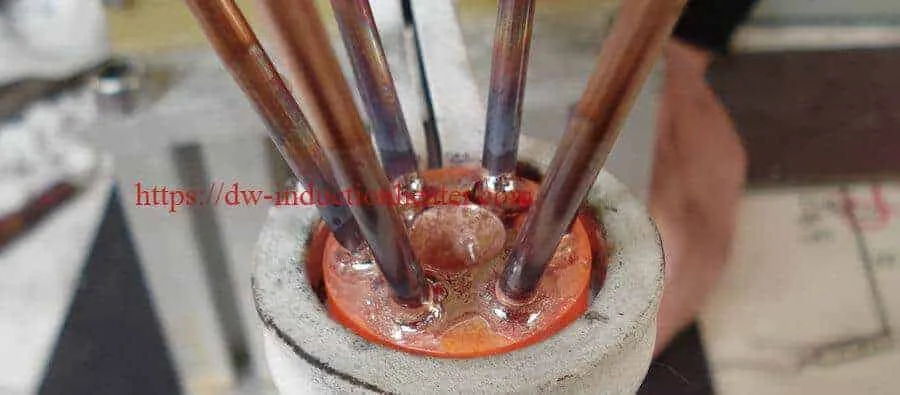
Multiple copper tubes silver brazed by MSI Automation’s proprietary induction brazing technology.Induction heating with the proper induction heating coil technology can silver braze multiples of copper tube ends in one shot. This procedure eliminates tedious hand torch brazing, improves consistency and reduces the chance of leaking connections. 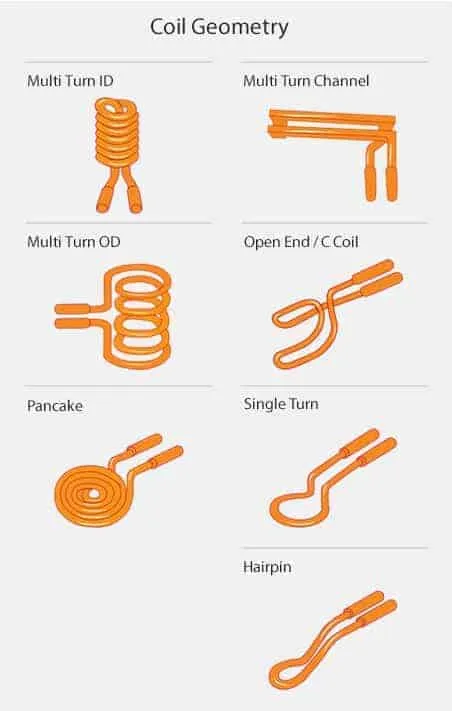
Joint brazed between the copper tube and brass body is complete. Heating time using MSI’s special induction heating coil is 1/4 that of conventional round copper tube coil designs.
How Induction Brazing Works for HVAC Tubing
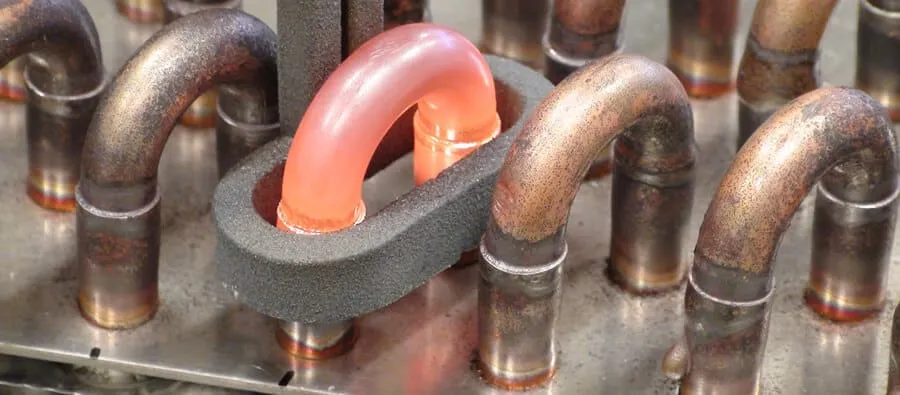
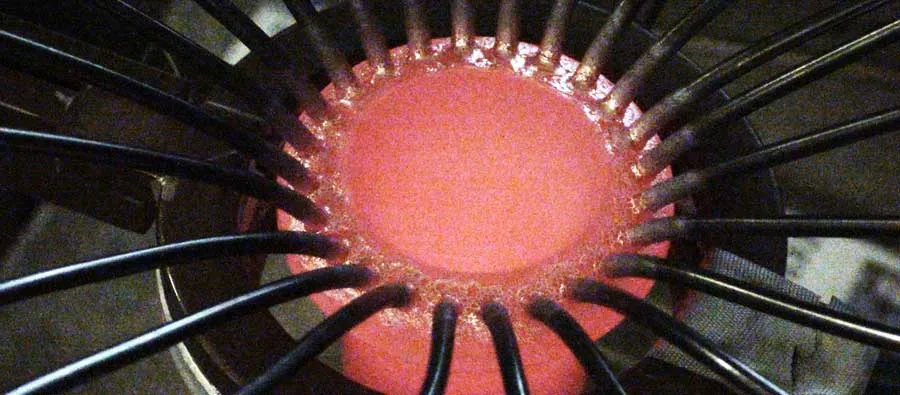
An induction brazing machine sends high-frequency alternating current through a specially designed induction coil. The coil generates an alternating magnetic field around the HVAC tube joint, inducing electrical currents in the conductive metal and producing localized heat.
When the joint reaches the required brazing temperature, the selected brazing filler metal melts and is drawn into the joint clearance by capillary action. The base materials themselves are not melted.
This makes induction brazing fundamentally different from welding and also distinguishes brazing from lower-temperature soldering.
For copper HVAC assemblies, filler-metal selection should be based on:
base materials → joint design → operating pressure → operating temperature → applicable HVAC/refrigeration standards → production requirements.
Technical Table
HVAC Pipe Induction Brazing Technical Parameters
| Parameter | Typical / Application Information |
|---|---|
| Application | HVAC and refrigeration pipe brazing |
| Typical Base Materials | Copper, brass, steel and suitable aluminum assemblies |
| Common Joint Types | Tube-to-tube, tube-to-fitting, tube-to-valve, tube-to-compressor |
| Heating Method | Electromagnetic induction |
| Brazing Definition | Filler metal liquidus above 450°C / 840°F |
| Typical Process Temperature | Determined by filler alloy and base material |
| Typical Copper HVAC Example | Approx. 700–800°C |
| Reference Power | 6–15 kW in documented small copper-tube applications |
| Reference Heating Time | Approx. 5–20 seconds per joint in documented applications |
| Coil Type | C-coil, U-coil, helical coil or custom-shaped coil |
| Filler Metal | Cu-P, Cu-P-Ag, silver brazing alloy, application dependent |
| Temperature Control | Time control, pyrometer or thermocouple |
| Cooling | Water-cooled induction power supply / coil |
| Operation | Manual, handheld, semi-automatic or robotic |
| Production Integration | HVAC assembly lines, heat exchanger lines, compressor manufacturing |
How to Select an Induction Brazing Machine for HVAC Pipes
For a new HVAC brazing project, equipment power should not be selected from pipe diameter alone.
Customers should provide:
| Required Information | Example |
|---|---|
| Tube Material | Copper / brass / steel / aluminum |
| Tube OD | mm or inch |
| Tube Wall Thickness | mm |
| Fitting Material | Copper / brass / steel |
| Joint Geometry | Tube-to-tube / tube-to-fitting |
| Brazing Alloy | Cu-P / Cu-P-Ag / Ag-based alloy |
| Required Heating Time | seconds |
| Production Rate | joints/hour |
| Operation | Manual / automatic |
| Coil Access | 360° / side access |
| Electrical Supply | Voltage / Hz / Phase |
| Cooling Conditions | Water chiller / cooling tower |
FAQ
1. Can induction heating be used to braze copper HVAC pipes?
Yes. Induction heating is well suited for copper tube-to-tube and tube-to-fitting brazing. A properly designed coil heats the joint area rapidly while the selected filler metal flows through the joint by capillary action. HLQ has documented copper-pipe applications using induction brazing for HVAC, refrigeration and heat-exchanger assemblies.
2. What temperature is required for induction brazing HVAC copper pipes?
The correct temperature depends on the brazing filler metal and base materials. Brazing is defined as a joining process using filler metal with a liquidus above 450°C (840°F). Actual copper HVAC brazing processes commonly operate higher; HLQ’s documented copper-pipe examples include approximately 700–800°C.
3. How long does induction brazing a copper pipe take?
Heating time depends on tube diameter, wall thickness, fitting mass, coil coupling, power and brazing alloy. HLQ’s documented examples range from approximately 5 seconds per joint for one heat-exchanger application to approximately 20 seconds for another copper-pipe application. These values should be treated as application examples rather than universal cycle times.
4. What brazing alloy is suitable for copper HVAC tubing?
Copper-phosphorus and copper-phosphorus-silver filler metals are commonly associated with copper brazing applications. The correct alloy should be selected according to the base metals, service conditions, joint design and applicable refrigeration or HVAC requirements. Your current page already discusses phosphorus/copper/silver filler alloys for copper HVAC joints.
5. Is induction brazing better suited to automated HVAC production than torch brazing?
Induction brazing can be highly suitable for automated production because heating time, power and workpiece position can be programmed and repeated. It can also be integrated with robotic movement, filler feeding and shielding-gas systems. Whether it is preferable to torch brazing depends on production volume, joint access, required flexibility and capital cost. Induction brazing copper to copper pipes
6. What induction coil is suitable for HVAC pipe brazing?
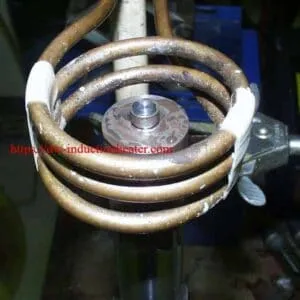
Coil design depends on the pipe diameter, joint geometry and available access. Common configurations include C-shaped, U-shaped and helical coils. For production lines, custom coils can be designed to heat one or several joints while minimizing heat exposure to surrounding components.