Induction Annealing Copper Tube
Copper Tube Induction Annealing: Localized End Softening, DW-HF-45 Equipment and Engineering Guide
Quick Answer
Copper tube induction annealing is a heat-treatment process that uses electromagnetic induction to heat a selected section of copper tubing. It can be used to soften cold-worked tube ends while limiting thermal exposure to the adjacent material.
The original HLQ application describes localized annealing at both ends of a copper tube measuring 1.625 inches (41.275 mm) in outside diameter and 24 inches (609.6 mm) in overall length. The intended softened zone extends 1.5 inches (38.1 mm) from each end.
The published equipment configuration identifies a DW-HF-45 induction heating system operating at 60 kHz, a remote workhead containing eight 1.0 µF capacitors, and a four-turn helical induction coil.
The published process specifies a target temperature of 1500°F (approximately 815.6°C), a heating duration of 7.5 seconds per end, and a 180-degree tube rotation after 3.75 seconds. Rapid cooling is applied after heating before the opposite end is processed.
Technical verification: These are values published on the original application page, not independently verified HLQ performance-test results. The copper grade, wall thickness, initial temper, actual temperature distribution, final hardness and hardness-transition length are not documented.
The published heating temperature is higher than the conventional soft-annealing ranges commonly specified for unalloyed copper. Therefore, a qualified process requires material-specific temperature control, confirmation of the resulting microstructure, and hardness measurements along the tube.
Unlike the quench hardening of steel, rapid cooling does not re-harden ordinary unalloyed copper. Its purpose in this application is to limit further thermal exposure beyond the targeted heating zone.
Table of Contents
- What Is Copper Tube Induction Annealing?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages and Limitations
- Why Choose HLQ?
- 6 Core FAQs
What Is Copper Tube Induction Annealing?
Copper tube induction annealing is an electromagnetic heating application used to modify the mechanical properties of copper tubing through a controlled temperature-time cycle.
Copper becomes stronger and less ductile during cold-working processes such as drawing, rolling and forming. Annealing can reverse some of these effects by promoting recovery and recrystallization, depending on the material condition and heating cycle.
For applications requiring localized softening, induction heating can concentrate energy around a selected section rather than heating the entire tube in a furnace.
The main engineering objectives may include restoring ductility, reducing hardness in the selected region and preparing the material for subsequent forming operations.
However, localized induction heating does not automatically guarantee that the neighboring material remains in its original temper.
The final hardness distribution depends on the copper grade, previous cold work, heating temperature, exposure duration, thermal conductivity and cooling conditions.
For the broader metallurgical process, see the induction annealing process.
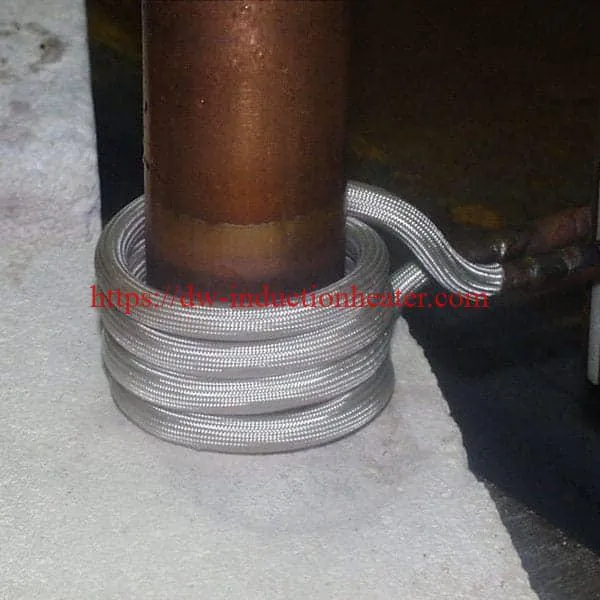
Original Copper Tube Induction Annealing Photograph

Localized End Annealing Versus Full-Length Tube Annealing
| Characteristic | Localized Copper Tube End Annealing | Full-Length Copper Tube Annealing |
|---|---|---|
| Heating region | Selected length near one or both tube ends | The specified length or complete tube |
| Primary objective | Obtain a specified local soft condition | Obtain a specified temper throughout the treated length |
| Typical equipment arrangement | Localized induction heating station | Continuous or batch annealing system |
| Temperature uniformity | Required within the specified local treatment zone | Required throughout the specified full treatment region |
| Hardness-transition zone | Must be characterized between treated and untreated material | Generally less relevant when the entire tube is treated |
| Cooling | May be used to limit further heat spreading | Defined by material and process requirements |
| Quality verification | Local hardness, treated length, tube geometry and surface condition | Temper, mechanical properties and uniformity along the treated tube |
A short induction heating pulse may be appropriate for some localized operations, but final process qualification must be based on the required material properties rather than heating time alone.
Key Applications
1. Localized Annealing of Copper Tube Ends
The primary application described on this page is localized heating of both ends of a copper tube.
The published objective is to produce a softened region extending approximately 38.1 mm from each tube end while minimizing changes in the adjacent hard-drawn material.
This requires careful control of the temperature distribution and a defined method of measuring the final hardness-transition profile.
The original page does not supply quantitative hardness measurements before or after processing.
2. Preparing Copper Tube Ends for Forming
Cold-worked copper tube ends may require improved ductility before selected forming operations.
Depending on the tube dimensions and product requirements, localized softening may be evaluated before end expansion, flaring or other forming operations.
The suitability of induction heating must be confirmed for the actual tube grade, starting temper and forming requirements.
3. Copper Tubing Used in Heat-Exchange Equipment
Copper tubing is widely used in heat exchangers, heating equipment and refrigeration-related systems.
Some manufacturing operations require controlled tube-end properties or dimensional preparation before subsequent joining or forming.
Where localized annealing is required, the heating zone and final material condition should be specified independently of any subsequent brazing or joining process.
4. Industrial Copper Pipe and Tube Manufacturing
Induction annealing can be evaluated as part of industrial tube-processing operations involving cold-worked copper products.
Potential manufacturing advantages depend on the required annealed length, tube geometry, process time, heating efficiency and quality requirements.
These advantages must be demonstrated for the individual production line rather than assumed from a published heating-cycle duration.
5. Automated Copper Tube Processing
A localized induction heating station may be combined with tube positioning, controlled rotation, temperature measurement, cooling and handling equipment.
Automated processing can help control the sequence of heating and cooling operations, provided that the mechanical arrangement and thermal process have been validated.
The original page does not provide a verified automated production capacity.
Suitable Materials
The original application identifies the workpiece only as a copper tube. It does not specify the copper alloy designation, original temper or wall thickness.
This information is essential because annealing response depends on copper composition and the amount of previous cold work.
Common Copper Grades Relevant to Tube Manufacturing
| Copper Grade | UNS Designation | Material Description | Heat-Treatment Consideration |
|---|---|---|---|
| Cu-ETP | C11000 | Electrolytic tough-pitch copper | Softening behavior depends on cold work, temperature and atmosphere |
| Cu-OF | C10200 | Oxygen-free copper | Can be annealed using an appropriate material-specific process |
| Cu-DLP | C12000 | Phosphorus-deoxidized copper with low residual phosphorus | Follow the applicable material and tube specification |
| Cu-DHP | C12200 | Phosphorus-deoxidized high-residual-phosphorus copper | Common copper tubing material; annealing requirements depend on temper |
| Unspecified copper tube | Not provided | Original HLQ application material | Grade identification required before final thermal-process qualification |
These grades are published copper material designations. The original application does not establish which grade was used.
Published Copper Soft-Annealing Reference Temperatures
The following values are published by the German copper industry organization Kupferverband. They describe reference heat treatments for selected copper materials.
| Material | Published Soft-Annealing Temperature | Published Conventional Batch Holding Time |
|---|---|---|
| Cu-ETP / Cu-FRHC | 300–650°C | 0.5–3 hours |
| Cu-OF | 425–650°C | 0.5–3 hours |
| Cu-PHC / Cu-HCP | 350–650°C | 0.5–3 hours |
| Cu-DHP | 350–650°C | 0.5–3 hours |
| Original published tube application | 815.5°C | 7.5 seconds heating per end |
Important: The first four rows are conventional material-reference schedules, not recommended settings for the original seven-and-a-half-second induction heating cycle.
Rapid induction heating and conventional batch annealing have different temperature-time histories.
The published 815.5°C target is above the conventional reference ranges shown for common unalloyed copper grades. The original process must therefore be independently validated for grain size, hardness, surface oxidation and dimensional stability.
Reference: Kupferverband — Heat Treating Copper Materials.
Copper Tube Temper Conditions
Commercial copper tubing is supplied in different temper conditions according to the applicable product specification.
| Temper Designation | Description | Engineering Relevance |
|---|---|---|
| O50 | Light annealed | Defines a specified annealed condition under applicable standards |
| O60 | Soft annealed | Defines a softer annealed temper for applicable copper tube products |
| H58 | Drawn general purpose | Represents a cold-worked condition for specified copper tube products |
Exact acceptance requirements vary by standard, grade and tube dimensions.
The Copper Development Association identifies ASTM B68 and ASTM B88 among the standards used for seamless copper tubing and discusses the different annealed and drawn conditions.
Reference: Copper Development Association — Copper Tube and Pipe Standards.
Working Principle
Induction heating uses electromagnetic energy to generate heat within an electrically conductive workpiece.
For copper tube end annealing, an alternating current passes through a specially designed induction coil surrounding the selected tube region.
Electromagnetic Heating Sequence
- The induction power supply converts incoming electrical energy into high-frequency alternating current.
- The current passes through the matching workhead and induction heating coil.
- An alternating magnetic field develops around the coil.
- The magnetic field induces electrical currents within the copper tube wall.
- Electrical resistance converts induced-current energy into heat.
- Heat spreads through the tube wall and into adjacent material by thermal conduction.
- The temperature-time profile produces the required softening only if the copper grade and thermal conditions are suitable.
Copper has high electrical and thermal conductivity. Efficient induction heating therefore requires suitable coil coupling, adequate electrical power and controlled heating duration.
Thermal conductivity also makes it necessary to consider heat spreading away from the intended annealing zone.
Additional explanations are available in the induction heating fundamentals.
Original Four-Turn Helical Coil Arrangement
The original application specifies a four-turn helical induction coil positioned around one end of the copper tube.
The published process includes a 180-degree tube rotation halfway through the heating interval.
The purpose of the rotation is to support more even circumferential heating.
However, a 180-degree rotation alone does not prove that the complete tube circumference or wall thickness reaches a uniform temperature.
Heating uniformity should be confirmed by suitable temperature measurements and subsequent material testing.
Important Engineering Factors
| Parameter | Effect on Heating | Engineering Consideration |
|---|---|---|
| Operating frequency | Influences induced-current distribution and electromagnetic penetration | Match the frequency to tube geometry and electrical properties |
| Coil diameter | Influences electromagnetic coupling | Maintain appropriate coil-to-tube clearance |
| Number of turns | Affects coil inductance and matching requirements | Verify compatibility with the selected workhead |
| Tube wall thickness | Determines thermal mass and through-wall heat distribution | Obtain actual wall thickness before equipment sizing |
| Effective heated length | Determines the volume receiving substantial thermal energy | Match coil geometry and power application to the treatment zone |
| Applied power | Influences heating rate | Measure temperature rather than assuming fixed efficiency |
| Heating time | Controls exposure duration and thermal diffusion | Validate the complete time-temperature cycle |
| Tube rotation | Can alter circumferential exposure to the heating field | Validate the final temperature and hardness uniformity |
| Cooling timing | Limits continued thermal exposure after heating | Optimize cooling without unacceptable distortion |
Correct induction heating coil design is essential for controlling the heating region and achieving repeatable process conditions.
Technical Specifications
Original HLQ Published Copper Tube Application
The following information preserves the technical values published on the existing HLQ product page.
| Parameter | Original Published Value | Verification Status |
|---|---|---|
| Application | Induction annealing copper tube | Original page |
| Heat-treatment objective | Localized softening of both tube ends | Published objective |
| Copper alloy grade | Not specified | Material identification required |
| Tube outside diameter | 1.625 inches / 41.275 mm | Published dimension |
| Tube overall length | 24 inches / 609.6 mm | Published dimension |
| Targeted annealing length | 1.5 inches / 38.1 mm per end | Published objective; final measured zone not provided |
| Tube wall thickness | Not specified | Required for thermal-load calculation |
| Target temperature | 1500°F / approximately 815.6°C | Published target; actual measurement method not provided |
| Operating frequency | 60 kHz | Published value |
| Equipment designation | DW-HF-45kW | Original model description |
| Workhead capacitance | Eight 1.0 µF capacitors | Published configuration |
| Total nominal capacitance | 8.0 µF | Published value; electrical circuit must be verified |
| Induction coil | Four-turn helical coil | Published configuration |
| Heating duration | 7.5 seconds per end | Published heating time |
| Tube rotation | 180 degrees after 3.75 seconds | Published sequence |
| Post-heating cooling | Immediate water cooling | Published procedure |
| Opposite-end treatment | Tube flipped and process repeated | Published sequence |
| Original temper | Not provided | Required to assess hardness retention |
| Final hardness | Not provided | Requires testing |
| Actual annealed length | Not measured in published information | Requires hardness-profile verification |
| Production capacity | Not provided | No verified throughput available |
Published DW-HF-45 Equipment Specifications
The current HLQ DW-HF-45 equipment page provides the following nominal equipment information.
| Equipment Parameter | Published Specification | Engineering Note |
|---|---|---|
| Model | DW-HF-45KW | Published model designation |
| Maximum oscillation capacity | 45 kVA | Not equal to verified workpiece heating power |
| Frequency range | 30–80 kHz | Includes the original 60 kHz setting |
| Input electrical supply | Three-phase 380 V, 50–60 Hz | Confirm actual voltage configuration |
| Maximum input apparent power | 50 kVA | Published electrical rating |
| Oscillating current | 15–90 A | Published equipment range |
| Cooling-water flow | At least 6 L/min in the published specification | Confirm operating pressure and cooling requirements |
| Main equipment dimensions | 550 × 240 × 535 mm | Published main-unit dimensions |
| Extension dimensions | 470 × 265 × 440 mm | Published extension dimensions |
| Interconnecting cable length | 2 m | Published value |
Reference: HLQ DW-HF-45KW Induction Heating Equipment.
Power-rating clarification: The 45 kW model name and the published 45 kVA maximum oscillation capacity should not be treated as proof of 45 kW thermal power absorbed by the copper tube.
Copper Heat-Treatment Reference Comparison
| Treatment Condition | Temperature | Source / Status |
|---|---|---|
| Cu-ETP conventional soft annealing | 300–650°C | Kupferverband material reference |
| Cu-OF conventional soft annealing | 425–650°C | Kupferverband material reference |
| Cu-DHP conventional soft annealing | 350–650°C | Kupferverband material reference |
| Original short-duration induction application | 815.6°C | Original page value; process qualification unavailable |
| Pure copper melting point | 1084.62°C | Published physical property, not an annealing setting |
The published application temperature is considerably higher than conventional copper soft-annealing reference temperatures.
This does not automatically make the short-duration application impossible, but it makes temperature measurement, grain-size evaluation and dimensional inspection especially important.
Recommended Model Selection
Equipment selection for copper tube end annealing depends on the tube dimensions, copper grade, original temper, target softened length, required heating time, electromagnetic coupling and cooling requirements.
The original page identifies a DW-HF-45 induction heating system operating at 60 kHz.
That frequency lies within the currently published 30–80 kHz operating range of the DW-HF-45 series.
Published HLQ Equipment Options
| Equipment Model | Published Nominal Capacity | Published Frequency Range | Selection Assessment |
|---|---|---|---|
| DW-HF-25 series | 25 kVA | 20–80 kHz in the published equipment summary | Alternative for engineering evaluation; insufficient evidence to establish suitability for the original heating duty |
| DW-HF-45 | 45 kVA | 30–80 kHz | Original application series and primary model for verification |
| DW-HF-60 | 60 kVA | 30–80 kHz | Higher-capacity alternative; final suitability and thermal performance require testing |
These values are published HLQ equipment ratings, not verified copper tube annealing capacities.
Increasing nominal equipment capacity does not automatically improve temperature uniformity or reduce the hardness-transition length.
For additional equipment ranges, see the induction heating power supply selection guide.
Required Data for Final Equipment Selection
| Required Parameter | Purpose |
|---|---|
| Copper alloy grade | Determine material properties and appropriate thermal cycle |
| Original temper | Establish starting hardness and cold-work condition |
| Tube outside diameter | Determine coil clearance and workpiece geometry |
| Tube wall thickness | Determine the mass of the heated section |
| Target annealed length | Define heating-zone and hardness-transition requirements |
| Required final hardness | Establish process acceptance criteria |
| Maximum acceptable transition length | Define allowable thermal influence outside the target region |
| Heating cycle | Establish generator and coil requirements |
| Cooling procedure | Control the post-heating thermal history |
| Production throughput | Determine equipment duty cycle and station arrangement |
| Electrical supply | Verify generator compatibility |
| Cooling-water supply | Verify coil and equipment cooling requirements |
Process Workflow
The original application processes the two ends of a copper tube sequentially.
The following workflow preserves the published heating sequence while adding the verification steps required for a controlled industrial process.
Step 1 — Material Identification and Inspection
Confirm the copper alloy designation, initial temper, tube outside diameter, wall thickness and overall length.
Inspect the tube for existing damage, contamination and dimensional nonconformity.
Step 2 — Position the First Tube End
Place one end of the copper tube inside the induction coil.
Establish the required position relative to the coil and maintain suitable mechanical clearance.
Step 3 — Apply the Initial Heating Interval
The original application specifies 3.75 seconds of heating before rotating the tube.
The electrical settings and workpiece temperature should be verified during process development.
Step 4 — Rotate the Tube
Rotate the tube 180 degrees as described in the original application.
Continue heating for the remaining 3.75 seconds, completing the published 7.5-second heating period for the first end.
The purpose of rotation is to improve circumferential heating consistency, but actual uniformity must be confirmed by measurement.
Step 5 — Apply Rapid Cooling
The original process specifies immediate water cooling after heating.
Rapid cooling can limit additional thermal exposure and reduce further heat spreading into neighboring material.
For ordinary non-hardenable copper grades, water cooling does not create the martensitic hardening effect associated with steel quenching.
Step 6 — Flip and Process the Opposite End
Reposition the copper tube so that the opposite end can be treated.
Repeat the heating, rotation and cooling sequence using the validated process settings.
Step 7 — Final Inspection
Measure the final treated-zone length, hardness distribution, roundness, surface condition and any additional properties required by the tube specification.
Compare the hardness of the annealed section, transition region and untreated tube body.
Process Validation and Quality Control
| Inspection Point | Required Measurement or Record | Reason |
|---|---|---|
| Incoming material | Alloy grade and initial temper | Confirm the correct material condition |
| Tube dimensions | Outside diameter, wall thickness and length | Establish geometry and heating load |
| Coil positioning | Insertion depth and clearance | Improve process repeatability |
| Electrical settings | Frequency, power setting and heating time | Document the applied heating cycle |
| Temperature measurement | Surface temperature at defined locations | Verify the thermal profile |
| Cooling | Cooling timing and relevant water conditions | Control post-heating thermal exposure |
| Annealed-zone hardness | Appropriate hardness measurement | Verify the required softening |
| Adjacent-zone hardness | Hardness measurements beyond the targeted zone | Check preservation of the original temper |
| Dimensional inspection | Roundness, straightness and diameter | Identify possible thermal distortion |
| Surface inspection | Oxidation, discoloration and surface condition | Verify product acceptability |
Common Problems and Solutions
| Problem | Possible Cause | Recommended Engineering Action |
|---|---|---|
| Annealed zone extends beyond the target | Excessive heating duration, thermal conduction or delayed cooling | Review temperature-time profile, coil design and cooling sequence |
| Insufficient softening | Inadequate thermal exposure or unsuitable initial material condition | Verify copper grade, temperature distribution and hardness response |
| Uneven circumferential heating | Coil misalignment or nonuniform electromagnetic coupling | Improve positioning and verify the temperature distribution |
| Uneven tube-wall heating | Insufficient thermal diffusion or unsuitable frequency and power settings | Evaluate through-wall temperature response and adjust the heating cycle |
| Excessive grain growth | High-temperature exposure beyond the required treatment | Review the thermal cycle and perform metallographic evaluation where required |
| Excessive oxidation | High-temperature exposure in an unsuitable atmosphere | Review temperature, exposure duration and atmosphere requirements |
| Tube distortion | Thermal gradients, mechanical restraint or uneven cooling | Optimize support, temperature distribution and cooling |
| Inconsistent hardness | Variations in initial temper, heating or cooling | Improve material traceability and process control |
| Incorrect temperature readings | Emissivity variation, oxidation or unsuitable sensor positioning | Validate the temperature measurement method |
| Coil overheating | Inadequate cooling-water flow or unsuitable operating conditions | Inspect the cooling system and verify equipment limits |
| Unstable resonant matching | Coil or workhead electrical mismatch | Verify the coil and capacitor configuration |
Engineering Selection Guide
1. Confirm the Copper Grade
Identify the exact alloy and material specification.
Common copper tube grades include C11000, C10200, C12000 and C12200, but the original application does not identify which grade was used.
2. Confirm the Original Temper
Determine whether the incoming tube is hard drawn, light annealed, soft annealed or another specified condition.
The initial hardness and amount of previous cold work affect recrystallization behavior and the required thermal cycle.
3. Define the Required Softened Zone
Specify the intended softened length at each tube end.
For the original application, the published target is 38.1 mm per end.
The definition of the acceptable transition region must also be established, because the temperature distribution cannot change instantaneously at the boundary of the treated zone.
4. Determine the Heated Mass
The mass of the heated tube section depends on outside diameter, inside diameter, heated length and material density.
For a cylindrical tube:
m = ρ × π × (Do² − Di²) × L / 4
Where:
- m = mass of the tube section, kg
- ρ = copper density, kg/m³
- Do = outside diameter, m
- Di = inside diameter, m
- L = effective heated length, m
The original page provides outside diameter and nominal annealed length, but not wall thickness or inside diameter.
Therefore, the heated mass cannot be calculated reliably from the original information alone.
5. Estimate the Sensible Thermal Energy
The sensible energy required to increase the temperature of the specified copper mass can be expressed as:
Q = m × ∫cp(T)dT
The integral is evaluated from the initial temperature to the final temperature.
Where:
- Q = sensible thermal energy, J
- m = heated mass, kg
- cp(T) = temperature-dependent specific heat capacity, J/(kg·K)
This calculation does not include electromagnetic coupling losses, electrical conversion losses or heat transferred to adjacent material and the environment.
The required input power must be evaluated using the actual process conditions and equipment characteristics.
6. Select the Operating Frequency
Frequency affects electromagnetic penetration and the distribution of induced electrical currents in the tube wall.
Because copper has high electrical conductivity, operating frequency and coil design should be selected together.
The original published operating frequency is 60 kHz.
Its suitability for other copper tube dimensions or wall thicknesses must be evaluated independently.
7. Design the Induction Heating Coil
The coil should be designed for the tube outside diameter, insertion depth, required heated length, operating frequency and cooling arrangement.
The original example uses a four-turn helical coil.
The complete coil geometry, turn spacing, tube-to-coil clearance and electrical matching details are not provided.
These parameters must be determined during the engineering design process.
8. Select Temperature Monitoring
Temperature measurement on copper can be difficult because surface emissivity changes with oxidation and temperature.
The chosen measurement method should be validated against an appropriate reference.
Temperature measurements should be taken at locations relevant to the required annealed zone and the adjacent region.
9. Evaluate the Cooling Arrangement
The workpiece cooling system and the induction coil cooling system perform different functions.
The coil cooling circuit removes heat from the induction equipment, while the workpiece cooling process controls the thermal history of the copper tube.
The two systems should be specified separately.
Rapid workpiece cooling can limit continued heat spreading but cannot automatically restore hardness already lost through annealing.
10. Verify the Hardness Profile
A successful localized annealing process should be evaluated using hardness measurements at defined distances from the tube end.
The measurement plan should include the intended annealed zone, the transition region and the unaffected tube body.
Where necessary, additional tests should assess grain size, ductility and dimensional condition.
11. Confirm Equipment Requirements
The selected induction generator must support the required frequency, coil configuration, duty cycle and heating load.
Electrical input, cooling-water requirements and safety interlocks must be verified using the actual equipment documentation.
12. Qualify the Final Process
Representative test pieces should be processed using the intended equipment, coil and cooling arrangement.
The final acceptance criteria should be established before production, including hardness limits, softened-zone length, transition-zone requirements and dimensional tolerances.
Conceptual Equipment Layout
A localized copper tube end-annealing station may include a high-frequency induction power supply, remote matching workhead, helical coil, tube-positioning fixture, rotation mechanism, workpiece cooling system and temperature measurement equipment.
A suitable mechanical arrangement should support the complete sequence of first-end heating, rotation, cooling, tube repositioning and opposite-end processing.
Actual equipment dimensions, cooling flow, safety guarding and automation requirements must be confirmed for the selected system.
Advantages and Limitations
Advantages of Copper Tube Induction Annealing
- Localized energy delivery: Induction heating can concentrate thermal energy within a selected region of the tube.
- Non-contact heating: Electromagnetic energy is transferred without requiring direct physical contact between the coil and workpiece.
- Adjustable thermal input: Power and heating time can be controlled within equipment operating limits.
- Process integration potential: The induction station can be incorporated into suitable tube-processing equipment.
- Flameless operation: Heating is generated electromagnetically rather than by direct flame impingement.
- Repeatable positioning: Suitable fixtures and handling mechanisms can support consistent tube placement.
- Selective treatment: The process can be evaluated for applications requiring different material conditions along the tube.
Limitations
- Actual softening behavior depends on copper grade and initial temper.
- Thermal conduction can extend the affected zone beyond the intended heating region.
- A defined heating time does not guarantee a specified hardness profile.
- The coil must be matched to the tube geometry and the selected power supply.
- High-temperature heating may cause oxidation, grain growth or dimensional changes.
- Rapid cooling does not re-harden ordinary unalloyed copper.
- Surface temperature measurements require careful calibration and interpretation.
- Final equipment performance must be demonstrated through representative process testing.
Why Choose HLQ?
HLQ Induction Equipment Co., Ltd. publishes high-frequency, medium-frequency and ultra-high-frequency induction heating equipment for industrial metal-processing applications.
The published product range includes induction heating systems used for annealing, brazing, preheating, hardening and related processes.
For the copper tube end-annealing application, the original page identifies a DW-HF-45 induction heating system with a remote workhead and a four-turn helical coil.
The appropriate engineering evaluation should focus on electrical compatibility, coil matching, temperature control, tube positioning, cooling and the required finished material properties.
Relevant Published HLQ Equipment Information
| Equipment Area | Published Information |
|---|---|
| Original application model | DW-HF-45kW designation |
| Current DW-HF-45 oscillation capacity | 45 kVA |
| Published DW-HF-45 operating frequency | 30–80 kHz |
| Original application frequency | 60 kHz |
| Original workhead configuration | Eight 1.0 µF capacitors; 8.0 µF total nominal capacitance |
| Original coil configuration | Four-turn helical coil |
| Published equipment cooling | Water-cooled induction system |
| Process qualification | Requires testing with the actual copper grade and tube geometry |
These statements describe published equipment information and technical evaluation requirements. They do not claim an independently verified customer installation, quantified energy savings or proven final hardness distribution for the original application.
Published Copper Tube End-Annealing Application
The original application can be summarized as follows:
| Application Parameter | Published Value |
|---|---|
| Workpiece | Copper tube |
| Outside diameter | 41.275 mm |
| Overall length | 609.6 mm |
| Targeted annealed length | 38.1 mm per end |
| Induction equipment | DW-HF-45kW |
| Frequency | 60 kHz |
| Published target temperature | 815.6°C |
| Heating time | 7.5 seconds per end |
| Rotation | 180 degrees after 3.75 seconds |
| Coil | Four-turn helical coil |
| Workhead capacitance | 8.0 µF total nominal capacitance |
| Post-heating operation | Immediate water cooling |
| Opposite-end processing | Tube repositioned and heating sequence repeated |
| Actual copper grade | Not specified |
| Final hardness measurements | Not provided |
| Verified hardness-transition length | Not provided |
Related Induction Annealing Applications
Localized tube-end annealing should be distinguished from full-length continuous annealing operations.
For example, continuous induction annealing for wire and cable involves different workpiece geometries, handling methods and temperature-control requirements.
Equipment settings should not be transferred from wire processing to copper tube end annealing without independent process verification.
6 Core FAQs
1. What is copper tube induction annealing?
Copper tube induction annealing is a heat-treatment process that uses an alternating electromagnetic field to generate heat within a conductive copper tube. It can be used to soften selected regions after cold working, provided that the required temperature-time cycle and final material properties are achieved.
2. What is the recommended induction annealing temperature for copper tubes?
There is no universal annealing temperature for all copper tubes. Published conventional soft-annealing reference ranges include 300–650°C for Cu-ETP, 425–650°C for Cu-OF and 350–650°C for Cu-DHP. The original HLQ page reports a higher target of approximately 815.6°C for a short-duration localized heating process. That value requires independent validation and should not be adopted as a general copper tube annealing setting.
3. Can induction heating anneal only the ends of a copper tube?
Yes. An induction coil can be designed to concentrate energy near a tube end. However, copper conducts heat efficiently, so the thermal influence can extend beyond the coil region. The actual annealed-zone length and hardness-transition region must be verified by appropriate measurements.
4. Does water quenching harden copper after induction annealing?
Not for ordinary non-hardenable copper grades such as Cu-ETP, Cu-OF and Cu-DHP. Rapid cooling does not produce the same hardening mechanism associated with quenched steel. In localized copper tube annealing, rapid cooling may help limit further thermal exposure outside the target zone, but it cannot restore hardness already lost through recrystallization or annealing.
5. Which induction heating machine is suitable for copper tube end annealing?
The original application identifies a DW-HF-45 induction heating system operating at 60 kHz. The current DW-HF-45 series is published with a 45 kVA maximum oscillation capacity and a 30–80 kHz frequency range. Final equipment selection depends on copper grade, tube outside diameter, wall thickness, heated length, required temperature profile, heating time and coil design.
6. Can copper tube end annealing be integrated into an automated production line?
Yes. A suitable induction heating station can be combined with tube positioning, controlled rotation, heating, temperature monitoring, cooling and handling equipment. However, the achievable throughput depends on the complete processing sequence, duty cycle and required material properties. The original application provides a 7.5-second heating interval per end but does not establish a verified production rate.