Ultimate Guide to Induction Hardening: Enhancing the Surface of Shafts, Rollers, and Pins.
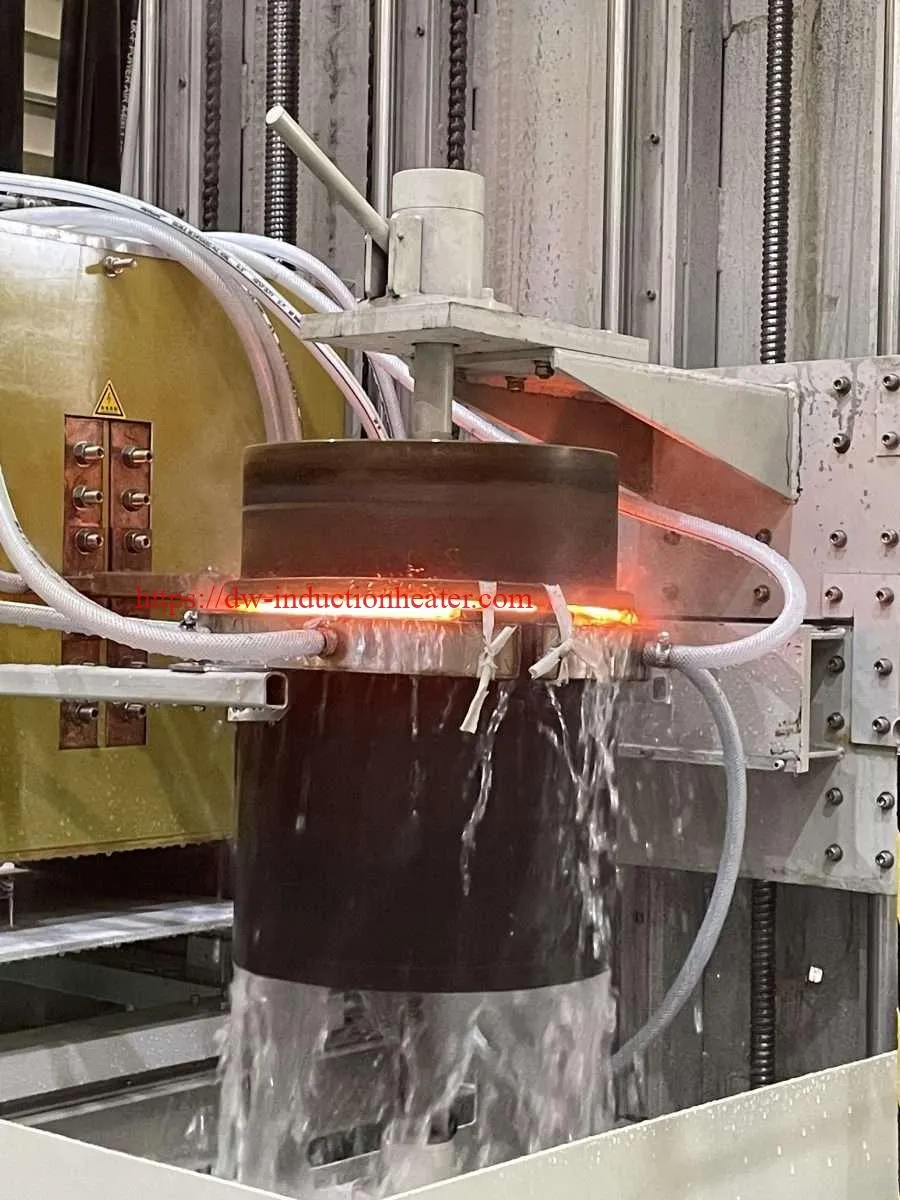 Induction hardening is a specialized heat treatment process that can significantly enhance the surface properties of various components, including shafts, rollers, and pins. This advanced technique involves selectively heating the surface of the material using high-frequency induction coils and then rapidly quenching it to achieve optimal hardness and wear resistance. In this comprehensive guide, we will explore the intricacies of induction hardening, from the science behind the process to the benefits it offers in terms of improving the durability and performance of these crucial industrial components. Whether you are a manufacturer looking to optimize your production processes or simply curious about the fascinating world of heat treatments, this article will provide you with the ultimate insights into induction hardening.
1. What is induction hardening?
Induction hardening is a heat treatment process used to enhance the surface properties of various components such as shafts, rollers, and pins. It involves heating the surface of the component using high-frequency electrical currents, which are generated by an induction coil. The intense heat generated quickly raises the temperature of the surface, while the core remains relatively cool. This rapid heating and cooling process results in a hardened surface with improved wear resistance, hardness, and strength. The induction hardening process begins by positioning the component within the induction coil. The coil is connected to a power source, which produces an alternating current that flows through the coil, creating a magnetic field. When the component is placed within this magnetic field, eddy currents are induced in its surface. These eddy currents generate heat due to the resistance of the material. As the surface temperature increases, it reaches the austenitizing temperature, which is the critical temperature required for transformation to occur. At this point, the heat is quickly removed, usually through the use of a water spray or quenching medium. The rapid cooling causes the austenite to transform into martensite, a hard and brittle phase that contributes to the enhanced surface properties. Induction hardening offers several advantages over traditional hardening methods. It is a highly localized process, focusing only on the areas that require hardening, which minimizes distortion and reduces energy consumption. The precise control over the heating and cooling process allows for customization of hardness profiles according to specific requirements. Additionally, induction hardening is a fast and efficient process that can be easily automated for high-volume production. In summary, induction hardening is a specialized heat treatment technique that selectively improves the surface properties of components like shafts, rollers, and pins. By harnessing the power of high-frequency electrical currents, this process provides enhanced wear resistance, hardness, and strength, making it a valuable method for enhancing the performance and durability of various industrial components.
2. The science behind induction hardening
Induction hardening is a fascinating process that involves enhancing the surface of shafts, rollers, and pins to increase their durability and strength. To understand the science behind induction hardening, we must first delve into the principles of induction heating. The process of induction heating utilizes an alternating magnetic field generated by an induction coil. When an electric current passes through the coil, it generates the magnetic field, which creates eddy currents within the workpiece. These eddy currents produce heat due to the resistance of the material, leading to localized heating. During induction hardening, the workpiece is rapidly heated to a specific temperature above its transformation point, known as the austenitizing temperature. This temperature varies depending on the material being hardened. Once the desired temperature is reached, the workpiece is quenched, typically using water or oil, to rapidly cool it down. The science behind induction hardening lies in the transformation of the material’s microstructure. By rapidly heating and cooling the surface, the material undergoes a phase change from its initial state to a hardened state. 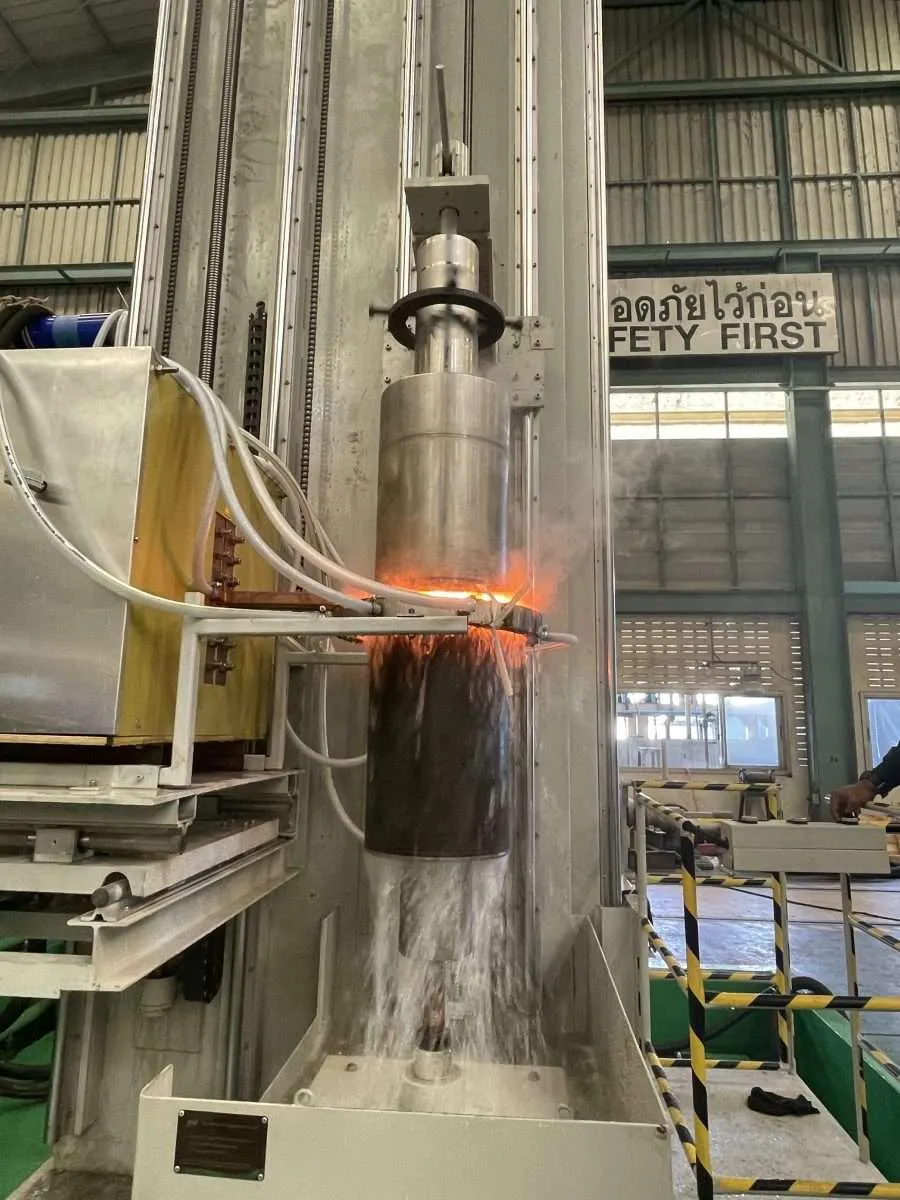 This phase change results in the formation of martensite, a hard and brittle structure that significantly enhances the surface’s mechanical properties. The depth of hardened layer, known as the case depth, can be controlled by adjusting various parameters such as the frequency of the magnetic field, power input, and quenching medium. These variables directly influence the heating rate, cooling rate, and ultimately, the final hardness and wear resistance of the hardened surface. It’s important to note that induction hardening is a highly precise process, offering excellent control over localized heating. By selectively heating only the desired areas, such as shafts, rollers, and pins, manufacturers can achieve optimal hardness and wear resistance while maintaining the core’s toughness and ductility. In conclusion, the science behind induction hardening lies in the principles of induction heating, the transformation of microstructure, and the control of various parameters. This process enables the enhancement of the surface properties of shafts, rollers, and pins, resulting in improved durability and performance in various industrial applications.
3. Benefits of induction hardening for shafts, rollers, and pins
Induction hardening is a widely used heat treatment process that offers numerous benefits for enhancing the surface of shafts, rollers, and pins. The primary advantage of induction hardening is its ability to selectively heat treat specific areas, resulting in a hardened surface while maintaining the core’s desired properties. This process improves the durability and wear resistance of these components, making them ideal for heavy-duty applications. One of the key benefits of induction hardening is the significant increase in hardness achieved on the surface of shafts, rollers, and pins. This enhanced hardness helps to prevent surface damage, such as abrasion and deformation, extending the lifespan of the components. The hardened surface also provides improved resistance to fatigue, ensuring that these parts can withstand high-stress conditions without compromising their performance. In addition to hardness, induction hardening improves the overall strength of shafts, rollers, and pins. The localized heating and rapid quenching process during induction hardening results in a transformation of the microstructure, leading to increased tensile strength and toughness. This makes the components more resistant to bending, breaking, and deformation, enhancing their reliability and longevity. Another significant advantage of induction hardening is its efficiency and speed. The process is known for its rapid heating and quenching cycles, enabling high production rates and cost-effective manufacturing. Compared to traditional methods such as case hardening or through-hardening, induction hardening offers shorter cycle times, reducing energy consumption and improving productivity. Furthermore, induction hardening allows for precise control over the hardened depth. By adjusting the power and frequency of the induction heating, manufacturers can achieve the desired hardened depth specific to their application requirements.  This flexibility ensures that the surface hardness is optimized while maintaining the appropriate core properties. Overall, the benefits of induction hardening make it an ideal choice for enhancing the surface of shafts, rollers, and pins. From increased hardness and strength to improved durability and efficiency, induction hardening offers manufacturers a reliable and cost-effective method to enhance the performance and longevity of these critical components in various industries.
4. The induction hardening process explained
Induction hardening is a widely used technique in the manufacturing industry to enhance the surface properties of various components, such as shafts, rollers, and pins. This process involves heating the selected areas of the component using high-frequency induction heating, followed by rapid quenching to achieve a hardened surface layer. The induction hardening process begins with the positioning of the component in the induction coil, which generates a high-frequency alternating magnetic field. This magnetic field induces eddy currents in the workpiece, leading to rapid and localized heating of the surface. The depth of the hardened layer can be controlled by adjusting the frequency, power, and time of the induction heating. As the surface temperature rises above the critical transformation temperature, the austenite phase is formed. This phase is then rapidly quenched using a suitable medium, such as water or oil, to transform it into martensite. The martensitic structure provides excellent hardness, wear resistance, and strength to the treated surface, while the core of the component retains its original properties. One of the significant advantages of induction hardening is its ability to achieve precise and controlled hardening patterns. By carefully designing the shape and configuration of the induction coil, specific areas of the component can be targeted for hardening. This selective heating minimizes distortion and ensures that only the required surface areas are hardened, preserving the desired mechanical properties of the core. Induction hardening is highly efficient and can be integrated into automated production lines, ensuring consistent and repeatable results. It offers several benefits over other surface hardening methods, such as flame hardening or carburizing, including shorter heating times, reduced energy consumption, and minimal material distortion.  However, it is crucial to note that the induction hardening process requires careful process design and parameter optimization to ensure optimal results. Factors such as the component material, geometry, and desired hardening depth must be taken into consideration. In conclusion, induction hardening is a versatile and effective method for enhancing the surface properties of shafts, rollers, and pins. Its ability to provide localized and controlled hardening makes it ideal for various industrial applications where wear resistance, hardness, and strength are essential. By understanding the induction hardening process, manufacturers can harness its benefits to produce high-quality and durable components.
5. Induction Hardening Power Supplier
| Models | Rated output power | Frequency rage | Input current | Input voltage | Duty cycle | Water flow | weight | Dimension |
| MFS-100 | 100KW | 0.5-10KHz | 160A | 3phase 380V 50Hz | 100% | 10-20m³/h | 175KG | 800x650x1800mm |
| MFS-160 | 160KW | 0.5-10KHz | 250A | 10-20m³/h | 180KG | 800x 650 x 1800mm | ||
| MFS-200 | 200KW | 0.5-10KHz | 310A | 10-20m³/h | 180KG | 800x 650 x 1800mm | ||
| MFS-250 | 250KW | 0.5-10KHz | 380A | 10-20m³/h | 192KG | 800x 650 x 1800mm | ||
| MFS-300 | 300KW | 0.5-8KHz | 460A | 25-35m³/h | 198KG | 800x 650 x 1800mm | ||
| MFS-400 | 400KW | 0.5-8KHz | 610A | 25-35m³/h | 225KG | 800x 650 x 1800mm | ||
| MFS-500 | 500KW | 0.5-8KHz | 760A | 25-35m³/h | 350KG | 1500 x 800 x 2000mm | ||
| MFS-600 | 600KW | 0.5-8KHz | 920A | 25-35m³/h | 360KG | 1500 x 800 x 2000mm | ||
| MFS-750 | 750KW | 0.5-6KHz | 1150A | 50-60m³/h | 380KG | 1500 x 800 x 2000mm | ||
| MFS-800 | 800KW | 0.5-6KHz | 1300A | 50-60m³/h | 390KG | 1500 x 800 x 2000mm |
6. CNC Hardening / Quenching Machine Tools
Technical Parameter
| Model | SK-500 | SK-1000 | SK-1200 | SK-1500 |
| Max heating length(mm) | 500 | 1000 | 1200 | 1500 |
| Max heating diameter(mm) | 500 | 500 | 600 | 600 |
| Max holding length(mm) | 600 | 1100 | 1300 | 1600 |
| Max weight of workpiece(Kg) | 100 | 100 | 100 | 100 |
| Workpiece rotation speed(r/min) | 0-300 | 0-300 | 0-300 | 0-300 |
| workpiece moving speed(mm/min) | 6-3000 | 6-3000 | 6-3000 | 6-3000 |
| Cooling method | Hydrojet cooling | Hydrojet cooling | Hydrojet cooling | Hydrojet cooling |
| Input voltage | 3P 380V 50Hz | 3P 380V 50Hz | 3P 380V 50Hz | 3P 380V 50Hz |
| Motor power | 1.1KW | 1.1KW | 1.2KW | 1.5KW |
| Dimension LxWxH (mm) | 1600 x800 x2000 | 1600 x800 x2400 | 1900 x900 x2900 | 1900 x900 x3200 |
| weight(Kg) | 800 | 900 | 1100 | 1200 |
| Model | SK-2000 | SK-2500 | SK-3000 | SK-4000 |
| Max heating length(mm) | 2000 | 2500 | 3000 | 4000 |
| Max heating diameter(mm) | 600 | 600 | 600 | 600 |
| Max holding length(mm) | 2000 | 2500 | 3000 | 4000 |
| Max weight of workpiece(Kg) | 800 | 1000 | 1200 | 1500 |
| workpiece rotation speed(r/min) | 0-300 | 0-300 | 0-300 | 0-300 |
| workpiece moving speed(mm/min) | 6-3000 | 6-3000 | 6-3000 | 6-3000 |
| Cooling method | Hydrojet cooling | Hydrojet cooling | Hydrojet cooling | Hydrojet cooling |
| Input voltage | 3P 380V 50Hz | 3P 380V 50Hz | 3P 380V 50Hz | 3P 380V 50Hz |
| Motor power | 2KW | 2.2KW | 2.5KW | 3KW |
| Dimension LxWxH (mm) | 1900 x900 x2400 | 1900 x900 x2900 | 1900 x900 x3400 | 1900 x900 x4300 |
| weight(Kg) | 1200 | 1300 | 1400 | 1500 |
7. Conclusion
The specific parameters of the induction hardening process, such as heating time, frequency, power, and quenching medium, are determined based on the material composition, component geometry, desired hardness, and application requirements.
Induction hardening provides localized hardening, which allows for a combination of a hard and wear-resistant surface with a tough and ductile core. This makes it suitable for components like shafts, rollers, and pins that require high surface hardness and wear resistance while maintaining sufficient strength and toughness in the core.