
Induction Hot Forming Stainless Steel Tape
Induction Hot Forming Stainless Steel Tape: Continuous “J” Profile Heating at 15 ft/min
Quick Answer
Induction hot forming stainless steel tape heats a continuously fed flat strip so it can be formed into a profile, here a “J” shape. In this HLQ case, stainless steel tape 0.562″ wide and 0.028″ thick was heated by a DW-HF-15kW solid state induction power supply at 80 kHz. The equipment used one remote heat station with one 1.2 µF capacitor and a fifteen-turn oval coil 6″ long, 1 1/4″ wide and 1″ high. In a static test, a 6″ section reached the target temperature within 2 seconds, which translates into a continuous feed rate of over 15 feet per minute.
Table of Contents
- What is Induction Hot Forming of Stainless Steel Tape?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages and Limitations
- Why Choose HLQ?
- 10 Core FAQs
What is Induction Hot Forming Stainless Steel Tape?
Induction hot forming of stainless steel tape heats the tape inline, as it is fed continuously, to aid forming a profile from flat stock. The induction coil surrounds the moving tape, and eddy currents heat it without contact. In the HLQ case, the material was heated to aid in forming the “J” shape from flat stock. For the general process, see induction forging and hot forming.
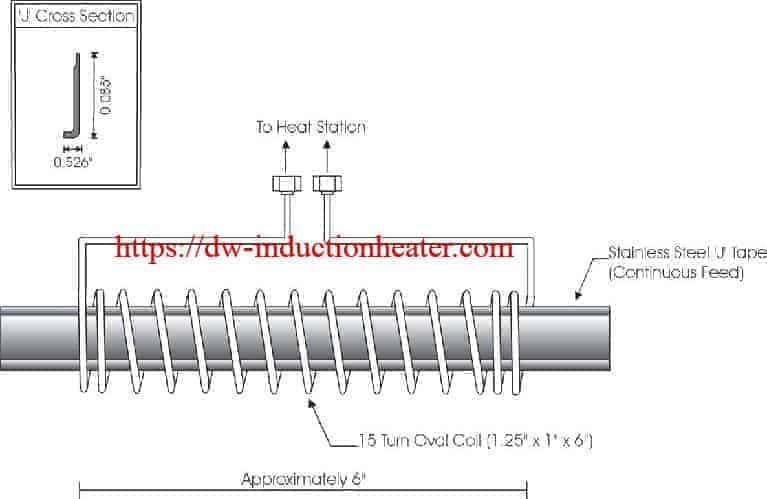
 The case drawing shows the “J” cross section, the stainless steel “J” tape in continuous feed, and the 15-turn oval coil (1.25″ × 1″ × 6″), approximately 6″ long, connected to the heat station.
Key Applications
- Profile forming of stainless tape: “J” tape formed from flat stock (this case).
- Continuous strip heating: see HLQ induction strip heating solutions.
- Strip heating before forging: see induction forging steel strip.
- Strip annealing lines: see continuous induction steel strip annealing machines.
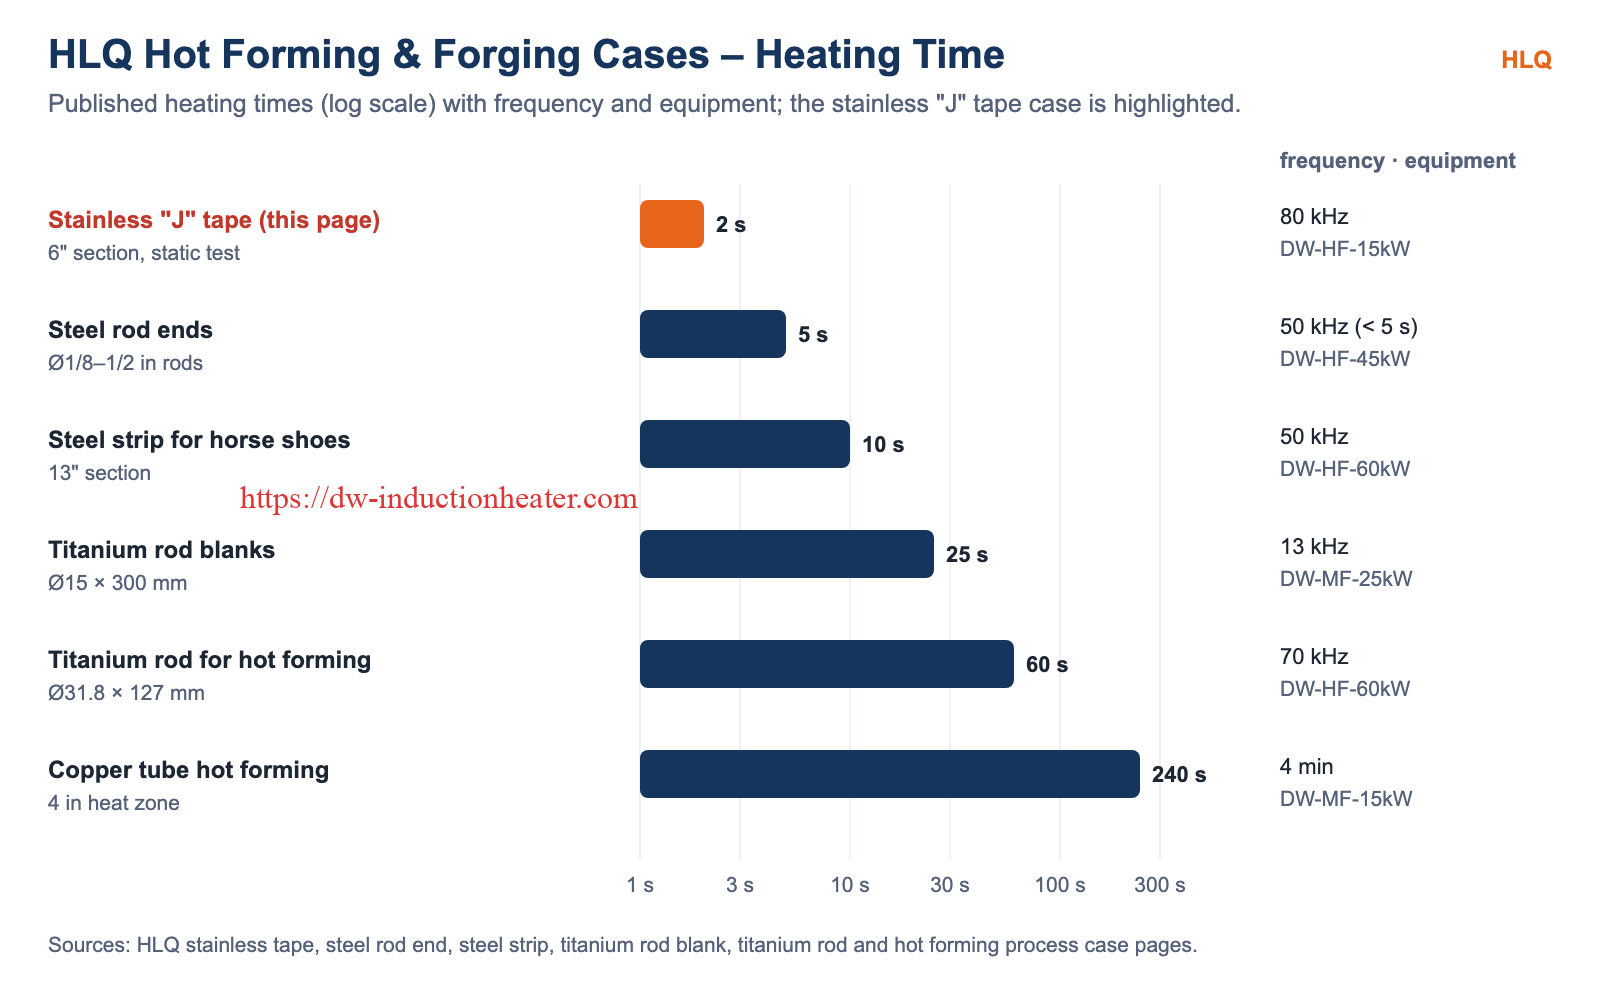
| HLQ case | Part | Heating time | Frequency | Equipment |
|---|---|---|---|---|
| Stainless “J” tape (this page) | 0.562″ × 0.028″ tape, 6″ section | 2 s (static test) | 80 kHz | DW-HF-15kW |
| Steel rod ends | Ø1/8″–1/2″ rods | < 5 s | 50 kHz | DW-HF-45kW |
| Steel strip for horse shoes | 1025 steel, 13″ section | 10 s | 50 kHz | DW-HF-60kW |
| Titanium rod blanks | Ø15 × 300 mm | 25 s | 13 kHz | DW-MF-25kW |
| Titanium rod for hot forming | Ø31.8 × 127 mm | 60 s | 70 kHz | DW-HF-60kW |
| Copper tube hot forming | 4 in heat zone | 4 min | – | DW-MF-15kW |
Suitable Materials
| Material | Data | Source |
|---|---|---|
| Stainless steel “J” tape (grade not stated) | 0.562″ (14.3 mm) wide × 0.028″ (0.71 mm) thick, continuously fed | This case |
| Stainless steel | Typical heating range 1050–1180 °C for forging and forming | HLQ induction forging billet heating guide |
| Stainless steel | Good heating suitability; may require longer heating time than carbon steel | HLQ DW-HF-60kW equipment page |
Working Principle
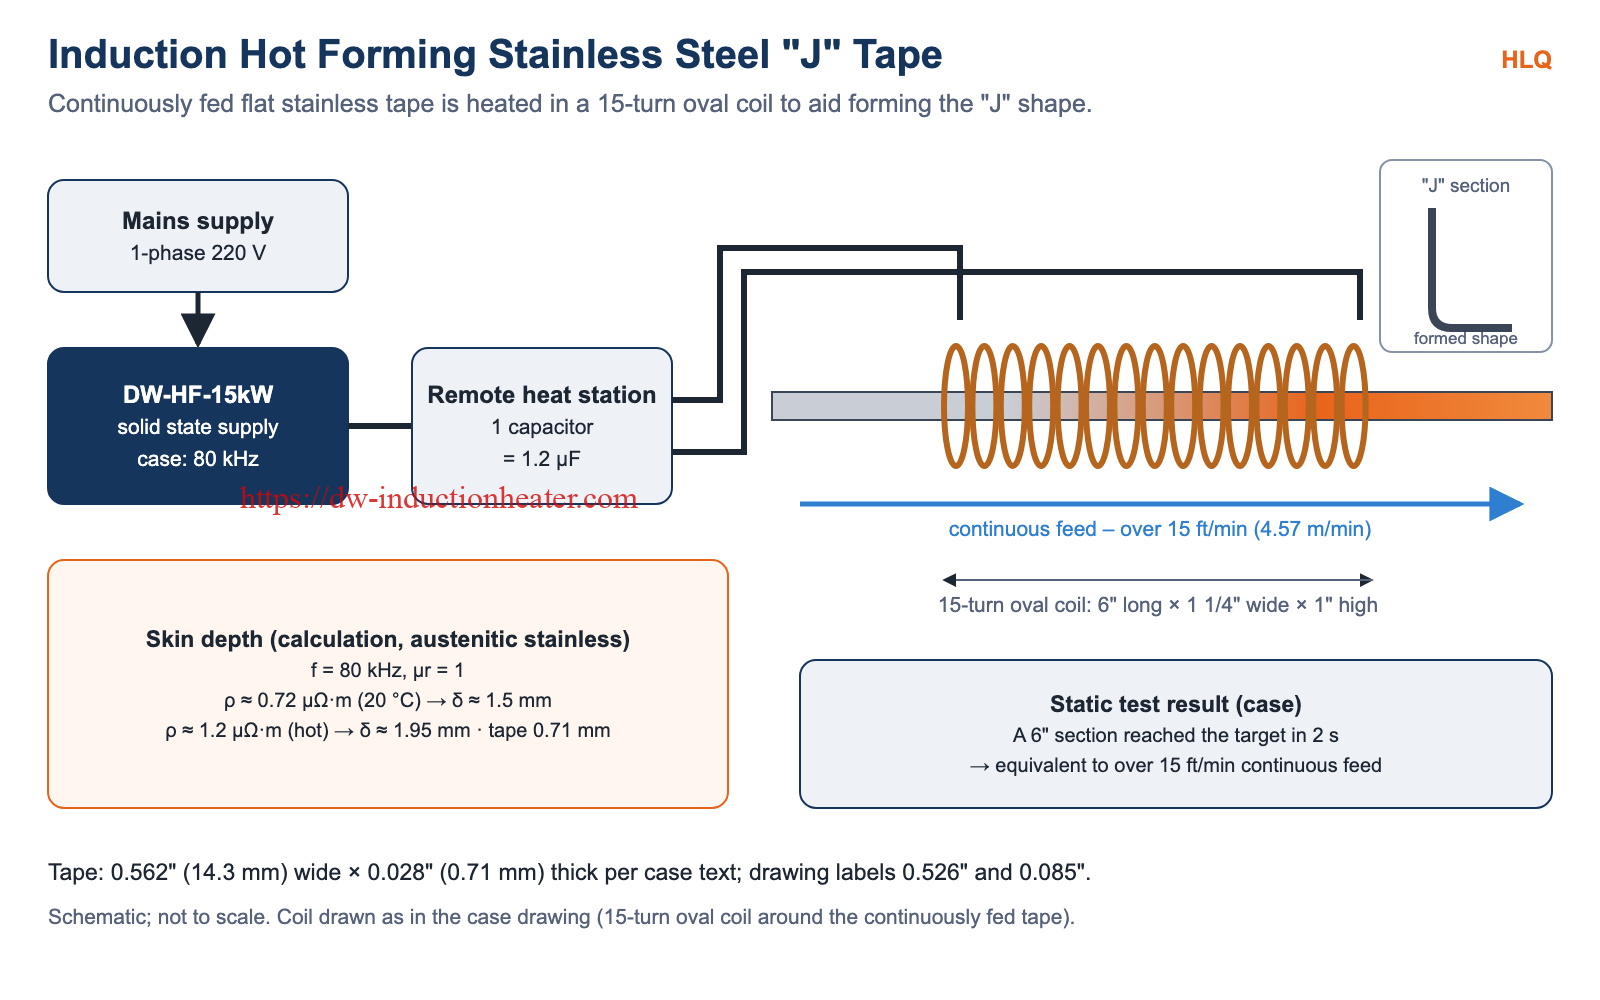
The DW-HF-15kW supplies 80 kHz current to the remote heat station (one 1.2 µF capacitor) and the fifteen-turn oval coil. The tape passes through the 6″ coil, so each section is heated as it moves towards the forming station. In the static test, a 6″ section was heated within 2 seconds. Moving the tape 6″ every 2 seconds gives 3 in/s, which is 15 ft/min.
Current distribution follows the skin effect. Calculation (δ = 503·√(ρ/f), µr = 1, typical austenitic stainless resistivity):
| Condition | Resistivity | δ at 80 kHz | Tape thickness |
|---|---|---|---|
| Room temperature | ≈ 0.72 µΩ·m | ≈ 1.5 mm | 0.71 mm |
| Hot | ≈ 1.2 µΩ·m | ≈ 1.95 mm | 0.71 mm |
Technical Specifications
| Parameter | Case data |
|---|---|
| Objective | Heat a stainless steel “J” tape from room temperature at a rate of 15 feet per minute, to aid in forming the “J” shape from flat stock |
| Material | Stainless steel “J” tape, 0.562″ (14.3 mm) wide, 0.028″ (0.71 mm) thick, continuously fed |
| Temperature (as stated in the original case, under review) | 3000F |
| Frequency | 80 kHz |
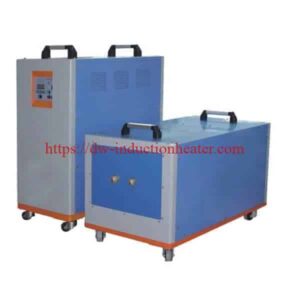
| Equipment | DW-HF-15kW output solid state induction power supply, including one remote heat station containing one capacitor with a value of 1.2 µF |
| Coil | Fifteen-turn oval coil, 6″ long, 1 1/4″ wide and 1″ high |
| Result | Target reached on a 6″ section within 2 seconds in a static test, which translates into over 15 feet per minute |
| Feed rate (calculation) | 6″ / 2 s = 3 in/s = 15 ft/min (4.57 m/min) |
| Mass of the 6″ section (calculation, 7.9 g/cm³) | ≈ 12 g |
Recommended Model Selection
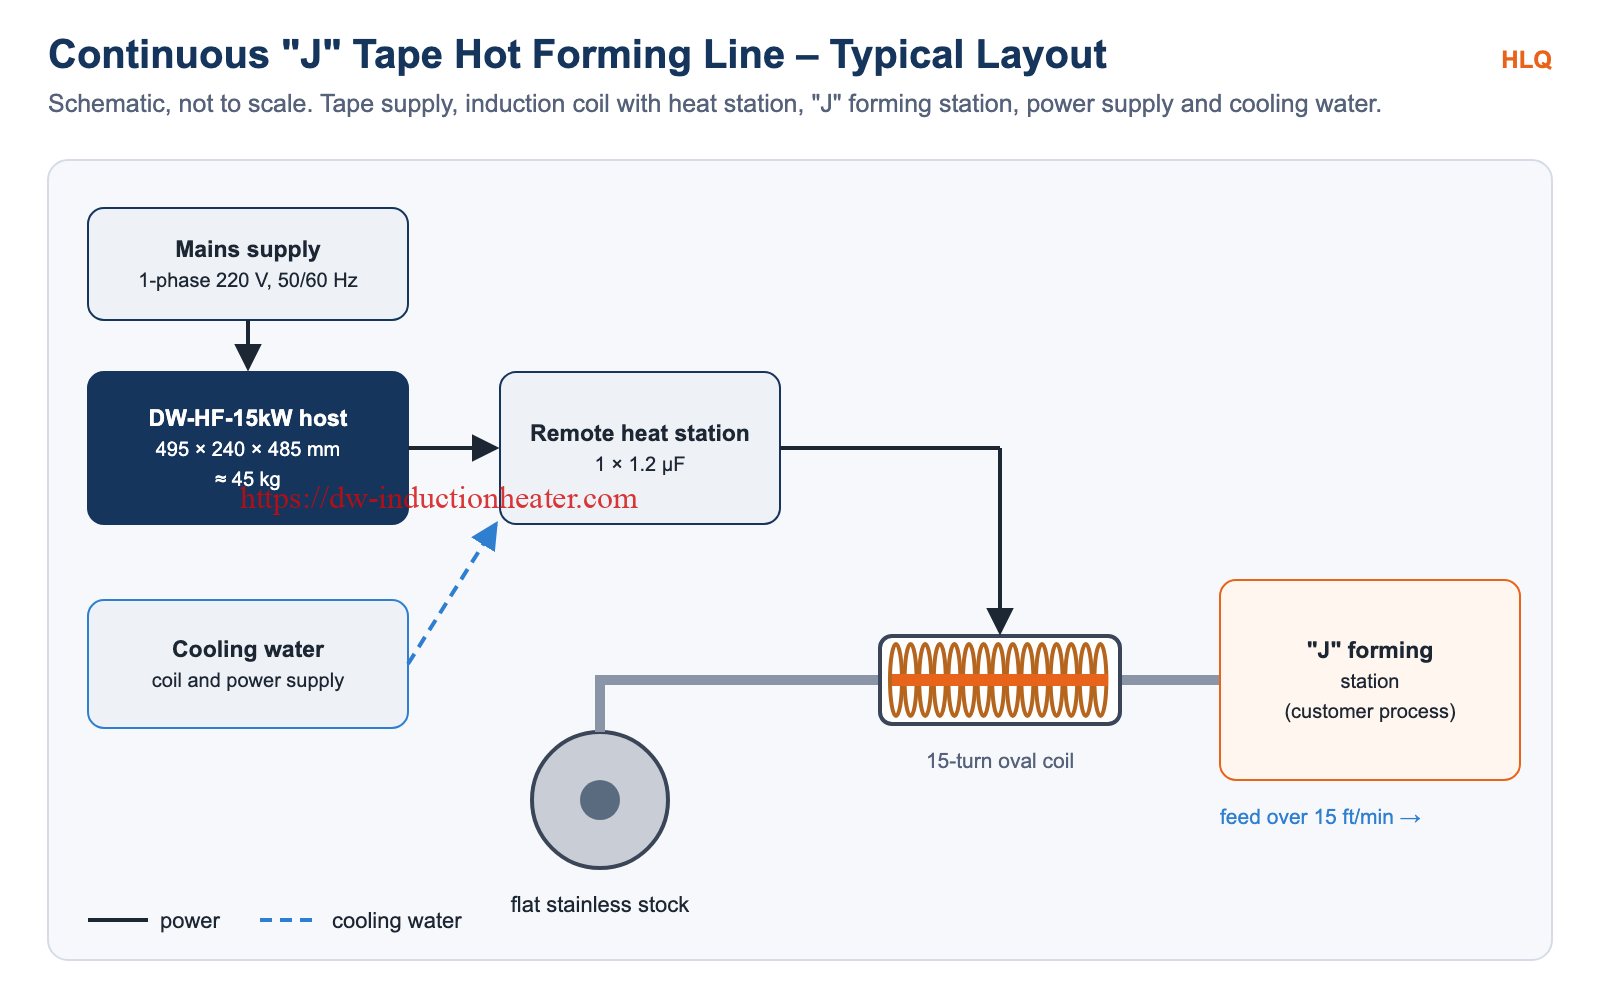
Specifications of the DW-HF-15kW induction heating equipment:
| Parameter | DW-HF-15kW |
|---|---|
| Rated output power | 15 kVA |
| Input power | Single-phase 220 V, 50/60 Hz |
| Oscillation frequency | 30–80 kHz |
| Duty cycle | 80% at 30 °C |
| Host size | 495 × 240 × 485 mm |
| Approx. weight | 45 kg |
| Cable length | 2–6 m |
| Cooling / control | Water cooling; manual or timer-controlled heating |
DW-HF series from the HLQ induction heating device model table:
| Model | Power | Max. input current | Supply |
|---|---|---|---|
| DW-HF-15 (this case) | 15 kVA | 32 A | Single-phase 220 V |
| DW-HF-25 | 25 kVA | 23 A | 3-phase 380 V |
| DW-HF-35 | 35 kVA | 51 A | 3-phase 380 V |
| DW-HF-45 | 45 kVA | 68 A | 3-phase 380 V |
| DW-HF-60 | 60 kVA | 105 A | 3-phase 380 V |
Process Workflow
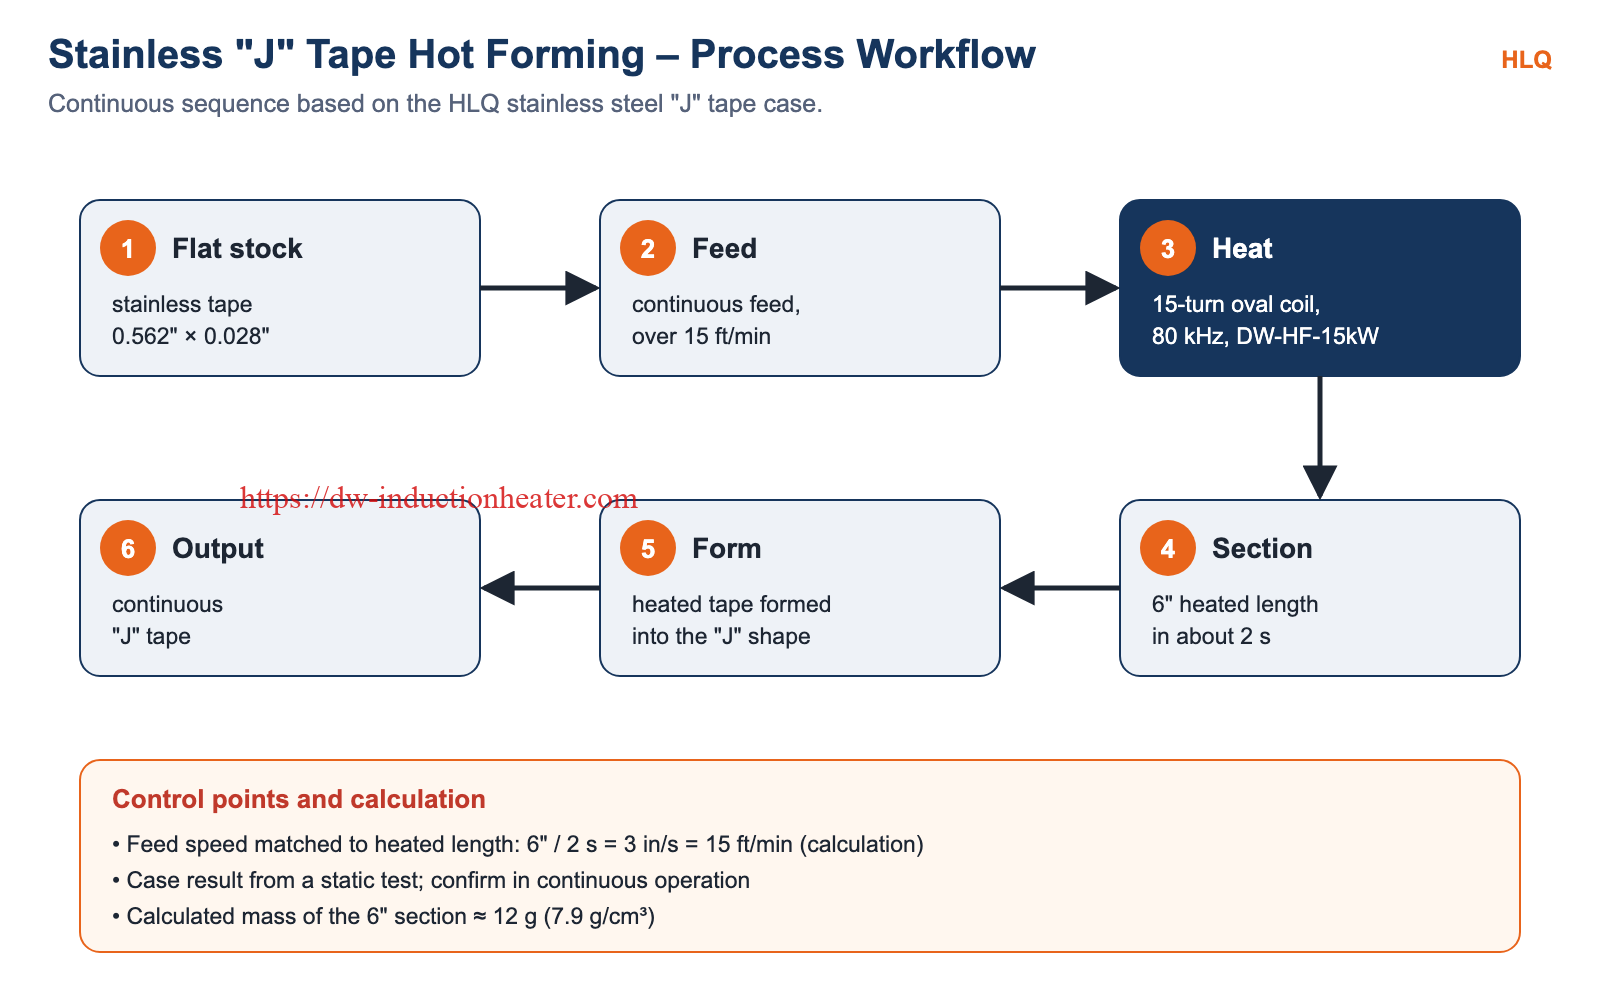
- Flat stock – stainless tape, 0.562″ × 0.028″.
- Feed – continuous feed at over 15 ft/min.
- Heat – the 15-turn oval coil at 80 kHz, powered by the DW-HF-15kW.
- Heated section – each 6″ length heated in about 2 seconds.
- Form – the heated tape is formed into the “J” shape.
- Output – continuous “J” tape.
Common Problems and Solutions
| Problem | Possible cause | Solution |
|---|---|---|
| Static test result not reached in continuous running | The case result comes from a static test | Confirm temperature at the forming station at full line speed |
| Heating too slow | Coil gap too large, wrong coil design, insufficient power or oversized workpiece | Reduce the coil gap, redesign the coil, increase power or select a larger induction heater |
| Tape overheats | Heating time too long or power too high | Match feed speed to heated length; lower power; use timer or temperature monitoring |
| Weak coupling to thin tape | Tape thickness (0.71 mm) is below the calculated skin depth at 80 kHz | Use a close-fitting coil around the tape (oval coil in this case) and confirm by test |
| Coil becomes hot | Insufficient cooling water, blocked coil or poor water quality | Check water flow, clean the coil and use proper cooling water circulation |
| Machine alarms or stops | Overcurrent, water shortage, overheating or incorrect connection | Check cooling, workpiece position, coil connection and operating parameters |
Problem data from the HLQ DW-HF-15kW product page and this case.
Engineering Selection Guide
- Line speed and heated length: they set the heating time. Here, 6″ of tape had to be heated every 2 seconds for 15 ft/min.
- Tape cross section: it sets the coil shape. A 1 1/4″ × 1″ oval coil fitted the 0.562″ tape in this case.
- Frequency: 80 kHz is within the DW-HF-15kW range of 30–80 kHz.
- Supply: the DW-HF-15kW runs on single-phase 220 V; DW-HF-25 and above use 3-phase 380 V.
- Temperature: confirm the forming temperature for the stainless grade (HLQ guide range for stainless steel: 1050–1180 °C).
- Data to send: stainless grade, tape width and thickness, line speed, forming temperature, formed profile, supply voltage and cooling water.
Advantages and Limitations
| Advantages | Limitations |
|---|---|
| 6″ section heated within 2 seconds | Result based on a static test |
| Supports continuous feed at over 15 ft/min | The coil must suit the tape cross section |
| Compact single-phase 220 V power supply | DW-HF-15kW duty cycle is 80% at 30 °C |
| Non-contact inline heating ahead of forming | Water cooling is required |
Why Choose HLQ?
- A documented continuous tape case: a 6″ section in 2 s, over 15 ft/min.
- Custom coils for strip and tape, such as the 15-turn oval coil.
- DW-HF power supplies from the single-phase DW-HF-15 to 160 kVA.
- Hot forming and forging cases in stainless tape, steel strip, steel rods and titanium.
10 Core FAQs
1. What was heated in this case?
A continuously fed stainless steel “J” tape, 0.562″ wide and 0.028″ thick.
2. Why is the tape heated?
To aid in forming the “J” shape from flat stock.
3. How fast was the tape heated?
A 6″ section reached the target within 2 seconds in a static test.
4. What line speed does that support?
Over 15 feet per minute (6″ every 2 seconds = 3 in/s).
5. Which induction machine was used?
A DW-HF-15kW output solid state induction power supply.
6. What frequency was used?
80 kHz.
7. What does the heat station contain?
One capacitor with a value of 1.2 µF.
8. Which coil was used?
A fifteen-turn oval coil, 6″ long, 1 1/4″ wide and 1″ high.
9. What power supply does the DW-HF-15kW need?
Single-phase 220 V, 50/60 Hz, plus water cooling.
10. What information is needed for a quotation?
The stainless grade, tape width and thickness, line speed, forming temperature, formed profile, and available power supply and cooling water.