



Induction Heating Steel Handle For Bending
Induction Heating Steel Pliers Handles for Bending
Quick Answer
Induction heating steel handles for bending brings only the zone to be shaped up to forming temperature, so the part is not overheated.
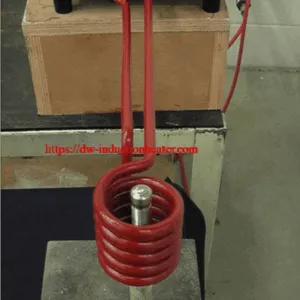
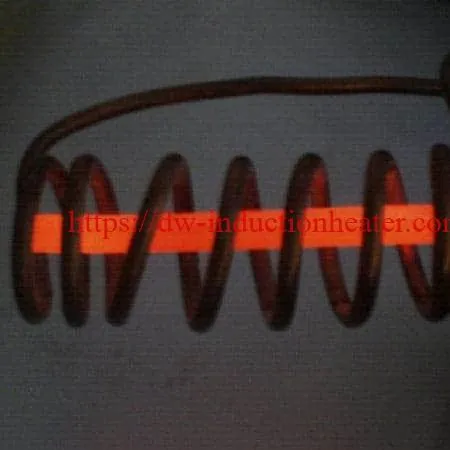
In this HLQ case, a multi-turn helical coil heated a 3.75″ (9.53 cm) zone on one steel pliers handle at a time to 1200 °F (649 °C) in 30 seconds. The handles were 5″ (12.7 cm) long and 0.14″ (3.56 mm) thick. The coil ran at 50 kHz from a DW-HF-4.5kW induction heating system, with a remote heat station of two 0.33 µF capacitors (0.66 µF). The heated part then went to a press for final shaping. Precise zone heating gives higher quality than heating with a torch.
What is Induction Heating of Steel Handles for Bending?
The coil heats only the section of the handle that will be bent, so the steel is soft enough to form in a press while the rest of the part stays cooler. In this case, each handle is heated and formed one at a time.
| Item | HLQ case data |
|---|---|
| Objective | Heat pliers for final shaping of the handles |
| Material | Steel pliers handles, 5″ (12.7 cm) long, 0.14″ (3.56 mm) thick |
| Temperature | 1200 °F (649 °C) |
| Frequency | 50 kHz |
| Equipment | DW-HF-4.5kW induction heating system with a remote heat station containing two 0.33 µF capacitors (0.66 µF total), plus a coil designed for this application |
| Coil | Multi-turn helical coil heating a 3.75″ (9.53 cm) zone on one handle at a time; easy loading and unloading without rotating the part |
| Cycle | Heated 30 seconds to 1200 °F, then transferred to a press and formed into the correct handle shape |
Key Applications

| Application | HLQ case data | Reference |
|---|---|---|
| Bending steel pliers handles | 3.75″ zone, 1200 °F, 30 s, then press | This case |
| Hot forming steel shovel plates | 4 plates to 950 °C, target under 5 s, DW-HF-45KW, then press | steel plate shovels hot forming with induction preheating |
| Heating bar and rod ends for forming | Channel and solenoid coils | induction heating the end of rods, billets and bars |
| Rivet head forming | 700 °C in 10–15 s | induction heating rivet ends |
| Pipe bending | Steel pipe and tube | induction pipe bending machine |
Suitable Materials
| Material | Notes |
|---|---|
| Steel pliers handles | 5″ long, 0.14″ thick; formed at 1200 °F (this case) |
| Steel plates | Hot formed into shovels at 950 °C (HLQ shovel case) |

Working Principle

- The power supply drives the remote heat station (2 × 0.33 µF) and the helical coil at 50 kHz.
- One handle is inserted into the coil; the coil allows loading and unloading without rotating the part.
- Eddy currents heat the 3.75″ zone inside the coil to 1200 °F in 30 seconds.
- The part is transferred to a press and formed.
More: induction heating coil design and skin effect in induction heating.
Technical Specifications
| Parameter | Value |
|---|---|
| Part | Steel pliers handles |
| Handle length | 5″ (12.7 cm) |
| Thickness | 0.14″ (3.56 mm) |
| Heated zone | 3.75″ (9.53 cm) on one handle at a time |
| Temperature | 1200 °F (649 °C) |
| Heating time | 30 s |
| Frequency | 50 kHz |
| Capacitors | 2 × 0.33 µF (0.66 µF) |
| Coil | Multi-turn helical |
| Forming | Press |
Recommended Model Selection
The case equipment was a DW-HF-4.5kW induction heating system at 50 kHz. Several pliers handles can be heated at the same time with a higher-kW power supply. HLQ DW-HF models:
| Model | Power | Input current | Supply |
|---|---|---|---|
| DW-HF-15KW | 15 kVA | 32 A | 1-phase 220 V |
| DW-HF-25KW | 25 kVA | 23 A | 3-phase 380 V |
| DW-HF-35KW | 35 kVA | 51 A | 3-phase 380 V |
| DW-HF-45KW | 45 kVA | 68 A | 3-phase 380 V |
| DW-HF-60KW | 60 kVA | 105 A | 3-phase 380 V |
| DW-HF-80KW | 80 kVA | 130 A | 3-phase 380 V |
Smallest DW-HF model: DW-HF-15 high frequency induction heater. All models: HLQ induction heating device models.
Process Workflow

| Step | Action |
|---|---|
| 1 | Insert one handle into the helical coil |
| 2 | Heat the 3.75″ zone for 30 s |
| 3 | The zone reaches 1200 °F (649 °C) |
| 4 | Transfer the part to the press |
| 5 | Form the handle into its final shape |
| 6 | Heat and form the second handle |
| 7 | Formed pliers go to the next step |
Cell layout

Common Problems and Solutions
| Problem | Cause | Solution |
|---|---|---|
| Part overheated | Torch heats beyond the zone | Coil heats only the 3.75″ zone (case result) |
| Slow loading | Part must be rotated into the coil | Coil designed for loading and unloading without rotating the part |
| Uneven forming results | Heating time varies | Fixed 30 s heating time for every handle |
| Output too low | One handle at a time | Higher-kW supply to heat several handles at once |
Engineering Selection Guide
| Factor | What to confirm | Why it matters |
|---|---|---|
| Part geometry | Length, thickness, zone to bend | Coil size and length |
| Forming temperature | For example, 1200 °F (649 °C) | Power and time |
| Parts heated at once | One or several | Power rating |
| Handling | Manual or automated transfer to the press | Coil opening and layout |
| Supply | 1-phase or 3-phase | Model choice |
Advantages and Limitations
| Advantages | Limitations |
|---|---|
| Precise zone heating avoids overheating the part | The coil is designed for each part |
| Higher quality than torch heating | One handle at a time with a small supply |
| Easy loading without rotating the part | The part must be transferred to the press |
| Repeatable 30 s cycle | — |
Why Choose HLQ?
| Strength | Evidence |
|---|---|
| Forming experience | Pliers handles, shovel plates, bar and rivet ends |
| Practical coils | Helical coil that loads without rotating the part |
| Scalable | Higher-kW supplies for several parts at once |
| DW-HF series | 15–160 kVA |
| Quality | Zone heating, no overheating |
10 Core FAQs
1. What is heated in this application?
A 3.75″ (9.53 cm) zone on one steel pliers handle at a time, before final shaping.
2. What size are the handles?
5″ (12.7 cm) long and 0.14″ (3.56 mm) thick.
3. What temperature is used?
1200 °F (649 °C).
4. How long does heating take?
30 seconds per handle.
5. What frequency was used?
50 kHz.
6. What is in the heat station?
Two 0.33 µF capacitors, 0.66 µF in total.
7. Which coil was used?
A multi-turn helical coil that allows easy loading and unloading without rotating the part.
8. What happens after heating?
The part is transferred to a press and formed into the correct handle shape.
9. Can several handles be heated at once?
Yes, with a higher-kW power supply.
10. What is needed for a quotation?
The part drawing and material, the zone to be heated, the forming temperature, the number of parts per hour, and the available supply.