Hardening Stainless Steel Knife Blades With Induction
Induction Hardening Stainless Steel Knife Blades: 420 Surgical Blades to 48–53 HRC
Quick Answer
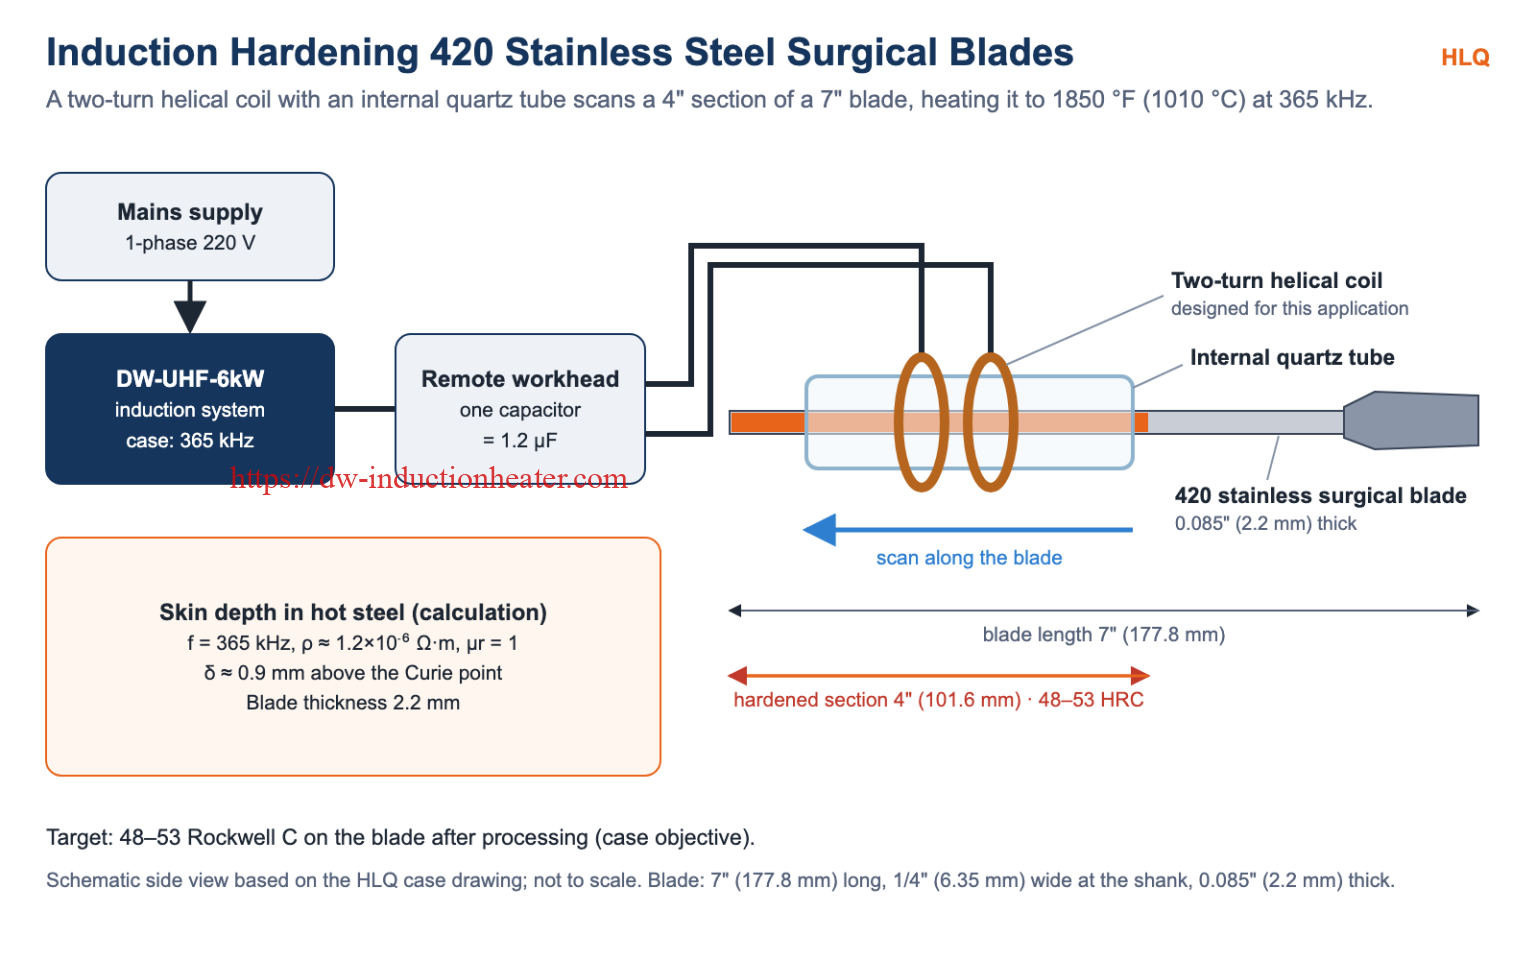
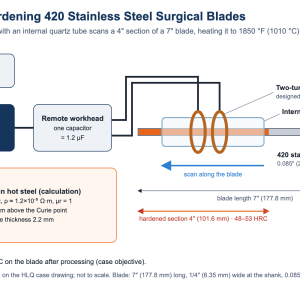
To induction harden stainless steel knife blades, an induction coil heats the blade section to hardening temperature without flame or contact. In this HLQ case, a 4″ (101.6 mm) section of a 7″ (177.8 mm) 420 stainless steel surgical blade was heated to 1850 °F (1010 °C) at 365 kHz. The equipment was a DW-UHF-6kW induction heating system with a remote workhead including one 1.2 µF capacitor, and the coil was a two-turn helical coil with an internal quartz tube designed to scan the blade. The target hardness was 48–53 Rockwell C. Induction heating gave a flameless process, an improved production rate, and consistent and repeatable results.
Table of Contents
- What is Induction Hardening of Stainless Steel Knife Blades?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages and Limitations
- Why Choose HLQ?
- 10 Core FAQs
What is Induction Hardening of Stainless Steel Knife Blades?
Induction hardening of stainless steel knife blades uses a high-frequency magnetic field to heat a defined section of the blade to hardening temperature. Eddy currents generate the heat inside the steel, so the process is flameless and the coil does not touch the blade. HLQ applied this method to 420 stainless steel surgical blades: a 4″ (101.6 mm) section of a 7″ (177.8 mm) blade was heated to 1850 °F (1010 °C) to achieve 48–53 Rockwell C after processing.
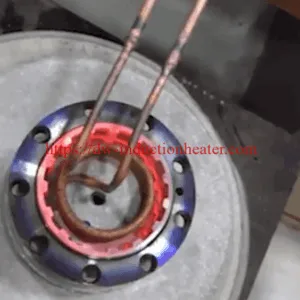
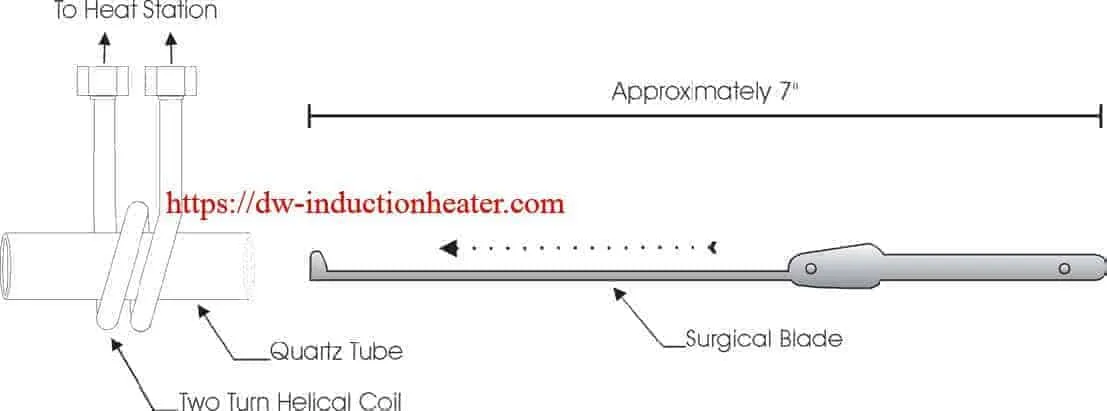
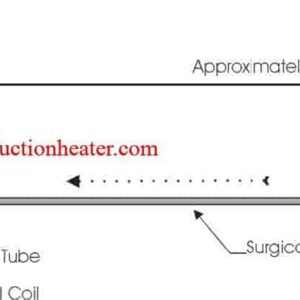
 The case drawing shows the two-turn helical coil with its internal quartz tube, connected to the heat station, and the approximately 7″ surgical blade that it scans.
Key Applications
- Stainless steel surgical blades – 4″ section hardening of 420 stainless blades (this case).
- Carbon steel knife blades – see induction hardening knife blade for an 18″ 1070 steel bed knife.
- Blades and knives before forming – see induction preheating blades and knives.
- Saw teeth – see induction hardening saw teeth of blade.
- Band saw blades – see induction tempering saw blades.
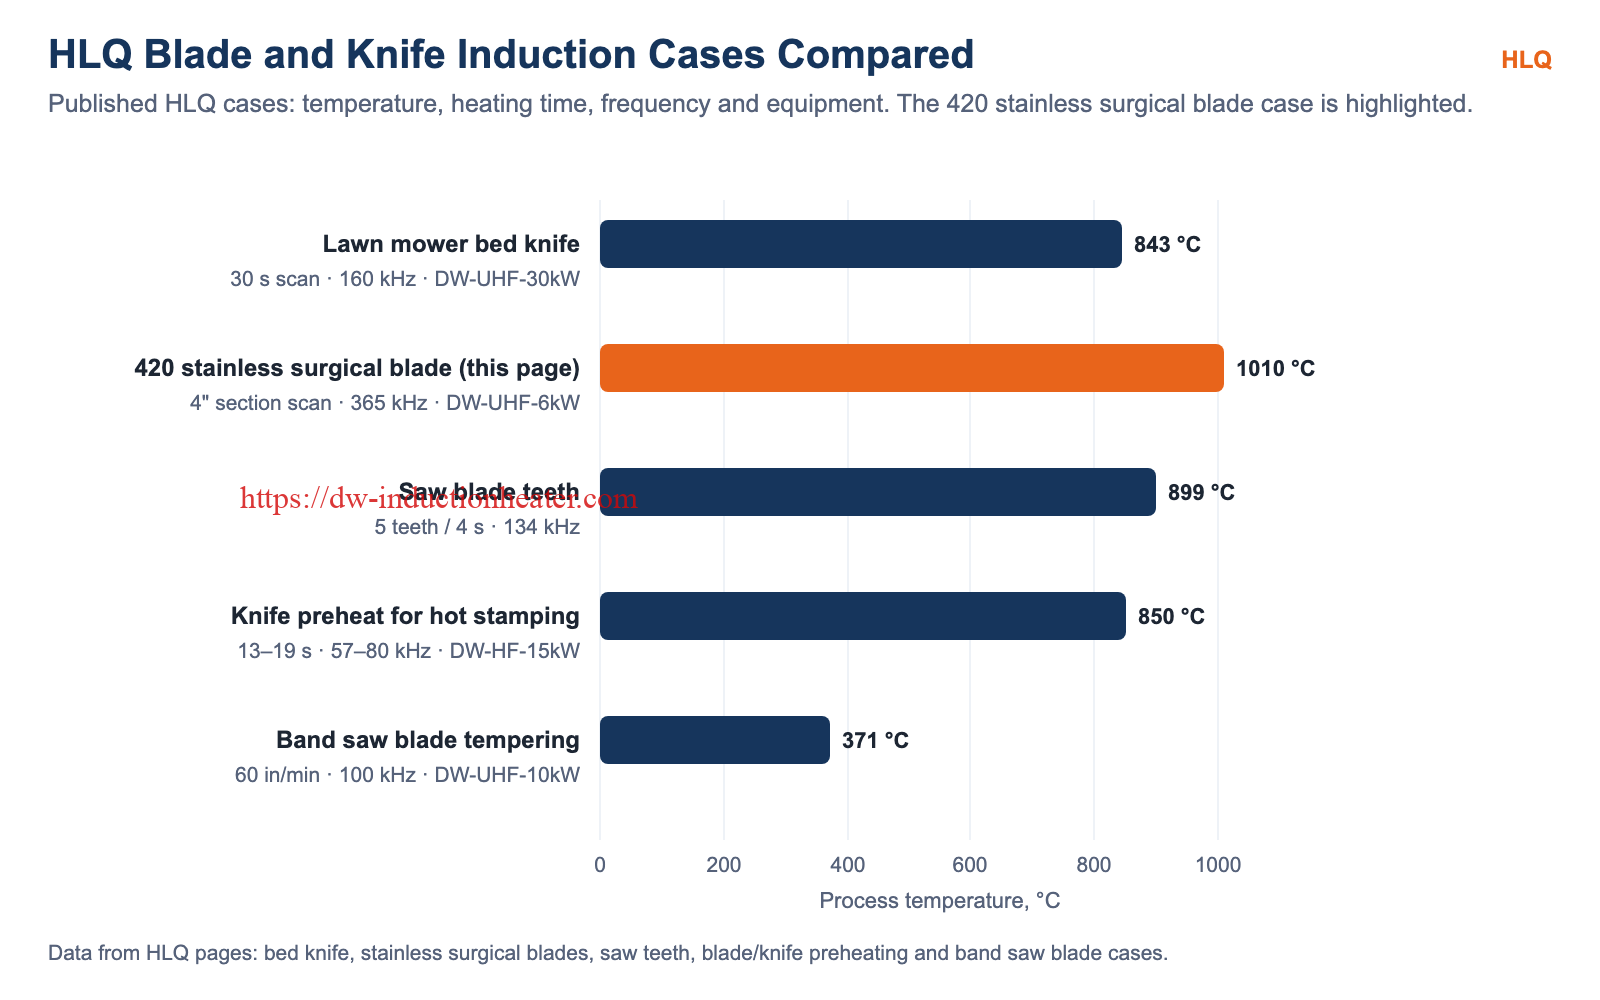
| HLQ case | Temperature | Frequency | Equipment |
|---|---|---|---|
| 420 stainless surgical blades (this page) | 1850 °F (1010 °C) | 365 kHz | DW-UHF-6kW |
| Lawn mower bed knife, 1070 steel | 1550 °F (843.3 °C), 30 s scan | 160 kHz | DW-UHF-30kW |
| Saw blade teeth | 1650 °F (899 °C), five teeth | 134 kHz | – |
| Blade and knife preheating | 850 °C in 13–19 s | 57–80 kHz | DW-HF-15kW |
| Band saw blade tempering | 700 °F (371 °C), 60 in/min | 100 kHz | DW-UHF-10kW |
Suitable Materials
| Material | HLQ case | Process data | Result |
|---|---|---|---|
| 420 stainless steel | Surgical blades, 7″ × 1/4″ × 0.085″ | 1850 °F (1010 °C), 365 kHz | 48–53 HRC on the blade |
| 1070 carbon steel | Lawn mower bed knife, 18″ × 1 17/32″ × 0.135″ | 1550 °F (843.3 °C), 160 kHz | 45–55 HRC at 0.062″ from the edge |
Send the steel grade with your inquiry so the hardening temperature can be confirmed for your blade.
Working Principle
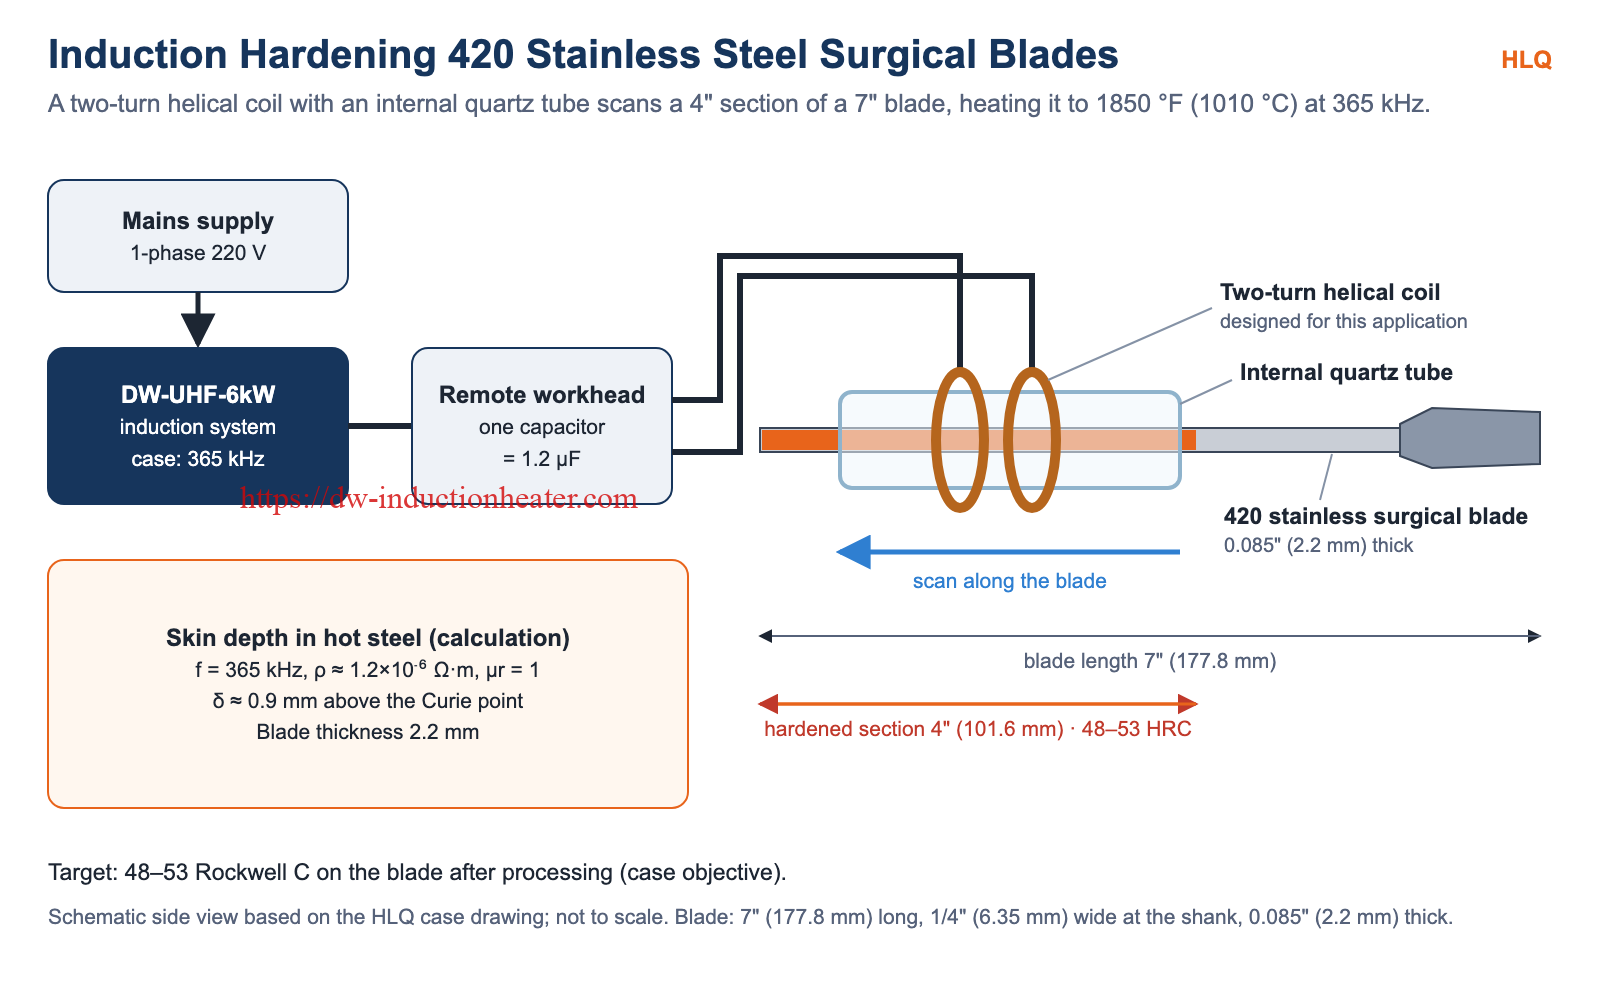
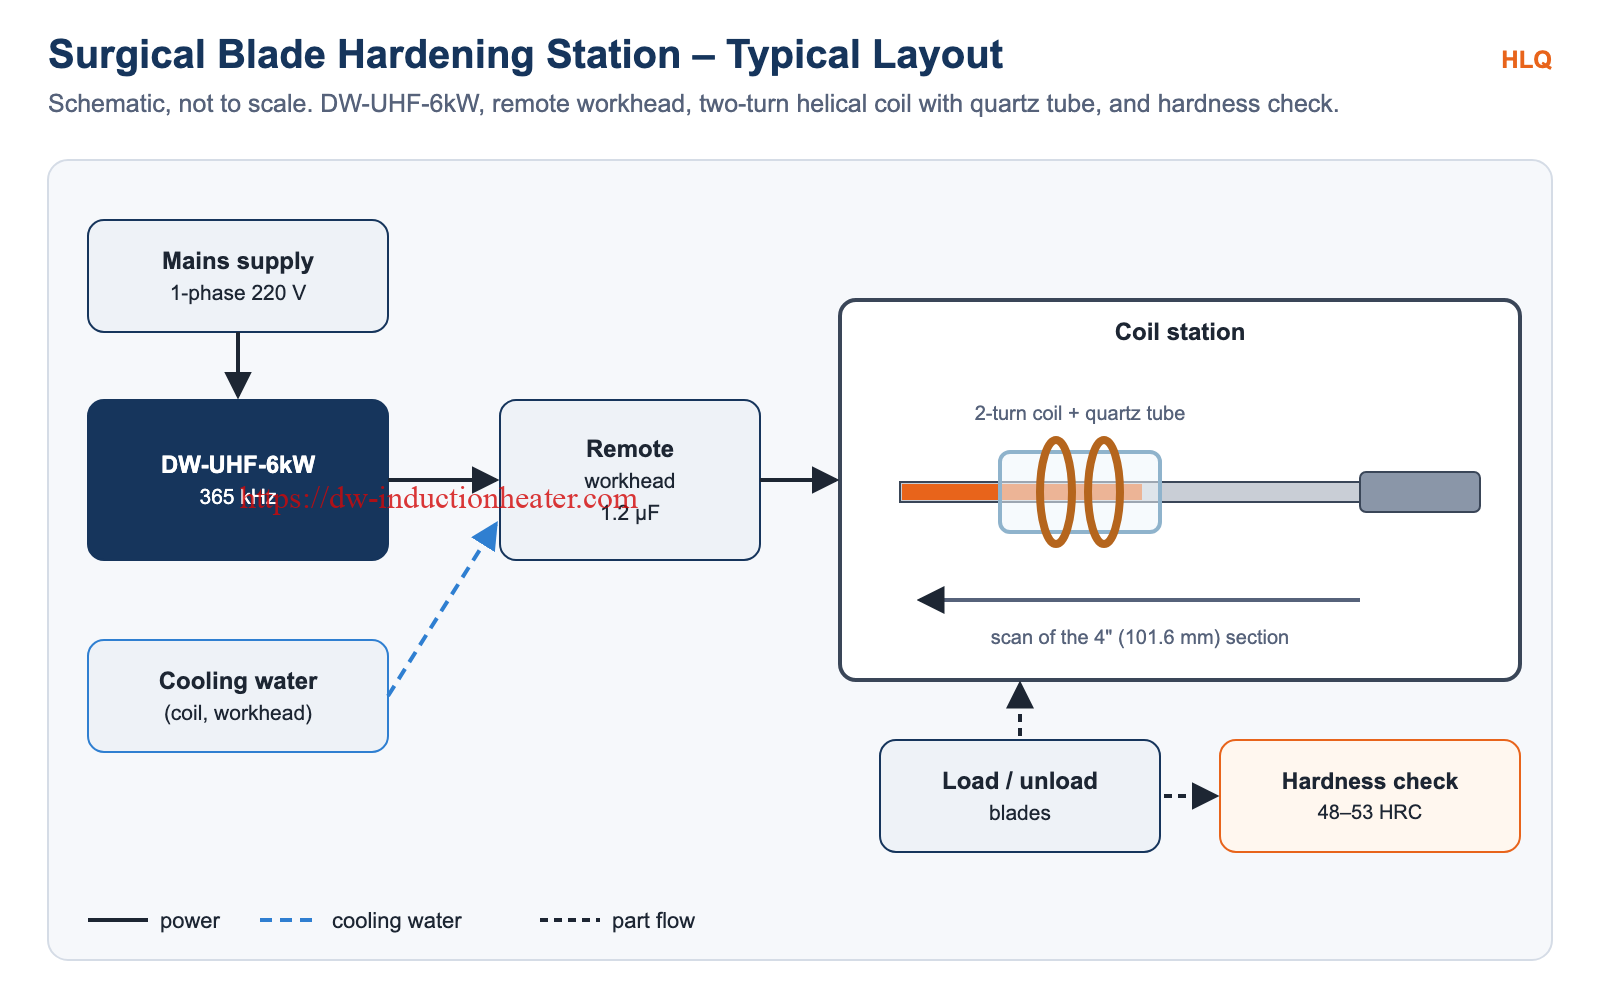
The DW-UHF-6kW supplies 365 kHz current to a remote workhead with one 1.2 µF capacitor. The two-turn helical coil, which has an internal quartz tube, scans the blade. The alternating magnetic field induces eddy currents in the 420 stainless steel and heats the blade to 1850 °F (1010 °C).
Heating depth follows the skin effect. Calculation (δ = 503·√(ρ/f), hot steel above the Curie point, ρ ≈ 1.2×10⁻⁶ Ω·m, µr = 1): at 365 kHz, δ ≈ 0.9 mm, compared with the 2.2 mm blade thickness.
Technical Specifications
| Parameter | Case data |
|---|---|
| Objective | Harden a 4″ (101.6 mm) section of a stainless steel surgical blade measuring 7″ (177.8 mm) long |
| Material | 420 stainless steel surgical blades |
| Blade size | 7″ (177.8 mm) long, 1/4″ (6.35 mm) wide at the shank, 0.085″ (2.2 mm) thick at the blade |
| Temperature | 1850 °F (1010 °C) |
| Frequency | 365 kHz |
| Equipment | DW-UHF-6kW induction heating system with a remote workhead including one (1) capacitor equaling 1.2 µF |
| Coil | Two-turn helical coil with an internal quartz tube, designed and developed specifically for this application |
| Process | The coil is designed to scan the length of the blade, heating it to 1850 °F (1010 °C) |
| Hardness target | 48–53 Rockwell C on the blade after processing |
| Benefits | Flameless process; improved production rate; consistent and repeatable results |
Recommended Model Selection
This case used the DW-UHF-6kW. The DW-UHF series data below comes from the HLQ induction heating device model table.
| Model | Power | Max. input current | Frequency | Supply |
|---|---|---|---|---|
| DW-UHF-4.5kW | 4.5 kW | 20 A | 1.1–2.0 MHz | 1-phase 220 V |
| DW-UHF-6.0kW (this case) | 6.0 kW | 28 A | 300–1100 kHz | 1-phase 220 V |
| DW-UHF-10kW | 10 kW | 15 A | 100–500 kHz | 3-phase 380 V |
| DW-UHF-20kW | 20 kW | 30 A | 50–250 kHz | 3-phase 380 V |
| DW-UHF-30kW | 30 kW | 45 A | 50–200 kHz | 3-phase 380 V |
| DW-UHF-40kW | 40 kW | 60 A | 50–200 kHz | 3-phase 380 V |
| DW-UHF-60kW | 60 kW | 90 A | 50–150 kHz | 3-phase 380 V |
All DW-UHF models are rated for 100% duty cycle.
Process Workflow
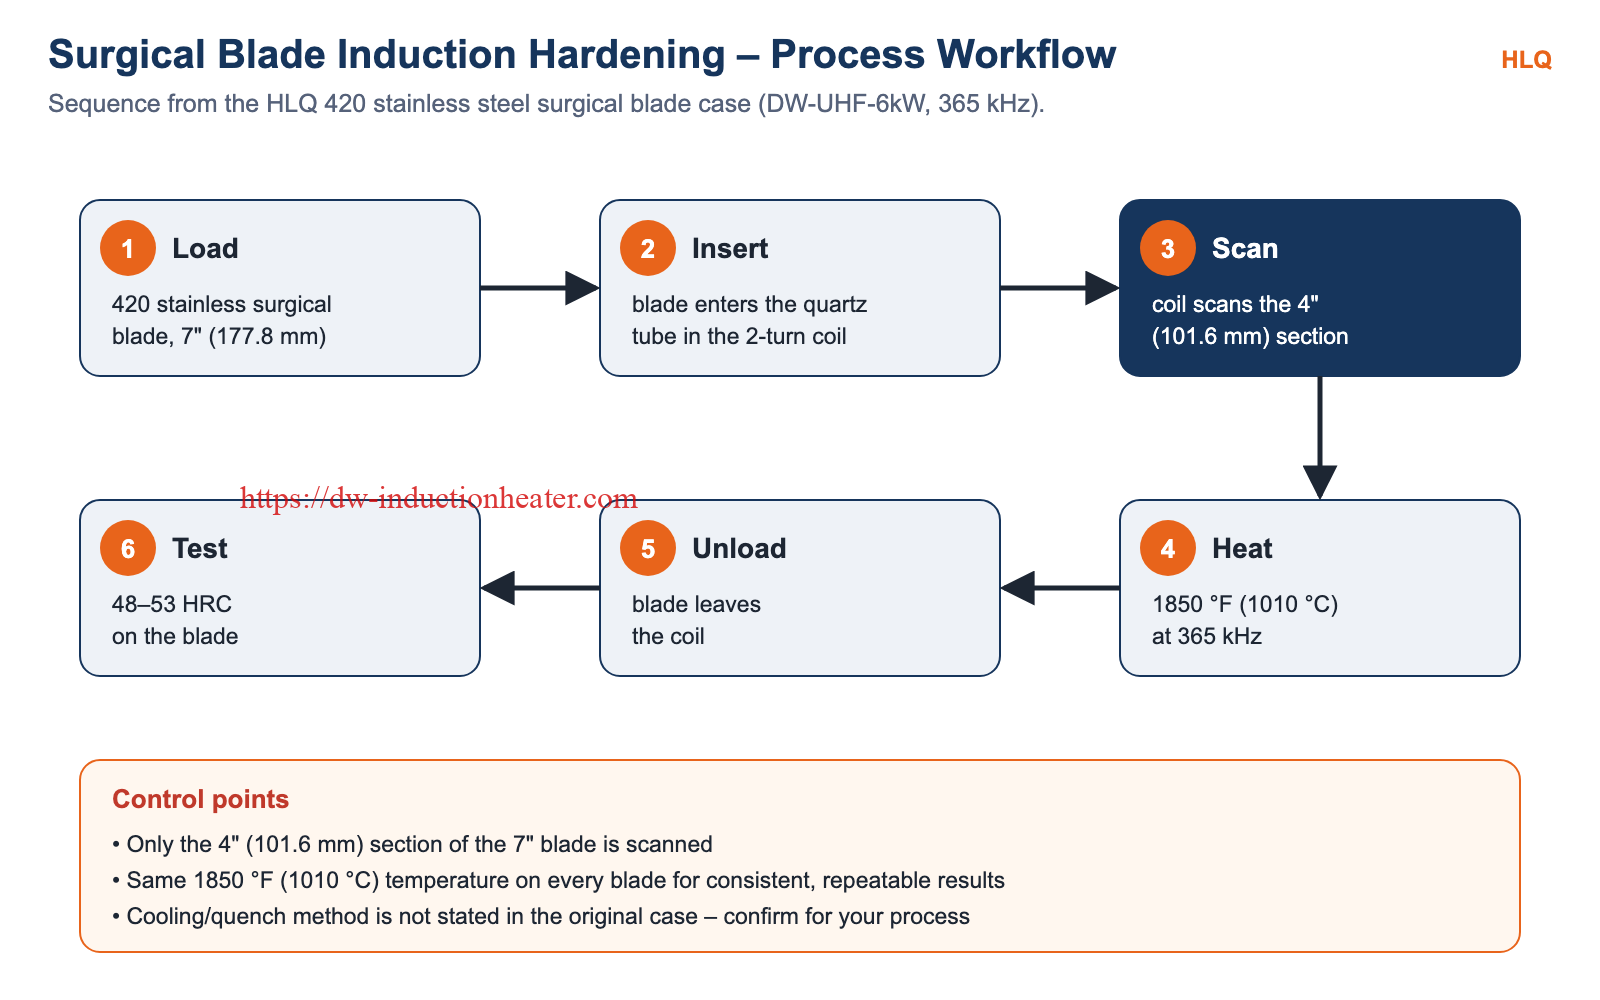
- Load – a 420 stainless steel surgical blade, 7″ (177.8 mm) long.
- Insert – the blade enters the quartz tube inside the two-turn helical coil.
- Scan – the coil scans the blade over the 4″ (101.6 mm) section to be hardened.
- Heat – the blade reaches 1850 °F (1010 °C) at 365 kHz.
- Unload – the blade leaves the coil.
- Test – check for 48–53 Rockwell C on the blade.
The original case does not state the cooling or quench method; confirm it for your process.
Common Problems and Solutions
| Problem | Cause | Solution (from this case) |
|---|---|---|
| Hardness varies from blade to blade | Heating not repeated identically | Induction heating to the same 1850 °F (1010 °C) gives consistent and repeatable results |
| Heat outside the section to be hardened | Coil not matched to the blade | Use a coil designed and developed specifically for the blade; this case used a two-turn helical coil with an internal quartz tube |
| Low output with flame heating | Flame process | Induction heating gives a flameless process and an improved production rate |
| Hardness outside 48–53 HRC | Temperature or cooling not as specified | Verify 1850 °F (1010 °C) and confirm the cooling method for the blade |
For coil design guidance, see induction hardening coil for steel surface hardening.
Engineering Selection Guide
| Frequency | Calculated skin depth in hot steel (µr = 1, ρ ≈ 1.2×10⁻⁶ Ω·m) |
|---|---|
| 300 kHz | ≈ 1.0 mm |
| 365 kHz (this case) | ≈ 0.9 mm |
| 500 kHz | ≈ 0.8 mm |
| 1100 kHz | ≈ 0.5 mm |
- Small, thin stainless blades: DW-UHF-6kW at 365 kHz with a two-turn helical coil (this case).
- Long carbon steel blades, edge zone only: DW-UHF-30kW at 160 kHz with a single-turn channel coil (bed knife case).
- Tempering after hardening: DW-UHF-10kW at 100 kHz (band saw blade case).
- Data to send: blade drawing (length, width, thickness), steel grade, section to be hardened, hardness, parts per hour, available power supply and cooling water.
For other surface hardening tasks, see induction hardening treatment.
Advantages and Limitations
| Advantages | Limitations |
|---|---|
| Flameless process | The coil must be designed for each blade |
| Improved production rate | The cooling method is not documented in this case and must be defined |
| Consistent and repeatable results | Process data applies to 420 stainless blades of these dimensions |
| Non-contact heating of a defined section | Temperature and hardness must be confirmed for other steel grades |
Why Choose HLQ?
- Documented blade cases: stainless surgical blades, bed knives, saw teeth, band saw blades and knife preheating.
- A DW-UHF range from 4.5 kW to 60 kW, all rated for 100% duty cycle.
- Coils designed and developed specifically for each application.
- Remote workheads that put the coil at the point of use.
10 Core FAQs
1. What was hardened in this case?
A 4″ (101.6 mm) section of a 7″ (177.8 mm) 420 stainless steel surgical blade.
2. What hardness was specified?
48 to 53 Rockwell C on the blade after processing.
3. What temperature was used?
1850 °F (1010 °C).
4. Which frequency was used?
365 kHz.
5. Which induction machine was used?
A DW-UHF-6kW induction heating system with a remote workhead including one 1.2 µF capacitor.
6. Which coil was used?
A two-turn helical coil with an internal quartz tube, designed to scan the length of the blade.
7. What are the blade dimensions?
7″ (177.8 mm) long, 1/4″ (6.35 mm) wide at the shank, and 0.085″ (2.2 mm) thick at the blade.
8. What are the benefits of induction heating here?
A flameless process, an improved production rate, and consistent and repeatable results.
9. How deep does 365 kHz heat in hot steel?
Calculated skin depth is about 0.9 mm above the Curie point, compared with the 2.2 mm blade thickness.
10. What information is needed for a quotation?
The blade drawing, steel grade, section to be hardened, hardness, output, and available power supply and cooling water.
HLQ-Induction-Hardening-Stainless-Steel-Knife-Blades-Brochure