


Induction Forging
Induction Forging & Hot Forming: Billet, Bar and End Heating
Quick Answer
Induction forging and hot forming use induction heating to bring a metal billet, bar or block to a temperature at which its resistance to deformation is weak, so it can be forged, bent or shaped. Approximate hot forming temperatures are 1200 °C for steel, 750 °C for brass and 550 °C for aluminium. Parts can be heated completely (billets, bars, brass and titanium blocks) or only at the forming zone (pipe ends, axle ends, automotive parts and bar ends). Compared with conventional furnaces, induction gives much shorter heating times with less scaling and oxidation, accurate temperature control, no furnace ramp-up, automated operation and greater thermal efficiency.
Table of Contents
- What is Induction Forging & Hot Forming?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages and Limitations
- Why Choose HLQ?
- 10 Core FAQs
What is Induction Forging & Hot Forming?
Forging and hot forming are methods of plastically deforming metal. Industrial forging and hot forming processes bend or shape a metal billet or bloom after it has been heated to a temperature at which its resistance to deformation is weak. Induction heating is an excellent way to reach that temperature: the heat is generated in the part itself, so it does not need to be produced in a large chamber. Blocks of non-ferrous materials can also be used, and induction forging solutions have been installed in many countries, mainly in the metal and foundry sector.
Key Applications
Total Forging / Hot Forming Applications
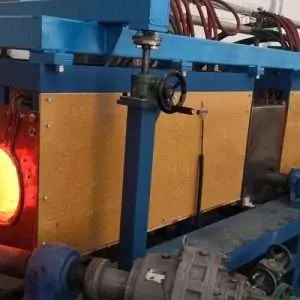
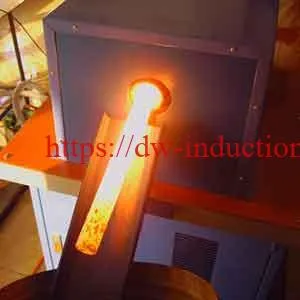
Induction heating machines are commonly used to heat steel billets, bars, brass blocks and titanium blocks to the proper temperature for forging and hot forming.

Ends Forging / Hot Forming Applications
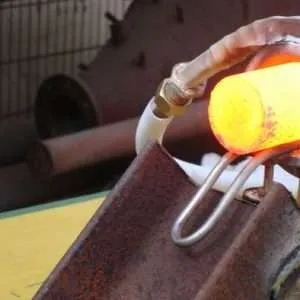
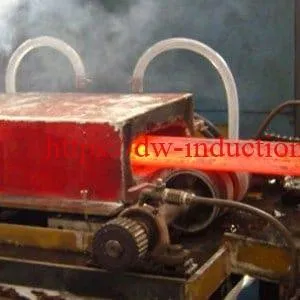
Induction heating is also used to heat parts such as pipe ends, axle ends, automotive parts and bar ends for partial forming and forging. An HLQ example is induction forging steel rod ends.
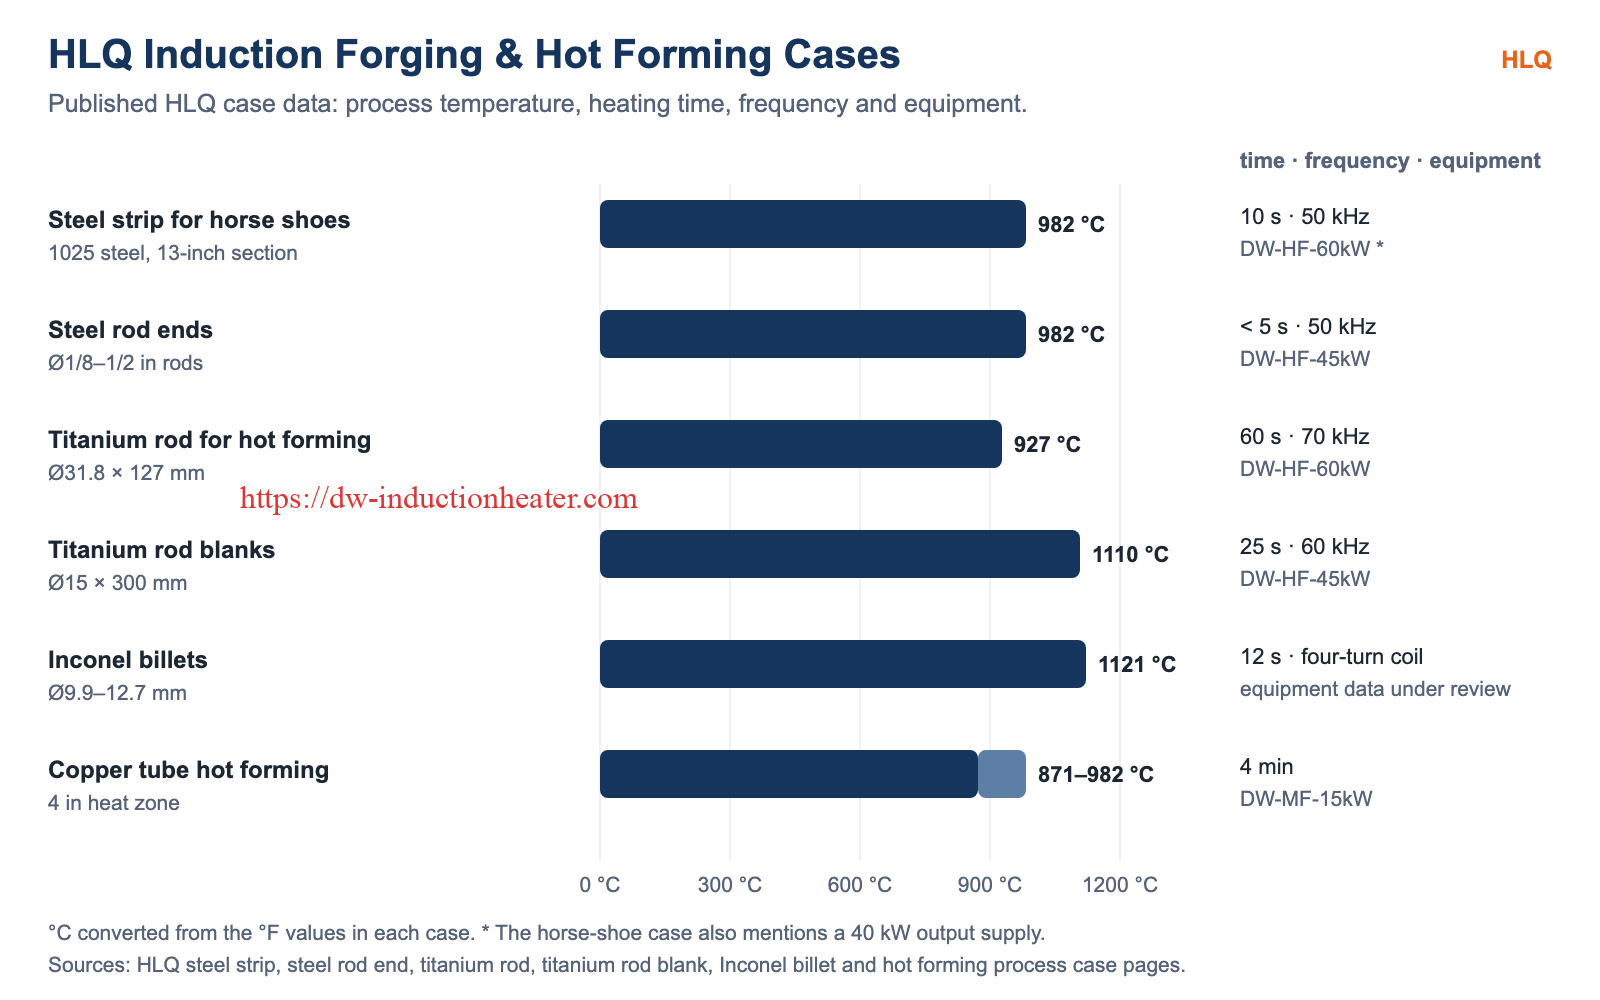
| HLQ case | Part | Temperature | Time | Frequency / equipment |
|---|---|---|---|---|
| Steel strip for horse shoes | 1025 steel strip, 13″ section | 1800 °F | 10 s | 50 kHz |
| Steel rod ends | Rods 1/8″–1/2″ diameter | 1800 °F | < 5 s | 50 kHz, DW-HF-45kW |
| Induction hot forming titanium rod | Ø31.8 × 127 mm | 1700 °F (926.7 °C) | 60 s | 70 kHz, DW-HF-60kW |
| Induction forging titanium rods | Ø15 × 300 mm rod blanks | 2030 °F (1110 °C) | 25 s | 60 kHz, DW-HF-45kW |
| Copper tube hot forming | 4 in heat zone | 1600–1800 °F (871–982 °C) | 4 min | DW-MF-15kW |
Suitable Materials
Materials processed with induction forging and hot forming include aluminium, brass, copper, steel, iron and stainless steel; titanium blocks are also heated. Typical heating ranges come from the HLQ induction forging billet heating guide.
| Material | Approximate hot forming temperature (this page) | HLQ typical heating range | Notes (HLQ guide) |
|---|---|---|---|
| Steel | 1200 °C | 1050–1250 °C | Magnetic below the Curie point; heats efficiently |
| Stainless steel | – | 1050–1180 °C | – |
| Brass | 750 °C | 600–800 °C | Easy to control; stable billet temperature |
| Copper | – | 650–850 °C | Non-magnetic, very high conductivity; needs optimized power matching |
| Aluminium | 550 °C | 350–550 °C (alloy) | Avoid overheating |
| Titanium alloy | – | 850–1100 °C | Narrow temperature window; tight control required |
Working Principle
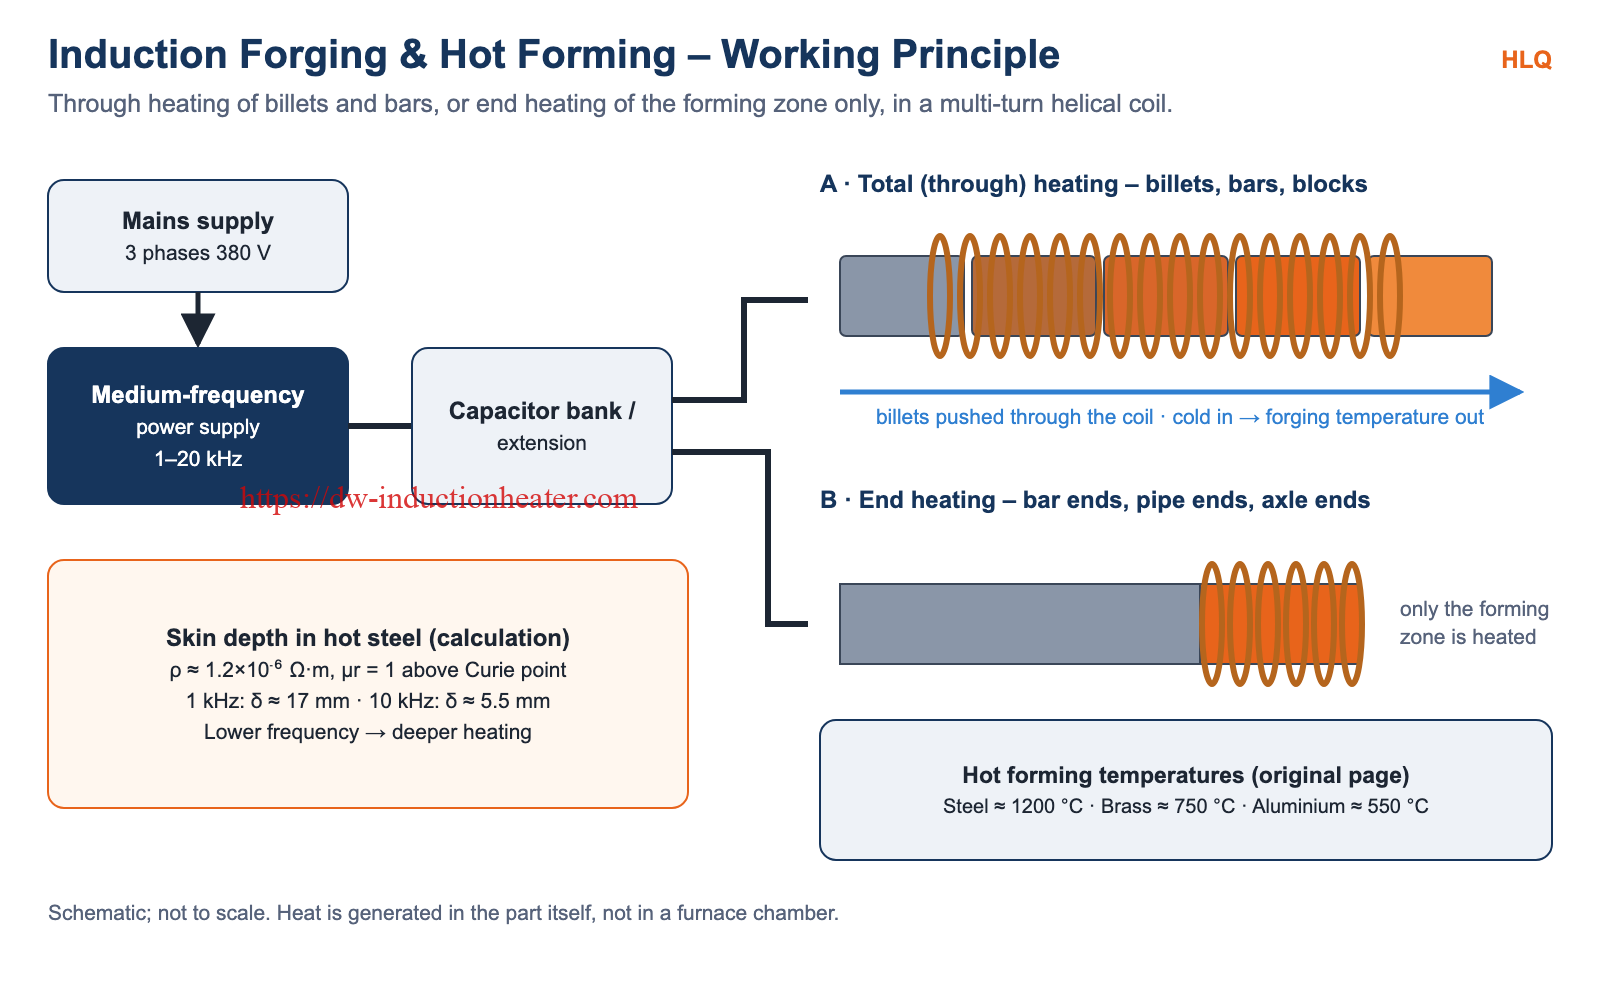
The power supply drives alternating current through a water-cooled, multi-turn helical copper coil. The magnetic field induces eddy currents in the billet, which heats from the inside of the part rather than from a furnace chamber. In through heating, billets are pushed through the coil and leave at forging temperature. In end heating, only the bar, pipe or axle end that will be formed sits inside the coil.
The heated layer depth follows the skin effect. Calculation (δ = 503·√(ρ/f), hot steel above the Curie point, ρ ≈ 1.2×10⁻⁶ Ω·m, µr = 1): δ ≈ 17 mm at 1 kHz and ≈ 5.5 mm at 10 kHz. Lower frequency gives deeper heating, so larger billets use lower frequencies.
Technical Specifications
HLQ forge furnace data by system size (steel billets):
| Parameter | 80–250 kW | 250–500 kW | 500–1000 kW |
|---|---|---|---|
| Operating frequency | 500–3000 Hz | 300–1000 Hz | 150–600 Hz |
| Heating capacity | 100–300 kg/hr | 300–800 kg/hr | 800–2500 kg/hr |
| Temperature range | 900–1250 °C | 900–1250 °C | 900–1250 °C |
| Typical billet size | Ø30–100 mm | Ø80–180 mm | Ø150–300 mm |
| Heating time | 1–5 min | 3–8 min | 5–15 min |
| Energy consumption | 350–450 kWh/ton | 300–400 kWh/ton | 280–380 kWh/ton |
| Cooling water | 15–40 m³/hr | 40–80 m³/hr | 80–160 m³/hr |
| Material (80–250 kW systems) | Frequency | Capacity | Temperature | Size | Heating time |
|---|---|---|---|---|---|
| Steel billets | 500–3000 Hz | 100–300 kg/hr | 900–1250 °C | Ø30–100 mm | 1–5 min |
| Copper bars | 800–5000 Hz | 150–400 kg/hr | 700–950 °C | Ø20–80 mm | 0.8–3 min |
| Aluminium rods | 1000–8000 Hz | 180–500 kg/hr | 400–550 °C | Ø20–80 mm | 0.5–2 min |
| Component | Specification |
|---|---|
| Input voltage | 380–480 V, 3-phase, 50/60 Hz |
| Power factor | 0.92–0.98 with power factor correction |
| Conversion efficiency | 85–95% |
| Cooling | Water-cooled, closed-loop deionized water system (conductivity < 20 µS/cm) |
| Control | PLC with HMI touchscreen |
| Coil | Multi-turn helical copper tubing, pressurized water cooling |
Source: HLQ induction forge furnaces for hot forming steel billets.
Recommended Model Selection
DW-MF induction heating rod forging furnaces, from the HLQ induction heating device model table:
| Model | Max. input power | Max. input current | Frequency | Input voltage | Duty cycle |
|---|---|---|---|---|---|
| DW-MF-45 | 45 kW | 68 A | 1–20 kHz | 3 phases 380 V ±10% | 100% |
| DW-MF-70 | 70 kW | 105 A | 1–20 kHz | 3 phases 380 V ±10% | 100% |
| DW-MF-90 | 90 kW | 135 A | 1–20 kHz | 3 phases 380 V ±10% | 100% |
| DW-MF-110 | 110 kW | 170 A | 1–20 kHz | 3 phases 380 V ±10% | 100% |
| DW-MF-160 | 160 kW | 240 A | 1–20 kHz | 3 phases 380 V ±10% | 100% |
Larger units from the induction forging bar and billet furnace page:
| Model | DW-MF-200 | DW-MF-250 | DW-MF-300 | DW-MF-400 | DW-MF-500 | DW-MF-600 |
|---|---|---|---|---|---|---|
| Max. input current | 320 A | 400 A | 480 A | 640 A | 800 A | 960 A |
| Weight (host) | 110 kg | 150 kg | 160 kg | 170 kg | 200 kg | 220 kg |
DW-MF-200 to 600: 3 phases 380/410/440 V, 50/60 Hz; oscillating frequency 0.5–20 kHz, customized to the part size; 100% duty, 24 h continuous work; cooling water 0.1–0.3 MPa, hardness < 50. Small rods and bar ends in HLQ cases used DW-HF units (DW-HF-45kW and DW-HF-60kW, 50–70 kHz).
Process Workflow

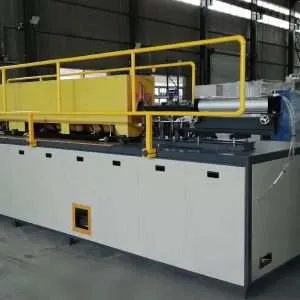
- Bar stock – billets, bars or blocks are loaded.
- Cut – cut to forging length.
- Feed – roller or pusher feed into the coil.
- Heat – the induction coil heats the part to forging temperature.
- Check – a pyrometer checks temperature; parts outside specifications are detected and removed.
- Transfer – automatic transfer to the press.
- Forge – forging or hot forming.

Common Problems and Solutions
| Problem | Cause | Solution (HLQ data) |
|---|---|---|
| Scaling and oxidation | Long heating times in conventional furnaces | Induction’s much shorter heating time minimizes scaling and oxidation |
| Parts at the wrong temperature reach the press | No temperature check | Detect parts outside specification with a pyrometer and remove them |
| Centre colder than surface on thicker bars | Time needed to conduct heat from the outside edge to the centre | In the HLQ 1/2″ rod case, heating was limited by heat transfer to the centre without melting the surface; allow enough heating time |
| Low efficiency on very small diameters | Frequency too low for the diameter | In the same case, the 1/8″ rod was limited by induction efficiency at the chosen frequency; match frequency to diameter |
| Waiting for the heater | Furnace ramp-up | Induction needs no ramp-up time |
| Whole part heated when only one area is formed | Furnace heating | Direct heat to one specific point with end heating |
Engineering Selection Guide
| Frequency | Calculated skin depth in hot steel (µr = 1, ρ ≈ 1.2×10⁻⁶ Ω·m) | HLQ data at this frequency |
|---|---|---|
| 1 kHz | ≈ 17 mm | Steel billets Ø80–300 mm: 150–1000 Hz (250–1000 kW systems) |
| 10 kHz | ≈ 5.5 mm | Within the DW-MF 1–20 kHz range |
| 30 kHz | ≈ 3.2 mm | – |
| 50 kHz | ≈ 2.5 mm | Steel rod ends and steel strip cases |
- Total or end heating: billets and bars heated through, or only the end that is formed.
- Material: it sets the temperature (steel ≈ 1200 °C, brass ≈ 750 °C, aluminium ≈ 550 °C).
- Billet size: it sets the frequency. Larger billets use lower frequency (see the system tables).
- Output: kg/hr or parts per hour sets the power, from 80–250 kW (100–300 kg/hr of steel) to 500–1000 kW (800–2500 kg/hr).
- Utilities: confirm the supply voltage and cooling water capacity.
Advantages and Limitations
| Advantages (compared with conventional furnaces) | Limitations |
|---|---|
| 1. Much shorter heating times, minimizing scaling and oxidation | The coil must suit the billet or bar size |
| 2. Easy and accurate temperature control; parts outside specifications can be detected and removed | Frequency must be matched to the diameter |
| 3. No time lost waiting for the furnace to ramp up | Water cooling is required for the coil and power supply |
| 4. Automated induction heating machines require minimal manual labour | Thick sections need time for heat to reach the centre |
| 5. Heat can be directed to one specific point, important for parts with only one forming area | – |
| 6. Greater thermal efficiency: heat is generated in the part itself | – |
| 7. Better working conditions: the only heat in the air is that of the parts | – |
Why Choose HLQ?
- DW-MF rod forging furnaces from 45 to 160 kW, DW-MF-200 to 600 for larger lines, and DW-HF units for small rods and ends.
- Published forging and hot forming cases in steel, titanium, Inconel and copper.
- Complete lines: feeder, coil line, pyrometer sorting and closed-loop cooling.
- Induction forging solutions installed in many countries, mainly in the metal and foundry sector.
10 Core FAQs
1. What is induction forging and hot forming?
Heating a metal billet, bar or block by induction to a temperature at which its resistance to deformation is weak, before it is forged, bent or shaped.
2. Which materials can be forged with induction heating?
Aluminium, brass, copper, steel, iron and stainless steel; titanium blocks and other non-ferrous blocks can also be heated.
3. What are typical hot forming temperatures?
Approximately 1200 °C for steel, 750 °C for brass and 550 °C for aluminium.
4. What is the difference between total and end heating?
Total heating brings the whole billet or bar to temperature; end heating heats only pipe ends, axle ends, automotive parts or bar ends for partial forming.
5. Why use induction instead of a fuel furnace?
Shorter heating times, less scaling and oxidation, accurate temperature control, no ramp-up, minimal manual labour, higher thermal efficiency and better working conditions.
6. Which HLQ machines are used for forging?
DW-MF induction heating rod forging furnaces (45–160 kW, 1–20 kHz) and DW-MF-200 to DW-MF-600 (0.5–20 kHz) for larger lines.
7. How is the frequency chosen?
By billet size: lower frequency heats deeper. HLQ steel billet systems use 500–3000 Hz for Ø30–100 mm and 150–600 Hz for Ø150–300 mm.
8. What output can an induction forge furnace reach?
For steel billets, 100–300 kg/hr with 80–250 kW systems and up to 800–2500 kg/hr with 500–1000 kW systems.
9. How fast can small bars be heated?
In HLQ cases, steel rod ends reached 1800 °F in under 5 seconds, and a 13″ section of steel strip reached 1800 °F in 10 seconds.
10. What information is needed for a quotation?
The material, billet or bar diameter and length, forging temperature, total or end heating, output, and available power supply and cooling water.
Related products
-

Steel Billet Heating Furnace with Induction For forging rolling mills and extrusion bars-billets-rods
-
Aluminium Billet Induction Heater for Extrusion Energy Efficient Metals Heating Solution
-
Induction Forging Bar and Billet Furnace
-
Steel Bar Induction Forging, Aluminum Billet Induction Heating, Titanium Rod Forging Heater, Brass Extrusion Die Induction Heater, Copper Billet Induction Heating-Ferrous Billet Induction Forging
-
Induction Heating titanium and stainless steel for hot heading