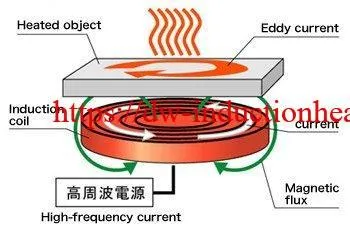
A source of high frequency electricity is used to drive a large alternating current through a induction coil. This induction heating coil is known as the work coil. See the picture opposite.
The passage of current through this induction heating coil generates a very intense and rapidly changing magnetic field in the space within the work coil. The workpiece to be heated is placed within this intense alternating magnetic field.
Depending on the nature of the workpiece material, a number of things happen…
The alternating magnetic field induces a current flow in the conductive workpiece. The arrangement of the work coil and the workpiece can be thought of as an electrical transformer. The work coil is like the primary where electrical energy is fed in, and the workpiece is like a single turn secondary that is short-circuited. This causes tremendous currents to flow through the workpiece. These are known as eddy currents.
In addition to this, the high frequency used in Induction Heating applications gives rise to a phenomenon called skin effect. This skin effect forces the alternating current to flow in a thin layer towards the surface of the workpiece. The skin effect increases the effective resistance of the metal to the passage of the large current. Therefore it greatly increases the induction heating effect of the induction heater caused by the current induced in the workpiece.
Magnetic Induction Heater is a process equipment which is used to melt,braze,forge,bond,heat treating,harden or soften metals or other conductive materials. For many modern manufacturing processes, Magnetic induction heating equipment offers an attractive combination of speed, consistency and control.The basic principles of magnetic induction heating have been understood and applied to manufacturing since the 1920s. During World War II, the technology developed rapidly to meet urgent wartime requirements for a fast, reliable process to harden metal engine parts. More recently, the focus on lean manufacturing techniques and emphasis on improved quality control have led to a rediscovery of induction technology, along with the development of precisely controlled, all solid state induction power supplies.
Magnetic Induction Heaterrelies on the unique characteristics of induction heating radio frequency (RF) energy – that portion of the electromagnetic spectrum below infrared and microwave energy. Since heat is transferred to the product via electromagnetic waves, the part never comes into direct contact with any flame, the inductor itself does not get hot, and there is no product contamination. When properly set up, the process becomes very repeatable and controllable.
Main Characteristics:
1.IGBT module and soft switiching inverting technologies are as in the production of the generator,higher reliability can be do.
2. Small and portable ,compared with SCR controlled machine only 1/10 working space is needed.
3. High efficiency to save energy,high efficiency and power far can be maintained
4. The generator is adatable in a large frequency range from 1KHZ to 1100KHZ,installation can be done very easily according to our manual.
5. 100%duty cycle ,continuous working ability at maximum power.
6. Constant power or constant voltage control mode.
7. Display of output power,output frequency,and output voltage.
Induction Heating Magnetic Iron Oxide in water for hyperthermia application
Objective Heating magnetic iron oxide (Fe2O3) in water for hyperthermia application to determine the curve of temperature vs. time during induction heating
Material Magnetic iron oxide in water (magnetic field is 50-200kHz, 30kA/m), glass vial
Temperature Varies
Frequency 344 kHz
Equipment • DW-UHF-4.5kW induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66 μF
• An induction heating coil designed and developed specifically for this application.
Process A two turn helical coil is used to heat the glass vial. The temperature vs. time results are:
• 66º – 107 ºF (19º – 42 ºC) in 10 seconds
• 66º – 145 ºF (19º – 63 ºC) in 20 seconds
• 66º – 170 ºF (19º – 77 ºC) in 30 seconds
Results/Benefits Induction heating provides:
• Rapid & localized heating
• Uniform controllable heat
• Small bench top footprint
• Even distribution of heating
Manage Consent
To provide the best experiences, we use technologies like cookies to store and/or access device information. Consenting to these technologies will allow us to process data such as browsing behavior or unique IDs on this site. Not consenting or withdrawing consent, may adversely affect certain features and functions.
Functional
Always active
The technical storage or access is strictly necessary for the legitimate purpose of enabling the use of a specific service explicitly requested by the subscriber or user, or for the sole purpose of carrying out the transmission of a communication over an electronic communications network.
Preferences
The technical storage or access is necessary for the legitimate purpose of storing preferences that are not requested by the subscriber or user.
Statistics
The technical storage or access that is used exclusively for statistical purposes.The technical storage or access that is used exclusively for anonymous statistical purposes. Without a subpoena, voluntary compliance on the part of your Internet Service Provider, or additional records from a third party, information stored or retrieved for this purpose alone cannot usually be used to identify you.
Marketing
The technical storage or access is required to create user profiles to send advertising, or to track the user on a website or across several websites for similar marketing purposes.
 Induction_heating_catalogue.pdf
