Induction Bonding Rubber To Steel
Induction Bonding Rubber To Steel With High Frequency Heating System
Quick Answer
Induction bonding of rubber to steel heats the steel part so that rubber placed on it bonds at a controlled temperature. In the HLQ case, flat and round rubber gaskets were bonded to the top and bottom of a steel gas tank assembly. Two two-turn pancake coils, contoured to the shape of the tank, produced uniform heat in the gasket areas. A DW-UHF-10kW ran at 200 kHz for the flat gasket and 231 kHz for the round gasket, and reached the 320 °F (160 °C) bonding temperature in 6.5 seconds, within the 300–350 °F (148.9–176.7 °C) window. The result was repeatable, rapid and accurate heating cycles with even heat distribution.
Table of Contents
- What is Induction Bonding of Rubber to Steel?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages and Limitations
- Why Choose HLQ?
- 10 Core FAQs
What is Induction Bonding of Rubber to Steel?
Induction bonding of rubber to steel uses an induction coil to heat the steel at the joint, and the rubber gasket in contact with it bonds at the required temperature. The rubber is not heated directly; the heat comes from the steel. It is one form of induction bonding, which is also used for plastics, polymers and adhesives.
Key Applications
- Rubber gaskets on steel gas tanks: flat and round gaskets on the top and bottom of the assembly (this page).
- Steel clips press-bonded into rubber seals: see bonding steel into rubber with induction.
- Polymer encapsulant on solar panel shingles: see induction bonding solar panel.
- Plastic catheter tubing: see induction heating plastic catheter tube.
- Metal inserts in plastic parts: see induction heating stainless steel insertion.
| HLQ case | Temperature | Time | Frequency | Equipment |
|---|---|---|---|---|
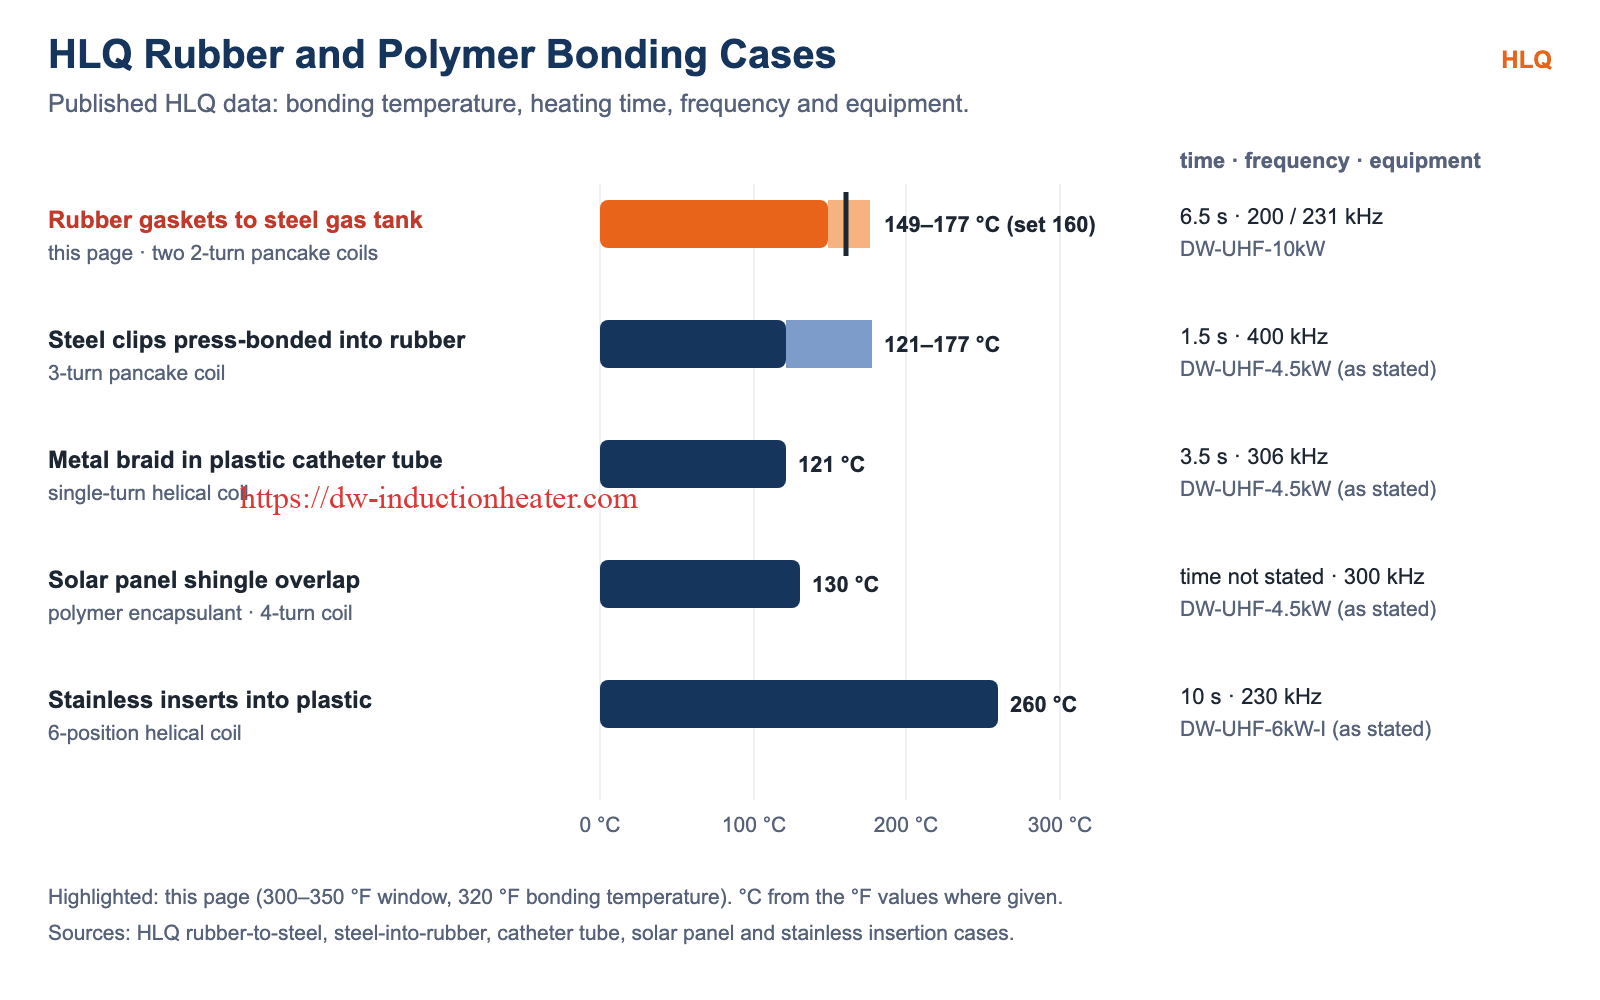
| Rubber gaskets to steel gas tank (this page) | 320 °F (160 °C) | 6.5 s | 200 / 231 kHz | DW-UHF-10kW |
| Steel clips press-bonded into rubber | 250–350 °F (121–177 °C) | 1.5 s | 400 kHz (as stated) | DW-UHF-4.5kW |
| Metal braid in plastic catheter tube | 250 °F (121 °C) | 3.5 s | 306 kHz (as stated) | DW-UHF-4.5kW |
| Solar panel shingle overlap | 130 °C | – | 300 kHz (as stated) | DW-UHF-4.5kW |
| Stainless steel inserts into plastic | 500 °F (260 °C) | 10 s | 230 kHz (as stated) | DW-UHF-6kW-I |
Suitable Materials
| Steel part (heated) | Rubber / polymer (bonded) | HLQ source |
|---|---|---|
| Steel gas tank assembly | Flat and round rubber gaskets | This page |
| Steel clips | Rubber sealer blocks | Steel-into-rubber case |
| Stainless steel substrate | Polymer encapsulant | Solar panel case |

Working Principle
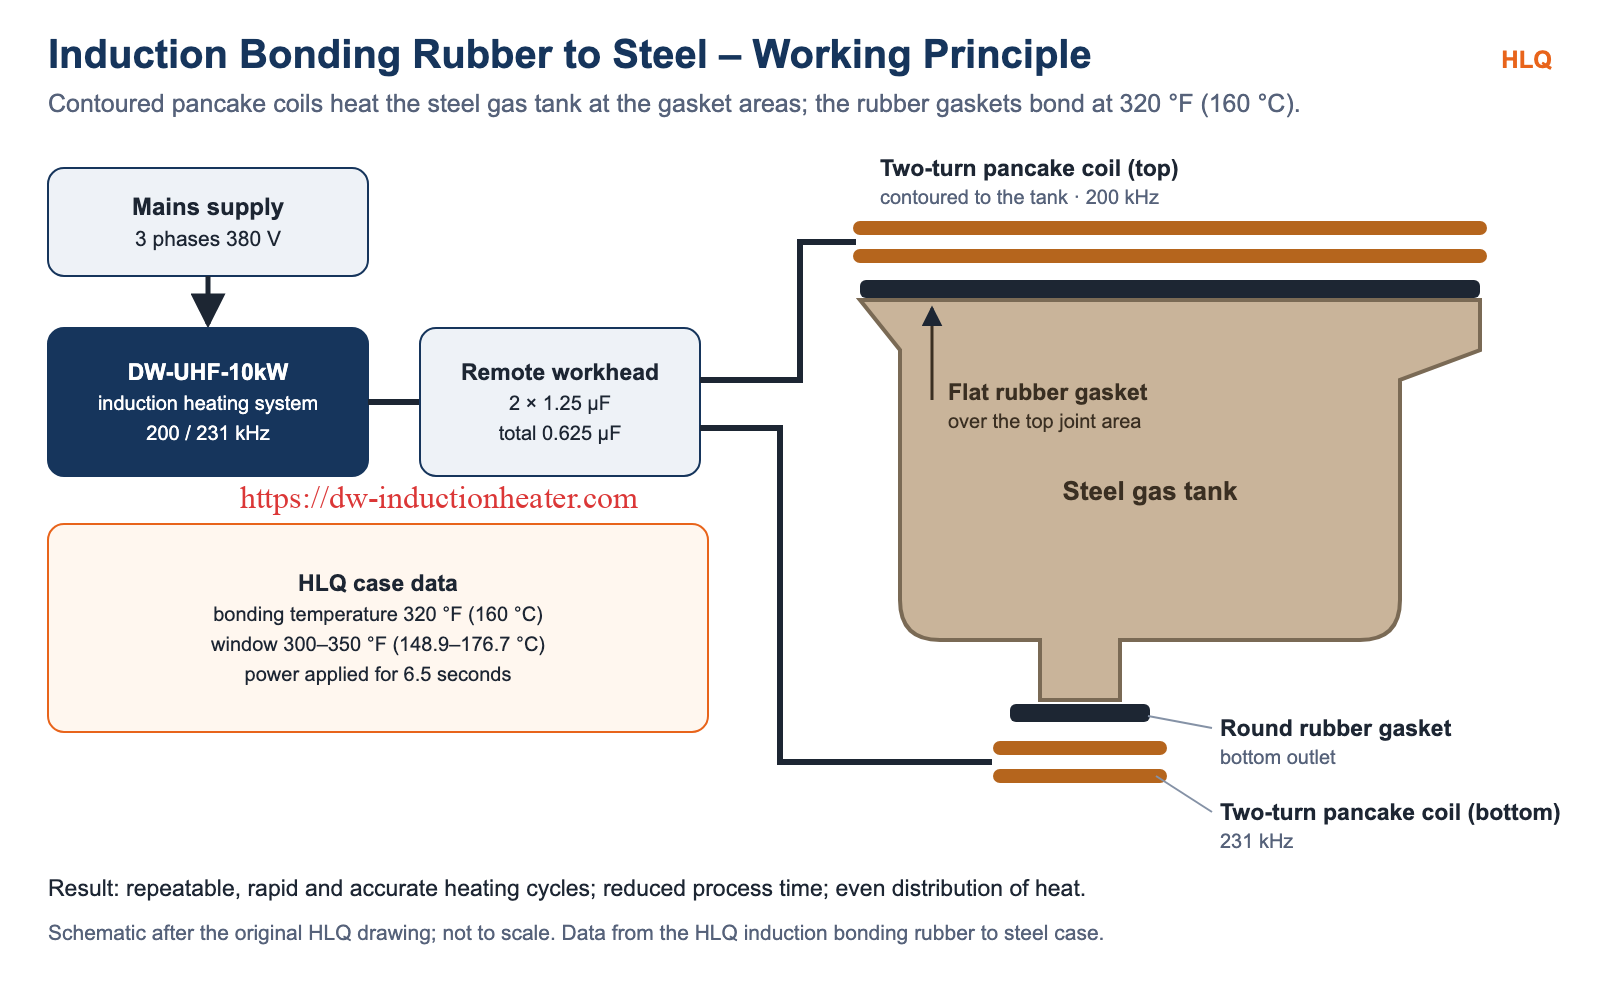
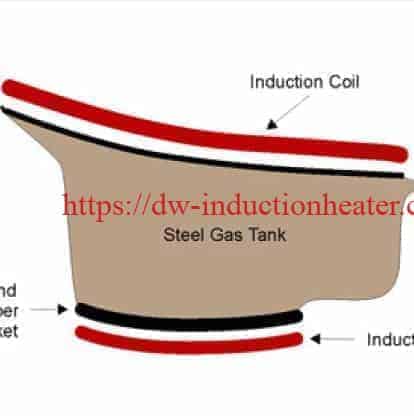
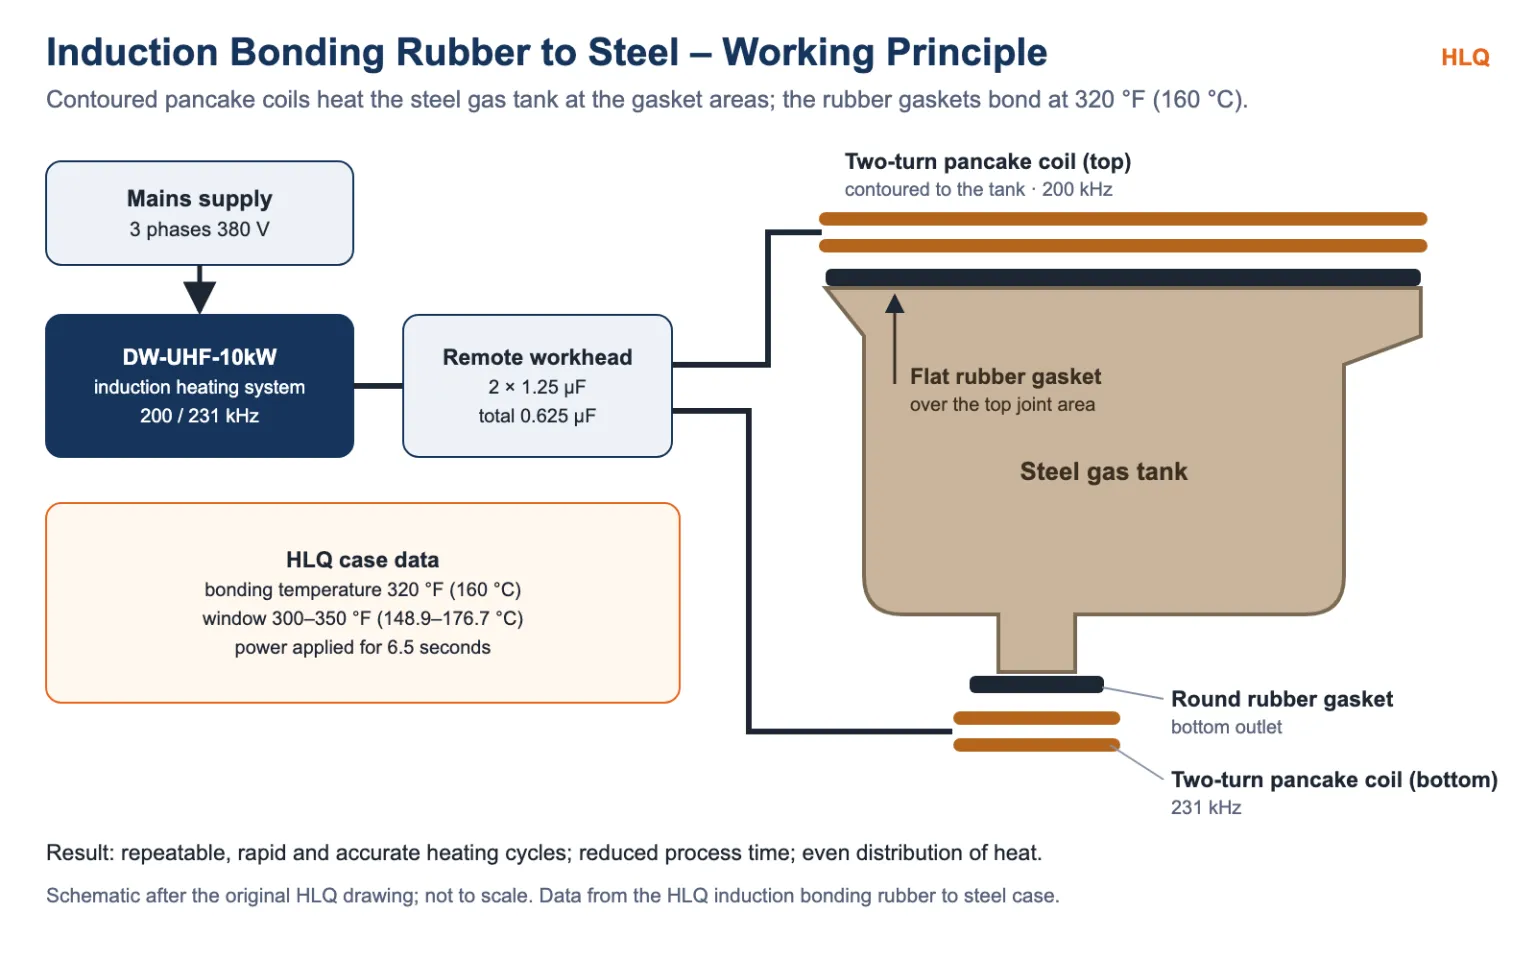
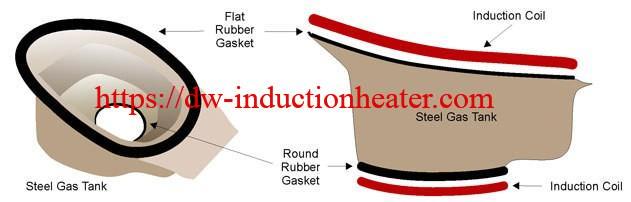
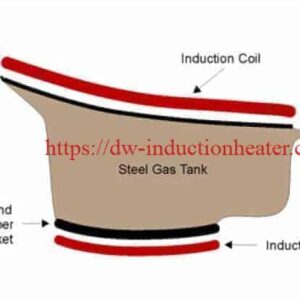
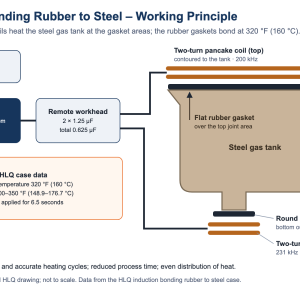
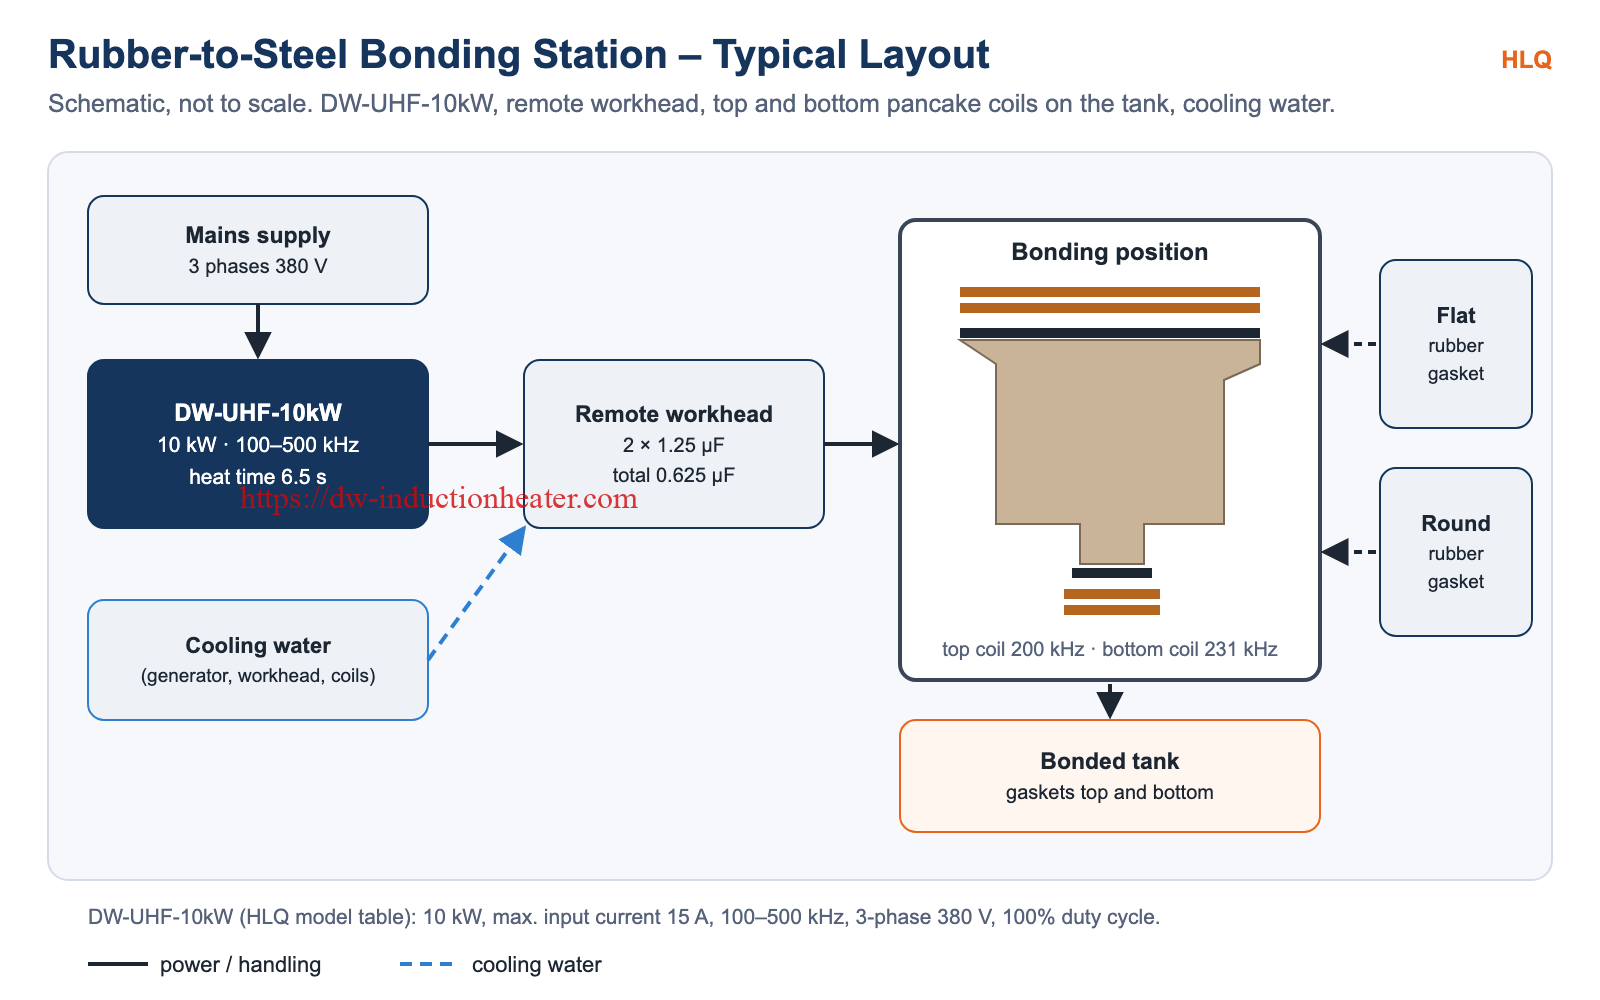
The DW-UHF-10kW drives current through a remote workhead with two 1.25 µF capacitors (total 0.625 µF). The workhead feeds two two-turn pancake coils designed for this application: one over the flat gasket on top of the tank (200 kHz) and one at the round gasket on the bottom (231 kHz). Because each coil is contoured to the shape of the steel assembly, the steel heats uniformly in the gasket areas and brings the rubber to the 320 °F (160 °C) bonding temperature. See induction heating coil design for HLQ coil types.
Technical Specifications
| Parameter | HLQ case data |
|---|---|
| Objective | To bond rubber gaskets to the top and bottom of a steel gas tank assembly |
| Material | Flat and round rubber gaskets, steel gas tank assembly |
| Temperature | 300 to 350 °F (148.9–176.7 °C); bonding temperature 320 °F (160 °C) |
| Frequency | 200 kHz for the flat gasket; 231 kHz for the round gasket |
| Equipment | DW-UHF-10kW induction heating system with a remote workhead containing two 1.25 µF capacitors for a total of 0.625 µF |
| Coil | Two two-turn pancake coils, specially contoured to the shape of the steel assembly |
| Heating time | Power applied for 6.5 seconds |
| Results | Repeatable, rapid and accurate heating cycles; reduced process time; even distribution of heat |
Recommended Model Selection
DW-UHF series data from the HLQ model table (100% duty cycle):
| Model | Power | Max. input current | Frequency | Supply | HLQ bonding case |
|---|---|---|---|---|---|
| DW-UHF-4.5kW | 4.5 kW | 20 A | 1.1–2.0 MHz | 1-phase 220 V | Steel clips into rubber; catheter tube (cases state 306–400 kHz) |
| DW-UHF-6.0kW | 6.0 kW | 28 A | 300–1100 kHz | 1-phase 220 V | Stainless inserts into plastic (case states 230 kHz) |
| DW-UHF-10kW | 10 kW | 15 A | 100–500 kHz | 3-phase 380 V | Rubber gaskets to steel gas tank (this page) |
| DW-UHF-20kW | 20 kW | 30 A | 50–250 kHz | 3-phase 380 V | – |
Process Workflow
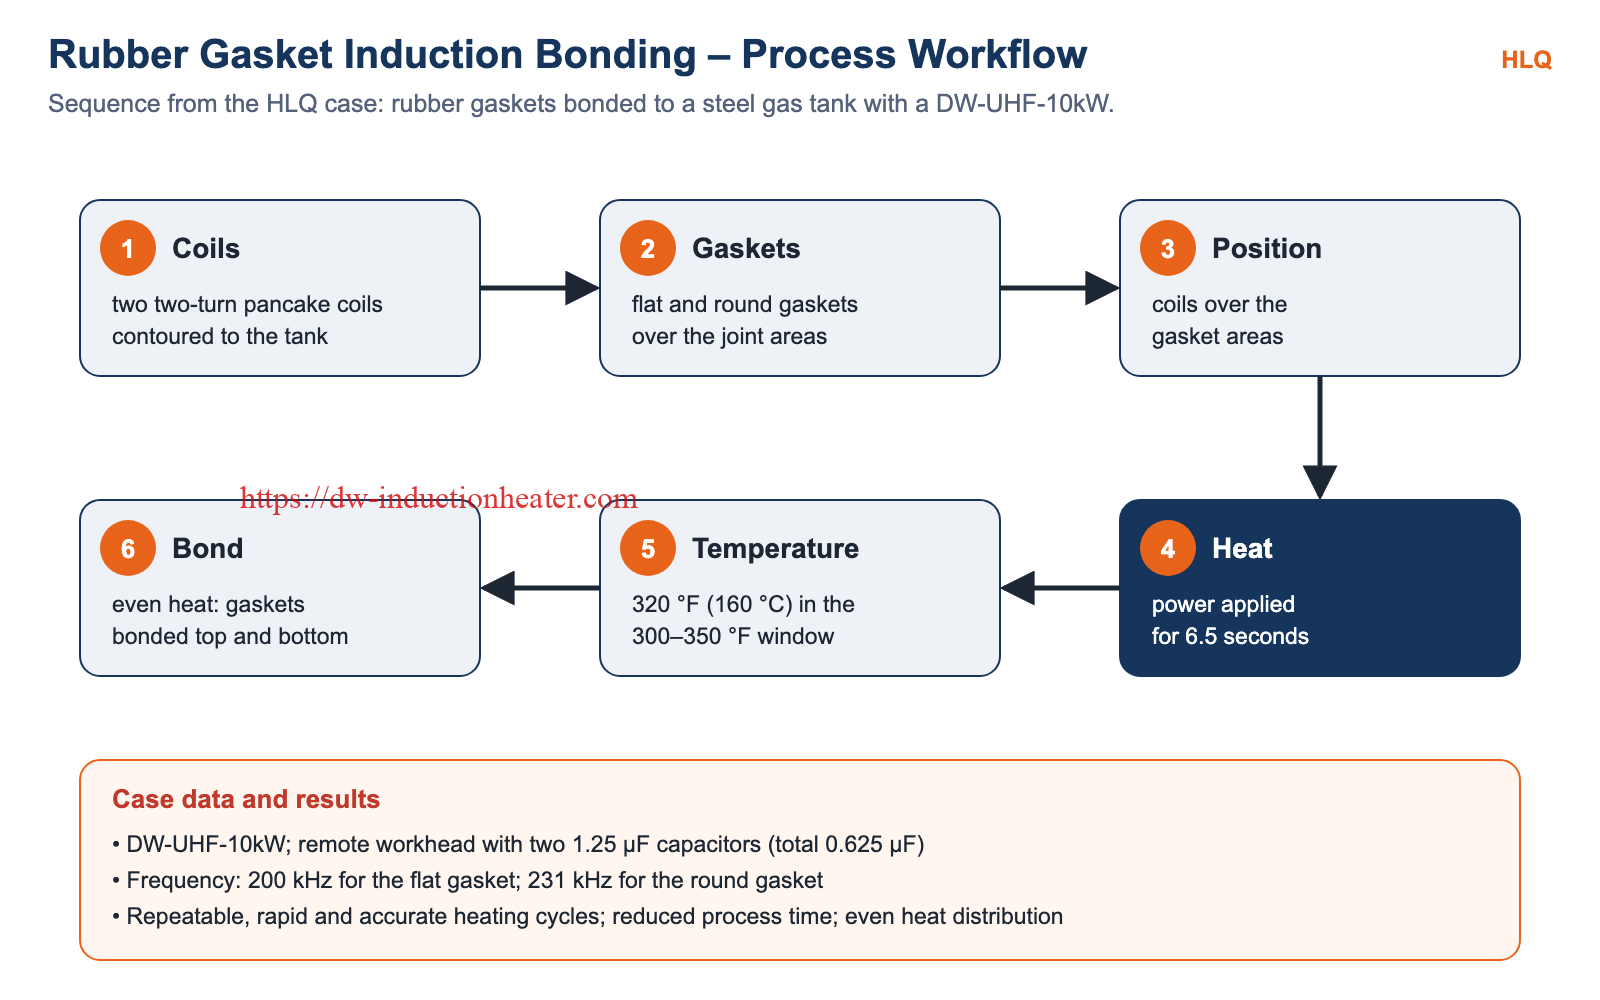
- Coils – two two-turn pancake coils are contoured to the shape of the steel tank.
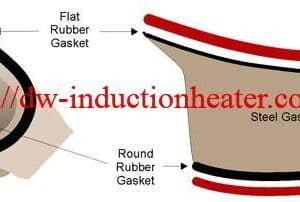
- Gaskets – the flat and round rubber gaskets are positioned over the joint areas.
- Position – the coils are placed over the gasket areas.
- Heat – power is applied for 6.5 seconds.
- Temperature – the bonding temperature of 320 °F (160 °C) is reached, within the 300–350 °F window.
- Bond – with even heat in the gasket areas, the gaskets bond to the top and bottom of the tank.
Common Problems and Solutions
| Problem | Cause | Solution (HLQ data) |
|---|---|---|
| Uneven heat around the gasket | Coil does not follow the part shape | Pancake coils specially contoured to the shape of the steel assembly |
| Temperature outside the bonding window | Uncontrolled heating time | Fixed 6.5 s cycle to reach 320 °F (160 °C) inside the 300–350 °F window |
| Different gasket geometries on one part | Flat and round gaskets need different heating | Separate coils for each gasket: 200 kHz flat, 231 kHz round |
| Long process time | Slow heating method | Induction reduced process time |
| Inconsistent results | Variable heating cycles | Repeatable, rapid and accurate induction heating cycles |
Engineering Selection Guide
- Steel assemblies with rubber gaskets: DW-UHF-10kW (3-phase 380 V) with contoured pancake coils, 6.5 s in the HLQ case.
- Small steel clips into rubber: DW-UHF-4.5kW with a three-turn pancake coil, 1.5 s (HLQ case).
- Coil: contour the coil to the part so the gasket area heats evenly.
- Temperature: define the bonding window (300–350 °F in this case) and the target (320 °F).
- Data to send: steel part drawing, gasket type and size, bonding temperature window, cycle time and output.
Advantages and Limitations
| Advantages | Limitations |
|---|---|
| 6.5-second bonding cycle | Coils must be contoured to each part shape |
| Repeatable, rapid and accurate heating cycles | Different gasket shapes may need separate coils and tuning |
| Even distribution of heat in the gasket areas | Only the steel is heated; the rubber must be in contact with it |
| Reduced process time | Water cooling is required |
Why Choose HLQ?
- Published rubber, plastic and polymer bonding data.
- Coils designed and contoured for each assembly.
- DW-UHF systems from 4.5 to 20 kW.
- Repeatable, rapid and accurate heating cycles.
10 Core FAQs
1. What was bonded?
Flat and round rubber gaskets to the top and bottom of a steel gas tank assembly.
2. What temperature is used?
A 300–350 °F (148.9–176.7 °C) window, with a bonding temperature of 320 °F (160 °C).
3. How long is the heating cycle?
Power is applied for 6.5 seconds.
4. Which frequencies were used?
200 kHz for the flat gasket and 231 kHz for the round gasket.
5. Which equipment?
A DW-UHF-10kW with a remote workhead containing two 1.25 µF capacitors (total 0.625 µF).
6. Which coils?
Two two-turn pancake coils, specially contoured to the shape of the steel assembly.
7. Is the rubber heated directly?
No. The coils heat the steel in the gasket areas, and the rubber bonds where it contacts the hot steel.
8. What are the benefits?
Repeatable, rapid and accurate heating cycles, reduced process time and even distribution of heat.
9. Can steel parts be bonded into rubber?
Yes. HLQ heated steel clips to 250–350 °F in 1.5 seconds and press-bonded them into rubber seals.
10. What information is needed for a quotation?
The steel part drawing, gasket type and size, bonding temperature window, cycle time and output.