Post Welding Heat Treatment Machine with Induction
Post Welding Heat Treatment With Induction Machine for Pipelines and Steel Weldments
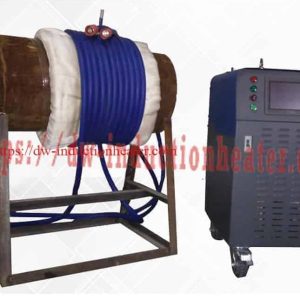
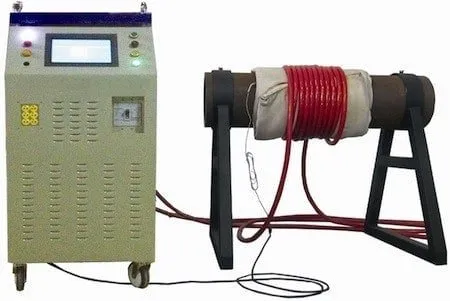
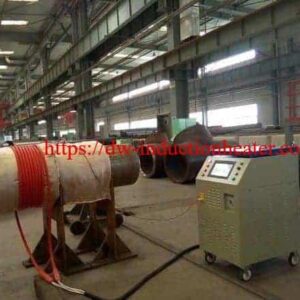
The HLQ Induction Post Welding Heat Treatment (PWHT) Machine is an industrial induction heating system designed for controlled thermal processing of suitable welded steel pipes, pressure-containing components, fabricated steel structures and industrial weldments.
The published HLQ MYD industrial series includes six models: MYD-40, MYD-50, MYD-60, MYD-80, MYD-100 and MYD-120, with nominal output ratings from 40 kW to 120 kW.
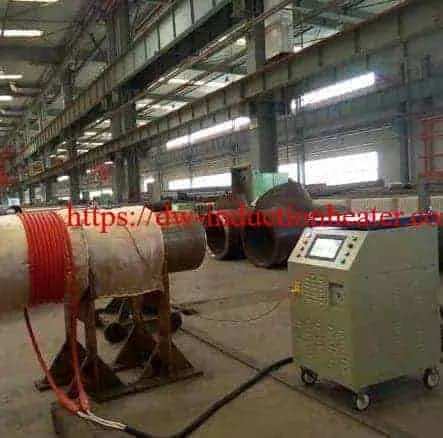
The system combines IGBT induction power conversion, application-specific heating coils, PLC touchscreen operation and multi-point temperature monitoring to support industrial welding-related thermal processes.
Depending on the equipment configuration, temperature recording accessories may be used to document the heating and cooling cycle.
A typical post-weld heat treatment procedure may include controlled heating, a specified soaking temperature, a required holding period and controlled cooling.
The required thermal cycle depends on the steel grade, wall thickness, original heat-treatment condition, component geometry, applicable standard and approved heat-treatment procedure.
Engineering note: An induction generator provides heating energy. Compliance with a specified PWHT procedure must be established through the complete heating arrangement, process control, temperature measurement and recorded results.
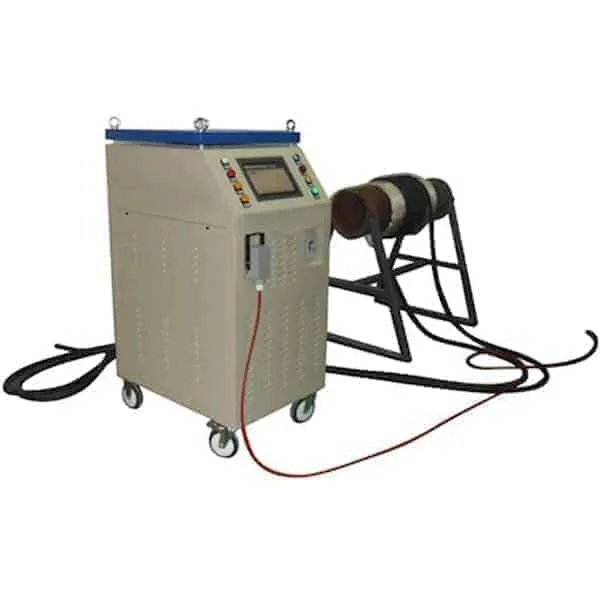
Quick Answer
What Is an Induction PWHT Machine?
An induction PWHT machine uses electromagnetic induction to heat suitable welded metal components according to a specified post-weld thermal treatment procedure.
During operation, an induction generator supplies high-frequency alternating current to a heating coil. The resulting magnetic field induces electrical currents inside the conductive workpiece, generating heat through electrical resistance.
Temperature sensors monitor selected metal-surface locations while the control system manages supported heating functions.
The HLQ MYD industrial series provides published nominal output ratings of 40–120 kW and a listed output frequency range of 2–36 kHz.
Main applications: Pipe weld heat treatment, industrial pipeline maintenance, selected pressure-vessel weld treatments, localized stress relieving and controlled heating of fabricated steel components.
Typical PWHT sequence: Controlled Heating → Soaking Temperature → Holding Period → Controlled Cooling → Temperature Record Review.
Important: The treatment temperature, heating rate, holding time and cooling rate must follow the approved procedure for the particular material and application.
MYD Induction PWHT System at a Glance
| Model | Nominal Power | Published Frequency | Published Weight |
|---|---|---|---|
| MYD-40 | 40 kW | 2–36 kHz | 130 kg |
| MYD-50 | 50 kW | 2–36 kHz | 136 kg |
| MYD-60 | 60 kW | 2–36 kHz | 140 kg |
| MYD-80 | 80 kW | 2–36 kHz | 145 kg |
| MYD-100 | 100 kW | 2–36 kHz | 168 kg |
| MYD-120 | 120 kW | 2–36 kHz | 180 kg |
These are manufacturer-published values. Actual electrical ratings, continuous output capability and model-specific operating limits require confirmation.
Table of Contents
- What Is an Induction Post-Weld Heat Treatment Machine?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages and Limitations
- Why Choose HLQ?
- 10 Core FAQs
What Is an Induction Post-Weld Heat Treatment Machine?
An induction post-weld heat treatment machine is an industrial electrical heating system used to apply a controlled thermal cycle to selected welded metal components after welding.
The equipment produces electromagnetic heating inside conductive materials. This allows suitable workpiece regions to be heated without relying exclusively on heat transferred from an external flame or resistance element.
Post-weld heat treatment may be specified for metallurgical reasons, residual stress management or compliance with an applicable fabrication or repair procedure.
The actual treatment objective depends on the material and governing requirements.
Not all post-weld thermal treatments are identical, and not every steel weld requires PWHT.
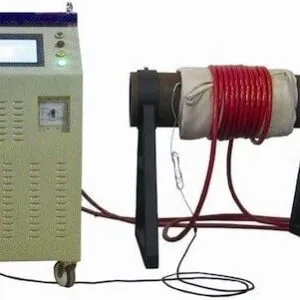
Main Components of an Induction PWHT System
| Component | Main Function | Engineering Consideration |
|---|---|---|
| IGBT Induction Generator | Converts electrical input into high-frequency induction power. | Rated output, frequency, cooling and operating duty. |
| PLC Touchscreen Controller | Provides supported heating and operator-control functions. | Available ramp, hold, cooling and alarm functions. |
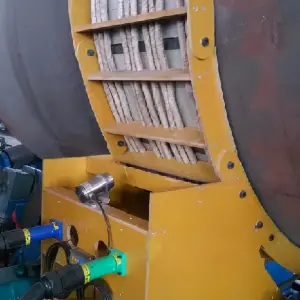
| Flexible Induction Heating Coil | Generates the magnetic field around the workpiece. | Coil geometry, length, spacing and electrical matching. |
| Induction Output Connections | Connect the heating circuit to the generator. | Current rating and connection compatibility. |
| K-Type Thermocouples | Measure selected workpiece temperatures. | Direct metal contact, calibration and positioning. |
| Temperature Controller | Supervises the heating process using available feedback signals. | Sensor channels and independent control capability. |
| Digital Temperature Recorder | Documents thermal-cycle measurements when equipped. | Channel count, data storage and traceability. |
| Thermal Insulation Blankets | Reduce external heat losses. | Temperature rating, coverage and insulation thickness. |
| Non-Metallic Insulating Straps | Secure insulation and approved heating arrangements. | High-temperature resistance and electrical insulation. |
| Cooling System | Removes heat from specified equipment components. | Generator and coil cooling requirements. |
What Is the Purpose of PWHT?
Depending on the material and treatment procedure, PWHT may be used to modify the weldment’s metallurgical condition, temper certain hardened structures, reduce selected residual stresses or satisfy a governing fabrication requirement.
The treatment must be suitable for the steel’s composition, prior processing and mechanical-property requirements.
For example, an excessive temperature may adversely affect a quenched-and-tempered steel, while an unsuitable cycle for an alloy steel may fail to produce the intended material condition.
Therefore, a PWHT machine must be selected together with a qualified process rather than independently of the material requirements.
Preheating, Postheating and PWHT Compared
| Process | Timing | Primary Objective | Key Requirement |
|---|---|---|---|
| Welding Preheating | Before welding | Establish the required base-metal temperature. | Minimum preheat temperature. |
| Interpass Temperature Control | Between welding passes | Control weld-area temperature. | Approved minimum and maximum temperatures. |
| Postheating | After welding, when specified | Apply a prescribed thermal operation. | Temperature and holding time. |
| Stress Relief Heat Treatment | After fabrication or welding | Reduce selected residual stresses. | Material-specific thermal cycle. |
| Formal PWHT | After welding | Apply a qualified post-weld thermal treatment. | Approved heating, holding, cooling and records. |
For additional industrial machine configurations, see HLQ induction PWHT equipment.
Key Applications
1. Steel Pipe Weld Heat Treatment
Industrial steel pipe welds may require PWHT depending on the material, wall thickness, applicable design code and fabrication procedure.
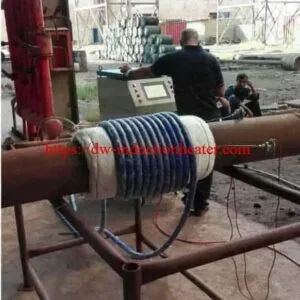
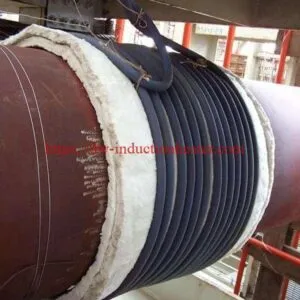
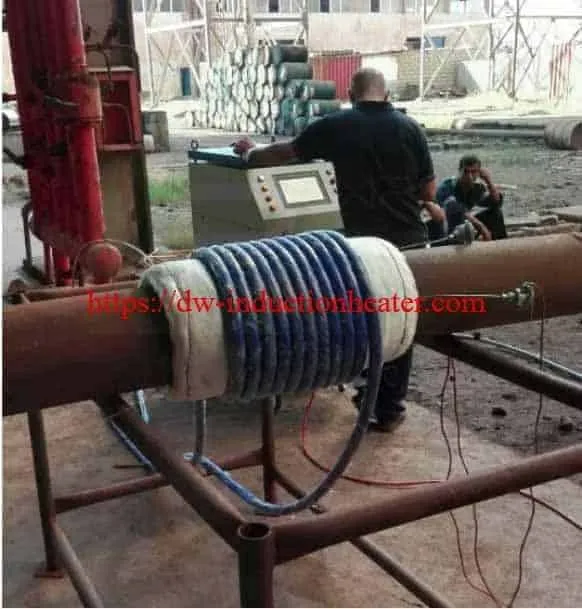
Flexible induction coils can be installed around suitable insulated pipe sections to heat the required treatment band.
The coil arrangement must be designed to achieve the prescribed temperatures at the required measurement points.
Pipe outside diameter, wall thickness, heating-band width and adjacent heat conduction all influence equipment selection.
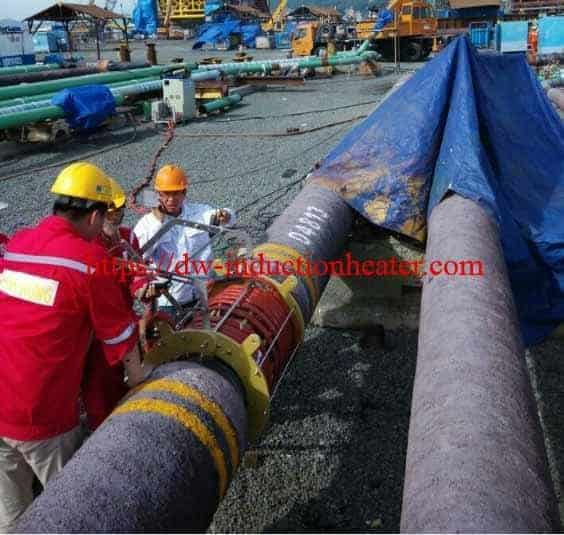
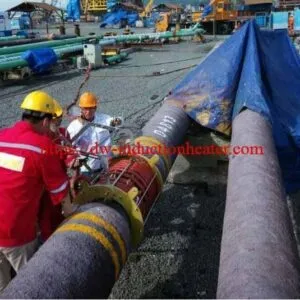
2. Oil and Gas Pipeline PWHT
Some oil and gas piping welds require specified post-weld thermal treatment.
Induction heating may be suitable for approved local heating arrangements where the required thermal cycle can be achieved and verified.
Field work requires evaluation of access conditions, electrical supply, component isolation, internal contents and worksite safety.
3. Pressure Vessel Weld Heat Treatment
Certain pressure-containing components may require thermal treatment after welding under the applicable construction or repair code.
Local induction heating can be evaluated where permitted by the governing procedure.
Particular attention must be given to the geometry of shell welds, nozzles, attachments, circumferential joints and transitions between different thicknesses.
For related industrial applications, review HLQ induction heating for pressure vessels.
4. Boiler and Steam Piping Welds
Industrial boiler and steam-piping components may require carefully controlled thermal treatment when specified for the selected alloy and welded joint.
Some alloy steels have strict requirements for treatment temperature, soaking time and cooling conditions.
Multiple thermocouples may be necessary to verify the required temperature distribution.
5. Structural Steel Weldments
Large structural weldments may contain residual stresses associated with nonuniform welding temperatures and contraction.
Induction heating can be evaluated for localized treatment where the steel grade and applicable requirements permit it.
However, localized heating does not guarantee uniform stress reduction throughout a complete structure.
6. Industrial Weld Repair
Selected repair procedures may require post-weld thermal treatment.
Suitable induction heating equipment may provide the necessary thermal energy when the treatment area is accessible and the heating cycle can be monitored.
Repair procedures must establish the material-specific temperature limits and acceptance requirements.
7. Localized Stress Relieving
Where permitted, a localized thermal cycle may be used to reduce selected residual stresses around welded regions.
Stress reduction depends on the material, applied temperature, holding time, restraint and temperature distribution.
Complete removal of all residual stresses cannot be assumed.
Industrial Application Comparison
| Application | Heating Objective | Key Selection Parameter |
|---|---|---|
| Pipe Weld PWHT | Follow a specified post-weld thermal cycle. | OD, wall thickness, heating band and procedure. |
| Pressure Vessel Welds | Meet applicable heat-treatment requirements. | Construction code, geometry and material. |
| Steam Piping | Control post-weld thermal treatment of suitable alloys. | Steel grade, soaking temperature and cooling rate. |
| Structural Weldments | Apply approved local thermal treatment. | Restraint, thickness and temperature gradients. |
| Weld Repair | Complete the qualified repair procedure. | Approved thermal cycle and inspection. |
| Stress Relieving | Reduce selected residual stresses. | Material properties and treatment conditions. |
Suitable Materials
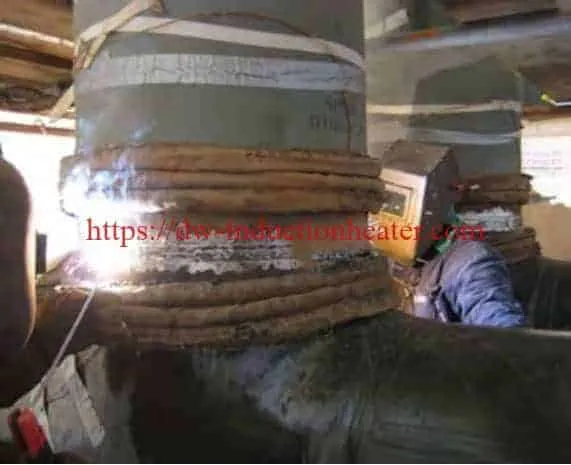
Induction heating is applicable to electrically conductive materials, but the suitability of a particular PWHT procedure depends on the material’s metallurgical condition and governing requirements.
Material Compatibility and PWHT Considerations
| Material | Induction Heating Suitability | PWHT Engineering Consideration |
|---|---|---|
| Carbon Steel | Generally suitable for induction heating. | Follow the specified material and welding procedure. |
| Low-Alloy Steel | Generally suitable for induction heating. | Confirm alloy-specific PWHT conditions. |
| Cr-Mo Alloy Steel | Application-dependent. | May require tightly controlled temperature and cooling conditions. |
| Structural Carbon Steel | Generally suitable for heating. | Assess mechanical-property and fabrication requirements. |
| Quenched and Tempered Steel | Special evaluation required. | Excessive temperature may reduce strength or hardness. |
| High-Strength Low-Alloy Steel | Conditional. | Review original material condition and treatment limits. |
| Austenitic Stainless Steel | Requires electromagnetic and metallurgical evaluation. | Grade-specific corrosion and sensitization considerations. |
| Ferritic Stainless Steel | Application-dependent. | Review grade-specific heat-treatment requirements. |
| Cast Iron | Special evaluation required. | Thermal gradients and crack susceptibility. |
Material Properties Affecting PWHT
| Material Property | Effect on the Heating Process |
|---|---|
| Electrical Resistivity | Influences resistive heating from induced currents. |
| Magnetic Permeability | Affects electromagnetic coupling and current distribution. |
| Thermal Conductivity | Controls heat flow through the workpiece. |
| Specific Heat Capacity | Determines the sensible energy requirement. |
| Wall Thickness | Affects thermal mass and through-wall temperature gradients. |
| Original Heat Treatment | May limit permissible PWHT temperature. |
| High-Temperature Mechanical Properties | Influence material response during thermal treatment. |
Material safety note: No universal PWHT temperature, soaking time or cooling rate is suitable for every material. The actual cycle must be taken from the approved application-specific procedure.
Working Principle
How Does Induction PWHT Work?
An induction PWHT system converts industrial electrical input into high-frequency alternating electrical power.
This power is delivered to an induction coil arranged around or near the conductive workpiece.
The alternating coil current generates a time-varying magnetic field.
Electrical currents are induced inside the metal, producing thermal energy through electrical resistance.
Thermal conduction distributes heat through the workpiece.
Thermocouples measure selected metal-surface temperatures so the heating process can be monitored and controlled according to the available equipment functions.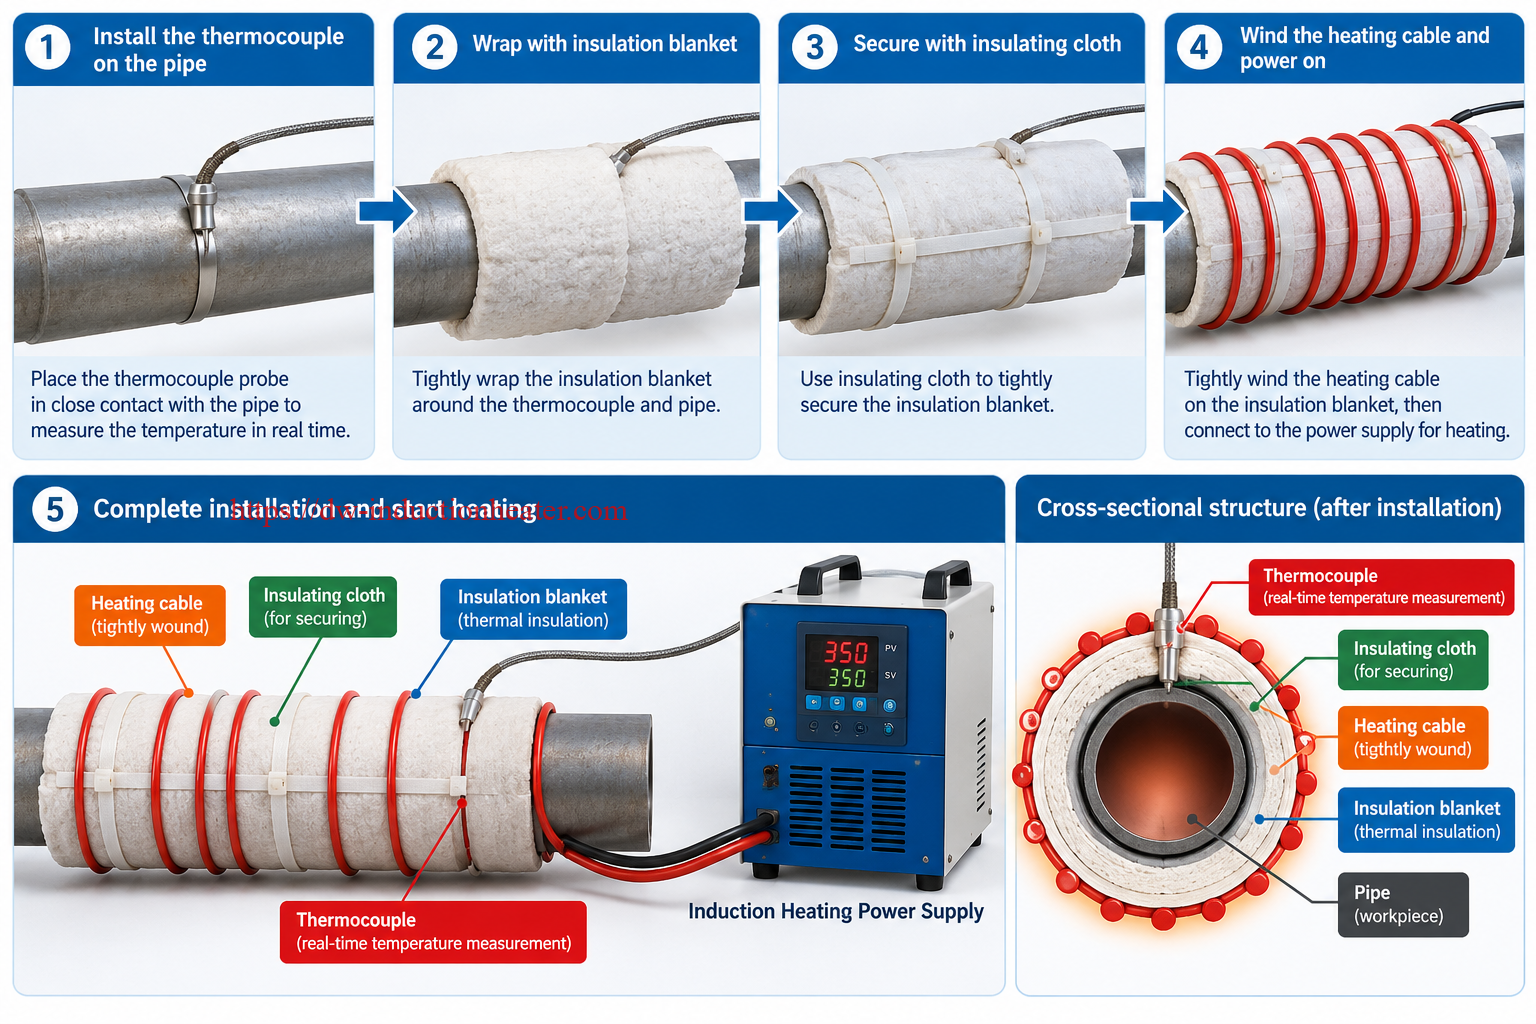
Energy Conversion and PWHT Control
| Stage | Operation | Technical Result |
|---|---|---|
| 1 | Three-Phase AC Input | Supplies power to the induction generator. |
| 2 | IGBT Power Conversion | Produces high-frequency electrical output. |
| 3 | Induction Coil Energization | Generates an alternating magnetic field. |
| 4 | Eddy Current Generation | Induces current inside the conductive steel. |
| 5 | Resistance Heating | Generates heat inside the metal. |
| 6 | Temperature Measurement | Monitors selected workpiece locations. |
| 7 | Heating Control | Supports the prescribed thermal process. |
| 8 | Temperature Recording | Documents thermal-cycle measurements when equipped. |
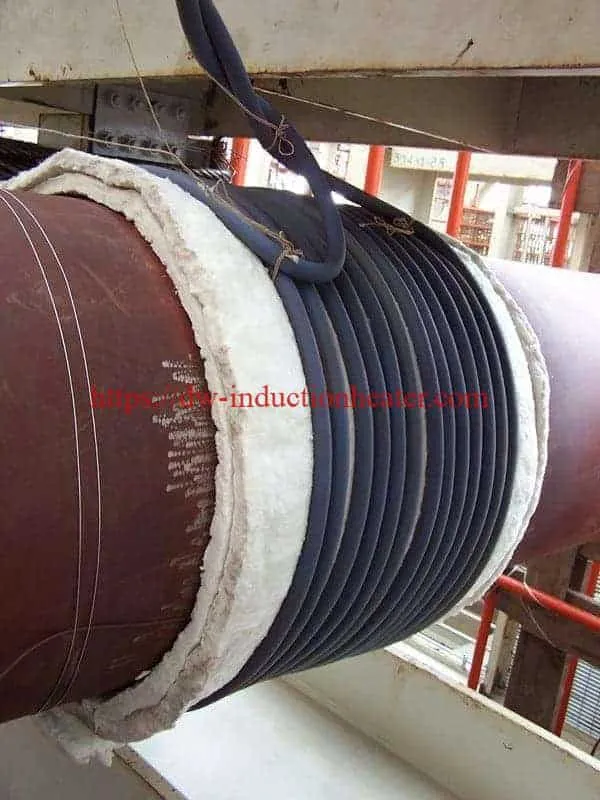
Correct Installation for Induction Pipe PWHT
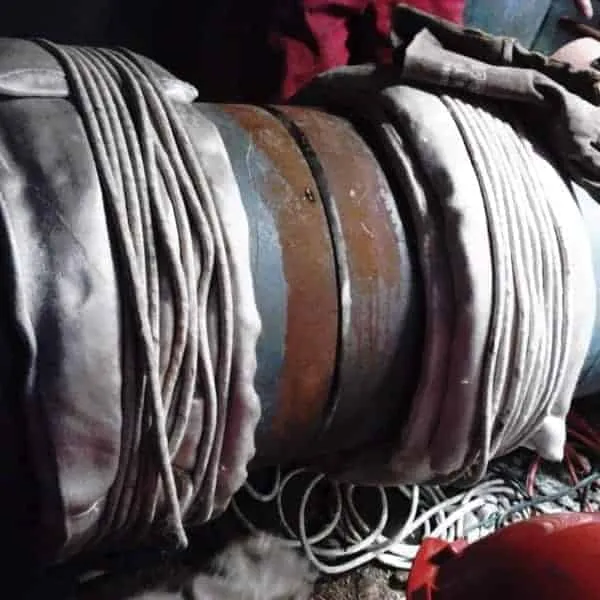
For a typical insulated steel-pipe heating arrangement, the temperature sensors, thermal insulation and induction heating cable must be installed in the correct sequence.
Correct installation sequence:
- Prepare and clean the steel pipe surface.
- Attach the specified K-type thermocouple junctions directly to the metal pipe.
- Check that the temperature sensors have reliable metal contact.
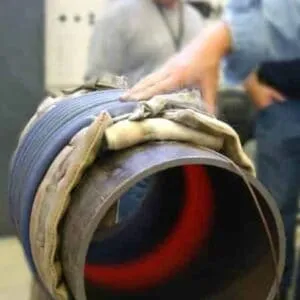
- Cover the steel pipe and thermocouples tightly with suitable thermal insulation blankets.
- Secure the blankets using approved non-metallic, high-temperature insulating fabric straps.
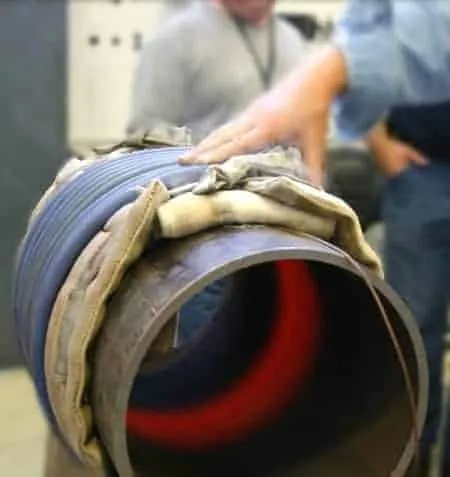
- Wind the flexible induction heating cable around the outside of the insulation blanket.
- Secure the induction cable using approved electrically insulating fixing materials.
- Connect the induction cable and temperature sensors to the appropriate equipment terminals.
- Verify electrical connections, cooling requirements, temperature readings and safety interlocks.
- Energize the system only after the installation has been checked.
Correct Pipe Heating Layer Structure
| Position | Component | Function |
|---|---|---|
| Inner Workpiece | Steel Pipe | Conductive workpiece heated by induction. |
| Direct Metal Contact | Thermocouple Junctions | Measure the actual steel temperature. |
| Middle Layer | Thermal Insulation Blankets | Cover sensors and pipe while reducing heat loss. |
| Blanket Fixing | Non-Metallic Insulating Straps | Secure the insulation without unapproved conductive fasteners. |
| Outer Heating Layer | Flexible Induction Heating Cable | Generates the alternating magnetic field. |
Important safety requirement: Do not use unapproved metallic fixing bands, steel wires or conductive straps around the thermal insulation blanket in the energized induction-heating zone.
Approved non-metallic, high-temperature insulating materials should be used to secure the blanket and cable arrangement.
The thermocouple junctions must remain in contact with the steel beneath the thermal insulation.
For related coil configurations, see HLQ flexible induction heating cables.
Four Main Stages of a PWHT Temperature Cycle
| Stage | Process Objective | Required Monitoring |
|---|---|---|
| Controlled Heating | Increase the workpiece temperature according to the approved procedure. | Heating rate and temperature gradients. |
| Soaking | Bring required measurement locations into the specified temperature range. | Minimum and maximum temperatures. |
| Holding | Maintain the prescribed conditions for the required duration. | Temperature records and soak duration. |
| Controlled Cooling | Reduce temperature according to the approved procedure. | Cooling rate and temperature distribution. |
Illustrative PWHT Temperature Profile
For educational purposes, consider a hypothetical thermal cycle using the following parameters:
| Parameter | Illustrative Value |
|---|---|
| Initial Temperature | 25°C |
| Hypothetical Soaking Temperature | 620°C |
| Hypothetical Heating Rate | 100°C/hour |
| Hypothetical Holding Time | 60 minutes |
| Hypothetical Controlled Cooling | 100°C/hour from 620°C to 300°C |
Technical warning: These are illustrative calculation values, not an approved PWHT cycle for any particular steel or pressure component.
The applicable procedure determines the real heating-rate limits, holding temperature, soak-time rules, thermocouple positions and cooling requirements.
Technical Specifications
The following specifications reproduce the core technical information published on the original HLQ product page.
Actual operating ratings and configuration-dependent functions require confirmation against current manufacturer specifications.
MYD-40 to MYD-120 Technical Parameters
| Parameter | MYD-40 | MYD-50 | MYD-60 | MYD-80 | MYD-100 | MYD-120 |
|---|---|---|---|---|---|---|
| Nominal Output Power | 40 kW | 50 kW | 60 kW | 80 kW | 100 kW | 120 kW |
| Published Input Current | 60 A | 75 A | 90 A | 120 A | 150 A | 180 A |
| Published Weight | 130 kg | 136 kg | 140 kg | 145 kg | 168 kg | 180 kg |
| Published Output Frequency | 2–36 kHz | 2–36 kHz | 2–36 kHz | 2–36 kHz | 2–36 kHz | 2–36 kHz |
Common Published System Specifications
| Technical Item | Published Information | Engineering Clarification |
|---|---|---|
| Standard Input Voltage | Three-Phase 380 VAC | Confirm frequency and actual rated input current. |
| Optional Voltage | Three-Phase 220 VAC / 440 VAC | Availability depends on model. |
| Power Electronics | IGBT | Confirm current production version. |
| Control Interface | PLC Touchscreen | Verify available programmed heating functions. |
| Temperature Monitoring | Published Six-Channel Capability | Confirm measurement channels and independent zones. |
| Published Temperature Tolerance | ±3°C | Test conditions are not specified. |
| Temperature Recording | Digital Recorder with Optional Printer | Confirm channels, storage and data export. |
| Cooling | Air-Cooled System Category | Verify power unit and coil cooling requirements. |
| Machine Dimensions | 800 × 560 × 1350 mm | Confirm model-specific dimensions. |
| Packing Dimensions | 900 × 660 × 1560 mm | Confirm final shipping package. |
| Published Ambient Range | −30°C to +50°C | Requires operating-condition verification. |
Electrical Input Verification
For a balanced three-phase electrical supply, apparent power is calculated using:
S = √3 × V × I / 1000
Where:
- S = apparent input power, kVA.
- V = line-to-line voltage, V.
- I = line input current, A.
Published Current and Calculated Apparent Power
| Model | Published Input Current | Calculated Input Apparent Power at 380V | Published Output Power |
|---|---|---|---|
| MYD-40 | 60 A | 39.49 kVA | 40 kW |
| MYD-50 | 75 A | 49.36 kVA | 50 kW |
| MYD-60 | 90 A | 59.24 kVA | 60 kW |
| MYD-80 | 120 A | 78.97 kVA | 80 kW |
| MYD-100 | 150 A | 98.73 kVA | 100 kW |
| MYD-120 | 180 A | 118.47 kVA | 120 kW |
The calculated apparent input powers are lower than the corresponding nominal output powers.
Since actual electrical conversion involves losses, the published input-current and output-power values cannot be treated as simultaneously verified continuous ratings without further clarification.
Confirm the latest rated input current, power factor, efficiency and continuous output capability before designing the electrical installation.
Temperature Control and Recording Functions
| Function | Engineering Purpose | Verification Requirement |
|---|---|---|
| Thermocouple Measurement | Measures selected metal-surface temperatures. | Channel count and calibration. |
| Temperature Setpoint | Defines the required process temperature. | Available setpoint functions. |
| Heating-Rate Control | Supports the prescribed heating ramp. | Programmability and feedback arrangement. |
| Soaking Control | Maintains the specified temperature range. | Temperature tolerance and timer logic. |
| Cooling Control | Supports the required cooling process. | Available cooling functions and limits. |
| Temperature Recording | Documents the heating cycle. | Data storage, export and traceability. |
| Alarm and Protection | Indicates abnormal operating conditions. | Alarm settings and protective functions. |
The original page’s six-channel claim must not be interpreted as six independently controlled induction outputs unless the selected equipment configuration confirms this capability.
Recommended Model Selection
Choosing an induction PWHT machine requires an assessment of the complete thermal cycle, not only the desired peak temperature.
The generator must provide sufficient useful thermal power while also complying with the required heating rate, holding period and operating duty.
Preliminary MYD Model Selection
| Model | Nominal Power | Preliminary Application Consideration | Important Verification |
|---|---|---|---|
| MYD-40 | 40 kW | Localized industrial heating with relatively lower thermal loads. | Actual heated mass and sustained output. |
| MYD-50 | 50 kW | Selected welded steel pipe components. | Coil matching and temperature distribution. |
| MYD-60 | 60 kW | Moderate industrial pipe heating applications. | Heating-band size and continuous operating duty. |
| MYD-80 | 80 kW | Higher thermal-load applications. | Useful thermal power and heating uniformity. |
| MYD-100 | 100 kW | Selected larger pipe or fabricated metal applications. | Electrical supply, cooling and sustained performance. |
| MYD-120 | 120 kW | Applications requiring higher nominal output capacity. | Continuous rating, coil arrangement and process control. |
The application categories are preliminary engineering considerations, not guaranteed processing capacities.
Required Data for PWHT Equipment Selection
| Required Information | Engineering Purpose |
|---|---|
| Material Grade | Determines permissible treatment conditions. |
| Original Material Condition | Identifies possible temperature restrictions. |
| Pipe Outside Diameter | Determines circumference and coil layout. |
| Wall Thickness | Determines thermal mass and through-wall gradients. |
| Heating Band Width | Defines the selected heated region. |
| Soaking Temperature | Defines the required treatment temperature. |
| Heating Rate | Determines the permitted ramp. |
| Holding Time | Determines sustained operation requirements. |
| Cooling Rate | Determines the required cooling process. |
| Temperature Uniformity | Determines measurement and heating-zone requirements. |
| Recorder Requirements | Determine monitoring and data-retention needs. |
| Electrical Supply | Determines installation compatibility. |
When Should a Higher-Power System Be Considered?
A higher-power induction generator may be required when the selected workpiece has a larger heated mass, significant conductive heat losses or demanding thermal processing requirements.
However, a higher generator rating does not automatically permit faster heating because the qualified procedure may impose a maximum heating rate.
For related large-pipe applications, compare HLQ induction pipeline preheating machines.
Process Workflow
A qualified PWHT process requires correct equipment installation, reliable temperature measurement and appropriate thermal-cycle documentation.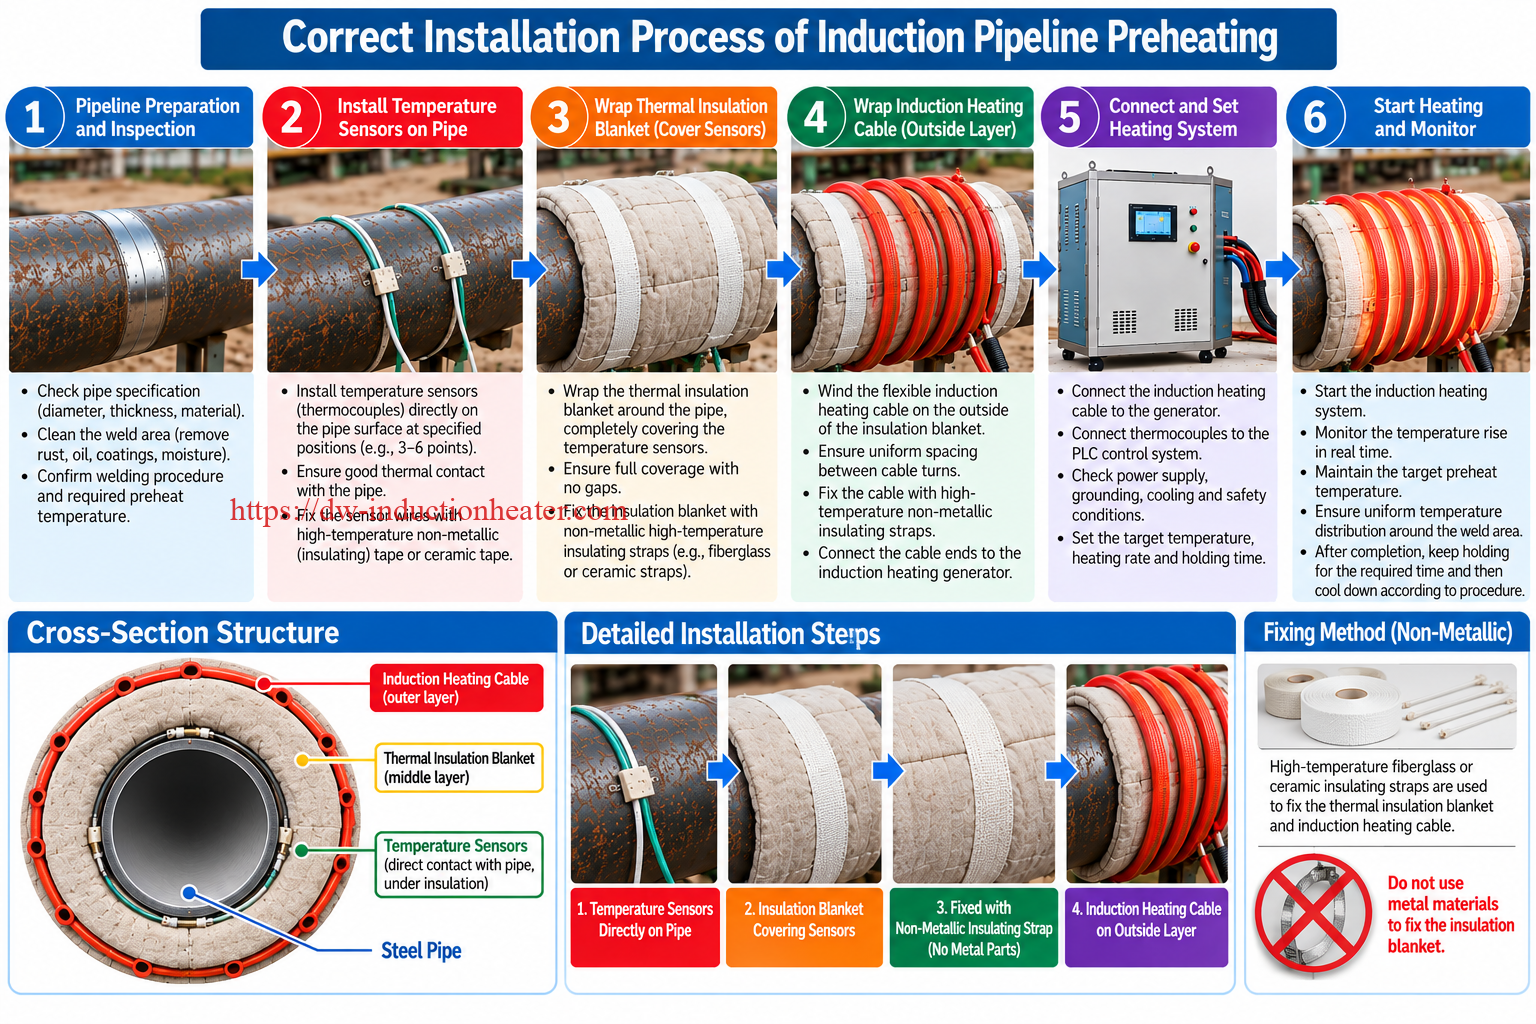
Step 1: Review the Approved PWHT Procedure
Confirm the material grade, applicable standard, treatment temperature, heating rate, holding time and cooling requirements.
Step 2: Inspect the Workpiece
Verify the pipe dimensions, weld location, wall thickness, heating band and surrounding conditions.
Step 3: Prepare the Thermocouple Locations
Clean the specified measurement positions to allow reliable temperature-sensor attachment.
Step 4: Install Thermocouples Directly on the Steel
Attach K-type thermocouple junctions directly against the metal at the required locations.
Use approved attachment methods and verify sensor identification.
Step 5: Wrap the Thermal Insulation Blankets
Cover the steel pipe and temperature sensors tightly with suitable thermal insulation blankets.
Ensure the required treatment region is properly covered.
Step 6: Secure the Insulation with Non-Metallic Straps
Use approved high-temperature, electrically insulating fabric straps to secure the blankets.
Do not use unapproved metallic fixing bands or steel wire in the active induction-heating zone.
Step 7: Wind the Induction Heating Cable
Wrap the flexible induction heating cable around the outside of the insulation blanket.
Maintain the required cable spacing and installation geometry.
Step 8: Connect the Heating System
Connect the induction cable, thermocouples and other required accessories.
Check the electrical input, grounding, cooling conditions and protective functions.
Step 9: Configure the Thermal Cycle
Set the available heating parameters according to the approved procedure.
Confirm the required ramp rate, soaking temperature, holding duration and cooling requirements.
Step 10: Start Controlled Heating
Energize the induction system and monitor temperatures at the required measurement positions.
Maintain the temperature distribution within applicable limits.
Step 11: Complete the Soaking Period
Maintain the specified treatment temperature for the prescribed period.
Apply the qualified procedure’s rules for determining when soaking begins and ends.
Step 12: Complete Controlled Cooling
Reduce the workpiece temperature according to the approved cooling requirements.
Step 13: Review Temperature Records
Check the recorded time-temperature information against the process requirements.
Retain records where required by the project or governing standard.
PWHT Process Verification Checklist
| Inspection Item | Required Condition |
|---|---|
| Material | Correct grade and approved treatment procedure. |
| Thermocouples | Direct metal contact at specified locations. |
| Thermal Insulation | Covers the workpiece and temperature sensors. |
| Insulation Fixing | Approved non-metallic insulating straps. |
| Induction Cable | Outside the insulation blanket. |
| Electrical Connections | Correctly connected and inspected. |
| Heating Program | Matches the approved procedure. |
| Temperature Measurements | Reliable and appropriately calibrated. |
| Soaking Period | Meets the applicable temperature and time requirements. |
| Cooling | Follows the prescribed cooling procedure. |
| Records | Complete and traceable where required. |
Common Problems and Solutions
PWHT requires reliable equipment operation and accurate temperature monitoring throughout the prescribed thermal cycle.
PWHT Troubleshooting Table
| Problem | Possible Cause | Recommended Action |
|---|---|---|
| Slow Temperature Rise | Insufficient useful power or high thermal losses. | Review thermal load, coil matching and insulation. |
| Uneven Pipe Temperature | Nonuniform cable spacing or adjacent heat conduction. | Check coil arrangement and measurement locations. |
| Incorrect Thermocouple Reading | Poor metal contact or incorrect sensor installation. | Reinstall the sensor directly against the steel. |
| Temperature Overshoot | Control response or heating settings unsuitable for the workpiece. | Review feedback and programmed settings. |
| Soaking Temperature Cannot Be Maintained | Heat losses exceed useful heating power. | Evaluate insulation, equipment capacity and cooling limits. |
| Heating Cable Overheats | Incorrect electrical matching or installation. | Stop operation and inspect the heating circuit. |
| Metallic Fixing Material Becomes Hot | Conductive fastening components near the induction coil. | Stop heating and remove unapproved metallic fasteners. |
| Generator Overheating | Insufficient cooling or excessive operating duty. | Check cooling and verified equipment ratings. |
| Recorder Data Missing | Recorder, sensor or channel configuration problem. | Check channel mapping, storage and recording operation. |
| PWHT Record Does Not Meet Requirements | Temperature or timing outside the approved limits. | Refer to the qualified procedure and responsible engineer. |
Preventive Maintenance Checklist
| Component | Inspection Requirement |
|---|---|
| Induction Power Generator | Check cooling, electrical condition and protective functions. |
| Induction Heating Cable | Inspect insulation, mechanical damage and connections. |
| Thermocouples | Check contact, condition and calibration. |
| Thermocouple Extension Cables | Inspect insulation and connection integrity. |
| Temperature Recorder | Verify channel mapping, recording and data export. |
| Thermal Insulation Blankets | Inspect for moisture, tears and deterioration. |
| Non-Metallic Straps | Check mechanical strength and temperature suitability. |
| Controller | Verify programmed functions and alarm indications. |
Engineering Selection Guide
Engineering selection should consider the approximate sensible heat requirement, the prescribed thermal cycle and the actual useful heating performance of the induction system.
The nominal generator power is not identical to the thermal power absorbed by the workpiece.
1. Calculate the Heated Pipe Mass
For a cylindrical steel pipe with a selected axial heating band:
m = π × (D − t) × t × L × ρ
Where:
- m = selected heated metal mass, kg.
- D = outside pipe diameter, m.
- t = pipe wall thickness, m.
- L = axial heating-band length, m.
- ρ = steel density, kg/m³.
2. Calculate the Approximate Sensible Heat
Q = m × Cp × ΔT
Where:
- Q = sensible heat, kJ.
- m = heated metal mass, kg.
- Cp = average specific heat capacity, kJ/(kg·K).
- ΔT = temperature increase, K.
3. Engineering Example: PWHT Heating of a Steel Pipe
Consider a hypothetical steel pipe heating calculation.
The following parameters are used only to illustrate the sizing method. They do not describe a measured customer project or a qualified PWHT procedure.
| Parameter | Assumed Value |
|---|---|
| Pipe Outside Diameter | 323.9 mm |
| Wall Thickness | 12.7 mm |
| Selected Heating Band | 400 mm |
| Initial Temperature | 25°C |
| Illustrative Treatment Temperature | 620°C |
| Temperature Increase | 595 K |
| Assumed Steel Density | 7,850 kg/m³ |
| Assumed Mean Specific Heat | 0.58 kJ/(kg·K) |
4. Calculate the Heated Metal Mass
m = π × (0.3239 − 0.0127) × 0.0127 × 0.400 × 7850
m ≈ 38.99 kg
5. Calculate the Required Sensible Heat
Q = 38.99 × 0.58 × 595
Q ≈ 13,455 kJ
Converting to kilowatt-hours:
Q ≈ 3.74 kWh
This represents the approximate sensible heat needed for the selected pipe-band volume.
Actual electrical consumption will be higher because of power-conversion losses, electromagnetic coupling losses, heat conducted into adjacent steel and external thermal losses.
6. Theoretical Heating Time at Different Useful Thermal Powers
Heating Time = Required Sensible Heat / Average Useful Thermal Power
| Hypothetical Useful Thermal Power | Idealized Heating Time |
|---|---|
| 4 kW | 56.1 minutes |
| 6 kW | 37.4 minutes |
| 8 kW | 28.0 minutes |
| 10 kW | 22.4 minutes |
| 12 kW | 18.7 minutes |
| 15 kW | 14.9 minutes |
| 20 kW | 11.2 minutes |
Important: These are idealized energy calculations. They do not establish a permissible PWHT heating rate or guaranteed performance of a specific MYD model.
7. Why PWHT May Require Several Hours
Suppose a hypothetical procedure permits an average heating rate of 100°C/hour from 25°C to 620°C.
The calculated heating duration would be:
Heating Time = (620 − 25) / 100 = 5.95 hours
If the procedure also includes a 60-minute soak and controlled cooling from 620°C to 300°C at 100°C/hour, those stages would add another 4.2 hours.
The combined illustrative duration would be approximately 10.15 hours, excluding further cooling and other process steps.
This explains why a generator capable of producing rapid heat may still be required to operate for several hours during a controlled PWHT process.
The assumed rates and temperature values are calculation examples only.
8. Estimate the Power Required During Soaking
During soaking, the workpiece must remain within the prescribed temperature range.
Although the workpiece has already reached the target temperature, additional thermal energy may still be required to replace heat lost by radiation, convection and conduction into adjacent metal.
Therefore, equipment sizing must consider both the initial heat-up stage and the sustained heating requirements during soaking.
9. Important Equipment Sizing Factors
| Parameter | Influence on PWHT |
|---|---|
| Material Grade | Determines permissible treatment cycle. |
| Pipe Diameter | Affects circumference and induction cable length. |
| Wall Thickness | Determines thermal mass and gradients. |
| Heating Band Width | Determines the selected heated volume. |
| Temperature Setpoint | Determines the required temperature rise. |
| Heating Rate | Determines the allowed temperature ramp. |
| Holding Time | Determines sustained operation requirements. |
| Cooling Rate | Determines the required cooling process. |
| Temperature Uniformity | Determines measurement positions and possible zoning. |
| Thermal Insulation | Influences heat losses. |
| Operating Duty | Determines continuous output requirements. |
10. Induction PWHT Versus Furnace PWHT
| Comparison | Induction PWHT | Furnace PWHT |
|---|---|---|
| Heating Location | Selected workpiece region. | Complete component or furnace-loaded assembly. |
| Heating Method | Electromagnetic induction. | Furnace heat transfer. |
| Equipment | Induction generator, coil and temperature controls. | Heat-treatment furnace and control system. |
| Temperature Distribution | Depends on coil arrangement, insulation and workpiece. | Depends on furnace design and loading. |
| Localized Treatment | Possible where qualified and permitted. | Generally treats the complete loaded component. |
| Process Compliance | Requires qualified local PWHT procedure. | Requires qualified furnace PWHT procedure. |
Advantages and Limitations
Main Advantages of Induction PWHT
1. Localized Metal Heating
Induction coils can heat selected conductive metal regions without requiring the complete component to be placed inside a furnace.
2. Flexible Heating Arrangements
Compatible flexible induction cables can be installed around suitable cylindrical workpieces.
3. Multi-Point Temperature Measurement
Multiple thermocouples can monitor temperatures at selected positions during the thermal cycle.
4. Temperature Recording Options
Digital temperature-recording systems can document the thermal process when included in the equipment configuration.
5. Industrial Power Range
The published MYD series includes six nominal ratings from 40 kW to 120 kW.
6. Reduced Dependence on Open Flames
Induction heating does not require a combustion flame as the primary heat source.
Appropriate electrical, thermal and worksite safety controls remain necessary.
7. Suitable for Selected Field Applications
Induction heating can be considered for approved field heat-treatment operations where large furnace heating is impractical.
Important Technical Limitations
| Limitation | Engineering Explanation | Recommended Action |
|---|---|---|
| Material Restrictions | Incorrect treatment conditions may change mechanical properties. | Follow the approved material-specific procedure. |
| Local Temperature Gradients | Localized heating may produce nonuniform temperatures. | Verify heating-band and thermocouple arrangements. |
| Continuous Operating Duty | Long soaking periods require sustained equipment operation. | Confirm rated cooling and output capability. |
| Input Current Data | Historical published values are not fully consistent with output ratings. | Obtain verified factory electrical specifications. |
| Temperature Accuracy | Published tolerance lacks complete test conditions. | Verify measuring and control performance. |
| Independent Heating Zones | Six measurement channels do not establish six independent outputs. | Confirm control-zone configuration. |
| PWHT Compliance | Equipment features alone do not establish process compliance. | Use qualified procedures and required records. |
Why Choose HLQ?
HLQ Induction Equipment Co., Ltd. supplies industrial induction heating equipment for metal processing, welding preparation, pipe heating and selected post-weld thermal treatment applications.
Industrial MYD Model Range
The MYD series provides published nominal output ratings from 40 kW to 120 kW for industrial heating requirements.
IGBT Induction Power Technology
IGBT-based induction generators produce high-frequency electrical power for compatible heating coils.
Application-Specific Induction Coils
Flexible cable arrangements can be evaluated for suitable steel pipes and fabricated metal components.
PLC-Based Operation
The published equipment includes PLC touchscreen control and multi-point temperature-monitoring features.
Temperature Recording Options
Selected system configurations can include digital temperature recording and associated accessories.
Engineering-Oriented Equipment Selection
Appropriate equipment selection considers workpiece material, dimensions, thermal cycle, heating-zone geometry, temperature uniformity, monitoring requirements and operating duty.
For material-specific stress management, review HLQ induction stress relief systems.
Other related industrial processes are described in HLQ welding preheating equipment resources.
10 Core FAQs
1. What Is an Induction PWHT Machine?
An induction PWHT machine is an industrial heating system that uses electromagnetic induction to heat suitable welded metal components according to a specified post-weld thermal cycle. The process may involve controlled heating, soaking, holding and cooling.
2. What Power Ratings Are Available in the HLQ MYD Series?
The original HLQ product page lists six nominal output ratings: 40 kW, 50 kW, 60 kW, 80 kW, 100 kW and 120 kW.
3. What Is the Output Frequency of the MYD PWHT Machine?
The published output frequency range on this product page is 2–36 kHz. Actual operation depends on the generator configuration and connected induction heating circuit.
4. Can Induction Heating Be Used for Pipeline Weld PWHT?
Yes, when the material, applicable standard and approved thermal procedure permit localized induction PWHT. The heating system must achieve the required temperature distribution, heating and cooling rates, holding conditions and records.
5. Where Should Thermocouples Be Installed?
Thermocouple junctions should contact the steel pipe directly at the required measurement locations. The thermal insulation blanket then covers the pipe and sensors, while the induction heating cable is installed outside the insulation.
6. Can Metallic Bands Be Used to Secure Thermal Insulation?
Unapproved metallic bands or steel wire should not be used within the active induction-heating region. Suitable non-metallic, high-temperature insulating straps should be used according to the approved installation requirements.
7. Does a Six-Channel Temperature Controller Provide Six Independent Heating Zones?
Not necessarily. Six measurement channels may allow six thermocouples to be monitored, but this does not automatically mean that six independent induction outputs are available. The actual control-zone configuration must be confirmed.
8. What Temperature Is Required for Post-Weld Heat Treatment?
There is no universal PWHT temperature suitable for every steel. Required treatment conditions depend on the material grade, original heat-treatment condition, wall thickness, welding procedure and applicable standard.
9. How Much Electrical Power Is Required for Induction PWHT?
Required power depends on the heated metal mass, target temperature, thermal losses, induction coil coupling, heating-rate requirements and sustained holding conditions. A reliable selection requires engineering calculations and verification of the generator’s operating capability.
10. Does Using an Induction PWHT Machine Guarantee Compliance with ASME or Other Standards?
No. Equipment capability alone does not establish code compliance. The complete thermal treatment must follow the applicable qualified procedure and satisfy requirements for temperature measurement, heating and cooling rates, soaking duration, records and acceptance.
Technical Information Notice
The MYD equipment specifications presented on this page are based on historical manufacturer-published information.
Published input currents, continuous output capability, temperature accuracy, cooling configuration and operating limits require verification against current factory data.
The engineering calculations and thermal-cycle examples are illustrative and do not represent measured customer performance or approved material-specific treatment schedules.
Actual PWHT operations must comply with the applicable construction or repair requirements, approved thermal procedure, equipment instructions and relevant safety standards.