

Steel Bar Induction Forging, Aluminum Billet Induction Heating, Titanium Rod Forging Heater, Brass Extrusion Die Induction Heater, Copper Billet Induction Heating-Ferrous Billet Induction Forging
Steel Bar Induction Forging, Aluminum Billet Induction Heating, Titanium Rod Forging Heater, Brass Extrusion Die Induction Heater, Copper Billet Induction Heating, Ferrous Billet Induction Forging, and Non-Ferrous Metal Forging Heater Guide
Table 1. Induction Heating vs Traditional Heating
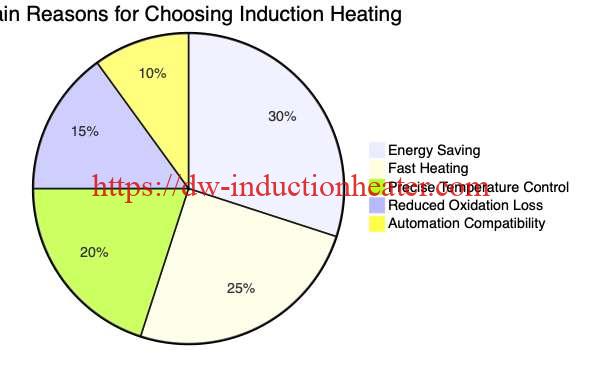
Chart 1. Main Reasons Manufacturers Use Induction Heating
Table 2. Main Components of an Induction Forging Heater
Table 3. Typical Heating Targets by Workpiece
Which Materials Are Suitable for Billet Forge Induction Heating?
Table 4. Suitable Materials for Induction Heating
Table 5. Typical Heating Temperature Range by Material
Table 6. Material Heating Characteristics
Chart 2. Typical Temperature Band Comparison
Chart 3. Induction Heating Principle Flow
Table 7. Factors Affecting Heating Performance
Table 8. Recommended Frequency Trend by Billet Diameter
Table 9. Common Heating Problems and Solutions
Table 10. Application Matrix by Material
Table 11. Typical Products After Induction Heating
Chart 4. Typical Production Line Sequence
Table 12. Industry-Based Application Summary
Table 13. Main Advantages of Induction Forging Heaters
Table 14. Induction Heating vs Conventional Furnace in Production
Table 15. Economic Benefit Comparison
Table 16. Common Types of Equipments
Table 17. Equipment Selection by Metal Family
Equipment & Technical Parameters
Table 19. Typical Technical Parameter Range
Table 20. Material-Based Parameter Reference
Table 21. Example Equipment Configurations
Table 22. Utility and Control Requirements
Table 23. Typical Capacity Guide
Chart 6. Billet Size vs Equipment Trend
How to Choose a Suitable Equipment?
Table 24. Equipment Selection Checklist
Table 25. Quick Selection Guide
Chart 7. Equipment Selection Flow
Chart 8. Material Suitability Overview
Frequently Asked Questions (FAQs)
- What is a billet induction heater used for?
- Can induction heating be used for both ferrous and non-ferrous metals?
- Is induction heating good for aluminum billets?
- Can titanium rods be heated by induction?
- Why is a brass extrusion die induction heater important?
- Is copper difficult to heat by induction?
- What frequency is best for steel billet forging?
- Does induction heating reduce oxidation loss?
- Is induction heating easy to automate?
- How do I choose the right induction forging heater?
- Can one machine heat different materials?
- Why is coil design important?
- What is the biggest advantage of induction heating?
- Is induction heating suitable for continuous production lines?
- What technical data should be prepared before buying equipment?
Introduction
Induction heating has become one of the most efficient heating technologies in modern metal forging, extrusion, and hot-forming industries. Manufacturers today require fast heating speed, accurate temperature control, low oxidation loss, high productivity, and easy integration with automatic production lines. This is why steel bar induction forging, aluminum billet induction heating, titanium rod forging heater systems, brass extrusion die induction heater units, copper billet induction heating machines, ferrous billet induction forging lines, and non-ferrous metal forging heaters are widely used across industrial plants.
Compared with traditional coal, gas, and resistance furnaces, induction heating provides several important advantages. It heats the metal directly instead of heating the surrounding furnace chamber. This reduces wasted energy and shortens heating time. It also lowers oxidation and decarburization, which helps improve product quality and metal yield. Because induction equipment can be linked with feeding systems, temperature sensors, PLC controls, and forging presses, it also supports cleaner and smarter factory operation.
Table 1. Induction Heating vs Traditional Heating
| Item | Induction Heating | Gas Furnace | Resistance Furnace |
| Heating speed | Very fast | Slow | Medium |
| Energy efficiency | High | Medium | Medium |
| Temperature control | Precise | Moderate | Good |
| Oxidation loss | Low | High | Medium |
| Automation capability | Excellent | Limited | Moderate |
| Workshop cleanliness | Clean | More fumes and heat | Cleaner than gas |
| Start/stop flexibility | Strong | Weak | Moderate |
| Space requirement | Compact | Larger | Medium |
Chart 1. Main Reasons Manufacturers Use Induction Heating
What is it?
A billet forge induction heating system is an industrial machine used to heat metal bars, rods, billets, tubes, or dies before hot forging, extrusion, upsetting, rolling, bending, or preheating operations. Depending on the application, it may be called an induction forging heater, induction billet heater, induction bar heating machine, forging induction furnace, or die induction heater.
The equipment usually consists of an induction power supply, induction coil, water cooling unit, feeding device, temperature monitoring unit, and control system. When alternating current flows through the induction coil, it generates an alternating magnetic field. When the metal workpiece enters this magnetic field, eddy currents are generated inside the material. The metal’s own resistance converts these currents into heat, causing rapid internal heating.
Table 2. Main Components of an Induction Forging Heater
| Component | Function |
| Induction power supply | Converts incoming electricity into controlled induction output |
| Induction coil | Generates electromagnetic field around the billet |
| Water cooling system | Cools coil and power components |
| PLC/HMI control system | Controls heating cycle and operating parameters |
| Infrared pyrometer | Measures billet surface temperature |
| Feeding mechanism | Transfers workpieces into the heating zone |
| Discharge/transfer device | Moves heated billet to press or extrusion machine |
| Safety protection unit | Protects operators and equipment |
Table 3. Typical Heating Targets by Workpiece
| Workpiece | Typical Process | Heating Goal |
| Steel bar | Forging/upsetting | Full forging temperature |
| Aluminum billet | Extrusion/forging | Uniform lower-temperature heating |
| Titanium rod | Precision forging | Accurate temperature control |
| Brass die | Extrusion die preheating | Reduce thermal shock |
| Copper billet | Hot forming | Fast and even heating |
| Ferrous billet | Open/closed die forging | Deep heat penetration |
| Non-ferrous bar | Forming/pressing | Clean and controlled heating |
Which Materials Are Suitable for Billet Forge Induction Heating?
Induction heating is suitable for a wide range of metallic materials. These can generally be divided into ferrous metals and non-ferrous metals. Ferrous materials include carbon steel, alloy steel, stainless steel, spring steel, bearing steel, and iron-based billets. Non-ferrous materials include aluminum alloys, copper, brass, bronze, titanium, and titanium alloys.
Material properties strongly affect induction heating behavior. Steel usually responds very efficiently because of its magnetic and electrical characteristics, especially at moderate temperatures. Aluminum and copper can also be heated successfully, but because they are non-magnetic and highly conductive, the equipment must be carefully matched in terms of power, frequency, and coil design. Titanium also requires high precision because improper heating can affect metallurgical quality and final mechanical performance.
Table 4. Suitable Materials for Induction Heating
| Material Category | Typical Grades | Suitability | Main Uses |
| Carbon steel | 1045, C45, S45C | Excellent | Shafts, bolts, flanges |
| Alloy steel | 4140, 42CrMo | Excellent | Automotive and machinery parts |
| Stainless steel | 304, 316, 410 | Good | Fittings, valves, special parts |
| Tool steel | H13, D2 | Good | Forging blanks and tools |
| Aluminum alloy | 6061, 6063, 7075 | Excellent | Extrusion and lightweight forgings |
| Copper | C110, ETP copper | Good | Conductive and formed components |
| Brass | H62, H65, C360 | Excellent | Hardware, fittings, valves |
| Bronze | Tin bronze, phosphor bronze | Good | Bushings and wear parts |
| Titanium alloy | Ti-6Al-4V | Good | Aerospace and medical components |
Table 5. Typical Heating Temperature Range by Material
| Material | Typical Heating Range | Notes |
| Carbon steel | 1050 to 1250 C | Common forging temperature |
| Alloy steel | 1000 to 1200 C | Depends on alloy grade |
| Stainless steel | 1050 to 1180 C | Requires uniform heating |
| Aluminum alloy | 350 to 550 C | Avoid overheating |
| Copper | 650 to 850 C | Needs optimized power matching |
| Brass | 600 to 800 C | Suitable for billet and die heating |
| Titanium alloy | 850 to 1100 C | Tight control required |
Table 6. Material Heating Characteristics
| Material | Magnetic Property | Conductivity | Heating Characteristic | Control Focus |
| Carbon steel | Magnetic | Medium | Fast and efficient | Prevent excessive scale |
| Alloy steel | Magnetic | Medium | Stable response | Uniform cross-section heating |
| Stainless steel | Varies | Medium | Good with proper tuning | Temperature consistency |
| Aluminum alloy | Non-magnetic | High | Needs matched design | Avoid local overheating |
| Copper | Non-magnetic | Very high | Requires optimized system | Raise efficiency |
| Brass | Non-magnetic | Medium-high | Easy to control | Stable billet temperature |
| Titanium alloy | Non-magnetic | Low-medium | Good with precision control | Narrow temperature window |
Chart 2. Typical Temperature Band Comparison
Steel            1050-1250 C  |####################|
Alloy steel      1000-1200 C  |##################  |
Stainless steel  1050-1180 C  |#################   |
Aluminum alloy    350-550 C   |######              |
Copper            650-850 C   |##########          |
Brass             600-800 C   |#########           |
Titanium alloy    850-1100 C  |###############     |
Principle
The principle of induction heating is based on electromagnetic induction. Alternating current passes through an induction coil and creates an alternating magnetic field. When a conductive metal workpiece is placed inside or near the coil, this changing magnetic field induces eddy currents in the metal. These eddy currents flow through the workpiece and generate heat because of the electrical resistance of the material.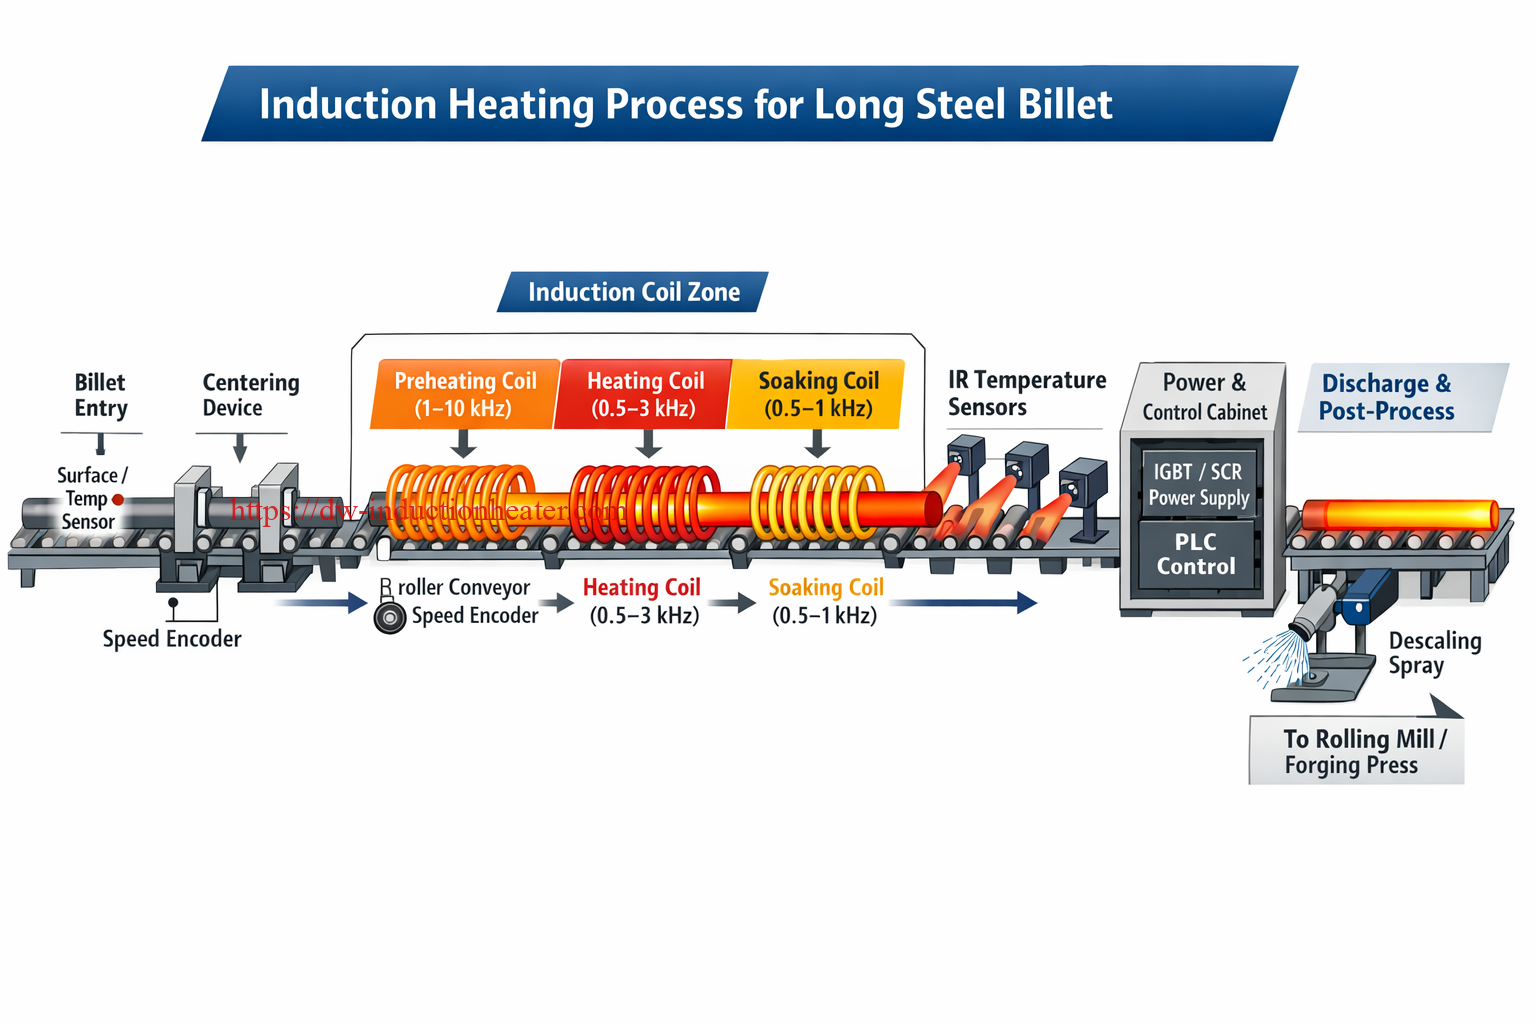
For ferromagnetic materials such as carbon steel, another effect called hysteresis heating also contributes below the Curie temperature. Together, these effects make the workpiece heat rapidly and efficiently from within. Heating depth depends on frequency, billet diameter, material conductivity, and magnetic properties. Lower frequencies are often better for large ferrous billets because they allow deeper penetration. Higher frequencies are more suitable for smaller bars, local heating, or surface heating.
Chart 3. Induction Heating Principle Flow
AC Input Power
Induction Power Supply
Induction Coil
Alternating Magnetic Field
Eddy Currents in Metal
Internal Heat Generation
Temperature Monitoring
Forging / Extrusion / Pressing
Table 7. Factors Affecting Heating Performance
| Factor | Influence | Practical Effect |
| Frequency | Controls heating depth | Must match billet size |
| Power | Controls heating speed | Higher power means higher throughput |
| Coil design | Controls coupling efficiency | Affects uniformity and energy use |
| Heating time | Controls final temperature | Must match line speed |
| Material conductivity | Affects heat generation | Important for copper and aluminum |
| Magnetic permeability | Influences induction efficiency | Important for steel |
| Cooling system | Protects equipment | Essential for stable operation |
| Temperature feedback | Improves control accuracy | Reduces overheating and rejects |
Table 8. Recommended Frequency Trend by Billet Diameter
| Billet Diameter | Frequency Trend | Typical Use |
| 10 to 25 mm | Higher frequency | Small rods and local heating |
| 25 to 60 mm | Medium-high frequency | Bars and small billets |
| 60 to 120 mm | Medium frequency | Standard forging billets |
| 120 mm and above | Lower-medium/custom | Large-section ferrous billets |
Table 9. Common Heating Problems and Solutions
| Problem | Possible Cause | Recommended Solution |
| Uneven temperature | Poor coil design | Optimize coil geometry |
| Surface overheating | Frequency too high | Adjust frequency or power |
| Core underheating | Penetration too shallow | Increase heating time or lower frequency |
| High oxidation | Temperature too high | Optimize setpoint and transfer speed |
| Low efficiency on copper | Coil mismatch | Redesign system for copper heating |
| Equipment overheating | Poor water cooling | Improve cooling flow and quality |
| Temperature fluctuation | Manual feeding inconsistency | Add automatic feeding and pyrometer control |
Applications
Induction heating equipment is widely used in forging, extrusion, rolling, upsetting, die preheating, and hot-forming industries. Steel bar induction forging is common in automotive, tools, construction hardware, and fastener production. Aluminum billet induction heating is widely used before extrusion and forging to ensure more stable material flow and improved surface quality. Titanium rod forging heaters are important in aerospace, medical, and defense manufacturing where precise temperature control is essential.
Brass extrusion die induction heaters are used to preheat dies and reduce cracking caused by thermal shock. Copper billet induction heating systems are used in electrical, connector, and specialized copper component manufacturing. Ferrous billet induction forging lines are widely used for large steel shafts, rings, gears, and machine parts. Non-ferrous metal forging heaters are used for aluminum, brass, bronze, and copper applications requiring clean and efficient billet heating.
Table 10. Application Matrix by Material
| Material | Main Application | Typical Industry |
| Steel bar | Forging, upsetting | Automotive, tools, fasteners |
| Ferrous billet | Open/closed die forging | Heavy machinery, mining, railway |
| Aluminum billet | Extrusion, forging | Construction, transport, profiles |
| Titanium rod | Precision forging | Aerospace, medical |
| Brass billet | Hot forming | Hardware, sanitary ware, fittings |
| Brass die | Die preheating | Extrusion lines |
| Copper billet | Hot forming, upsetting | Electrical and industrial components |
| Non-ferrous bars | Pressing, bending, preheating | General metalworking |
Table 11. Typical Products After Induction Heating
| Heated Material | Final Product Example |
| Steel bar | Bolts, gears, axles, sockets |
| Ferrous billet | Rings, shafts, large forgings |
| Aluminum billet | Profiles, forgings, transport parts |
| Titanium rod | Turbine parts, implants, aerospace fittings |
| Brass billet | Valves, plumbing fittings |
| Copper billet | Connectors, conductive formed parts |
| Non-ferrous bars | Precision hot-formed sections |
Chart 4. Typical Production Line Sequence
Raw Billet or Bar
Automatic Feeding
Induction Heating Zone
Temperature Detection
Transfer to Press or Extruder
Forming Operation
Trimming / Finishing
Table 12. Industry-Based Application Summary
| Industry | Common Material | Induction Heating Purpose |
| Automotive | Steel, alloy steel, aluminum | Forged shafts, gears, lightweight parts |
| Aerospace | Titanium, alloy steel | Precision hot forging |
| Construction | Aluminum billets | Extrusion of profiles and frames |
| Hardware | Brass, steel | Fittings, valves, fasteners |
| Electrical | Copper, brass | Conductive component forming |
| Heavy machinery | Ferrous billets | Large forged blanks and shafts |
Advantages
Induction forging heaters offer major advantages over conventional furnaces. The most important advantage is high efficiency. Since the heat is generated directly inside the workpiece, energy waste is much lower. Another key advantage is fast heating speed, which improves productivity and shortens the production cycle. Precise temperature control is also very important, especially for titanium, aluminum, and high-value alloy forging processes.
Induction heating also reduces oxidation and decarburization because the material spends less time at high temperature. This improves metal yield and helps maintain surface quality. In addition, induction systems are easier to automate and produce a cleaner workshop environment because there is no open flame or combustion gas in the heating area.
Table 13. Main Advantages of Induction Forging Heaters
| Advantage | Operational Benefit |
| Fast heating | Higher production efficiency |
| Accurate control | Better process stability |
| Lower oxidation | Higher material yield |
| Energy saving | Lower operating cost |
| Compact layout | Better use of workshop space |
| Easy automation | Reduced labor intensity |
| Cleaner production | Improved working environment |
| High repeatability | Lower defect rate |
Table 14. Induction Heating vs Conventional Furnace in Production
| Production Indicator | Induction Heating | Conventional Furnace |
| Heating cycle | Short | Long |
| Oxidation scale | Low | High |
| Start-up time | Short | Long |
| Control response | Fast | Slow |
| Product consistency | High | Moderate |
| Automation integration | Strong | Weak |
| Energy loss | Low | High |
Table 15. Economic Benefit Comparison
| Cost Factor | Traditional Furnace | Induction Heating | Benefit |
| Energy consumption | Higher | Lower | Cost saving |
| Oxidation loss | Higher | Lower | Better yield |
| Labor requirement | Higher | Lower | Better efficiency |
| Scrap risk | Higher | Lower | Improved quality |
| Maintenance environment | Dirtier | Cleaner | Easier maintenance |
Chart 5. Main ROI Drivers
Energy saving -> High impactLower oxidation loss -> High impactFaster cycle time -> High impactLower labor cost -> Medium-high impactBetter temperature -> High impactLess scrap -> Medium-high impact
Types of Equipments
There are different types of induction heating equipment depending on production style, billet shape, size, and heating requirement. Horizontal billet heaters are common for continuous bar and billet feeding. Vertical induction heaters are chosen where floor space or handling method favors vertical positioning. Medium-frequency induction heaters are widely used for steel and large ferrous billets because they offer strong penetration. High-frequency systems are typically used for smaller bars, local heating, or surface applications.
Modern power supplies often use IGBT technology due to its high efficiency and compact design. SCR-based systems are also used in heavy-duty applications. Some systems are dedicated to billet heating, while others are designed for end heating, die preheating, or integrated automation lines.
Table 16. Common Types of Equipments
| Equipment Type | Features | Best For |
| Horizontal billet heater | Continuous feeding, high output | Steel bars and billets |
| Vertical induction heater | Space-saving layout | Special production lines |
| Medium-frequency heater | Good penetration depth | Ferrous billets and bars |
| High-frequency heater | Fast and localized heating | Small rods and ends |
| IGBT induction system | Efficient and compact | Modern production lines |
| SCR induction system | Heavy-duty power capacity | Large industrial applications |
| Automatic heating line | PLC, conveyors, sensors | Integrated forging cells |
| Die induction heater | Precise local preheating | Brass extrusion dies |
| End heating machine | Heats only one section | Upsetting and bolt making |
Table 17. Equipment Selection by Metal Family
| Metal Family | Preferred Equipment Trend |
| Carbon steel and alloy steel | Medium-frequency billet heater |
| Large ferrous billets | High-power continuous line |
| Aluminum alloy | Optimized non-ferrous billet heater |
| Copper | Customized matched induction heater |
| Brass | Billet heater or die preheater |
| Titanium | Precision-controlled forging heater |
Table 18. Automation Modules
| Automation Module | Main Function | Benefit |
| Automatic feeder | Loads billets continuously | Higher throughput |
| Infrared pyrometer | Monitors temperature | Better control |
| PLC + HMI | Stores recipes and alarms | Easier operation |
| Billet separator | Spaces billets correctly | More stable heating |
| Robot transfer arm | Moves billet to press | Lower manual handling |
| Safety interlock | Protects line operation | Improved safety |
Equipment & Technical Parameters
The technical parameters of an induction forging heater vary according to material type, billet size, production speed, and target temperature. Buyers usually compare systems by rated power, frequency range, billet diameter, billet length, heating temperature, cycle time, automation level, and cooling requirement.
Table 19. Typical Technical Parameter Range
| Parameter | Typical Range |
| Power rating | 50 kW to 3000 kW |
| Frequency | 500 Hz to 100 kHz |
| Billet diameter | 10 mm to 300 mm or more |
| Billet length | Customized |
| Heating temperature | 200 C to 1250 C |
| Heating time | Seconds to several minutes |
| Control mode | Manual, semi-automatic, fully automatic |
| Cooling method | Water cooling |
| Temperature monitoring | Infrared pyrometer, thermal feedback |
| Interface | PLC, HMI, machine linkage |
Table 20. Material-Based Parameter Reference
| Material | Power Trend | Frequency Trend | Priority |
| Steel bar | Medium to high | Medium | Throughput and penetration |
| Ferrous billet | High | Medium/lower-medium | Deep uniform heating |
| Aluminum billet | Medium | Carefully matched | Low-temp uniformity |
| Copper billet | Medium to high | Optimized | Efficiency and consistency |
| Brass billet | Medium | Medium/high | Stable temperature |
| Titanium rod | Medium | Precision controlled | Tight temperature window |
| Brass die | Low to medium | Localized | Die temperature accuracy |
Table 21. Example Equipment Configurations
| Application | Billet Size Example | Temperature | Suggested Equipment |
| Steel bar forging | 30 to 80 mm | 1100 to 1250 C | Medium-frequency horizontal heater |
| Large ferrous billet forging | 100 to 180 mm | 1150 to 1250 C | High-power continuous line |
| Aluminum billet extrusion | 60 to 150 mm | 400 to 550 C | Non-ferrous billet heater |
| Titanium rod forging | 20 to 70 mm | 850 to 1050 C | Precision-controlled induction heater |
| Brass die preheating | Custom die size | 300 to 600 C | Dedicated die induction heater |
| Copper billet heating | 20 to 100 mm | 650 to 850 C | Optimized copper billet heater |
Table 22. Utility and Control Requirements
| Item | Typical Requirement |
| Electrical supply | Must match installed power |
| Cooling water | Stable flow, pressure, clean water |
| Floor layout | Feeding zone, heating zone, transfer route |
| Control system | PLC and HMI recommended |
| Safety system | Overcurrent, overheat, low-water alarm |
| Coil maintenance | Quick-change design preferred |
Table 23. Typical Capacity Guide
| Power Range | Billet Size | Typical Use |
| 50 to 150 kW | Small rods and ends | End heating, small forging |
| 160 to 300 kW | Small to medium billets | General bar forging |
| 300 to 600 kW | Medium billets | Continuous forging line |
| 600 to 1200 kW | Large steel billets | Heavy-duty forging |
| 1200 kW and above | Large-section heating | High-output industrial lines |
Chart 6. Billet Size vs Equipment Trend
10-25 mm -> Higher frequency, fast heating25-60 mm -> Medium-high frequency, stable output60-120 mm -> Medium frequency, deeper penetration120 mm+ -> Lower-medium/custom, high power
How to Choose a Suitable Equipment?
Choosing the right induction forging equipment starts with understanding the material, billet dimensions, and process target. Different materials respond differently to induction heating, so a machine for steel forging may not be ideal for copper or aluminum heating. The user should first determine the material grade, billet diameter, length, and final process temperature. After that, the required hourly output, heating uniformity, and automation level should be confirmed.
Another important factor is factory condition. Available electrical capacity, water cooling capacity, floor layout, and interface requirements with existing forging or extrusion equipment all affect final machine selection. It is also important to choose a supplier that can provide coil design, sample testing, commissioning support, and after-sales service.
Table 24. Equipment Selection Checklist
| Selection Factor | Why It Matters |
| Material type | Affects heating behavior |
| Billet diameter | Determines penetration depth |
| Billet length | Affects coil design and feeding |
| Target temperature | Defines machine capability |
| Required output | Determines power selection |
| Heating uniformity | Directly affects product quality |
| Automation level | Influences control and transfer design |
| Cooling conditions | Protects machine stability |
| Installation space | Affects equipment layout |
| Supplier experience | Important for reliable results |
Table 25. Quick Selection Guide
| If Your Priority Is | Focus On |
| Maximum output | High power and continuous feeding |
| Best temperature consistency | Pyrometer feedback and coil optimization |
| Large steel billet heating | Medium/lower-medium frequency penetration |
| Aluminum extrusion | Uniform low-temperature control |
| Titanium forging | Tight temperature window control |
| Brass die preheating | Accurate local heating |
| Product change flexibility | Quick-change coil design |
Chart 7. Equipment Selection Flow
Ferrous
Non-Ferrous
Define Material
Ferrous or Non-Ferrous
Check Billet Diameter and Penetration Need
Check Conductivity and Temperature Sensitivity
Set Required Output
Choose Power and Frequency
Decide Automation Level
Confirm Utilities and Layout
Finalize Equipment Configuration
Chart 8. Material Suitability Overview
Billet Forge Induction Heating
Ferrous Metals
Non-Ferrous Metals
Carbon Steel
Alloy Steel
Stainless Steel
Aluminum Alloy
Copper
Brass
Titanium Alloy
Conclusion
Steel bar induction forging, aluminum billet induction heating, titanium rod forging heater systems, brass extrusion die induction heaters, copper billet induction heating systems, ferrous billet induction forging equipment, and non-ferrous metal forging heaters are all key parts of modern induction heating technology. They deliver fast heating, accurate control, lower oxidation, compact equipment layout, and strong automation compatibility.
Compared with conventional furnaces, induction heating provides better productivity and cleaner manufacturing conditions. It is suitable for many industrial materials and can be customized according to billet size, heating temperature, and production capacity. With the right system design and correct technical parameter matching, induction heating becomes a highly efficient and cost-effective solution for modern forging and hot-forming operations.
Frequently Asked Questions (FAQs)
1. What is a billet induction heater used for?
A billet induction heater is used to heat bars, billets, rods, or dies before forging, extrusion, upsetting, pressing, or other hot-forming processes.
2. Can induction heating be used for both ferrous and non-ferrous metals?
Yes. It is suitable for carbon steel, alloy steel, stainless steel, aluminum, copper, brass, titanium, and many other alloys.
3. Is induction heating good for aluminum billets?
Yes. Aluminum billet induction heating is widely used before extrusion and forging because it offers fast and controlled heating.
4. Can titanium rods be heated by induction?
Yes. Titanium rods can be heated effectively, but they require strict temperature control.
5. Why is a brass extrusion die induction heater important?
It helps preheat the die, reduce thermal shock, improve extrusion stability, and extend die service life.
6. Is copper difficult to heat by induction?
Copper can be heated well by induction, but it requires optimized power supply, frequency, and coil design because of its high conductivity.
7. What frequency is best for steel billet forging?
It depends on billet diameter. Medium frequency is commonly used for steel bars and forging billets.
8. Does induction heating reduce oxidation loss?
Yes. Because the heating time is shorter, oxidation and scale loss are usually lower than with traditional furnaces.
9. Is induction heating easy to automate?
Yes. It can be connected with feeders, PLC systems, pyrometers, robots, and forging presses.
10. How do I choose the right induction forging heater?
You should consider material type, billet size, target temperature, required capacity, automation needs, utilities, and supplier technical support.
11. Can one machine heat different materials?
In some cases, yes, but the settings, coil, and process parameters may need to be adjusted for each material.
12. Why is coil design important?
Coil design strongly affects heating efficiency, uniformity, power usage, and final process quality.
13. What is the biggest advantage of induction heating?
The biggest advantages are fast heating, accurate control, energy saving, and easy automation.
14. Is induction heating suitable for continuous production lines?
Yes. It is one of the best options for semi-automatic and fully automatic forging and extrusion lines.
15. What technical data should be prepared before buying equipment?
You should prepare the material grade, billet size, required temperature, output per hour, heating method, and factory power and cooling conditions.
Multi-Metal Induction Heating Systems_Steel Bar Forging_Aluminum Billet Heating_Titanium Rod Forging
Related products
-

Induction Forge Furnaces for Hot Forming Steel Billets-Copper Bars and Aluminum Rods
-
Steel Copper Aluminum Billet Forge Induction Heater | Efficient Induction Heating for Metals Forging
-
Aluminium Billet Induction Heater for Extrusion Energy Efficient Metals Heating Solution
-
Induction Forge Furnace
-
Semi-Automatic Induction Foging Rod Furnace