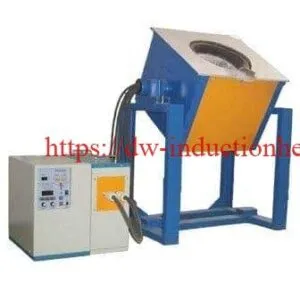





Induction Aluminum Melting Furnace
Induction Aluminum Melting Furnace for Foundry Casting and Recycling
Quick Answer: The HLQ JLRRL induction aluminum melting furnace series is designed for aluminum foundries, alloy casting and sorted scrap remelting. The current product page publishes three configurations: JLRRL-150 (150 kg batch, 30 kW, 65 kg/h), JLRRL-300 (300 kg, 60 kW, 130 kg/h), and JLRRL-500 (500 kg, 70 kW, 170 kg/h). All three list an 850°C maximum temperature. These are manufacturer-stated nominal figures, not independently verified melt tests. The exact induction output frequency and utility ratings must be confirmed for the selected unit.
Selection principle: Match the furnace first to hourly production, alloy and scrap condition, then verify crucible working volume, electrical capacity, cooling, pouring method and the supplier’s factory acceptance test (FAT). Batch capacity alone does not determine production throughput.
Table of Contents
- What is the Induction Aluminum Melting Furnace?
- Key Applications
- Suitable Materials
- Working Principle
- Technical Specifications
- Recommended Model Selection
- Process Workflow
- Coil and Fixture Design
- Control System and Automation
- Common Problems and Solutions
- Engineering Selection Guide
- Advantages
- Limitations
- Why Choose HLQ Induction Equipment?
- Core FAQs
What is the Induction Aluminum Melting Furnace?
An induction aluminum melting furnace is an electric system that uses a water-cooled induction coil and a power inverter to heat an aluminum charge, either directly or through a conductive crucible or susceptor. It is best suited to organized foundry operations that need repeated melts of aluminum ingots, selected alloys or clean, sorted returns with controllable temperature and planned pouring. The JLRRL series is a 150-500 kg nominal batch range; the equipment must be matched to the actual target kg/h rather than the nameplate batch size alone.
Unlike a general-purpose steel-melting furnace, an aluminum system must account for aluminum’s relatively low density, its nonferromagnetic behavior, reactive surface oxide and the large physical volume occupied by a given charge mass. Coil matching, vessel geometry and contamination control therefore play major roles in real furnace performance.
For a broader process layout that includes metal charging, remelting and industrial applications, compare HLQ’s aluminum induction melting furnace for casting and recycling overview; this guide focuses on selecting the three published JLRRL models.
| Buyer Question | Direct Engineering Answer | Purchase Implication |
|---|---|---|
| What size of job? | 150, 300 or 500 kg nominal batch models | Check safe working fill and hourly melt demand. |
| What feedstock? | Aluminum ingots, approved alloy charge and pretreated/clean scrap | Wet, oily, coated, closed or mixed-metal scrap needs processing and risk assessment. |
| What is published? | 30-70 kW; 65-170 kg/h; 850°C maximum | Final inputs, power basis and performance-test conditions remain to be confirmed. |
| Is it a casting line? | It is a melting system; casting machines, degassing and molds are separate process items | Request line-level scope and integration responsibilities. |
Key Applications
The same melting technology can serve distinct production goals, but the charge preparation and melt handling are not interchangeable. A die-casting cell values steady delivery and holding; a secondary-aluminum recycler values sorted feed and dross recovery; a jobbing foundry values alloy changeovers and repeatable temperature records.
| Application | Typical Feed | Process Priority | Selection Advice |
|---|---|---|---|
| Aluminum gravity casting | Clean ingots and approved returns | Pour temperature and batch repeatability | Match batch to mold line, ladle and casting cycle. |
| Low-pressure or die casting supply | Specified A-series or wrought-derived alloy | Stable clean metal to holding or transfer | Include melt treatment, transfer and holding balance. |
| Secondary aluminum recycling | Dry sorted extrusion/profile/clean casting scrap | Metal yield, energy per recovered kg, dross | Use a documented pretreatment and chemistry-control plan. |
| Automotive foundry | A356/AlSi7Mg or relevant casting alloys | Composition, hydrogen control and traceability | Provide sampling, degassing and temperature records. |
| Small ingot remelting | Known commercial alloy ingots | Throughput with limited floor area | Select based on average kg/h and number of shifts. |
| Trial alloy development | Identified alloy charge | Clean changes and controlled superheat | Assess cross-contamination and crucible/lining compatibility. |
For more specialized scrap and recovery equipment, compare the aluminum scrap recycling furnace product family; the exact scrap specification should always be established before selection.
Suitable Materials
Pure aluminum melts near 660°C. Aluminum casting alloys have a composition-dependent solidus-liquidus range; the correct holding and pouring temperatures depend on the specific alloy, die or mold process, grain-refining and degassing requirements. The JLRRL page states a maximum of 850°C, but that figure is a machine limit, not an instruction to run every melt at 850°C.
| Material or Feed | Suitability | Temperature / Metallurgy Note | Required Precondition |
|---|---|---|---|
| Commercial-purity aluminum ingot | Primary target | Pure aluminum fusion near 660°C | Clean, identified, dry ingots. |
| Al-Si casting alloys | Good candidate | Use alloy-specific liquidus and pouring range | Control Si/Mg chemistry and inclusions. |
| A356 / AlSi7Mg | Good candidate after trial | Avoid unnecessary overheating and hydrogen pickup | Melt treatment plan and quality check. |
| Clean gate/riser returns | Common foundry use | Remelt yield depends on oxidation and surface area | Alloy-segregated, clean and completely dry. |
| Painted or oily post-consumer scrap | Conditional | Smoke, emissions and dross can dominate operations | Approved pretreatment, extraction and recovery planning. |
| Beverage cans and thin sheet | Conditional | Large surface area causes high oxide/dross risk | Remove moisture/coatings; use verified charging strategy. |
| Aluminum dross | Not interchangeable with metal scrap | Contains oxides/flux salts and entrained metal | Use a dedicated dross recovery process, not assumed full-metal yield. |
| Magnesium-rich or reactive blends | Case-by-case | May demand additional fire/safety controls | Competent process review before quotation. |
| Reference | Approximate Value | Engineering Meaning |
|---|---|---|
| Pure Al melting point | 660°C | Elemental melting reference, not complete alloy process recipe. |
| Common liquid-aluminum operating band | About 680-760°C, process-dependent | Confirm the individual alloy and casting method. |
| JLRRL maximum published furnace temperature | 850°C | Rated upper figure, not a normal default operating setpoint. |
| Enthalpy to melt pure Al from near room temperature | About 0.30 kWh/kg theoretical | A thermodynamic lower bound before furnace losses and superheat. |
Working Principle
An inverter draws power from the factory electrical service and sends alternating current through a specially matched induction coil. The time-varying magnetic field induces circulating currents in conductive metal and potentially in a graphite or other susceptor crucible. These currents become heat by electrical resistance. In molten aluminum, electromagnetic forces may promote some bath circulation, but the degree of stirring is equipment-specific.
| Stage | Engineering Function | What Should Be Checked |
|---|---|---|
| Three-phase mains / supply | Provides electrical power | Input voltage, phase, frequency, full-load kVA, harmonics, power factor. |
| Inverter / matching network | Sets coil frequency and current | Exact operating kHz, matching range, protection design. |
| Water-cooled copper coil | Generates electromagnetic field | Coil turns, current, flow interlock and insulation clearances. |
| Crucible or refractory container | Contains charge and may absorb induction power | Material compatibility, erosion life, thermal shock and actual ID/height. |
| Charge and molten bath | Absorbs heat and reaches pour readiness | Load density, scrap shape, oxidation, temperature and hold time. |
| Pouring system | Transfers metal to the next process | Manual/tilting/ladle choice, spout and guarding. |
Fundamental Estimate: Q = m × [cp,s × (Tm − T0) + Lf + cp,l × (Tp − Tm)], with m in kg and Q in kJ. For an illustrative pure-aluminum charge at 25°C heated to 720°C, using cp,s ≈ 0.90 kJ/(kg·K), latent heat ≈ 397 kJ/kg and cp,l ≈ 1.18 kJ/(kg·K), the ideal charge heating requirement is approximately 0.29 kWh/kg. It deliberately excludes crucible heating, idle losses, dross formation, exhaust, holding and electrical losses. U.S. Department of Energy reference data describe around 0.30 kWh/kg as the theoretical minimum to melt pure aluminum from room temperature.
Technical Specifications
The following table transcribes the three principal JLRRL configurations from the original HLQ product page. Values shown as “not published” must be added to a formal specification or acceptance test; they must not be inferred from another HLQ furnace range.
| Parameter | JLRRL-150 | JLRRL-300 | JLRRL-500 |
|---|---|---|---|
| Nominal power | 30 kW | 60 kW | 70 kW |
| Nominal aluminum batch capacity | 150 kg | 300 kg | 500 kg |
| Published melting rate | 65 kg/h | 130 kg/h | 170 kg/h |
| Maximum temperature | 850°C | 850°C | 850°C |
| Crucible ID × H | 42 × 67 cm | 53 × 65 cm | 63 × 72 cm |
| Furnace external dimensions | 1240 × 1210 × 980 mm | 1400 × 1370 × 980 mm | 1570 × 1540 × 1080 mm |
| Induction output frequency | Not published | Not published | Not published |
| Electrical input V / A / kVA | Not published | Not published | Not published |
| Cooling-water flow / pressure | Not published | Not published | Not published |
| Measured kWh per kg | Not published | Not published | Not published |
| Parameter | Specification | Notes |
|---|---|---|
| Equipment type | Electromagnetic induction aluminum melting furnace | JLRRL-150 / 300 / 500. |
| Furnace working capacity | 150 / 300 / 500 kg as published | Safe fill must be checked using actual refractory internal geometry. |
| Nominal power | 30 / 60 / 70 kW as published | Page does not clarify input-versus-output reference. |
| Melting rate | 65 / 130 / 170 kg/h as published | Need test conditions: alloy, hot/cold start, metal yield, pour temperature. |
| Published temperature ceiling | 850°C | Confirm instrument point and control range. |
| Crucible technology | Vendor-specific refractory/crucible assembly | Material and life not fully identified in target page. |
| Temperature control | PID and digital controller described on page | Claims of ±3°C require measurement validation. |
| Power-stage protection | Over/undervoltage, phase, current and overheat functions claimed | Review safety circuit drawings and FAT procedures. |
| Power converter | IGBT-based induction circuit described | Obtain OEM bill of materials and warranty terms. |
| Cooling and utilities | Confirm per selected model | No verified flow, pressure, heat rejection or water-quality schedule supplied. |
| Operating duty | Continuous-duty capability claimed | Define ambient, duty, maintenance and cooling requirements in writing. |
| Model | Capacity (kg) | Published Melting Rate (kg/h) | Implied Time: Full Charge / Rate |
|---|---|---|---|
| JLRRL-150 | 150 | 65 | 2.31 h |
| JLRRL-300 | 300 | 130 | 2.31 h |
| JLRRL-500 | 500 | 170 | 2.94 h |
The implied durations above are arithmetic capacity divided by nominal kg/h, not guaranteed first-melt cycle times. A cold start, retained heel, hot crucible, melting-and-pouring overlap and batch scheduling all change actual cycle behavior.
| Model | Published kW ÷ kg/h | Numerical Quotient (kWh/kg) | Interpretation |
|---|---|---|---|
| JLRRL-150 | 30 / 65 | 0.462 | Not a metered electricity-consumption figure. |
| JLRRL-300 | 60 / 130 | 0.462 | Not a verified furnace efficiency claim. |
| JLRRL-500 | 70 / 170 | 0.412 | Requires full-load power and time measurements. |
Recommended Model Selection
Choose from the actual JLRRL range if its documented hourly performance meets the production target. For unusually high volumes, ask about multi-furnace arrangements, automated charge handling or a larger induction melting furnace rather than oversizing batch capacity while keeping the same melting power.
| Application | Material | Recommended Power | Frequency |
|---|---|---|---|
| Up to around 65 kg/h nominal melt line | Clean Al ingots / approved casting returns | JLRRL-150: 30 kW published | Exact induction output kHz not published – obtain from HLQ |
| Up to around 130 kg/h nominal melt line | Al-Si cast alloy / clean returns | JLRRL-300: 60 kW published | Exact induction output kHz not published – obtain from HLQ |
| Up to around 170 kg/h nominal melt line | Sorted aluminum charge | JLRRL-500: 70 kW published | Exact induction output kHz not published – obtain from HLQ |
| 250 kg/h melting target | Clean aluminum or treated scrap | Requires custom sizing; no listed JLRRL model meets nominal rate alone | Specify in engineered RFQ |
| 500-1,000 kg/h industrial target | Aluminum foundry/secondary aluminum | Custom parallel or larger installation; calculate demand from SEC and throughput | Specify after vessel and load design |
| Buyer Priority | Likely Starting Model | Critical Confirmation |
|---|---|---|
| Minimum floor space and smaller periodic charge | JLRRL-150 | Does 65 kg/h nominal satisfy casting rhythm? |
| Moderate foundry throughput | JLRRL-300 | Confirm 130 kg/h at stated alloy and pouring temperature. |
| Larger batch plus slower turnover | JLRRL-500 | Verify 500 kg safe fill; only 170 kg/h nominal. |
| High continuous kg/h | Higher-power custom line | Size melting output and holding separately. |
Process Workflow
Process Flow: Material specification → scrap sorting and drying → furnace/cooling inspection → charge preparation → controlled induction heat-up → temperature and chemistry measurement → flux/degassing when specified → dross removal → safe pouring/transfer → sample/record → next batch.
| Step | Main Operation | Measured Checkpoint / Risk Control |
|---|---|---|
| 1. Material receiving | Identify alloy, inspect scrap and remove incompatible items | Alloy certificate, visual checks, no sealed or wet containers. |
| 2. Charge preparation | Separate and dry feedstock; preheat only under an approved procedure | No moisture, oils, pressure vessels or high-vapor contaminants. |
| 3. Pre-start checks | Inspect refractory, power cables, grounding and cooling | Approved coolant flow, return temperature, no leaks. |
| 4. Controlled melting | Apply matched power as charge settles | Power/current trend, elapsed time, abnormal noise/arc checks. |
| 5. Molten bath quality | Check temperature, sample composition and treat melt | Alloy-specific target; dross/oxide and hydrogen management. |
| 6. Pouring | Transfer with approved tilting and preheated dry tools | Ladle/transfer route, splash barriers, mold dryness. |
| 7. Production logging | Record mass, meter readings, time, yield and faults | kWh/kg of poured good metal and downtime trends. |
Coil and Fixture Design
Aluminum occupies a much larger volume than dense ferrous metals for the same mass. Furnace drawings must state the usable hot-face internal dimensions, not only a nominal crucible size. Effective melt volume also changes with refractory wear, spout layout and safe freeboard. One or more water-cooled coils surround the melting vessel, and magnetic flux, coil turns and inductor-to-load spacing must be tuned to the real charge.
| Component | Design Consideration | Approval Document |
|---|---|---|
| Induction coil | Turns, tube size, current, axial height, insulation | Coil drawing; electrical and water-flow test. |
| Crucible / refractory | Compatible with molten Al and flux; monitored wear | Material certificate, lining profile, drying/curing schedule. |
| Top freeboard | Headspace for wave motion, charging and pouring | Maximum allowed molten level marked on drawing. |
| Tilting/transfer mechanism | Stable center of gravity and controlled spout movement | Load path, guarding, limit switches and interlock proof. |
| Cooling-water lines | Separated from molten-metal spill path where possible | Flow, water quality, leak detection and loss-of-flow trip. |
| Maintenance access | Safe coil insulation, lining removal and electrical isolation | Lockout procedure and replacement spare dimensions. |
Crucible Capacity Screen: Treat the listed diameter and height as an ideal internal cylinder only for illustration, with molten Al density assumed 2.37 kg/L. Geometric volumes and implied fills are shown below. These numbers do not establish actual safe fill capacities, and particularly the JLRRL-500 requires explicit headspace verification.
| Model | Published ID × H | Ideal Cylindrical Volume | Metal Volume at 2.37 kg/L | Implied Fill |
|---|---|---|---|---|
| JLRRL-150 | 42 × 67 cm | 92.8 L | 63.3 L | 68.2% |
| JLRRL-300 | 53 × 65 cm | 143.4 L | 126.6 L | 88.3% |
| JLRRL-500 | 63 × 72 cm | 224.4 L | 211.0 L | 94.0% |
Because actual crucibles are not perfect internal cylinders and liquid density depends on temperature/alloy, these ratios are order-of-magnitude checks. Request the lining drawing, actual usable molten volume, approved maximum filling height and loading procedure; never use the theoretical cylinder volume as the operating fill limit.
Control System and Automation
The original listing refers to PID temperature regulation, closed-loop power control, frequency tracking and multiple fault protections. These feature statements must be translated into a signed control specification: define where the melt temperature is measured, whether PID controls bath temperature or another location, the alarm setpoints, and how loss of coolant or unexpected tilting is handled.
| Function | Baseline / Option | Acceptance Test |
|---|---|---|
| Power setpoint and ramp | Published general closed-loop power claim | Confirm displayed vs independently metered kW across loading levels. |
| Temperature feedback | PID/digital controller claimed | Check immersion probe calibration and actual bath error. |
| Cooling permissive | Essential interlock; implementation to confirm | Prove low-flow trip and safe restart sequence. |
| Electrical faults | Voltage/current/phase/overheat protections described | Test alarm logging and fail-safe shutdown. |
| Pouring actuator | Specify if manual, mechanical or hydraulic | Limit and emergency-stop checks under realistic loading. |
| PLC/HMI recipes | Optional, not confirmed on target JLRRL page | Recipe selection, access control and parameter retention. |
| Data logging | Optional | Batch mass, kWh, kg/h, bath temperature, alarms and downtime. |
| Factory interfaces | Optional Modbus/PROFINET/Ethernet per project | Signed point list and FAT protocol; do not assume standard inclusion. |
Common Problems and Solutions
| Problem | Likely Root Cause | Recommended Action |
|---|---|---|
| Melting rate below advertised kg/h | Cold furnace; wet/heavy scrap; low coupling; lost output | Log alloy, charge, actual power and cold/hot cycles; conduct controlled FAT. |
| High dross or oxidation | Dirty thin scrap, long hold, excessive superheat | Improve feed pretreatment, use minimum validated holding time/temperature. |
| Excessive kWh/kg | Idle holding, light partial loads, poor refractory, excess exhaust | Meter electricity and metal output separately; tune batch schedule. |
| Temperature reading drifts | Incorrect sensor location, calibration, oxide/slag interference | Use a validated immersion probe; recalibrate and record method. |
| Crucible or lining cracks | Poor dry-out, thermal shock, chemical incompatibility | Stop; replace/reline and follow OEM curing schedule. |
| Water-flow or overheat alarm | Scaling, pump fault, hot inlet, blocked coil | Shut down according to SOP; repair circuit before reuse. |
| Molten bath contaminated | Wrong alloy returns, tools or refractory particles | Sort charge, inspect vessels and verify chemistry before pouring. |
| Tilting mechanism unstable | Improper balance, worn pivot, pressure loss | Stop pouring; inspect mechanical/hydraulic system and interlocks. |
| Splashing during charge | Water, sealed scrap or uncontrolled insertion | Never introduce wet or sealed items; maintain defined dry-charge protocol. |
Engineering Selection Guide
1. Size Hourly Metal Output Before Nameplate Batch Capacity
Suppose a foundry needs 250 kg/h of liquid aluminum for eight productive hours. No single JLRRL model on this page claims 250 kg/h: even the 500 kg vessel lists only 170 kg/h. A 500 kg batch label does not make a 500 kg/h furnace. The process engineer should size required molten output, evaluate spare capacity, the cold-start penalty and the downstream holding requirement.
2. Calculate a Transparent Electrical-Energy Scenario
A useful planning sensitivity is required average electrical input (kW) = net delivered aluminum (kg/h) × assumed site-specific electricity (kWh/kg). It is not a guaranteed rating for a particular machine. The scenarios below are illustrative assumptions (0.45, 0.60 and 0.75 kWh/kg) that must be replaced by measured commissioning data, including appropriate loss and yield accounting.
| Poured Liquid Aluminum | 0.45 kWh/kg | 0.60 kWh/kg | 0.75 kWh/kg |
|---|---|---|---|
| 100 kg/h | 45 kW | 60 kW | 75 kW |
| 250 kg/h | 112.5 kW | 150 kW | 187.5 kW |
| 500 kg/h | 225 kW | 300 kW | 375 kW |
| 1,000 kg/h | 450 kW | 600 kW | 750 kW |
3. Calculate Electricity Cost Against Good-Metal Yield
At an example electricity tariff of US$0.12/kWh, 0.60 kWh/kg corresponds to US$0.072/kg of liquid metal for melting electricity alone. If only 95% becomes saleable metal, the same energy corresponds to roughly US$0.076/kg of good metal, before labor, crucibles, flux, maintenance, emissions control, depreciation and scrap-metal losses. Use local prices and metered plant results rather than marketing savings percentages.
| Electricity Intensity | Power Cost at $0.12/kWh | Cost per Saleable kg at 95% Yield |
|---|---|---|
| 0.45 kWh/kg | $0.054 per kg melted | $0.057 per kg saleable |
| 0.60 kWh/kg | $0.072 per kg melted | $0.076 per kg saleable |
| 0.75 kWh/kg | $0.090 per kg melted | $0.095 per kg saleable |
4. Request a Batch-Specific Factory Acceptance Test
Provide the alloy, feed form, moisture/contamination controls, kg per cycle, starting furnace condition, target poured-metal temperature and permissible power connection. The FAT should show charge mass, electrical kWh from a suitable meter, clock time, actual poured metal mass, chemistry, cooling parameters, alarms and operator sign-off.
| Topic | Required Buyer Input or Supplier Evidence | Why Critical |
|---|---|---|
| Process duty | kg/h, shifts, batches/day, longest continuous run | Separates vessel capacity from throughput. |
| Chemistry | Alloy grade, scrap fraction, acceptable contamination | Determines melting/holding recipe and yield. |
| Energy | Measured plant kWh, meter boundary and product yield | Makes SEC comparable. |
| Electrical | Grid voltage, phase, kVA and site transformer margin | Avoids undersized cables and protection. |
| Magnetic load | Output kHz range, coil geometry and matching scheme | Avoids frequency assumptions from other product families. |
| Crucible | Effective volume, max fill line and refractory specification | Critical for 500 kg capacity claim. |
| Safety | Dry-feed SOP, ventilation, molten-metal guarding, interlocks | Risk control for water/metal interactions. |
| Documentation | General arrangement, P&ID, wiring diagrams, spares and FAT | Enables commissioning and maintainability. |
Advantages
| Advantage | Practical Benefit | Boundary Condition |
|---|---|---|
| Local electromagnetic heating | Power couples directly to the load or susceptor | Efficiency depends on load, coil, lining and operating schedule. |
| Electric heating without burner combustion at the furnace | Eliminates on-site furnace fuel combustion products | Upstream electricity emissions and metal fumes still matter. |
| Repeatable inverter power control | Supports consistent operator recipes | Requires reliable sensing and an approved process window. |
| Compact furnace design | Can reduce equipment footprint for a specified batch size | Allow clearance for utilities, lifting, ventilation and pouring. |
| Compatibility with automated foundries | Potential PLC/HMI and batch data integration | Specify interfaces and testing as optional project scope. |
| Reduced fuel handling | No burner fuel needed for melting energy | Water-cooled electrical infrastructure needs skilled upkeep. |
For custom industrial configurations beyond the three nominal JLRRL sizes, compare HLQ industrial induction furnace systems with independently specified melting-duty targets.
Limitations
| Limitation | What It Means | Mitigation |
|---|---|---|
| Aluminum is a nonferromagnetic conductor | Coupling differs from ferrous charges | Verify crucible/susceptor choice and matching by trial. |
| High crucible filling ratios in published geometry screen | Nominal kg may not provide adequate working freeboard | Insist on certified safe working volume and fill line. |
| Energy-saving percentages not supported by controlled test details | 20-40% saving claims on source page cannot be generalized | Compare measured net kWh/kg at equal alloy, yield and duty. |
| Frequency and input data missing | Difficult to validate electrical integration | Request complete electrical and cooling schedules. |
| Oxidation, dross and hydrogen | Induction heating does not replace melt treatment | Use validated degassing, skimming and chemistry controls. |
| Water/molten-metal contact hazard | Wet charge or leaks can cause violent explosions | Dry materials, inspected cooling and robust guarding/interlocks. |
| Continuous 24-hour use depends on utilities | High duty increases thermal/mechanical load | Design cooling and preventive maintenance for the actual cycle. |
Why Choose HLQ Induction Equipment?
HLQ Induction Equipment Co., Ltd. publishes a JLRRL aluminum-furnace series and a wider range of induction heating equipment. The strongest reason to shortlist a vendor is not an unsubstantiated “best manufacturer” claim; it is the ability to turn a casting requirement into drawings, a complete utility schedule, a reproducible melt trial and long-term spare-parts support.
| Document / Test | What Must Be Stated | Buyer Benefit |
|---|---|---|
| Model data sheet | Capacity, rated power basis, frequency, input V/A/kVA | Comparable technical quotations. |
| Thermal and production test | Charge, initial state, poured kg/h and metered kWh | Real performance under specified conditions. |
| Furnace / crucible GA drawing | Usable volume, freeboard, shell and handling clearances | Validates charge and factory layout. |
| Water/electrical P&ID | Cooling circuit, alarms, sensor list, interlocks | Reliable and safe site integration. |
| Control description | PID sensor point, PLC options, interfaces and alarms | Clear automation scope. |
| After-sales plan | Lining/coil spares, maintenance, warranty and response terms | Lifecycle risk control. |
For safer handling of recurring foundry pours, ask about a tilting induction melting furnace configuration and compare the full transfer system, not just furnace heating power.

Core FAQs
1. What capacities are available in the JLRRL aluminum furnace series?
The target page lists 150 kg, 300 kg and 500 kg nominal batch models. Effective safe molten capacity must be confirmed by the actual crucible lining and maximum fill height.
2. What powers are published for JLRRL-150, JLRRL-300 and JLRRL-500?
The page lists 30 kW, 60 kW and 70 kW. It does not make the input-versus-output basis sufficiently clear for final utility sizing.
3. What are the stated aluminum melting rates?
The nominal values are 65 kg/h, 130 kg/h and 170 kg/h, respectively. Ask for measured rates at the intended alloy, pour temperature and start condition.
4. What induction frequency does the furnace use?
The numerical output frequency is not given for these three JLRRL models. The correct kHz depends on coil, inverter and load; obtain the exact OEM specification.
5. Can the 500 kg model melt 500 kg every hour?
No such rate is published. It has a 500 kg batch label but a stated 170 kg/h melting rate. These terms describe different performance measures.
6. How much electricity does it take to melt 1 kg of aluminum?
Pure aluminum has a theoretical minimum near 0.30 kWh/kg from room temperature to melting, excluding furnace losses and superheat. Real metered kWh/kg varies with furnace, scrap, production rhythm and yield; the target JLRRL page does not publish verified values.
7. Can an induction aluminum furnace melt beverage cans?
Potentially, after a properly engineered pretreatment and charging process. Thin coated cans bring oxidation, emissions, contamination and metal-yield challenges. Never introduce wet or sealed feedstock.
8. Is 850°C the correct operating temperature?
No. 850°C is the published machine maximum. Most aluminum melting and pouring operations use lower alloy-specific targets. Avoid unnecessary superheat.
9. Does induction melting remove hydrogen or guarantee casting quality?
No. Melt quality can require chemistry checks, degassing, filtration, oxide control and proper temperature management. Furnace heating alone is not a complete melt-treatment process.
10. Does it need cooling water and safety interlocks?
Yes. Water-cooled induction equipment requires an approved cooling circuit, flow and temperature protections, and leak/risk assessment near molten metal.
11. Which model should I select for 250 kg/h production?
None of the three published JLRRL models individually lists 250 kg/h. Seek a larger-power or parallel-furnace proposal based on measured throughput and energy intensity.
Aluminium Scraps Recycling Melting Process
SMJD induction melting furnace parameter
Aluminum,Copper,Iron Induction Melting Furnace manual
aluminum-melting-furnace-guide