15 Key FAQs on Induction Hardening Machines You Need to Know
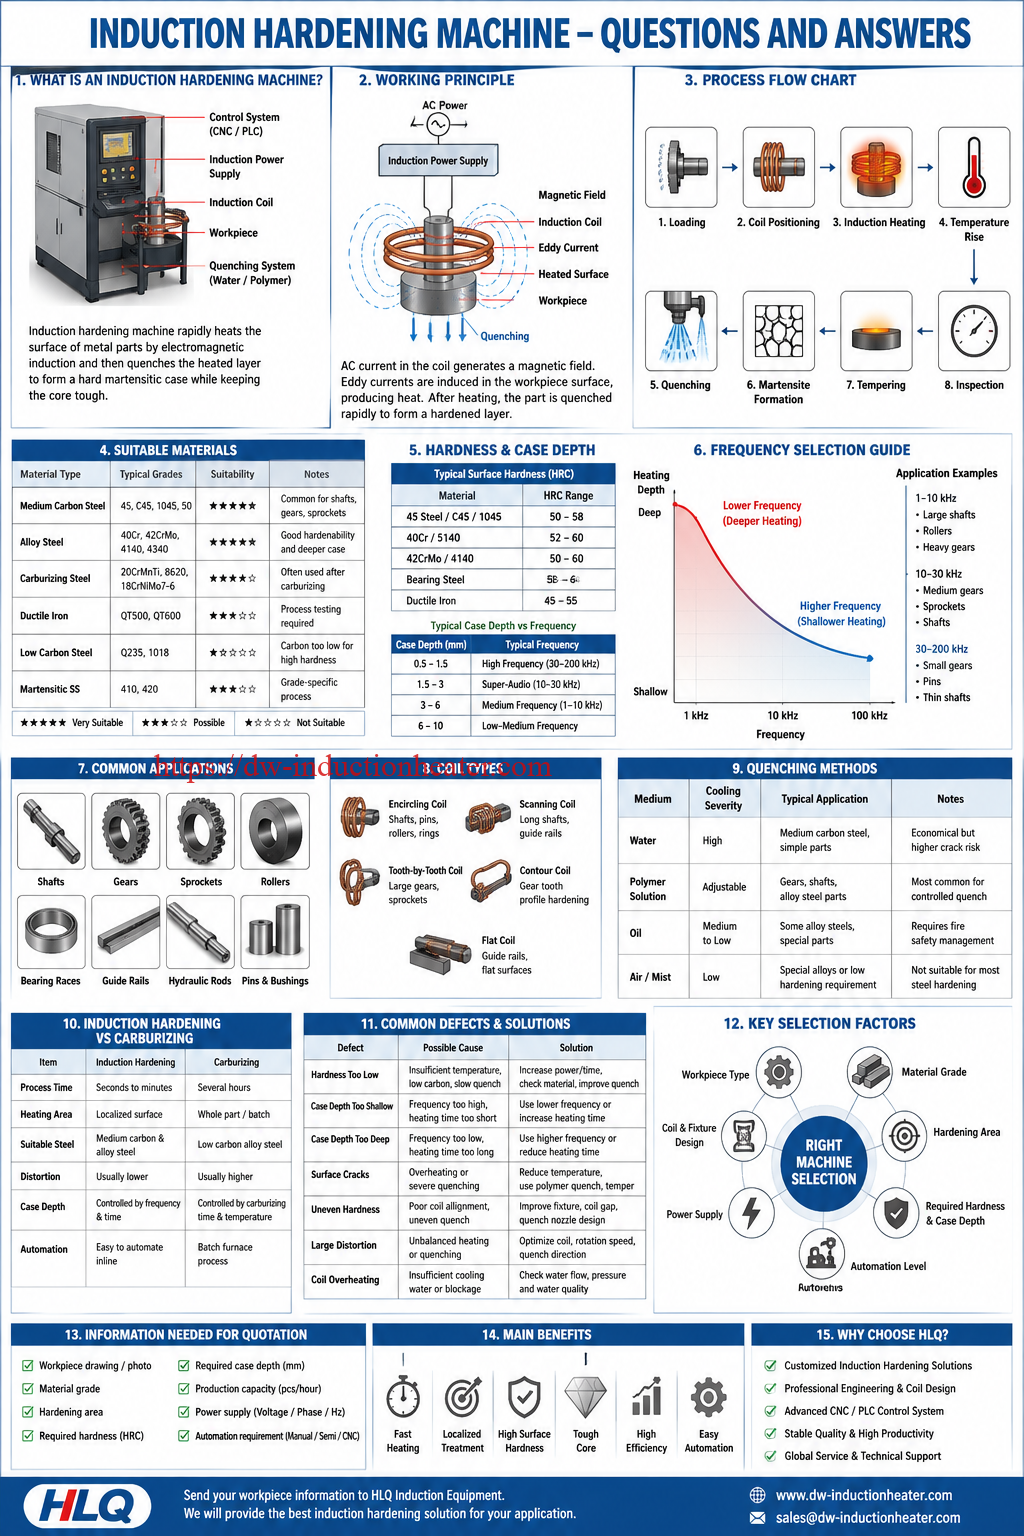
An induction hardening machine is an industrial heat treatment system used to harden the surface of steel parts such as shafts, gears, sprockets, pins, rollers, bearing races, guide rails and hydraulic rods. It rapidly heats the surface by electromagnetic induction and then quenches the heated layer to create a hard martensitic case while keeping the core tough. This FAQ guide explains working principle, suitable materials, hardness range, case depth, frequency selection, coil design, quenching methods, common defects and machine selection. It is written for engineers, buyers, production managers and maintenance teams who need reliable surface hardening equipment.
Table of Contents
- Quick Answer
- 1. What Is an Induction Hardening Machine?
- 2. How Does an Induction Hardening Machine Work?
- 3. What Parts Can Be Processed by Induction Hardening?
- 4. What Materials Are Suitable for Induction Hardening?
- 5. What Hardness Can Induction Hardening Achieve?
- 6. What Is the Typical Induction Hardening Depth?
- 7. How to Choose Frequency for Induction Hardening?
- 8. What Is the Difference Between High Frequency and Medium Frequency Induction Hardening?
- 9. What Is the Difference Between Induction Hardening and Carburizing?
- 10. How to Choose an Induction Hardening Machine?
- 11. What Coil Is Used for Induction Hardening?
- 12. What Quenching Medium Is Used?
- 13. Why Do Induction Hardened Parts Crack?
- 14. What Are the Advantages of Induction Hardening?
- 15. What Information Is Needed for a Quotation?
- Why Choose HLQ Induction Equipment?
Quick Answer
An induction hardening machine is a surface heat treatment system that uses electromagnetic induction to heat only the required surface area of a metal part, followed by rapid quenching to form a hardened layer. It is best used for medium carbon steel, alloy steel and some cast iron parts that require high surface hardness, wear resistance and fatigue strength while maintaining a tough core. Common applications include shafts, gears, sprockets, rollers, pins, bearing rings, guide rails and automotive or machinery transmission components.
1. What Is an Induction Hardening Machine?
An induction hardening machine is a specialized heat treatment machine used to increase the surface hardness of metal components. The system usually includes an induction power supply, transformer, induction coil, CNC or PLC motion system, quenching device, cooling water system, machine bed, control cabinet and safety protection system.
Unlike furnace hardening, which heats the entire part, induction hardening heats only the selected area. This localized heating reduces distortion, shortens cycle time and improves production efficiency. The process is widely used when a part needs a hard wear-resistant surface but still needs a tough, impact-resistant core.
| Main Component | Function | Engineering Importance |
|---|---|---|
| Induction power supply | Generates high-frequency or medium-frequency current | Determines heating power, frequency and process stability |
| Induction coil | Creates electromagnetic field around the workpiece | Determines heating pattern and energy efficiency |
| Quenching system | Rapidly cools the heated surface | Controls hardness, case depth and crack risk |
| CNC/PLC control | Controls movement, power, time and recipes | Ensures repeatability in production |
| Cooling water system | Cools coil, power supply and transformer | Protects the equipment from overheating |
2. How Does an Induction Hardening Machine Work?
The machine works by passing alternating current through a copper induction coil. This produces a rapidly changing magnetic field. When a steel part is placed inside or near the coil, eddy currents are induced in the surface layer of the workpiece. These eddy currents generate heat due to electrical resistance. After the surface reaches the required hardening temperature, the part is immediately quenched by water, polymer solution or oil.
The rapid cooling transforms the heated surface into martensite, which is much harder than the original structure. The core is not fully heated, so it remains tougher and more ductile.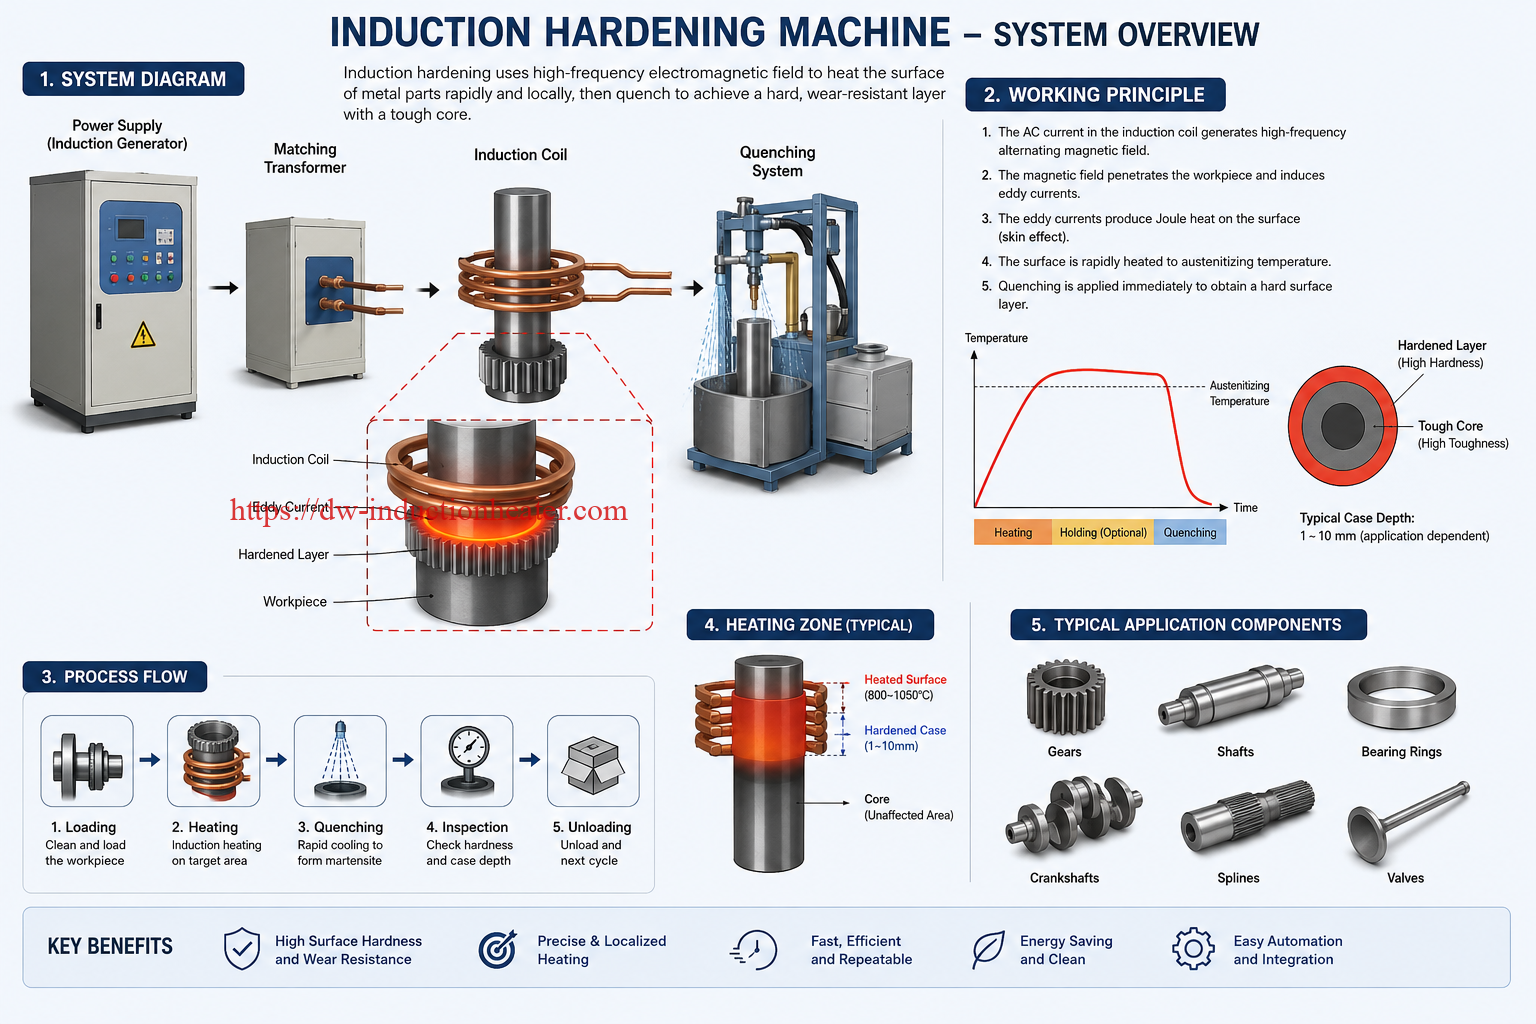
Induction Hardening Process Flow Chart
Workpiece Loading → Coil Positioning → Induction Heating → Temperature Rise → Immediate Quenching → Martensite Formation → Tempering → Hardness Inspection → Case Depth Inspection → Final Approval
| Process Stage | What Happens | Key Control Parameter |
|---|---|---|
| Loading | Part is clamped on fixture or machine spindle | Alignment, runout, clamping force |
| Heating | Surface is heated by induced current | Power, frequency, coil gap, heating time |
| Quenching | Heated layer is rapidly cooled | Flow rate, pressure, medium concentration |
| Tempering | Brittleness is reduced after hardening | Temperature and holding time |
| Inspection | Hardness and case depth are checked | HRC, ECD, microstructure, cracks |
3. What Parts Can Be Processed by Induction Hardening?
Induction hardening is suitable for components that experience friction, wear, contact stress, rolling load, sliding load or repeated impact. It is especially useful for rotating or transmission parts.
| Workpiece | Typical Hardening Area | Common Industry |
|---|---|---|
| Shafts | Outer surface, journals, spline areas | Automotive, machinery, hydraulic systems |
| Gears | Tooth flank, tooth root, tooth tip | Gearbox, reducer, mining machinery |
| Sprockets | Tooth profile and working surface | Chain transmission, agricultural machinery |
| Rollers | Outer cylindrical surface | Steel mills, conveyors, printing machinery |
| Bearing races | Raceway surface | Bearing manufacturing |
| Guide rails | Sliding surface | Machine tools and linear motion systems |
| Hydraulic rods | Outer surface | Hydraulic cylinders and construction machinery |
| Pins and bushings | Contact and wear surface | Excavators, loaders, agricultural equipment |
4. What Materials Are Suitable for Induction Hardening?
The best materials for induction hardening are steels with enough carbon to form martensite after quenching. Medium carbon steels and alloy steels are the most common choices. Low carbon steels usually need carburizing or carbon enrichment before they can be hardened effectively.
| Material Type | Typical Grades | Suitability | Notes |
|---|---|---|---|
| Medium carbon steel | 45 steel, C45, 1045, 50 steel | Very suitable | Common for shafts, gears and sprockets |
| Alloy steel | 40Cr, 42CrMo, 4140, 4340 | Very suitable | Good hardenability and deeper case depth |
| Carburizing steel | 20CrMnTi, 8620, 18CrNiMo7-6 | Conditionally suitable | Often used after carburizing or for special gear processes |
| Ductile iron | QT500, QT600, nodular cast iron | Possible | Requires process testing to avoid cracking |
| Low carbon steel | Q235, 1018, mild steel | Not ideal directly | Carbon content is usually too low for high hardness |
| Martensitic stainless steel | 410, 420 and similar grades | Special application | Requires grade-specific process design |
5. What Hardness Can Induction Hardening Achieve?
The final hardness depends on material grade, carbon content, heating temperature, quenching speed and tempering process. For many medium carbon and alloy steels, induction hardening can typically achieve about HRC 50–62 on the surface. Higher hardness may be possible for some high-carbon steels, but crack risk also increases.
| Material | Typical Surface Hardness After Induction Hardening | Common Application |
|---|---|---|
| 45 steel / C45 / 1045 | HRC 50–58 | Shafts, sprockets, pins |
| 40Cr / 5140 | HRC 52–60 | Gears, shafts, transmission parts |
| 42CrMo / 4140 | HRC 50–60 | Heavy-duty shafts, rollers, gears |
| Bearing steel | HRC 58–64 | Bearing races and precision parts |
| Ductile iron | HRC 45–55 | Rollers, guide parts, wear surfaces |
6. What Is the Typical Induction Hardening Depth?
Induction hardening depth, also called case depth or effective hardened depth, depends mainly on frequency, power density, heating time, material and quenching condition. Higher frequency produces shallower heating, while lower frequency provides deeper heating.
| Required Case Depth | Typical Frequency Range | Typical Workpieces |
|---|---|---|
| 0.5–1.5 mm | High frequency | Small pins, small shafts, light gears |
| 1.5–3 mm | Super-audio frequency | Medium gears, sprockets, shafts |
| 3–6 mm | Medium frequency | Large shafts, rollers, heavy gears |
| 6–10 mm | Low-medium frequency | Large rollers, mining parts, large shafts |
7. How to Choose Frequency for Induction Hardening?
Frequency selection is one of the most important decisions in induction hardening. It affects heating depth, energy distribution and final case depth. As a general rule, shallow hardening requires higher frequency, while deeper hardening requires lower frequency.
| Frequency Type | Typical Range | Heating Characteristic | Best Application |
|---|---|---|---|
| High frequency | 30–200 kHz | Shallow surface heating | Small gears, pins, thin shafts, precision parts |
| Super-audio frequency | 10–30 kHz | Medium surface depth | Medium shafts, gears, sprockets |
| Medium frequency | 1–10 kHz | Deeper heating penetration | Large shafts, rollers, heavy-duty gears |
| Dual frequency | Combination of low and high frequency | Improves contour heating | Gear tooth flank and root hardening |
 8. What Is the Difference Between High Frequency and Medium Frequency Induction Hardening?
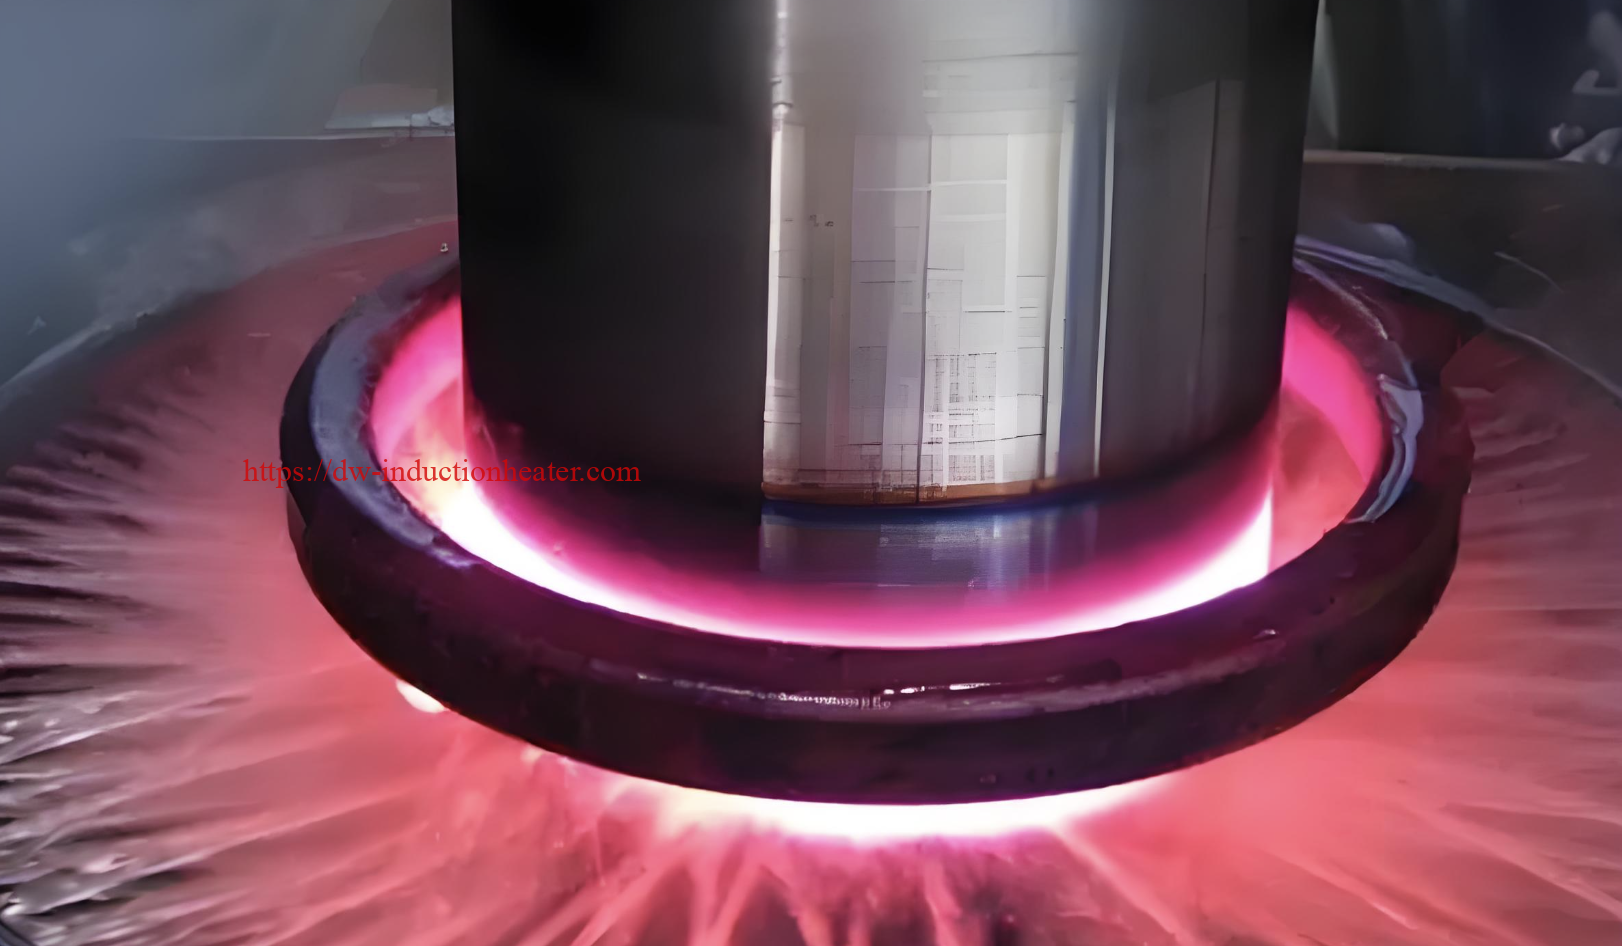
High frequency induction hardening concentrates heat near the surface and is suitable for smaller parts or shallow hardening. Medium frequency induction hardening provides deeper heat penetration and is better for larger parts and deeper case depth.
| Item | High Frequency Induction Hardening | Medium Frequency Induction Hardening |
|---|---|---|
| Heating depth | Shallow | Deeper |
| Typical frequency | 30–200 kHz | 1–10 kHz |
| Best for | Small parts, thin surface layer, precision components | Large shafts, rollers, heavy gears, deep case depth |
| Power requirement | Lower to medium | Medium to high |
| Common machine type | High frequency hardening machine | Medium frequency hardening machine |
9. What Is the Difference Between Induction Hardening and Carburizing?
Induction hardening directly heats and quenches the surface of a steel part. It requires enough carbon in the base material to form martensite. Carburizing adds carbon to the surface of low-carbon steel before quenching. Induction hardening is faster and more localized, while carburizing is suitable for low-carbon alloy steels that need a carbon-rich case.
| Comparison Item | Induction Hardening | Carburizing |
|---|---|---|
| Process time | Seconds to minutes | Several hours |
| Heating area | Localized surface area | Whole part or batch |
| Suitable steel | Medium carbon and alloy steel | Low carbon alloy steel |
| Distortion | Usually lower | Usually higher |
| Case depth | Controlled by frequency and heating time | Controlled by carburizing time and temperature |
| Production mode | Easy to automate inline | Batch furnace process |
10. How to Choose an Induction Hardening Machine?
To choose the right induction hardening machine, the buyer must define the workpiece, material, hardened area, required hardness, required case depth, production quantity and automation level. The machine should not be selected by power alone. Coil design, fixture accuracy and quenching system are equally important.
| Selection Factor | Why It Matters | Example |
|---|---|---|
| Workpiece type | Determines machine structure and fixture | Shaft, gear, roller, sprocket, bearing ring |
| Material grade | Determines hardenability and crack risk | 45 steel, 40Cr, 42CrMo, 4140 |
| Hardening area | Determines coil design | Outer surface, tooth, spline, raceway |
| Required hardness | Determines heating and quenching process | HRC 50–60 |
| Required case depth | Determines frequency selection | 1.5 mm, 3 mm, 5 mm |
| Production capacity | Determines automation level | 10 pcs/hour, 100 pcs/hour |
| Available power supply | Determines electrical design | 380V, 415V, 440V, 480V, 3 phase |
11. What Coil Is Used for Induction Hardening?
The induction coil is designed according to workpiece shape and hardening area. A shaft may use an encircling coil. A gear may use an encircling coil, tooth-by-tooth inductor or contour coil. A flat guide rail may use a scanning coil. Coil design directly affects heating uniformity, case depth and energy efficiency.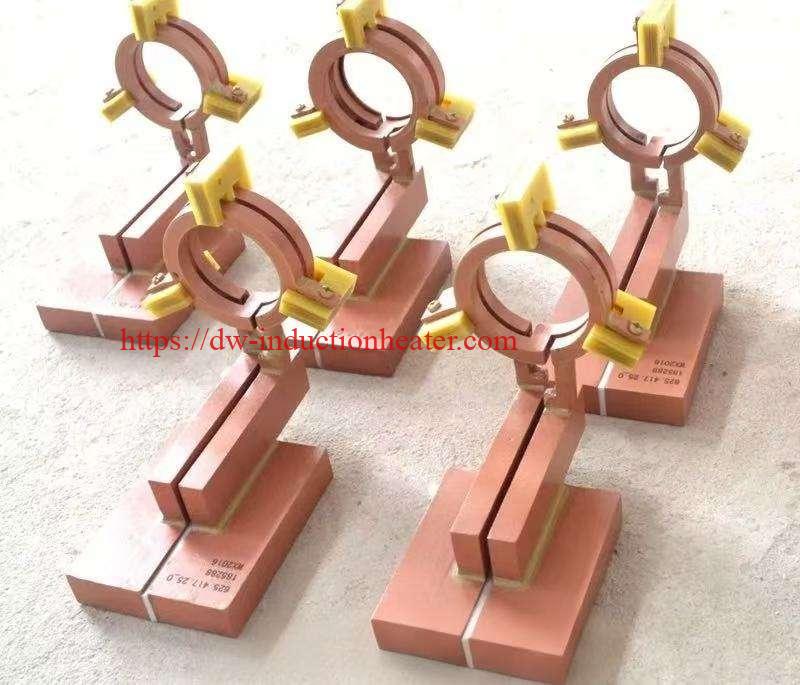
| Coil Type | Best Application | Design Notes |
|---|---|---|
| Encircling coil | Shafts, pins, rollers, rings | Uniform heating around cylindrical parts |
| Scanning coil | Long shafts, guide rails, hydraulic rods | Moves along the hardening length |
| Tooth-by-tooth coil | Large gears and sprockets | Heats one tooth or tooth gap at a time |
| Contour coil | Gear tooth profile hardening | Designed to follow tooth flank and root area |
| Flat coil | Guide rails and flat surfaces | Used for local surface hardening |
12. What Quenching Medium Is Used?
The quenching medium must cool the heated surface fast enough to form martensite but not so aggressively that it causes cracks. Water is fast and economical, while polymer solution gives adjustable cooling severity. Oil may be used for some crack-sensitive materials but is less common in modern automated induction hardening systems.
| Quenching Medium | Cooling Severity | Typical Application | Notes |
|---|---|---|---|
| Water | High | Medium carbon steel, simple parts | Economical but higher crack risk |
| Polymer solution | Adjustable | Gears, shafts, alloy steel parts | Common for controlled quenching |
| Oil | Medium to low | Some alloy steels and special parts | Requires fire safety management |
| Air or mist | Low | Special alloys or low hardening requirement | Not suitable for most steel hardening |
13. Why Do Induction Hardened Parts Crack?
Cracking is usually caused by excessive thermal stress, overly severe quenching, overheating, unsuitable steel composition, sharp corners, poor part design or incorrect process parameters. Gear roots, keyways, shoulders and sharp transitions are common crack-sensitive areas.
| Crack Cause | Typical Symptom | Engineering Solution |
|---|---|---|
| Overheating | Coarse grain, burned surface, brittle layer | Reduce power or heating time; improve temperature control |
| Severe quenching | Surface cracks after cooling | Use polymer quench and reduce cooling severity |
| Sharp corners | Cracks at keyway, root or shoulder | Improve fillet radius and optimize coil position |
| Wrong material | Unstable hardness or cracks | Confirm steel grade and prior heat treatment |
| Uneven heating | Local cracks and distortion | Improve coil design and fixture alignment |
14. What Are the Advantages of Induction Hardening?
Induction hardening provides fast cycle time, localized heating, good energy efficiency, lower distortion, high repeatability and easy automation. It is especially valuable for mass production of gears, shafts, rollers and transmission components.
| Advantage | Engineering Meaning | Buyer Benefit |
|---|---|---|
| Fast heating | Surface reaches hardening temperature within seconds | Higher productivity |
| Localized treatment | Only the required area is heated | Lower distortion and less energy waste |
| High hardness | Martensitic surface layer is formed | Better wear resistance |
| Tough core | Core is not fully hardened | Better impact resistance |
| Easy automation | CNC/PLC controls process recipe | Stable quality and lower labor cost |
| Clean process | No open flame or furnace atmosphere for many applications | Better workshop environment |
| Repeatability | Power, time, movement and quench are controlled | Consistent batch quality |
15. What Information Is Needed for an Induction Hardening Machine Quotation?
For an accurate quotation, the supplier needs enough technical information to select power, frequency, coil type, machine structure, quenching system and automation level. A drawing or photo of the workpiece is strongly recommended.
| Required Information | Example | Why It Is Needed |
|---|---|---|
| Workpiece name | Gear, shaft, roller, sprocket, bearing ring | Determines machine type |
| Material grade | 45 steel, 40Cr, 42CrMo, 4140 | Determines hardness and quenching process |
| Drawing or dimensions | Diameter, length, tooth module, width | Determines coil and fixture design |
| Hardening area | Surface, tooth, spline, journal, raceway | Determines heating pattern |
| Required hardness | HRC 50–60 | Determines process target |
| Required case depth | 1.5 mm, 3 mm, 5 mm | Determines frequency selection |
| Production capacity | Pieces per hour or pieces per day | Determines automation level |
| Power supply | 380V / 415V / 440V / 480V, 3 phase | Determines electrical design |
| Automation requirement | Manual, semi-automatic, CNC automatic | Determines machine configuration |
Common Problems and Solutions for Induction Hardening Machines
| Problem | Possible Cause | Solution |
|---|---|---|
| Hardness is too low | Insufficient temperature, low carbon material, slow quenching | Increase power or time; check material; improve quench flow |
| Case depth is too shallow | Frequency too high or heating time too short | Use lower frequency or increase heating time |
| Case depth is too deep | Frequency too low or heating time too long | Use higher frequency or reduce heating time |
| Surface cracks | Overheating or severe quenching | Reduce temperature, use polymer quench and temper after hardening |
| Uneven hardness | Poor coil alignment, runout or uneven spray | Improve fixture, coil gap and quench nozzle design |
| Large distortion | Unbalanced heating or quenching | Optimize coil, rotation speed and quench direction |
| Coil overheating | Insufficient cooling water or scale blockage | Check water flow, pressure and water quality |
Recommended Model Selection Table
| Application | Material | Recommended Power | Frequency | Machine Type |
|---|---|---|---|---|
| Small pin hardening | 45 steel, 40Cr | 30–80 kW | 30–100 kHz | High frequency hardening machine |
| Small gear hardening | 1045, 40Cr, 4140 | 50–150 kW | 20–80 kHz | Gear hardening machine |
| Shaft surface hardening | 45 steel, 40Cr, 42CrMo | 80–300 kW | 5–30 kHz | CNC shaft hardening scanner |
| Large roller hardening | 42CrMo, 4140, alloy steel | 200–600 kW | 1–10 kHz | Medium frequency hardening machine |
| Bearing race hardening | Bearing steel | 100–400 kW | 5–50 kHz | Rotary hardening machine |
| Large gear tooth hardening | 42CrMo, 34CrNiMo6 | 160–800 kW | 1–15 kHz | Tooth-by-tooth gear hardening machine |
Why Choose HLQ Induction Equipment?
HLQ Induction Equipment provides engineering-oriented induction hardening machines for shafts, gears, sprockets, pins, rollers, bearing races, guide rails and customized metal parts. Instead of only recommending machine power, HLQ helps customers evaluate the complete hardening process, including material grade, case depth, hardness target, frequency selection, coil design, fixture structure, quenching method, cooling system and automation level.
| HLQ Capability | Customer Value |
|---|---|
| Customized induction hardening machine design | Machine structure can match shafts, gears, rollers, sprockets and special parts |
| Power and frequency selection | Helps achieve correct case depth and heating efficiency |
| Induction coil engineering | Improves heating uniformity and hardening quality |
| CNC/PLC control system | Supports repeatable production and recipe management |
| Integrated quenching system | Controls hardness, distortion and crack risk |
| Engineering support | Helps customers optimize heating time, quenching and inspection process |
Conclusion
An induction hardening machine is one of the most efficient solutions for improving the surface hardness, wear resistance and service life of steel components. It is especially suitable for gears, shafts, sprockets, rollers, pins, guide rails and bearing races. To select the correct machine, buyers should consider material, part size, required hardness, case depth, production capacity, coil design, quenching system and automation requirements. For best results, the induction hardening machine should be designed as a complete process system, not only as a power supply.