Continuous induction billet heating systems have become the backbone of modern forging, rolling, and extrusion lines worldwide. As industries rebuild infrastructure and push toward Industry 4.0 and carbon-neutral manufacturing, these systems are increasingly replacing legacy gas-fired furnaces — delivering faster cycle times, tighter temperature tolerances, and dramatically lower operational emissions.
Yet despite their widespread adoption, many engineers and procurement teams still have fundamental questions about how these systems work, what they cost to run, and how to specify them correctly. This guide answers the 10 most important questions with authoritative, practical detail.
What Exactly Is a Continuous Induction Billet Heating System?
A continuous induction billet heating system is an industrial installation that heats cylindrical or rectangular metal billets — one after another in an uninterrupted flow — to the precise temperature required for downstream forming operations such as forging, hot rolling, or extrusion.
Unlike batch furnaces that load and heat a fixed charge of material, a continuous system passes individual billets through one or more induction coils at a controlled feed rate. Heat is generated inside the billet itself via electromagnetic induction, not transferred from an external flame or radiant element. The result is rapid, uniform heating with virtually no idle time between pieces.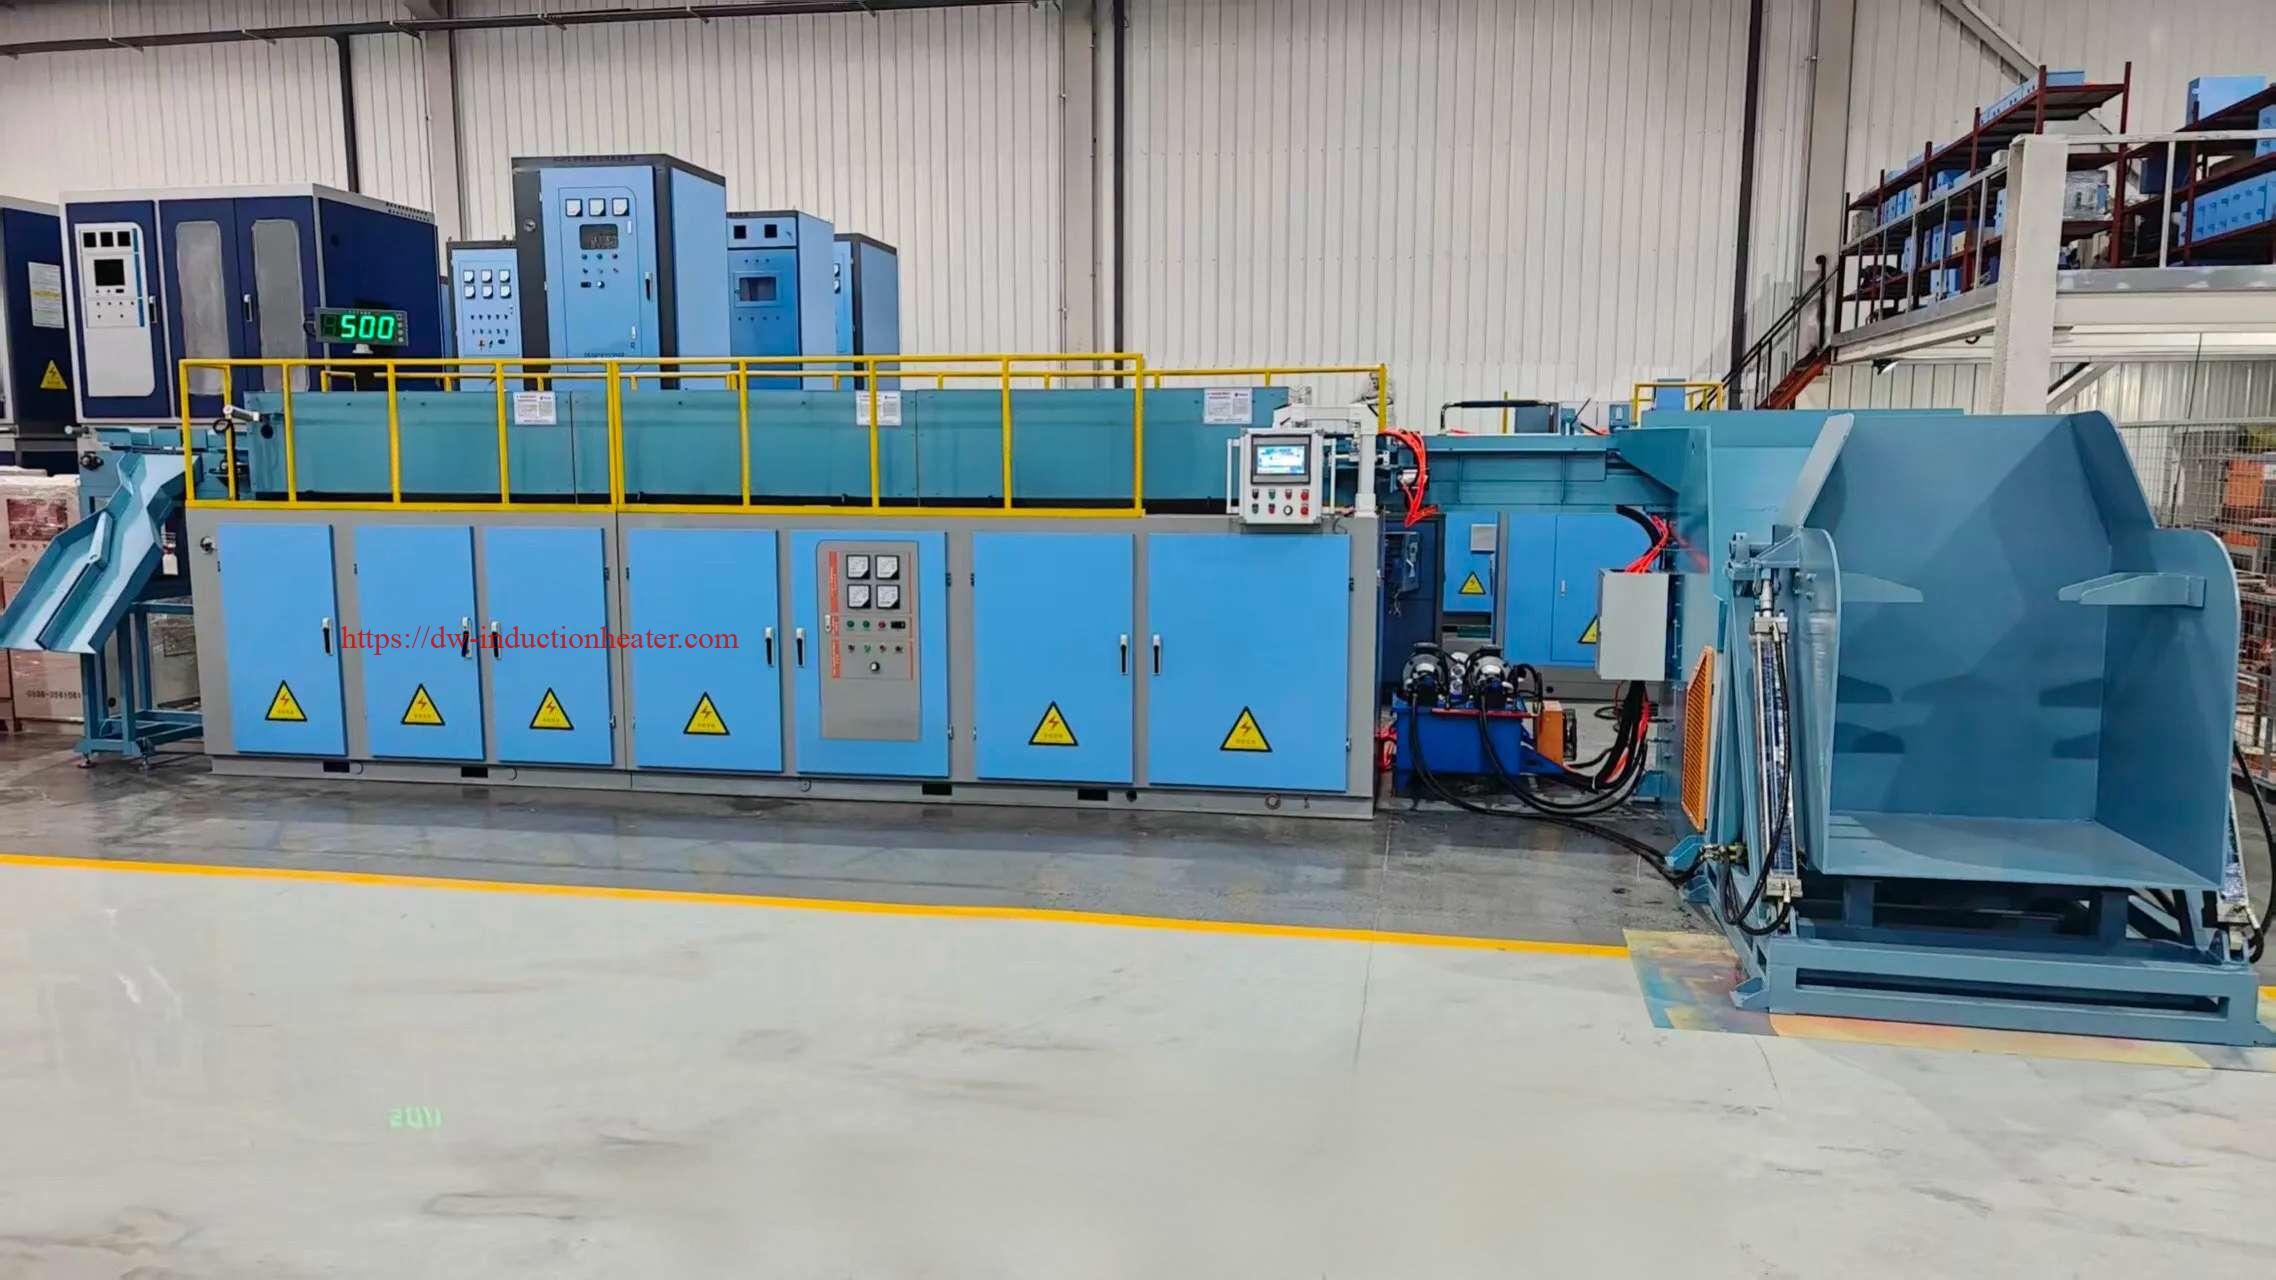
A complete system integrates five core subsystems: the power supply (IGBT-based solid-state inverter), the induction coil assembly, an automated material handling train (feeders, tractor drives, extractors), a temperature monitoring system, and a supervisory control platform (PLC/HMI).
How Does Electromagnetic Induction Actually Heat a Metal Billet?
The operating principle is Faraday’s law of electromagnetic induction, applied at industrial scale. When alternating current flows through the copper induction coil that surrounds the billet, it creates a rapidly changing magnetic field. This field penetrates the billet and induces circulating electrical currents — called eddy currents — within the metal.
Those eddy currents encounter the metal’s electrical resistance and, according to Joule’s law (W = I²·R·t), generate heat directly inside the billet’s cross-section. There is no combustion, no open flame, and no contact between the coil and the workpiece.

In a multi-coil continuous system, the billet passes through a staged heating sequence: the first coil(s) drive rapid bulk heat input, while the final coil(s) act as a soak zone, equalizing the temperature gradient between surface and core before the billet exits the line.
This physics-driven process delivers heating uniformity from surface to core and head to tail — a critical metallurgical requirement that determines the quality of the forged or rolled output.
Which Metals and Billet Sizes Can Be Processed?
Continuous induction billet heating systems are engineered to process a wide range of ferrous and non-ferrous metals. The determining factors are electrical conductivity, magnetic permeability, and the target forging or rolling temperature.
| Material | Typical Target Temp. | Frequency Range | Key Application |
|---|---|---|---|
| Carbon & Alloy Steel | 1,100–1,250 °C | 250–1,000 Hz | Forging, hot rolling |
| Stainless Steel | 1,150–1,250 °C | 250–1,000 Hz | Valve stems, fittings |
| Aluminum | 450–520 °C | 1,000–3,000 Hz | Extrusion billets |
| Copper & Brass | 750–900 °C | 1,000–10,000 Hz | Tube forming |
| Titanium | 900–1,050 °C | 500–2,000 Hz | Aerospace components |
In terms of geometry, most commercial systems handle round billets from 20 mm to 350 mm in diameter and lengths from 50 mm to several meters. Modular coil designs allow a single line to be re-tooled for different diameters with minimal downtime. Advanced systems support both square and round cross-sections within the same line.
What Power Output and Frequency Does the System Require?
Power and frequency are the two most critical specification variables, and they are determined by your material, billet geometry, and required throughput rate — not by convenience or cost alone.
(small billet lines)
(heavy mill lines)
to 1,200 °C / hr
As a practical rule of thumb: 1 kW of installed capacity can heat approximately 3 kg of steel to 1,200 °C per hour. For a line processing 10 tonnes/hour of steel billets, you would need roughly 3.3 MW of installed power — typically with a 20–30% safety margin added for startup loads and material variation.
Frequency selection follows the physics of skin depth penetration:
- 250–1,000 Hz: Large-diameter billets (steel, titanium) — ensures core-to-surface heating uniformity
- 1,000–3,000 Hz: Medium billets, aluminum extrusion
- 3,000–50,000 Hz: Small billets, high-conductivity metals, surface heating


Modern systems use IGBT (Insulated Gate Bipolar Transistor) solid-state inverters, which offer precise frequency control, high power factor, and significantly better efficiency than older thyristor-based designs.
How Is Temperature Controlled and Monitored Throughout the Process?
Precise temperature control is arguably the defining advantage of induction over gas heating. Modern continuous systems implement a multi-layer temperature management architecture that operates in real time, billet by billet.
Primary measurement is performed by non-contact infrared pyrometers or two-color ratio pyrometers positioned at the exit of each coil zone and at the final discharge point. These read the billet surface temperature with ±3–5 °C accuracy at production speeds.
Advanced control platforms such as Interpower Induction’s Forge-Link™ and similar HMI-based systems allow operators to enter billet parameters (diameter, length, feed rate, target temperature) directly, after which the system automatically computes the optimal power distribution across coil zones and dynamically compensates for process variations in real time — no offline programming required.
This closed-loop architecture achieves consistent exit temperatures across an entire production run, regardless of variations in incoming billet temperature, material grade, or ambient conditions.
How Energy-Efficient Is Induction Compared to Gas-Fired Furnaces?
Energy efficiency is one of the strongest arguments for continuous induction heating, and the difference versus conventional gas furnaces is substantial:
| Parameter | Gas Furnace | Induction System |
|---|---|---|
| Thermal efficiency | 30–45% | 55–75% |
| Idle energy consumption | High (continuous burn) | Near zero (power off = no draw) |
| Startup time to production temp. | 60–120 minutes | Under 5 minutes |
| Scale/oxidation loss | 1.5–3% of billet weight | 0.3–0.8% |
| CO₂ emissions | High (direct combustion) | Zero direct emissions |
A critical advantage is zero idle consumption: an induction system draws virtually no power when no billet is present in the coil. Gas furnaces, by contrast, must maintain operating temperature continuously, burning fuel around the clock even during shift changes, maintenance windows, or production gaps.
Reduced oxidation scale is another major economic benefit. A steel billet losing 2% to scale in a gas furnace at 10 tonnes/hour is losing 200 kg/hour of finished metal to waste. Induction’s lower oxidation translates directly into higher material yield and reduced downstream descaling costs.
What Automation Features Are Available for Continuous Lines?
Automation is where modern continuous induction heating systems differentiate most sharply from older technology. Today’s lines can be fully unmanned for extended production runs, addressing critical challenges such as labor shortages, quality compliance, and throughput optimization.
Infeed automation options include bin tippers, step feeders, vibratory conveyors, rotary feeders, billet descramblers, gantry de-stackers, and robotic arm loaders — all designed to accept a large volume of randomly oriented billets and present them in a precisely aligned, single-file orientation at the coil entrance.
Through-coil drive systems range from pinch-roll units (for simple applications) to “cat-track” tractor drives that maintain continuous contact over a longer billet length. Cat-track systems offer a critical advantage: their extended contact surface bridges the gap created by “tong holds” (handling tabs welded to billet ends), allowing uninterrupted continuous feed even with these attachments present.
At the outfeed, pyrometer-linked sorting gates automatically divert accepted billets to the press and reject out-of-specification billets to a separate channel. Full integration with the downstream forging press or rolling mill via PLC handshake signals completes the automation loop.
What Are the Key Maintenance Requirements and Expected Service Life?
Induction billet heating systems are regarded as highly reliable, low-maintenance equipment compared to gas furnaces — there are no burners, refractory linings, or combustion controls to service. However, a structured preventive maintenance program is essential to sustain peak performance.
Cooling water system: This is the most critical maintenance circuit. The induction coil and power electronics are water-cooled, and the cooling loop must maintain flow rate, pressure, and water quality (conductivity, pH, temperature) within specified limits. Monthly checks on flow sensors, conductivity monitors, and heat exchanger performance are recommended.
Induction coil inspection: Coil liners (refractory or ceramic) should be inspected at scheduled intervals for cracking or spalling. Coil copper integrity and connection tightness should be checked at each planned maintenance window.
Power electronics: IGBT modules, capacitor banks, and bus connections should be inspected annually for signs of thermal stress, loose connections, or capacitance drift. Built-in fault detection systems will log and alarm on most anomalies before they become failures.
Material handling: Conveyor rollers, feeder mechanisms, and tractor drive belts/tracks are the highest-wear mechanical components and should be inspected monthly with replacement cycles based on throughput volume.
What Safety Standards and Certifications Must the System Meet?
Industrial induction heating systems operate at high power levels and generate significant electromagnetic fields, making compliance with applicable safety standards a non-negotiable procurement requirement.
Electrical safety: Systems must comply with IEC 60519 (safety in electroheat installations) and relevant national electrical codes. All cabinets should be IP-rated for the installation environment.
EMC and EMF: Electromagnetic emissions must comply with regional directives. In the European Union, this means conformance with the EMC Directive (2014/30/EU) and the Low Voltage Directive (2014/35/EU), evidenced by CE marking. In the United States, UL certification is the applicable standard.
Operator protection: Physical barriers, interlocked guarding, and clearly demarcated EMF exclusion zones protect workers from electromagnetic field exposure. Emergency stop (E-stop) circuits must be hardwired and fail-safe, with response times typically under 200 milliseconds.
Cooling water isolation: Because the cooling loop operates at elevated temperatures and pressures, pressure relief valves, flow-loss interlocks, and leakage detection systems are required safety elements that must be commissioned and verified before production startup.
How Do I Select the Right System for My Production Line?
Selecting a continuous induction billet heating system is a systems engineering decision, not simply a power-rating exercise. Work through these parameters in sequence:
| Selection Parameter | Key Questions to Answer |
|---|---|
| Material specification | What alloys will you process? What are the Curie temperatures and resistivity values? |
| Billet geometry range | What diameter range? What min/max lengths? Round, square, or both? |
| Target temperature | What exit temperature is required? What temperature uniformity tolerance (±°C)? |
| Throughput | What is the required kg/hour or pieces/hour at peak production? |
| Downstream integration | What is the press or mill cycle time? What PLC communication protocol is required? |
| Power infrastructure | What is the available grid voltage and short-circuit capacity? Is a dedicated transformer needed? |
| Floor space envelope | What are the maximum system dimensions including material handling? |
| Automation level | Fully automatic, semi-automatic, or operator-loaded? What level of data logging and reporting is required? |
Once parameters are defined, evaluate vendors on reference installations in comparable applications, not just catalog specifications. Request factory acceptance testing (FAT) with your actual billet samples before shipment, and confirm that spare parts — particularly IGBT modules and coil liners — are held in inventory with committed lead times.
Finally, consider total cost of ownership (TCO) over a 10-year horizon: energy consumption at your local electricity tariff, projected maintenance parts cost, and the value of reduced scale loss and improved product yield often deliver a full ROI within 3–5 years versus a gas furnace alternative.
Conclusion
Upgrading to a continuous induction billet heating system is one of the most impactful investments a metalworking facility can make. By offering unmatched speed, energy efficiency, and temperature precision, these systems lower operating costs while elevating product quality.
Ready to optimize your production line? Contact an induction heating specialist today to discuss a custom continuous billet heating solution designed specifically for your throughput and material requirements.